
Feature first published in the July/August 2021 issue of 3D ADEPT Mag. Interviews, roles and examples reflect that period.
Moving from prototyping to series production brings automation to the foreground of many additive manufacturing projects. The challenge extends beyond machine speed to preparation, data exchange and the organisation of work.
Needless to say, automation is a vast topic. In the manufacturing field, where most of the tasks were historically done by hand, automated manufacturing has helped operators to rely on a number of computerized control systems to run equipment in a facility. In an industrial additive manufacturing setting especially, one quickly observes that depending on their needs, facilities can implement automation strategies at various levels of production – no matter what AM technology is harnessed – : software, pre-processing, manufacturing or even post-processing.
This feature focuses on software-enabled automation, its applications and the conditions for deploying it in an additive manufacturing facility.
What drives software automation in additive manufacturing? What are the key stages that are taken into account to advance Additive Manufacturing Software Automation? Where are the current needs/challenges? This article aims to address these questions with examples taken on various types of AM technologies.
Benjamin Schrauwen, then CEO of Oqton, shares his perspective on manufacturers’ needs and software capabilities.
What drives software automation in Additive Manufacturing?
In traditional manufacturing, automation is used to increase efficiency and speed. Not only do machine manufacturers and software developers want to bring those advantages to additive manufacturing, but they need to bring them at a more advanced level in order to justify the use of AM technologies in production. This explains the increasing number of collaborations between machine manufacturers and software developers, software developers and material producers, or even between software companies with various expertise.
Software supports several stages of the production workflow. Distinguishing these roles helps define which tasks to automate and which data are needed.
These functions can be grouped into six areas: design (CAD), candidate-part identification, simulation (CAE), preparation and computer-aided manufacturing (CAM), workflow management, and quality assurance/security. Within workflow management, ERP supports enterprise resource planning, while MES manages and tracks production execution; their roles can complement each other.
Asked which tasks should be prioritised for automation, Schrauwen explains:
“Any manual, repetitive task that is currently performed by manufacturing engineers should and can be automated. This way, we can increase efficiency and productivity while freeing up their time to focus on value-adding work. This is also known as ‘end-to-end automation’ of the workflow.
We see this as very important, for example, dental and polymer AM service providers who produce high quantities of mass customized and personalized parts. Manufacturing Execution Systems (MES) is a big area for automation, too: we believe an intelligent way of scheduling is the way to go. This would be completely automated based on printer, material, and people capacity.”
While it highlights some of the key stages that are currently taken into account to advance software automation strategies, Schrauwen’s explanations also reveal that what currently drives software automation in AM has moved beyond the reach of the software that operates the equipment.
As volumes increase, automating selected tasks can reduce manual handling and repeated data entry. Time and cost savings nevertheless depend on the process, volumes and integration work.
Part repeatability requires control of the whole process. Software contributes alongside materials, machines, inspection and workforce expertise.
Most importantly, as Schrauwen’s notes, “any manual, repetitive task that is currently performed by manufacturing engineers should and can be automated”. This means that, the first step in deciding where one should focus their automation strategy consists in identifying those tasks and assessing the stage that will require an immediate action.
From individual tasks to a connected workflow
Not surprisingly, manual tasks can start way before the manufacturing process itself. They consist in but are not limited to entering data into systems, replying to customer requests, calculating and providing cost estimates or even bringing USB sticks to AM systems to have files 3D printed.
Spreadsheets such as Microsoft Excel can support data analysis, while tools such as Zapier connect compatible applications. These initial automations often focus on individual tasks.
As it requires a combination of manual tasks and simple tools, engineers can still encounter issues when it comes to processing information such as 3D printing requests, file conversions/repair, or project status update.
To address this issue, they often move to “basic or simple automation” and integrate a software tool that can handle multiple steps and applications. In this vein, on the market, one can find AM workflow software that can help engineers to automatically handle ordering, customer requests, rule-based automation for production scheduling, or even distribution of files to specific 3D printers for production.
Broader integration connects production stages and supports visibility, traceability and planning. This digital continuity does not always require artificial intelligence: some operations can use explicit rules.
Hyperautomation describes an approach combining multiple automation technologies and tools, potentially including AI and machine learning. It is not simply the addition of machine learning or a mandatory stage that is identical for every factory.
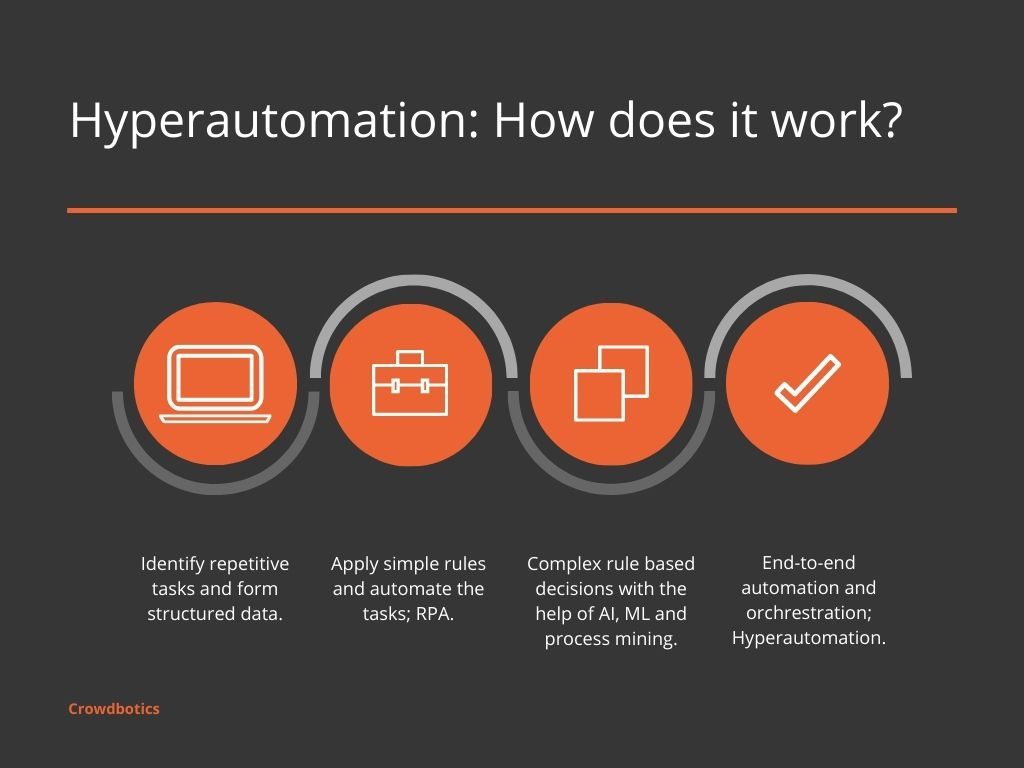
An AI system does not automatically improve simply because it receives more data. Data, any training and the resulting outputs must be evaluated; changes used in production require appropriate validation.
Interoperability then becomes central. Manufacturers need to check the formats, interfaces and access rights actually available on each machine, together with the system’s ability to evolve.
Define requirements before investing
The choice of functions to connect depends on the facility: production volumes, traceability, lead times, failure rates, skills and existing equipment.
Investment extends beyond the software price. Integration, data quality, training and maintenance also need to be assessed against measurable benefits.
The first step in understanding what these digital capabilities are, often comes down to recognizing the typical constituent components of additive manufacturing:
- Design & simulation stages;
- Print properties selection;
- Print preparation and orientation;
- Managing in-print queue;
- Initiating printing;
- Removing parts from the 3D printer;
- Post-processing; and
- Finished part retrieval.
“A good example of a specific use case is build preparation for laser powder bed fusion. There are many important factors like part orientation, support generation, and parameter assignment. A mistake can easily be made, and a failed print job can cost tens of thousands of dollars. Oqton [for instance], provides customers with the opportunity to create build preparation templates. We capture their knowledge and experience and couple it with our AI algorithms to automate the complete process.
In this way, we speed up the process and lower costs while substantially decreasing human error and improve reproducibility. When you reduce dependency on key operators, this also means that more people can program autonomously. You are no longer at the mercy of one key person’s holiday schedule or them falling sick. This also enables full end-to-end traceability, especially in regulated industries where full documentation is vital, such as medical and aerospace. Ultimately, we see clients increase machine efficiency by faster programming and using advanced manufacturing equipment like welding robots and industrial 3D printers”, Schrauwen notes.
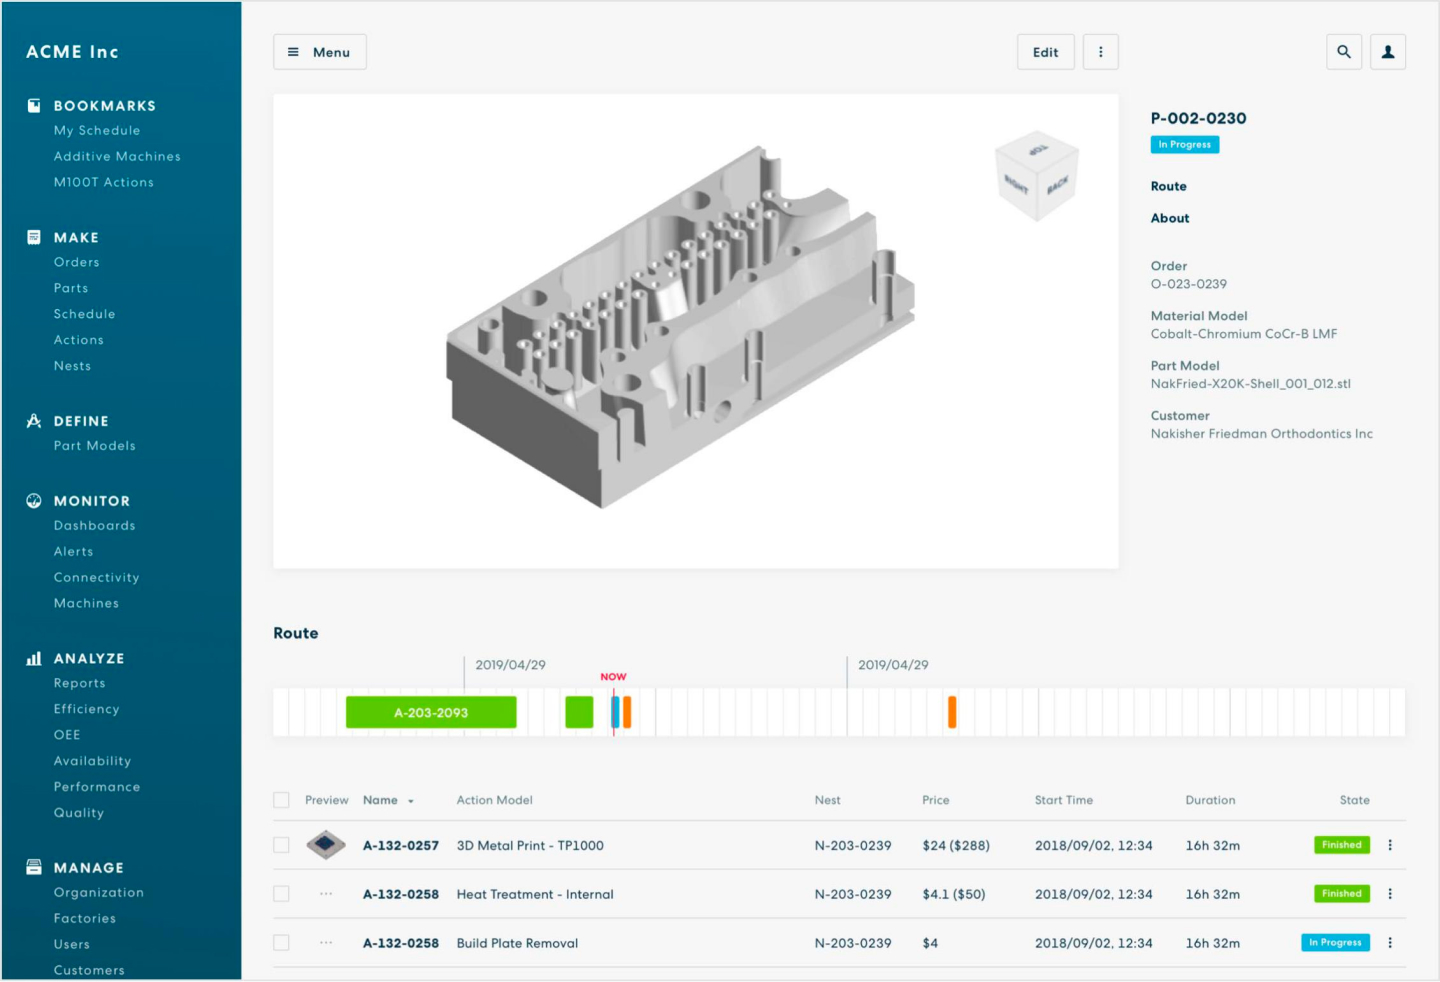
Apart from determining the right digital capabilities one aspires to, it is important to take into account the implementation of an automation strategy with regards to closed AM systems. Although it requires a dedicated article, that’s something we have partially addressed in the exclusive feature “What does “openness” truly mean in a metal AM system?”.
What does the future hold for software automation?
In this 2021 interview, order management, production and post-processing feature among the development opportunities. Practical priorities remain specific to each manufacturer.
Two areas frame the rest of this feature: design automation and automated data exchange.
Design automation for AM
It is no secret that AM helps to reinvent the design of parts and products in different application fields. Despite the design freedom that AM allows, most of the time, AM parts are designed manually. This can be explained by the fact that designing requires a lot of expert knowledge. Complex-shaped parts in particular, can often be an effortful process, both for novice CAD users and experienced designers, hence the need for design automation as an enabler for AM.
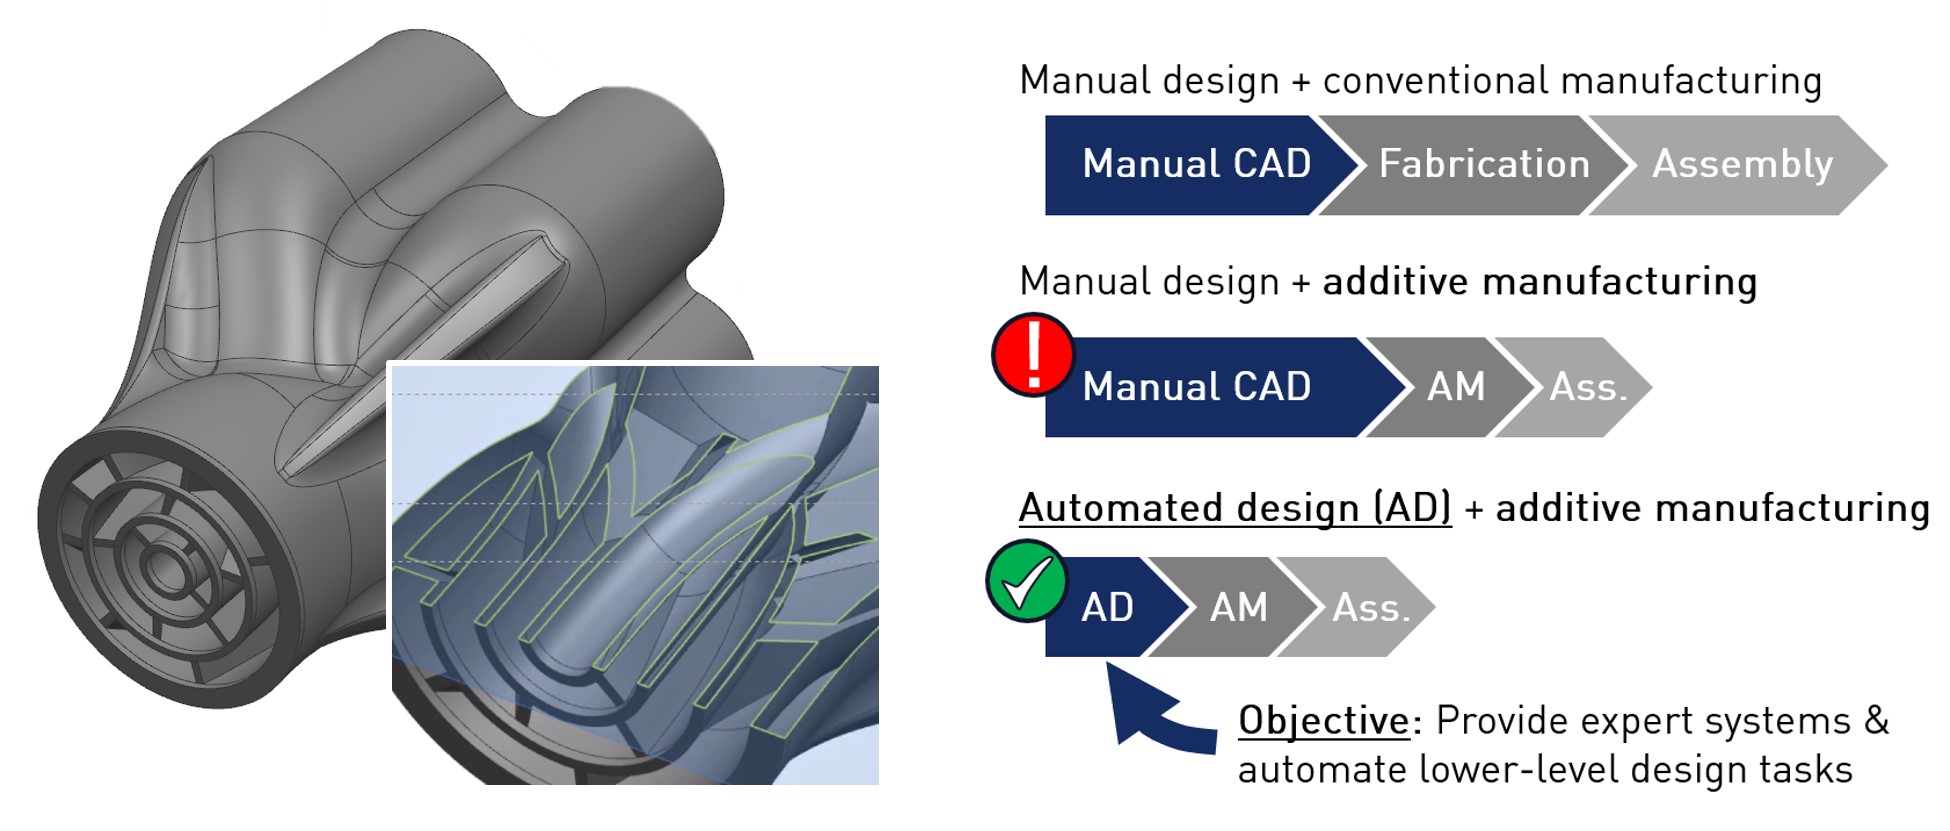
ETH Zurich researchers have examined the automation of design tasks for complex geometries. Their work on fluidic components illustrates this approach.
“The basic idea is to simplify and accelerate the design phase by providing expert systems that automate lower-level design tasks. Design intent and goals are specified on a high level of abstraction and automatically translated into optimized geometries while taking into account manufacturability restrictions of AM”, they said, speaking of the above image.
Another interesting example saw the development of computational procedures to automate the design of additive manufactured flow components such as hydraulic manifolds. “A designer specifies pathways of flow channels and manufacturing restrictions for AM. Based on these user inputs, algorithms automatically generate a production-ready 3D part geometry that can be used to fabricate prototypes or to conduct numerical simulations. Benefits for the product development include the shortening of iteration loops, the comparison of different production scenarios, and the cost-efficient customization of parts for small lot sizes”, the report reads.
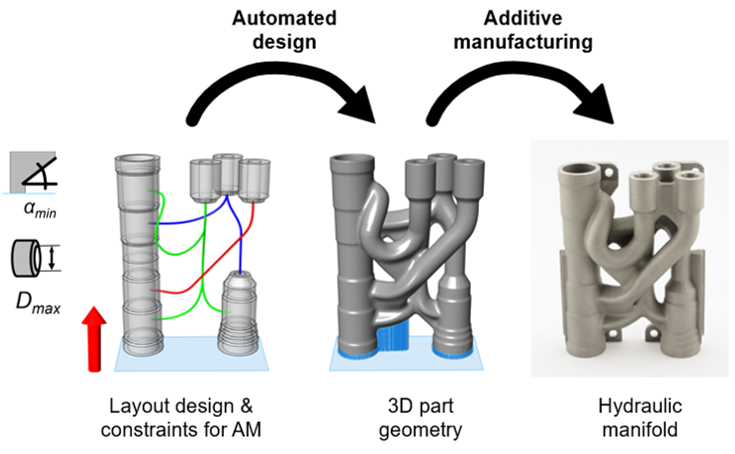
These examples include both geometries and physical demonstrators. Potential reductions in design effort must be measured for each application, including the technical validation of the resulting parts.
On the other hand, one notes the increasing number of collaborations between machine manufacturers and software providers to advance this specific area of manufacturing.
AM data sharing automation
The more technology providers create integrated, interoperable 3D printing workflows, the more open Application Programming Interfaces (APIs) are being used to enable connectivity between systems. This increasing use of APIs is a key trend that currently drives AM data sharing automation.
Simply put, an API is a software intermediary that allows two applications to talk to each other. For those who do not know, each time you use an app like Facebook, send an instant message, or check the weather on your phone for instance, you’re using an API.
The feature cites collaborations involving 3DControl Systems, AMFG and Dyndrite with manufacturers such as HP as integration examples. An API can facilitate data exchange without itself guaranteeing end-to-end compatibility.
“Admittedly, data preparation – build and process data is notoriously difficult to extract, analyse, visualize and share. Every machine manufacturer has its own standards and protocols. End users and the industry would benefit a lot if all manufacturers would openly share data through common protocols and APIs”, our expert notes.
Open interfaces need appropriate permissions, file confidentiality and connection security. The exchanged data must also retain a common meaning across systems.
A big shift in focus from hardware to software
However, moving forward the “trends coming around the corner include, a big shift in focus from hardware to software, which includes the move to cloud-based platforms, and the use of AI to automate that process.
IoT connected machines produce lots of data, which in turn requires machine learning AI as the only way to process all that information. Operations will therefore rely more and more on automation to manage their workflows. How to upskill their current workforce to take on new work responsibilities and work with automation is, therefore, both a coming trend and a challenge for the industry at large.
We also see a shift in manufacturing from using 3D printing just for prototyping towards its use within actual production.” Schrauwen says.
Machine learning is presented here as an Oqton direction. Other processing methods remain possible depending on the data and tasks; AI is not the only way to use data from connected machines.
The first step is therefore to map operations, identify repetitive tasks and select a trial scope. Measurable objectives, gradual integration and workforce involvement allow manufacturers to evaluate results before extending automation.
First published in 3D ADEPT Mag, July/August 2021.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.