
A 2023 feature on powder spreading, with Michael Wohlfart (EOS) and Thomas Spears (AAMT). The recommendations and configurations reflect the interview and must be assessed for the machine, material and application.
It might be easy for engineers or designers to think that, because they are not directly involved with the manufacturing of parts, they shouldn’t know about certain complexities surrounding the hands-on operation of machines. This is not true. Being aware of the variables and complexities related to the hands-on operation of machines helps to ensure clear communication with operators and most importantly, that design objectives perfectly meet manufacturing expectations. One of these complexities consists in understanding the importance of recoaters for metal Additive Manufacturing.
A recoater distributes a fresh layer of material. In powder-bed processes, it may use a blade, brush or roller to establish a uniform layer before selective consolidation. Recoating is not restricted to powders.
Some vat-photopolymerization machines also use a blade to distribute resin. Operation depends on the architecture, including top-down or bottom-up exposure, platform motion and resin replenishment. Not every machine in this family therefore uses a recoater blade.
Speaking of examples of AM machines that integrate a recoater, Thomas Spears, Director of AAMT, said [they] “include Electron Beam Melting (such as Arcam) [or] binder jetting (such as ExOne).” “Newer modalities I saw at Rapid+TCT were spreading a ceramic matrix material, photolithography machines like those from 3D Systems, and plastic sintering machines like those from EOS,” he adds.
That said, this article will focus on the use of recoaters in laser powder bed fusion processes.
The importance of recoaters in laser powder bed fusion processes
Laser powder bed fusion of metals (LPBF, or PBF-LB/M) uses a laser. Electron-beam powder bed fusion is a separate process (PBF-EB/M). In LPBF, a layer is spread over the platform and regions corresponding to a part cross-section are melted. The cycle repeats. Layer thickness depends on the system and material; 0.1 mm is not a universal value.
Apart from the fact that it lays the powder down uniformly, a recoater helps control the thickness of the powder layer deposition. The recoating speed plays an important role in this process as it may influence the surface morphology of the powder bed which in turn might jeopardize the manufacturing success of the part and the production’s reliability.
Long builds repeat these operations many times. Layer time depends on exposure, spreading and configuration rather than a fixed one-minute interval. Consistency, wear and process compatibility matter when choosing a recoater.
Types of recoater blades

“There are multiple variants of technologies to spread powder in commercial powder-based systems but all of them are referred to as “recoaters”, Michael Wohlfart clarifies from the outset.
Needless to say, peculiarities of some 3D printers may appear as different tools used to spread layers of powder evenly for each layer of a build. “Some manufacturers use a roller to help compact the powder and create a denser and more consistent packing density on the active surface. Velo3D uses a non-contact recoater where they use a vacuum to ensure proper layer thickness,” Spears explains.
One can identify four main types of recoaters. According to Wohlfart, there are:
- Hard recoaters: HSS (high speed steel), ceramic blades
- Soft recoaters: Different types of brushes (carbon fiber, metal), different types of polymer blades (silicone, NBR rubber, other types of polymers)
- Roller recoaters: Primarily used in polymer LPBF but also a niche technology in metal LPBF, especially for fine powders that are difficult to spread.
Contactless recoaters: these maintain clearance from the built surface. Speed, available layer thicknesses and tolerances depend on the system. Limitations discussed by Wohlfart in the 2023 interview should not be applied to every configuration.
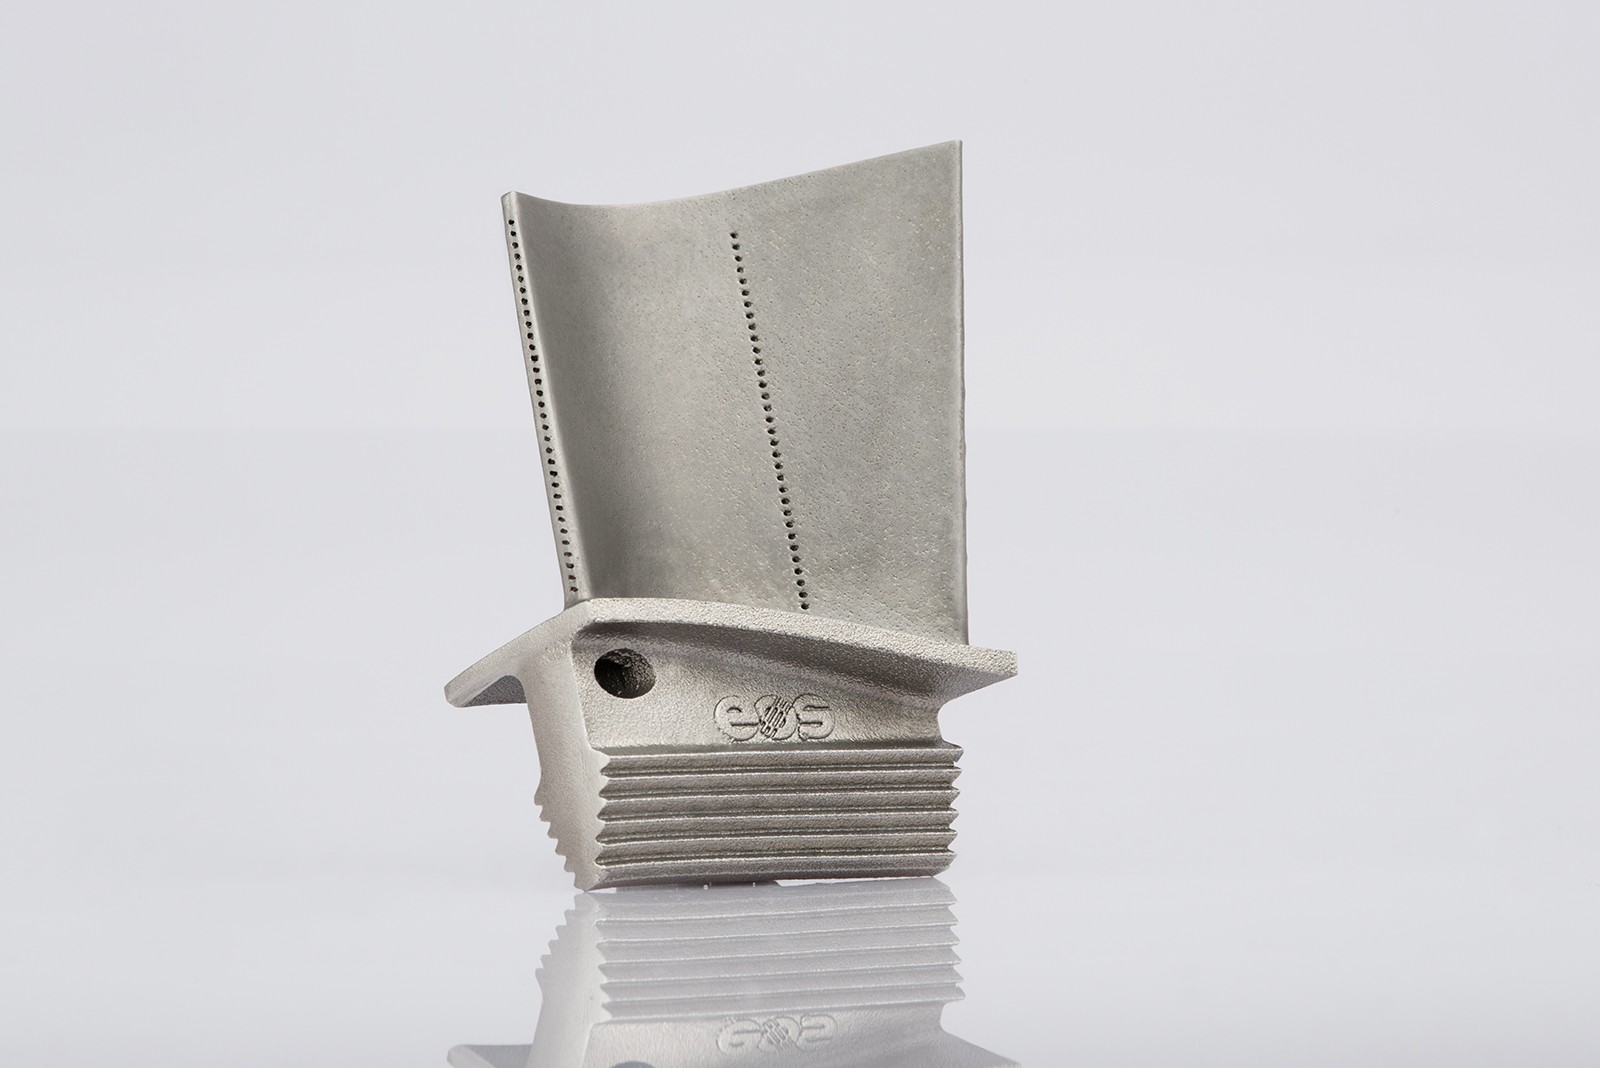
As you will realize in the industry, hard recoaters and soft recoaters are often mentioned as the main types of recoaters. That’s the reason why EOS’ AM expert refers to the two others as niche technology.
Choosing a rigid blade or a soft recoater is not simply a matter of whether parts are identical or different. Geometry, supports, distortion, powder and settings affect recoater interactions. A raised part can disrupt spreading without necessarily deforming every other part.
A soft recoater can accommodate some raised features and reduce forces on slender structures. It guarantees neither an uninterrupted build nor conforming parts. A completed build may still contain defects that inspection needs to detect.
Interestingly, sometimes, these differences are not enough to choose between a hard recoater and a soft recoater.
Some manufacturers will recommend the hard recoater for parts with highest demands given their ability to achieve repeatable quality whereas they will opt for a soft recoater for parts with high aspect ratios and for productions where lead time is more crucial than the risk of imperfections.
While the machines they build are compatible with both hard and soft recoaters, the Director of AAMT recognizes that “there is an element of subjectivity [when it comes to choosing the ideal recoater]. Some users prefer the forgiveness of the soft recoater while others prefer the consistency of the hard recoater despite its stronger likelihood of crashing due to top surface anomalies or part peel-up. Other process considerations can also dictate recoater type as silicone, carbon fiber brushes, and metal rakes are more appropriate for applications where very fine features are required that may be physically destroyed by a hard recoater making even modest contact with it.”
Wohlfart on the other hand, brings further clarification on the topic:
The following explanation concerns, in particular, EOS configurations discussed at that time. EOS comparative tests published in 2022 covered three powders and several blades; the results are not a universal ranking of every available combination.
“The processes for metal and polymer LPBF are fundamentally different and there are no machines on the market that could process both materials in the same system. However, there are still differences between the recoater systems than can be explained by the different material/process requirements but also the geometry to be printed may have an influence on the recoater type.
Polymer systems typically use hard recoaters or roller recoaters, because of the elevated temperature of the powder bed and the different nature of the processes. The shape of the hard recoater blade is typically also different compared to metal recoaters because compaction of the powder bed is more essential for the process.
Regarding hard recoaters for metal LPBF systems, a ceramic blade is required if the material is easily magnetizable (for example maraging steels) otherwise, HSS blades are used. While hard recoaters assure the best repeatability in layer height, soft recoaters are recommended for parts with a high aspect ratio.”
A couple of tips on part positioning
To minimize distortion or failed builds, and to a certain extent, ensure the efficiency of the recoater blade in the long run, the operator should pay attention to part positioning.
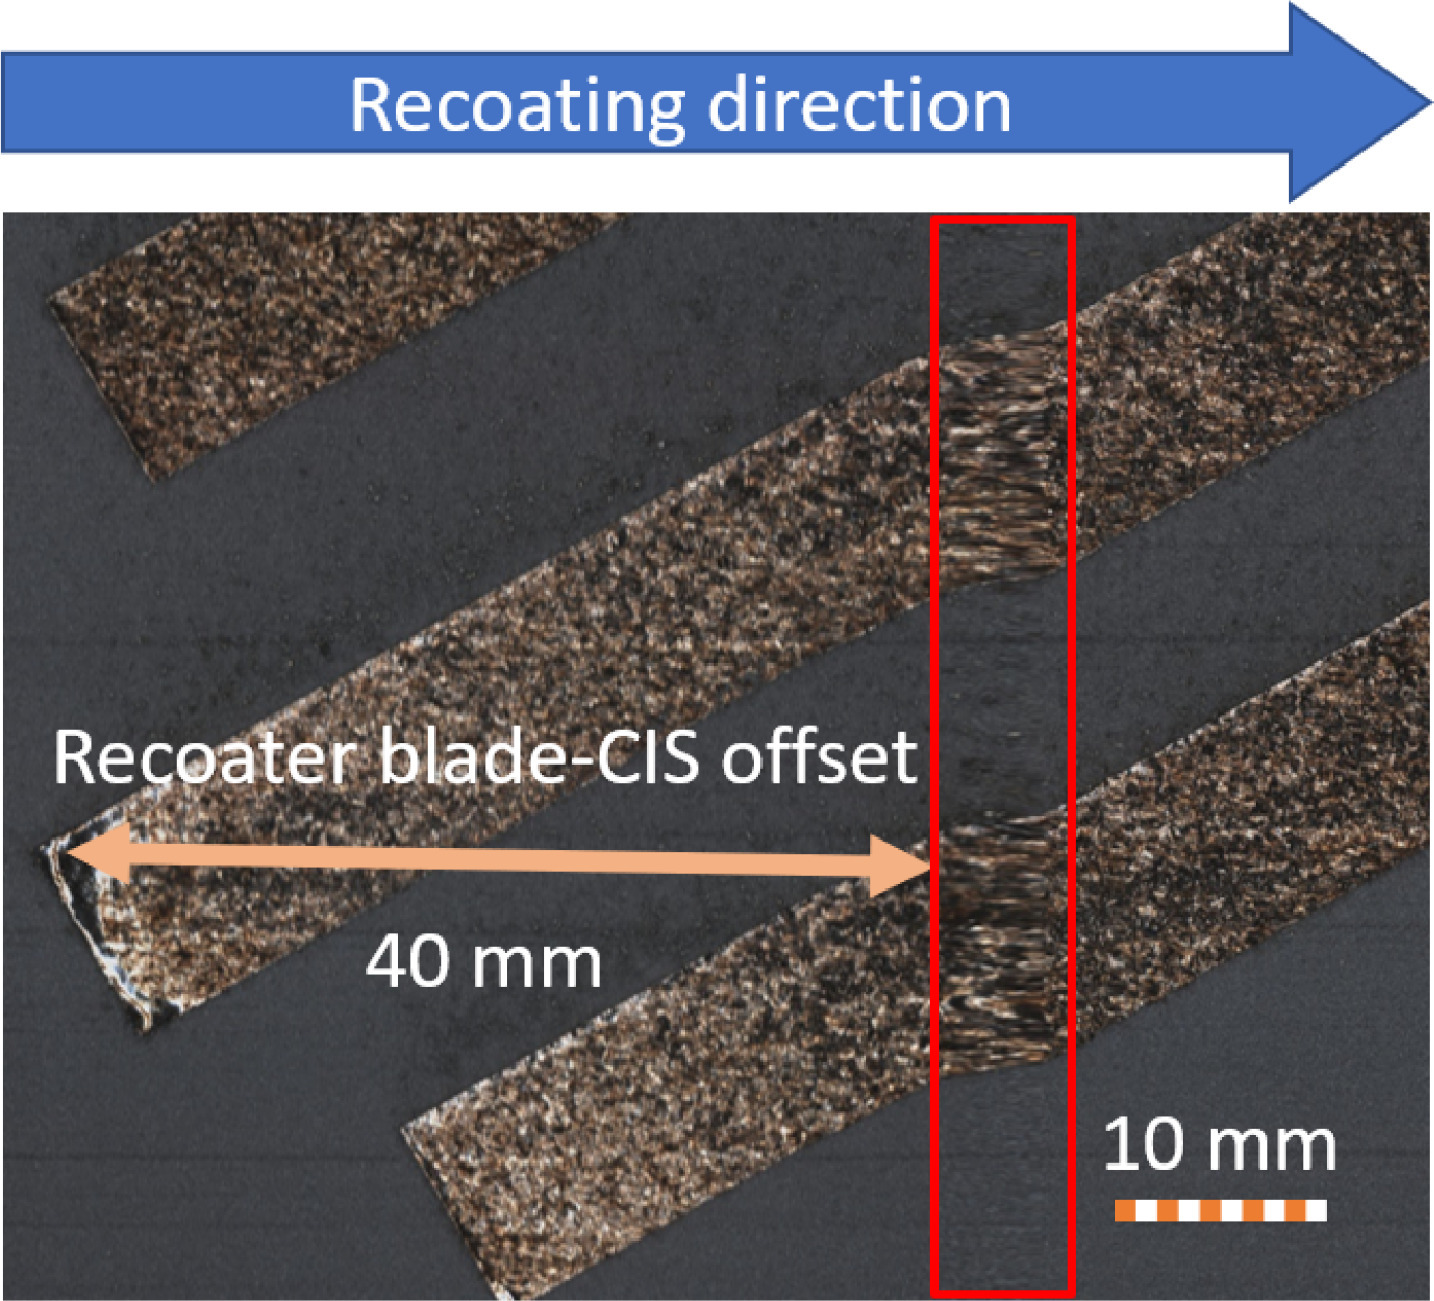
In an ideal world, once the recoater has spread a layer of powder, the area of the component built should not move. In practice, depending on many variables, the part could move, leading to a distortion that may apply pressure on the recoater. That pressure could bend or break the component, – or worst scenario, damage the recoater blade.
A correct part positioning may help prevent these issues. For instance, one may avoid having the recoater make simultaneous contact with several 3D printed components at once. The operator can stagger the parts on the build platform to mitigate this risk.
There is no general rule requiring the tallest parts to be placed closest to the recoater. Layout should account for spreading direction, supports, contact risks and machine-specific guidance.
Avoiding alignment of sensitive features along one travel path may form part of that assessment. Staggering alone does not guarantee continued production after damage to a part or blade.
In-process monitoring can help identify irregularities. Bugatti and Colosimo (2022) describe a scanner mounted on the recoater to observe the powder bed and printed surface. Detecting an anomaly and accepting a part remain distinct steps.
A few words on the contributing companies
In this 2023 feature, Open Additive is described as a metal-AM equipment and monitoring supplier within Arctos. The company was announcing AMSENSE Chimera with Recoat+ to identify recoating issues on EOS M400 and M290 machines. Higher throughput and fewer failures are supplier-stated aims, not guaranteed results for every installation.
EOS is a manufacturer of polymer and metal AM systems. The company provides a wide range of hard and soft recoaters. Depending on the magnetizability, an HSS (standard) or ceramic blade (magnetizable powders) would be used. While they provide their customers with maximum flexibility and openness, the company said the hard recoater configuration is in most cases the preferred option. Their soft recoater types include:
- Two types of polymer blade recoaters: Silicone and NBR for different temperature ranges and stiffness requirements.
- A carbon fiber brush, which is even more forgiving for fragile and high aspect ratio parts than a polymer blade soft recoater. However, if damage to the brush recoater occurs in case of rising edges or out-of-plane growth due to internal stress, it is also more costly to replace this kind of recoater type.
Based on detailed investigations of different recoater types, the company recommends the right configuration based on their use case.
Other references:
The intelligent recoater: A new solution for in-situ monitoring of geometric and surface defects in powder bed fusion; an article written by Matteo Bugatti, Bianca Maria Colosimo.
Further reading: EOS recoater configurations.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.