

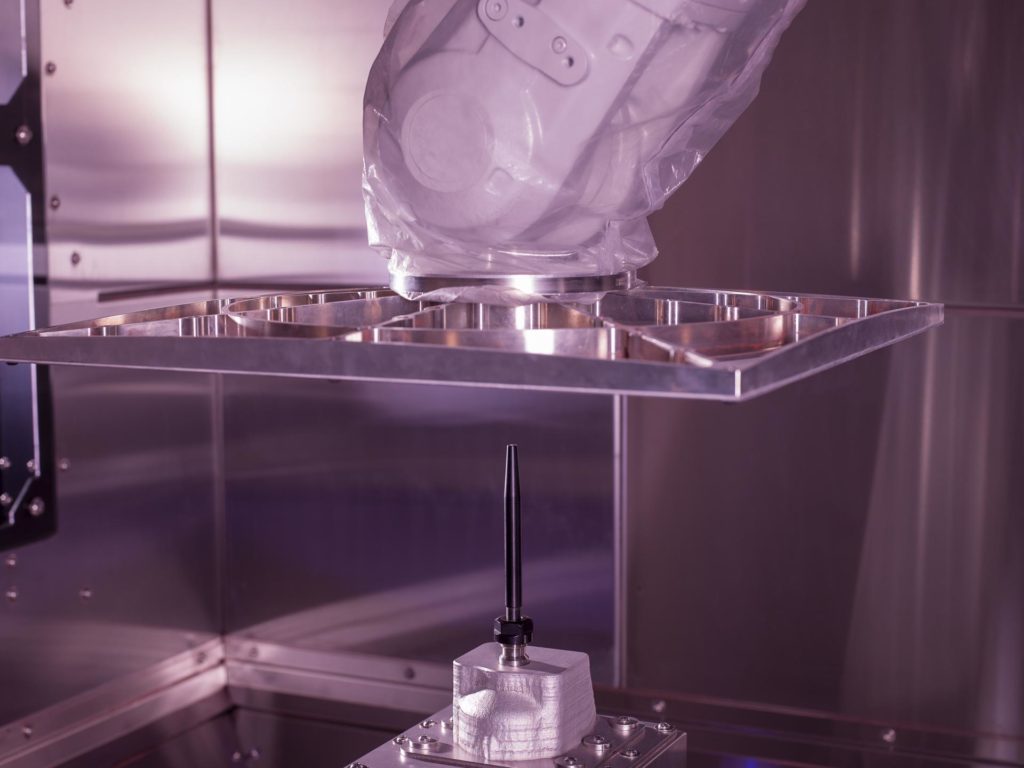
Feature first published in the January–February 2021 issue of 3D ADEPT MAG. Roles and performance claims reflect interviews from that period. Deposition rates do not represent the complete manufacturing time for a finished part.
Cold Spray Additive Manufacturing (CSAM) deposits high-speed particles without melting them. Also described as supersonic particle deposition (SPD), it interests manufacturers seeking to accelerate selected metal manufacturing or repair operations.
This exclusive feature aims to discuss the methods, challenges, and applications of this process and the reasons why it is uniquely positioned to meet the requirements of certain industries. To discuss these topics, we have invited two companies that have made this technique their core business: Titomic and SPEE3D. Jeff Lang, Founder of Titomic Limited, Executive Director and CTO as well as SPEE3D co-founders Byron Kennedy and Steven Camilleri are the main contributors of this exclusive feature.
Deposition rate and manufacturing lead time
Deposition rate is only one component of industrial lead time. Preparation, programming, material changes, heat treatment, machining and inspection also count.
For production runs or large parts, process selection must account for the complete cycle and required properties. A high melting temperature does not itself imply faster manufacturing.
The only thing is, as per the words of Jeff Lang, “the main factor, the metal 3D printing industry has struggled to realise, is its viability against the speed of traditional metal fabrication for industrial-scale metal parts, especially in the aerospace and defence industries.”
Indeed, “in traditional AM, the metal powder is melted with a laser – that process takes a solid powder, melts it into a liquid, and then reforms that into a solid. That process takes time, based on physics, and is easy to calculate. In order to speed this process up for more efficiency, you needed a process that does not melt the powder”, explain Byron Kennedy and Steven Camilleri.
The interviewees are describing processes that melt powder with a laser. This does not cover every additive manufacturing process family.
Those challenges, therefore, lead to the increasing interest in supersonic particle deposition (SPD) additive manufacturing (AM) technology (also known as Cold-Spray).
So, what is Cold Spray?
As Titomic’s Jeff Lang notes, Supersonic Particle Deposition (Cold-Spray) has been in commercial use for over 30 years but its application in additive manufacturing is quite recent.
Cold spray uses a gas jet to accelerate particles towards a substrate. In the metal applications discussed here, impact and deformation enable solid-state deposition as a coating or a near-net-shape preform.
A convergent-divergent de Laval nozzle accelerates the gas; particle velocity depends on material, particle size and spray conditions. The principle is not exclusive to one manufacturer.
Avoiding melting can limit changes and some defects associated with solidification. It does not guarantee zero oxides or porosity, or unlimited thickness and dimensions.
Cold describes deposition in the solid state. The gas can be heated, so it would be incorrect to infer that the entire process involves no heat.
Materials Considerations & Post-processing
Solid-state deposition can suit oxygen-sensitive metals such as titanium, aluminium or magnesium with suitable parameters. Powder ductility and condition remain important.
According to SPEE3D’s founders, “every powder has what is called a deposition speed. When accelerating a powder if its speed is too slow, the powder bounces off, too fast, and the powder will erode the substrate. In between is what we call the “speed deposition window”. For example, copper can be deposited at 450 metres per second, aluminium at 600 metres per second, and stainless steel at 700 metres per second. These are the ideal speeds.”
As far as SPEE3D is concerned, the founders explain that they accelerate “the powder to in-between Mach 1.5 and Mach 2 depending on the material we use (supersonic speed is greater than Mach 1 or greater than 343 metres per second).”
The values quoted describe the manufacturer’s operating conditions, not universal settings. Mach number depends on gas and temperature: 343 m/s is an approximation for air near 20 °C, not a constant for every flow.
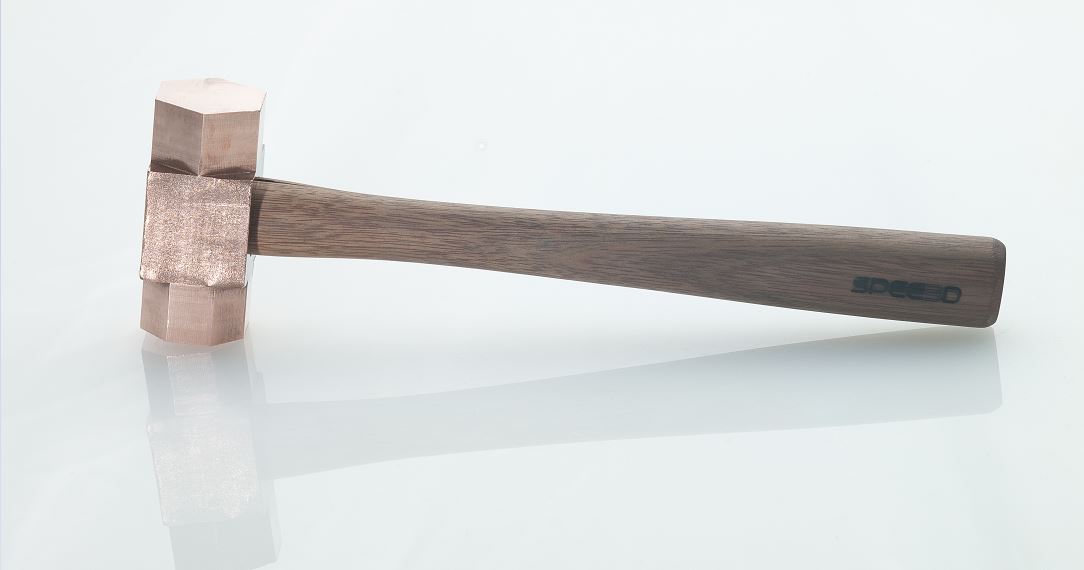
Deposit properties depend on material and spray conditions. Heat treatment, densification or machining may be needed for the required porosity, mechanical properties and tolerances. Hot isostatic pressing (HIP) is neither universal nor a guarantee of removing every defect; a ductile material still needs validation.
Different roads lead to “speed”
Titomic and SPEE3D developed different configurations and control strategies around cold spray. Their figures need reading alongside the stated conditions.
Branded as Titomic Kinetic Fusion (TKFTM), Titomic’s patented process allows for the production of industrial-scale additive manufacturing of Titanium parts.
Lang recalls being approached in 2008 by CSIRO, Australia’s national science organisation, to investigate a titanium value chain.
“To unlock this value chain required a deep investigation into production technologies for Titanium fabrication with the intent to find the most viable process with the most unique value proposition. After investigating various AM technologies for producing Titanium parts, the one apparent thing was the limitations of build speed and size with melt-based AM processes. As I was looking to utilise large quantities of Titanium powder, I needed to find a suitable AM technology that was commercially viable against traditional Titanium fabrication methods”, Lang explains.
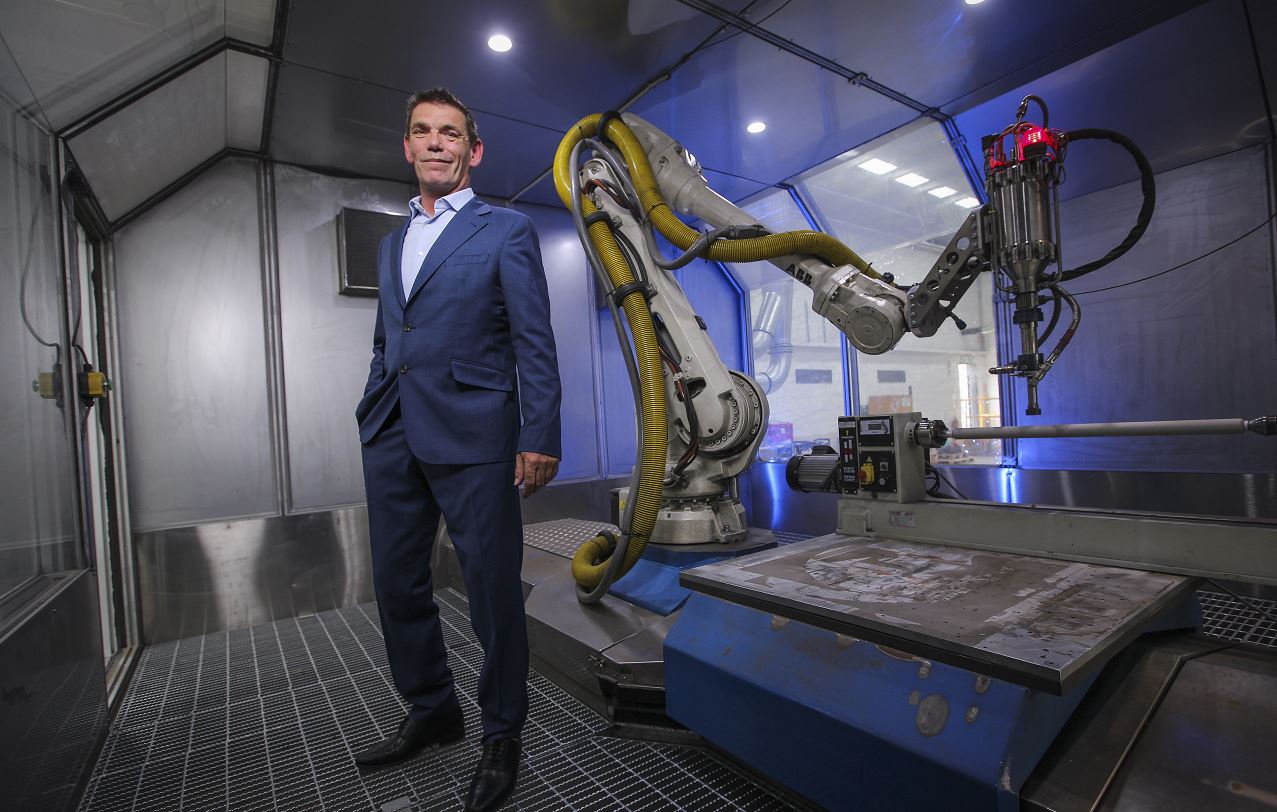
Lang realized that due to its high- deposition rates, the high-performance metal coating process was a great bet to produce AM parts faster and “without the size constraints of melt-based 3D printers.” At the time of this 2021 interview, the manufacturer described the TKF1000 system that delivers build speeds between 6-10 kg per hour depending on the type of metallic material used and its density.
“Our custom TKF systems can be configured with multiple heads to deliver build speeds of up to 75 kg per hour. As with all additive manufacturing equipment suppliers, there are some bold claims as far as build speeds that are unrealistic even though the machine may be rated to that maximum. On a single TKF system head, we can build 30-45 kg per hour, however there would be considerable porosity at these build speeds which affects the mechanical properties”, the expert adds.
Lang’s caution about porosity shows why a maximum deposition rate alone cannot compare productivity for parts meeting equivalent requirements.
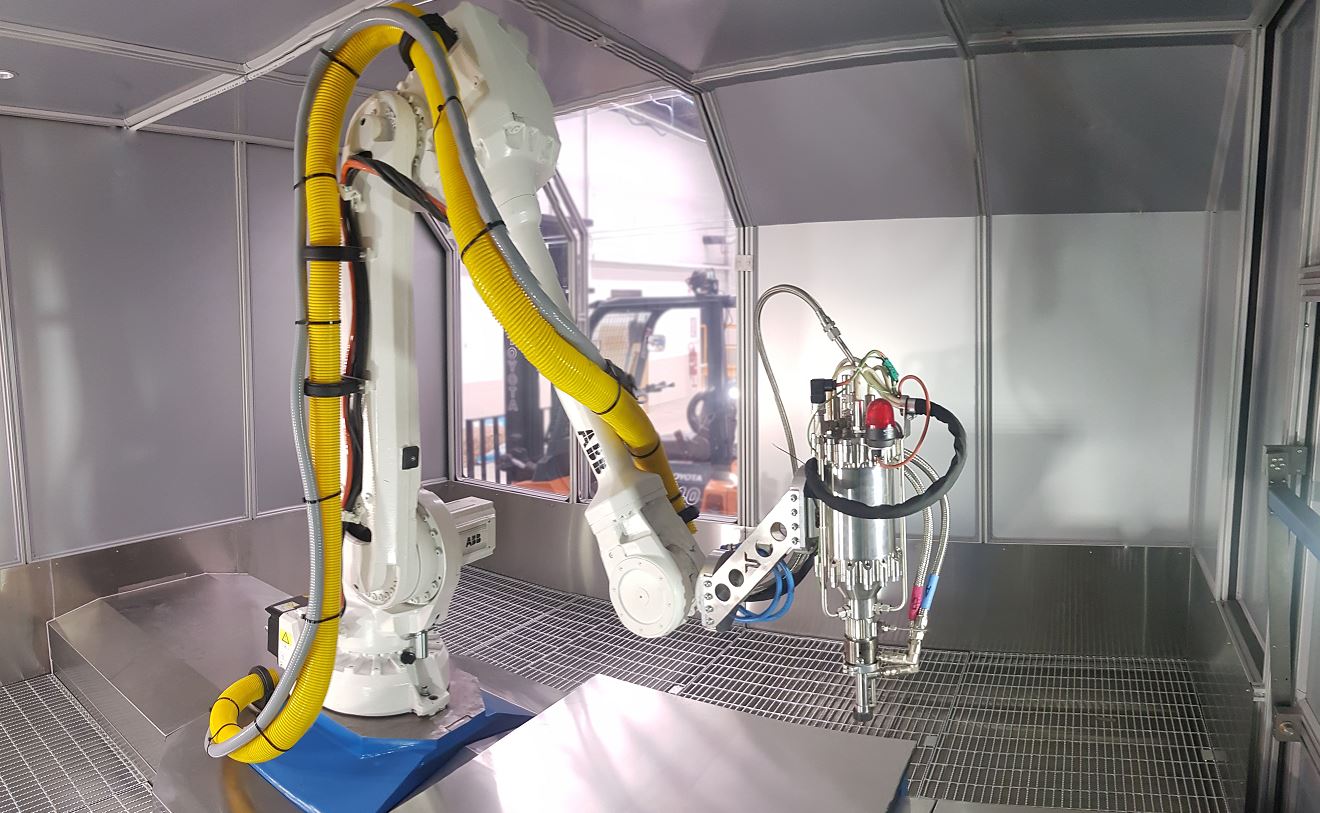
In the case of SPEE3D, it’s a different route that led to the development of their cold spray AM technology. With a decade of experience in manufacturing, SPEE3D is not Kennedy and Camilleri’s first entrepreneurial journey. In the life they had prior to SPEE3D, they realized the potential of metal 3D printing but also deplored its limitations.
“The challenge, however, was that traditional metal AM was too expensive and too slow. So, when finishing up with the manufacturing company, we decided to enter the additive manufacturing space. We began to look for a manufacturing-friendly AM technology – a fast and low cost technology. That is when we came across Cold Spray, which at the time was primarily used in military repair applications, and in a “manual way”. We found that this was something that could be fixed. So, with a background in Control Systems and Robotics, we took a manual Cold Spray Process and turned that into a metal AM machine” the founders point out.
Both founders share their long-term goals : “the limitation in SPEE3D’s printers is not the deposition speed, but the robotics keeping up with the Spray (Cold Spray). Theoretically, the process could be a lot faster, making the AM process even easier, and this what SPEE3D continuously works on as its long-term goal.”
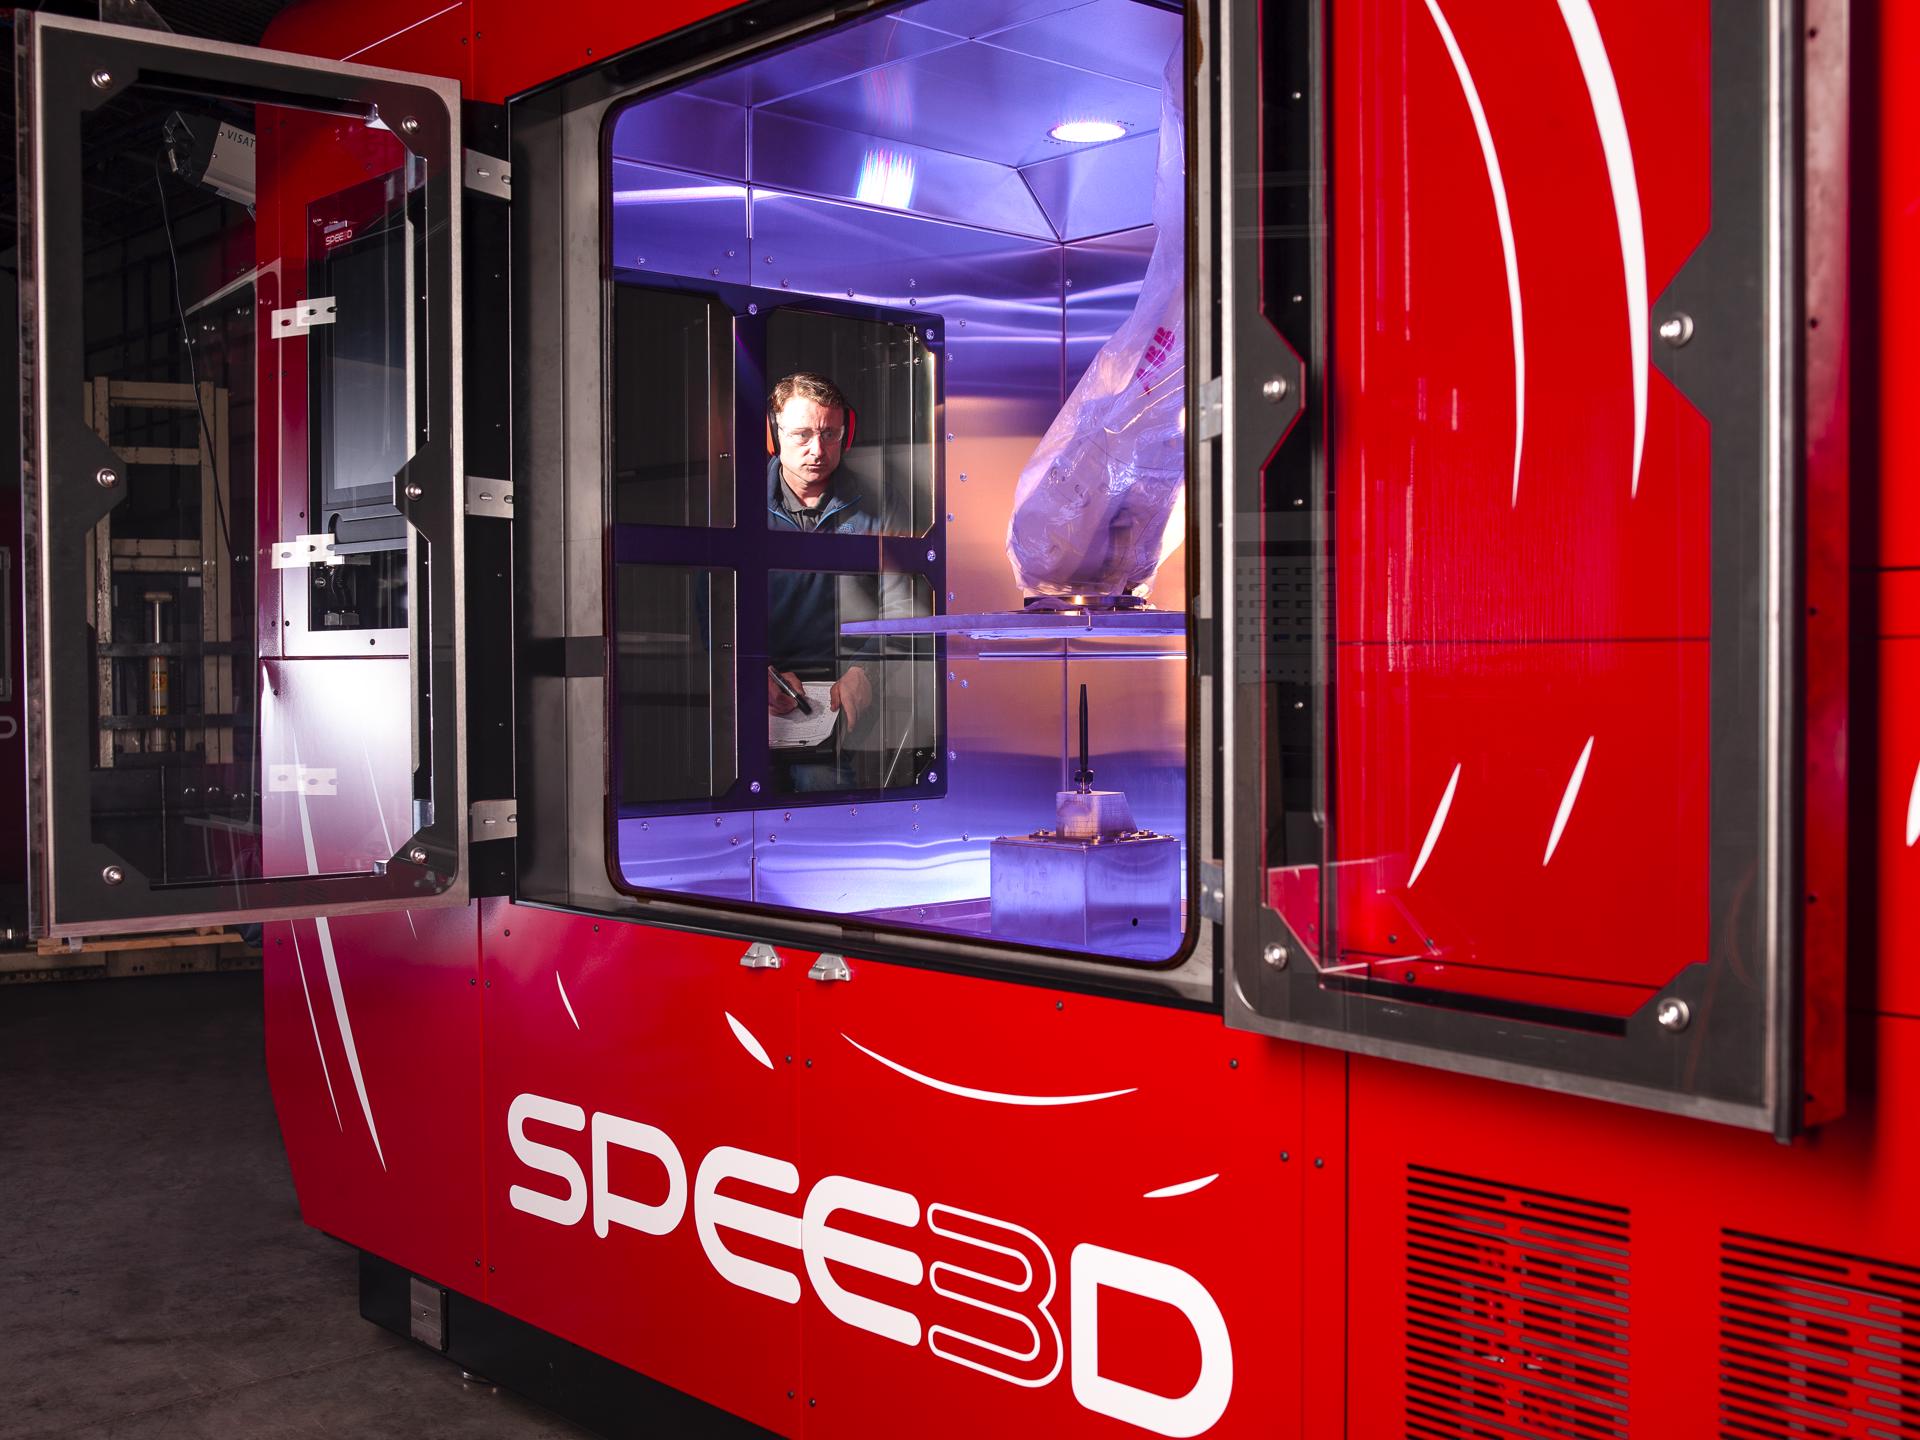
Material selection, toolpath programming, treatment and machining must be coordinated. Increasing deposition rate can change geometry or properties; optimisation is an application-specific trade-off.
Applications & challenges
Applications investigated for cold spray include helicopter gearbox repairs. WPI’s September 2019 research announcement describes powder development for repair. A demonstration or research programme does not constitute blanket approval to return components to service.
Speaking of helicopter gearboxes, Danielle Cote, assistant professor of materials science and engineering and director of WPI’s Center for Materials Processing Data notes: “If you need to replace a part like that, it can take months or even years, and the cost is significant—assuming that the part is available or even still being made. To repair a gearbox with cold spray, you need alloys with high strength, toughness, and ductility. Our methodology will enable us to develop powders that can be used to effectively repair or even manufacture parts like that and get helicopters back in the air quickly. The Army is especially interested in portable cold spray systems, but the technology can also be used on a larger scale—in industry, for example—and it will be exciting to see how robots can help expand the use of this and other additive manufacturing processes.”
Apart from military and defence applications, we have also seen Cold Spray AM applications in the space industry and certain luxurious consumer products.
At the time of these interviews, results and prospects varied by application. Industrial suitability needs assessing through qualified parts, complete costs and repeatable production.
Furthermore, researchers strongly encourage manufacturers to have a close look at materials selection as well as the microstructure and mechanical properties of deposits that may depend on different process parameters. In this vein, geometric control can often be a quite disturbing issue. “Low geometric control is attributed to a range of key issues that limit the application of additive manufacturing technologies such as the necessity of post-machining, difficulty in fabricating complex shapes, geometry-induced property variations, and inconsistent quality of fabricated parts. Therefore, addressing the challenge of geometric control is undoubtedly of great importance in Cold Spray AM as well as other high-speed additive manufacturing technologies”, the study reads.
The cited study was published in 2019 and examines track-profile modelling. It identifies a geometric-control challenge rather than validating every machine and material discussed in this feature.
Concluding notes
Cold spray can produce near-net-shape metal preforms and perform selected repairs. Its value depends on the material–application combination and the complete production chain, including finishing and inspection.
This feature was first published in the January–February 2021 issue of 3D ADEPT MAG.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.