

Feature published on July 18, 2024, with insights from Greg Lane, then Key Account Manager at Aalberts surface technologies. Process conditions depend on material, geometry and qualification requirements.
Hot isostatic pressing (HIP) combines heat and gas pressure to densify powders or previously manufactured parts. It can reduce internal porosity and improve certain mechanical properties, without guaranteeing removal of every defect. EPMA gives 100–200 MPa and 900–1,250 °C as examples for steels and superalloys, not a universal recipe. This feature examines where HIP can help with critical additively manufactured components.
This dossier is part of our series of “post-processing” articles, which aim to demystify each post-processing task that can be used at the end of the additive production. Remember that post-processing is an umbrella term that covers a variety of stages that 3D-printed parts may require before being used for their final purpose. Needless to say, the use of each post-processing task depends on several factors including the AM process and materials used as well as the ultimate goal to achieve for a given 3D printed part.
HIP is considered a type of heat treatment solution that can be applied to parts manufactured via both AM and traditional manufacturing processes. As a reminder, in a previous dossier, we discussed heat treatment for AM parts. This feature examines differences between manufacturing routes, the treatment cycle and criteria for selecting HIP.
Casting, MIM and AM: different starting points
HIP is used for metals and ceramics, among other applications. In this interview, Greg Lane lists iron-, nickel- and titanium-based alloy families, aluminum AlSi10Mg and A357, copper, stainless and tool steels, cobalt alloys and MCrAlY materials. This does not imply that one cycle suits them all. The examples below mainly concern metal parts; the stated temperatures should not be transferred to polymers.
Speaking of how porosity and defects occur, Greg Lane said: “Porosity is generated during solidification in investment castings and AM as well as during sintering. A remaining pore is always a weak spot and can serve as a possible crack initiation site, thus, limiting the lifetime of a part. Even a small network of pores within a part makes crack initiation and propagation very easy, especially when subjected to cyclic loading.”
For castings, metal injection molded (MIM) parts and AM components, the common aim is to treat internal porosity that is amenable to HIP. Defect types, microstructures and prior treatments differ between these routes, so the cycle needs to be selected accordingly.
How does a HIP cycle work?
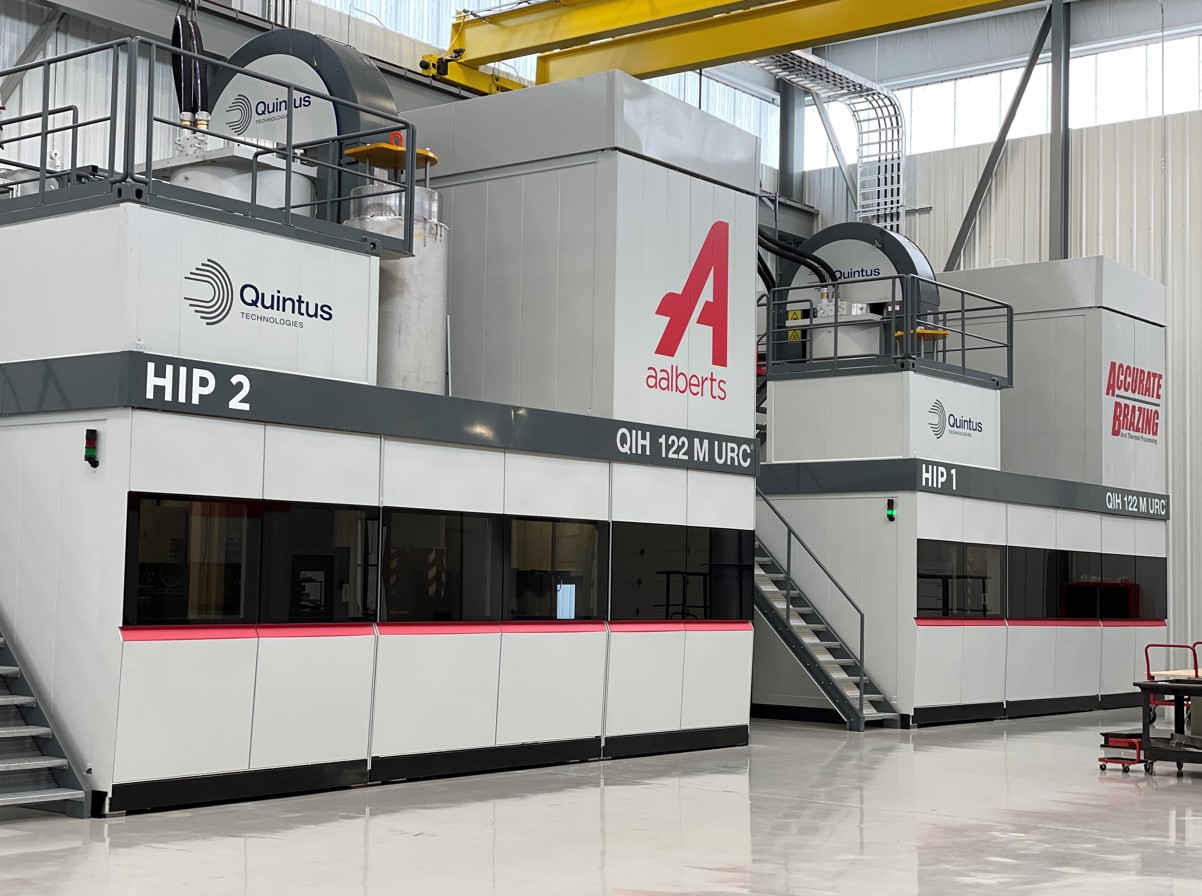
The equipment contains a furnace inside a pressure vessel. Parts are heated and subjected to pressurized gas, often argon. Temperature, pressure and holding time are set for the material and target properties, and cooling can also be controlled under pressure. This is not a liquid cooling bath. The 8–12 hours mentioned in the interview are an indicative range; total duration varies with equipment, load and cycle.
HIP’s suitability needs assessment for the manufacturing chain concerned. In his list of the most used processes, Lane counts Laser Beam Powder Bed Fusion (PBF-LB), Electron Beam Powder Bed Fusion (PBF-EB), Wire Arc Additive Manufacturing (WAAM), as well as Binder Jetting.
In the 2024 interview, Lane argues that simply transferring a casting cycle may be insufficient for an AM part. His observation about rapid solidification concerns processes that melt metal; it does not directly describe binder jetting followed by sintering.
“However, the nature of the AM process is quite different in comparison to the aforementioned manufacturing routes. The rapid solidification during the build job produces a very fine microstructure with unique properties. This structure can be up to two orders of magnitude finer in comparison to the investment cast counterparts, even for the same type of alloy. Because of this, a tailored HIP cycle can have a huge positive impact on the properties of an AM part and the AM production chain itself,” he adds.
“A typical HIP cycle starts with heating where pressure and temperature are increased. During the holding/soaking the combination of high temperature and pressure up to 200 MPa closes the pores and cracks in the material. The materials are virtually fused to a defect-free state. After a specific amount of time, the cycle is terminated via cooling. Modern HIP equipment can set desired heating and cooling rates as some processed materials require fast or fixed cooling rates,” he continues.
The phrase “defect-free state” above describes the speaker’s objective, not a general guarantee. Aalberts states that HIP does not correct surface-connected defects or dimensional inaccuracies. Defects need characterization before treatment and results need verification afterwards.
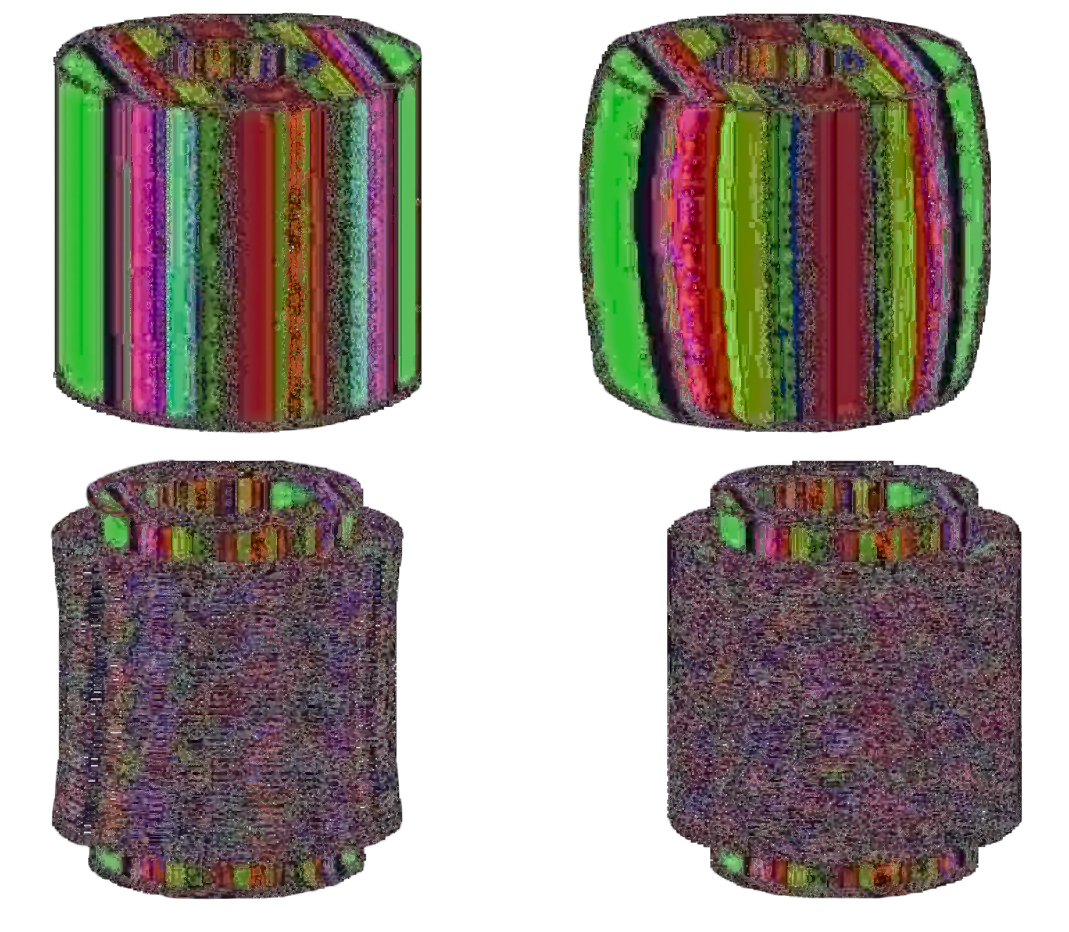
Temperature, pressure and hold time control densification, while heating and cooling rates help control microstructure. Here, density and residual porosity are assessed in the manufactured parts, not in loose powder. Feedstock and manufacturing parameters can influence these defects and fatigue behavior.
When should HIP be considered?
HIP can also make components by compacting encapsulated powder. EPMA cites oil and gas parts weighing up to 30 tonnes and near-net-shape impellers up to one metre in diameter. These PM-HIP examples do not establish that the parts were 3D printed. HIP post-processing of AM parts is a separate use, investigated in fields including aerospace, energy and medical applications.
So, when and how does one know that HIP is the post-processing step one should use for a given application? For Lane, it all comes down to porosity:
“A well-controlled build job can minimize the tendency to introduce internal defects such as porosity in AM components to an acceptable level for some non-demanding applications. However, for use in critical applications in demanding industries such as energy, aerospace, defense and medical, where performance and safety are key, porosity must be eliminated. In the as-built condition because without HIP, the remaining porosity can lead to differences in mechanical strength (scatter of properties), either between parts from the same built plate, or in different cross sections of larger parts. A residual network of pores makes crack propagation very easy when subjected to cyclic loading in jet engines (blades) or within the human body (HIP-implants).”
Lane’s emphasis on porosity does not make HIP mandatory for every critical part. The decision depends on observed defects, alloy, required performance and the qualified manufacturing route. Open porous structures can also be intentional and should be distinguished from unwanted internal pores.
To explain how HIP can generally improve productivity and product quality of critical 3D printed parts, he adds:
“The HIP process is often just one part out of the total processing route. A traditional route would include a pre-HIP stress relief treatment and post-HIP solution annealing and/or precipitation hardening carried out in a vacuum furnace. The state-of-the-art HIP equipment offers the possibility to incorporate stress relief and the solution annealing/hardening into the HIP cycle because defined heating rates with intermediate holding plateaus as well as fast cooling rates can be realized. This streamlines the AM post-process chain, increases productivity of the printers and, in the end, improve mechanical properties and the lifetime of AM components.”
The table below restates potential benefits alongside the checks they require. It does not give guarantees for every 3D-printed component.
| Objective | Checks required |
|---|---|
| Reduce internal porosity | Characterize the defects; HIP does not directly correct those connected to the surface. |
| Improve fatigue performance | Validate the treated alloy’s properties, microstructure and surface condition. |
| Preserve the useful geometry | Allow for and measure possible dimensional changes from densification. |
| Combine treatment stages | Check that the HIP cycle is compatible with other heat treatments and equipment capabilities. |
| Reduce cost or environmental impact | Assess the full chain: energy, gas, transport, scrap, machining and service life. No universal saving is quantified here. |
Concluding thoughts
This feature introduces HIP’s possibilities rather than specifying a universal treatment route. The task is to integrate HIP into a qualified chain and verify the properties obtained. The time, cost and performance gains discussed by Lane still need demonstration for the application concerned.
Contributor to this feature
Greg Lane contributed to this feature on behalf of Aalberts surface technologies, a surface- and heat-treatment service provider. The interview highlighted HIP capacity in Greenville, South Carolina, and the logistics of combining operations at one site. These are benefits proposed by the provider; the article supplies no independent cost or lead-time comparison.
Review note: the furnace has been located inside the pressure vessel, and HIP of AM parts distinguished from PM-HIP. Absolute promises in the table have been replaced by objectives that need verification. The French translations of “hip implants” and “holding/soaking” have been corrected, and the diagram caption aligned.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.