

Feature published in the May–June 2020 issue of 3D ADEPT MAG, then online in July 2020. Roles, products and interviewees’ estimates reflect that period.
Post-processing helps turn a 3D-printed part into a product suited to its intended use. The operations selected affect cost, quality and lead time.
It can remove supports or manufacturing residues, adjust dimensions and surface finish, or develop material properties. Its purpose extends beyond removing defects.
These operations follow printing, in a sequence defined by the process, material and application. Planning for them should begin during design.
Operations may include heat treatment, post-curing, support removal, cleaning and depowdering, machining, coating or infiltration, surface finishing, inspection and dyeing.
This dossier aims at giving industrials key insights into post-processing, its different segments and its importance in AM serial production. To address this issue, AMT’s CEO, Joseph Crabtree and Manuel Laux, Head of AM Solutions will mainly take the floor to share their opinion on several key points. We also thank FIT AG, Solukon, Protolabs and Girbau, for the examples provided.
A post-processing stage can bring many improvements such as better aesthetics, geometric accuracy, mechanical functionalities and properties, desired surface characteristics, to name a few. However, to get the product in its “ready-to-use” form, operators face two main challenges:
- The first one is that a large proportion of the tasks carried out after the printing process are manual.
According to AMT’s CEO, Joseph Crabtree, “currently, up to sixty percent of the manufacturing costs of a 3D printed part are attributed to the highly manual steps of post-processing, the part after it has been printed. By automating the post-processing workflow, manufacturers will reduce costs by producing end-use parts with a technology that is reliable, repeatable, and reproducible.”
The second challenge is process compatibility: resin, filament, metal powder and polymer powder require different approaches. Define the expected outcome and distinguish required operations from optional finishing.
“Apart from powder-based SLS, HP MJF and binder jetting techniques for plastic components practically all 3D printing systems require support structures for components with overhangs. As part of the post processing process, these support structures must be removed. Also, depending on the printing method, residual resin and powder must be removed. And, finally, the surface of the printed components must be refined by edge radiusing, surface smoothing and, frequently, polishing. On average the removal processes (support structure, resin, powder) and surface finishing account for about 75% of the post-processing work. Other post-processing activities may involve vacuum drying and dyeing of the printed components.
To be cost-effective, these jobs can no longer be handled by manual labour like pliers or old-fashioned immersion tanks for support removal, or hand sanding. This is too time-consuming, produces inconsistent results and is too costly. Preferably, the manual labor and traditional tanks must be completely replaced by fully automated chemical and mechanical systems”, explains Manuel Laux, Head of AM Solutions.
About the figures quoted: the 60% and 75% estimates reflect the interviewees’ observations in 2020. They are not universal averages; cost and workload depend on the process, part and degree of automation.
A look at the various post-processing steps
1- Heat Treatment
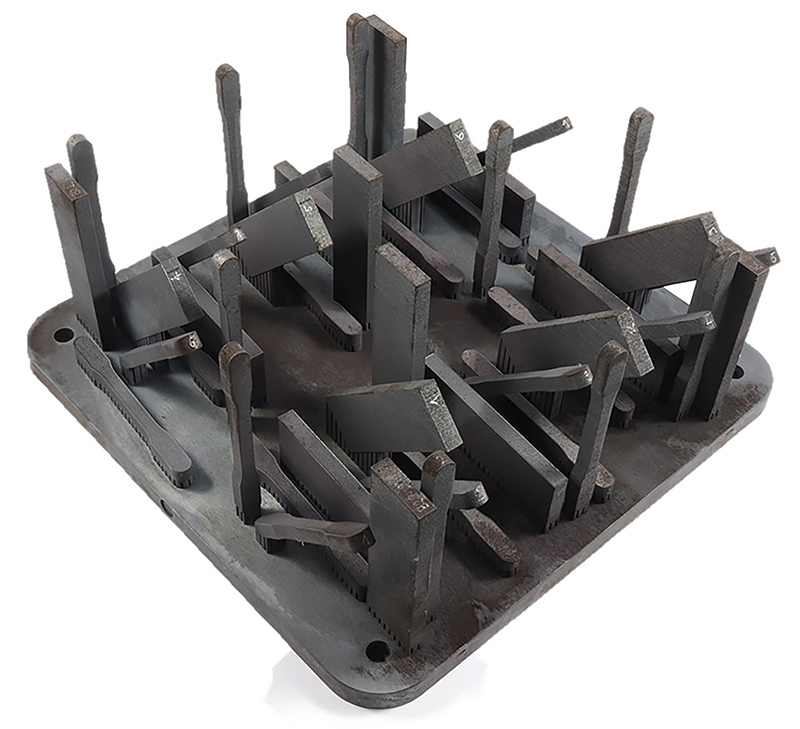
For some metal parts, controlled heat treatment reduces residual stress or adjusts the microstructure. The sequence, including treatment before or after separation from the build plate, depends on the alloy and qualified process. It guarantees neither freedom from distortion nor removal of surface contamination. Application requirements determine which properties must be verified.
High Pressure Heat Treatment (HPHT) can combine hot isostatic pressing (HIP) densification and heat treatment in one cycle. This feature reported, citing FIT AG, ranges of 15,000–30,000 psi, up to 4,000 °F and cooling rates up to 4,500 K/min. These historical indications, without an equipment reference here, are not a process recipe, necessarily simultaneous maxima, or suitable for every material. Quintus describes the HPHT principle and tailoring of cycles.
2 — Post-curing
Photopolymer resin processes may require post-curing after washing and drying. Light, heat, duration and operation sequence must follow instructions for the resin–printer combination. Some materials, including dual-cure systems, require thermal treatment: UV alone does not suit every formulation.
3- Support removal
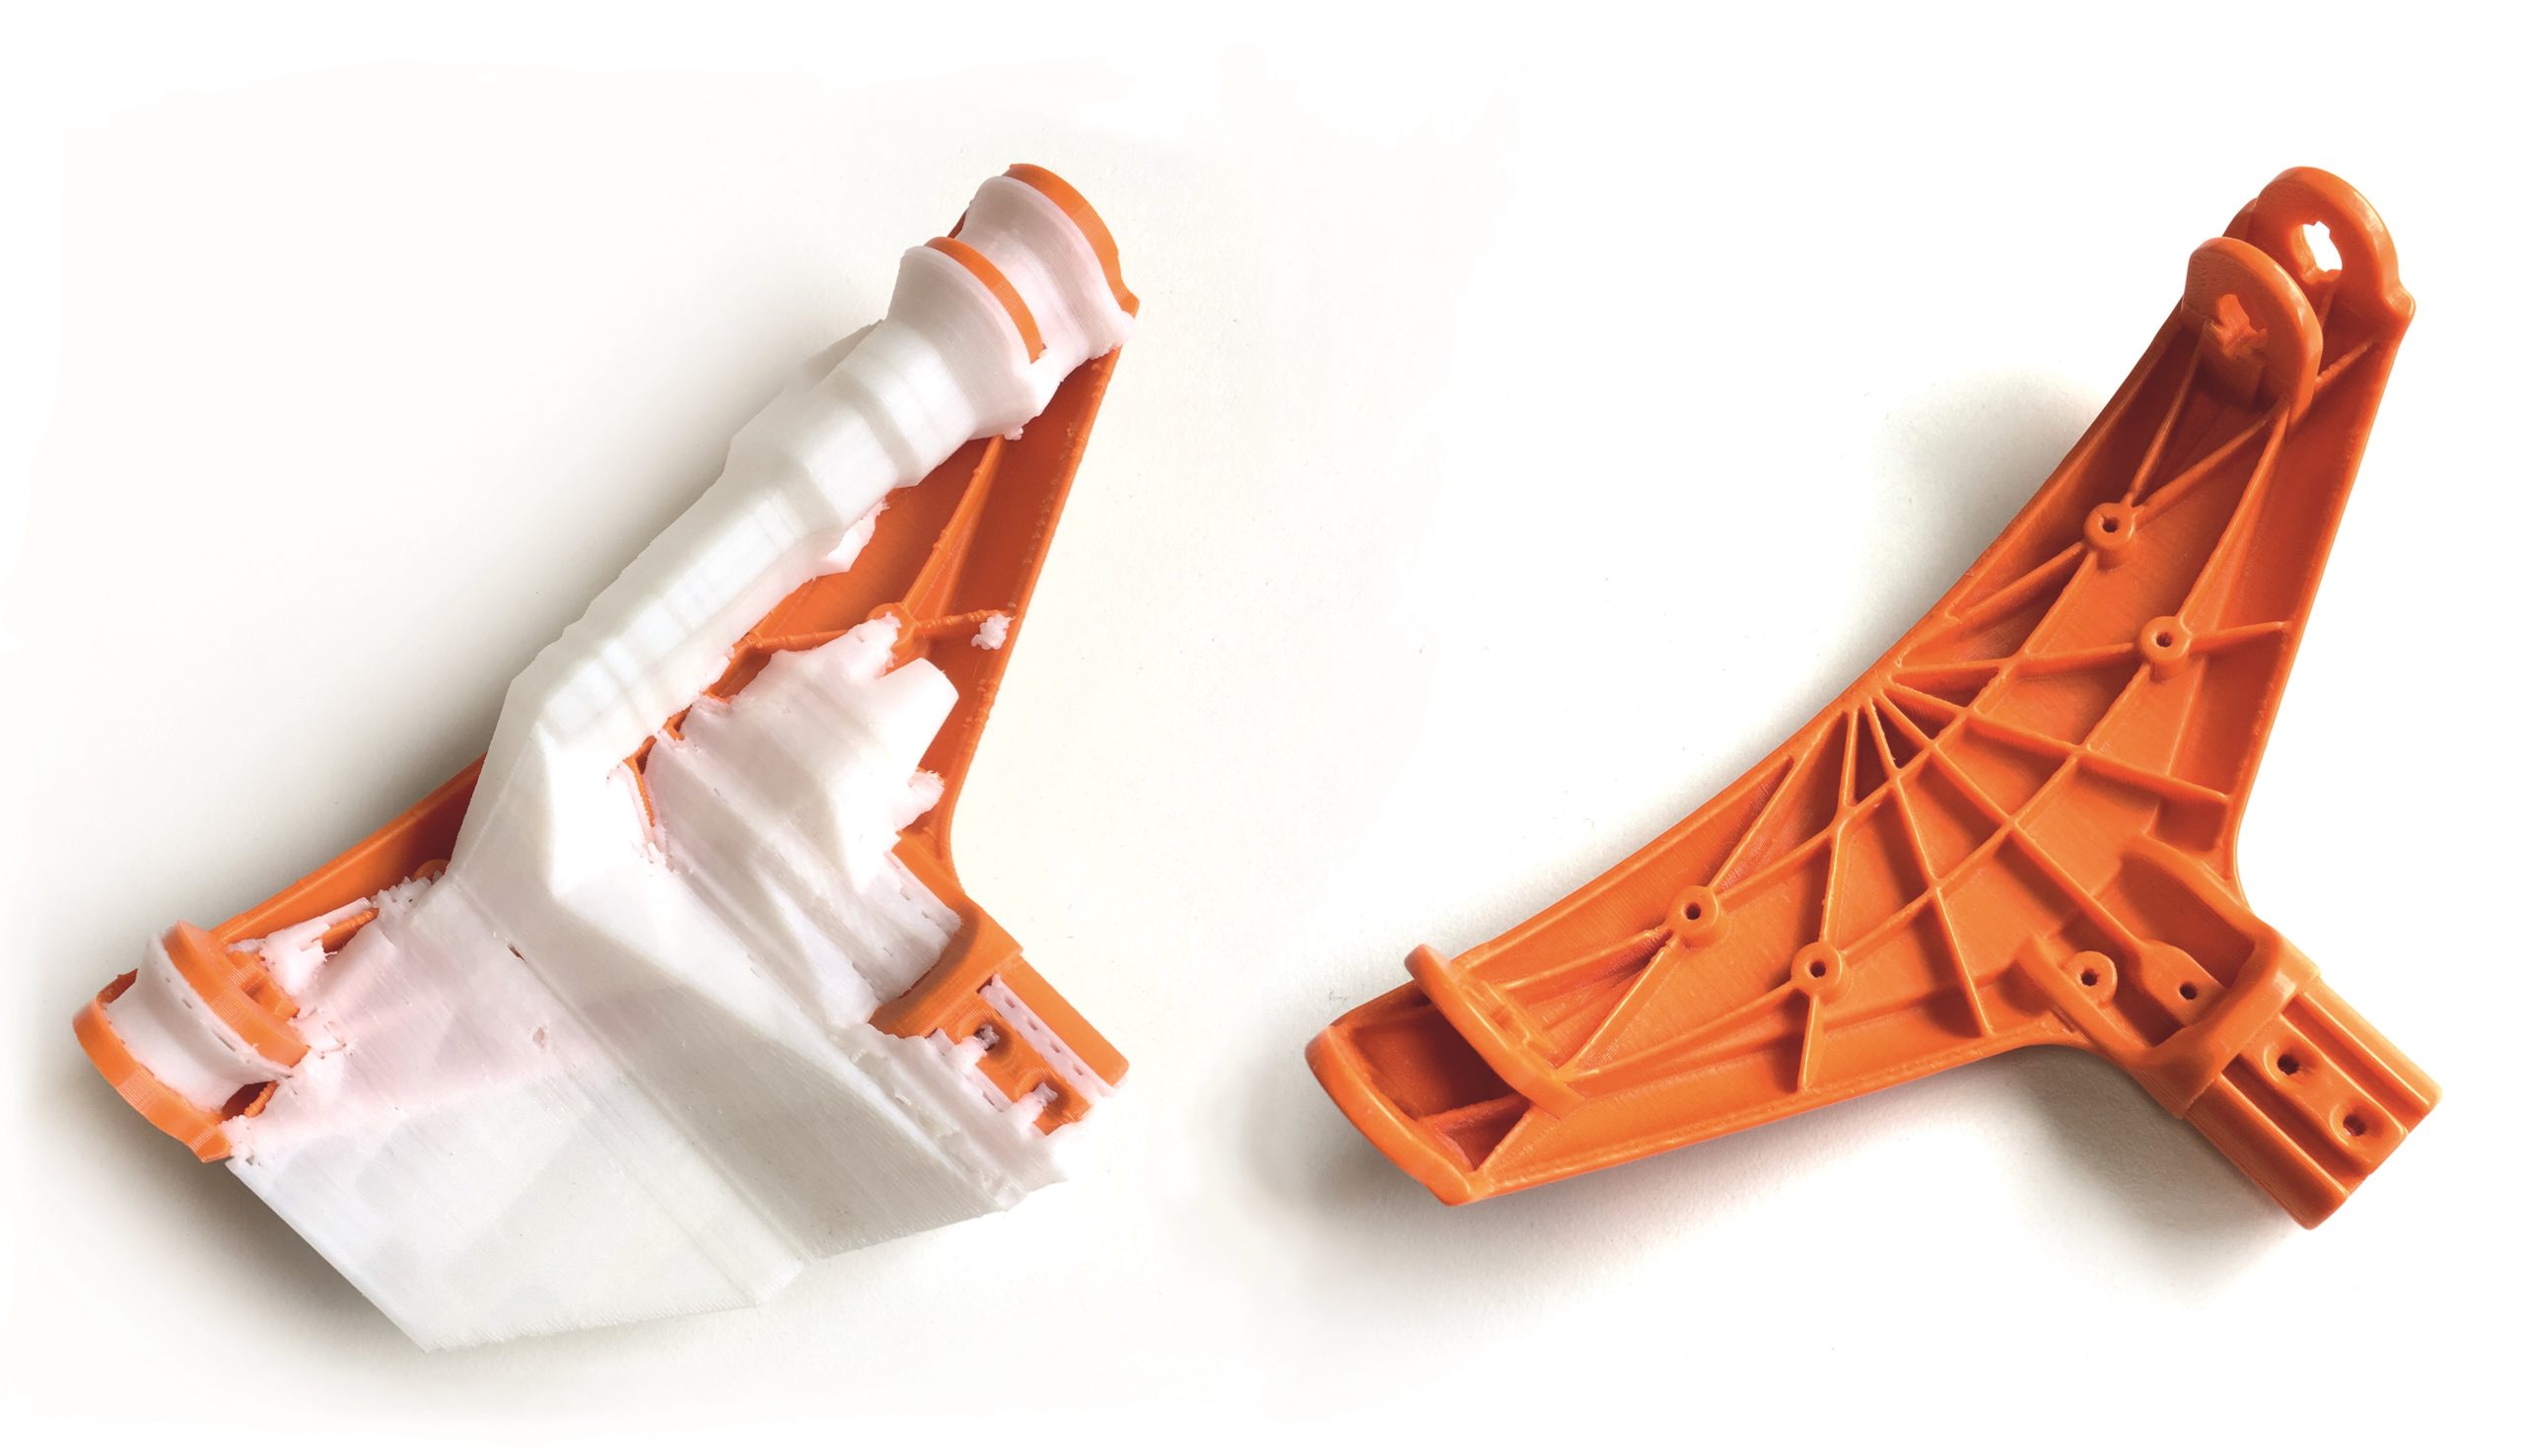
Supports used in resin printing, filament extrusion or some metal processes must be removed when they are not part of the final product. Their necessity depends on geometry, orientation and process. Removal is mechanical or, for compatible supports, by dissolution with the manufacturer-specified product. Water and limonene are not universal solutions; selection must account for the part and handling instructions. Furthermore, those who would like to reduce the manual work can opt for a more automated solution. PostProcess Technologies, for instance, a partner of AM Solutions, provides various solutions that meet the requirements of these different AM technologies: “With the “Submersed Vortex Cavitation (SVC)” technology the PostProcess systems DEMI and FORTI reliably remove supports and excess resin. For support removal of products made from filaments (FDM/FFF) PostProcess offers the DECI and BASE units using the “Volumetric Velocity Dispersion (VVD)” process”, states Manuel Laux.
4- Cleaning & depowdering
Cleaning covers various residue-removal operations. Depowdering specifically removes unconsolidated powder, including from surfaces and internal features.
Depowdering concerns powder-based processes, using metals or polymers. It follows printing and can be essential to subsequent operations. Its exact position depends on the technology and manufacturing instructions.
For a metal powder-bed-fusion part, internal channels can complicate depowdering. A brush or ordinary vacuum cleaner is not an appropriate default method: equipment must be designed for the powder and identified hazards, following its safety data sheet and manufacturer instructions. HSE has studied metal-powder exposure, including during handling and cleaning. Stress relief, separation, machining and other treatments are organised in a validated sequence; automation can reduce some manual tasks.
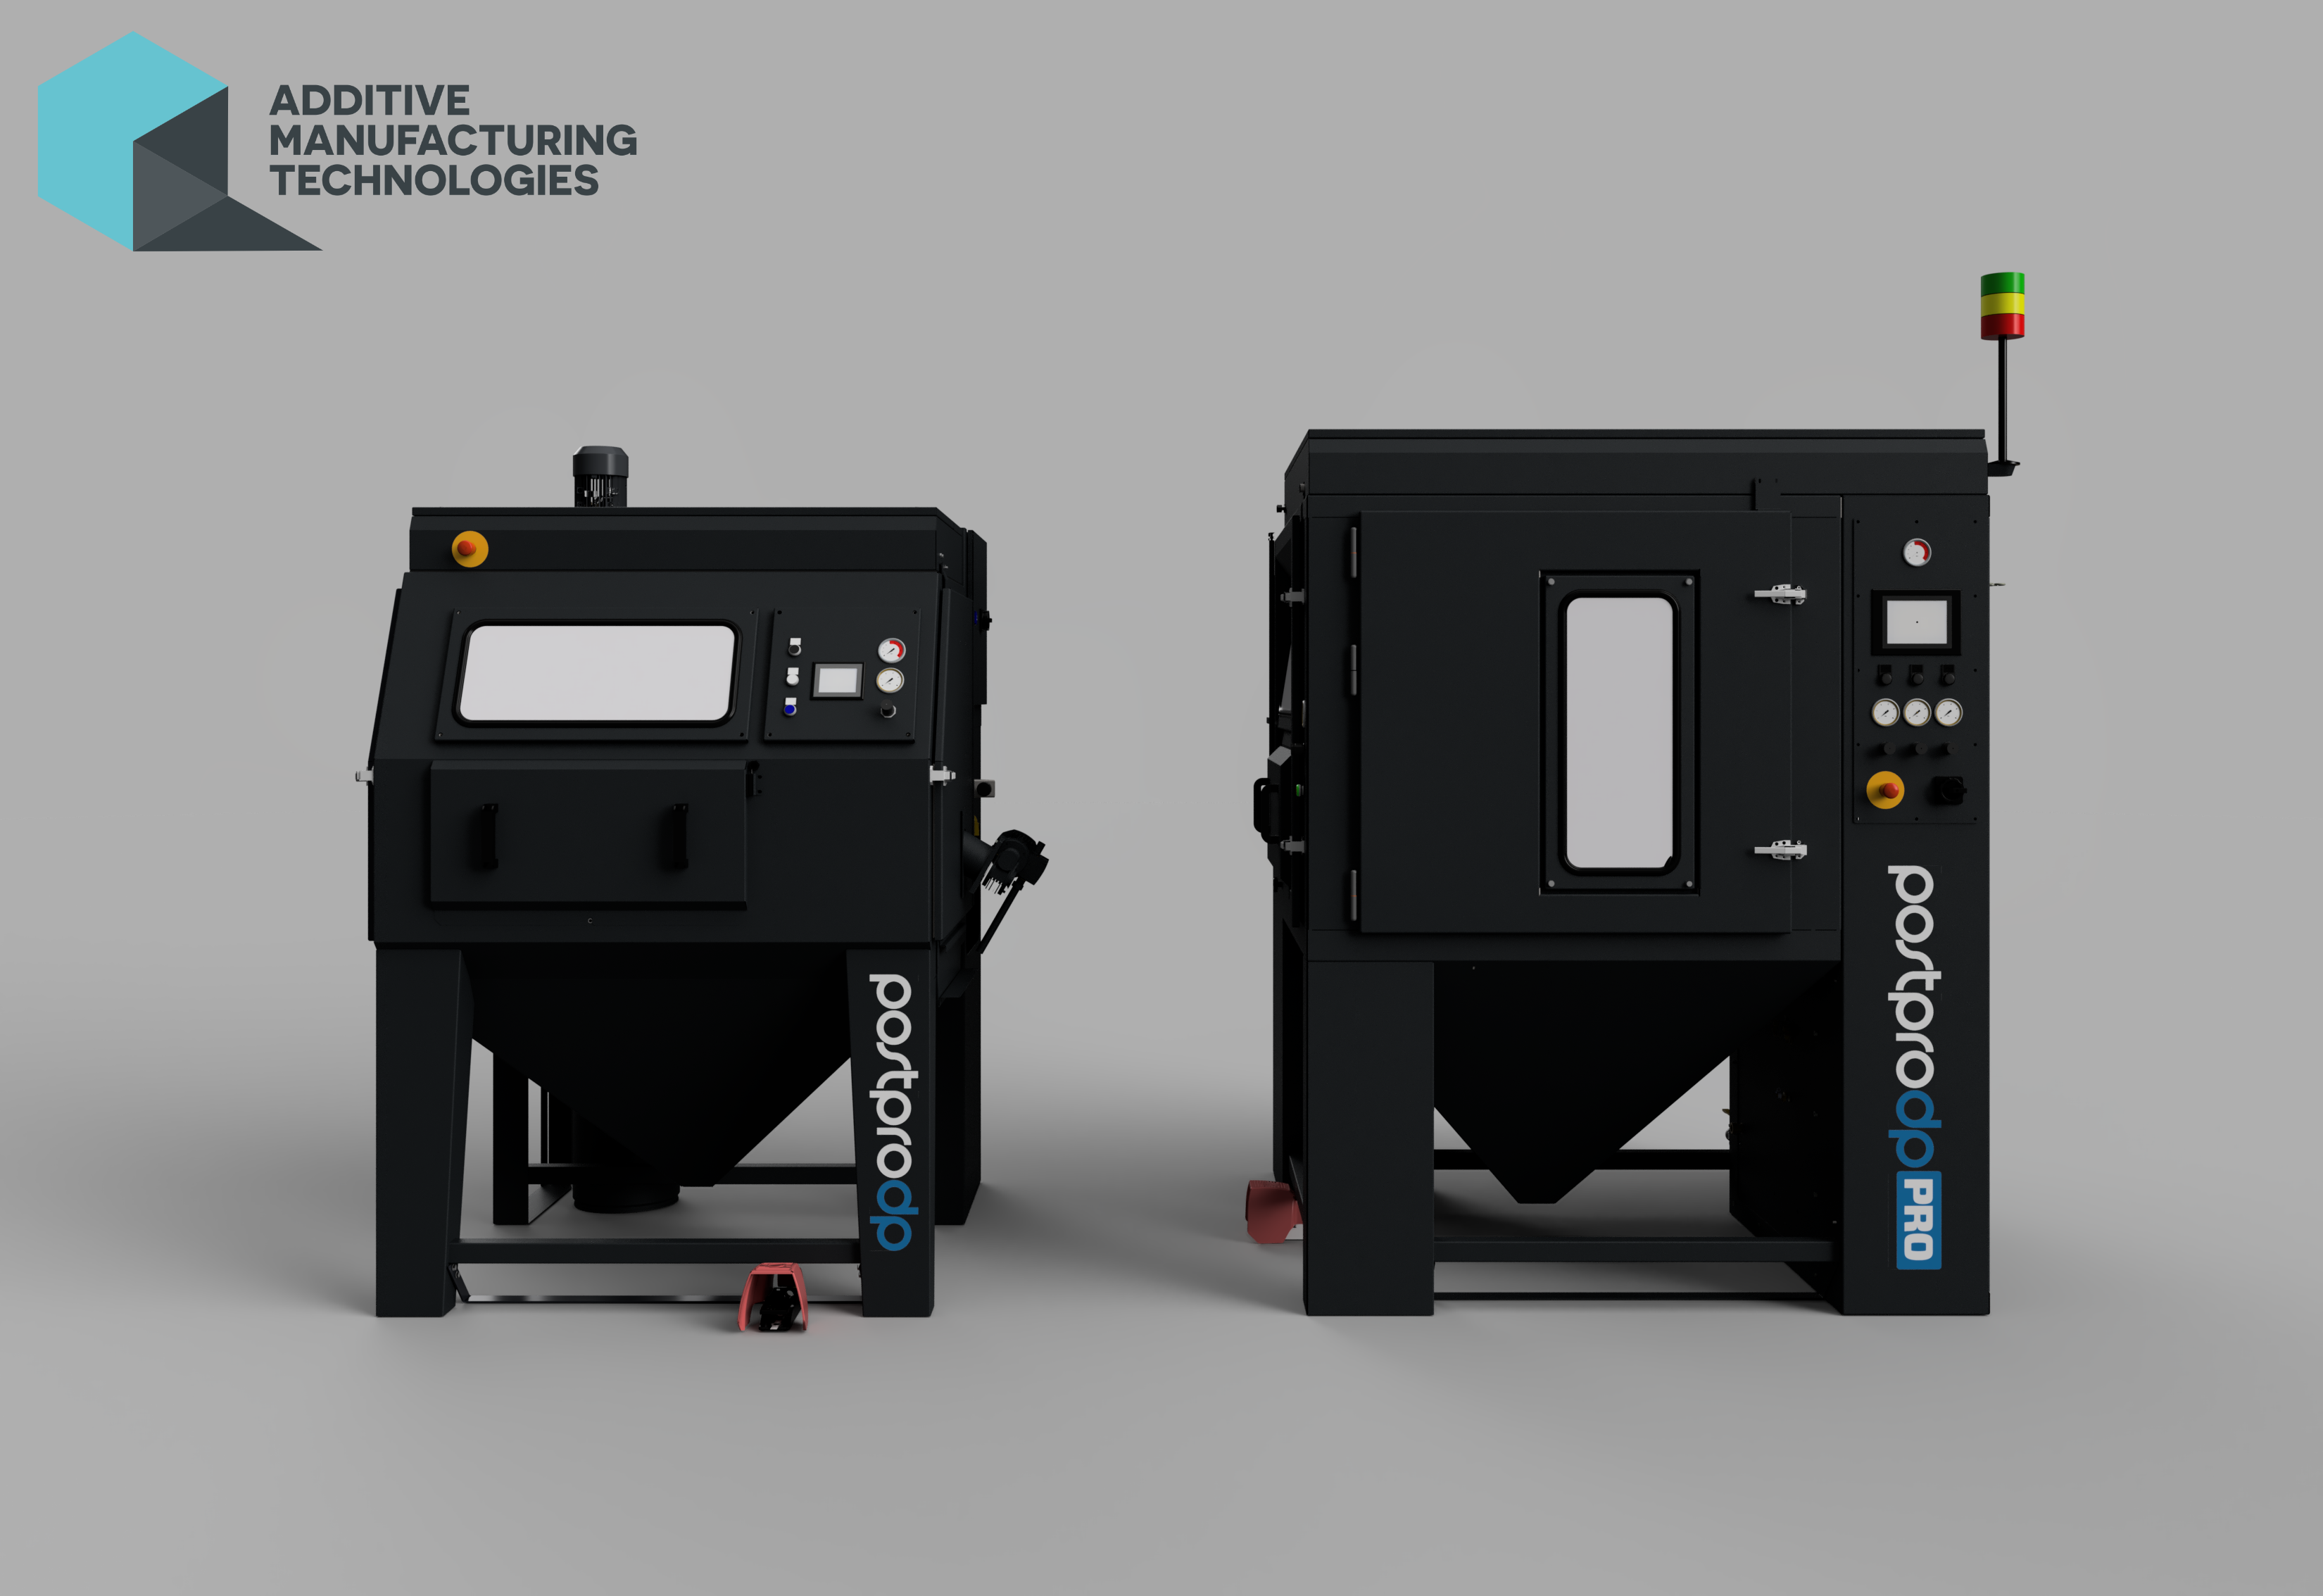
“A unique trait about AMT’s automated post-processing solutions is that all AMT’s technologies are safe and sustainable, and specifically designed for additive manufacturing, unlike other post-processing technologies on the market. Both AMT’s depowdering, PostProDP, and surface finishing, PostPro3D, technology gently finish parts on an industrial scale. Not only do AMT’s technologies improve the parts aesthetics, they also improve the part’s mechanical properties, such as elongation at break (EAB), and eliminate water and gas intake. Using smart algorithms and machine learning, AMT’s technologies are equipped with programmed recipes for each common material combination, therefore offering a truly plug and play solution”, Crabtree told 3D ADEPT Media.
The benefits and safety claims above are AMT’s. They require assessment for each material and application; automation does not replace risk assessment or validation of results.
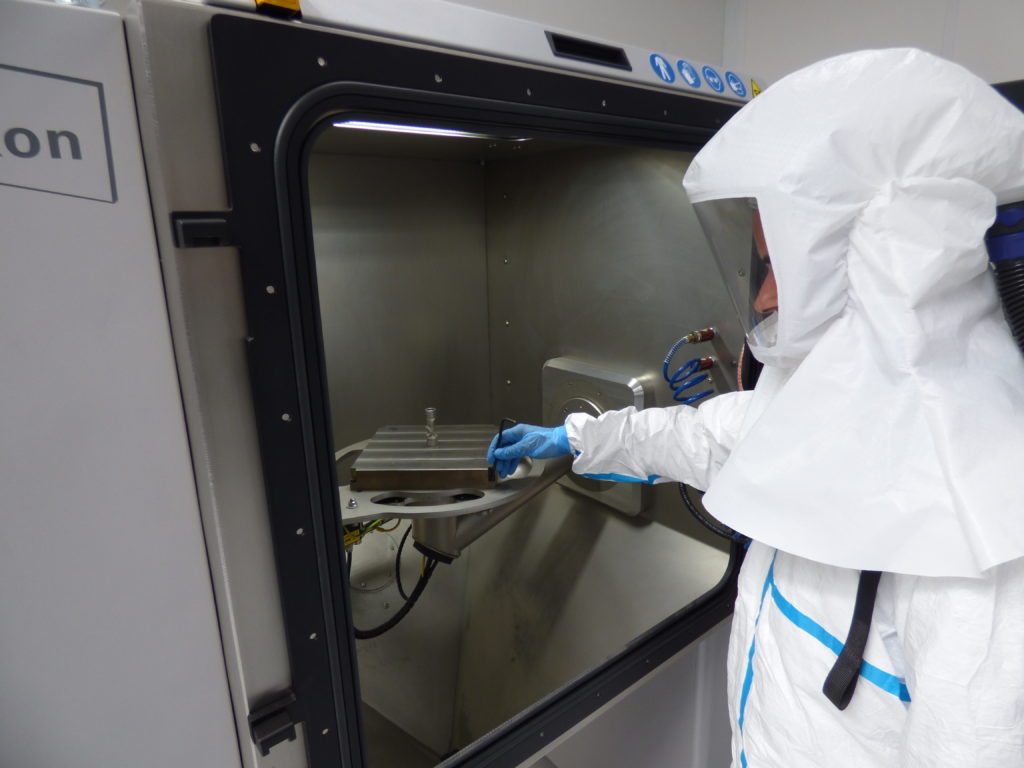
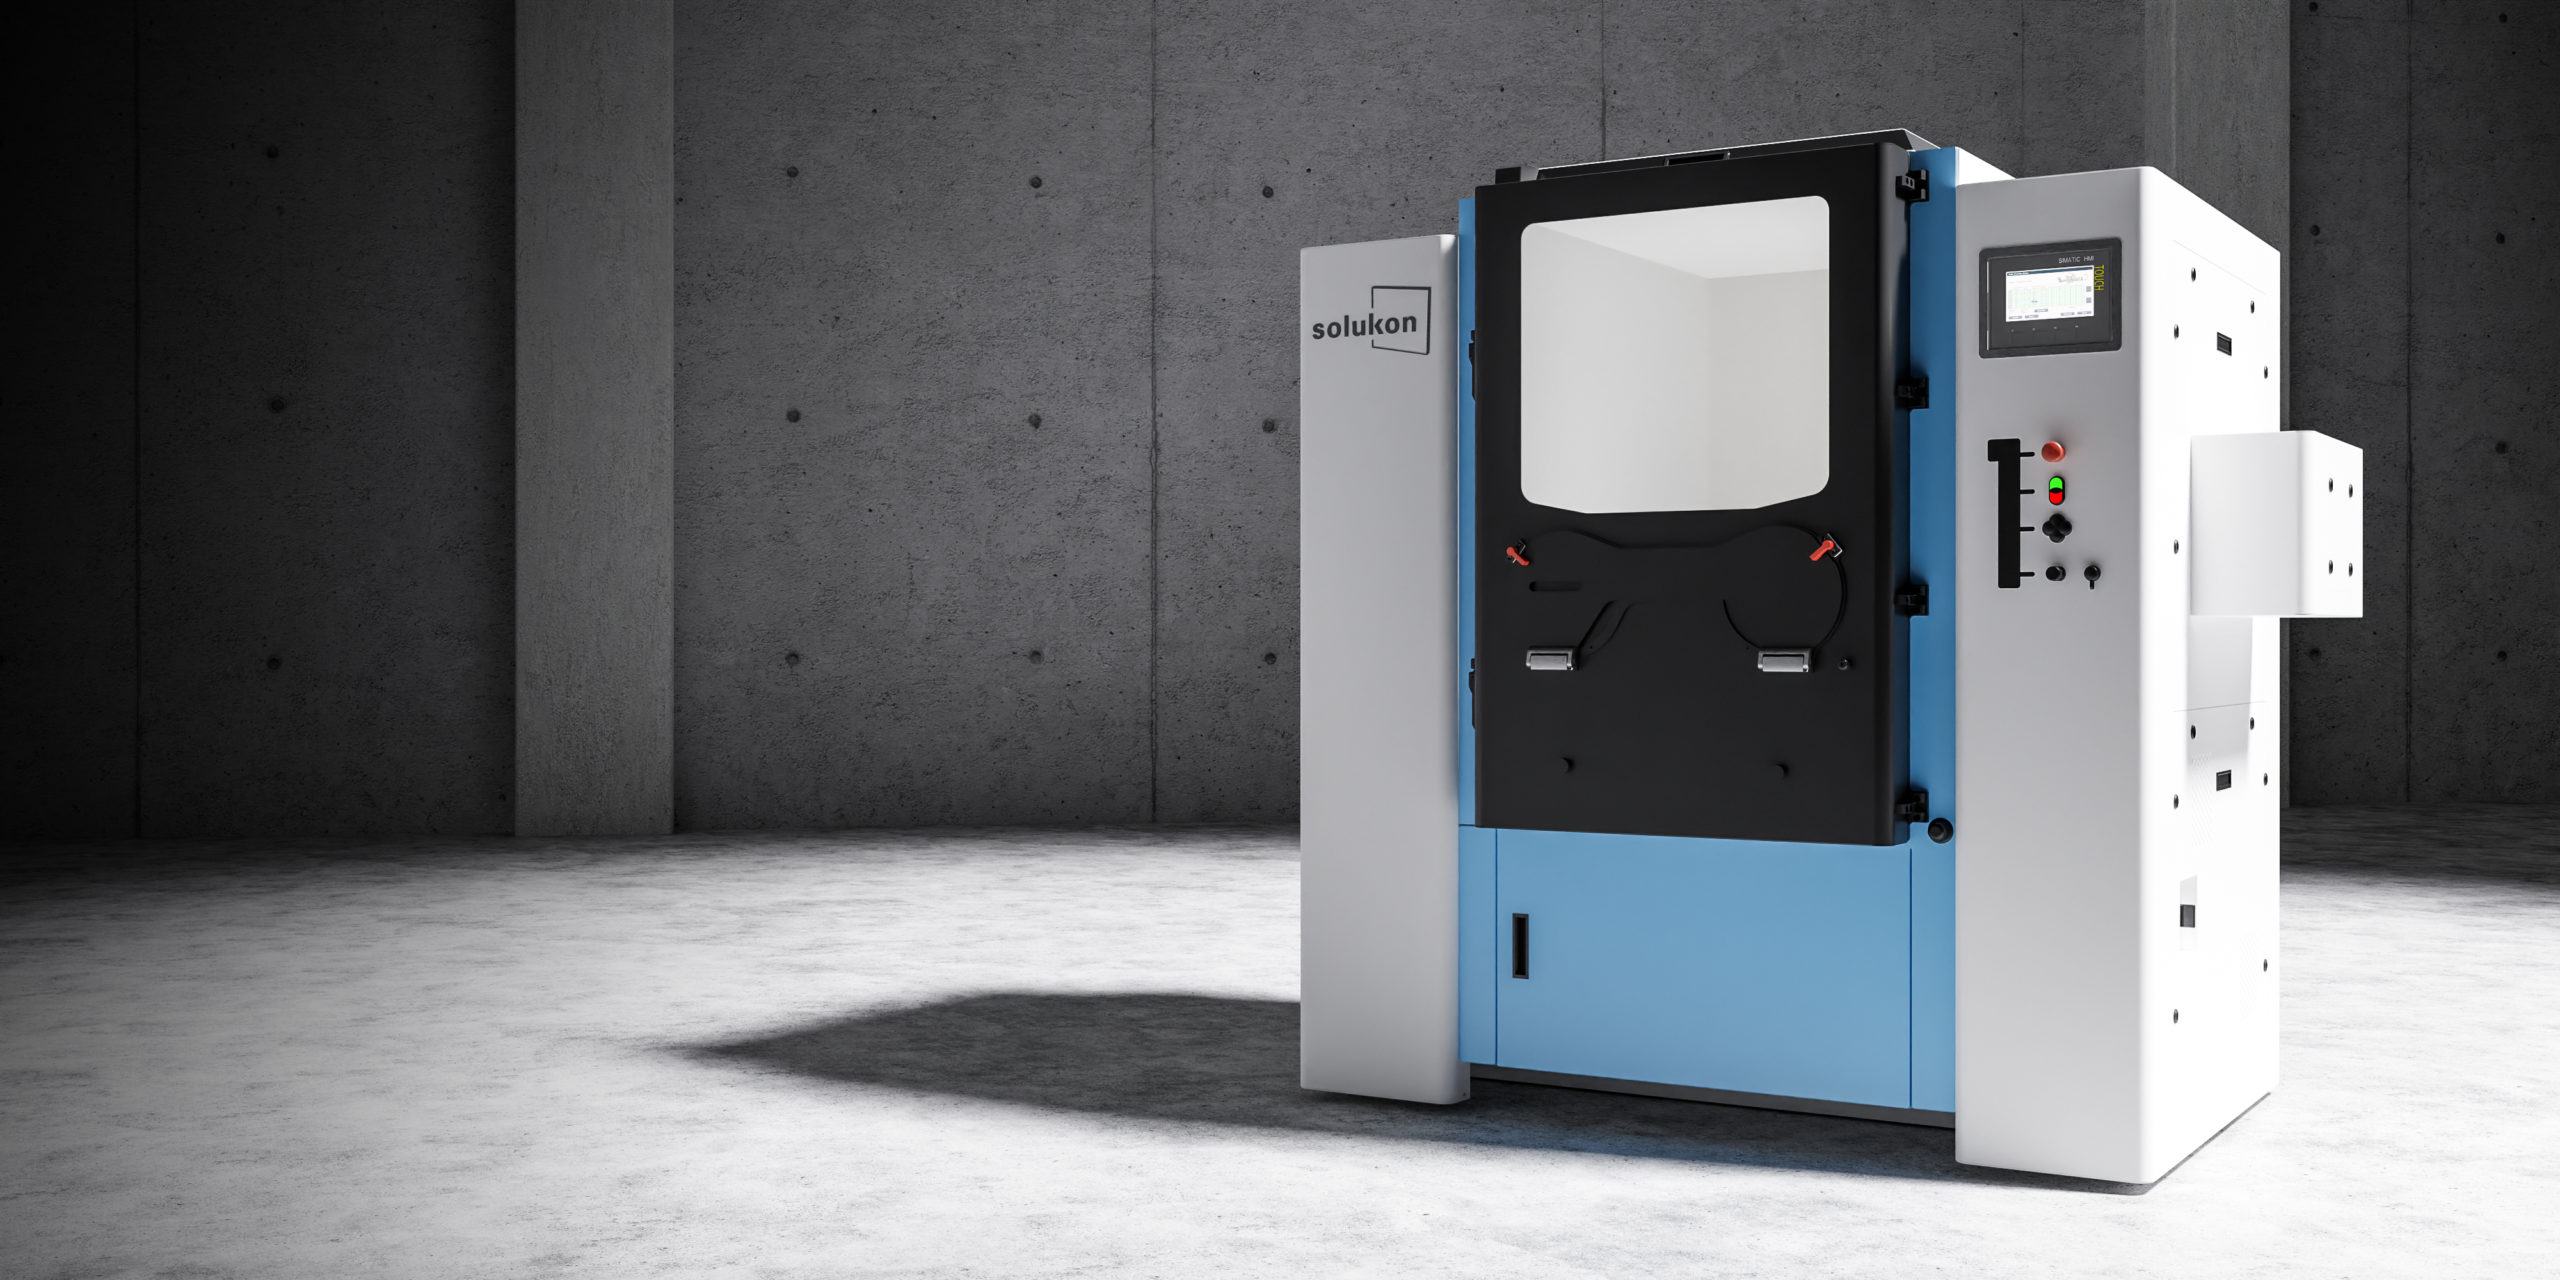
Solukon presented systems combining rotation and vibration to remove powder from metal parts. Depending on configuration, a closed chamber and controlled atmosphere help manage dust and reactive-powder hazards. Gas selection and operating conditions follow manufacturer instructions; these measures alone do not guarantee freedom from risk.
5- Surface finish processes
Depending on the application, surface finishing may include edge radiusing, smoothing and polishing.
In a surface refinement process that combines blasting and finishing systems, Laux, Head of AM Solutions, explains: “the initial surface of 3D printed parts can sometimes be quite rough with Ra readings of up to 1,000 micro inches. In such cases, it can be beneficial running the workpieces through a blasting process for an initial reduction of the surface roughness before processing them in the actual finishing system. This allows reducing the Ra values down to < 20 micro inches.”
If the operator is looking for extra smooth surfaces on metal components, AM Solutions can offer a “finishing system producing extremely fine surface finishes with Ra values of < 5 micro inches on 3D printed metal components. This is achieved with the patented DRYLITE® dry electro-polishing technology, which does not require any liquid electrolytes.”
Moreover, the term finishing designates a range of post-processing activities such as priming, filling, grinding, preparing ready for painting, deburring, etc. They are generally used as the basis for further post-processing, such as metal coating.
6- Machining
Machining can remove supports or achieve required functional surfaces, dimensions and tolerances. Allowances and tool access should be planned during design. Its necessity depends on the process and specification.
7- Coating or Infiltration
Coating adds a surface layer, whereas infiltration introduces material into a porous structure. Polymer infiltration can aim to improve sealing; tightness must be verified for the intended fluid, pressure, temperature and use.
8- Dyeing
Dyeing colours some polymer parts, including those made by SLS or MJF. Penetration, durability and uniformity depend on material and process. Appropriate manual or automated equipment can be used. Girbau was among the suppliers cited in this feature for MJF applications.
9- Inspection
Protolabs describes its measurement and inspection reports here. The company explained that the “inspection process verifies that final parts comply with the original drawing, purchase order, and other specifications. Dimensional inspection uses CMM equipment to ensure part dimensions are within tolerance and align with measurements provided in the original drawing.
Final report details location on the build plate, how the geometry was oriented, support structure placement, and a build log file detailing the entire build process from the machine.”
Dimensional inspection alone does not validate mechanical properties. Required tests and checks must be defined for the material, process and part requirements.
For DMLS parts, Protolabs cites X-ray computed tomography as a non-destructive way to inspect internal geometry, some wall-thickness variations and defects. Detection of cracks or residual powder depends on resolution, material and measurement capability: a scan does not automatically establish freedom from every defect.
Can the same post-processing technology be compatible with several types of additive manufacturing technologies?
First, it should be noted that specialists of post-processing technologies usually develop their solutions to respond to specific demand of the additive manufacturing industry. Over time, applications tend to extend their area of expertise to other technologies.
Selecting a post-processing solution requires checking compatibility with the part, material, production volume and expected outcome. Representative trials may be needed.
“A small number of post processing equipment, be it for removal of supports and residual resin, de-powdering & cleaning or surface finishing, can be used for whole groups of additive manufacturing technologies. For example, for de-powdering, cleaning and initial surface smoothing the AM Solutions S-Line equipment can be used for plastic components and in terms of metal for initial surface smoothing.
When it comes to surface finishing of the same plastic or metal components the AM Solutions M-Line equipment line is suitable”, says AM Solutions’ Manuel Laux.
Furthermore, experience in various applications might easily enable operators to determine the ideal post-processing technique for their project.
In some tooling applications, layer marks or required tolerances can justify machining functional surfaces after printing. This is not necessary for every printed tool.
Conventional polymer filaments differ from filaments containing metal powder and binder. For the latter, the printed part generally undergoes debinding and sintering using the specified system. Some metal binder-jetting processes also include these stages. Their method, detailed sequence and dimensional shrinkage cannot be inferred from a general comparison with polymer FFF.
“It’s not just about making parts look good, it’s about improving the mechanical properties of the parts for high performance.”
Serial production requires consideration of the entire chain: printing, handling, post-processing and inspection. The interviewees describe the opportunities they saw for automation in 2020.
For AM Solutions, “to a large extent, this is due to laborious post processing methods characterized by a preponderance of manual labour, use of old-style methods and lack of automation. The outcome is extremely time-consuming post-processing, inconsistent results with low throughput and very costly. Only with automated, intelligent post-processing solutions can additive manufacturing be truly integrated into industrial production lines. But automated post-processing will achieve a lot more: It will allow full usage of the printer capacities resulting in significantly reduced cycle times, an overall higher throughput and a drastically improved cost-efficiency. It will produce a consistently high quality of the post-processed components, thus significantly reducing the reject rate (less warpage & swelling due to water absorption, less breakage, etc.).
Welcome side effects of integrating automated post-processing treatments are lower work-in-process inventories, better workpiece traceability and higher workplace safety (manual de-powdering can be hazardous).”
“To scale post-processing safely and sustainably, new technology development and automation are key. It’s not just about making parts look good, it’s about improving the mechanical properties of the parts for high performance”, adds AMT.
Collaboration among printer manufacturers, post-processing suppliers and users helps define a coherent workflow. Selection should be based on part requirements, trials and total cost, rather than a promise of universal automation.
This dossier was initially published in the May / June 2020 issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.