

Feature first published in the January/February 2023 issue, with contributions from Tobias Stittgen (ponticon), Matt Petros (3DEO) and Tracy Beard (Quickparts). Examples concern particular processes whose results depend on material and application.
Whether it is light or cheap, a 3D printed part delivers value when it performs well. The thing is, achieving that performance often begins and ends at the surface. Ensuring the right surface of the 3D printed part often comes down to the right post-processing task. In our efforts to demystify every post-processing task that can be used at the end of the additive production, we’ll focus on infiltration and coating processes in this article.
Post-processing includes operations performed after printing to achieve required characteristics: removing residual material, consolidation, surface modification or adding functions. It is not limited to removing defects.
Among the various post-processing tasks that can be performed on 3D printed parts, we already studied the use of furnaces, heat treatment, and metal powder removal in previous editions of 3D ADEPT Mag.
Infiltration and coating are different operations. A coating adds a layer at the surface; infiltration introduces another phase into a porous network. Some treatments combine effects, and terminology varies across materials and processes.
We did our homework, we talked to industry experts and conducted some research to clarify each of those terms and the way they should be utilized in an additive manufacturing production.
Coating
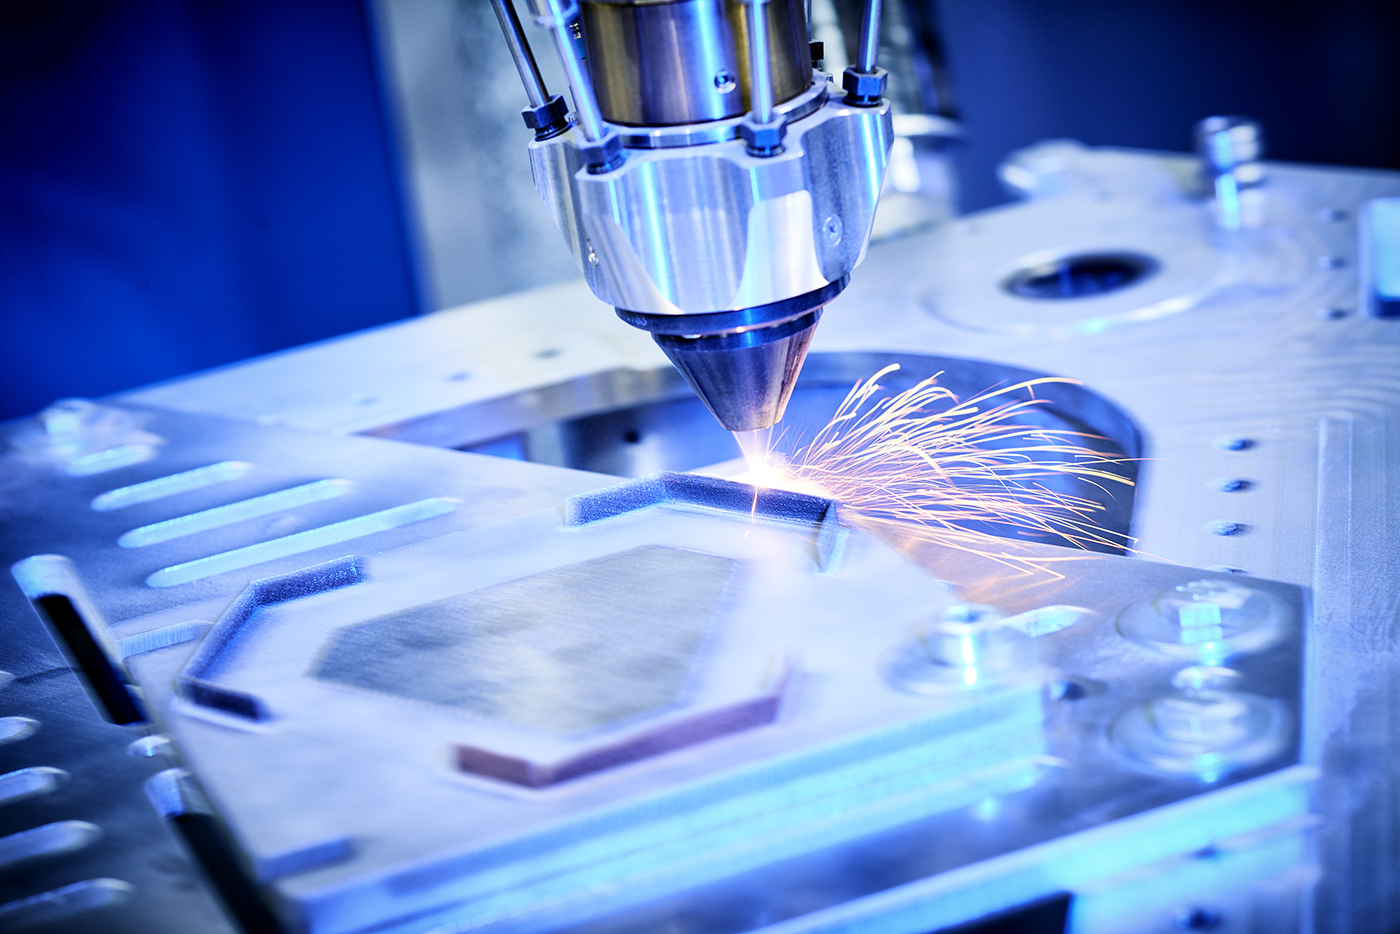
Coating is a word that is widely used in AM: Surface coatings, Additive Manufacturing Coatings, Coating for AM parts, Dry powder coating, Cold spray coating etc. Simply put, a coating is a layer of a substance added to a surface to provide protection and to enhance the appearance of the surface.
“According to our understanding, [it] is a manufacturing process to refine both conventionally and additively manufactured metal parts. The purpose of a coating is to protect a part from harms caused by the characteristics of its operating environment (e.g. high temperature, high humidity, presence of chemicals, mechanical stresses etc.)”, Dr. Ing. Tobias Stittgen, Managing Director at ponticon states. ponticon develops high-speed directed energy deposition (DED) systems for manufacturing and coating. Their use depends on compatibility between the deposited material, substrate and part geometry.
In general, to refine metal parts, operators often apply a layer of material onto the substrate to enhance the parts’ surface properties. As Stittgen implies, choosing a coating often depends on what is affected in the operating environment. It also depends on life expectancy, substrate material compatibility, component shape and size, and obviously price.
Furthermore, while coatings can be considered for different metal AM processes, it should be noted that “protective properties are better achieved with materials that differ from the actual part’s material. As the coating materials are often high-value, manufacturing the entire part is economically unviable”, Stittgen notes.
The families below distinguish deposition mechanisms from surface modification. They are not four equivalent deposition methods: some treatments modify the substrate without adding a distinct coating. Selection requires checking compatibility with the part and intended use.
| Family | Examples |
|---|---|
| Atomic-scale deposition | Electrolytic deposition, PVD, CVD, some plasma-assisted deposition processes |
| Particle deposition | Thermal spraying, impact plating, enamelling, electrophoresis |
| Bulk coating or cladding | Painting, dipping, laser cladding, weld overlays, roll bonding |
| Substrate modification | Anodising and conversion treatments |
Table adapted from TWI’s overview of surface engineering. See principles and selection considerations.
Mechanical and thermal surface treatments offer other approaches, including shot peening, laser treatment, friction-stir processing and mechanical impact or rolling treatments. Their effects need assessment for the material concerned.
These methods are often the least highlighted in the additive manufacturing of a part – probably because some of them are still being explored at the research level. However, it is important that manufacturers keep track of their influence on the surface quality of AM components to better assess innovations at the production and performance levels.
Infiltration
Infiltration is used in some manufacturing routes, including porous binder-jetted parts. It is neither mandatory for all metal binder jetting nor limited to two AM processes. Consolidation may use sintering alone or combine several stages depending on material and target properties.
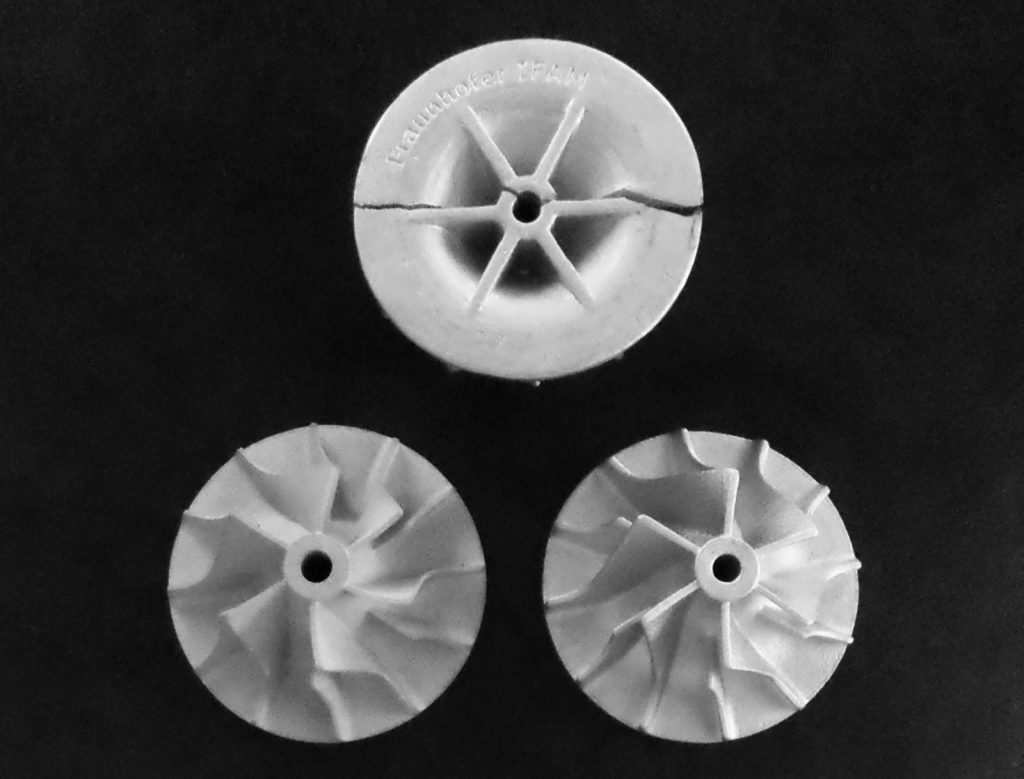
A green part contains particles and binder. Debinding removes the binder using an appropriate cycle; sintering develops bonds between particles and densifies the part. Final density and shrinkage depend on formulation, cycle and geometry. One should not assume a temperature always “just below” melting or negligible final porosity.
As per the words of 3DEO’s CEO Matt Petros, infiltration comes into play for two main reasons: “the full densification is not possible solely through sintering and high-temperature sintering can introduce extreme dimensional distortion to the part – [the ultimate goal being to improve part density]”. In case you’re not familiar with them, 3DEO is a machine manufacturer and a parts producer that provides manufacturing services based on a proprietary Intelligent Layering® technology. We have been following the company for a couple of years now and their expertise has helped us understand more than once many of the rules AM breaks. In this specific case, 3DEO does not use infiltration as a consolidation step. In their process Intelligent Layering®, the parts are sintered to full density.
Petros is describing cases where sintering alone does not achieve the intended result, not a limitation shared by every process. Intelligent Layering performance is reported by its manufacturer.
How does metal infiltration work?
In a metal-infiltration route, debinding and any pre-sintering leave an accessible porous network. A lower-melting metal can fill this network through capillary action. Density values depend on the system used; figures such as 60% or 90% are not universal thresholds.
Speaking of a specific process named liquid-metal Infiltration which can be employed as a post-sintering step to produce a fully-dense part, 3DEO’s CEO explains that “after binder removal, a low temperature sintering step is performed to initiate necking of the metal particles. This lightly sintered part will act as a frame for the liquid-metal to fill. A lower melting-temperature infiltrant is melted and diffused into the porous network of the part via capillary action.”
One of the advantages of this process, according to Petros, is the fact that one avoids “extreme dimensional distortions in the part after high-temperature sintering. Any open pores within the part are filled, bolstering its mechanical properties and structural integrity.”
Shrinkage is not a fixed 2%: it varies with material, geometry and processing cycle. Mechanical properties and residual porosity require assessment on the resulting part.
“One of the biggest drawbacks of infiltration is the heterogeneous nature of infiltrated metal parts. Infiltrated metal parts will exhibit properties that are difficult to predict due to the part being a composite of two different materials. Other disadvantages include increased processing time due to the additional steps required for infiltration” Petros adds.
Sintering aids or hot isostatic pressing (HIP) can be considered for some consolidation routes. Petros cites HIP as a way to approach theoretical density. These options are not interchangeable and require compatible porosity, composition and processing conditions.
While infiltration is mostly highlighted in the manufacturing of parts through metal binder jetting, it should be noted that this post-processing step has a different meaning and understanding for those working with SLS 3D printing.
For SLS polymer parts, impregnation may target sealing or colour changes. Dyeing alone does not guarantee leak-tightness, pressure resistance or protection against all contaminants.
Tracy Beard from 3D printing service bureau Quickparts explains that this post-processing method is mainly used to seal or color SLS parts. To do so, they use a vacuum impregnation process when parts need to be watertight. When a color other than the natural color of the SLS powder is required, they infiltrate or impregnate the parts with dye.
The infiltration process continues to be studied in conjunction with various thermal treatments to increase the strength and decrease the volatile content of the parts. Just like we saw with coating, highlighting their influence on the surface quality of AM components will help to better assess innovations at the production and performance levels.
This article was first published in the January/February 2023 issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.