

Archive — September 2019 feature with contributions from EOS, Solukon and Rösler. Equipment, trials and figures refer to that period.
With contributions from EOS, SOLUKON & RÖSLER
Depowdering removes unconsolidated material left around or inside a part made using powder. Difficulty depends on geometry, material and process. This feature examines powder recovery, safety and automation at this stage.
That’s the reason why we have decided to tackle this issue. In order to fully analyze the outlines of a powder removal process, we invited players that manufacture additive manufacturing systems, manufacturers of post-productions technologies and 3D printing service providers in order to have a user point of view in post-production technologies. Eduardo Alonso, Regional Manager France, EOS, Vincent Raman, specialist of Mass Finishing Technology at Rösler and Andreas Hartmann, Co-founder and technical director of Solukon share their respective expertise in this dossier. Other conversations and analyses from various experts including Lawrence Livermore National Laboratories will be brought throughout the dossier to highlight or give further precisions on some points.
Rösler is a surface finishing supplier that offers two essential finishing technologies, mass finishing and shot blasting, as well as industrial washing systems and in-house production and development. Due to the fact that a 3D printed part manufactured using DMLS, EBM, FDM, PolyJet, SL, SLM and SLS often comes out with corners, edges, burrs and rough spots, grinding, smoothing and polishing technologies of mass finishing are supplied by Rösler to enable manufacturers to get the expected rendering. In 2018, the company partnered with PostProcess, another specialist in post-production technologies to complete its portfolio.
EOS is a manufacturer of industrial 3D Printing systems. Founded in 1989, the company provides a wide range of holistic solutions in additive manufacturing. Their participation in this dossier is quite atypical to the extent that they often discuss powder removal as part of the general topic powder process or material management.
Lastly, Solukon is a German manufacturer of peripheral post-processing equipment for additive manufacturing technologies. The company lays emphasis on automatic depowdering units and unpacking stations for laser-melted metal and plastic parts.
The post production stage consists in a series of additional manufacturing processes such as heat treatment to achieve desirable properties. The removal of excess powder from the internal cavities and complex geometries of the printed parts is a crucial part of this stage. The lack of accurate skills regarding this stage of the AM process often results in outsourcing the postprocessing stage to achieve better results for the finished part. This might therefore explain the fact that single-source production of high-value functional AM parts remains out of reach for several manufacturers, in addition to the multiple steps the manufacturing requires.
Depowdering is needed after powder-bed processes including fusion and binder jetting. Binder jetting bonds particles during deposition rather than melting them; subsequent treatment is separate. Powder-fed directed energy deposition has other collection requirements and does not necessarily bury the part in a powder bed. This feature focuses on residual powder and hard-to-access cavities.
Challenges encountered during a metallic powder removal process
After a metal powder-bed process, unconsolidated powder can remain in channels or on surfaces. Removal and verification should be considered during design and process planning. Risks depend in part on material composition, fineness and reactivity.
Lengthy or difficult-to-repeat manual depowdering can limit throughput. Automation aims to reduce that constraint but needs assessment using the geometries actually manufactured.
Although Vincent Raman from Rösler explains that AM systems provide solutions for surface treatment & support removal, Eduardo Alonso on his side adds that “the main challenge is getting the powder completely out of the part, especially out of channels and small spaces where it is more difficult. Another important point is worker safety meaning to minimize powder contact during removal.”
Moreover, according to an expert from Lawrence Livermore National Laboratories “another challenge is being able to tell when all the powder has been removed” on the one hand,
on the other hand, as per Andreas Hartmann’s words, to “remove residual powder safely, efficiently, economically, with reproducible cleaning results and providing the residual powder contamination free for recycling.”
The first observation is that these challenges may vary from one user or manufacturer to another because of the type of removal processes they use.
Types of current removal processes
This feature distinguishes manual operations, automated dry processes, and some immersion or ultrasonic cleaning methods. These categories overlap and require compatibility checks for the powder, part and equipment. Open-air blowing can disperse dust. INRS guidance recommends suitable extraction or wiping for workstation cleaning, with equipment selected for chemical, fire and explosion risks.
For final part cleaning, INRS ED 144 limits blowing to a sealed enclosure held under negative pressure by extraction. This must not be confused with open workstation blowing.
Although it is referred by others as time-consuming, EOS believes that the “manual process is usually fully flexible because it can be done at any time on any 3D printing machine.” This would certainly be the biggest advantage of this process. However, in the constant quest for rapidity, the company also recognizes the importance of automation in post-processing. Indeed, Eduardo Alonso states that “the automation of the powder removal process is in pilot testing at EOS and selected pilot customers: automation in order to remove the majority of the powder for instance by rotating the exchangeable within the 3D printing system frame by 180° or by a robotic arm with a suction nozzle.”
Immersion cleaning and support dissolution are distinct from dry depowdering. XJet NanoParticle Jetting deposits particle-containing inks and a soluble support material. Washing removes that support; it is not loose-powder removal from a powder bed.
A water-based process is not automatically hazard-free. Compatibility of materials, cleaning products and residue handling needs assessment for the operation concerned.
Speaking of the liquid immersion process, Vincent Raman said “the liquid immersion removes support structures for different print techniques in both large batches but also on a single piece, without manually action needed.” However, for the Mass Finishing Technology specialist, “a lot of customers use a shot-blasting process which requires a lot of manual labor most of the times, hence the automation feature that Rösler integrated for smaller parts.”
Ultrasonic cleaning uses cavitation in a bath to dislodge residues. Effectiveness and compatibility depend on the part, liquid and material. Recovered powder should not be considered reusable without suitable checks; liquid contact can complicate recovery.
Solukon co-founder Andreas Hartmann compares these approaches in the 2019 interview:
“At first sight manual processes don´t need much know how and can be performed by using blowing or brushing devices. But looking at it closely, manual powder removal is very risky as the operator unavoidably comes into contact with particulate matter.
This metal material is very fine, and is light enough to be airborne in many cases. It is generally harmful to health and there is a risk that it may enter the body via the respiratory tract or through the skin. If the powder is released into the air it can create clouds of dust that may result in a dangerously explosive atmosphere.
At the same time, manual powder removal is also time-consuming, and the cleaning results are unpredictable with variable reproducibility compromising the quality.
All these factors carry risks for health, safety, quality and high costs.
Liquid immersion works very well for cleaning surfaces without leaving a residue but the parts should be pre-cleaned with a dry process as residual powder which often raises issues when internal channels are full of powder.
The powder gets stuck and the part is damaged. Ultrasonic can be very helpful but clogged channels are also here possible.
In general, when using immersion, the residual powder cannot be reused and has to be disposed.
Immersion with chemical solvents or electro chemical pulse methods-are perfect solutions as they can remove support structures and improve the part surfaces.
But also, in this case it is helpful to remove most of the powder in a dry process as the powder cannot be reused.”
Equipment may combine vibration, rotation and enclosed collection. Selection depends on geometry, channel access and powder properties. An ordinary vacuum or cleaning device is not necessarily suitable for metal dust.
A close look at each company’s technique to remove metallic powders during a post-production process
EOS
As announced earlier, the German manufacturer EOS provides a whole system for powder management. Called, IPCM M pro, it enables to convey out of the AM system, material that is not fused during the building process– without opening the process chamber door and therefore without the operator coming into direct contact with the material.
“A vacuum pump conveys the powder out of the system and into the IPCM M pro, where it is sieved under inert gas within the module at a throughput of 120 kilograms of material in 30 minutes – 50 percent faster than previous solutions. Powder treated in this way can be used for a new building process, the powder cycle starts anew.”
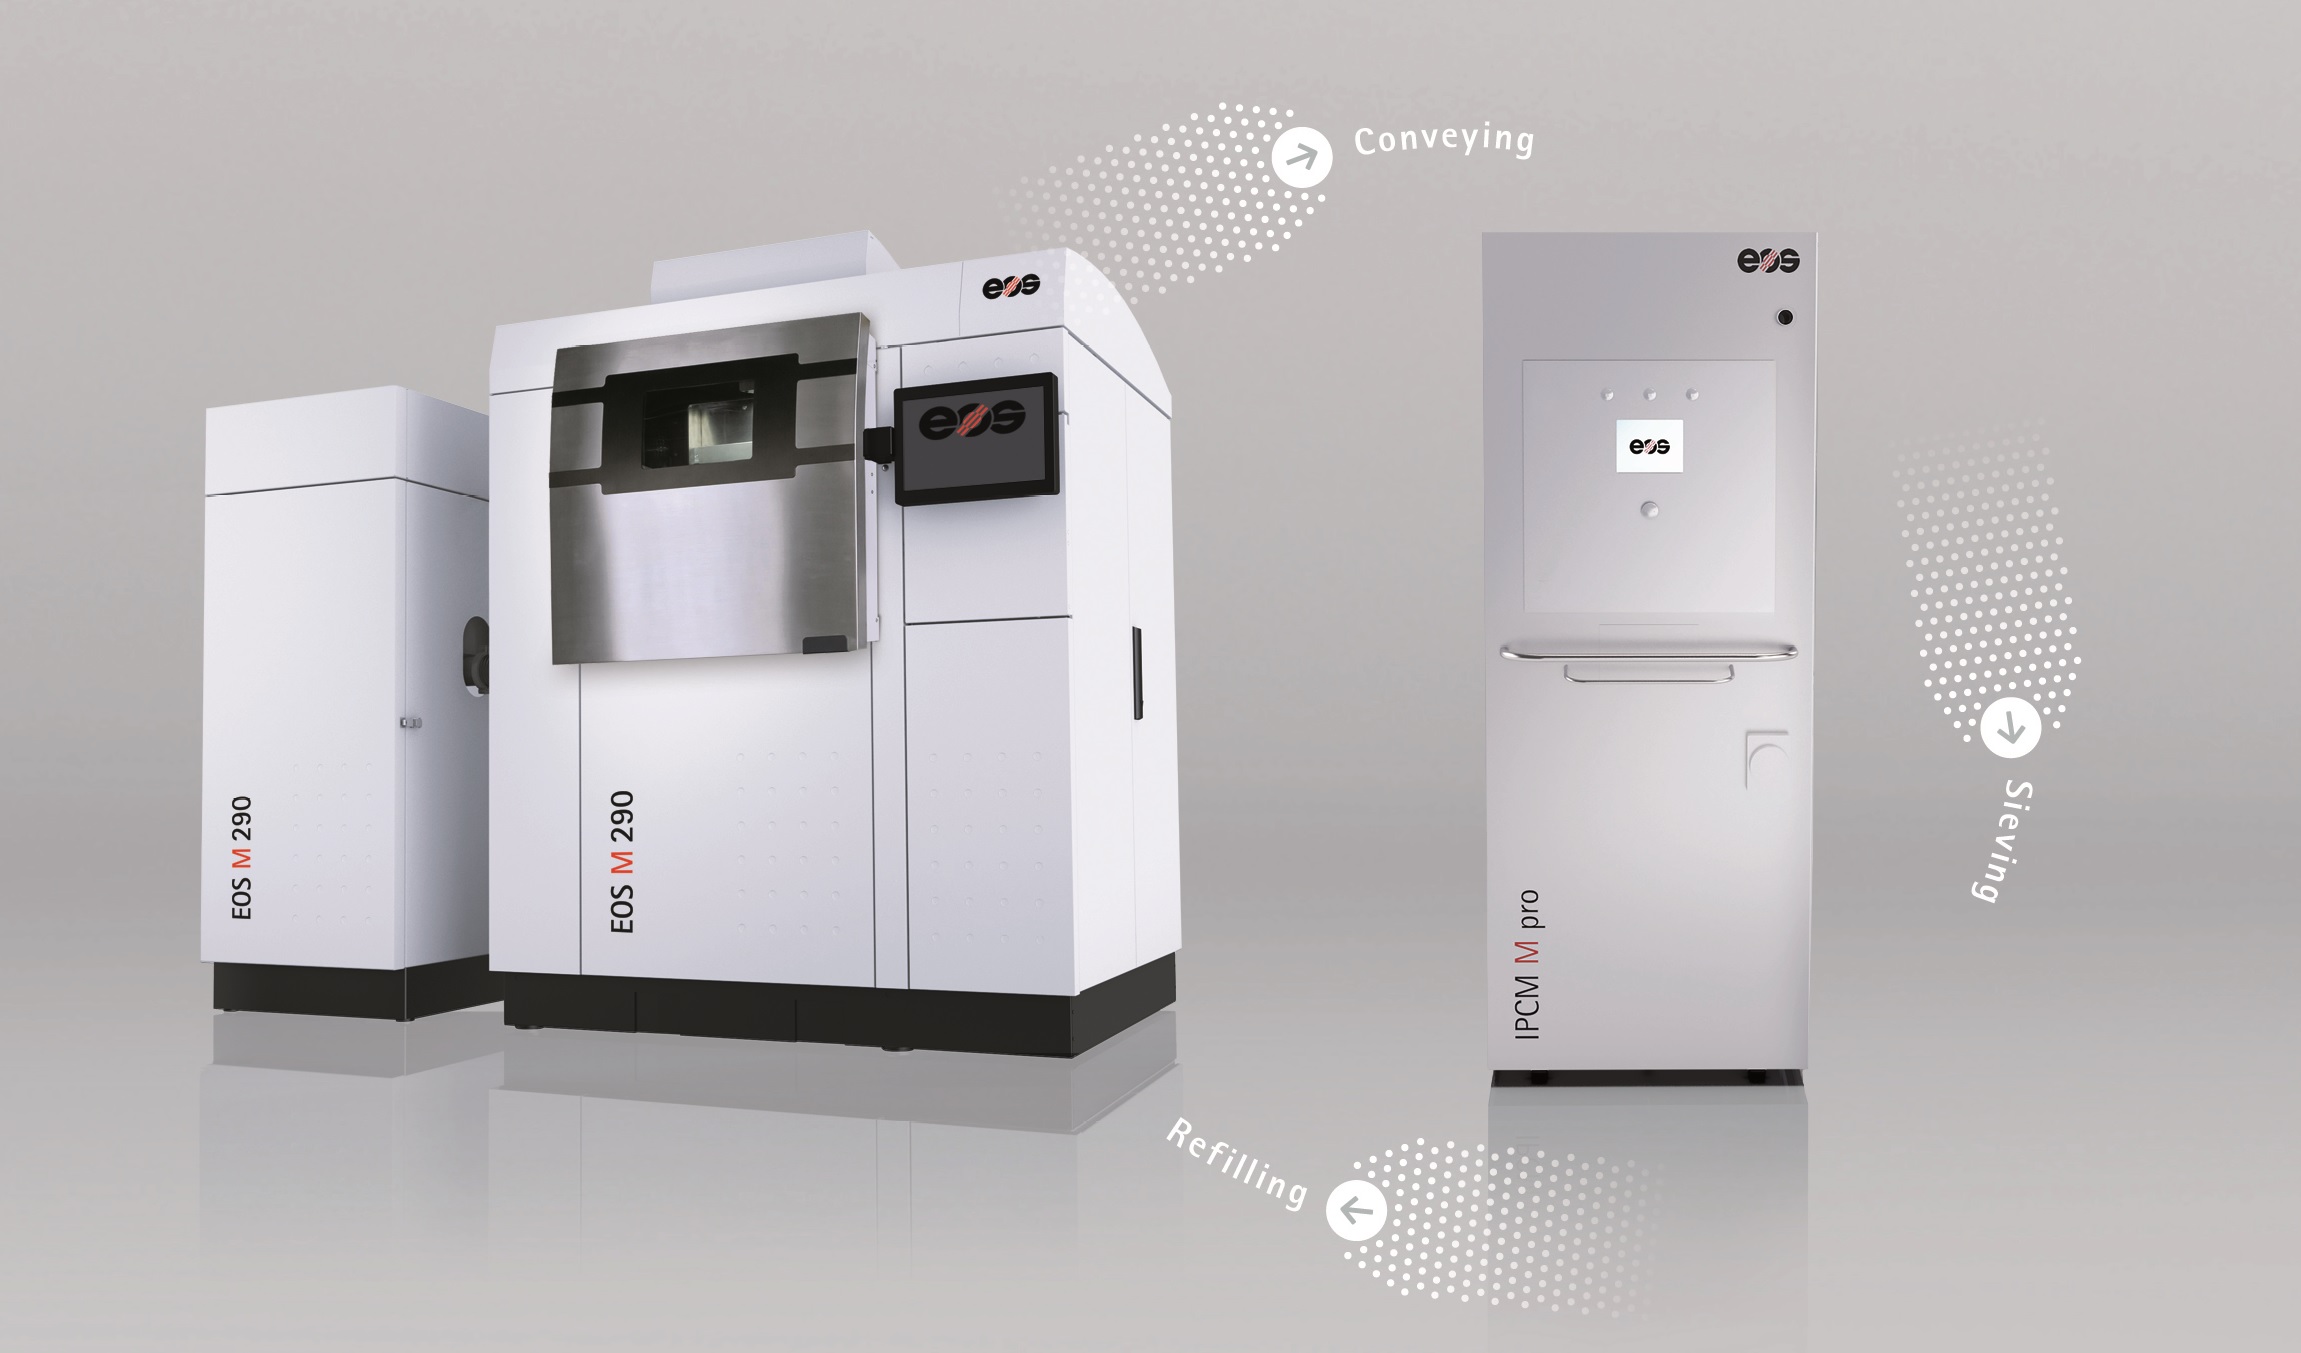
EOS presents the system as a way to limit powder contact. Reducing exposure does not replace risk assessment and suitable protective measures.
Rösler
Rösler does not only provide post-production technologies for metal additive manufacturing.
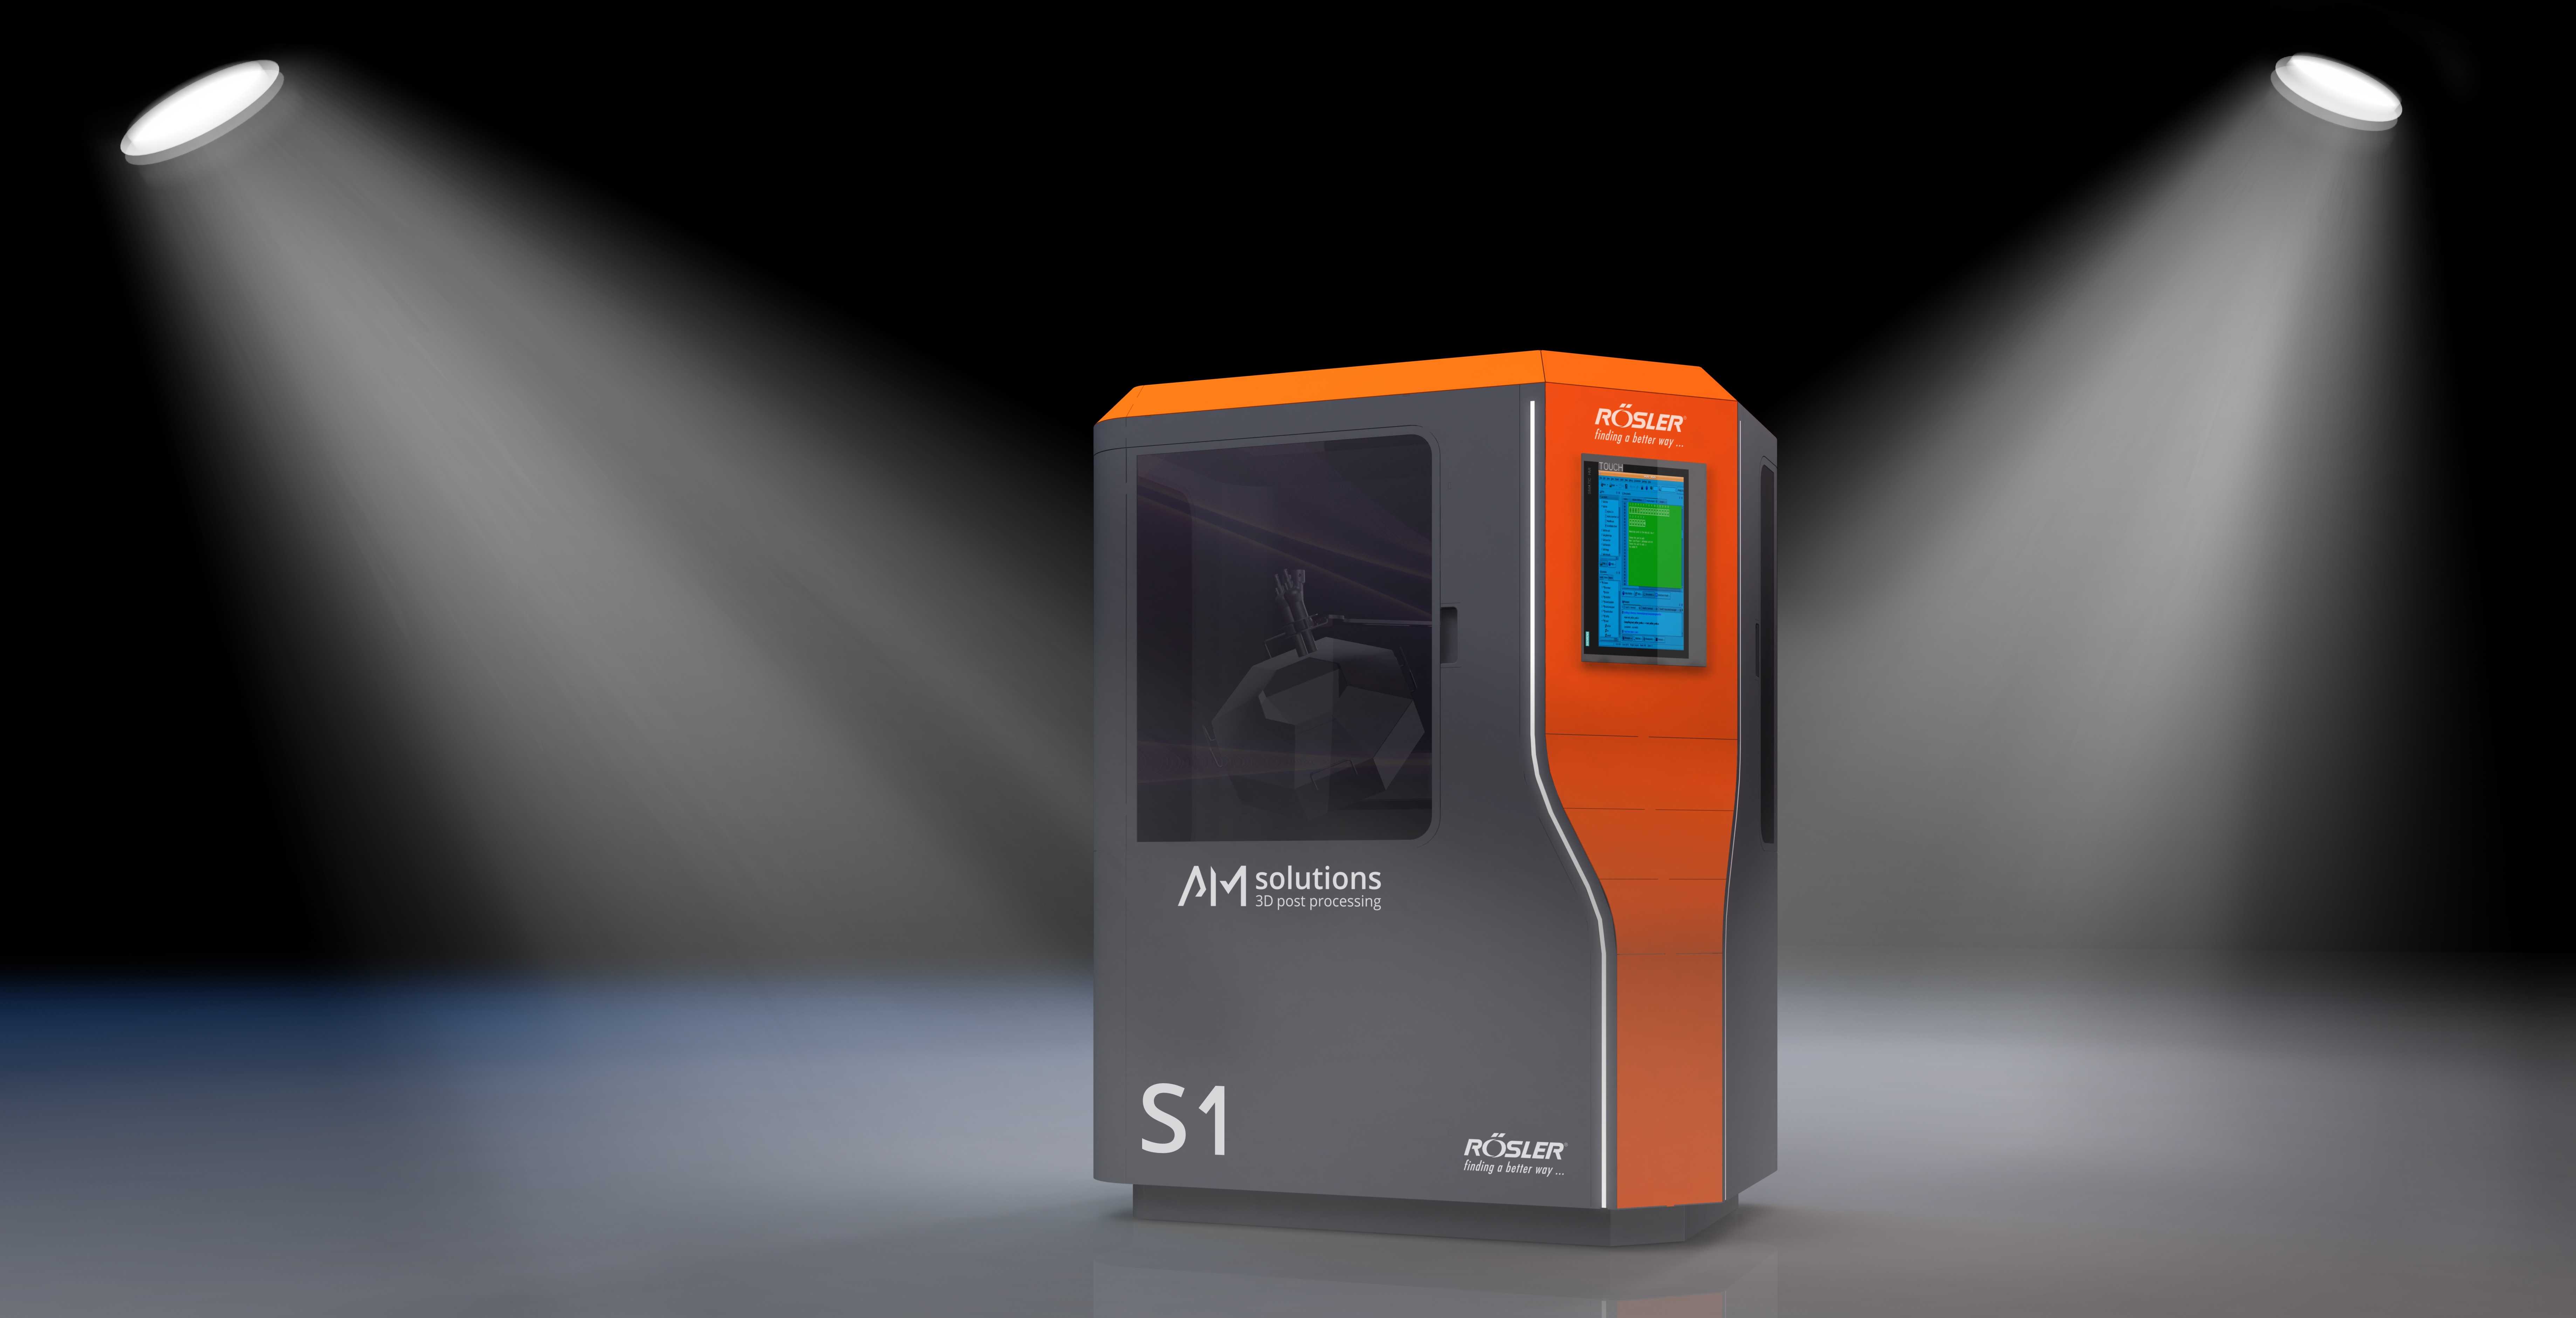
“We supply post printing & sintering processes. These processes are defined as removal of support structures (both metal and plastic parts) and aim to improve the surface (both metal & plastic parts). Our biggest advantage is the automated feature as well as the long experience the company has as surface specialists”, explains Vincent Raman.
Solukon
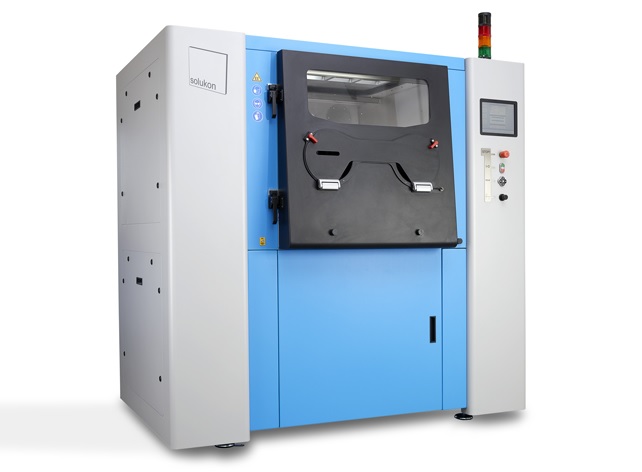
The Solukon equipment presented in this 2019 feature is the SFM-AT800-S, following the SFM-AT800.
Speaking of these equipment, Andreas Hartmann said that the “automated depowdering units remove and collect residual powder from complex laser melted parts with targeted vibration and programmable two-axis rotation within a protected atmosphere. The adjustable and high frequency vibration makes the powder flowable so that it can run out easily of very small gaps and intricate channels.
The flowing of the powder is supported by moving the part automated around two axis to all possible 3D positions continuously or to individually programmed positions. In addition to this, the systems are equipped with manual or automated blowing devices. To prevent explosive atmospheres for reactive materials like Titanium and Aluminium the process chamber can be rendered inert due to a safety controlled inert-gas-infusion.
The residual powder can be collected contamination free for recycling in special containers or directly recycled in a connected sieving system. In addition to mitigating the health and safety risks, users are able to significantly reduce cleaning time and improve the collection and recycling of expensive unused powders. Some users have reported labor reduction of up to 90% over manual powder removal processes.”
The company adds that, “due to adjustable vibration, the process is very gentle and does not influence the mechanical properties of the part or surface.”
Reported performance concerns the trials and users cited. Cleaning results need verification for the particular part; inerting also requires control of oxygen-deficiency risks.
Getting the desired finished part
At a GE Additive seminar cited in the feature, an engineer estimated post-processing at nearly 30% of final part cost. The precise reference and calculation scope are not supplied: this remains a reported estimate, not a general proportion.
Assessment should combine removal quality, cycle time, material recovery, safety and subsequent operations. A reported time saving alone does not establish that a part is clean or that recovered powder can be reused.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.