

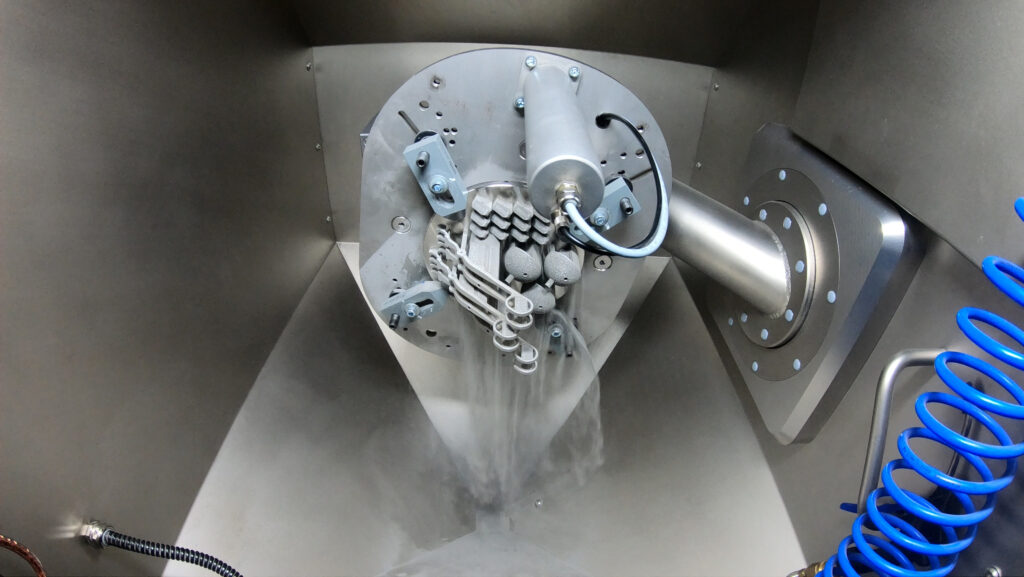
Test reported in the March/April 2024 magazine and published online on August 28, 2024. Results were supplied by Solukon and Swiss m4m for this build plate; they do not constitute medical certification.
Key insights into a depowdering test with a build plate of medical 3D printed parts
Selecting an automated depowdering system requires checking its suitability for the parts, materials and production requirements. We previously examined the technical features to consider. A trial with representative parts can inform the choice, but does not replace process qualification or validation of the finished device. To illustrate the approach, we asked Solukon Maschinenbau GmbH to describe a test conducted with Swiss m4m, which serves medical and dental applications.
The test used an SFM-AT350-E in its original configuration, announced for parts up to 60 kg, with the Swiss m4m Center. This capacity belongs to the context of the trial, before subsequent range updates: the manufacturer’s May 2024 data sheet lists 100 kg.
The system and test parts
Designed for metal 3D printed parts, the SFM-AT350-E is a special version of the automated depowdering machine SFM-AT350. Presented at Formnext 2023, the new machine comes with three key upgrades: full compatibility with intelligent SPR-Pathfinder® depowdering software, enhanced functions of the Digital Factory Tool as well as piezoelectric excitation.
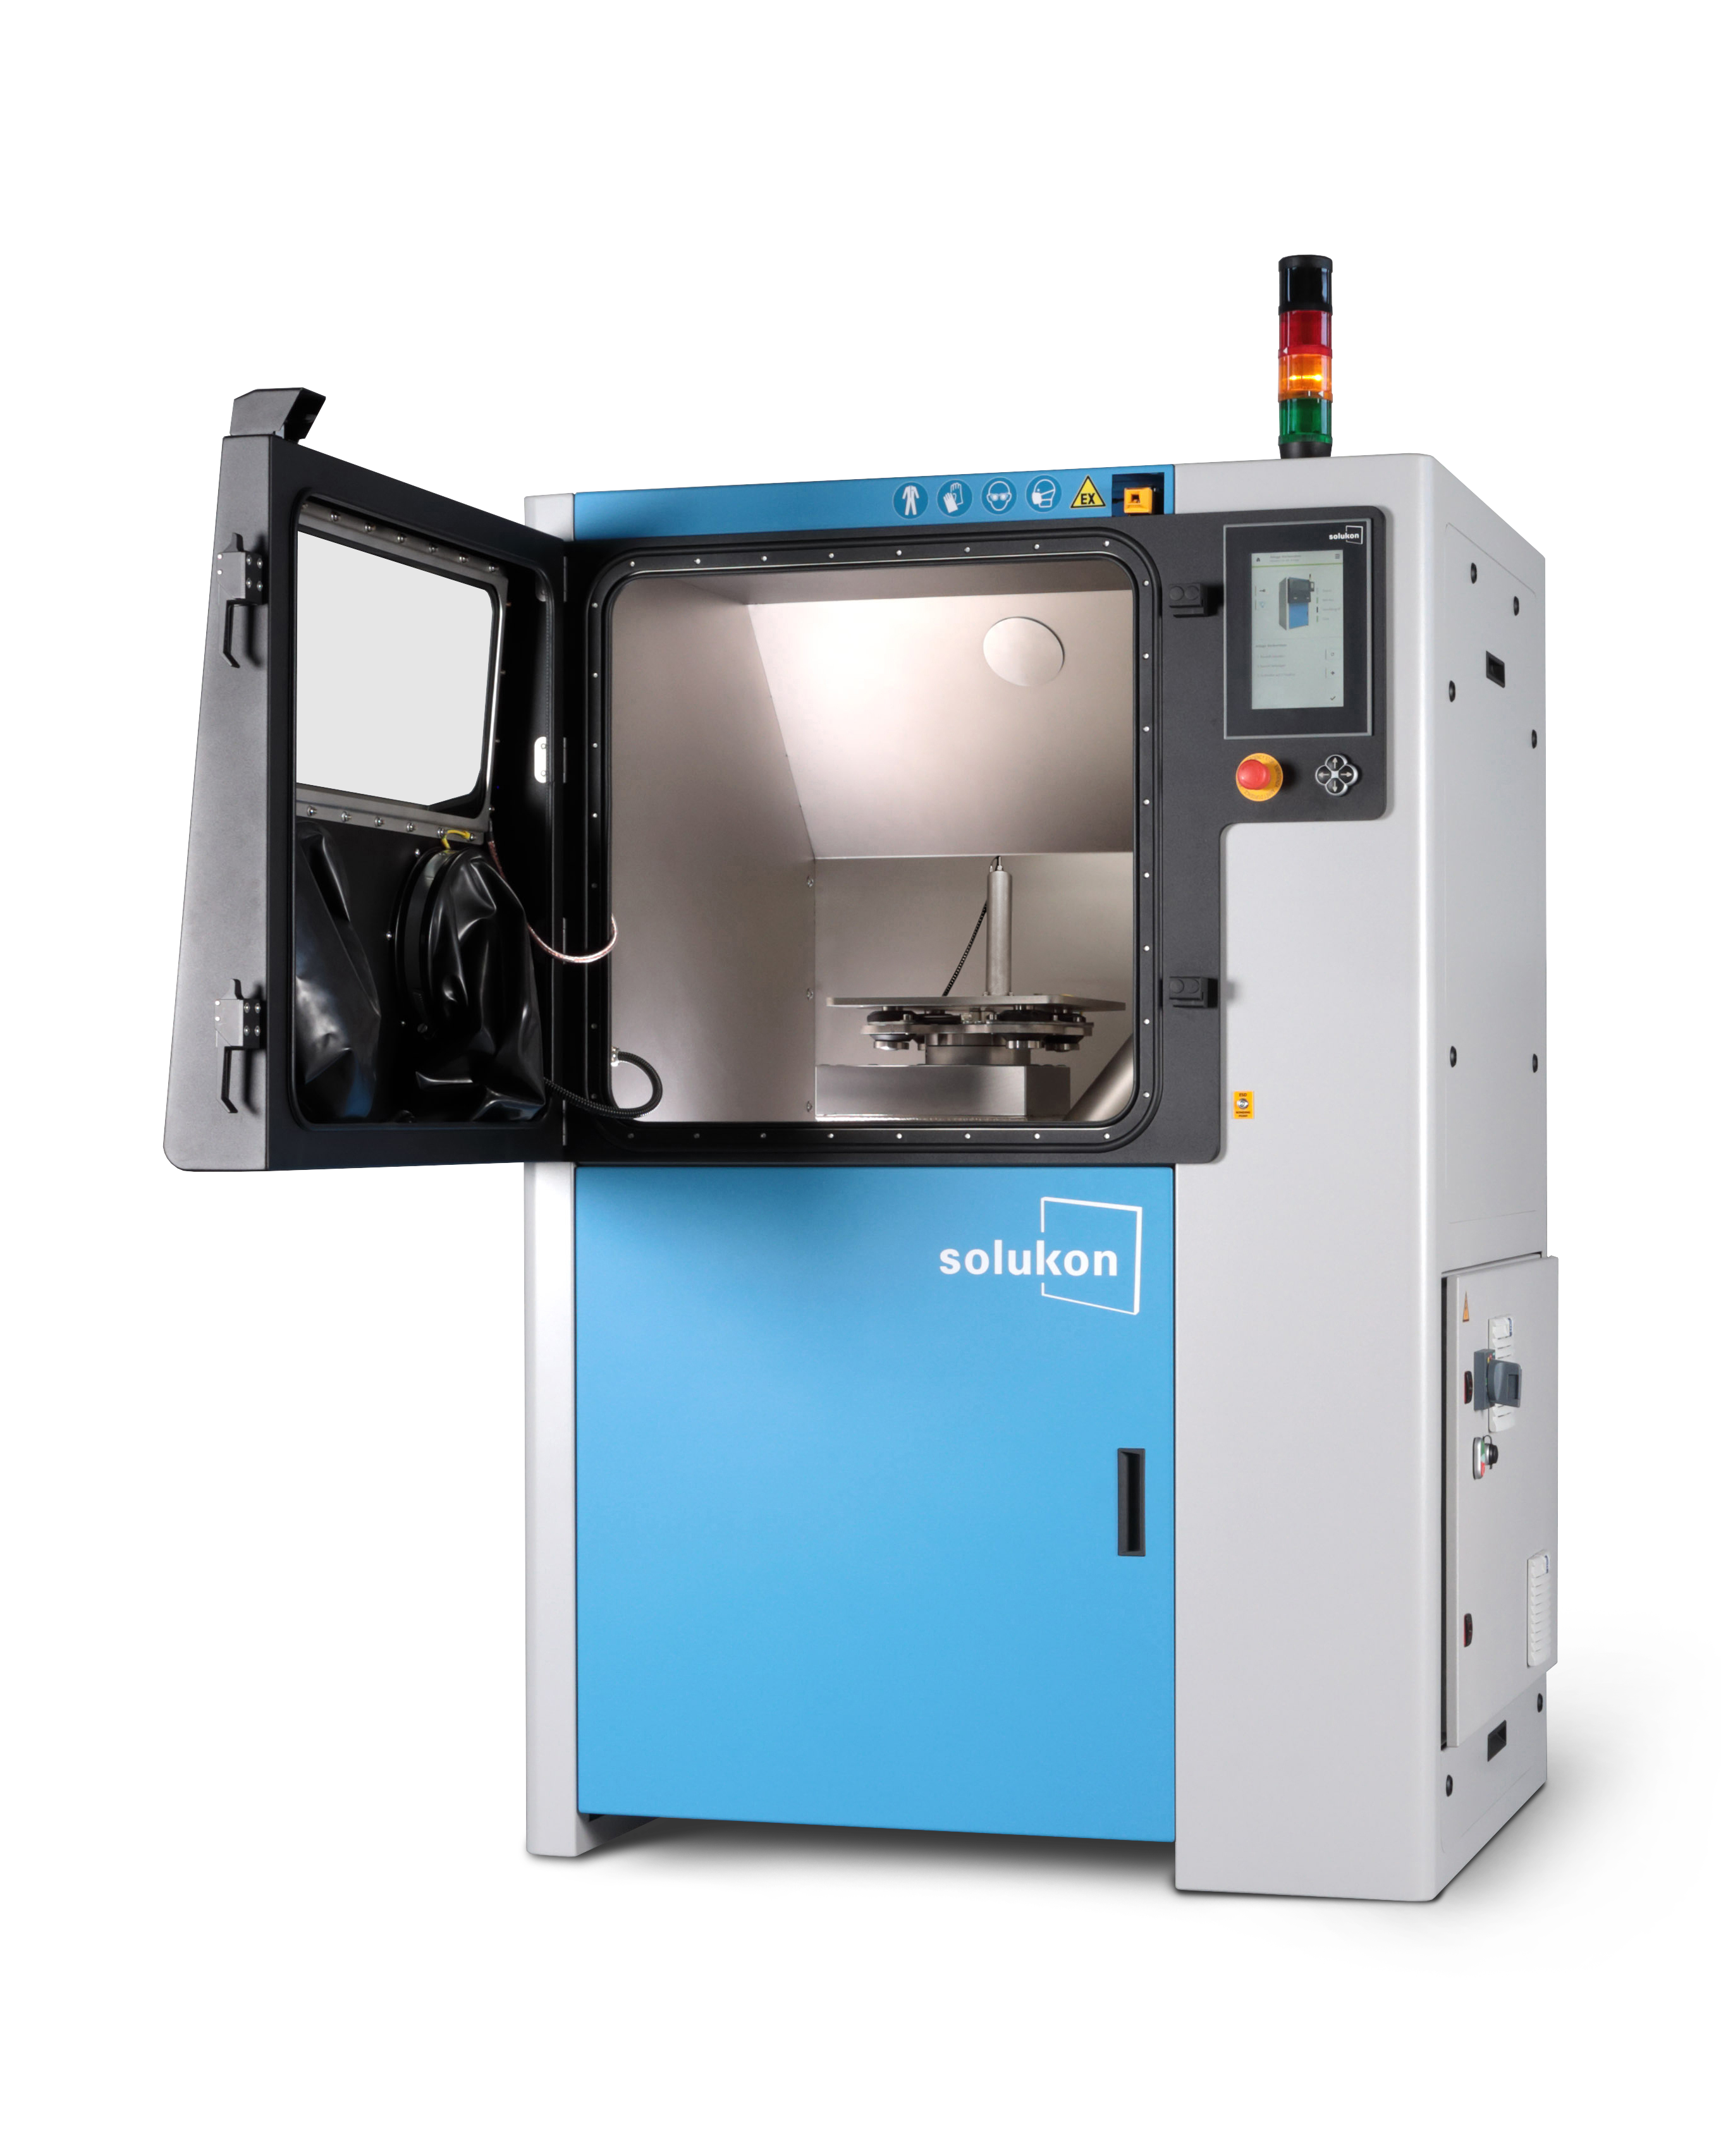
If the SPR-Pathfinder® depowdering software and the Digital Factory Tool are now well-known features of Solukon’s depowdering systems and also available for the standard SFM-AT350 machine, the piezoelectric excitation tool remains intriguing for most users as a unique and special solution in the field.
According to Solukon, piezoelectric excitation originates at the rotary table and uses a self-regulating ultrasonic frequency. The manufacturer aims to accommodate delicate structures. Absence of damage still needs to be checked for the specific parts and conditions; frequency alone cannot establish it.
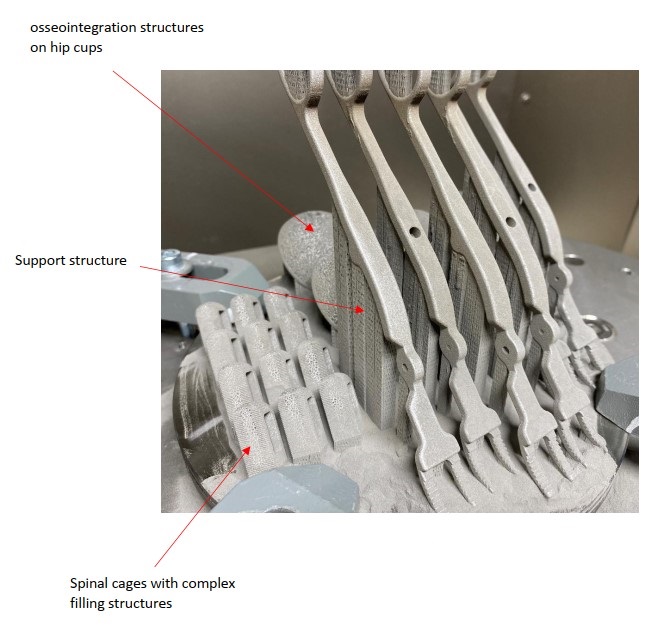
The test was performed with several medical 3D printed parts provided by Swiss m4m: hip cups, spinal cages and medical instruments.
“Hip cups are a very typical application. The characteristic lattice structures allow tissue ingrowth. Also, the spinal cages for stiffening the spine in cases of instability (e.g. herniated disc). The medical instruments are used as prototypes for wet room testing. Their complex support structures with lots of long tight channels are the most difficult to depowder,” Marco Flury, Project Manager at Swiss m4M explains. As you will see below, Swiss m4m provided Solukon with different data on these parts.
The test illustrates parameters to assess for these parts and characteristics of piezoelectric excitation.
The depowdering test in six stages
Hemank Raj, then Process Development Engineer at Solukon, describes six stages: reviewing machine data, reviewing component data, initial visual inspection, depowdering, checking the results and final inspection.
1. Review the machine conditions
The operators used a non-inert atmosphere for the 17-4 PH alloy in this trial, which they described as non-reactive. This condition should not be transferred to another powder: the system documentation provides for inerting with reactive materials.
2. Describe the build plate and parts
Swiss m4m supplied the part dimensions, build plate characteristics, combined weight and material. The reported values are summarized below.
| Parameter | Reported value |
|---|---|
| Parts and structures | Hip cups: Ø 60 mm, pores 0.3–0.9 mm; spinal cages: 23 × 10 × 10 mm, pores 0.3–0.9 mm; instruments: approximately 70 mm in Z-height, intricate support structures with smallest diameter below 1 mm. |
| Build plate | Round, 204 mm diameter. |
| Plate thickness | 23 mm. |
| Weight including plate | Approximately 13 kg. |
| Plate type | TRUMPF TruPrint 2000, without through holes. |
| Material | Stainless steel 17-4 PH. |
3. Inspect the initial condition
Initial visual inspection showed no apparent damage or powder lumps on the build plate, while the structures appeared filled with powder. That observation alone does not demonstrate resistance to moisture absorption.
4. Carry out depowdering
The build plate was secured to the rotating table with four clamps. The reported overall cycle took approximately 17.5 minutes from loading to unloading, including automatic operation, supplementary air cleaning and checks.
According to Solukon, the main stages remain comparable to those used for depowdering with pneumatic excitation.
Raj drew our attention to one key advantage though: “You do not have to set any excitation
parameters because the depowdering system automatically sets the best excitation (=
self-regulating frequency). In addition, the process was conducted in a volume maximum
of 53.6 dB (for reference: a normal conversation = 60 dB) which is very silent. The process
in ultrasonic excitation comes with a minimum compressed air consumption.”
The 53.6 dB figure is the value reported for this trial. Acoustic weighting, measurement distance and protocol are not specified in the feature, so it does not establish occupational exposure or a standardized comparison with other equipment.
In the pneumatic configuration, a programmable knocker can supplement the vibrator to break up powder clumps. SPR technology combines rotation and vibration.
Raj describes high-frequency, low-amplitude excitation to detach powder from surfaces. The comparison below is the manufacturer’s explanation; this feature does not present a complete comparative trial against pneumatic excitation.
5. Check the results
After automatic operation, the team inspected the parts and applied supplementary compressed air at their openings. These reported observations do not quantify all residues that could remain in internal structures.
For this trial, the team considers the SFM-AT350-E suitable for delicate and fragile structures. Not to mention that with the “Digital-Factory-Tool we have access to all relevant depowdering data (e.g. temperature in the machine chamber, humidity and all customer specified presets) – crucial for data-sensitive industries like MedTech”, Raj adds.
The team recommends additional final cleaning, for example ultrasonic cleaning, within the post-processing chain. The ultrasonic excitation used for depowdering here and this final cleaning are separate operations. Their effectiveness needs to be evaluated for the part concerned. ASTM F3335-20 describes qualitative and quantitative approaches to assessing AM residues; it does not establish universal acceptance limits.
6. Perform the final inspection
The reported final inspection found no visible damage or apparent powder deposits, and the parts remained attached to the build plate. Absence of visible residue does not by itself establish finished-device cleanliness or suitability for clinical use.
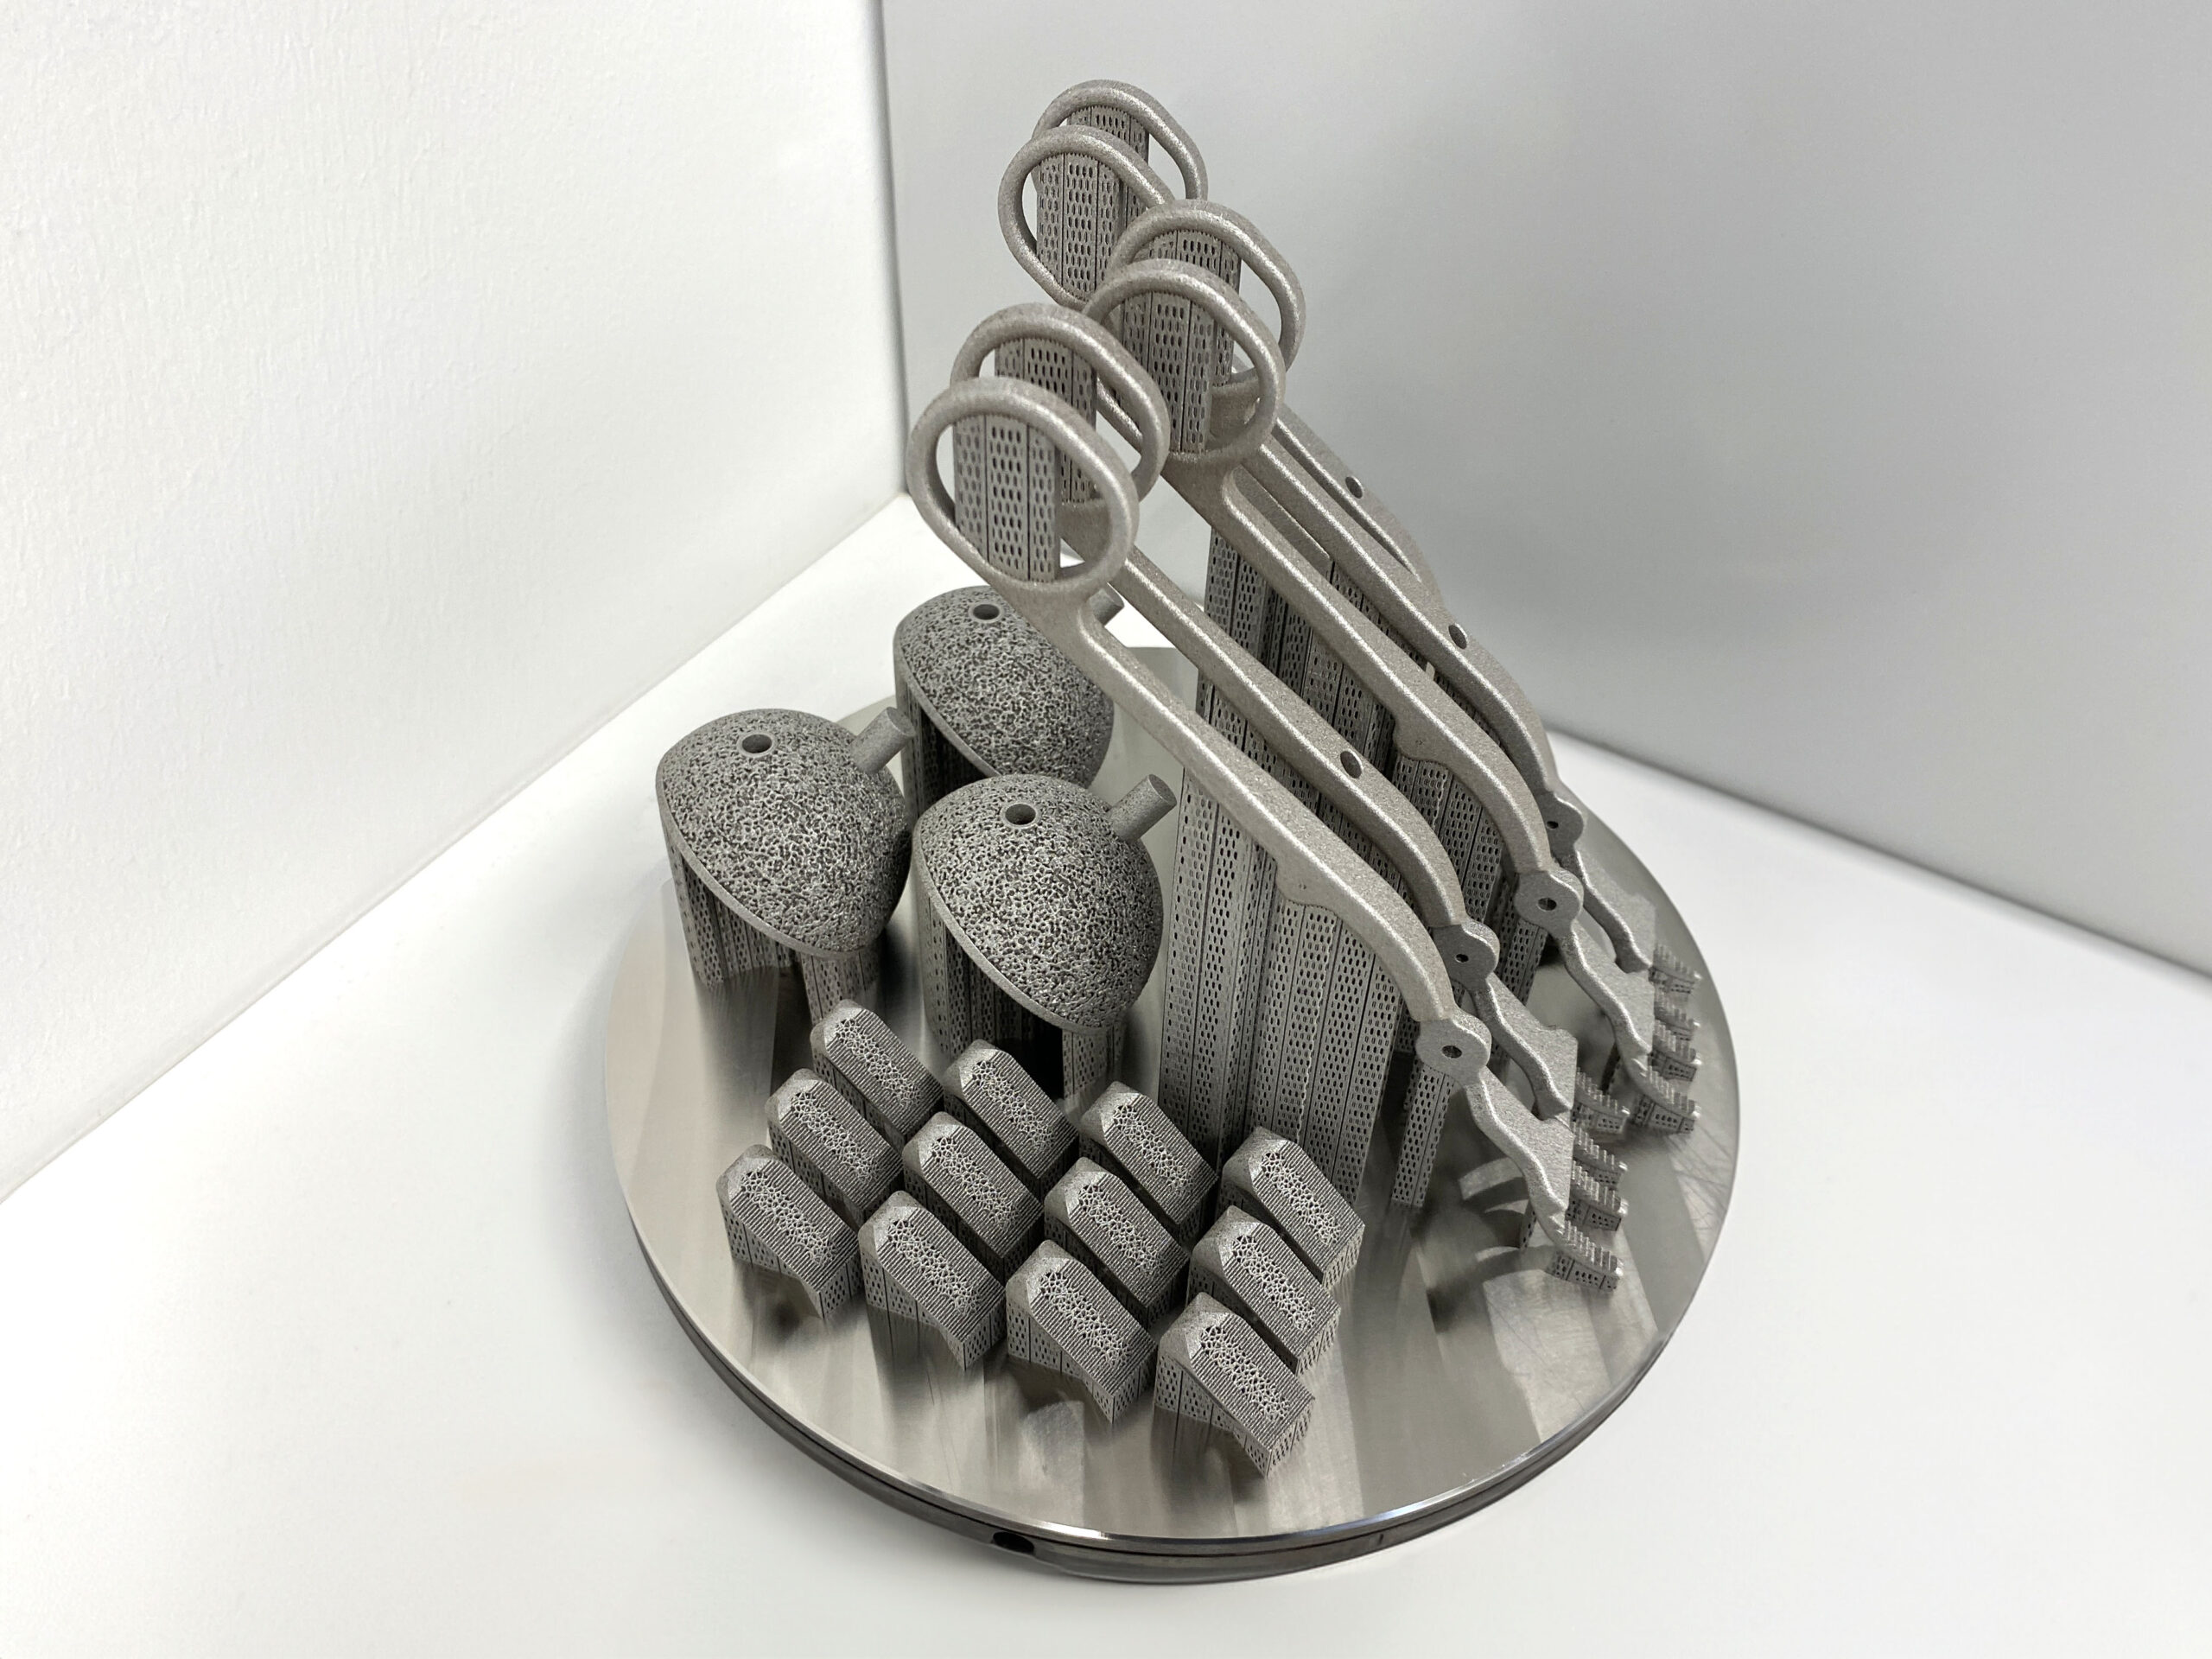
In total, Flury from Swiss m4m recovered 977 grams of powder from this testing.
What this trial establishes
These results concern a single build plate and its test conditions. Geometry, supports, alloy and cleanliness criteria need to be considered for each application. They do not demonstrate general superiority over every alternative depowdering method.
As Raj notes for instance, “compared to pneumatic excitation with a turbine or knocker, the acceleration and frequency are many times higher and the amplitude much lower. (This is why you do not see any vibration/movement of the component during excitation). The excitation frequency is between 30 kHz and 38 kHz. This means that we are far beyond the natural frequencies of the components. This prevents oscillation and damage at the resonance frequency.”
The optional Digital-Factory-Tool records process data, while SPR-Pathfinder® calculates motion sequences. Compatibility with these functions formed part of the upgrades announced at Formnext 2023.
“With specially developed technology, we were able to set up endless rotation of the turntable in the SFM-AT350-E and thus enabled the unlimited use of the SPR-Pathfinder software”, says Andreas Hartmann, then CEO/CTO at Solukon.
Raj suggests that comparable results might be achieved with titanium alloys. This remains a prospect in this feature: the documented trial used stainless steel 17-4 PH. Any necessary inerting would also have to be included in the relevant cycle.
Automatic cleaning is reported to take less than 7.5 minutes, with Raj assuming a further 10 minutes for loading and unloading. At the reported overall cycle of approximately 17.5 minutes, theoretical sequential throughput is about 3.4 cycles per hour, before other downtime. The original estimate of four cycles per hour would require a cycle of no more than 15 minutes or overlapping operations, which are not documented here.
All images: Courtesy of Solukon.
This feature was first published in the March – April 2024 edition of 3D ADEPT Mag.
Review note: test results have been distinguished from certification, and the limits of visual inspection and extrapolation to titanium clarified. Throughput has been recalculated from the reported total time, and the six stages have been structured consistently. Figures and quotations retain their 2024 context.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.