

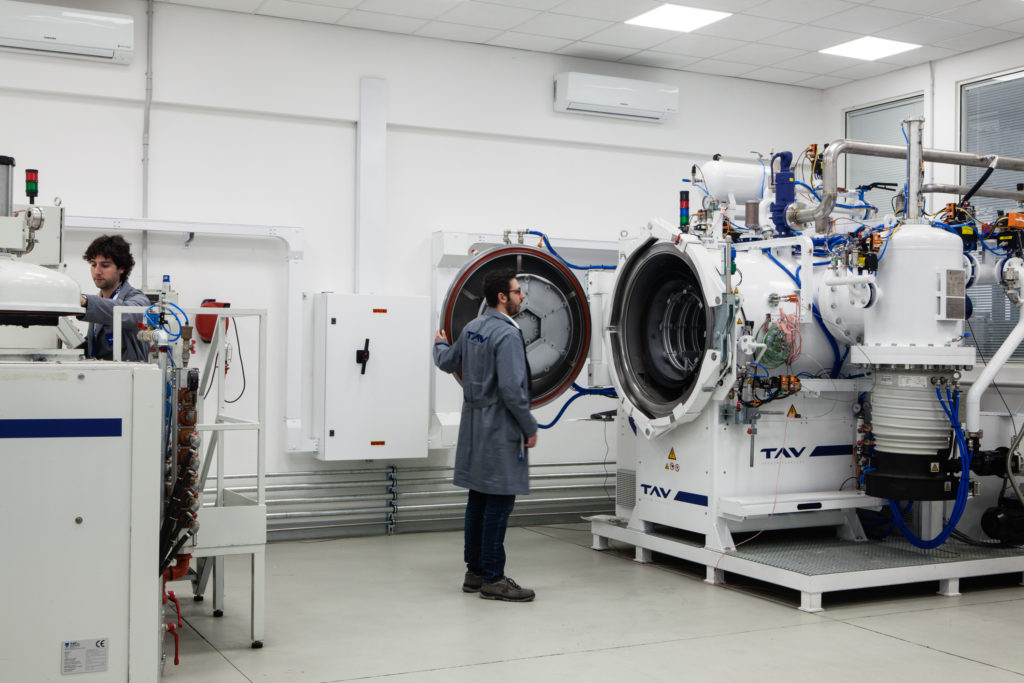
Feature first published in the July/August 2021 issue of 3D ADEPT Mag. Roles, interviews and examples reflect that period.
Debinding, sintering and some heat treatments bring furnaces into the production of 3D printed parts. Equipment selection depends on the material, printing process and required properties.
Suppliers draw on experience in metallurgy, ceramics and conventional heat treatment. This expertise must be adapted to the characteristics of additively manufactured parts.
So, why & where are furnaces used in the AM process? What type of 3D printed parts require furnaces? How do we use furnaces? And what are the main features of these machines?
This article aims to provide a glimpse of the use of furnaces for additively manufactured parts.
Why & where are furnaces used?
First and foremost, given their primary nature, furnaces are used for applications that require high processing temperatures.
Two broad functions are distinguished here: removing binder and densifying parts produced by certain manufacturing routes, and modifying the properties of already consolidated parts. These are process functions, not an exhaustive furnace classification.
Parts that require sintering (and often debinding) and parts that require heat treatment. To this end, “ceramics and composite 3D printed parts may require to be treated in a vacuum furnace, as do most metal 3D printed parts,”, Andrea Cassani, Sales Director at TAV VACUUM FURNACES SPA notes from the outset.
This possibility does not mean that every 3D printed part requires a furnace, or that vacuum suits every material. Atmosphere and thermal cycle must be selected for the process and feedstock.
Debinding and Sintering
In processes that print bound powder, shaping is followed by binder removal and densification. These operations require cycle control to limit defects and distortion.
Debinding removes some or all of the organic binder using a suitable sequence: solvent, catalytic treatment, heating or a combination. Duration depends on formulation, geometry and escape paths for decomposition products.
Sintering is often considered as the final step of all powder metallurgy processes, including some metal 3D printing processes. During this stage, “green parts (a combination of metal powder and binder) are first heated to a temperature where the binder evolves and is removed from the parts. The furnace then ramps up to the sintering temperature of the metal which is just below the melting temperature of the material, fusing together the metal particles. After sintering is complete there is little or no evidence of the original powder particles, fabrication process and parts have very low porosity”.
This simplified description is not a thermal recipe. Sintering densifies a particle structure, notably through diffusion; a liquid phase may be involved in some systems. Temperature, shrinkage and final porosity depend on the material and cycle.
Debinding cannot be arbitrarily omitted where binder removal is required. Some routes combine thermal debinding and sintering in one cycle; others use several machines or stages. A route validated for the material and part is required.
Sintering aims to densify the part while controlling shrinkage, microstructure and distortion. Desktop Metal’s discussion of temperature and holds underlines that increasing time or temperature does not always improve the outcome.
In general, the following three steps are often observed:
- Controlled binder removal using the selected method.
- Sintering densification, with control of shrinkage and microstructure.
- Cooling according to the validated cycle before unloading.
Heat Treatment
Heat treatment applies a heating, holding and cooling cycle to obtain specified microstructure and properties. Depending on material and application, it may relieve stress, anneal, solution-treat or harden a part.
To make it happen, what better way than using a furnace which can maintain heat at a desired temperature for a defined amount of time, before cooling.
“While it’s hot, the metal’s physical structure, also called the microstructure changes, ultimately resulting in its physical properties being changed. The length of time the metal is heated for is called the ‘soak time.’ Knowing what temperatures to heat and cool metals at, as well as how long each step of the process should take for a specific metal or alloy is extremely complicated. Because of that, material scientists known as metallurgists, study the effects of heat on metal and alloys and provide precise information on how to perform these processes correctly”, an expert from General Kinematics explains.
Taking the example of parts that have been manufactured using SLM technology, TAV VACUUM FURNACES SPA explains that most materials that are printed with SLM technology need a heat treatment.
“This heat treatment can be de-tensioning (to release most of the internal tensions accumulated in the material during the printing phase) or of another type (to try to optimize the mechanical properties of the component according to its specific application). Usually these treatments are carried out in air or in controlled atmosphere”, the expert highlights. Furthermore, materials such as stainless steel, titanium alloys, superalloys of nickel and CoCr alloys, could require the use of vacuum.
What type of 3D printed parts require furnaces?
Required treatments differ between metals, ceramics and polymers, and between processes with or without binder. The table gives examples from Nabertherm documentation; not every treatment applies to every material.
| Family | Treatment examples | Atmosphere in the diagram | Equipment examples |
|---|---|---|---|
| Metals | Debinding, sintering, stress relief, solution annealing, hardening | Protective or reaction gas; vacuum | Chamber furnaces with gas boxes; hot-wall or cold-wall retort furnaces |
| Ceramics, glass, composites, sand | Debinding, sintering, drying, curing depending on material | Air in the illustrated examples | Chamber furnaces, combined debinding/sintering furnaces, dewaxing furnaces |
| Polymers | Curing, thermal conditioning or drying depending on material | Air in the illustrated examples | Ovens, chamber dryers, forced-convection chamber furnaces |
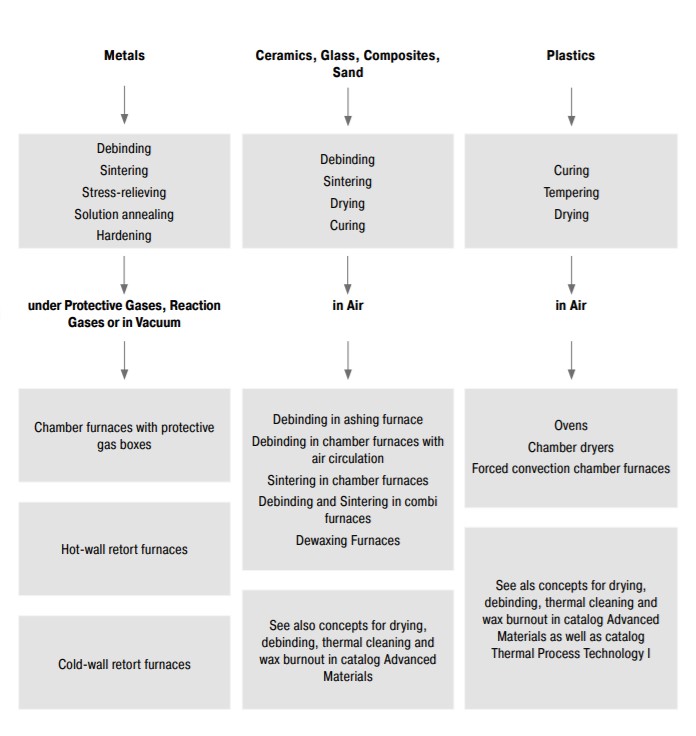
The required treatment must be defined before selecting the furnace: a ceramic, polymer and metal alloy do not necessarily share atmosphere or temperature requirements.
Source: Nabertherm, Additive Manufacturing. Atmosphere, exhaust treatment and equipment compatibility must be checked for the chosen material and cycle.
How do we use furnaces? And what are the main features of these machines?
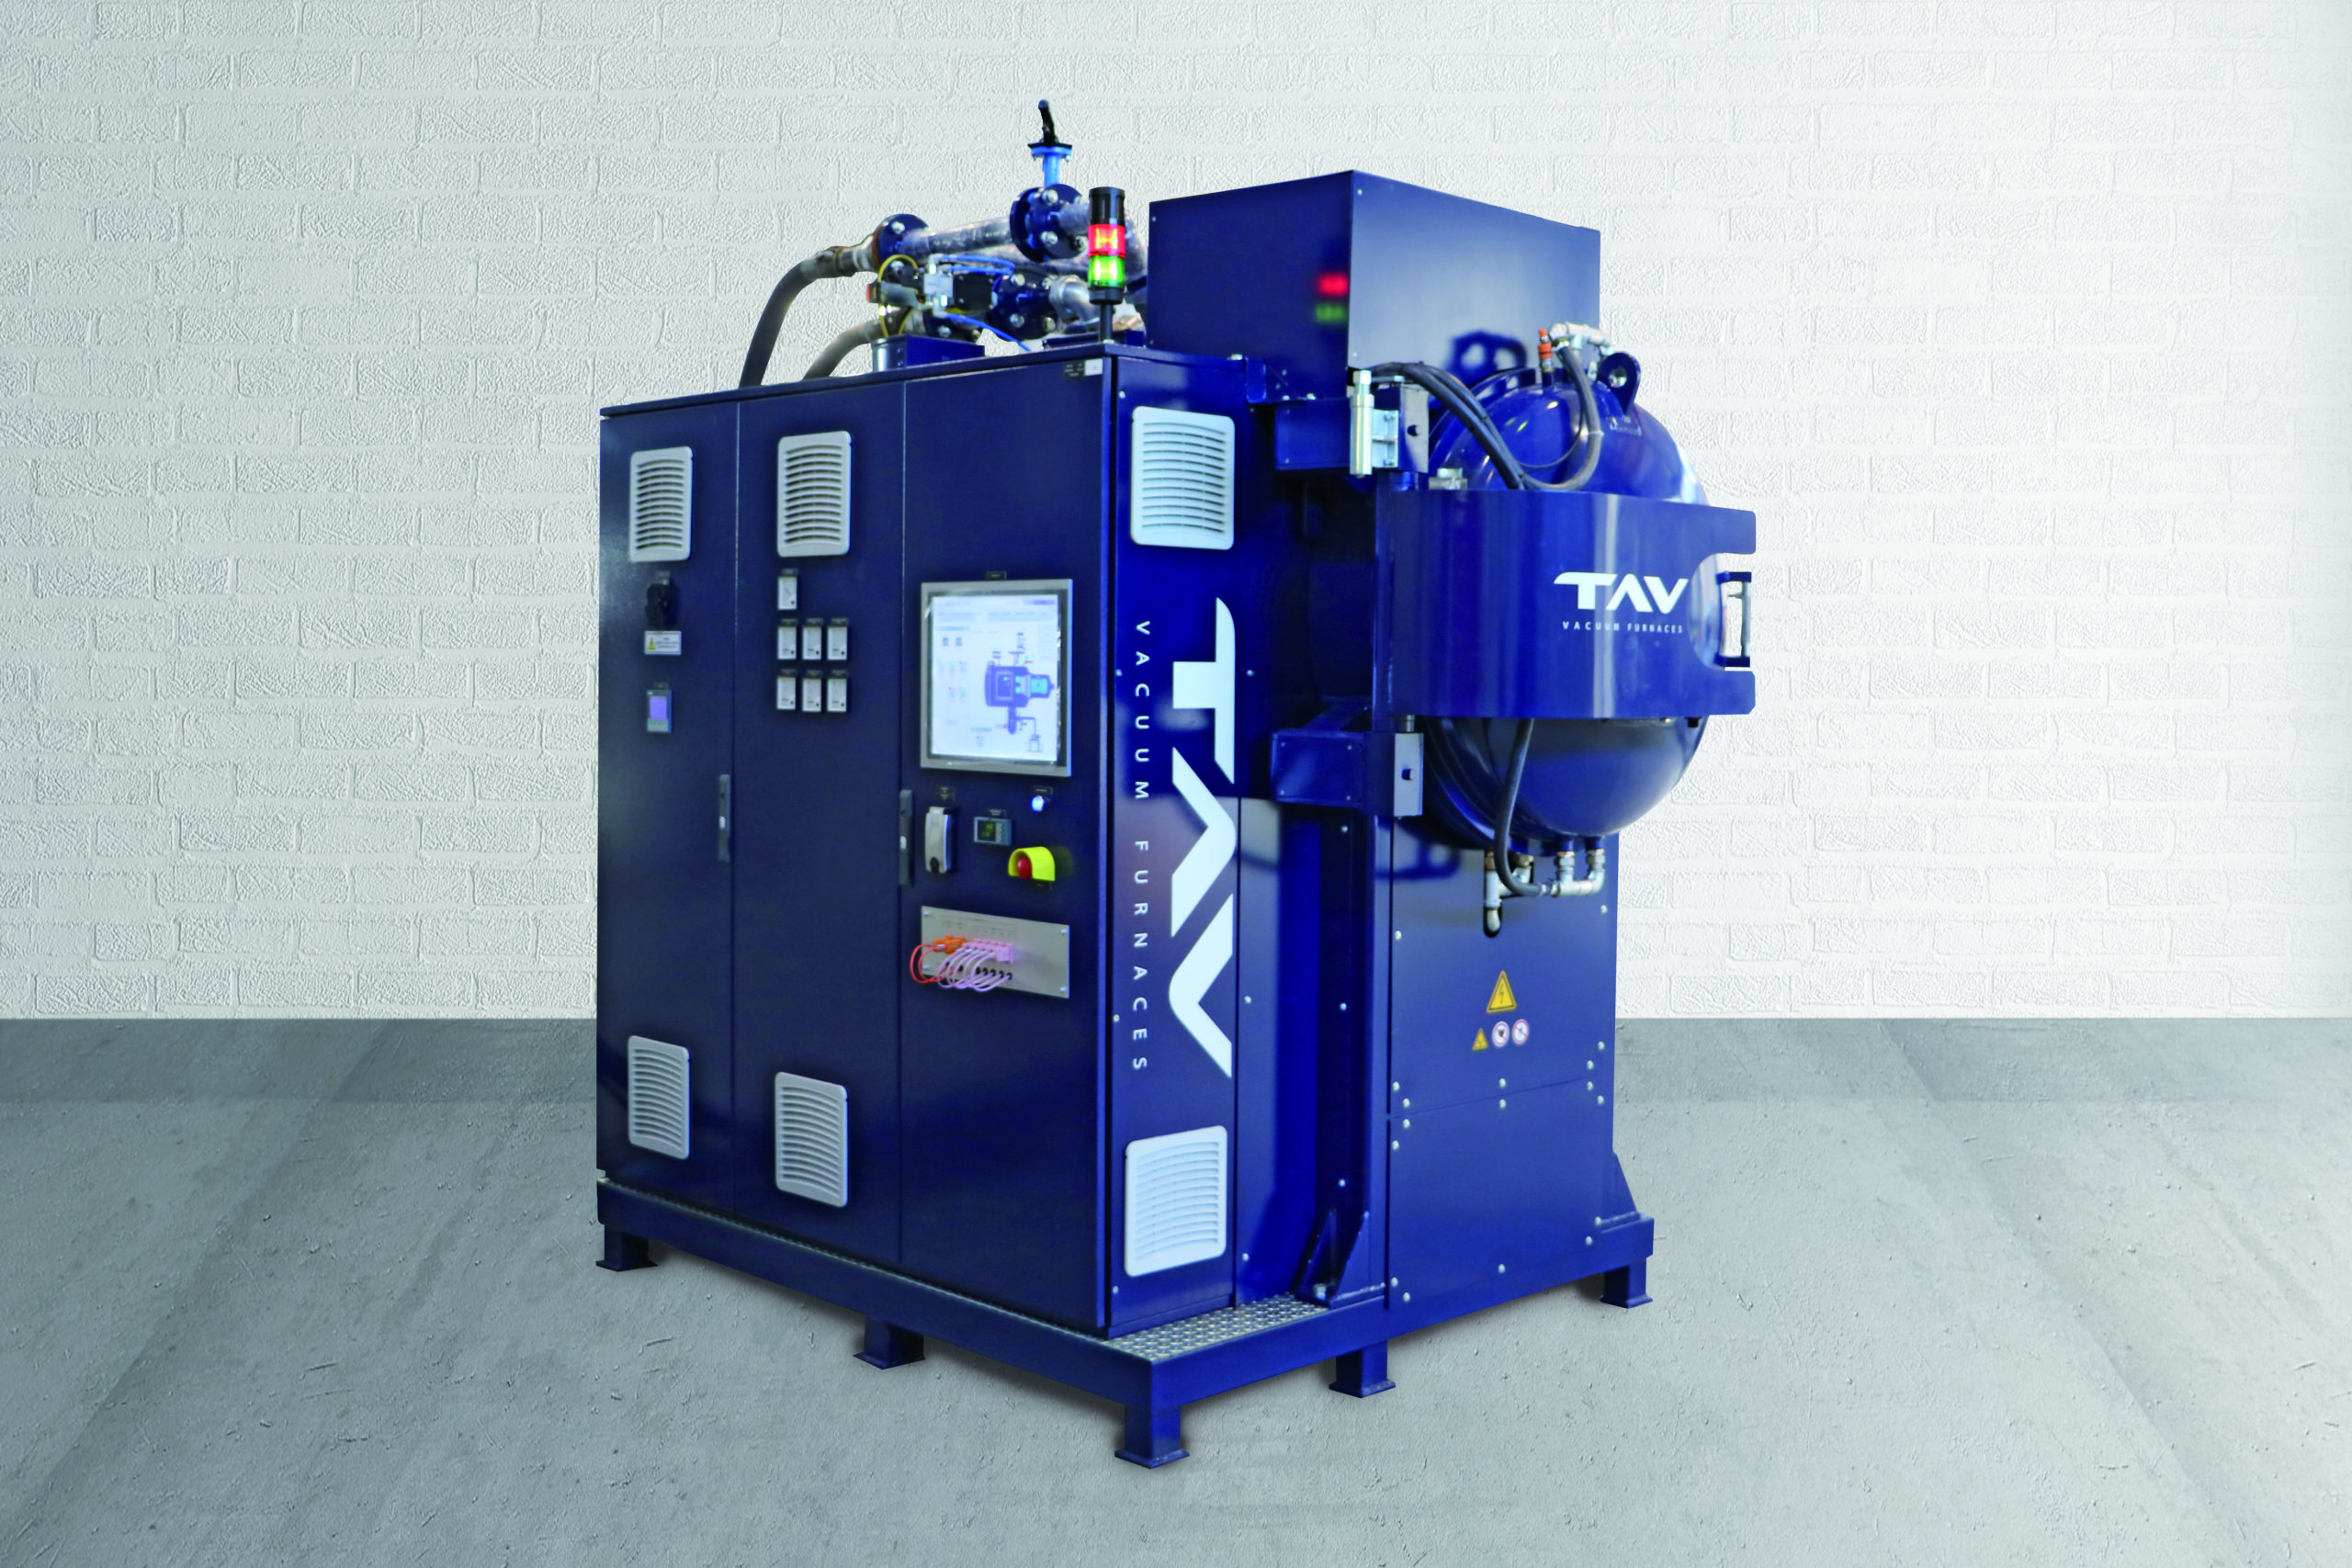
The diversity of materials and cycles prevents a universal furnace recommendation. Selection must start with the process, usable volume, load and quality requirements.
So, how can we help AM users to make a decision? Cassani attempts to provide a useful answer:
“We cannot make a generic statement valid for all kind of vacuum furnaces. We can say that today the temperature range required for 3D printing parts is approx. between 500 and 1400°C for sintering and heat treatment or below 900°C for debinding/presintering. In the case, a part has to be sintered often; we split the process and the furnaces in 2 steps: first step a debinding furnace to take out parts from the binder and second step (at higher temperature) a sintering furnace.
In the case of parts to have to be heat-treated the furnace is very close to a classic vacuum heat treatment furnace, with some specific features/characteristics. You often need to consider that whoever buys a furnace for the heat treatment of 3D printed parts uses the furnace only for these parts, so [an optimised design is generally justified].”
The temperatures cited by Cassani describe the applications discussed in this interview; they do not cover every material, including every ceramic. They must not be used as operating parameters without validation.
In the same vein, one can take note of the following recommendations from TAV VACUUM FURNACES SPA & SECO/WARWICK S.A. to companies looking for a new furnace:
- Check furnace compatibility with material, binders, atmosphere and exhaust products.
- Size the usable volume and batch capacity for cycle time and the production schedule.
- Plan inspection, finishing and any machining after treatment.
- Assess capital and operating costs for the full route. The number of printers served by a furnace depends on throughput and cycles, not a universal ratio.
Moving forward…
The development of additive manufacturing reinforces the need to control thermal operations alongside printing and finishing.
A facility may use several manufacturing processes. That diversity does not mean that one furnace or cycle automatically suits every part.
Choices must be validated by material family and process route, considering changing loads and contamination risks.
That’s the reason why collaborations between developers of furnaces and 3D printer manufacturers or private and public research centres/universities are also prevalent here. As is the case with TAV VACUUM FURNACES SPA, such collaborations help producers of 3D printers and research centres/universities define post-processing standards and constantly improve the furnace features in terms of performance, productivity and quality on the 3D printed parts.
Resources:
Main contribution: Interview with Andrea Cassani, Sales Director at TAV VACUUM FURNACES SPA.
External contributions: SECO/WARWICK S.A. – Desktop Metal – Nabertherm – General Kinematics
First published in 3D ADEPT Mag, July/August 2021. Featured image: TAV Vacuum Furnaces.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.