

This feature first appeared in May/June 2024 and was published online on October 9, 2024. Product ranges and interview statements are presented in that context.
Laser selection affects a 3D printer’s precision, productivity and cost. Wavelength, power, stability and beam profile must suit both the material and the process. This feature examines those choices with Alex Kingsbury, then Market Development Manager – Additive Manufacturing at nLIGHT, and Michael Rath, then an inside sales representative at Novanta.
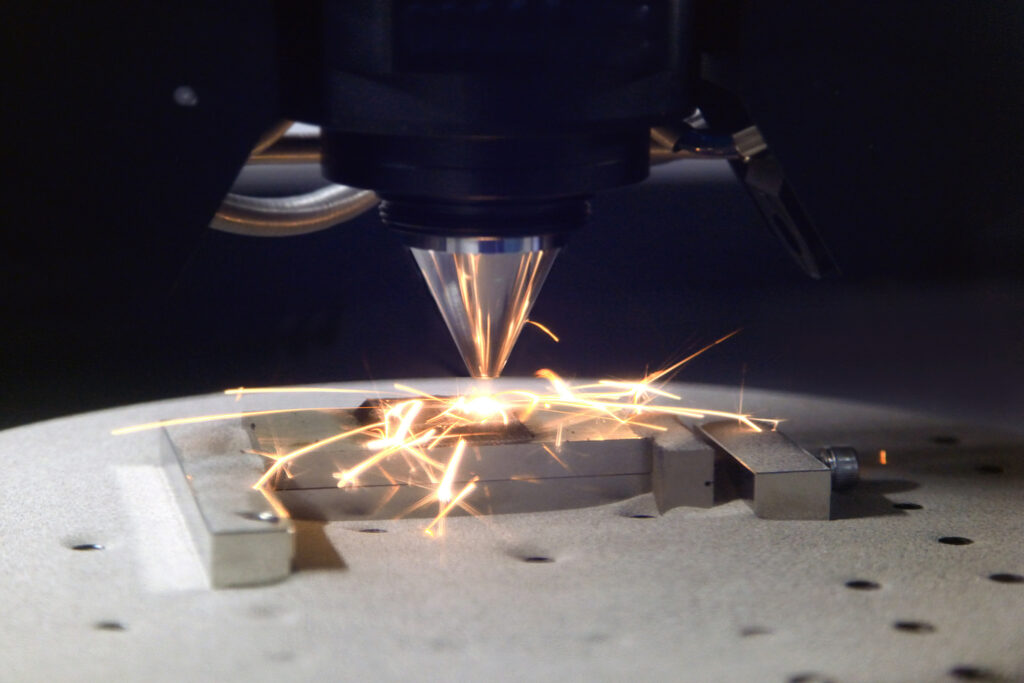
A laser beam concentrates energy into a small area. Depending on the material and process, that energy can cure a resin, sinter powder or melt metal.
A laser generally consists of a gain medium, a pump source and an optical resonator. Pumping supplies the energy used to amplify light by stimulated emission. The families discussed here include gas, bulk solid-state and fiber lasers; the last two both use a solid active medium.
CO₂, Nd:YAG and ytterbium-doped fiber (Yb-fiber) lasers are examples studied in AM. Excimer lasers also appear in the literature, including for certain UV applications; inclusion in a review does not imply widespread use in every type of 3D printer.
For those who are new to this space, please note that the CO2 laser is one of the first gas lasers that has been developed in the industry. In CO2 lasers, the gas-state gain medium fills the discharge tube and is electrically pumped by a DC or AC current to achieve population inversion for lasing.
Nd:YAG lasers (neodymium-doped yttrium aluminum garnet laser; Nd3+:Y3Al5O12 laser) are a type of solid-state laser using rod-shaped Nd:YAG crystals as a solid gain medium.
A fiber laser is a type of laser where the active gain medium is an optical fiber doped with rare-earth elements whereas excimer lasers use ‘excimers’ as the gain medium and are pumped by pulsed electrical discharge to produce nanosecond pulses in ultraviolet (UV) region.
Alex Kingsbury emphasizes that power settings must stay within the manufacturer’s specified limits: “Lasers also come in different power levels, and they can be turned up or down according to the parameter settings chosen for any given material or print feature desired.” The move towards fiber lasers in metal AM cannot, however, be explained by rated power alone: material absorption and beam delivery also matter. CO₂ lasers can reach high industrial powers; they are not inherently unable to melt metal.
Laser stereolithography (SLA), selective laser sintering (SLS), laser directed energy deposition and laser powder bed fusion of metals use sources suited to their materials. SLM in this interview refers to the last of these. Not every vat photopolymerization or directed energy deposition system uses a laser.
Michael Rath, Inside sales representative at Novanta explains the differences in the use of lasers within these processes :
“The lasers used in Laser Additive Manufacturing (LAM) machines are primarily defined by the laser-material interaction of the base printing material. The central wavelength of the laser must align with the absorption spectrum of the 3D printing material. UV lasers (around 355 nm) are required for machines that use photo-polymer resins, CO2 lasers (around 10 µm) are required for SLS machines that use polymer powders, and IR lasers (around 1 µm) are required SLM machines that use metal powders.
Photo-polymer resin machines typically use frequency-tripled UV solid-state lasers with 500 mW to 1.5 W output power. The polymer powder bed machines typically use RF-excited, enclosed, metal tube CO2 lasers that are optimized for CW emission with 30 W to 150 W output power. The metal powder bed machines use single-mode and ring mode YB-fiber lasers with 200 W to 3000 W output power.”
These examples describe machine families discussed in the interview. The wavelengths and powers are not requirements for every resin or metal: selection depends on absorption, material and system configuration.
Essential criteria for choosing a laser
“The central wavelength of the laser is the most [important] criteria for selecting a laser. As described above, the central wavelength of the laser must align with the absorption spectrum of the 3D printing material. In addition to wavelength optimization, lasers are qualified based on several performance characteristics including power stability, divergence stability, wavelength stability, output power, and beam quality (M²). The pulse-to-pulse stability for pulsed lasers or average power stability for CW lasers directly affects the width of the printed material, and thus the quality of the part to be built. Divergence stability and wavelength stability can have a similar impact. The output power of the laser typically dictates the print speed and throughput. Wavelength, beam quality (typically expressed as M²), and choice of scan head will affect the size of the beam focus, and therefore define the minimal feature size of the printed part,” Rath states from the outset.
The table below retains historical reference values from the 2017 review by Lee and colleagues. It is neither a current product catalogue nor a set of guaranteed printer specifications. Its power figures describe different industrial laser sources, not necessarily typical powers used in AM.
| Parameter | CO₂ | Nd:YAG | Yb-fiber | Excimer |
|---|---|---|---|---|
| Application examples | Polymer SLS; other thermal uses depending on system | Metal processes; SLA after UV conversion | Powder bed fusion and laser deposition | Specialized UV photopolymerization |
| Operation wavelength | 9.4 & 10.6 μm | 1.06 μm | 1.07 μm | 193, 248, and 308 nm |
| Output power — historical values | Up to 20 kW | Up to 16 kW | Up to 10 kW | 300 W average, pulsed operation |
| Pump source | Electrical discharge | Flashlamp or laser diode | Laser diode | Electrical discharge |
| Operating mode | CW or pulsed | CW or pulsed | CW or pulsed | Pulsed |
| Pulse duration | Hundreds ns-tens μs | Few ns – tens ms | Tens ns – tens ms | Tens ns |
| Beam parameter product, BPP (mm·mrad) | 3 – 5 | 0.4 – 20 | 0.3 – 4 | 160 × 20 (vertical × horizontal) |
Source: Lee et al., Lasers in additive manufacturing: A review (2017). Values depend on the model and operating mode. CW means continuous-wave operation. BPP, measured in mm·mrad, is distinct from the dimensionless M² factor.
Beyond the table, Kingsbury suggests several practical checks:
“For starters, there are some simple quality parameters you can check to quickly gauge the quality of a laser. The first is the beam parameter product (BPP). The BPP gives you information on how well a beam can be focused to a small spot size. This is relevant for AM as the laser spot size will determine your melt pool width.
Another good measure of beam quality for Gaussian-shaped beams, i.e. most laser beams used in additive manufacturing, is the M2 value. The lower the number and the closer to 1, the better the quality of the beam, and the more tightly you can control it.
An OEM that builds 3D printers will also consider other factors relating to the laser such as how much ‘overhead’, i.e. spare power, the laser has built in.
As we move increasingly to multi-laser systems, we also need to consider how well synchronized those lasers are.”
BPP combines beam waist radius and divergence. The dimensionless M² factor compares propagation with an ideal Gaussian beam at the same wavelength, as explained by Coherent. A value close to 1 supports tight focusing, but does not mean a Gaussian profile is optimal for every manufacturing operation.
The impact of lasers on 3D printer cost
While the focus has been made on 3D printers in this article, it should be noted that in AM, it’s possible to use CO2 lasers to polish the surfaces of 3D printed polymer parts and make them smoother. According to Novanta’s team of experts, this is a common procedure when printing customized shoe insoles.
Lasers and optical components contribute to industrial printer cost. Some equipment manufacturers, such as ONE Click Metal, have focused on this area to offer more accessible systems. Source cost nevertheless needs to be considered alongside cooling, scanning, integration and maintenance.
At the time of the interview, Novanta offered the following indicative segmentation, rather than quotations or universal pricing rules:
According to Novanta’s team of experts, “The type of laser (i.e. CO2 versus fiber) and output power will impact the total cost of the printer. For example, for fiber lasers, there are roughly three categories:
- Low-cost air-cooled continuous wave single mode fiber lasers up to 500 Watts
- Mid-cost water-cooled continuous wave single mode fiber laser above 500 Watts
- High-cost water-cooled continuous wave ring mode lasers
For CO2 lasers, there are similar categories:
- Low-cost glass tube CO2 lasers with under 100W output power
- Mid-cost RF-sealed CO2 lasers with under 100 W output power
- High-cost RF-sealed CO2 lasers with more than 100W output power”
To that, nLIGHT’s expert notes that “lasers, or the ‘light engine’, i.e. the whole optical train including the scanner, form the very heart of a 3D printer, and typically the light engine consists of a reasonable portion of the total bill of materials for a 3D printer. CO2 lasers, as mentioned above, are cheaper than fiber lasers, so in cases where they work well, i.e. for polymer systems, they are the laser of choice.” Scanner selection also affects system cost and capability.
Additive Manufacturing techniques involving lasers are used in several industries, including electronics, medical, automotive, and aerospace. With the growing need for industrial applications, lasers will continue to play a crucial role in the pursuit of target performances. Their choice should therefore always take into account their operating principles, optical configurations, and comparative analysis of their respective advantages and limitations.
Editor’s notes
To discuss this topic, we invited two companies with key expertise on laser technologies.
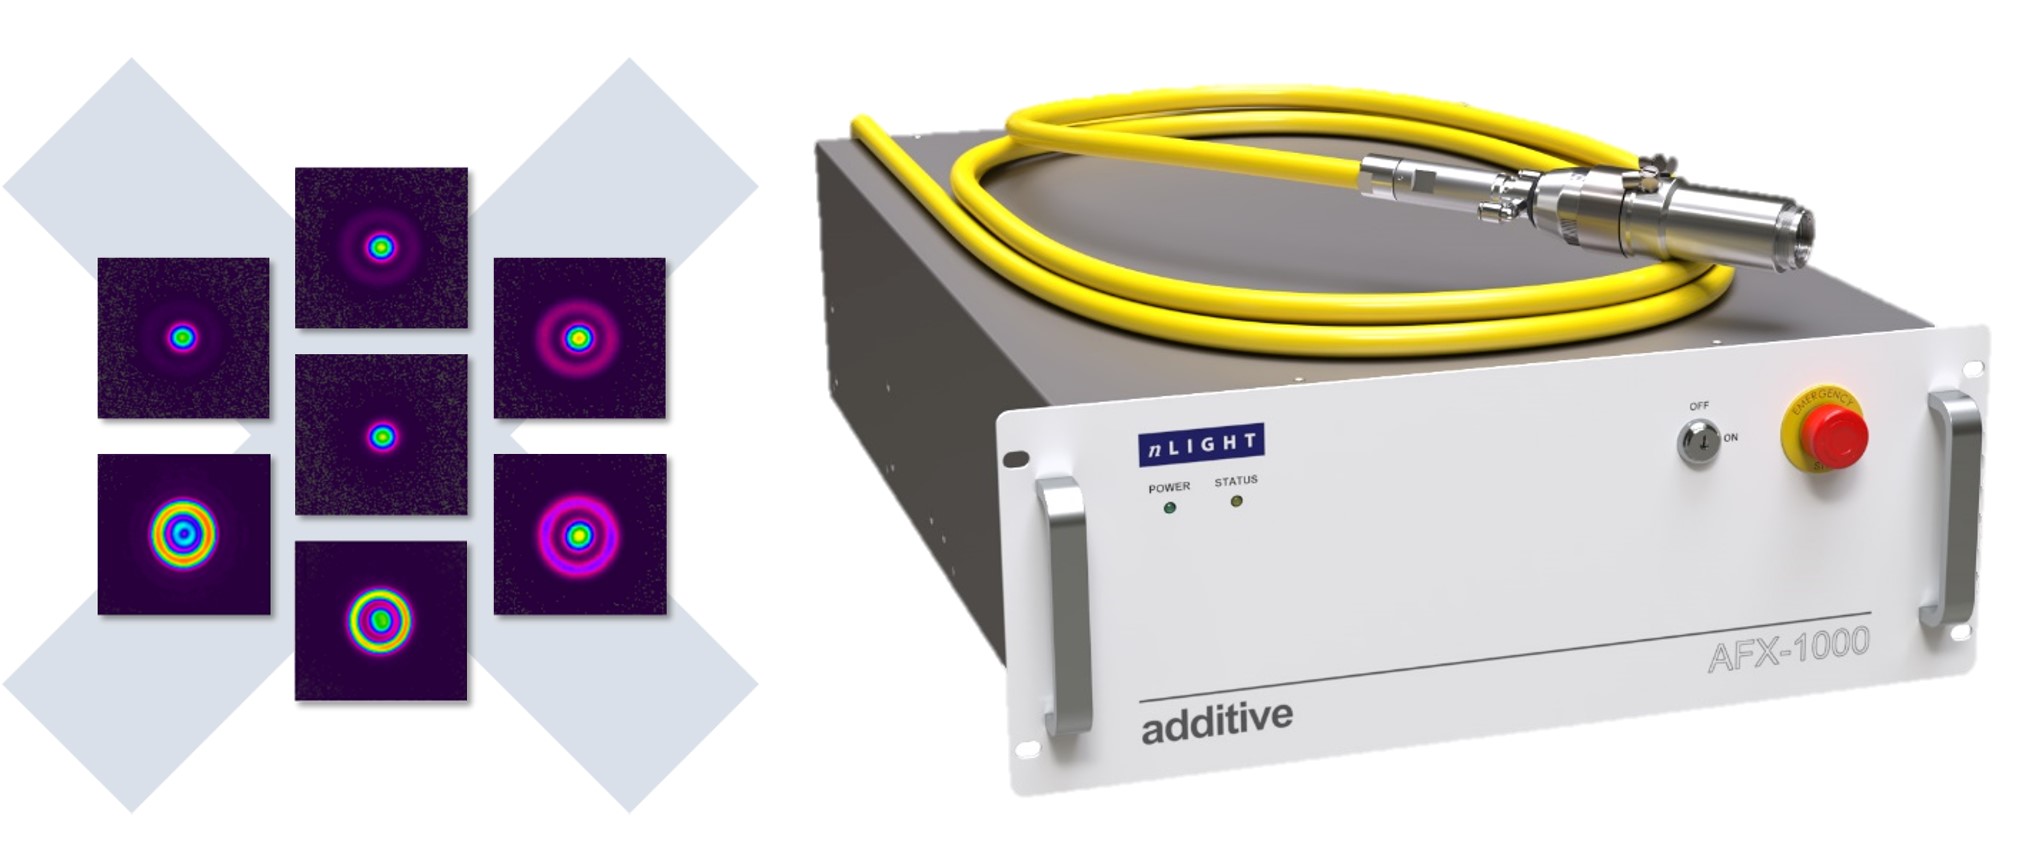
nLIGHT, founded in 2000, develops and manufactures laser sources. At the time of the interview, the company described Gaussian-profile lasers from 500 W to 1 kW and an AFX range from 1 to 1.5 kW. Its 2023 AFX data sheet shows selectable profiles from single-mode to ring-shaped distributions, without free-space beam-shaping optics. Selection depends on the material, geometry and intended result. Stability and productivity gains require qualification under the relevant process conditions. A power of 1 kW is neither a universal standard nor a physical threshold beyond which every melt pool becomes unstable.
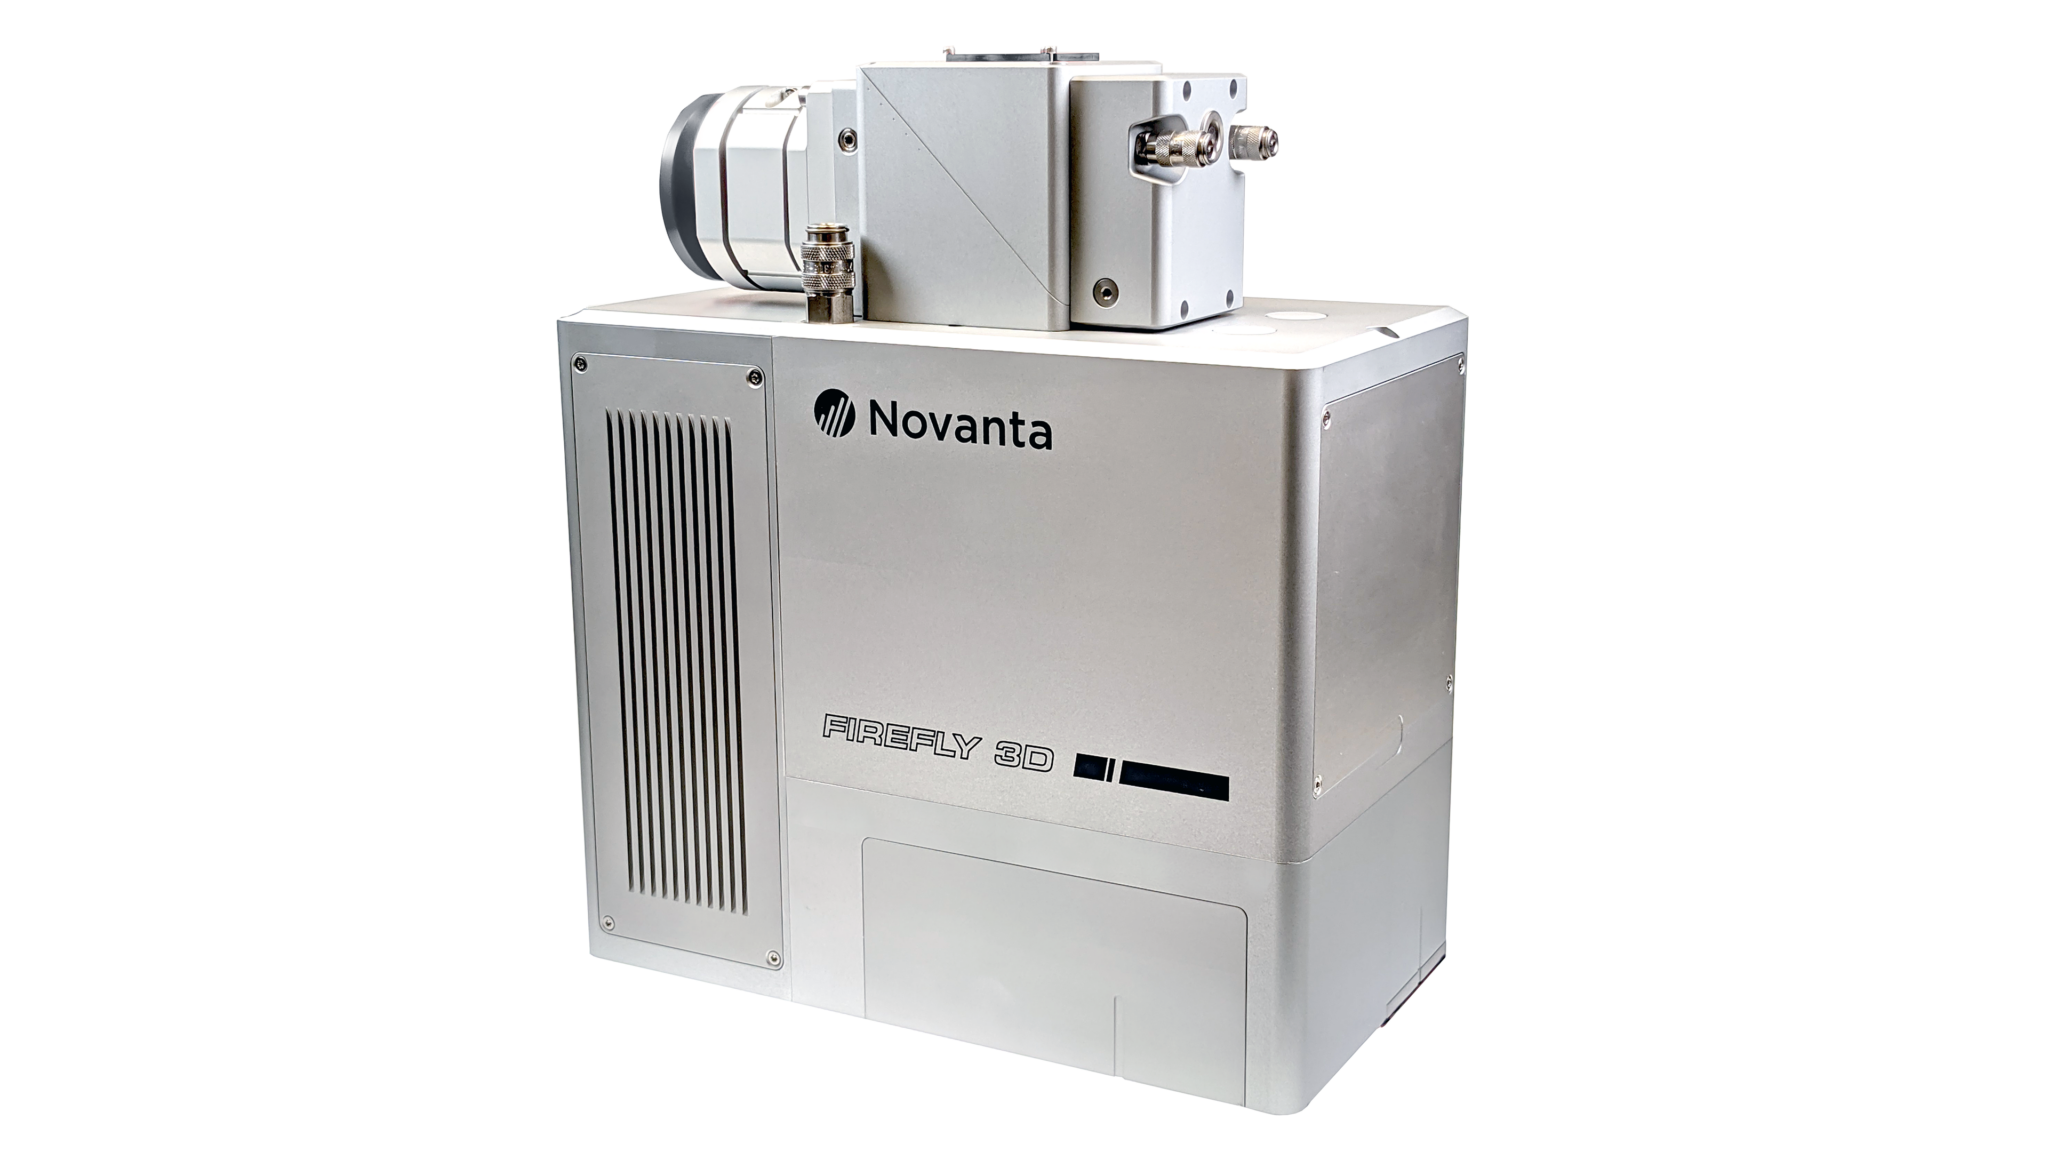
In this 2024 interview, Novanta discussed Synrad CO₂ lasers for polymer SLS and its beam delivery systems. Its three-axis FIREFLY3D scan head is intended for laser powder bed fusion. The manufacturer describes multi-head configurations, automated calibration and, depending on configuration, field overlap of up to 100%. These statements come from its product documentation; they do not by themselves guarantee the performance of a complete printer.
This feature was first published in the May/June 2024 edition of 3D ADEPT Mag.
Review note: the table has been clarified, and general claims of a 1 kW stability limit and the exclusive suitability of ring beams have been removed. Interview quotations are retained except for the shortened power passage, whose technical scope is clarified in the surrounding text.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.