
Feature published in 3D ADEPT MAG in July–August 2020, then online in February 2021. Interviewees’ roles, processes and economic examples reflect that period.
Selecting additive manufacturing (AM) requires assessing both the technical feasibility and the business case for a part. This feature examines three selection approaches, with insights from Julien Cohen, then an application engineer at metal AM manufacturer and service provider 3DEO Inc.
The discussion focuses on metal AM. As Julien Cohen notes, “there are many ways to address this issue”. His experience at 3DEO and in large companies managing tens or hundreds of thousands of stock-keeping units (SKUs) is considered alongside research and industrial examples.
Three approaches to candidate selection
We have outlined three different frameworks that can be assessed before going down the AM route for series production.
1- A database of components and assemblies
Not every part benefits from a switch to AM. A first step is to establish selection criteria: dimensions, material, functional requirements, volumes, lead times and cost.
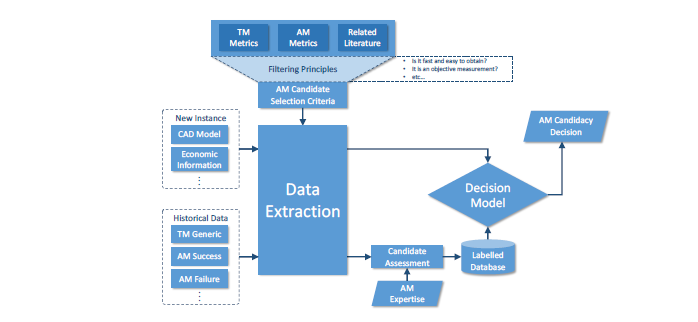
A framework proposed in 2019 by McGill University researchers combines design and production data with technical and economic criteria to identify candidate parts. It supports screening; the underlying data and assumptions still require verification before a production decision.
In practice, “there is no central library containing all the necessary data and metadata to make this decision. For example, how do I go search for parts in a specific size range, made via investment cast aluminum, at a certain annual quantity range? The first hurdle for many corporations is to make these data accessible in a searchable database.
Once that access is available, the problem can be addressed from multiple angles. In my opinion, rather than starting with a list of parts and identifying which AM process could be used for each, it’s more effective to identify a potential AM process and then filter out parts based on the known process limitations. This workflow can be roughly split into four steps:
- Choose an AM process to focus on (L-PBF, 3DEO’s Intelligent Layering®, DED, Cold Spray, etc.)
- Disqualify parts using absolute process limitations (i.e. maximum build volume, available materials, feature size capability, annual quantity)
- Rank the remaining parts using some kind of business case metric (which application would make the biggest impact to the business with a 20% cost reduction, 20% weight reduction, or faster time-to-market?)
- Pare this ranked list down to a manageable number of top opportunities, and examine these in-depth to determine which is worth pursuing”, Cohen explains.
2- The design analysis approach
Design analysis identifies parts whose performance could benefit from design for additive manufacturing (DfAM). Four aspects are considered here: functional integration, customization, lightweight design and efficiency in service.
Functional integration can combine several functions or components in one part. It may reduce assembly operations, size or manufacturing steps. The resulting design must still be checked for printability, cleaning, inspection and maintenance.
Customization allows geometry to be adapted for different uses or users, sometimes in small batches. Its value depends on the need for variation and the total cost of each configuration.
Lightweight design aims to reduce mass while meeting functional requirements. Topology optimization helps distribute material according to loads. Lower mass does not automatically mean lower manufacturing cost or reduced impacts: supports, machine time and post-processing must also be considered.
Efficiency in service concerns how the part performs during use: service life, operating costs, energy efficiency and other application-specific requirements.
This approach examines potential technical and economic benefits. Depending on the objective, a part may be a worthwhile AM candidate without redesign, although redesign can open further opportunities.
“People that work in the AM industry constantly get asked “can we 3D print this part?”, and the answer is almost always yes… but this is not the right question. What you need to ask is “should we 3D print this part?”
It’s possible that without redesign an organization can still reap benefits from switching to an AM process: shorter lead times, no tooling cost, decreased risk, etc. But without redesign, they will miss out on the incredible potential for optimization which AM design freedom offers. We have an incredible array of generative design, implicit modelling, and topology optimization software tools now at our fingertips, and it’s a shame to leave their capabilities on the table.
My strong opinion is that AM experience should be injected as far upstream in the design process as possible, and that AM can have a much greater effect on new product development and clean sheet design projects vs. existing products which are already tooled up and in production”, 3DEO’s application engineer points out.
Potential benefits alone are insufficient for selecting a part. The analysis must also identify incompatibilities in material, dimensions, quality or throughput, then account for post-processing, inspection and the supply chain.
3- “The supply chain scenarios”
Senvol proposes seven scenarios for identifying situations where AM deserves an economic assessment. They cover manufacturing cost, lead times, inventory, supplier dependence, remote locations, import and export costs, and functionality.
A part matching one or more scenarios warrants further investigation. This framework is a starting point, not proof of profitability or a rule that can definitively exclude AM on its own.
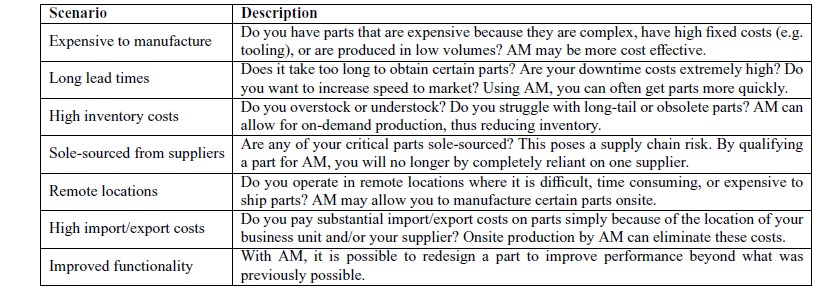
| Scenario | Questions and potential benefits |
|---|---|
| Expensive to manufacture | Are complexity, tooling costs or small batches making parts expensive? AM may offer a better business case. |
| Long lead times | Are procurement delays, downtime or time to market a problem? Assess whether AM can shorten the total lead time. |
| High inventory costs | Are stocks excessive, insufficient or difficult to manage for rarely ordered or obsolete parts? Consider on-demand production. |
| Single-source suppliers | Does reliance on one supplier create risk? Qualifying an AM route could provide another source. |
| Remote locations | Is delivering spare parts difficult, slow or costly? Consider whether local AM production is feasible. |
| High import/export costs | Do supplier or facility locations create significant trade costs? Assess whether local production could reduce them. |
| Improved functionality | Could redesign for AM provide performance that the existing manufacturing route cannot achieve? |
The questions make an initial assessment accessible. Potential benefits then need quantification with explicit assumptions and comparison with alternative processes; a positive answer does not replace that analysis.
Do these criteria differ from one AM technology to another?
Production volumes are part of the selection criteria. Cohen notes that “low volume” and “high volume” have different meanings across industries.
“High-volume production parts in the aerospace industry might mean a few hundred parts annually. Low-volume production in the industrial and automotive industries might mean tens of thousands of parts annually” the expert states.
Criteria must be adapted to the process under consideration. Cohen’s workflow above specifically starts with a technology’s limits; applying identical thresholds across processes would lead to misleading decisions.
“For example— while powder bed processes like L-PBF and EBM can enable significant optimization of strength-to-weight ratio, heat transfer capability, and internal fluid flow efficiency, the process is still extremely expensive and comes with a laundry list of limitations and considerations, especially in serial production (I’ve given conference talks specifically on the difficulty of using L-PBF in production). These processes can be fantastic tools for low-volume, high-cost parts, but with the right support design and process control can also be cost-effective for small parts which nest efficiently on the build plate.
Similarly, 3DEO’s Intelligent Layering® process was developed specifically for high-volume, low-cost applications— I’m talking 100k+ annual quantities and <$5 per part. Our process is unique in the metal AM space and overcomes many limitations inherent to emergent processes like binder jetting, as well as traditional processes like MIM and CNC machining. The types of applications that fit our process are completely different than those which fit many of the other processes on the market.
In the absence of widespread industry standards and technology maturity, making the correct choice of application requires deep knowledge of available AM processes, their pros and cons, and experience using them in the past. At 3DEO we maintain long-term production partnerships with our customers and offer our knowledge base to accelerate these types decisions” 3DEO’s spokesperson comments.
Editor’s note: the volumes, prices and process comparisons quoted by Julien Cohen describe 3DEO’s positioning at the time of this 2020 interview. They are neither a current quotation nor a guarantee for every part. Avoiding forming tools does not eliminate supports, finishing, inspection or industrialization costs.
In summary
Database screening, design analysis and supply-chain scenarios are three complementary selection approaches. They help structure the assessment of parts before comparing processes across manufacturing, post-processing, qualification, logistics and use.
This feature was first published in the July–August 2020 issue of 3D ADEPT MAG.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.