Opinion feature first published in the March/April 2022 issue of 3D ADEPT Mag. Contributors from 3Dresyns, Hexcel and Lehvoss share their views in the context of that period.
Powders, pellets, resins and filaments serve different needs in additive manufacturing (AM). Their use requires a material–process combination suited to the application. 3D ADEPT Media asked producers about resins, composites and filaments, their opportunities and their limitations.
3D printing Resins
Resin 3D printing covers several processes. In vat photopolymerisation, a light source selectively cures resin according to the digital model. Material jetting deposits material differently, so not every resin printer uses a vat. Formulation must match the wavelength, exposure and machine.
In 2022, laser stereolithography (SLA), DLP projection and LCD-mask systems were common approaches. Commercial solutions such as Digital Light Synthesis™ and Viscous Lithography Manufacturing (VLM) added to this landscape. Industrial suitability depends on repeatability, achieved properties and the cost of the production chain.
Single- and dual-cure chemistries have broadened the available properties, from rigid materials to elastomers. Comparison with injection-moulded thermoplastics remains useful when application, volume, performance and post-processing are considered. That comparison alone does not explain every obstacle to serial production.
Material jetting can combine materials where the machine supports it. Suitability for an end-use part depends on the system, formulation and service requirements. Choosing between lower- and higher-viscosity resins likewise involves processing trade-offs.
Viscosity describes resistance to flow and varies with conditions such as temperature. It affects processing. Nika Borges, 3Dresyns Sales & Marketing Manager in 2022, argues for higher-viscosity resins: “As a rule of thumb “the higher the viscosity of 3D resins the higher achievable mechanical properties and safety”, Nika Borges, Sales & Marketing Manager for materials producer 3Dresyns says, speaking of resin 3D printing.
In practice, two schools of thought are currently emerging when it comes to viscosity: the small group of people that see the advantages of low viscosity resins for SLA 3D printing and the other one that sees a range of opportunities in high viscosity resins. The role of resin viscosity has been largely explored for stereolithography, where a very low viscosity material is preferred. For Borges, the problem with low viscosity 3D resins, is that they “exhibit inferior mechanical properties, such as poor toughness and mechanical strength. They contain low viscosity monomers, [which can lead to] high toxicity (…).” The materials producer explains that “despite having lower viscosity”, its monomer free and monomer-based 3D resins stand out from the crowd as they“exhibit unique high performance and safety.”
These statements reflect the supplier’s view. Viscosity alone does not establish a resin’s safety or mechanical strength. Liquid resin must be distinguished from the cured part; its safety data sheet and product-specific printing and post-curing conditions must be consulted.
“A higher viscosity means a thicker resin. This has an effect on the reflux of the polymer and on the movements of the platform. If you know the volume of your 3D model and the density of the material you selected, you can easily calculate the weight of your 3D printed model”, resin materials producer Liqcreate said.
Viscosity and density are different quantities. Density relates mass to volume; it does not measure resistance to flow.
While high viscosity resins contribute in “making ultra-high performance safe materials”, Borges notes that at the production level, “they can be printed in most commercial printers at 25-50ºC after installing a heater.”
This statement is not an instruction to modify a printer: heating must be designed for or authorised by its manufacturer and remain within the material’s limits. Resin-specific processing guidance sets out applicable parameters and post-processing.
Viscosity can affect recoating, flow and resin drainage. Accuracy also depends on exposure, optics, calibration and shrinkage. A viscosity value alone therefore cannot predict a part’s accuracy or drainage.
No matter what type of materials are used, 3Dresyns currently urges 3D printer manufacturers to develop affordable and reliable bigger printers based on MLCD and DLP technology. At the end of the day, the variability related to each 3D printer can greatly influence the result of the finished product. Taking the example of light power, Borges explains:
“Depending on the chosen 3D printer technology, its design, configuration, light wavelength, power, its distribution across the vat and the cumulative operating time, the real light power available across the vat for printing may vary significantly, and consequently as well the printing settings for similar printers and even from unit to unit of the same model due to small production differences among units. The following graphs show the typical light output decays vs cumulative operating time of standard multicolor RGB LCD panels, monochrome LCD panels, digital lamp projectors and LED projectors, all typically used in SLA, DLP & LCD 3D printers.
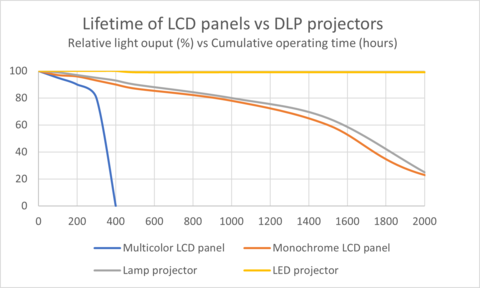
Unfortunately, light power varies and decays vs cumulative operating time. Even different units of the same model, new as supplied, often have 10-15% light power differences, which affect the overall printing results. Additionally, as shown on the graph above, light power decays versus the cumulative operating time of the printer. Light power variability upon usage and lack of light power control over time need to be addressed to promote the 3D industrial revolution. Right now, unfortunately, only few printer manufacturers have addressed these basic problems.
Lack of light power control, monitorization and prevention of its decay are some of the main reasons for frustration, printing problems, variability, or failure. Professional printing requires printers with constant specifications to promote the shift from traditional manufacturing into additive manufacturing.”
The chart and numerical variations above are presented by 3Dresyns as illustrations. They do not establish a guaranteed lifetime or tolerance for every printer; comparison requires measurements under defined conditions.
Today, the issues of costs and applications continue to enliven discussions across resin 3D printing users.
As far as applications are concerned, advanced users hope to see further developments with photo-curable composite or nanocomposite resins.
Industrial cost includes material, machine, consumables, post-processing, inspection and scrap. Higher volume can change this balance without automatically guaranteeing a lower unit cost.
Composites
Composites combine different constituents. Those discussed here use thermoset or thermoplastic polymer matrices reinforced with short or continuous fibres. Reinforcements can include carbon, glass, aramid or basalt, or plant fibres such as jute and flax. Aramid is synthetic and basalt is mineral-based.
Our feature on exclusive feature dedicated to composites 3D printing examines this combination of materials and processes and its industrial applications.
Several process families can shape these composites. The table below compares four approaches; advantages and limitations must be assessed for a specific material and machine.
| Process | Potential | Considerations | Fibre orientation |
|---|---|---|---|
| Sheet lamination | Assembly of reinforced layers, with orientation selected during lay-up. | Cutting waste, cavity access and interlayer bonding require attention. | Depends on the sheets and their lay-up. |
| Powder-bed fusion | Short-fibre-filled polymer powders; the powder bed can support parts. | Powder flow, fusion and porosity must be controlled. Reuse depends on powder condition and refresh requirements. | Depends on the powder and spreading; conventional processes do not lay continuous fibres. |
| Vat photopolymerisation | Shaping reinforced resins with the potential for fine detail. | Viscosity, settling and light penetration can limit fibre loading. | Depends on formulation and process; some experimental methods use a field to orient fibres. |
| Material extrusion | Short-fibre-filled polymers or continuous reinforcement with suitable equipment. | Nozzle wear or clogging, porosity and interlayer bonding require control. | Deposition paths influence orientation and part properties. |
Advancing composites AM mainly depends on the partnerships between manufacturers and adopters. According to Regina Pynn, expert at Hexcel, “end users drive the technical requirements, and that’s what flows up through the supply chain to inform what machine and material producers focus on. The tailoring of material properties you can achieve in composites and the differences that build orientation can drive in composite materials, make that link a real driver for innovation.”
That being said, it’s interesting to remember that composites AM opens up new possibilities for lightweighting, when experts are looking to transitioning from metal to polymer. “Lightweighting has been a driver in traditional composites adoption and that trend continues in additive”, Hexcel recalls. Indeed, while strength and stiffness are often mentioned as desired properties delivered when leveraging composites (and especially continuous fiber) with AM, they are not as powerful as the advantage of lightweighting.
“When we’re replacing metallic components with HexPEKK-100, which is an SLS fabricated CF PEKK material, the weight savings for our aerospace customers is as important as the cost savings we bring to the program. Composites also lend themselves to customization of materials properties. Conductivity, flexibility, impact resistance: all these areas affect where a material can be controlled and adjusted in a composites material system”, the expert outlines.
Carbon-fibre-reinforced polymers (CFRP) can offer useful stiffness-to-weight ratios. Electrical conductivity and cost depend on matrix, reinforcement, loading and orientation; neither is uniform across this material family.
Glass-fibre-reinforced polymers (GFRP) generally provide electrical insulation and use fibres that cost less than carbon fibres. The complete part’s properties still depend on composition and manufacture.
To open more room for opportunities, Hexcel prefers to focus on new properties composites enable when combined with AM – that one cannot achieve with conventional manufacturing processes. “At this phase of adoption most customers are trading AM versus traditional manufacturing methods. Composite AM has a great advantage when it comes to this competition. Against traditionally metallic components composites can bring properties like EM signal shielding, which we have in our HexPEKK-EM offering, that previously were a show stopped for non-metallic replacement.”
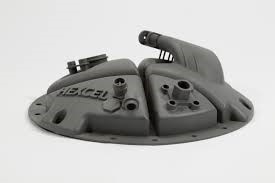
Another issue is generating material allowables alongside machine and part qualification. These design values need representative data and, where required, a statistical basis. The aim is not to redesign a material for every part, but to establish data that can be reused within a defined range of validity.
“For many of our aerospace composite customers it’s the current process around material allowable generation along with machine and part qualification, so for Hexcel that has led to us focusing on fleet homogeneity and material allowable work to give the technical community the information they need to design the material without starting at the beginning for each new part. Long term that means leaning more on in-process or post-process verification, like NDI or quality sampling, and less on locking down every specific build detail for every specific piece. You can move a lot faster with adoption if everyone agrees on what good hardware looks like at the end and you’re giving the manufacturing team the ability to change and optimize the process to get there. That feeds greater efficiency, which gives the adopters a broader business case for where this technology makes sense”, Hexcel notes.
Filaments
Filament extrusion is one family of additive manufacturing processes. It raises questions about performance, certification and environmental impact.
Environmental impact cannot be inferred from carbon content or reduced scrap alone. Some polymers can be bio-based; assessment should consider feedstock, energy, service life and end-of-life treatment. Recyclability claims must also consider the processing routes actually available.
In reality, they are quite “unclear about how sustainable [their materials] are, e.g. percentage of recycled material, the provenience of the recycled portion, etc. To increase the adoption of sustainable materials in production, customers have to trust that the material is sustainable with good engineering properties and, above all that, it will be reproducible”, Thiago Medeiros Araujo, LUVOCOM 3F Global Product Manager shares.
Characteristics like recyclability and reusability were a trend that came into full force in 2021 as a different approach to sustainability in 3D Printing but mentioning them alone is no longer enough today.
Certification
Certification applies to a defined scope: material, emissions, process or part, depending on the scheme. Indoor-air testing alone does not demonstrate mechanical performance or suitability for an industrial application. Medeiros Araujo stresses the link between material and process:
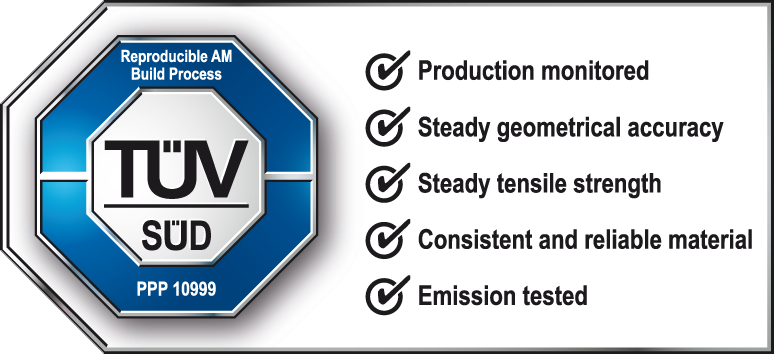
“Certifying a material per se in 3D printing is not something that adds value, as in most cases, its properties are directly related to the way the material was printed. However, having an independently certified build process has an enormous impact on the adoption of the material as it gives the customer enough confidence and trust to use the material straight away. So, it saves the user not only costs for having the material assessed but it also reduces the time for adoption”.
A certificate must be read together with its scope and conditions of validity. It does not remove the need to check application-specific requirements; the mark reproduced in this feature is a historical illustration.
Metal 3D printing
Metal-polymer filament extrusion is currently gaining momentum as professionals are continuously looking for affordable metal 3D printing solution.
In 2022, this segment included machines offered by 3DGence and filaments developed by Nanovia or BASF. These offerings combine printing with subsequent treatment steps.
“However, we have to bear in mind that it is not only about producing the metallic filament but providing the customer with the whole structure for further processing of the parts, e.g. de-binding and sintering”, Lehvoss’ expert alerts.
For filaments designed to produce a metal part after removing a polymer binder, debinding and sintering form part of the manufacturing chain. Shrinkage, density and final properties must be controlled. This does not apply to every filament containing a filler or additive.
Moving forward, one of the main challenges of the industry remains to achieve a “first time right” solution, no matter what material is used. And to do this, it’s important to recall that it’s a stage that can be reached through collaborations between various stakeholders. As Medeiros Araujo said, “each partnership demands a lot of commitment and effort from both sides to make it a flawless experience on the additive manufacturing journey of the customers.”
Notes to the readers
This opinion feature was first published in the March/April 2022 issue of 3D ADEPT Mag, with contributions from 3Dresyns, Hexcel and Lehvoss Group on resins, composites and filaments.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.