


Feature published in the January–February 2020 issue of 3D ADEPT MAG, then online in June 2020. XYZprinting’s account and the models mentioned reflect that period.
With the contribution of XYZprinting.
Resin 3D printing produces detailed parts from photopolymer formulations. This 2020 feature examines laser SLA, DLP and LCD processes, selection criteria and material-handling considerations. Stereolithography was developed in the 1980s; other exposure architectures subsequently expanded the range of resin systems.
Vat photopolymerisation selectively solidifies liquid resin, layer by layer. Laser SLA scans the cross-section with a laser; platform movement depends on machine architecture. DLP projects the section using a micromirror array. LCD, often called MSLA, uses a liquid-crystal screen to selectively mask LED light.
What should you consider when choosing a resin 3D printer?
Among all the additive manufacturing technologies that exist, resin 3D printing is mostly compared to FDM 3D printing. If the first reason that might explain such a comparison is the price of both types of technologies, it should be noted that other characteristics might help tip the balance in favour of one rather than the other. Indeed, the printing process, design considerations, pre-processing, and post-processing are very different.
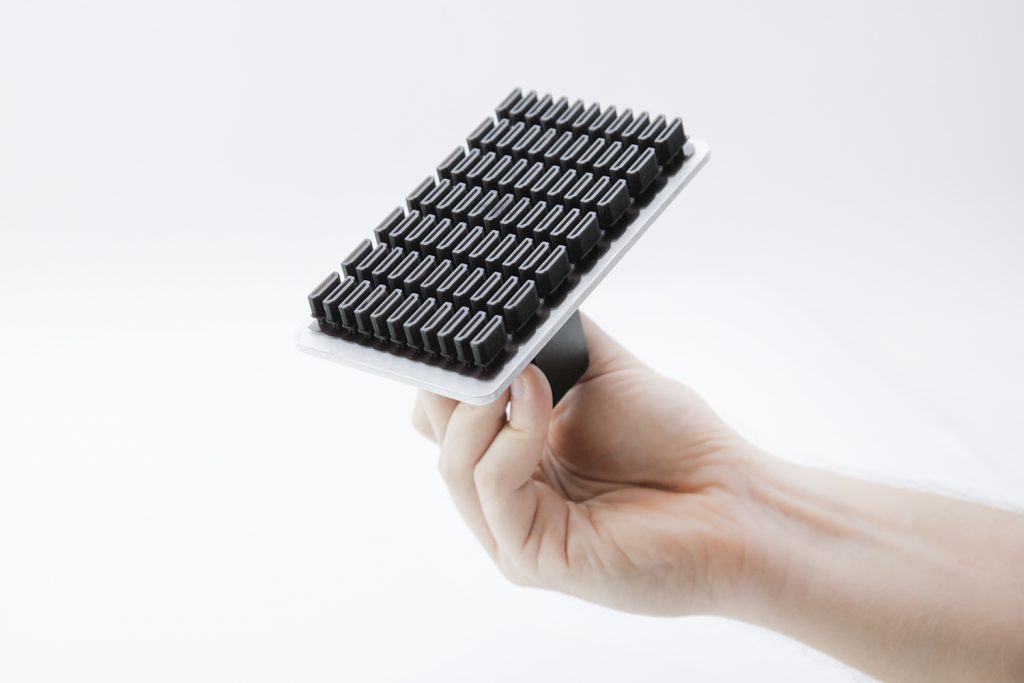
More importantly, when it comes to compare resin 3D printing technologies to one another and how they achieve the desired accuracy and precision, these features – alongside materials and software settings – also come into play. Indeed, we shouldn’t forget that 3D printing remains an additive process. Therefore, each layer might lead to an opportunity for inaccuracy and the printing process can determine the level of precision of each layer. Accuracy and precision are crucial in some applications like dental or surgical guides and despite the various analyses we could make, reality shows that accuracy and precision are often better portrayed and evaluated when we discover the differences between machines supplied by various manufacturers.
Machine footprint and build volume
Footprint and usable volume are distinct criteria. DLP does not imply a larger machine than laser SLA, and resin systems are not all limited to small parts. Assess the usable dimensions.
Orientation, overhangs and supports
Overhangs and isolated regions may require supports depending on orientation, geometry, resin and separation forces. Check the system’s design guidance; a failed feature can leave debris in the vat.
Plan for post-processing
As you may know, post-processing is no longer a step to neglect since every operator almost always has to go through it before getting the final and desired result.
Washing removes uncured resin. Drying, any required post-curing and support removal follow the material’s specified sequence. Wash product, duration and post-curing parameters must match the resin: isopropyl alcohol is not a universal instruction.
However, in this specific case, the post-processing stage should not always be seen as the “dirty work” to do. With resin 3D Printing, depending on the resin material that has been chosen – as well as the post-processing and finishing possibilities, the operator can achieve a very nice rendering.
Why should we use one specific resin 3D printing technology over another?
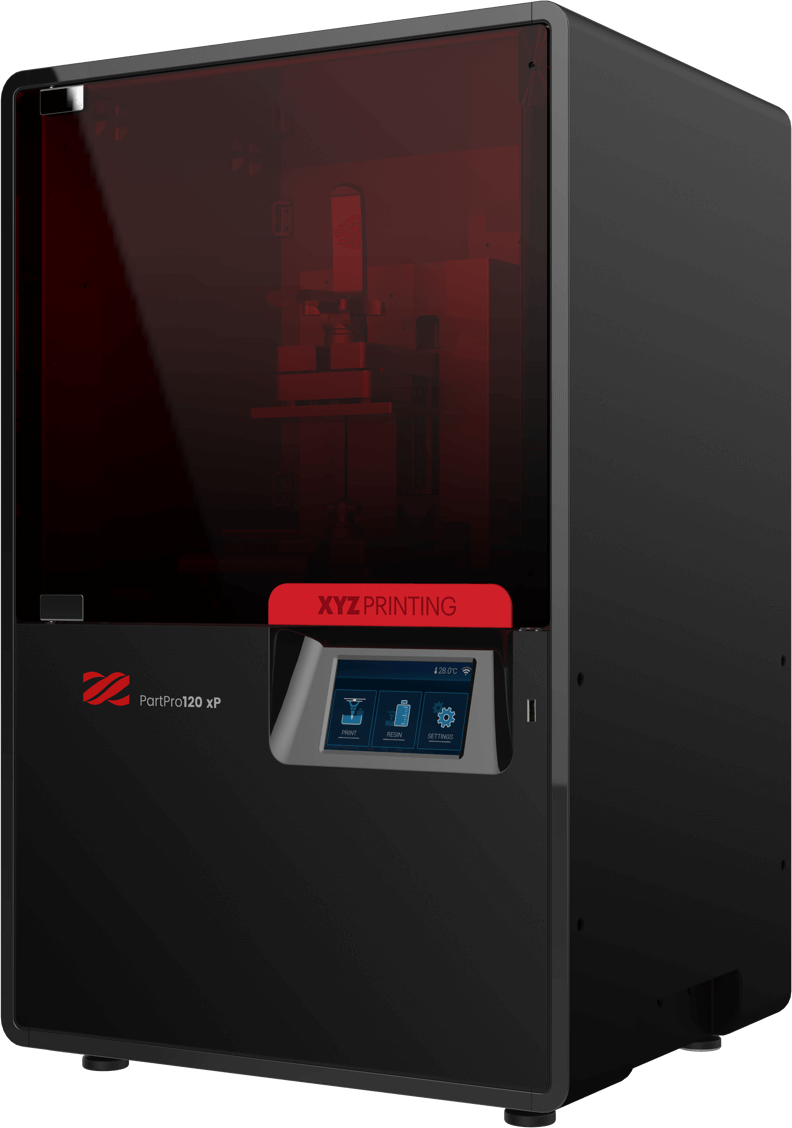
Fernando Hernandez, then Head of EMEA at XYZprinting, presents the manufacturer’s perspective. Its portfolio covered several technologies, including SLS, SLA, FDM and DLP; this feature highlighted the PartPro120 xP DLP printer.
Below, he describes the advantages and limitations he attributed to these technologies in 2020:
“It comes down to the taste of the chef in the kitchen. Each technology will have its fair share of pros and cons, but we maintain today that DLP technology now offers the best combination and balance of resolution, speed, build dimension and cost. That doesn’t mean SLA doesn’t continue to play a big role in the products we manufacture though, since it continues to provide very fine details for large building volumes, all the while keeping prices low.
LCD on the other hand is a technology that often falls short, for the reasons below:

1- LCD life is much shorter for UV light source. The life of the LCD panel with the UV LED back light wavelength (of 365 ~ 405nm) is generally very short (~ 1000 hours of life), which significantly increases the printing cost.
2- LCD uniformity is worse because of crosstalk issues. Once light is emitted from the pixels, it mixes with the light emitted from other nearby pixels. This effect favours consumer markets, since it smooths the image and prevents users from spotting any pixel mesh unless they are looking very closely. This works against 3D printing resolution though, as it means that the images are blurry and not crisp, meaning the models can’t be well-detailed. In LCD, small details are lost, so things like small holes may be closed or not circular, for instance.
3- LCD’s pixel size is larger than the DLP UV light source. Therefore, resolutions advertised on LCD panels are from the origin, but not the resolution at which the light source will reach the print bed.
4- LCD’s light intensity is much weaker and this negatively affects the overall printing quality.
5- The source of an LCD panel is irregular. The LCD panel is used in the consumer market, meaning that printing special sizes is difficult and it doesn’t guarantee supply and/or quality for 3D printing. For the moment, those panel prices are cheap because 3D printing is enjoying a wave of mass production of those panels for consumers Market (TV, tablets, etc). But once consumers jumps to other technologies, 3D printing market quantities won’t be able to sustain the production and therefore it won’t be possible to keep a similar market price to what is available now.
Meanwhile the print quality of the DLP printer exceeds LCD in multiple ways. The details are higher and within all resin technologies, DLP offer the lowest loss of details, and it also proportions from 3D model to physical. Historically, the biggest handicap for DLP was that it was difficult to get a decent building size for decent pricing, but that barrier is fixed nowadays; building plates are bigger and thanks to technologies such as our UFF (Ultra Fast Film) we are able to print up to 70 times faster than before, beating printing speed and productivity of equivalent technologies in FDM and SLA, while also beating in resolution and detail.”
Reading context: this comparison is XYZprinting’s commercial perspective in 2020. The 1,000-hour lifetime and “up to 70 times” improvement are not general guarantees. This is not a current comparison of all LCD and DLP printers; performance must be checked for the system and application concerned.
The good and the bad about resin 3D printing materials
Photopolymer resins are formulations designed to react to light. Properties and hazards vary with composition and state, whether liquid or cured.
Resins can produce fine detail and smooth surfaces. Results, throughput and accuracy depend on geometry, settings, material and post-processing; this does not establish general superiority over every other process.
Handle uncured resin and wash products according to their safety data sheets. Manufacturer guidance specifies ventilation and suitable skin and eye protection. Printer price does not remove these requirements.
Collect residues and wash liquids according to supplier instructions and local rules. “Water washable” does not mean contaminated liquid can go down a drain.
An “eco-friendly” claim needs evidence for the formulation and intended use; it does not guarantee harmlessness or biodegradability.
Long-term performance depends on formulation, post-curing and exposure to light, heat or moisture. UV ageing can degrade properties; it is not simply continued curing that necessarily ends in fracture.
Applications of resin 3D printing technologies
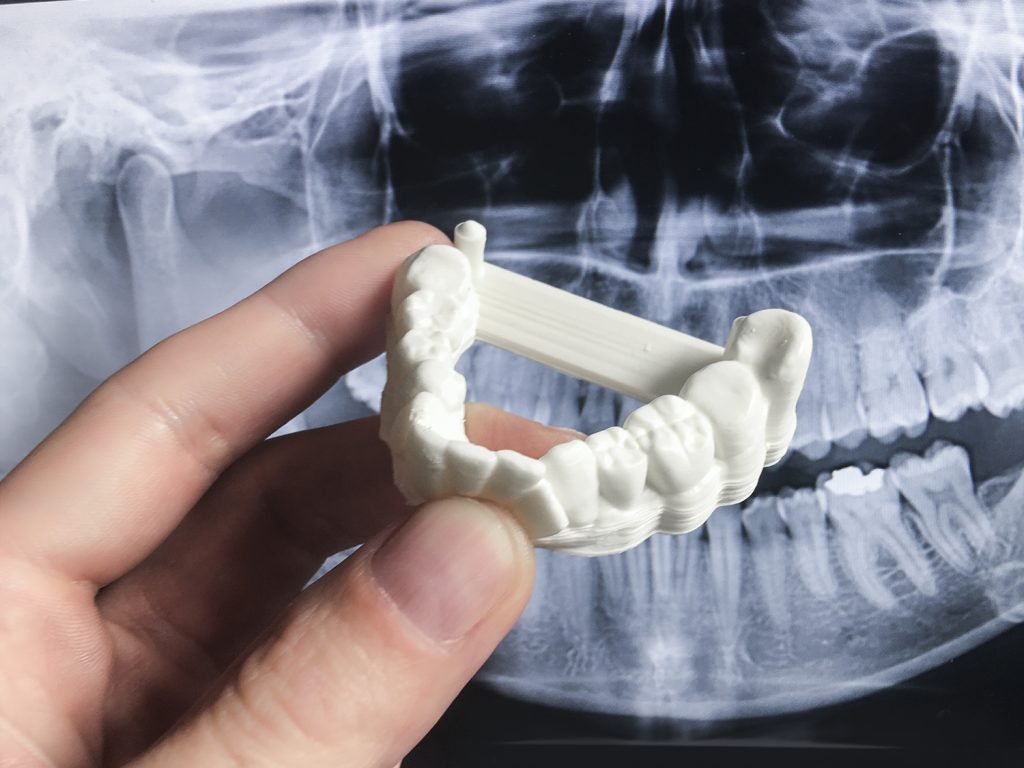
Jewellery and dentistry provide application examples, from working models to some final parts. They require suitable resin and manufacturing workflows; medical uses need validation for their intended purpose.
Fernando Hernandez also discusses end-use parts: “Printed resin models are not only used for prototyping, but also for creating the finished product. The key to doing this well, however, is to identify the precise mechanical properties required for the part’s final use. We need to consider the forces the end-product will be under, what temperatures it will be exposed to and more, and from there select the resin that is more suitable for the product’s needs. Nowadays, the industry is seeing resin-based printers used for mass production of parts in the automotive industry, production machines and final parts, to name a few. At The New Kinpo Group, we use resin-based printers to print a variety of final product parts.”
Furthermore, depending on the material used, it is possible to explore applications that go beyond these two sectors. “Certain resins can be more rigid, flexible and tougher than other resin strains. Some are able to simulate ABS mechanical properties while others have high temperature resistance, beating many of the most common thermoplastics. At times, the finished product of a resin-based model is smoother than its FDM counterpart for the same price range, making it a more viable and suitable option for creating final products”, explains XYZprinting spokesperson.
Material jetting, including PolyJet, can also use photopolymers and produce smooth surfaces. It differs from the vat photopolymerisation processes discussed above.
Mammoth is Materialise’s large-format stereolithography technology, not a generic resin family. Achievable size depends on the system and selected material.
A grey resin can suit display models and painting, but colour alone does not define its properties or fitness for an application.
Concluding thoughts
Selection should start with part requirements: size, detail, properties, throughput, total cost and working conditions. Representative test parts help compare results before investment. Assess post-processing, consumables, maintenance and material data, as well as purchase price and advertised resolution. Resin, filament and metal processes address different needs.
This dossier was initially published in the January–February 2020 issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.