

Feature first published in 3D ADEPT MAG in February 2019, then online in May 2021. Product examples and Linde’s statements reflect that context; editorial clarifications distinguish storage, printing and post-processing.
Additive manufacturing involves more than a machine and a material. In several processes, gases also help protect the feedstock, transport powder and control the build atmosphere.
Their role varies with the process, alloy or polymer, and required properties. Gases used during printing should therefore be distinguished from those used to produce, handle or store powders and in particular post-processing operations.
Argon and nitrogen are common process gases, but they are not interchangeable. Argon is inert; nitrogen can react with certain metals under process conditions. Linde’s argon documentation, for example, describes its use with metals susceptible to nitriding. Selection depends on the material–process combination.
How are they used in AM processes?
This feature examines laser powder bed fusion, laser directed energy deposition (L-DED), selective laser sintering (SLS), and arc- or plasma-based deposition. Their gas requirements differ.
In laser powder bed fusion of metal, argon helps limit reactions with the surrounding atmosphere. Controlling residual oxygen, humidity and gas flow contributes to process stability; it does not by itself guarantee part quality. Gas flow above the powder bed also carries away spatter and fumes that could interfere with the laser. Inerting is part of process control, not a substitute for appropriate powder-handling precautions.
According to a research carried out by Linde, a specialist of gases, for these reasons, “inert gases are introduced into the sealed printing chamber to create a highly controlled atmosphere, but there are other atmospheric gases used in a variety of applications vital to the AM process.”
In powder-fed L-DED, a carrier gas transports powder to the substrate through the feed nozzle. Shielding gas can also surround the melt zone. Wire-fed L-DED systems instead supply metal wire to the deposition zone.
“The powder or wire is thereafter melted to form a deposit that is bonded to the substrate and grown layer by layer. An additional gas jet – comprising of argon or tailored gas mixtures – which is concentric with the laser beam, provides additional shielding or process gas protection.”
In some polymer SLS systems, a CO₂ laser heats powder in a nitrogen atmosphere to limit reactions with air. CO₂ here identifies the laser’s active medium; it should not be confused with the gas surrounding the powder. Atmosphere compatibility must be checked for each material and machine.
Lastly, gas-metal arc welding (MIG/MAG) and plasma welding techniques enable the melting of metal filler to form a 3D component layer by layer. Shielding gases such as argon, helium and gas mixtures are compatible with this process. They “protect the hot substrate against the ambient atmosphere and adjust the metallurgical properties of the component being created. Efficient cooling of the generated component is done via the application of cool gases during the welding process to improve productivity.”
Editorial clarification: these examples are not a universal gas recipe. MAG uses active gas mixtures; other configurations employ inert gases. Mixtures and cooling conditions must suit the application, as noted in Linde’s overview of AM gases.
These uses show why atmosphere control is a manufacturing parameter in its own right. An enclosed chamber may use argon or nitrogen depending on the material; this does not imply mixing them. Other processes use local gas shielding.
Powder storage and print-atmosphere control
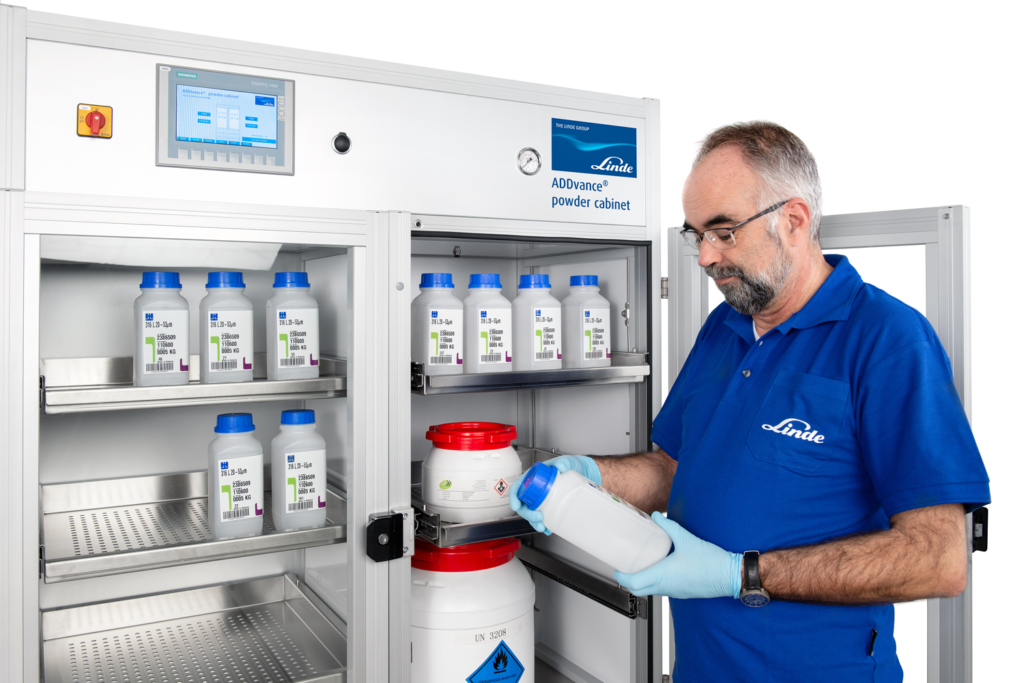
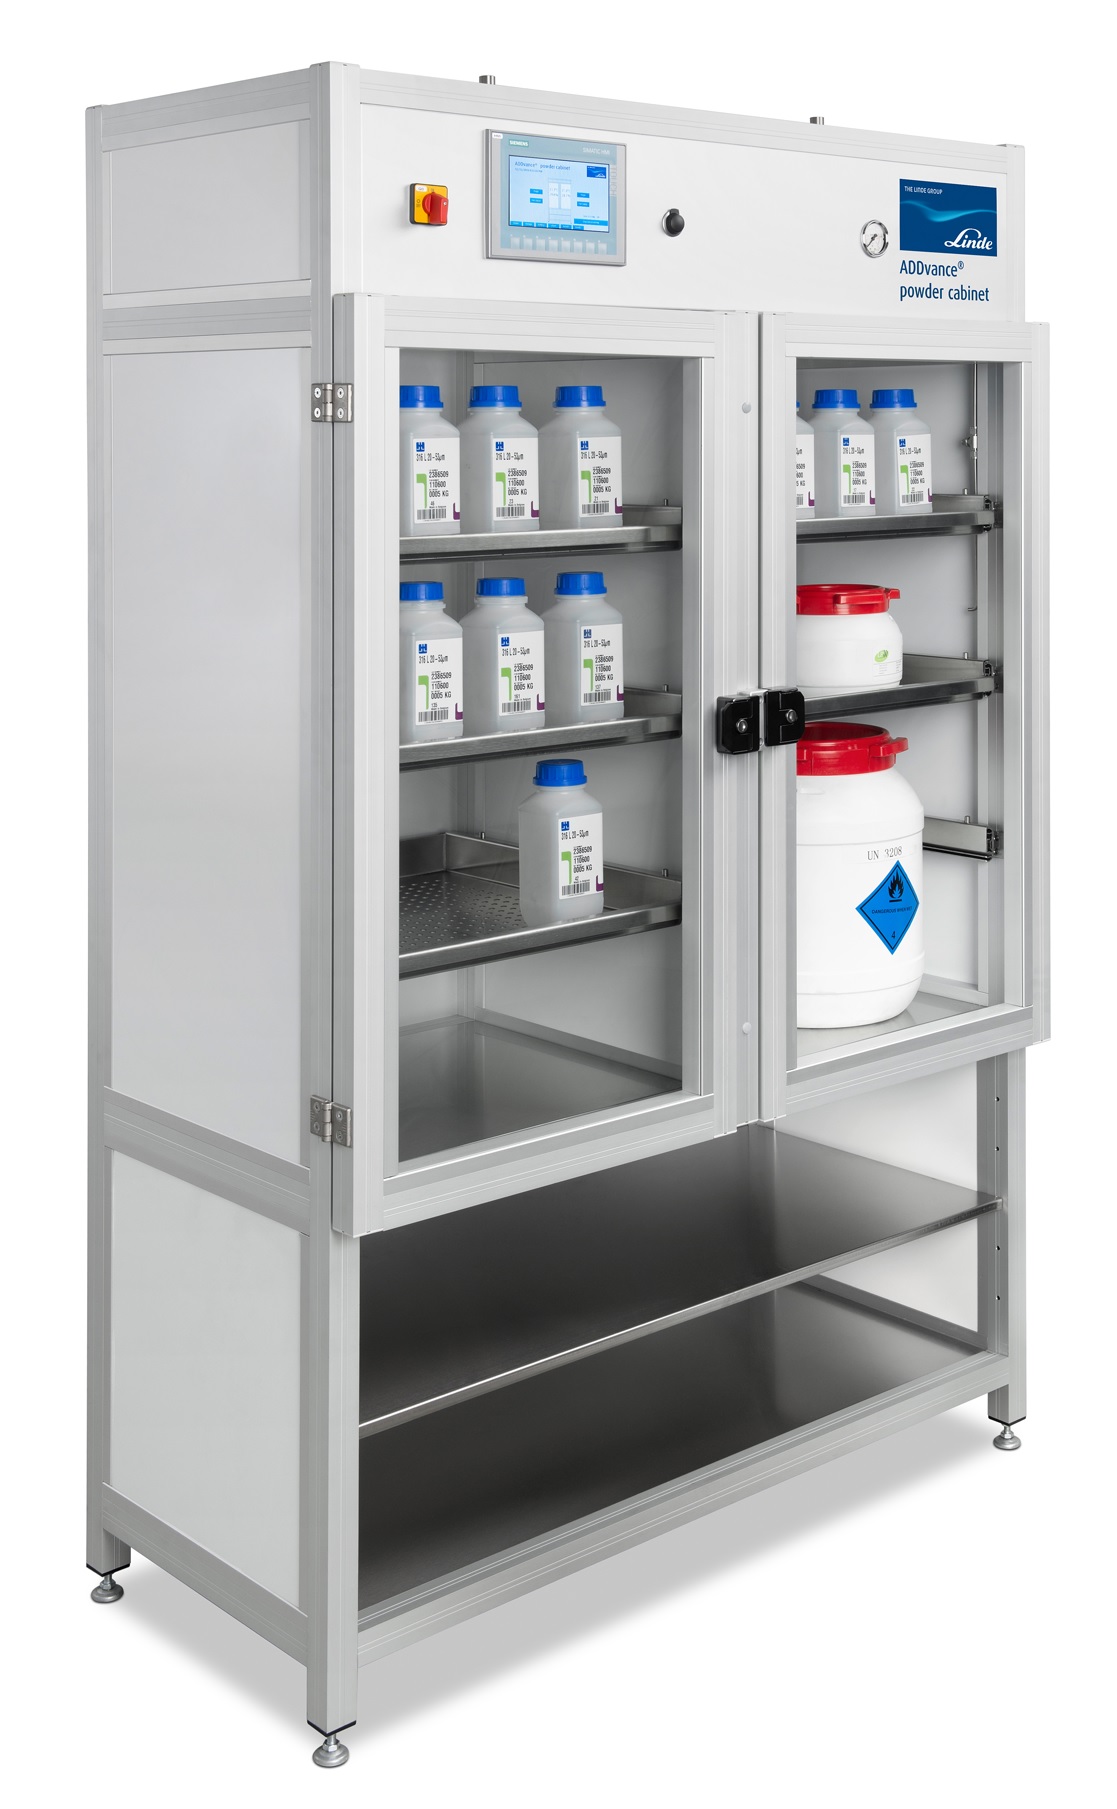
Gas suppliers also develop control equipment. Two Linde solutions mentioned in this feature serve different purposes: the ADDvance powder cabinet stores powders, while ADDvance O₂ precision monitors and controls the print-chamber atmosphere.
According to Linde, “ADDvance® O2 precision – provides continuous analysis of the gas atmosphere, detecting oxygen levels with high precision without cross-sensitivity. Recognising O2 concentrations as low as 10 parts per million (ppm), the unit automatically initiates a purging process to maintain the atmosphere as pure as needed.”
Editorial clarification: the 10 ppm figure refers to the detection capability stated for ADDvance O₂ precision. It is neither a universal setpoint for every powder nor a specification of the storage cabinet.
The cabinet, by contrast, monitors humidity and adjusts its gas supply. Linde describes a purge after the doors close, followed by a lower flow to maintain storage conditions.
The post-processing stage
Gases also feature in certain post-processing operations. Depending on the material and part requirements, heat treatment can reduce residual stresses or modify the microstructure. Not every AM process requires the same treatment.
Hot isostatic pressing (HIP) combines elevated temperature and gas pressure to densify materials. It is used for cast, sintered and additively manufactured components, as described by Quintus Technologies. High-purity argon is commonly used. Pressure and temperature depend on the selected cycle; gas purity must suit the material and application.
Under heat and pressure, plastic deformation, creep and diffusion can reduce internal porosity. Improvements in mechanical properties and fatigue resistance must be assessed for the particular part and cycle; they are not a general guarantee of service life. Applications include gas turbines, automotive engine and turbocharger components, aerospace structures, medical implants and near-net-shape parts.
For powder-based processes, depowdering is another important step. Unconsolidated particles can remain in inaccessible holes or cavities. Removal requires a method suited to the geometry and material; melting those residues is not a general cleaning recommendation. Subsequent finishing may use barrel finishing, abrasive flow machining, plasma polishing, micromachining or electrochemical polishing, depending on the surface requirements.
This dossier has first been published in the 2019 February issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.