

Feature first published in the September/October 2021 issue of 3D ADEPT Mag. Roles, research and interviews reflect that period.
Powder quality is central to metal additive manufacturing. Recovering powder after a build can reduce virgin-material demand, provided that the recovered powder remains suitable for the process and the part requirements.
This 2021 feature examines the economic and environmental reasons for doing so. Recovery, reuse and recycling are not interchangeable: collecting powder does not automatically qualify it for a new build.
We examine recovery and control methods, complementing the feature Issues raised by metal powder removal.
Why recover powder?
Whether powder can be reused depends on the material, its thermal and chemical history, contamination, the process and qualification criteria. Recycling may instead involve processing it to create new feedstock.
In a powder bed process, some powder is consolidated into parts and supports. Some remains around the parts or inside their cavities. The proportions depend on build utilisation and geometry.
Reuse can reduce virgin-powder purchases and disposal volumes. Its economic value also depends on collection, sieving, analysis, storage and qualification costs.
Environmental benefit must be assessed over the life cycle, including material losses and the resources used for recovery and reconditioning.
Andreas Hartmann, cofounder and CTO at Solukon Maschinenbau GmbH highlights each of these perspectives by laying emphasis on where powder recovery should take place:
“Firstly, taking into account the printing process itself. Only a small amount of the total amount of powder is actually fused into a component. The rest of the powder either remains in the chamber or is trapped in cavities or internal channels of the printed part – potentially reusable powder in both cases. Not recovering this powder would mean to dispose of a huge amount of powder which hasn’t been used for printing at all.
This way, powder recovery follows the fundamental idea of sustainability, i.e., the avoidance of the depletion of natural resources.
Secondly, resources are finite, this also applies to metal powder. It therefore is crucial to recover and recycle the metal powders in order to guarantee sustainability in additive manufacturing as far as possible.
The level of sustainability regarding powder recovery is heavily dependent on the industry and the application. There are industries where powder recycling is not possible (due to certifications). For these industries in particular, comprehensive concepts for proper disposal or downcycling of powder should be developed. Regarding down cycling, perhaps it is possible to use the powder for components that do not need to be certified (training components, prototypes, etc.).”
Reuse restrictions depend on the applicable specification and qualification process; they do not necessarily cover an entire industry. Powder rejected for one application must also be assessed before another use.
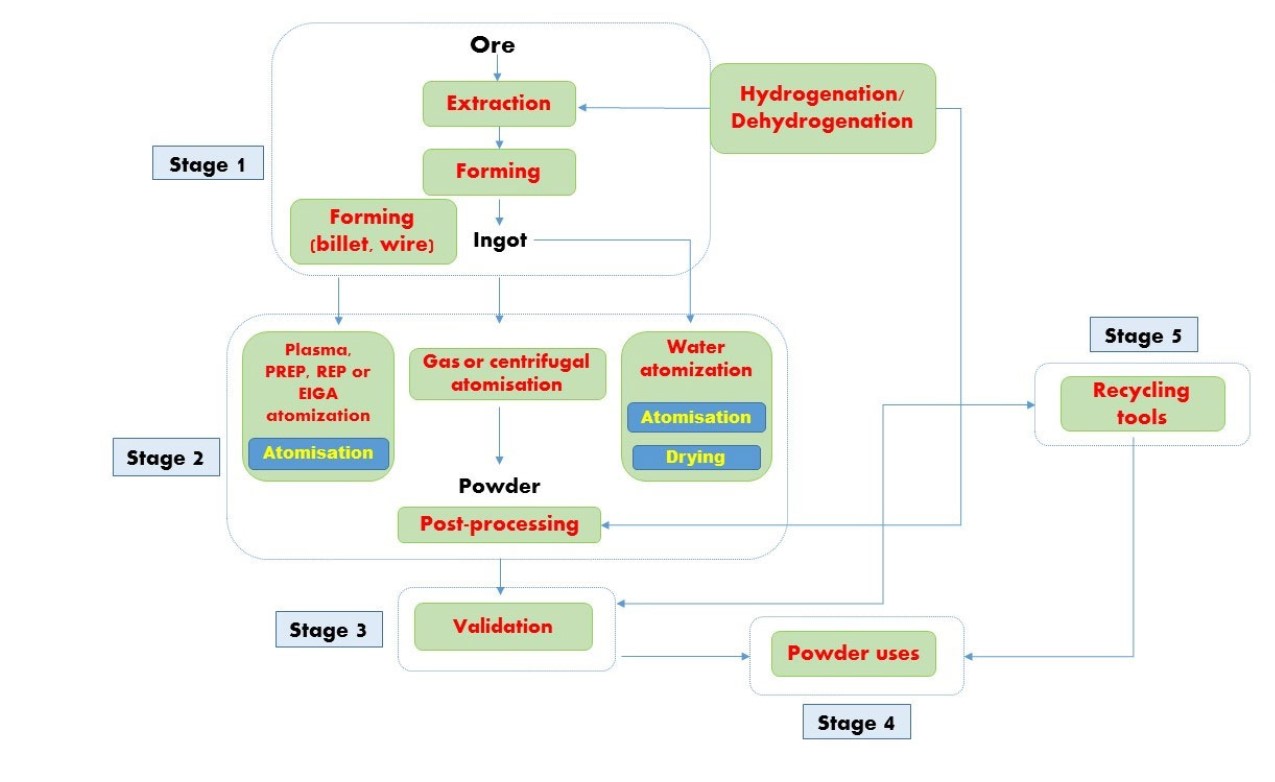
The 2019 study by Oros Daraban et al. outlines powder-production stages and ways of extending powder use. Its flow chart connects metal preparation, powder production, validation, use and recycling routes.
In other terms, this means taking into account water atomisation, gas atomisation, plasma atomisation, the plasma rotating electrode process, and centrifugal atomisation or hydride– dehydride process.
The stages to monitor differ between powder producers and parts manufacturers. For a parts manufacturer, batch control, traceability, build parameters and post-processing must remain consistent; depowdering does not replace this overall control.
How should powder be recovered and controlled?
How do we effectively recover powder? What impact can the recovery process & recovered powder have on other stages of manufacturing?
Recovery equipment and handling routes must suit the material, the part, the associated risks and the powder acceptance criteria.
First and foremost, one thing manufacturers should always keep in mind is that every material ages differently therefore their characteristics are likely to change during manufacturing, recovery and reuse. Also, it becomes pivotal to trace the evolution of powder characteristics at various stages of recycling to produce parts with consistent properties.
Hartmann describes Solukon’s approach to limiting changes and contamination during recovery:
“For trouble-free reuse the powder must inevitably be free of any contamination to minimize obstacles in subsequent printing processes. A clean environment for powder recovery therefore is mandatory. To improve the quality of the recovered powder a safety gas atmosphere is beneficial. Flowability of the powder is increased while humidity decreases – both mandatory for subsequent printing processes with reused powder.
In addition, when using reactive materials an inert atmosphere is mandatory to avoid the risk of explosions.
Another effect to be prevented is the so called “aging of powder“. Due to interaction with the surrounding atmosphere, the un-melted metal powder ages gradually which means the quality of the powder is reduced due to oxygen absorption. Correspondingly, the surface morphology and chemistry, the shape and size distribution as well as the flowability of the particles are modified. The aged powders may affect the final properties of the printed component negatively, making the number of times that metal powder can be cycled limited”.
This describes the supplier’s approach. Depowdering atmosphere and protective measures must be specified for the material and equipment. Inerting alone does not demonstrate that powder retains its characteristics or can be reused without checks.
All of these aspects provide a holistic approach to AM production, where process steps merge directly into one another. For Solukon, these steps consist in applying a secured unpacking stage, a depowdering stage as well as a post-processing stage.
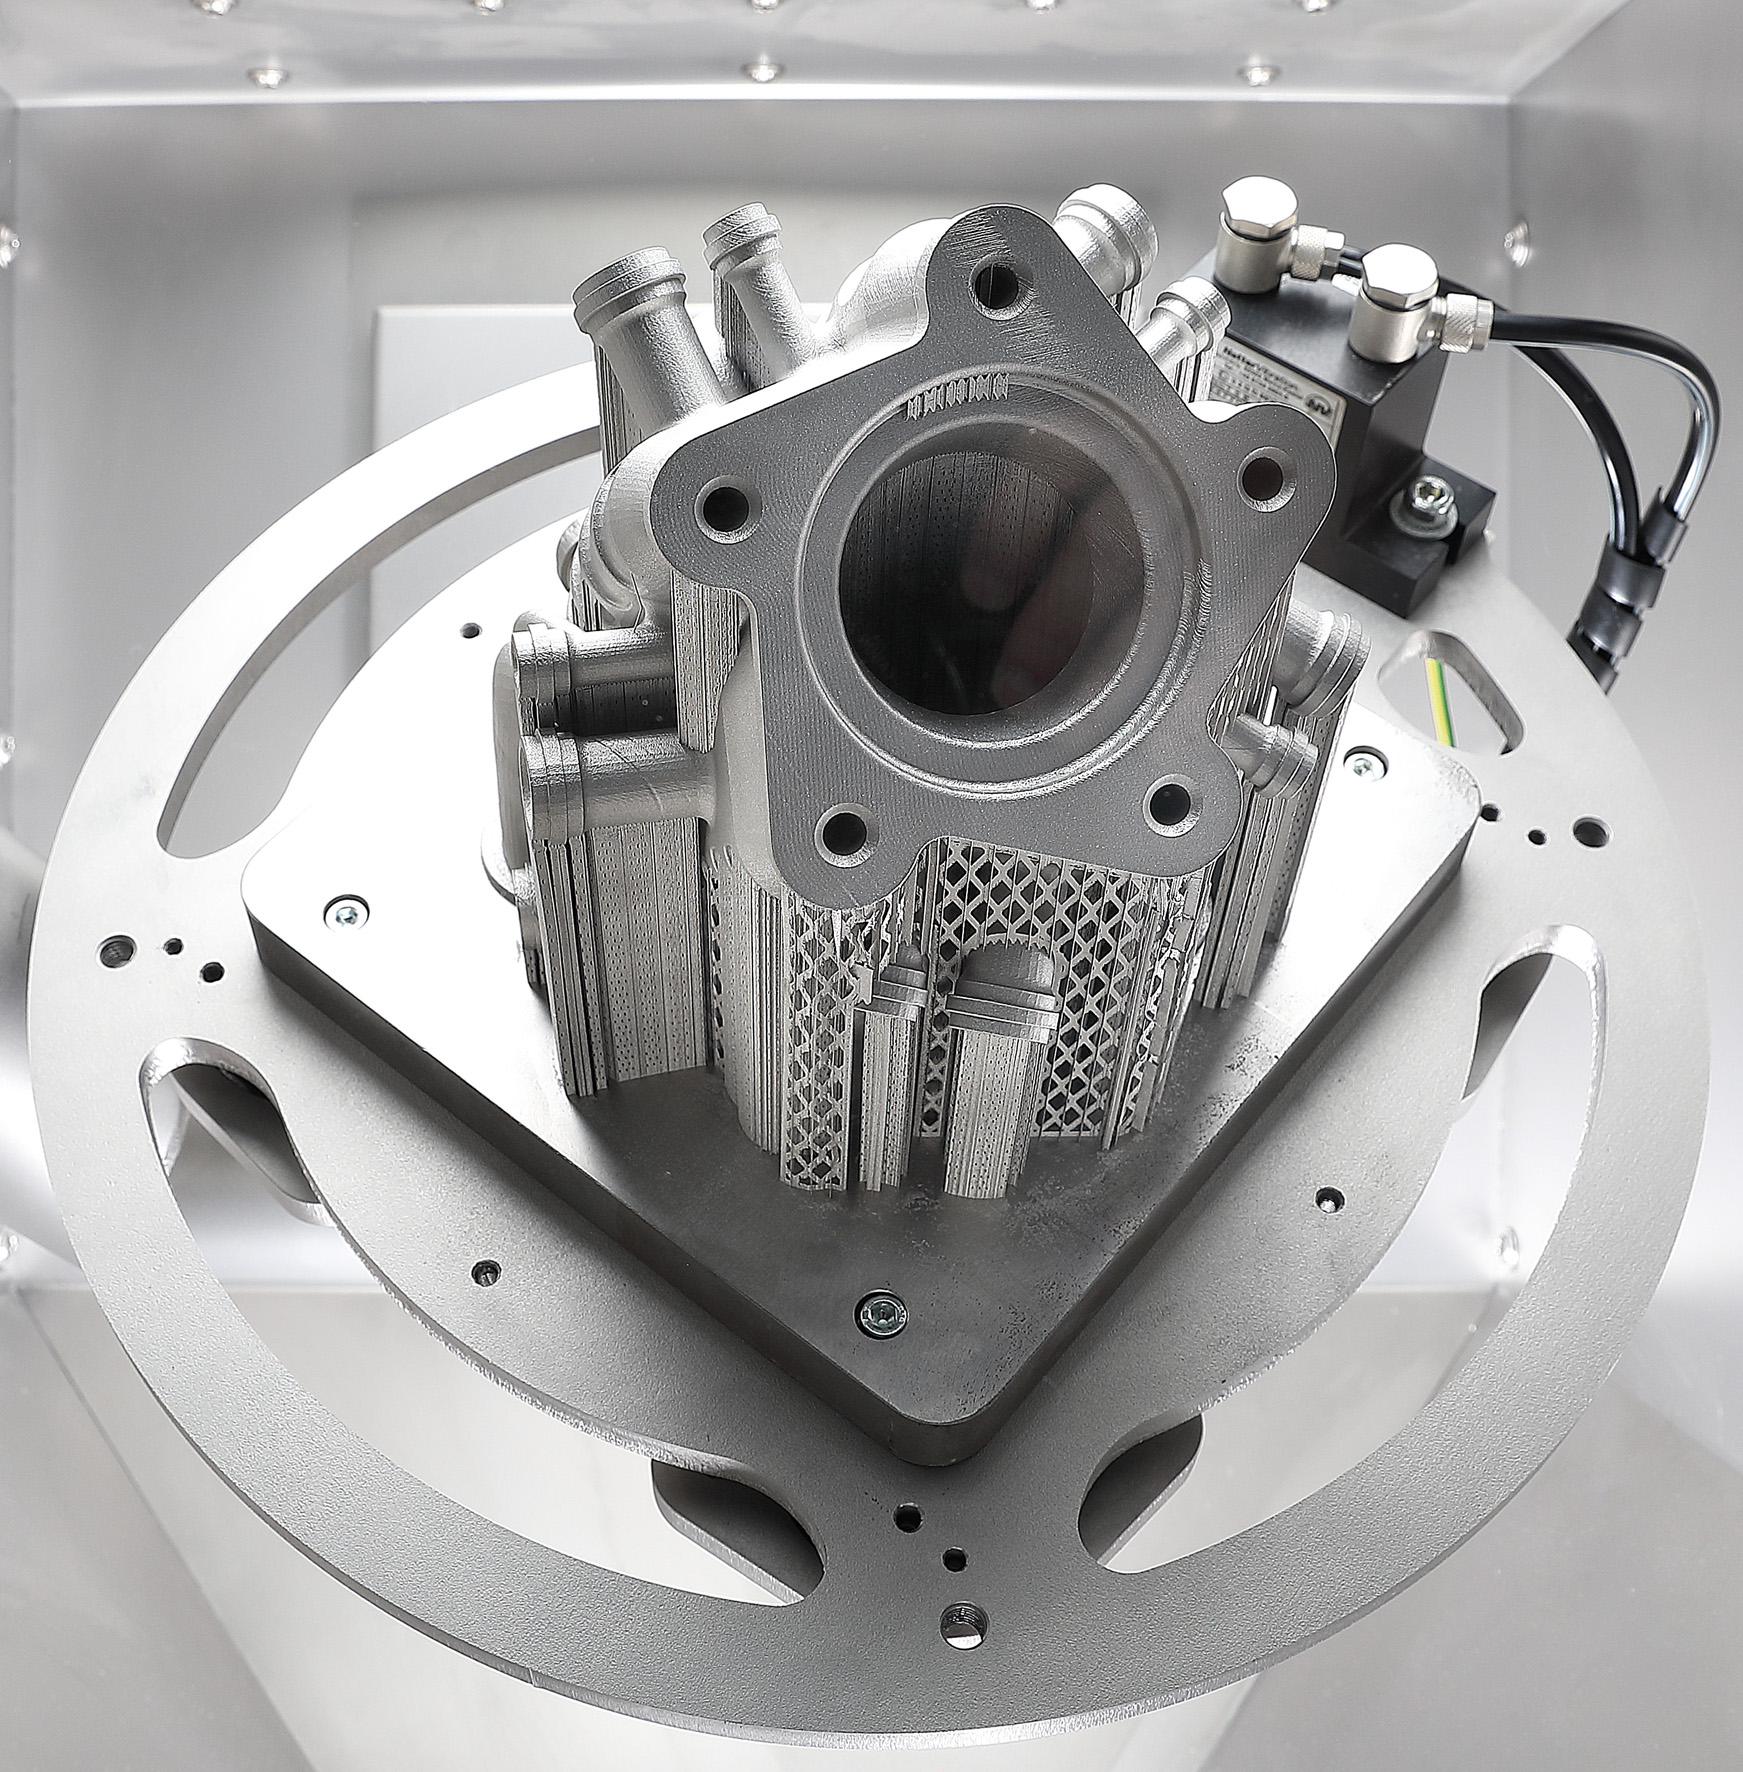
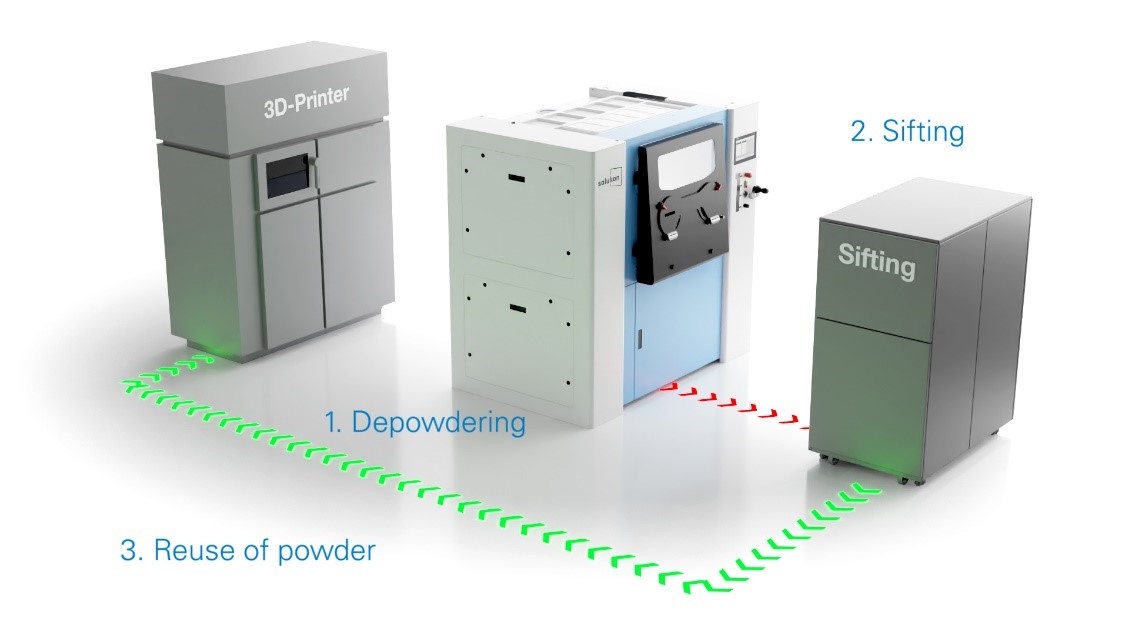
Solukon presents the following sequence for its recovery route:
“ – Depowdering: After unpacking the parts in the 3D printer, the depowdering station removes critical powder residues from the parts in a protected atmosphere and collects them contamination-free in the chamber bottom.
– Sifting: The powder residue can then be fed to the powder-recycling unit. There it is sieved and refreshed with fresh powder.
– Reuse of powder: the powder is now ready for further printing processes.”
Sieving separates certain fractions and agglomerates, but does not by itself remove oxidation or all contamination. Reuse remains subject to batch acceptance criteria. Collection equipment must suit the powder and safety requirements; an ordinary vacuum cleaner is not an appropriate default method.
Sieving and recirculation arrangements vary between machines. The Renishaw graph illustrates oxygen-content changes in an Inconel 718 batch; it does not define a universal number of reuse cycles.
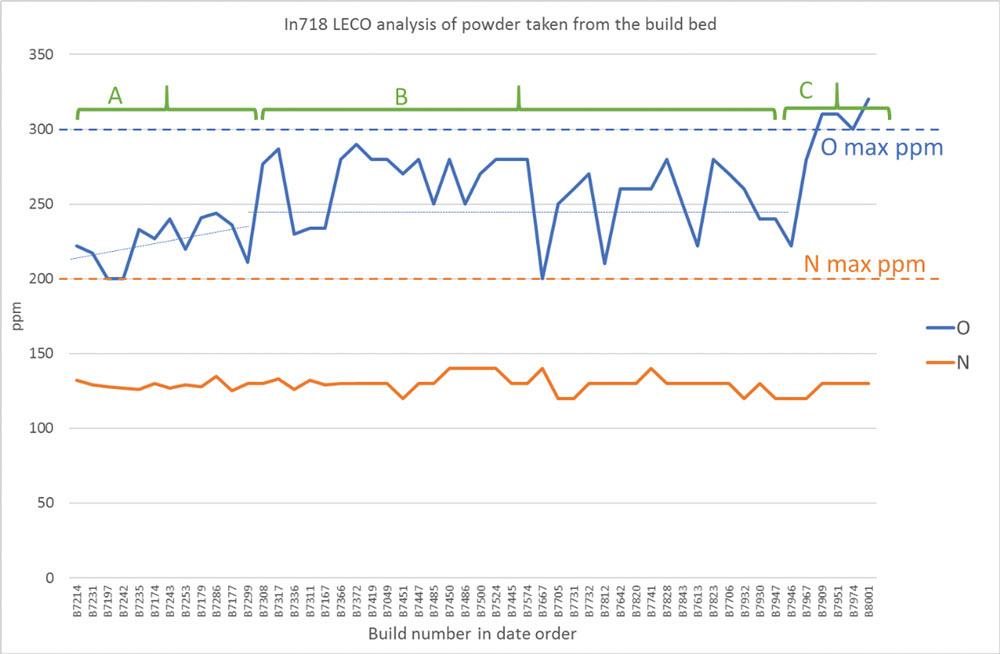
Furthermore, in order to know if reusing the unfused powder or if the recovery process is worthy for a specific project, operators should also take into account production and purchase considerations.
Distinguishing metal and polymer powder controls
Evonik raises our attention on the fact that the number of times one can reuse a powder “depends on the parts and the build job. Ideally [operators] should be able to work with a fix old/new ratio without any scrap.” The fact is, once the criteria that the parts need to meet have been defined, some operators often find if more affordable to purchase powders close to the production specifications. In this case, the number of reuse cycles will also be limited as the powder can degrade only so much before it is out of use. Not to mention that, the property requirements of the component to be printed will determine how much the operator will monitor the powder or how many times it can be reused.
As for the viability of the powder, sometimes, recovery and reuse might result in a refined particle size distribution, but with marginal change in powder morphology. Other times, “viscosity has to be measured” – as is the case with polymer powders. “Depending on the result the old/new ratio has to be adjusted”, Evonik told us.
Evonik’s remarks about viscosity refer here to polymer powders and their melt behaviour. They do not define a viscosity criterion for loose metal powder at room temperature. The used-to-virgin powder ratio must be validated for the material and process.
Measuring environmental performance
“How sustainable is powder recovery process in AM?” Reality shows that powder recovery has a proven record in terms of overall costs of production parts, and reuse of powders. Unlike ten years ago, the current AM market is filled with automated post-processing solutions that can facilitate this process. “Solukon depowdering systems for instance, usually recollect up to 100 % of the powder, contamination free and in a protected atmosphere”, the company notes. But is it enough? As Hartmann continues, it “is the door-opener for a reasonable approach to sustainability in the first place.”
The “up to 100%” figure is Solukon’s claim about powder collection under its operating conditions. It does not mean that every recovered particle is reusable or that the process has no environmental impact.
A useful assessment must define the part or function, the study boundary and its data: virgin material avoided, rejected powder, energy, gas and inspection operations. Results cannot be extrapolated to every process without this information.
In this 2021 interview, the contributors stressed the need for more representative data. “With rising serial production, the need for sustainability will grow not only for ethical recycling reasons but also with regard to costly disposal of the powder”, Hartmann said.
The approach is therefore to recover material under controlled conditions, verify its characteristics, document its use cycles and then measure the benefit. Collection yield and the ability to produce a conforming part remain distinct indicators.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.