

Interview first published in the January–February 2021 issue of 3D ADEPT MAG. Roles, products and manufacturing data reflect that period. The medical example describes a manufacturing case supplied by GF Machining Solutions, without establishing the device’s clinical status.
A look at GF Machining Solutions’ post-processing approach and medical applications
In 2021, GF Machining Solutions brought together milling, electrical discharge machining (EDM), laser texturing and additive manufacturing activities. This interview examines how they connect after a metal part is printed, within the Georg Fischer group’s structure at that time.
Although its extensive experience in machining has helped build its presence in the additive manufacturing arena, like its fellow companies, GF Machining Solutions also relied on collaborations with other AM companies, the most prominent collaboration being the one with 3D Systems. In this continuous quest to address the unique needs of companies that are battling to adopt AM in production environment, the advanced manufacturing unit is continuously making adjustments and improvements on hardware and software environments; improvements in a nutshell that will simplify the path to a seamless and efficient production workflow.
These adjustments also require a focus on “automation products which are tooling and robotics – as well as digital transformation which is quite transversal to all technologies”, Romain Dubreuil, Head of Additive Technologies told 3D ADEPT Media in an interview.
Furthermore, although the company usually talks about it as part of its “integrated manufacturing solutions” and rarely as an individual solution, our conversation with Dubreuil sheds light on specific hardware that has been developed for the much-required post-processing stage.
Separating parts and preparing for finishing
“This stage of the manufacturing process can either be done by ‘depowdering’ or finishing of AM parts by machining operations.
As far as finishing is concerned, we can complement the printing of the part with one of the conventional manufacturing machines in our portfolio. This can be a standard milling machine or a standard wire EDM machine. In many cases, they can fit well as many operators after the printing stage, machine the part to improve the finishing in a certain area for instance”, Dubreuil outlines.
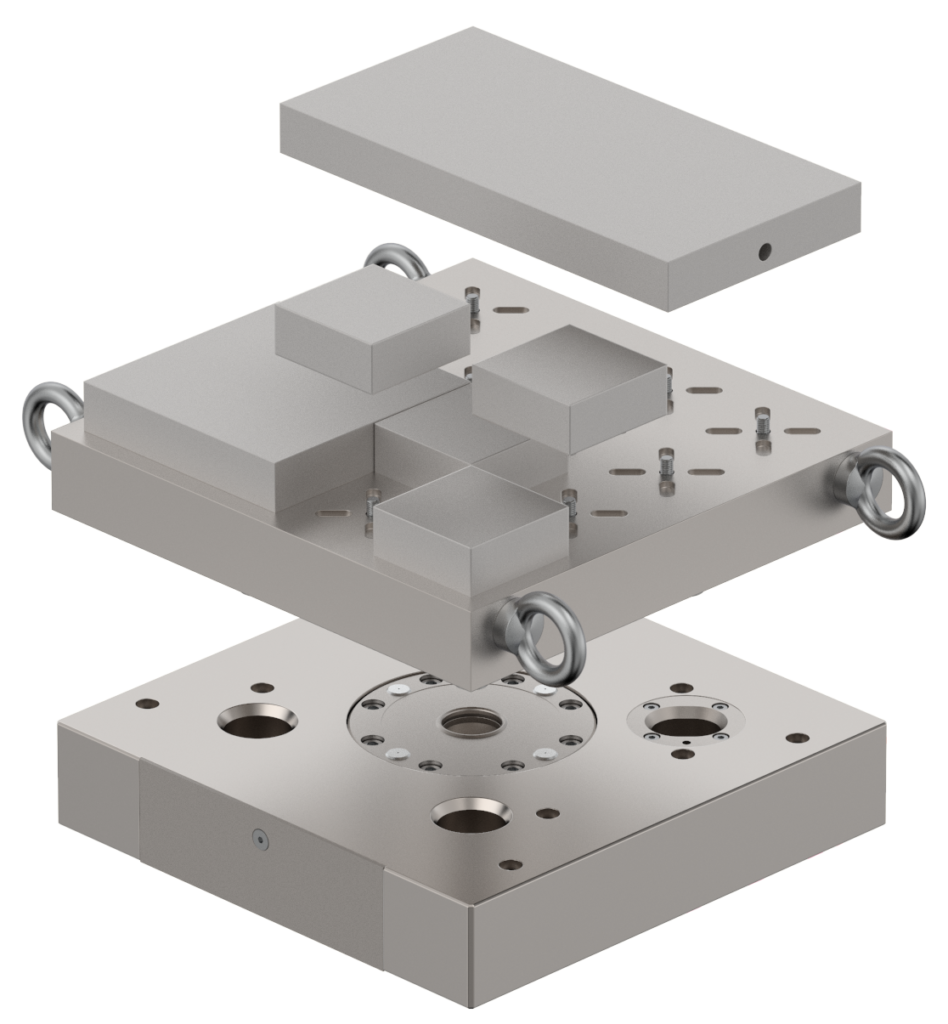
As we will discover later on, in the lines below, AM offers so much possibilities for complex implants and biomedical products that 3D printed parts sometimes need further machining and finishing. At this level, workpiece fixturing devices for clamping are often used to process the part and to facilitate subsequent processes.
“We have also developed a specific solution that can cover the needs of AM in this regard”, Dubreuil points out.
The CUT AM 500 separates metal parts from their build plate using horizontal wire EDM. It is an alternative to sawing, not a band saw: electrical discharges remove the material. Discussed in 3D Systems’ Formnext 2019 announcement, the solution targets workflows including laser powder bed fusion (LPBF).
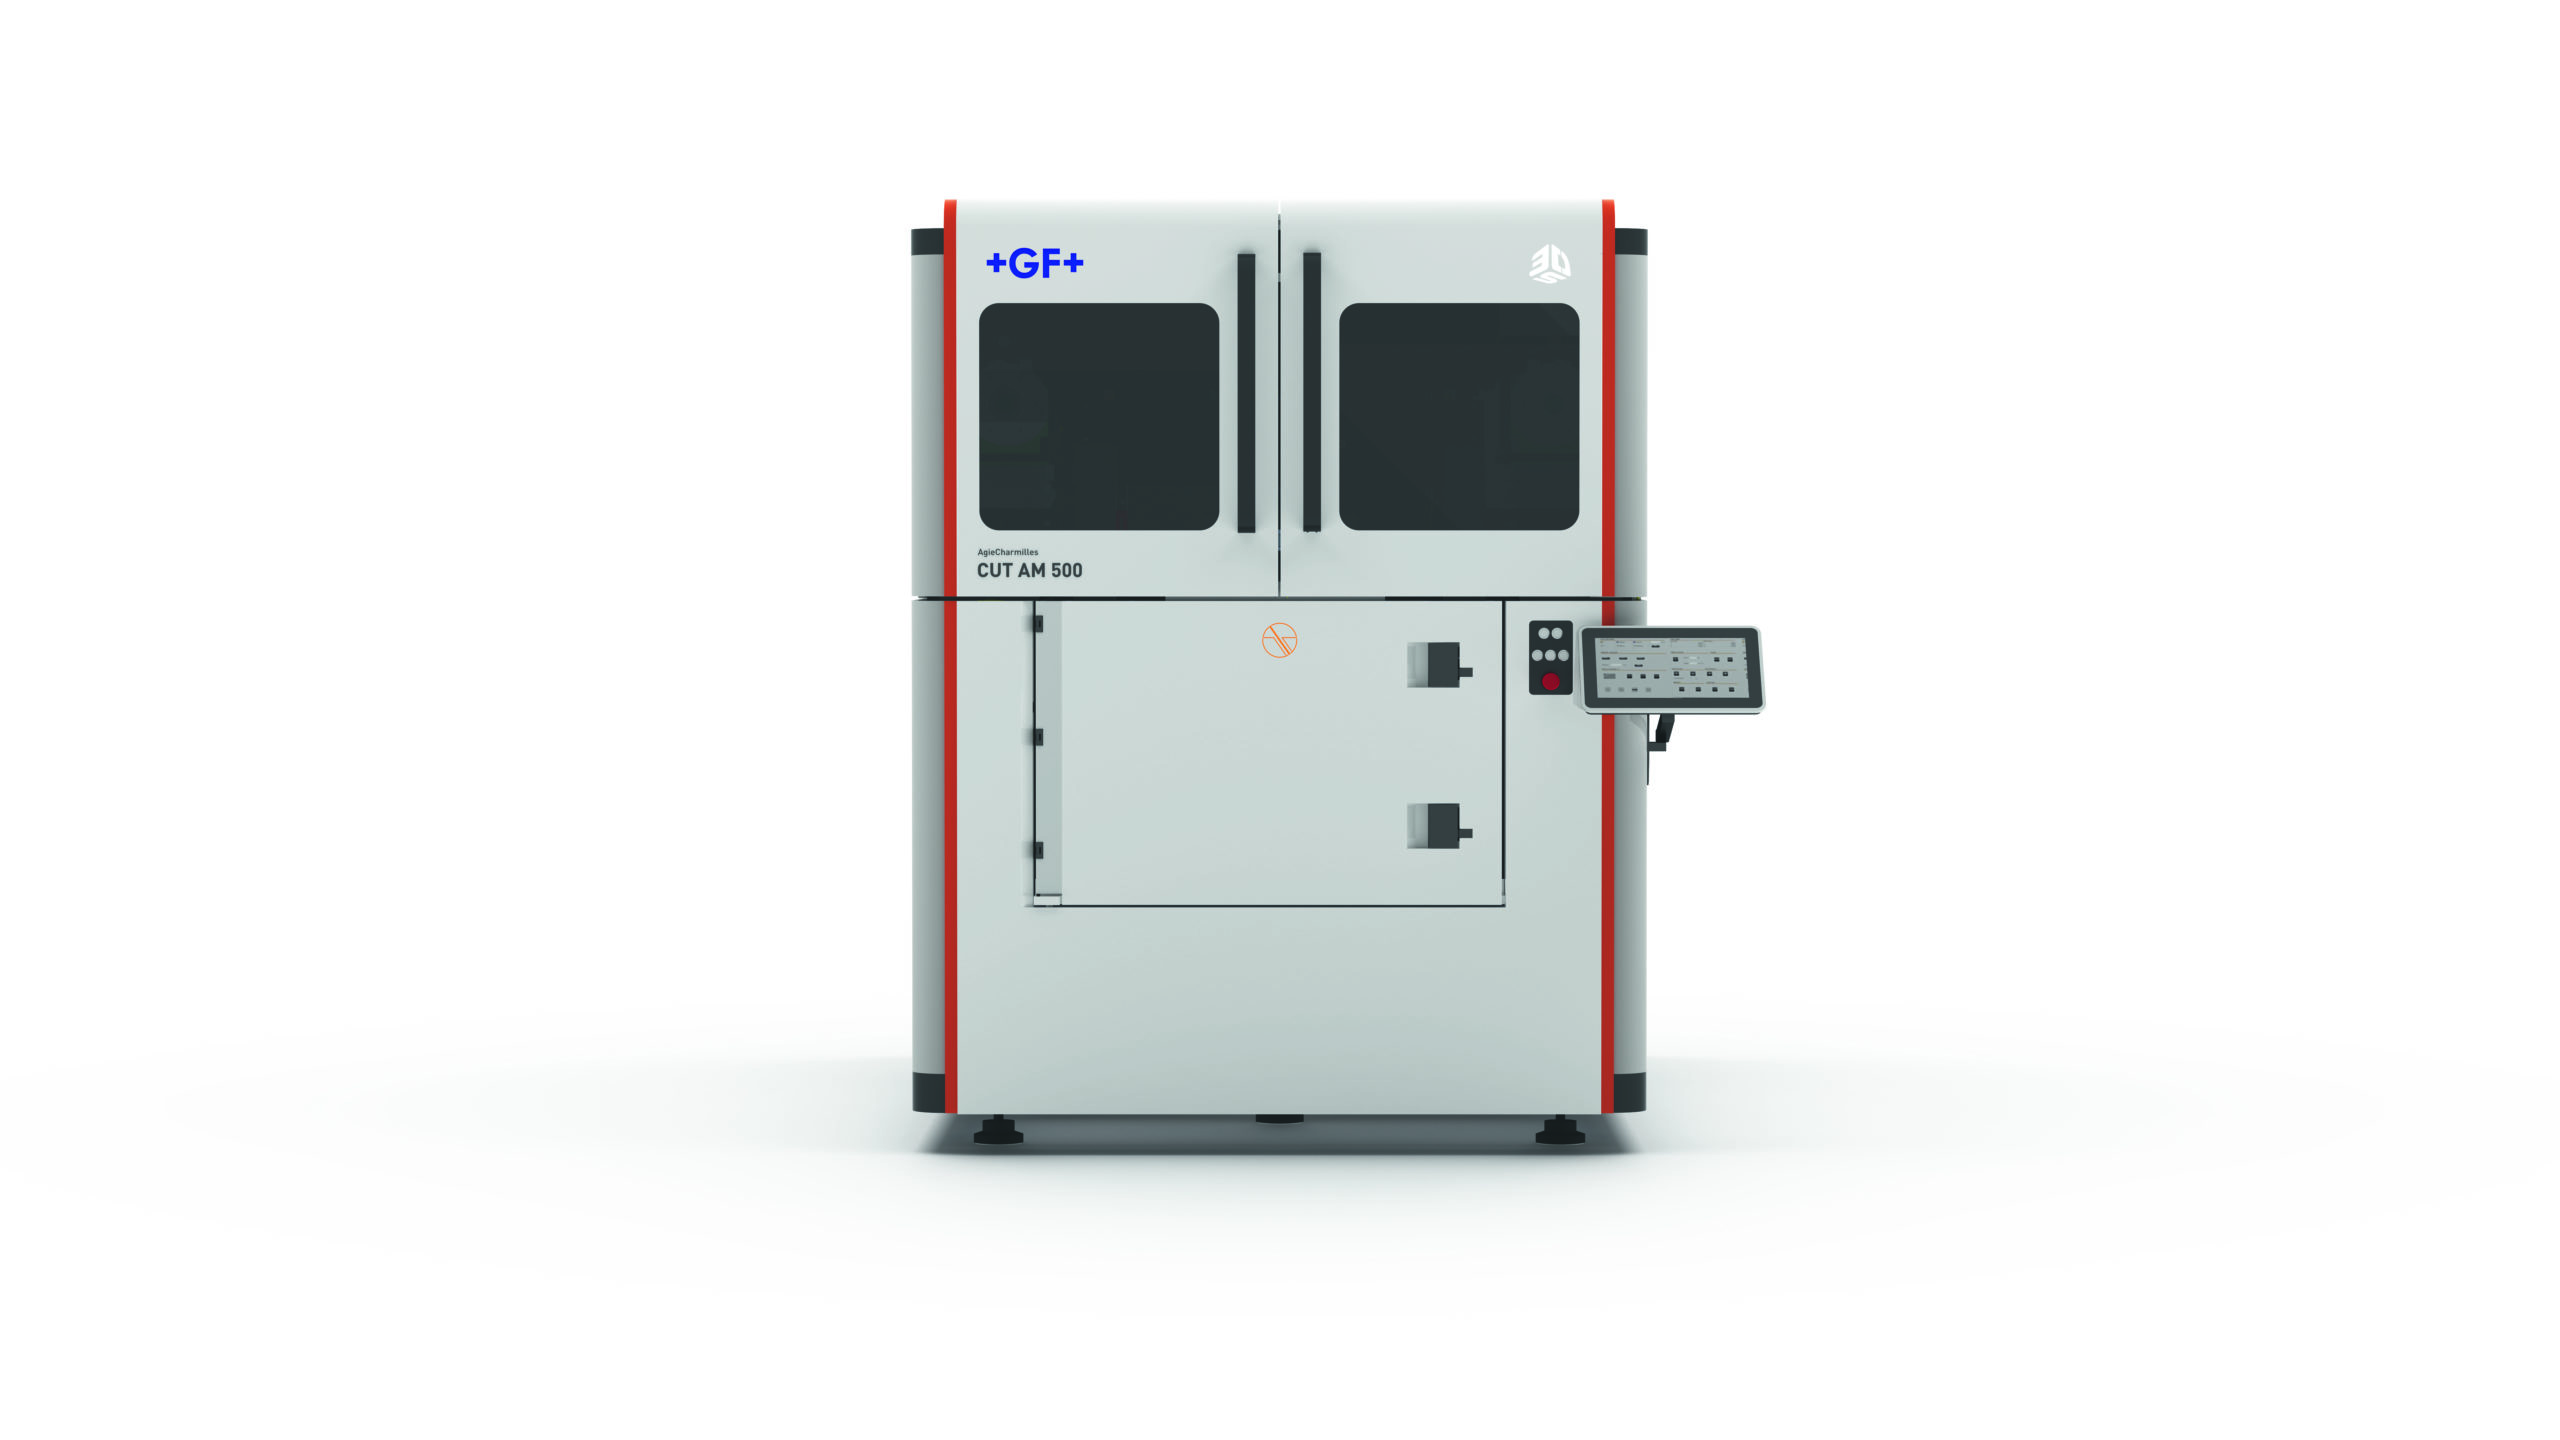
“Although it has been developed with LPBF in mind, it does not necessarily mean that our portfolio cannot be used for other manufacturing technologies such as Electron Beam Melting or simply metal applications in general”, the Head of Additive Technologies notes.
Data supplied for this interview specify a 510 × 510 × 510 mm plate-and-parts envelope and a maximum load of 500 kg. These describe the workpiece capacity, not the machine’s external dimensions. GF highlights the horizontal wire, tilting table and receiving baskets to support parts during separation. Workholding and handling integration depend on the configuration.
Manufacturing choices
Taking a product from idea to design and 3D printing requires both experience and the appropriate technologies. Although we only focus on post-processing here, let us remind that the ideal AM process includes the entire ecosystem, from quality control processes for incoming powder to software, post-processing, and process controls on finished products. We can never stress this enough but each of these items is crucial to a successful production in highly regulated sectors.
“In general, we focus more on production applications. We are very active in different segments: mould and die, energy and aerospace, industries in a nutshell, where AM can bring benefits to increase performance and weight, and improve parts accuracy. That being said, we also keep a strong focus on the medical industry. One of the major applications in this field remains spinal implants that require technologies that meet the requirements of AM”, Dubreuil states.
A quick look at the manufacturing of a dental implant.
As applications remain a good proof-of-concept of the way technology works, the Head of Additive Technologies and his colleague Dogan Basic share with us a few details on the production of a dental implant as well as several post-processing tasks that can be achieved before getting the desired finished part.
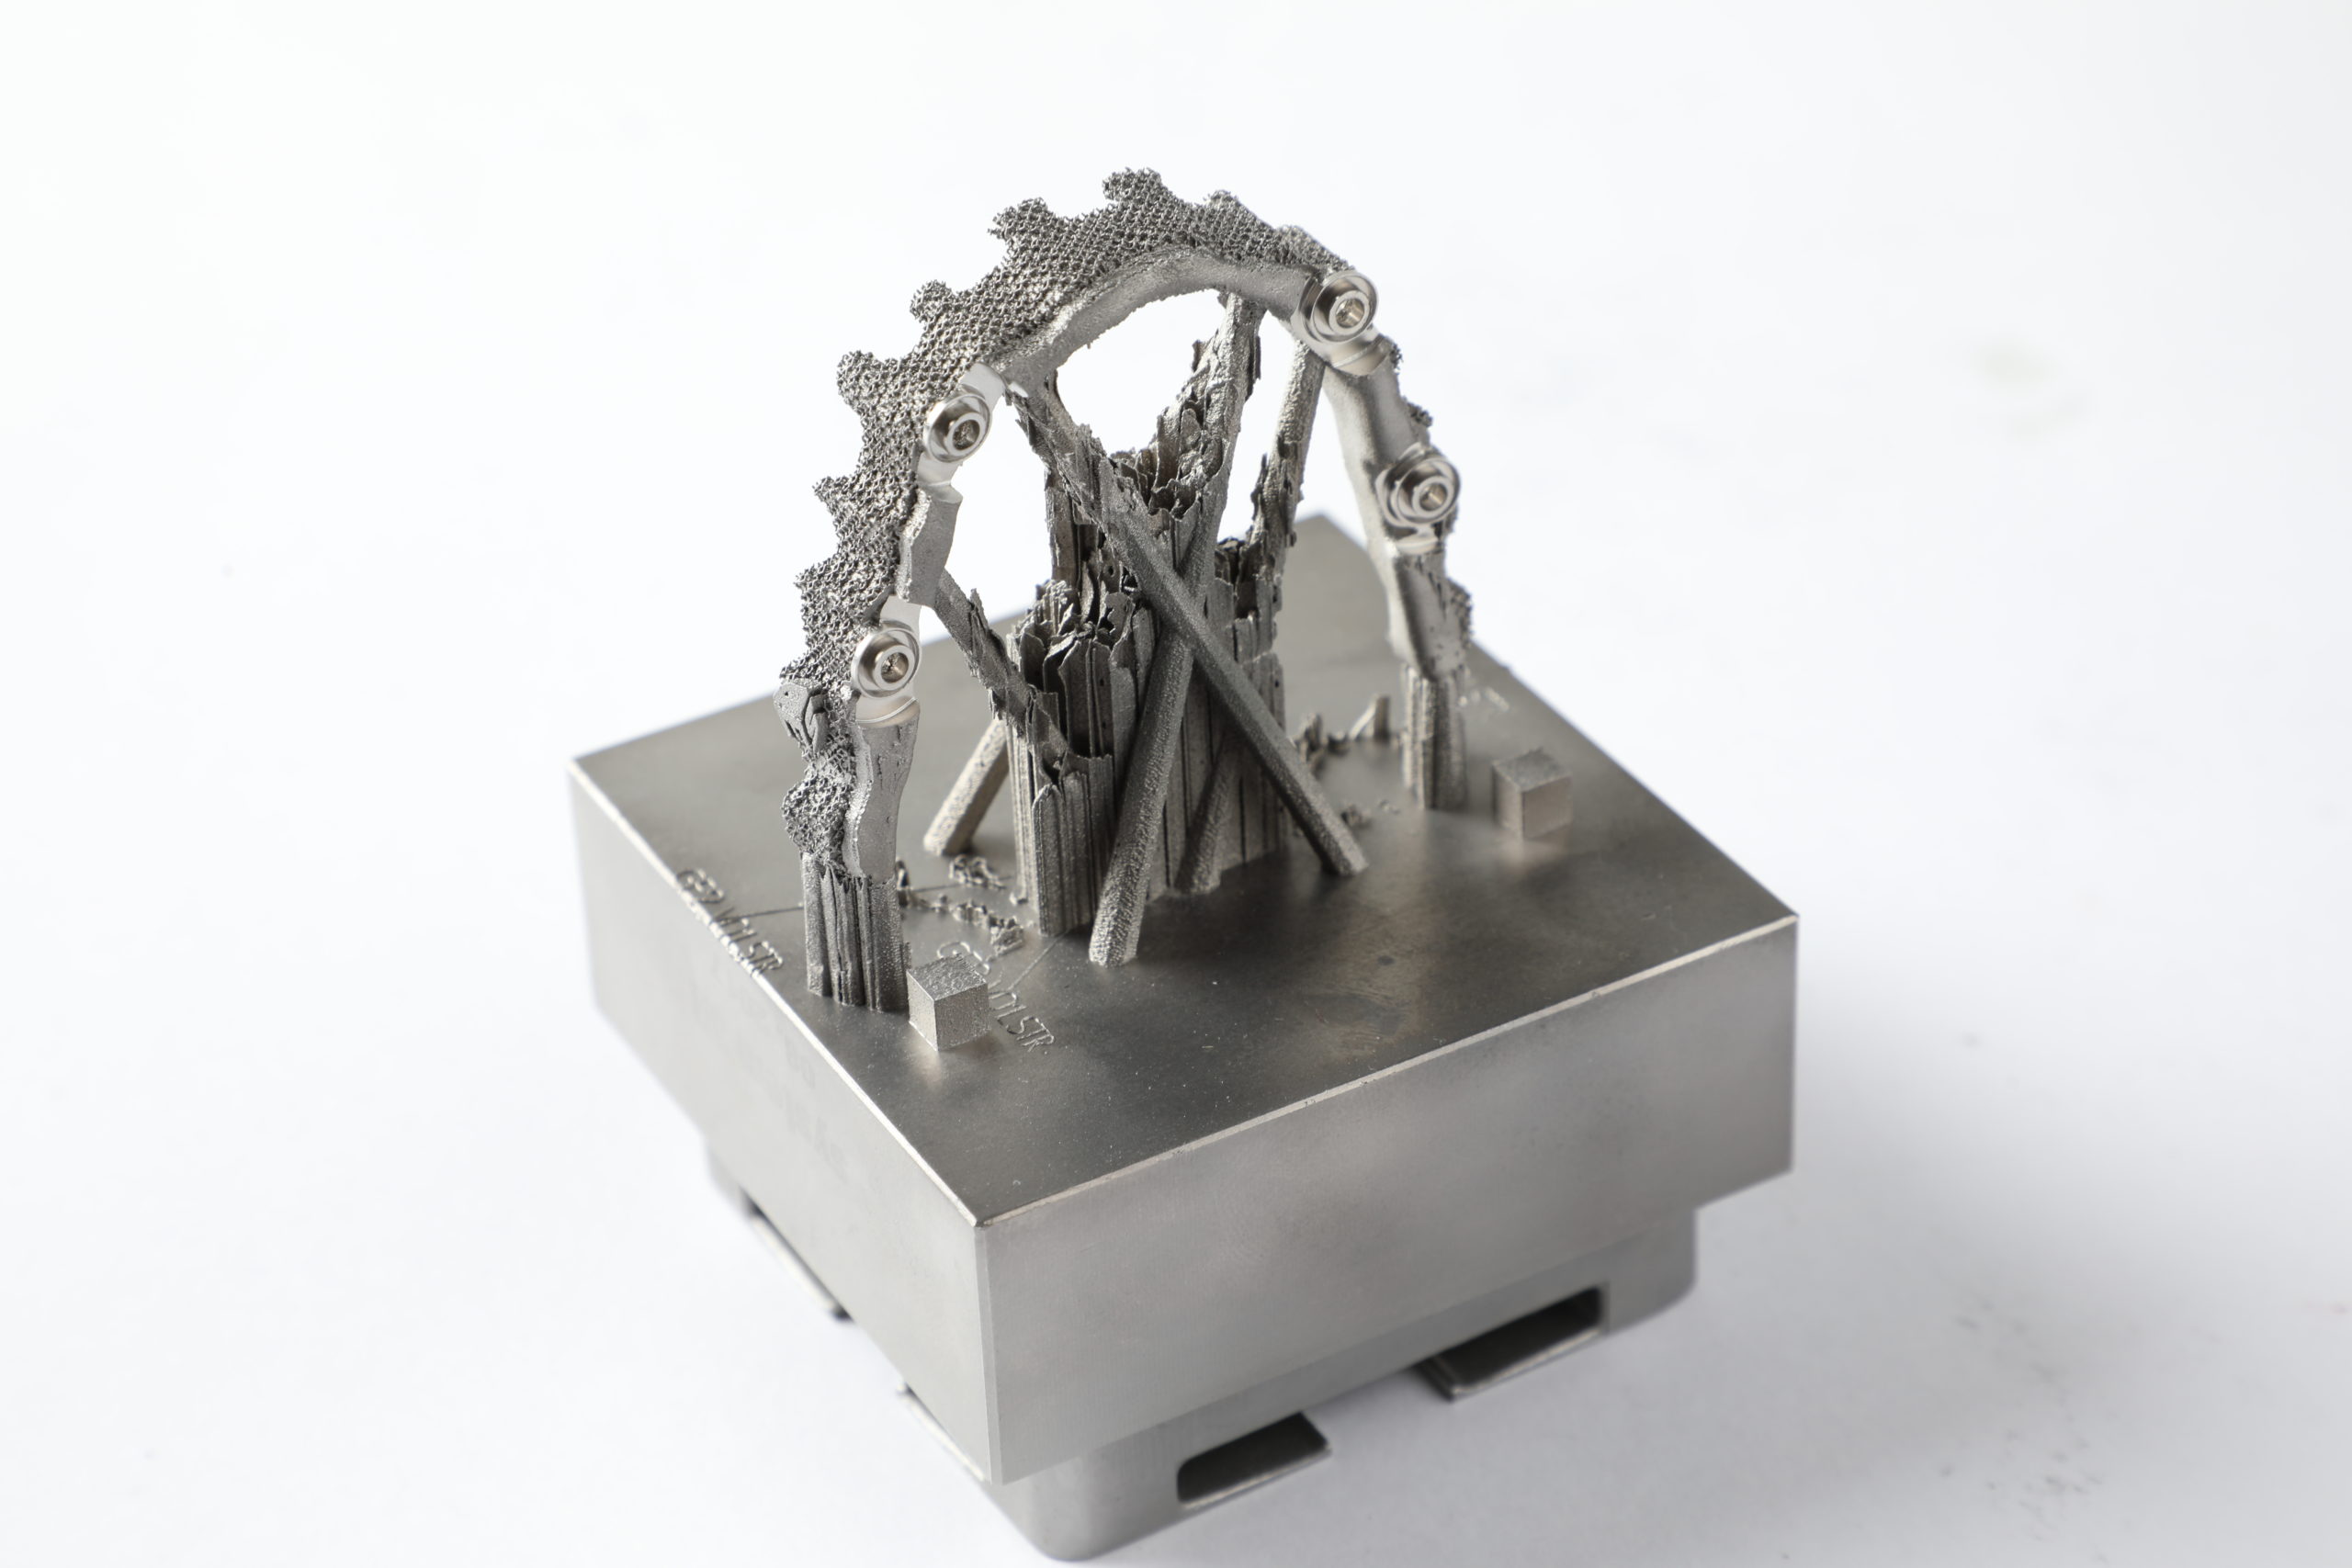
The example’s status—research or a marketed device—was not specified. According to GF, the part was printed on a DMP Flex 350 in LaserForm CoCrF7 with 30 µm layers. Atmosphere control and the target density concern the manufacturing process; they do not establish clinical suitability. The machine also featured in our EMO Hannover 2019 report.
However, what raises the most our interest, is both the accuracy in terms of manufacturing time and post-processing operations.
“It will take 34 min to print one part but obviously, you will print multiple parts at the same time. (9 hours to print 20 parts). We print them on our small System 3R plates in order to facilitate the post-processing operations. It will take around 23 min to mill each part and just a couple of minutes to separate them with the CUT AM 500”, Dogan Basic from GF Machining explains.
These are GF’s estimates for this case and its batches, not universal production rates. The stated 34 minutes for one part and nine hours for twenty parts refer to different configurations and should not be extrapolated by simple multiplication. They are not a complete lead time covering every operation and inspection.
System 3R tooling references and transfers workpieces between operations. Its documentation distinguishes the BuildPal printing base from the AMCarrier that carries it. Separating the part from the BuildPal can use wire EDM or sawing; this is distinct from releasing the pallets. The bases are then prepared for reuse.
In this specific case, Dogan explains that before the milling operation, the part traditionally goes through heat treatment operation and thereafter, through a 5-axis milling operation to ensure that the “connections” are milled for the screws.
Thereafter, “you will have potentially hand finishing to remove potential residual supports and a cleaning operation.”
Manufacturing and finishing this example do not, by themselves, establish that it can be implanted in a patient. Device-specific checks and validation remain necessary, including performance, residues, cleaning and sterilisation. The FDA’s 2017 technical guidance details these considerations for additively manufactured medical devices.
Concluding Thoughts
This case illustrates why post-processing should be planned as part of the workflow: workholding, separation, treatments, machining and inspection need to work together. Benefits depend on the component, volumes and requirements; purchasing a machine alone does not guarantee them.
This feature has first been posted in the 2021 January/February issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.