

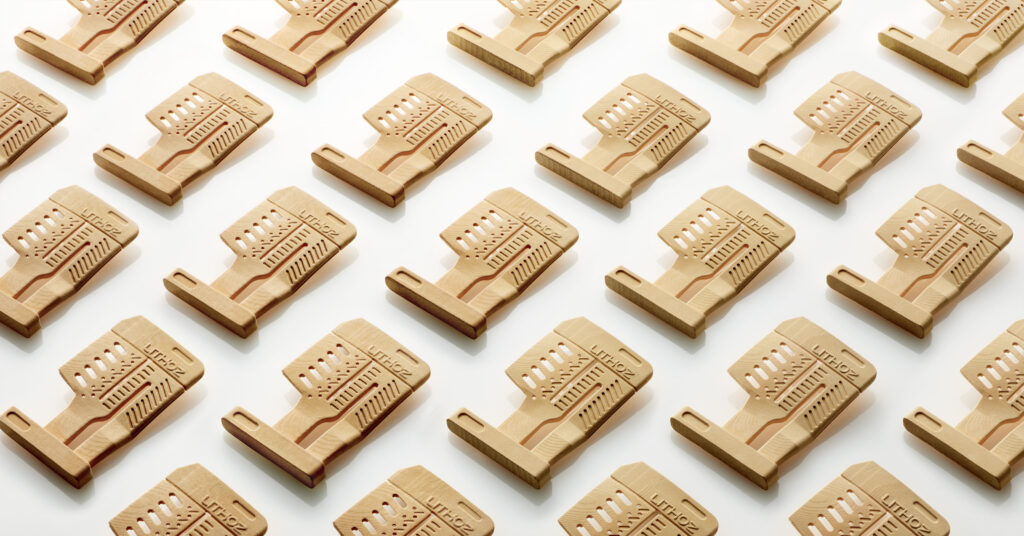
Feature first published in the March/April 2022 issue of 3D ADEPT Mag. Interviews, roles, commercial offerings and outlook statements reflect 2022; the infographic depicts the June 2022 landscape.
Beyond vases and homeware, ceramic 3D printing opens opportunities for industrial applications. In 2022 it was still a newer segment than polymer or metal AM. In a forecast published in September 2021, IDTechEx projected seven-fold market growth by 2032. This was a forecast, not growth already achieved.
Pressing, extrusion and injection moulding are ceramic manufacturing routes, each with application-specific tooling costs and constraints. Hot isostatic pressing can contribute to densification. AM can reduce some tooling needs or enable complex geometries, but its value for small and medium batches depends on the whole chain, including thermal processing and inspection.
The exclusive feature below ambitions to understand and identify:
- The technological landscape in which ceramic 3D printing fits;
- What didn’t work before, and what works today in terms of material & manufacturing solutions?
- The established business model in the ceramic 3D printing market and applications where there is a real potential.
The technological landscape of ceramic 3D printing
Ceramics are inorganic, non-metallic materials. Many are shaped and then thermally processed; preparation, densification and resulting properties depend on composition.
A common distinction is between traditional ceramics, often clay-based, and technical ceramics developed for specific functions. The latter are described here as “materials used for engineering purposes instead of tableware”. Their properties vary with composition and processing; high hardness does not imply high fracture toughness.
From the very beginning, whether it was meant for art or industrial purpose, the use of ceramic 3D printing has been defined by materials. And these materials have somehow defined the different technologies that can enable ceramic 3D printing applications for industry or art products.
Approaches include vat photopolymerisation, material extrusion, binder jetting, material jetting and laser processes using powders or slurries. SLA and DLP are photopolymerisation approaches; robocasting or direct ink writing (DIW) deposits paste. Final density depends on process, material and post-processing.
Extrusion can process clay-based pastes as well as technical-ceramic formulations supplied as paste, filament or pellets. Technical materials include alumina (Al₂O₃), zirconia or zirconium oxide (ZrO₂), silicon nitride (Si₃N₄) and silicon carbide (SiC). Zirconia and zirconium oxide refer here to the same material, not separate families.
Overview of ceramic AM processes
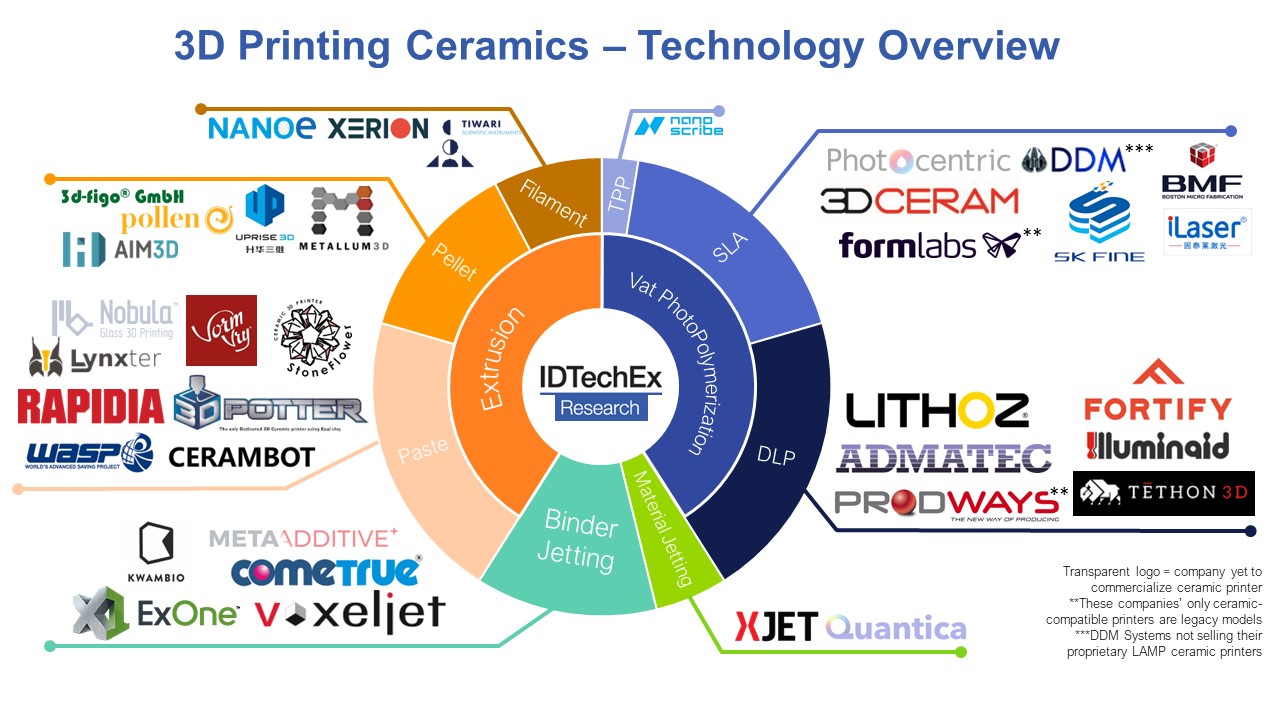
Extrusion deposits process-compatible paste, filament or pellet-based feedstock layer by layer. In the 2022 landscape, WASP offered ceramic-paste systems and Pollen AM worked with pellet extrusion, including technical ceramics.
KU Leuven research on laser processing of ceramics distinguishes direct and indirect routes. A direct route applies laser energy to the ceramic; an indirect route consolidates a binder phase. The resulting green part in the latter route subsequently needs debinding and furnace sintering. These approaches do not all have the same maturity.
In vat photopolymerisation, a suspension of ceramic particles in a photosensitive binder is selectively cured. The green part subsequently needs debinding and sintering. Lithoz’s LCM technology belongs to this family.
“Our range of 3D printers are based on LCM technology, building individually-cured layers of ceramic slurry in a bottom-up manner to create high-performance complex parts without the need of a mold or other tools. Using this technique, it is possible to build far more intricate and fine features with outstanding levels of precision and accuracy unachievable using other production techniques. Our ceramic materials also offer significant advantages over other materials, such as high heat and chemical resistance and biresorbable qualities for medical applications”, Zoran Ostic, business & application expert at Lithoz states.
The properties cited by Lithoz depend on formulation and application. Not every ceramic is bioresorbable, and accuracy must be verified for the relevant geometry and manufacturing chain.
Binder jetting selectively deposits binder onto a powder bed. Powder packing, binder dosage and green strength must be balanced. In 2022, ExOne, then part of Desktop Metal, and voxeljet were among binder-jetting suppliers. Parts per build depend on size, arrangement and available volume; green-part handling and surface condition remain control points.
XJet’s NanoParticle Jetting (NPJ) deposits droplets containing ceramic particles alongside a separate support material. The manufacturer describes heat-driven evaporation during deposition, not UV curing. Supports are subsequently dissolved before the parts are sintered.
Many indirect routes require binder removal followed by sintering. The sequence depends on formulation and system: no separate debinding step in a given workflow does not mean that every organic constituent or thermal treatment is absent.
The materials standpoint
“Ceramics are hard – and not just mechanically speaking! Compared with metals and polymers, ceramic materials are incredibly difficult to shape through subtractive forming methods like machining, thanks to their inherent mechanical hardness and brittleness. This is why 3D printing of ceramics is very enticing to the industry at large”,Bram Neirinck and Kevin Eckes, Research Engineers at Aerosint observed.
Challenges can include sintering shrinkage and distortion, porosity, cracks or interlayer bonding. Where glazing is required, compatibility is an additional issue. These defects are not inherent in every part; prevention depends on material and processing conditions.
For Trent Allen, Tethon3D’s CEO at the time of this interview, these issues call for work on both formulations and processing.
“In traditional aqueous material science, you are more limited in the materials you can process. Also, there is immense opportunity in taking materials that are difficult to process in traditional manufacturing like SiC(Wet Layup) and being able to use a non-aqueous binder to make producing parts much easier. For us at Tethon, nearly 1/3 of our business is taking powders used in traditional manufacturing at Fortune 500 companies and turning them into 3D printing resins, or powders for binder jetting. We fully expect this business to grow as additive grows in parallel”, Allen explains.
Allen compares continual material improvement with software development, particularly when explaining formulation changes to customers and moving from laboratory to production batches: “anyone that has built software knows a product is never truly finished. Technology improvements within polymer material science and finding ways to improve powder processing is accelerating. With over 1,300 customers who trust our materials it can be challenging for us to make sure our global customer base knows why a material was altered, upgraded, or killed-off. Another challenge when innovating so quickly is you need to figure out how to scale from lab batches to production batches.”
Today, taking examples on UV printing & Binder Jetting which are the main processes the company has developed expertise in, Allen explains that to truly move into production and create great parts, it’s essential to have consistent materials and limit the amount of shrinkage.
“Binder Jetting & UV printing complement each other. For us we generally print more precise, smaller, denser objects using UV and larger, blockier objects with thicker walls using Binder Jetting”, he adds.
Production requires repeatable final properties, a controlled process and suitable working conditions. Formulation, parameters and treatments must be validated at the intended scale; a successful laboratory batch is not sufficient.
The established business model in the ceramic 3D printing market and applications where there is a real potential
It always starts with R&D and eventually prototypes. In addition to these two usages, first applications in ceramic 3D printing reveal an interest for ceramic tooling and small-batch parts across industries such as investment casting for aerospace & defense, chemical engineering, and dentistry.
Decorative-ceramic services and technical-ceramic production meet different needs. The withdrawal of a consumer service does not establish an absence of industrial service providers. Lithoz emphasises supporting its customers and developing applications with them.
“Many of our customers service the industry by providing their specific know-how of our Lithography-based Ceramic Manufacturing (LCM) technology to players of various industries, from medical and dental to aerospace and semiconductors”, Peter Schneider, Business and Application development expert at Lithoz states. “Ceramic 3D printing, while very well suited to modern manufacturing and development in every field, is however still currently seen as a ‘new’ technology, much more than metal or polymer AM, and therefore companies need incentive to switch over from conventional methods. Service bureaus have by far the highest requirements for a manufacturing technology, meaning that they only offer processes with the best ROI at the lowest technical risk – there is little room for trying new technologies. In the same way, these bureaus do not have the time or resources to waste on a technology they do not already know for certain will deliver”, he continues.
Moving forward, Schneider believes it’s only a matter of time for service providers to implement industrial ceramic 3D printing into their workflow. For the expert, one incentive that will drive this change is the combination of DfAM with the desirable material properties of ceramic materials – such as high chemical resistance, high strength and hardness – Such combination can open the door to applications that were previously unachievable and break into markets where metals and polymers have already reached their limits.
This incentive refocuses the debate on applications and the ones that are not yet fully explored by technical ceramics.
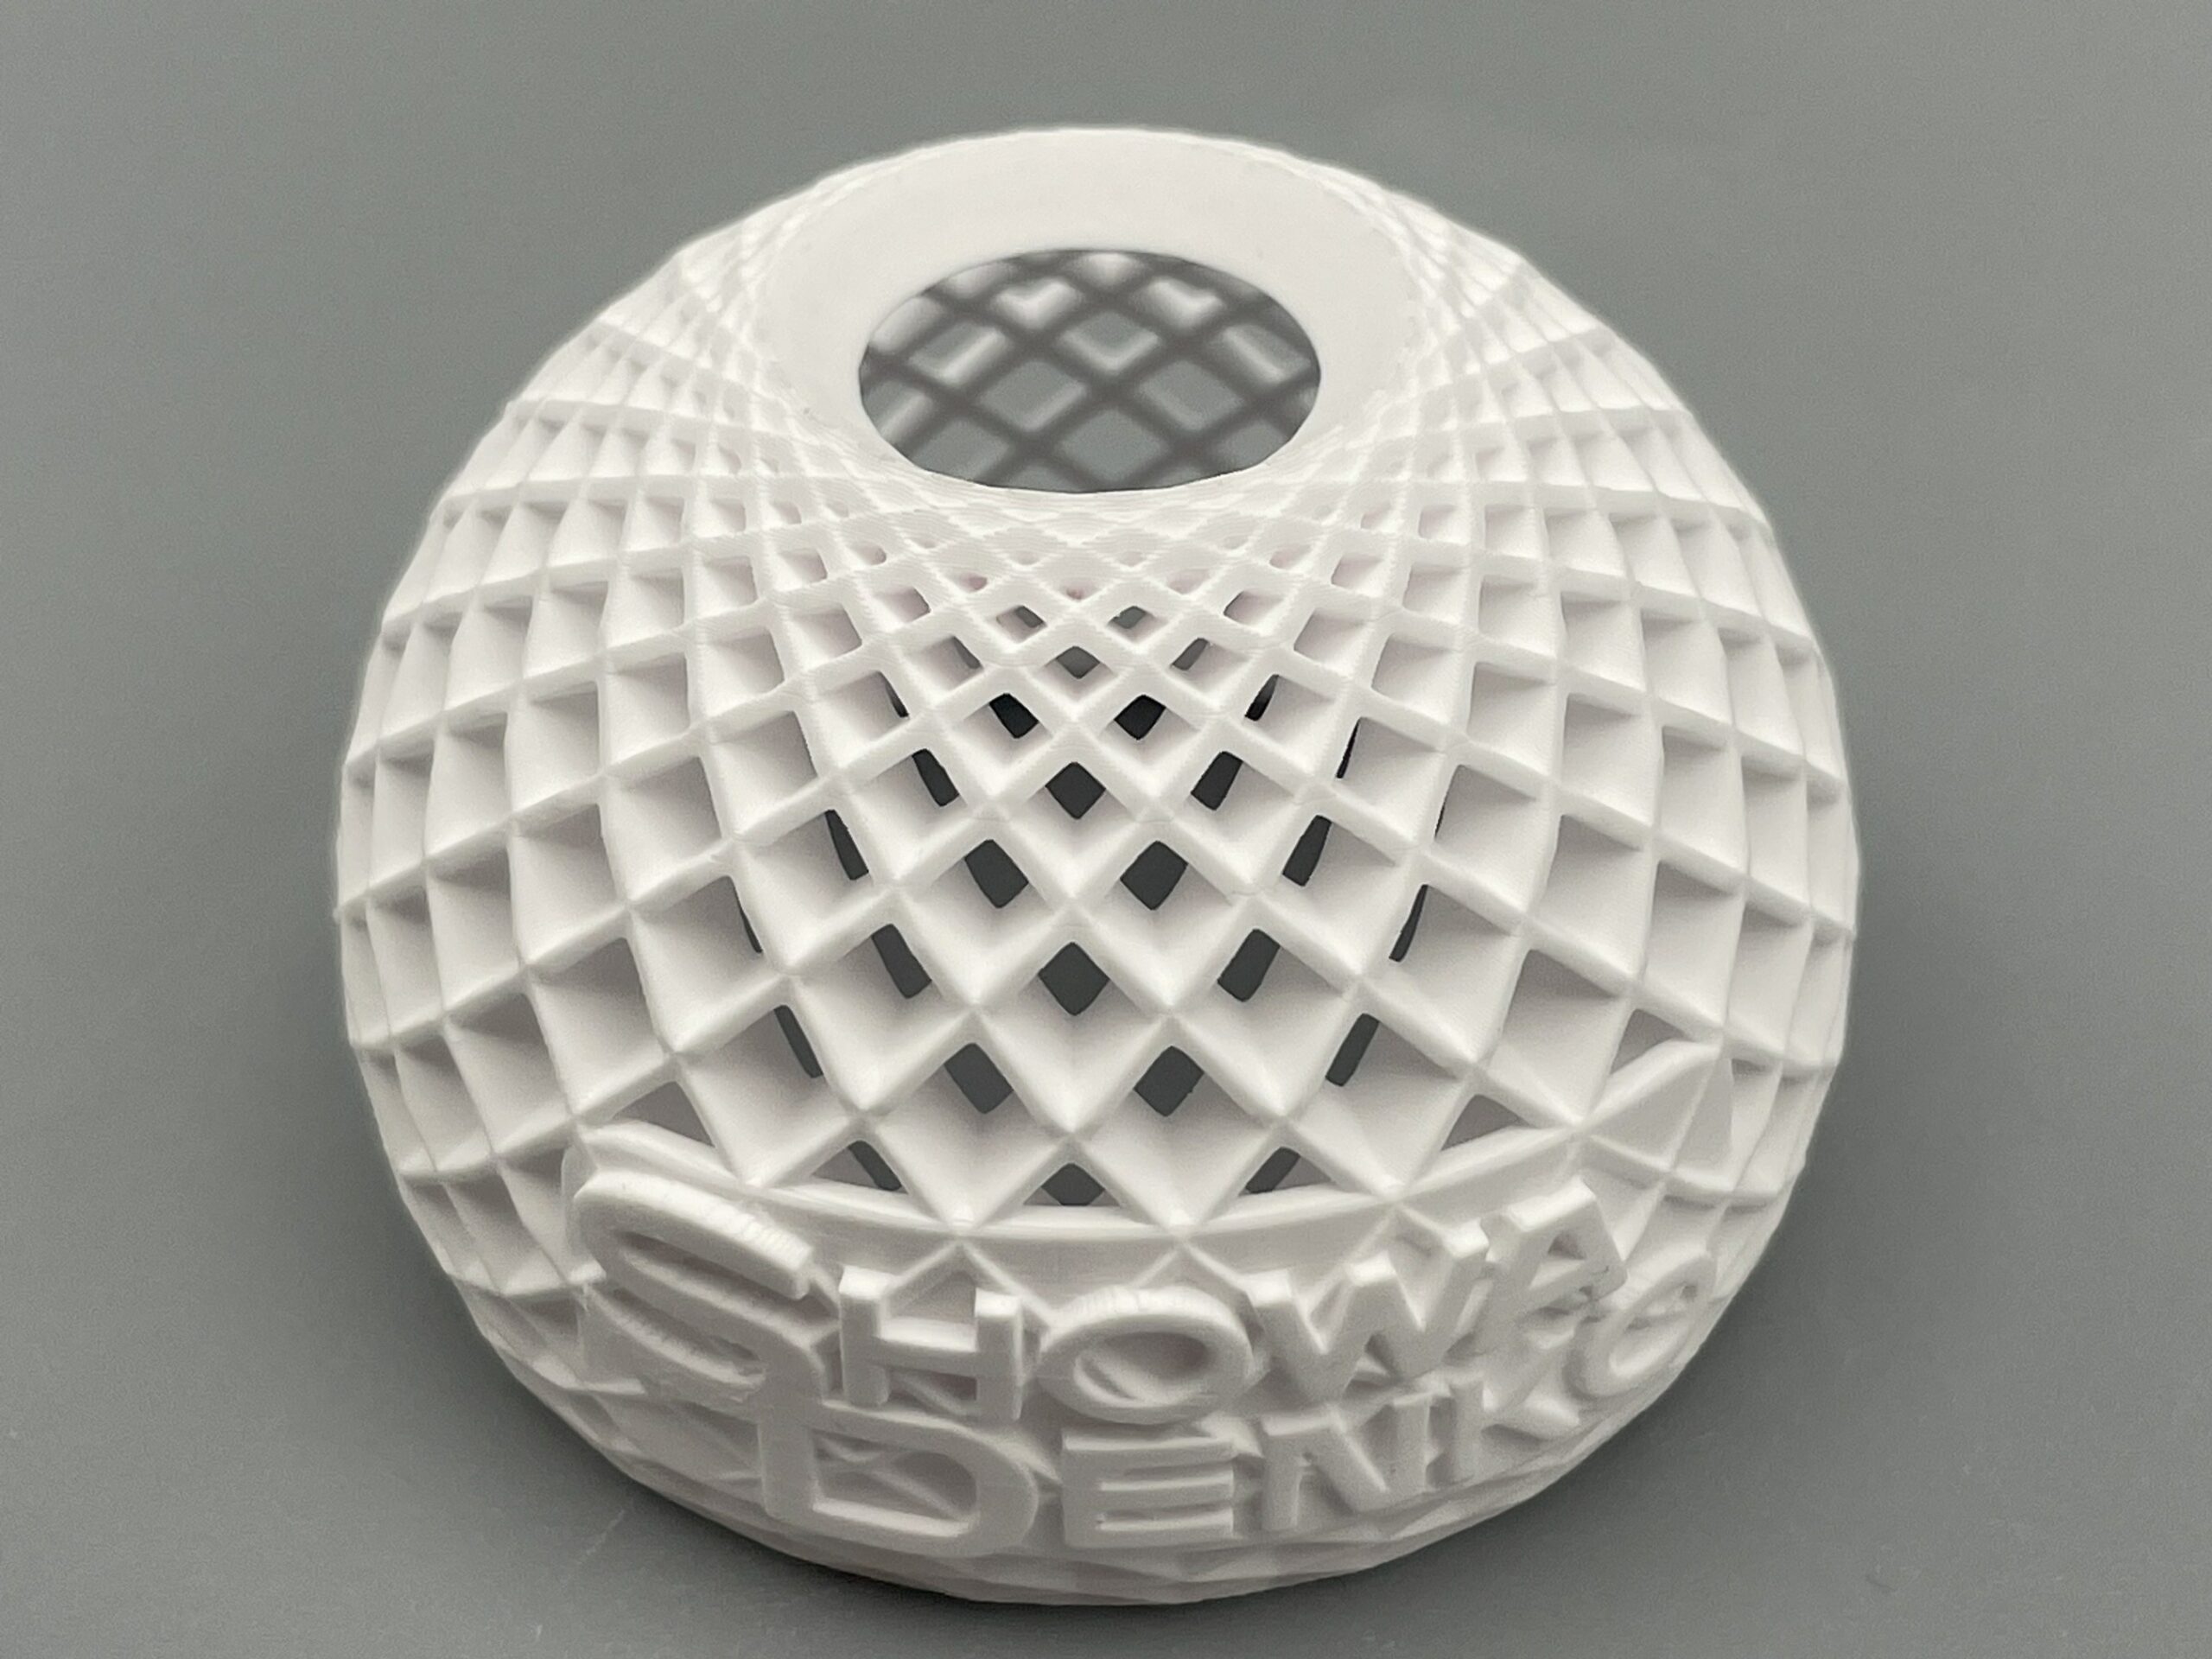
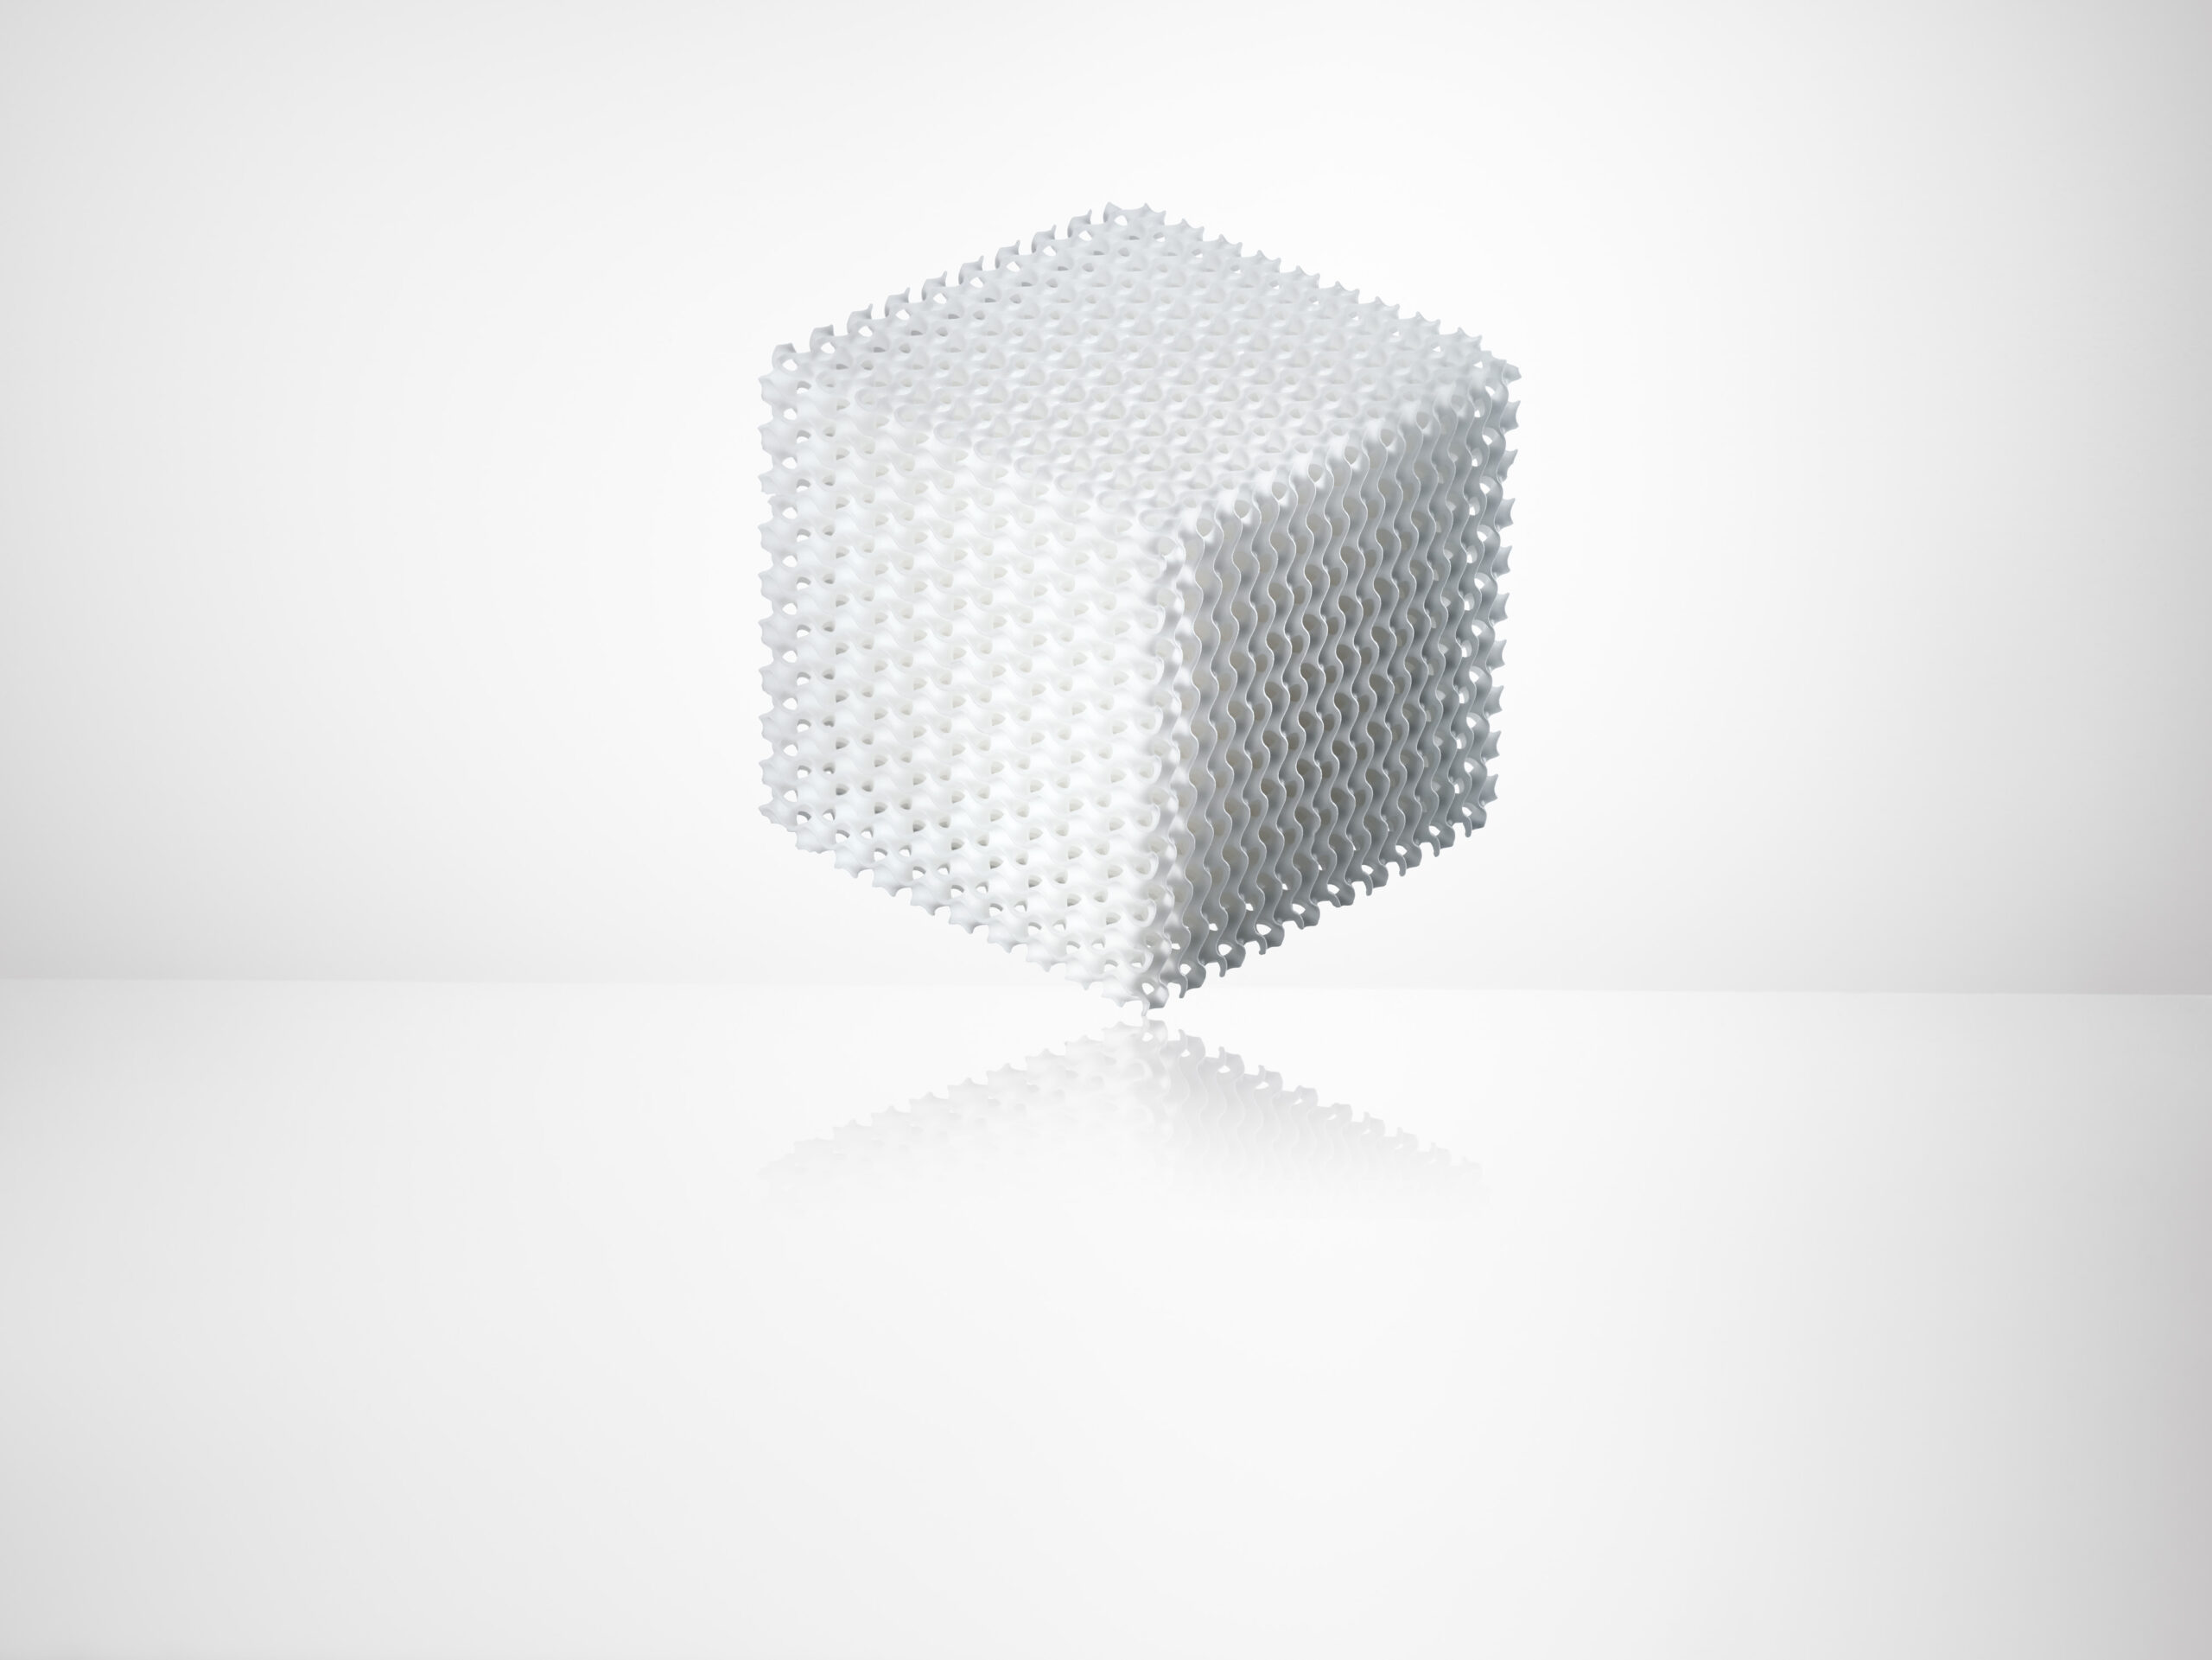
For the Tethon3D demonstrator shown here, the original caption reports loading above 75% by volume and 90% by weight, with post-sintering shrinkage below 10% in each axis. These are supplier-reported figures without an accompanying test protocol in this feature; they do not apply to every alumina resin.
Dentistry and selected implants are among the applications being explored. Bioresorbability concerns materials such as particular calcium-phosphate formulations, whose behaviour differs; it is not a property of every technical ceramic. Zoran Ostic outlines Lithoz’s view in 2022 below.
“Bioresorbable ceramic implants, made of materials such as tricalcium phosphate or hydroxyapatite, dissolve in the body as the organic bone heals and grows. As such, ceramic implants promote bone healing and the need for a second surgery to remove the implant is completely eliminated. At the moment, however, metal implants – which often have considerable long-term side effects for the human body – are still the most common solution, meaning that the main challenge here is encouraging surgeons to shift away from a trusted solution to try a more innovative material.
In general, many applications for high-performance ceramics are under-developed by the market due to the fact that end-users of conventional technical ceramics buy from more established service providers. These manufacturers utilise traditional forming technologies and therefore have certain design limitations which the customer is accustomed to. They will design their parts based on these existing and well-known limits, despite there being huge potential improvements in part efficiency, design evolution and functionality using additive manufacturing instead. There is little motivation for the established service providers to move towards AM as they already have a successful and selling product. But we have also clearly seen that with the publication of some profitable business cases, the ceramic industry has really been roused from that sluggishness. Therefore, the most important focus of the ceramic AM market is to educate the industry and end-users in particular about the advantages of this technology, encouraging uptake and therefore spreading the message of this game-changing technique further”, the expert adds.
Lithoz’s calcium-phosphate materials do not all behave identically. The statement above does not guarantee resorption within a given time or rule out further surgery for every patient. Clinical suitability and risk must be evaluated for the device and intended use; it does not establish general superiority over metal implants. The FDA also distinguishes assessment of the finished device from that of a material in isolation.
What’s the next big question?
The 2022 interviews describe a developing market with production applications already in use. Adoption depends on total cost, qualification, skills, reliability and user needs; it cannot be reduced to fear of change.
Lithoz’s experts argue that their technology has advanced towards industrial production and that viable business cases can encourage adoption. This supplier perspective does not mean that scaling, qualification and quality challenges have been solved for every application.
The next step is to identify use cases, compare processes and validate performance on representative parts before committing to wider production.
This feature was first published in the March/April 2022 issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.