Feature first published in the March–April 2021 issue of 3D ADEPT MAG. Roles, products and estimates reflect interviews from that period. Manufacturer performance claims depend on the application and configuration.
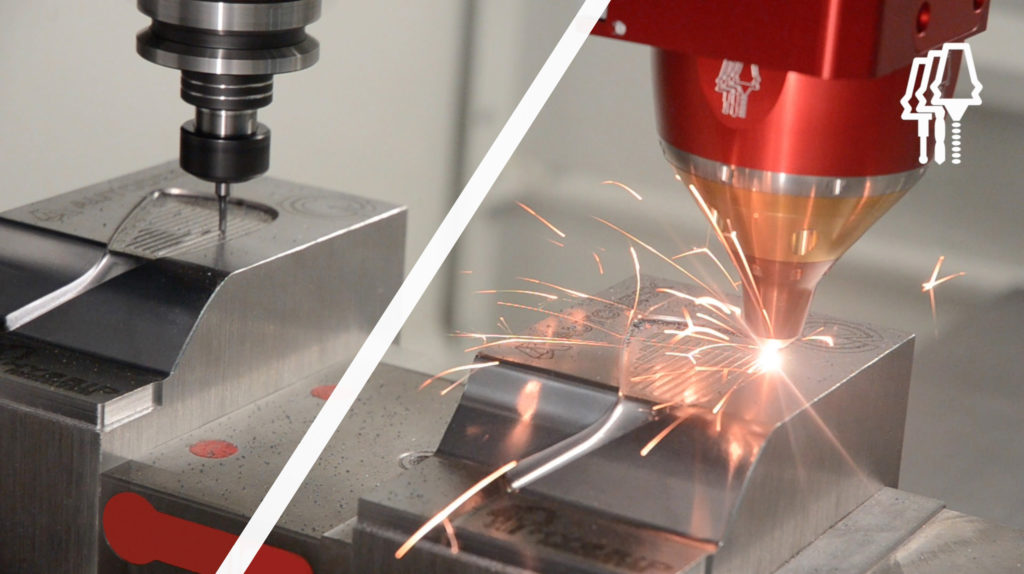
Hybrid manufacturing combines production processes. This feature focuses on additive and subtractive operations within one machine: adding material where needed, then machining surfaces that require it. Integrating these operations raises design, control and qualification questions.
Material addition and removal can alternate in different sequences depending on geometry and tool access. Which technologies can be combined? How should the sequence be planned, and how do hybrid costs compare with separate machines?
As we saw with AM, the potential benefits of HM have convinced some early adopters on the market. As a matter of fact, in the non-exhaustive list of companies contributing machines, software or applications to hybrid manufacturing, one counts DMG MORI, ELB-Schliff, Matsuura, Mazak, Mitsui Seiki, Okuma, Meltio, 3D-Hybrid Solutions, Inc., Hermle, Siemens, Sodick, Diversified Machine Systems, Fabrisonic, Optomec, Thermwood, Weber Additive, Sulzer, and Hybrid Manufacturing Technologies, Imperial Machine & Tool Co. to name a few.
However, to tackle this topic, we have invited Hybrid Manufacturing Technologies’ Co-founder and CEO Dr. Jason Jones as well as Hans Weber Maschinenfabrik GmbH’s Commercial Director Additive Manufacturing Manuel Kolb to share the manufacturer’s perspective. CGTECH’s Product Manager, Gene Granata will touch on the software aspect of this topic.
The combination of additive and subtractive processes
AM feedstock can take the form of powders, wire, pellets, sheets or liquid resins. These forms do not constitute three standard process families: ISO/ASTM 52900 terminology distinguishes seven categories by manufacturing mechanism.
Subtractive processes remove material from metals and other materials, depending on the technique. Milling, grinding, EDM and cutting methods have different constraints. CNC describes numerical control, not a material family. Directed energy deposition (DED) is commonly combined with machining, but it is not the only additive option.
“Any type of additive process that uses a nozzle for deposition can be combined with milling, grinding, or even laser cutting/ablation. The most common combination is Directed Energy Deposition (DED) with CNC milling of metal parts. Material Extrusion (ME) with CNC milling for polymer composites is also a growing adoption path, particularly for making fixtures and tooling”, Jason Jones from Hybrid Manufacturing Technologies states.
The combination must accommodate material compatibility, temperatures, tool access and machine safeguards; not every pairing is feasible without adaptation.
Systems can be designed as hybrids or retrofitted to existing equipment. DED, sheet lamination and some powder bed fusion configurations can be combined with machining. Laser cladding is a form of DED: integration requires coordinated axes, material delivery, control and safeguards, beyond simply mounting a head.
Speaking of hybrid machines his company develops and commercializes, Jones explains:
“The part shape and material(s) determine the processes required and the required accuracy for the machine. We choose the best combination of machine and processing heads/tools for our customers. We integrate the modules into existing machines or supply new turnkey systems. When budgets are tight, often customers will opt for field integration into machines that they already own. However, additional capabilities come with one of our fully optimized turnkey solutions. We have solutions running on CNC machines (verticals, universals, mill-turns, etc.), gantries, grinders, robots, and parallel kinematic machines (hexapods, etc.).”

Wire arc additive manufacturing (WAAM), combined with milling, can suit large metal parts. Deposition rate depends on material, energy source, strategy and geometry; there is no universal comparison ratio with laser or electron-beam processes. Machine reach, handling and thermal constraints still limit the build envelope.
Ultrasonic additive manufacturing (UAM) combines solid-state joining of metal foils with machining. This sheet-lamination approach can enable multi-material structures and embedded components, subject to material and process compatibility.
Cold spray deposits metal particles without melting them and can be followed by machining. Deposit properties and any required treatments depend on material and processing conditions. See our cold-spray feature in the January–February 2021 issue of 3D ADEPT MAG.
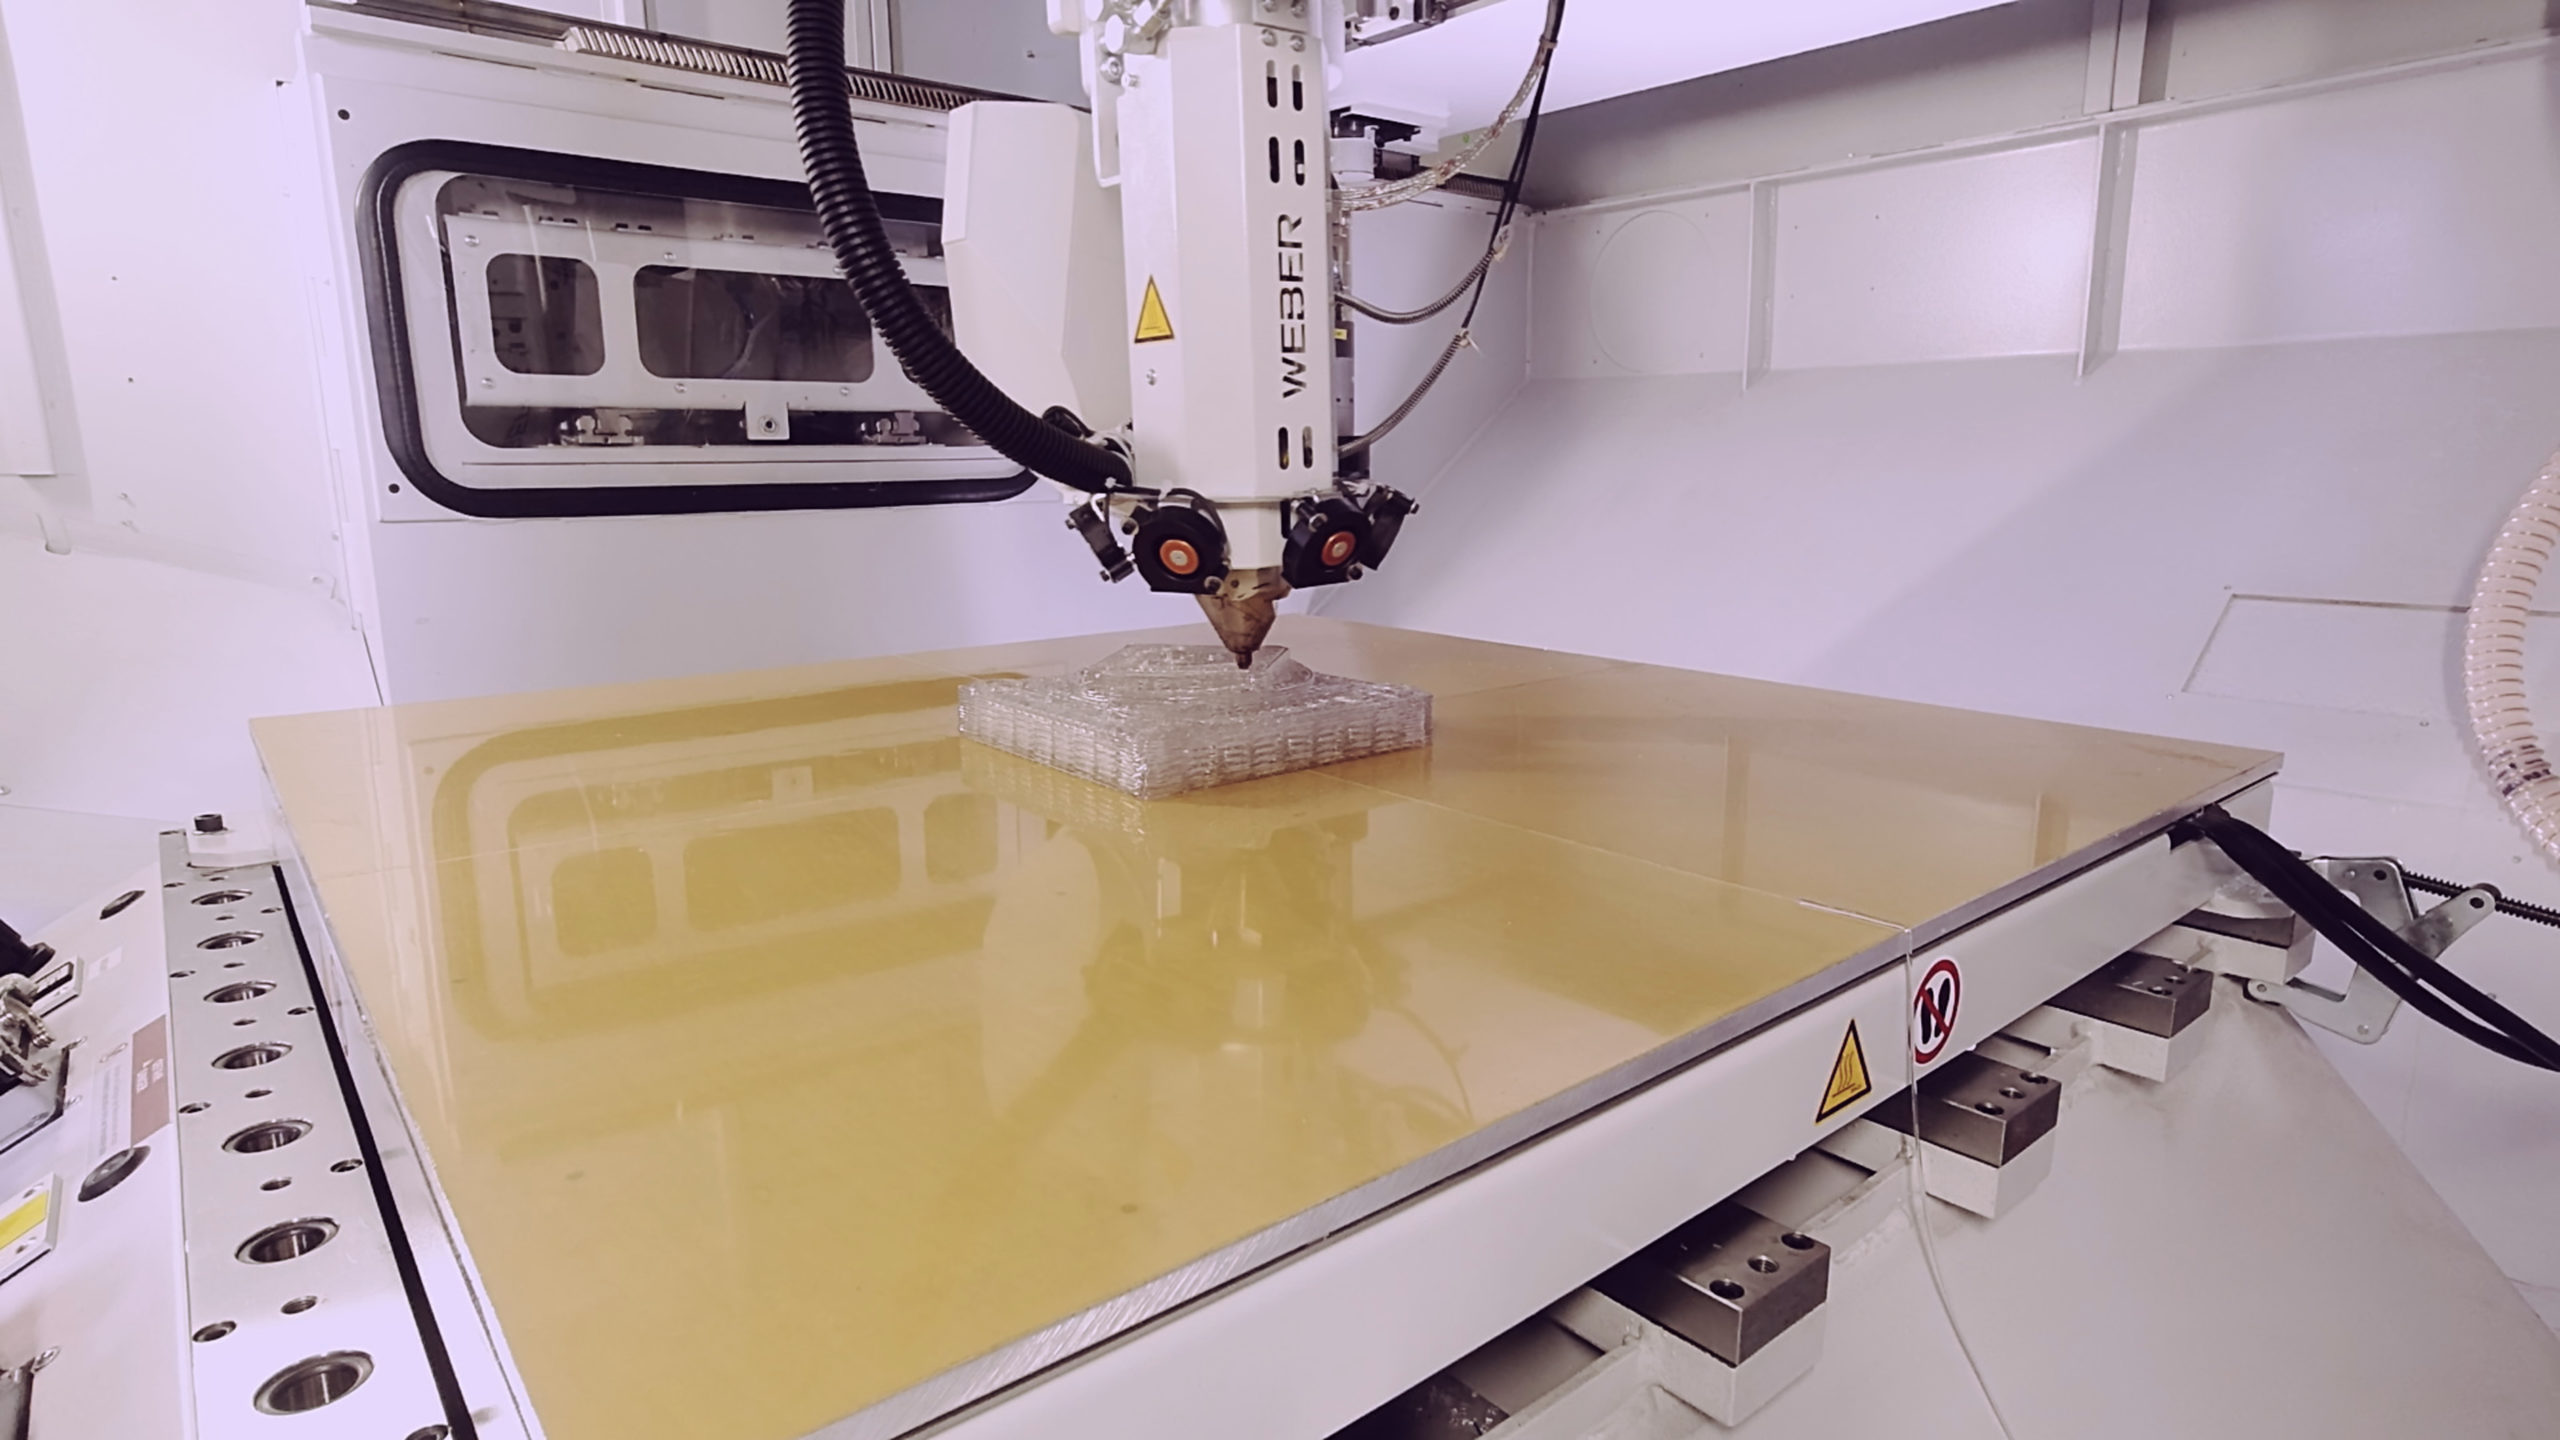
Another example of hybrid manufacturing technology can be seen with the extrusion of plastic pellets. “We can combine fused granular fabrication with 5-axis milling to fabricate large, complex parts, with high surface quality and minimum material use. The additive process is a planar layer-by-layer melt deposition process, as known from fused filament fabrication. The milling process follows the same CNC machining concept Reichenbacher Hamuel is implementing in their classical subtractive machining centers. The two processes can be carried out sequentially: first the mentioned additive process, then the conventional milling process” Hans Weber Maschinenfabrik GmbH’s Manuel Kolb explains.
The manufacturing process of hybrid machines
Given the wide range of possibilities that exist in the HM portfolio, it won’t be possible to have a closer look at each process developed by market players. With examples provided by Hybrid Manufacturing Technologies, Weber Additive and CGTech, we will have a look at what to expect from the manufacturing process at the software, and post-processing levels.
The software perspective
Design must account for deposition and machining access, stock allowances, workholding and operation changes. CAD defines geometry, CAM prepares toolpaths, and simulation and verification tools check execution within their capabilities.
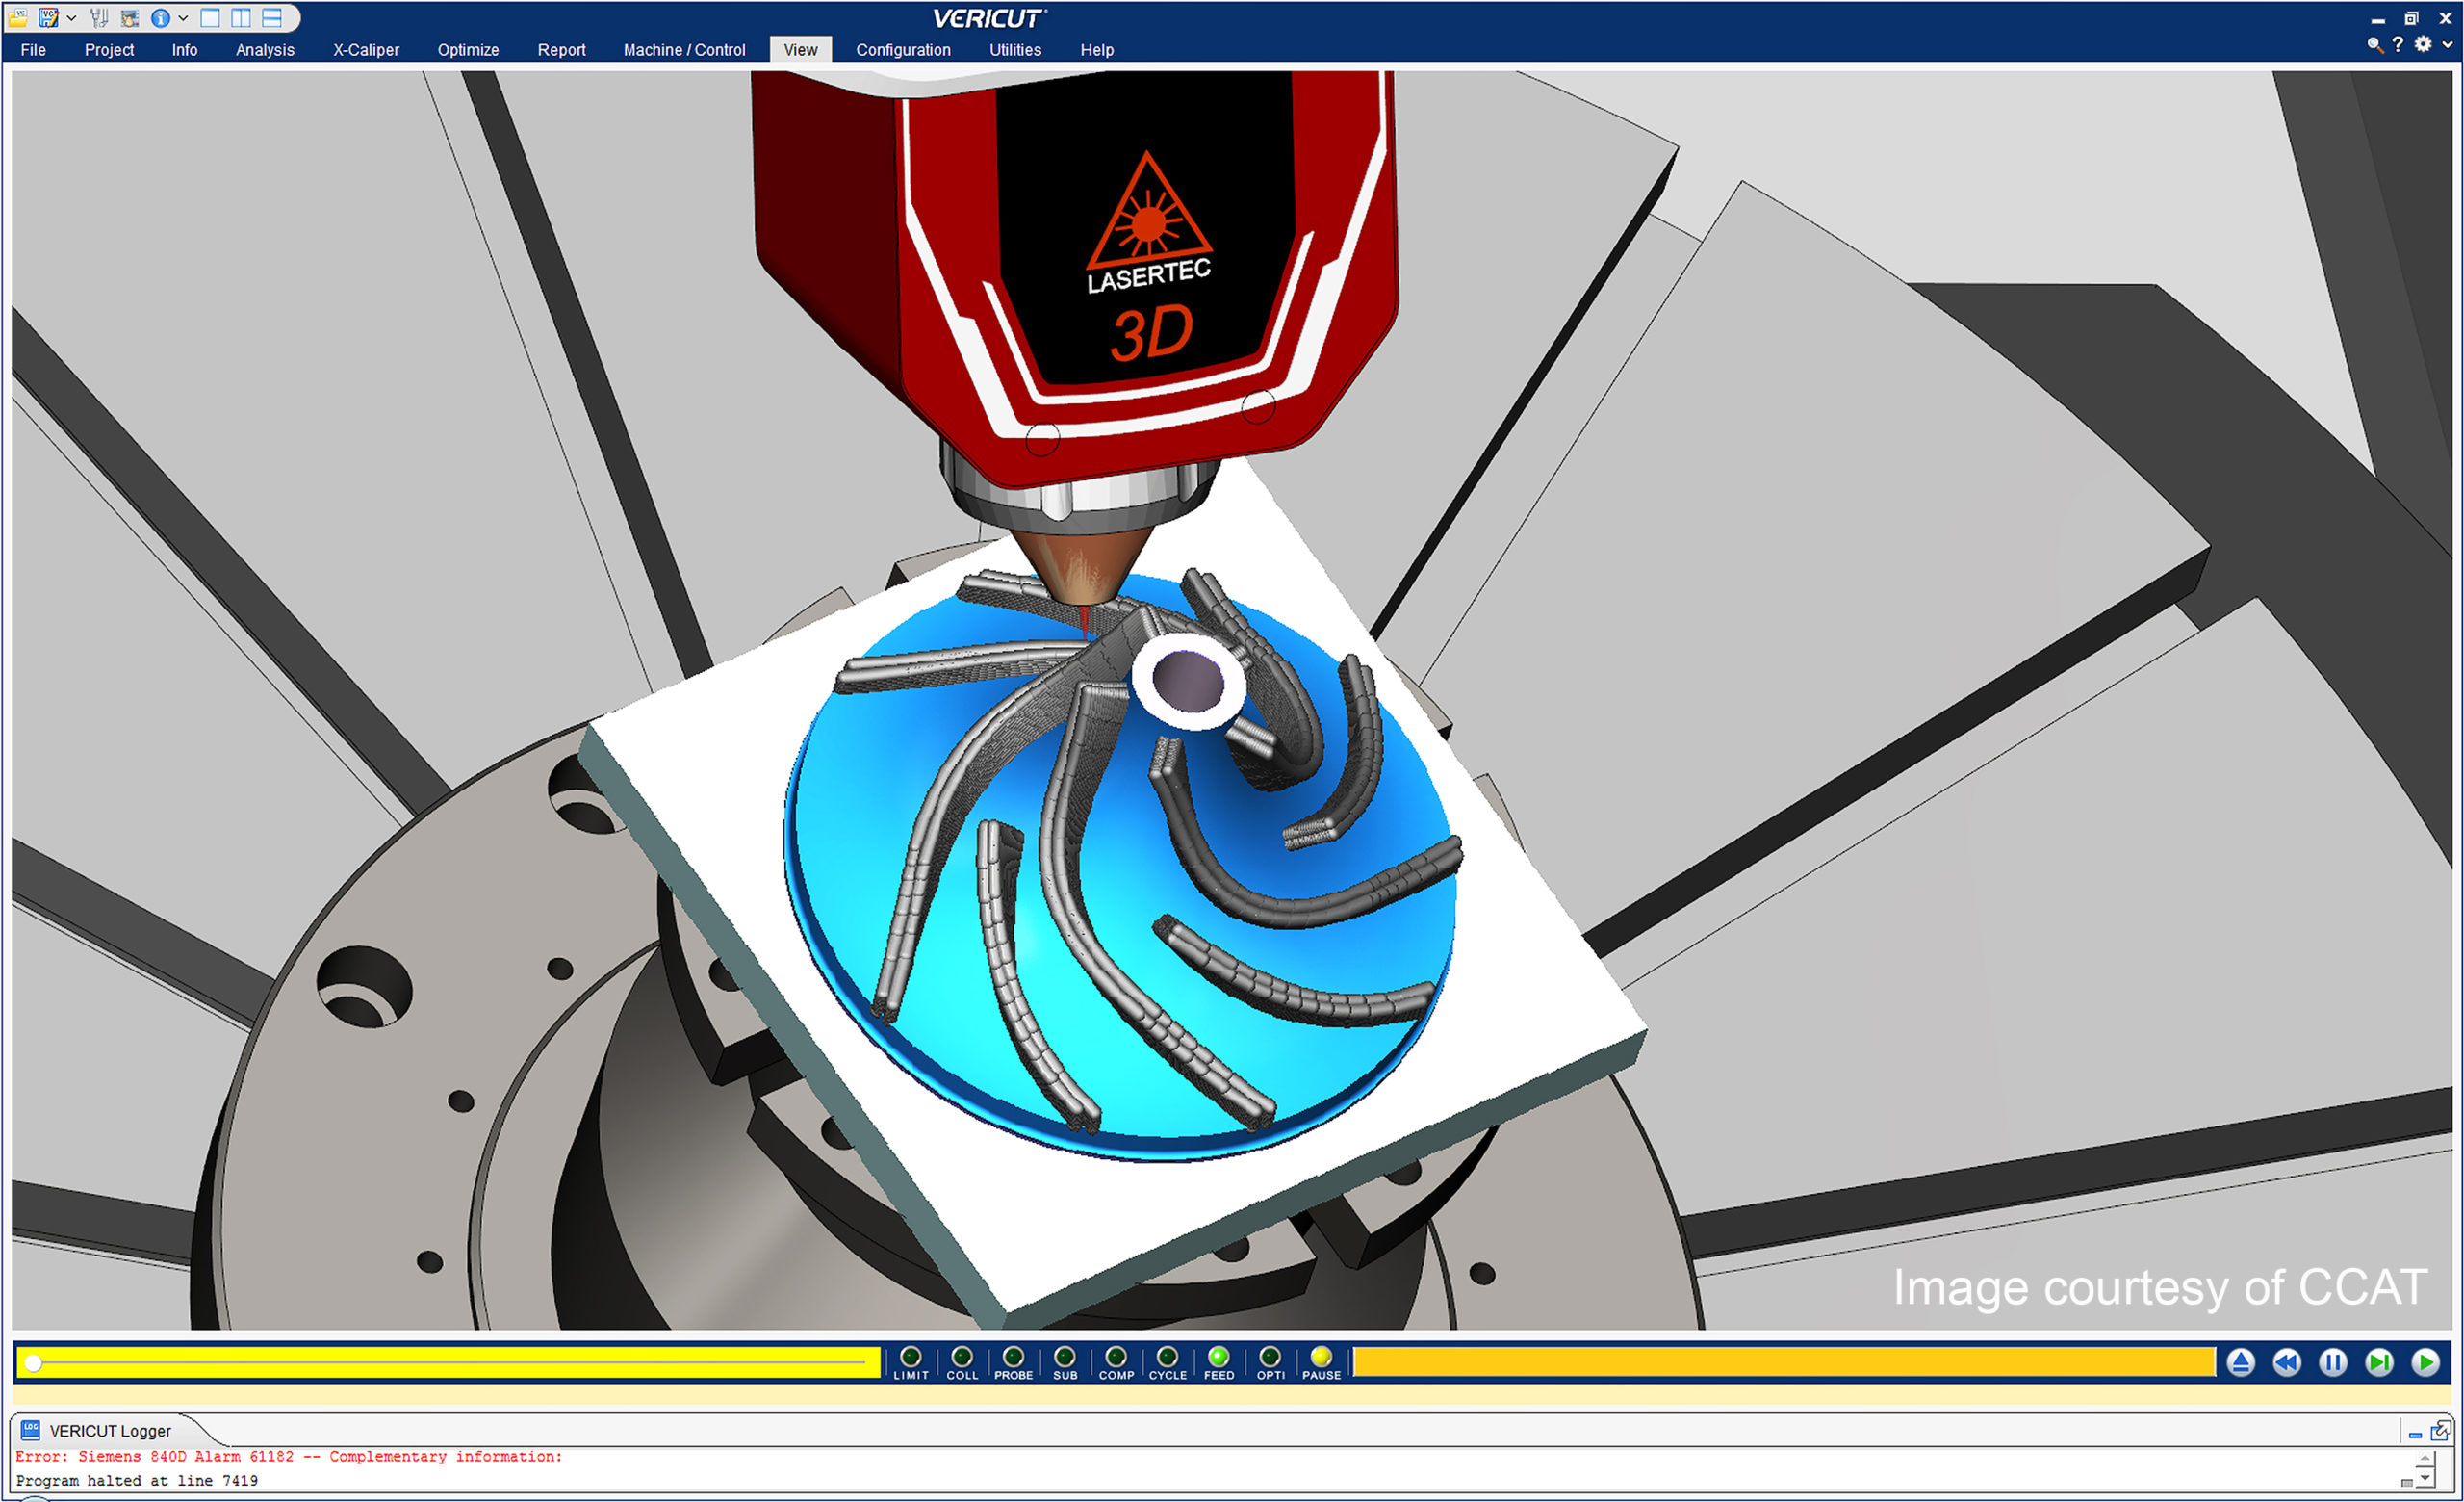
“Dedicated CAD/CAM and verification software is HIGHLY recommended to facilitate efficient and SAFE hybrid manufacturing. Every aspect of hybrid part manufacturing is more challenging, more expensive, and often unfamiliar to many companies breaking into this exploding field. Software dedicated to hybrid manufacturing helps by optimizing part designs for Additive Manufacturing (AM), offering unique operations not available in “subtractive-only” CAM software, and by verifying that the entire hybrid manufacturing process (sometimes involving multiple CNC setups and machines) will work as expected to produce the designed part.
Some manufacturers avoided investing in dedicated hybrid manufacturing software, and instead opted to use less efficient combinations of traditional subtractive CAD/CAM design and toolpath technology. They even resorted to manual editing/merging NC programs to create programs for hybrid CNC manufacturing. However, this approach is extremely inefficient and error prone, and sometimes led to expensive incidents in the shop with costly downtimes that followed”, CGTECH’s Gene Granata points out.
While Hans Weber Maschinenfabrik GmbH’s commercial director of AM believes in the importance of design software advances, he lays emphasis on three important aspects: the necessity to have an excellent 3D model quality or resolution, the calculation of the necessary printing offset of the contours as well as the thermally induced intrinsic bulk stress. Taking the example of a HM process based on plastic pellets and milling, he states:
“One important aspect is the 3D model quality or resolution. It is highly recommended to avoid meshed formats like .stl, because the precise milling process can make these artefacts visible. If it cannot be avoided, then a proper mesh resolution is important.
Another aspect is the calculation of the necessary printing offset of the contours, so that the milling process has enough material to remove and guarantee a homogeneous and void free surface finish. The offsetting can be very individual depending on the exact geometric requirements. The third aspect is the thermally induced intrinsic bulk stress in the printed material. During the milling process and removal of eventual support structures, the part can be deformed by the bulk stress and the release of fine structures by material removal. This must be respected during the planning of the milling process, to avoid excessive material removal at respective surfaces.”
In a hybrid DED+CNC machine on the other hand, Hybrid Manufacturing Technologies’ CEO observes that “the deposition paths and the machining tool paths both need preparation. Fortunately, the digital workflow for both of these processes is nearly identical. In fact, both can be generated from the same computer model and often in the same CADCAM software.”
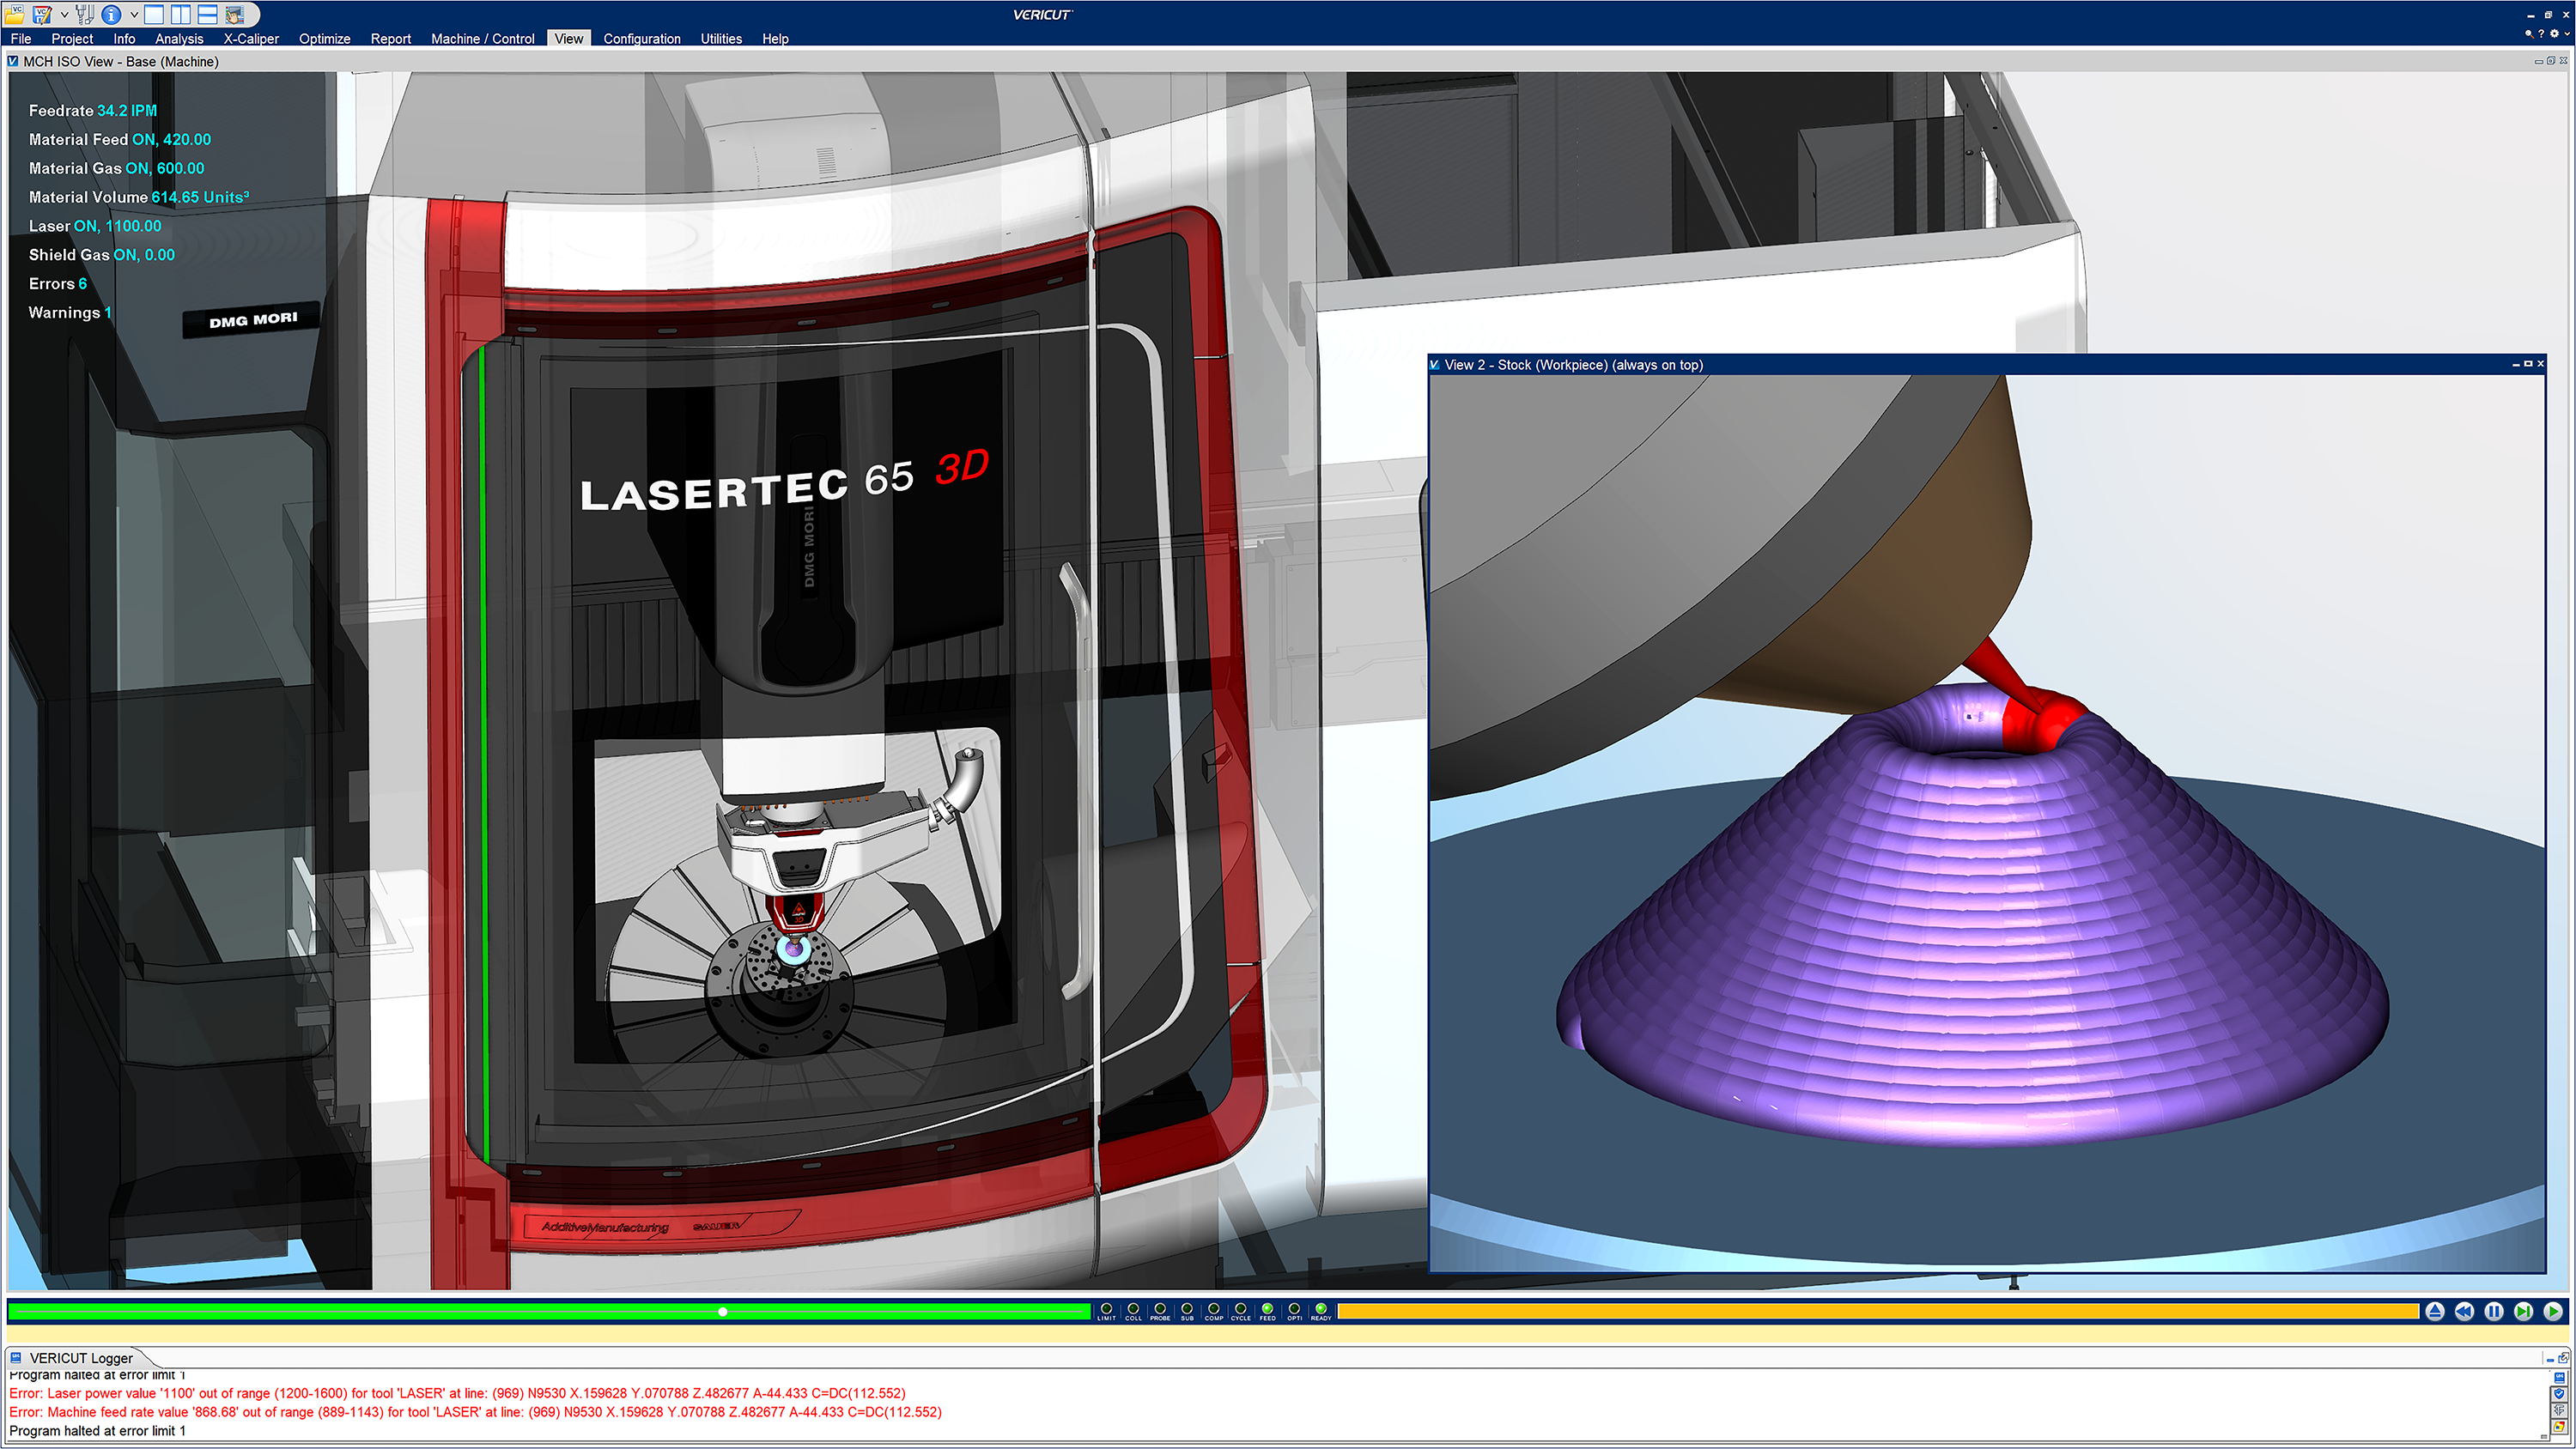
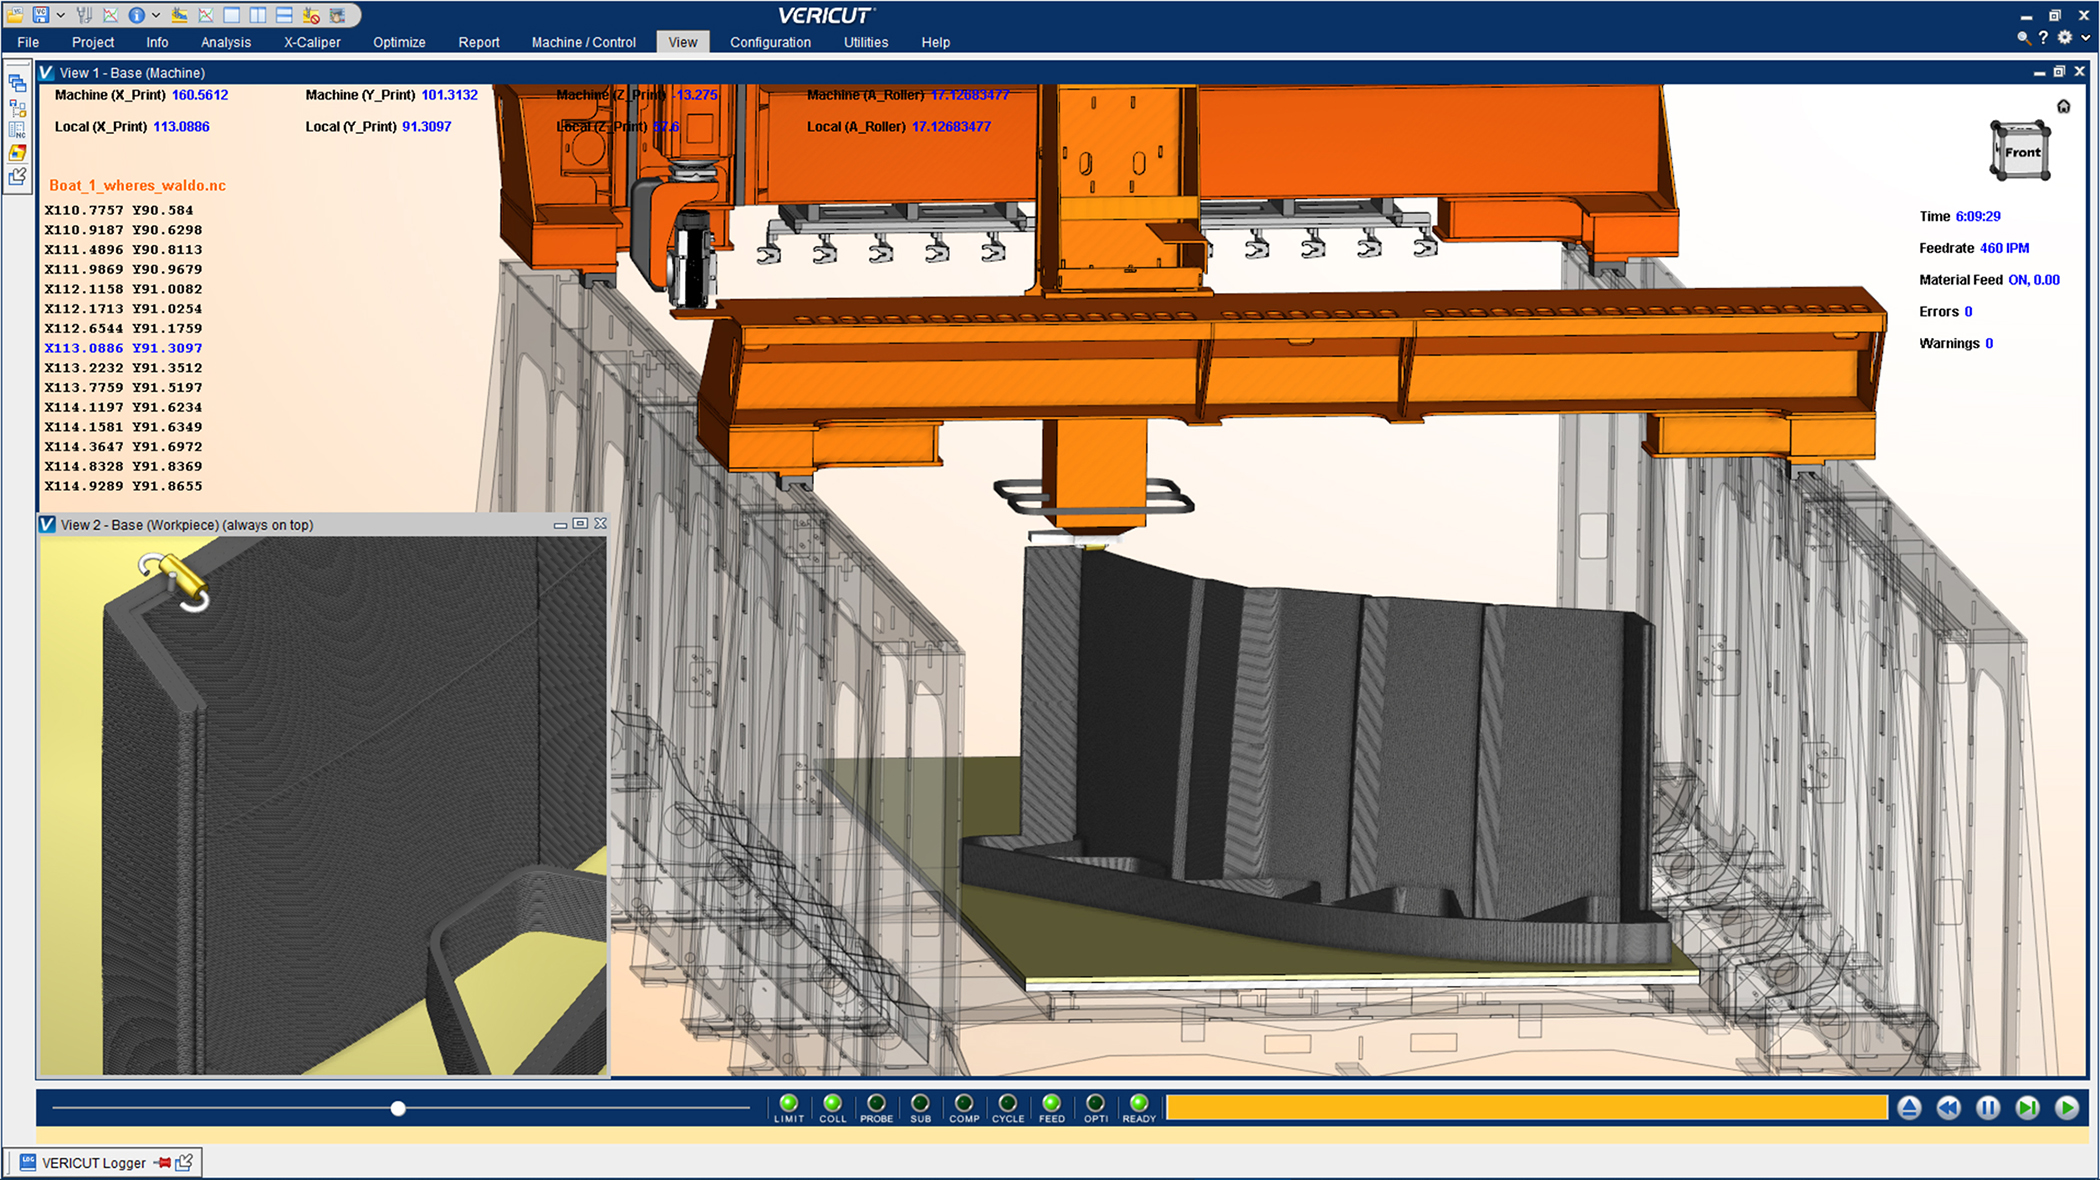
CGTech, previously discussed in our Thermwood interview, describes hybrid-machine program verification. The 2017 VERICUT 8.1 documentation presents simulation of additive and subtractive operations. Toolpath and geometry verification does not, by itself, establish metallurgical or mechanical qualification.
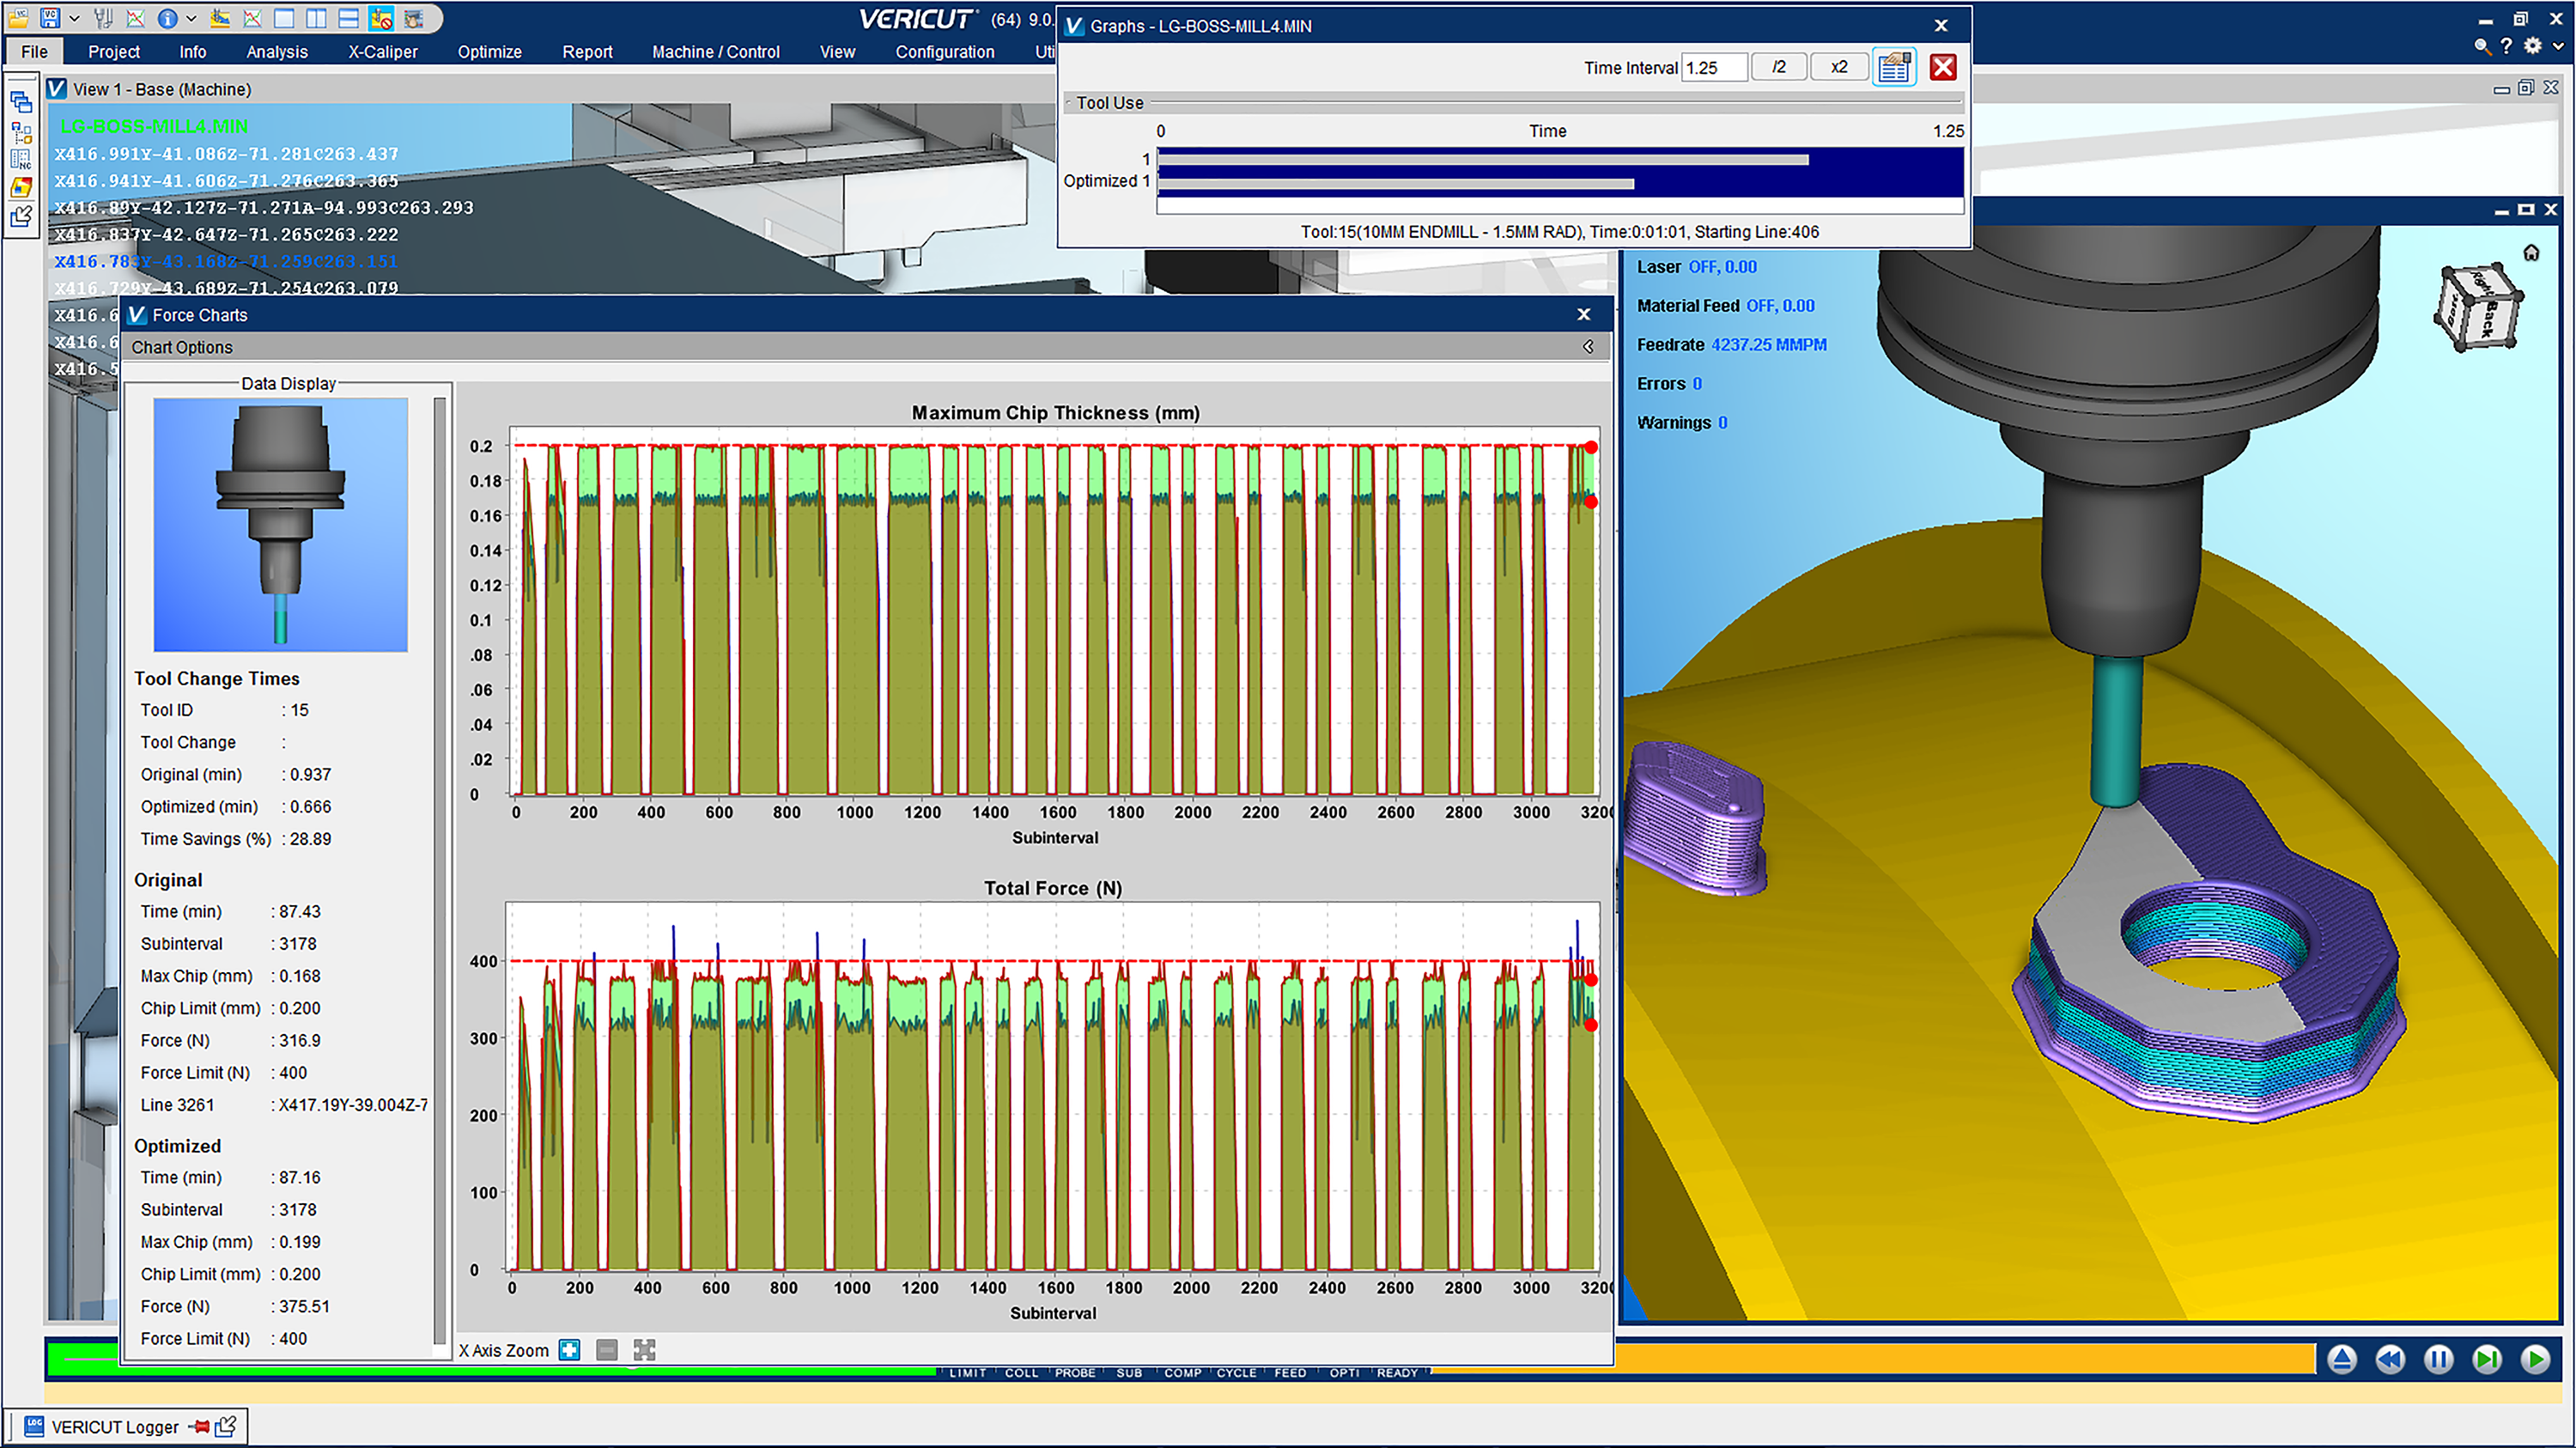
First, “an important and valuable aspect of hybrid manufacturing is optimizing the subtractive machining paths. With VERICUT Force optimization, this can be done while verifying NC programs, ensuring the final NC programs are not only free from errors, but the overall process is efficient as possible.”
Verification depends on the machine, tool and workpiece models and the functions actually simulated. It does not guarantee the absence of every physical manufacturing error.
“As we do with all of VERICUT’s digital twin CNC machine simulations, we worked closely with the folks at Thermwood to simulate their LSAM machines, including the NC machine codes that control the additive functions: dispensing and monitoring of material, roller tangential following that presses the composites material onto the layer beneath it, and ensuring each layer builds on top of previously deposited material or some other build surface.
A simulation that runs in minutes can inform users when conditions are not suitable for additive deposition on their LSAM machine, detect when expensive collisions could occur with work holding fixtures or the part being built, optimize machining, and check that the final hybrid manufactured part matches the intended design”, Granata notes.
Part consolidation, topology optimisation and generative design may reduce some interfaces or assembly mass. These possibilities remain subject to manufacturing, inspection, maintenance and service requirements.
Taking the example of VERICUT, Granata sheds light on software specifications related to AM, subtractive processes and hybrid technologies: “Users can add then cut, or cut then add in any order. On hybrid CNC machines, the choices about the order in which additive versus subtractive process are applied to produce the part are controlled by the order of NC programs, and the specific NC codes and parameter values they contain. By processing NC programs in the same order as they will be used on the hybrid CNC machine users see exactly how the part will be built, and machined, to achieve the final shape.
Multiple operations that are performed on different CNC machines can also be simulated via multiple “setups” in VERICUT. For example, consider a turbine impeller type of part that is created by first turning the shaft/hub on a CNC lathe, then is moved to a hybrid 5-axis machine to deposit the blades on the hub, and perform the 5-axis blade and finish machining. VERICUT users verify the entire manufacturing process end to end, so they know it will work as expected to make the finished part.”
Manufacturing and post-processing
Alternating material addition and removal can apply to metals and polymers, but their processing conditions differ.
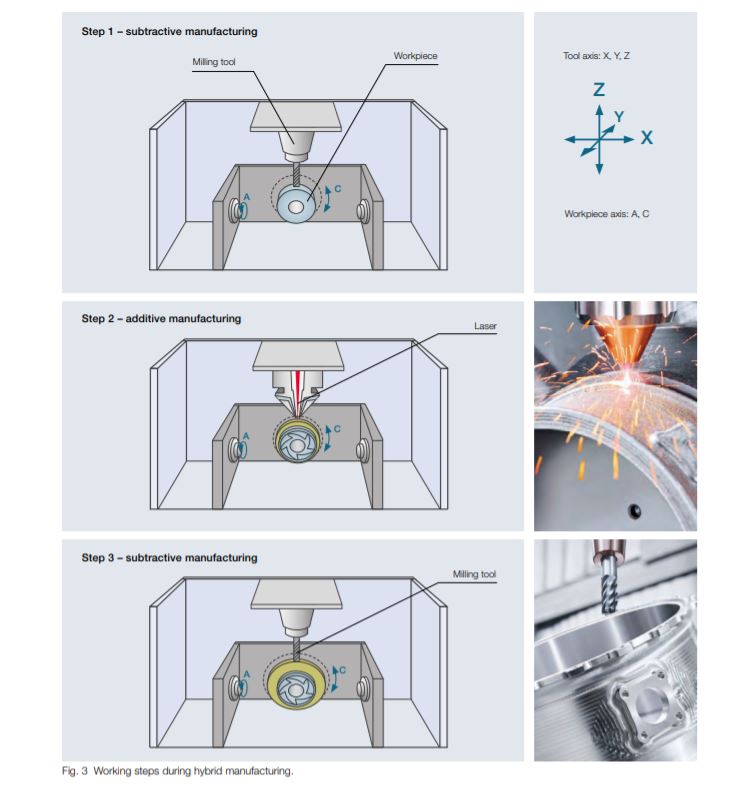
A deposition head can give way to a milling tool, then resume according to the programmed sequence. Tool changes may be manual or automatic. Differences between metals and polymers extend beyond temperature to cooling, chips or powders, workholding, safety and final properties.
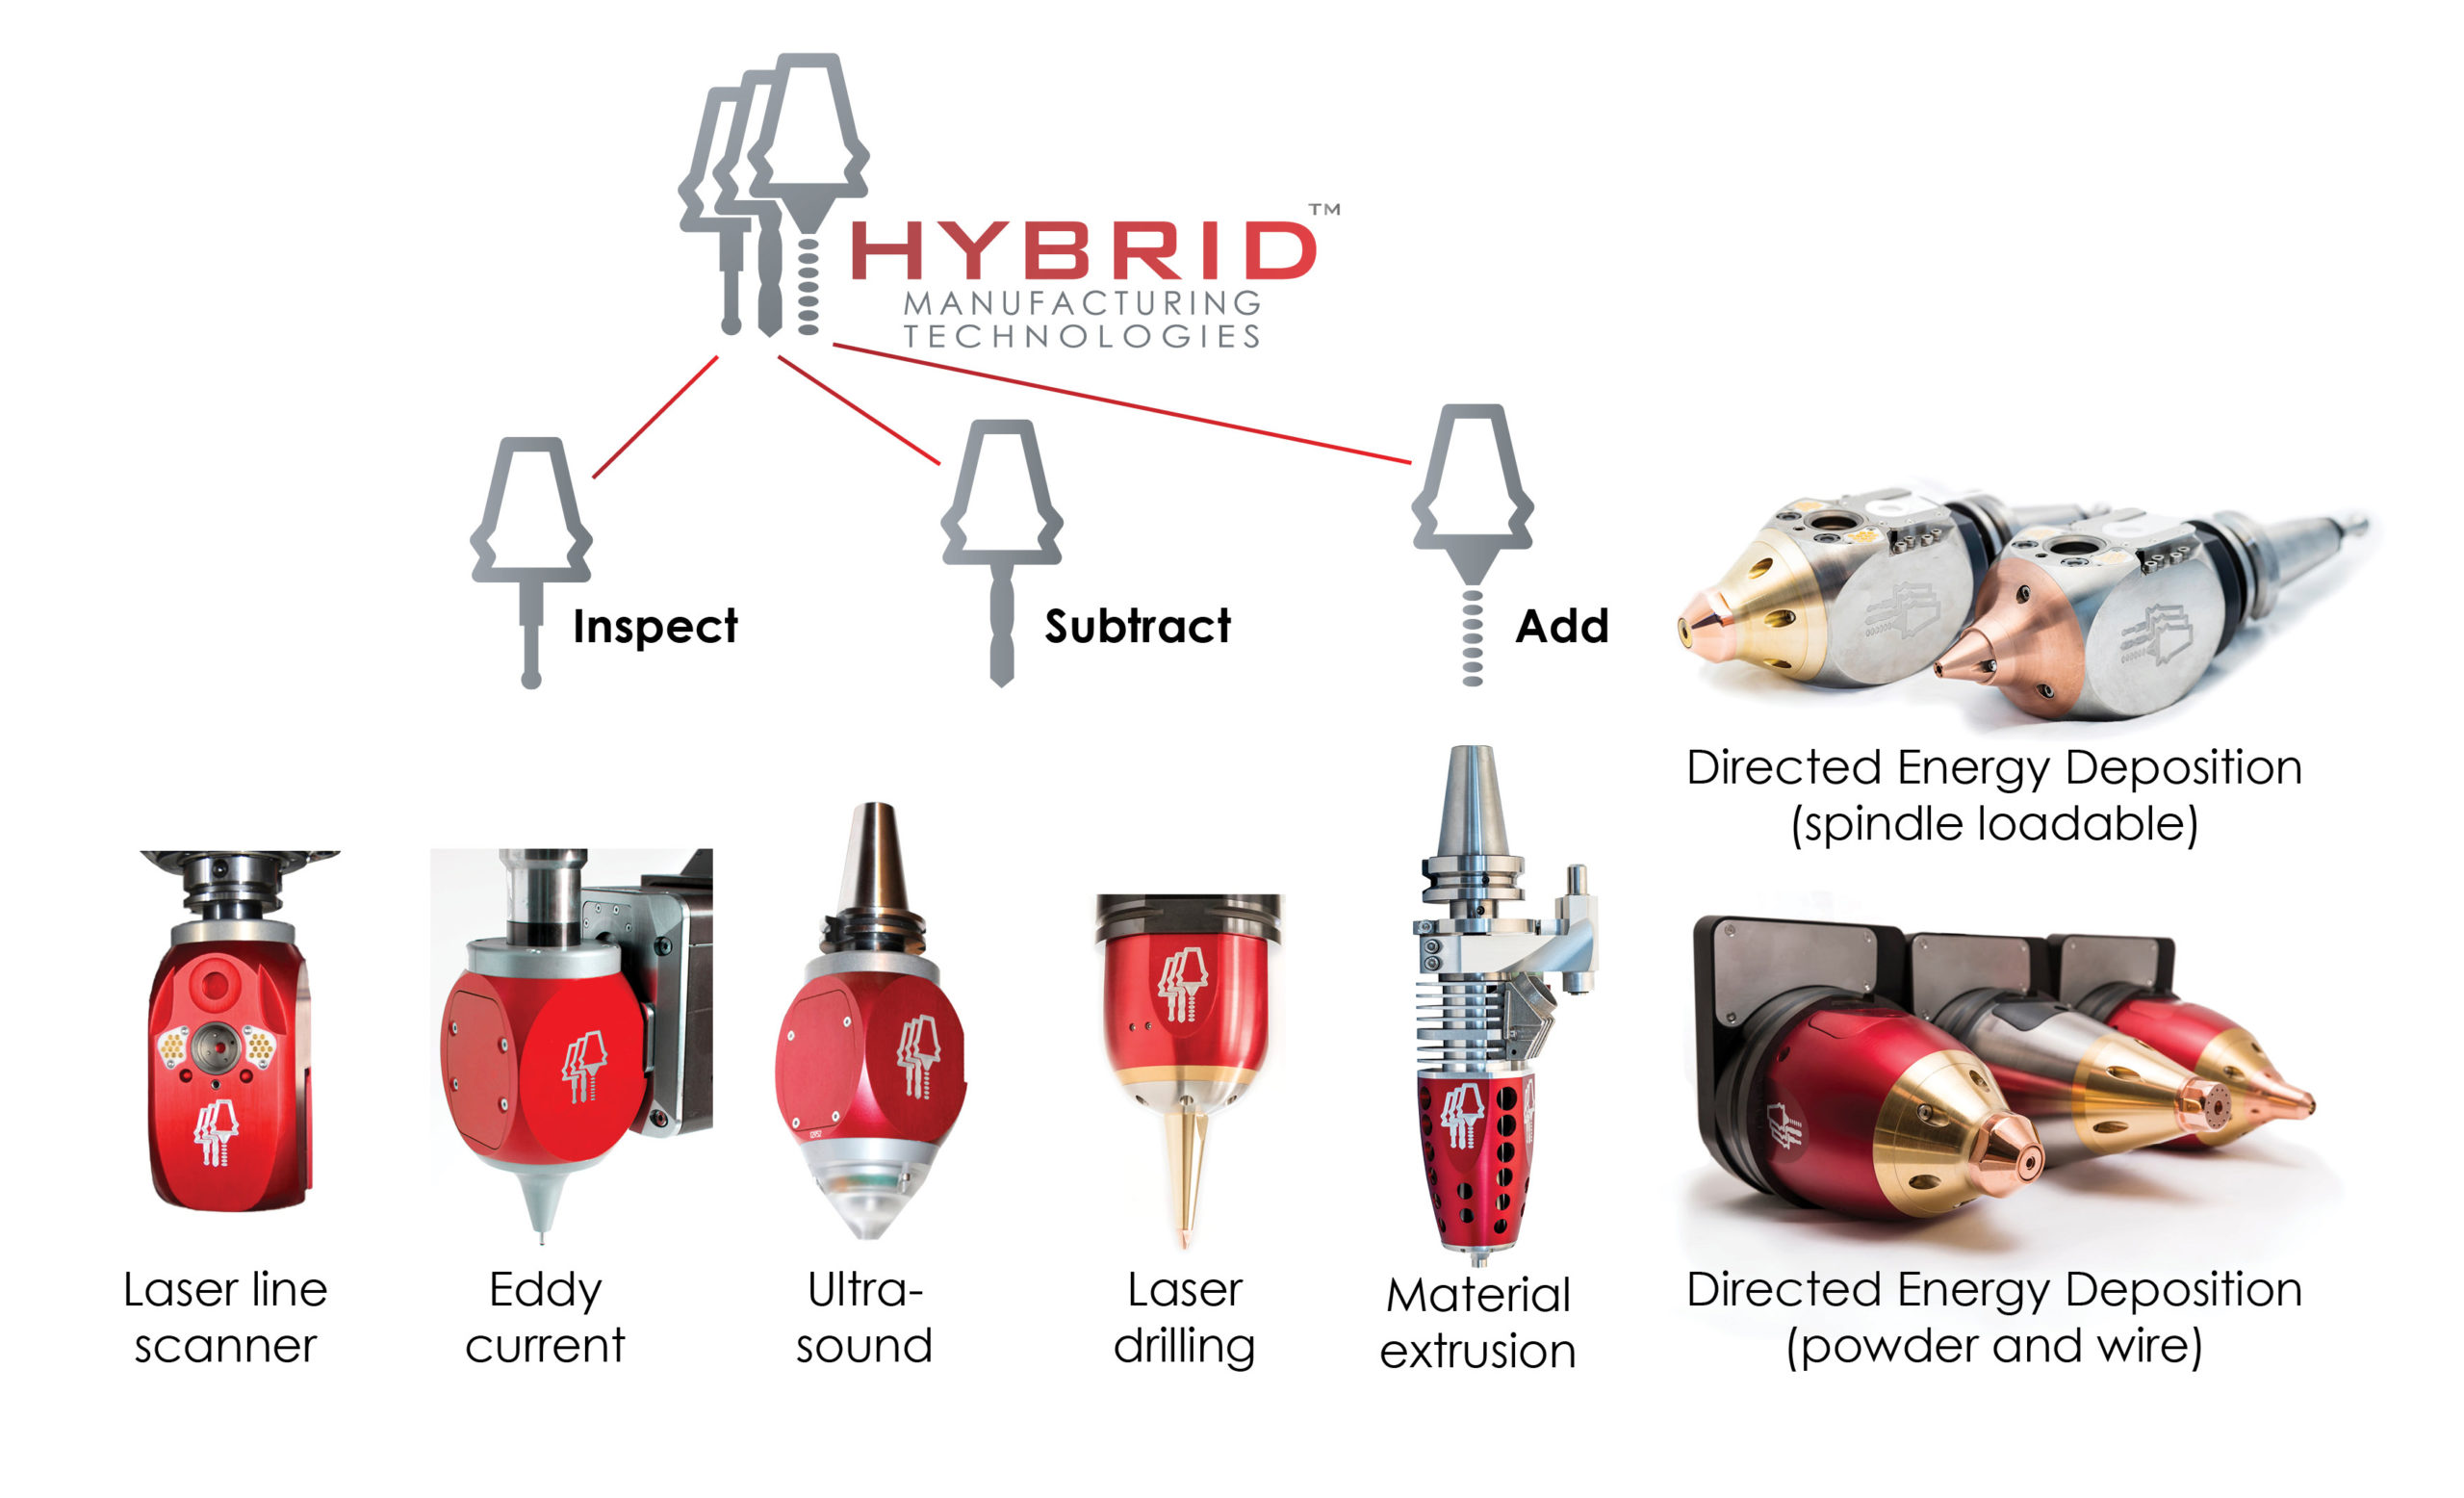
The company provides “a wide variety of additive (DED, ME, Jetting, Direct Write, etc.), subtractive, and inspection (probing, laser scanning, eddy current, and ultrasound) technologies integrated together”. “Our AMBIT™ processing heads are automatically interchangeable so a customer can choose the combination of processes that best addresses their application needs. These technologies are controlled using edge computing and closed loop feedback to enable robust, optimized, and traceable performance” Jones points out.
The inspection heads described by Hybrid Manufacturing Technologies perform checks during manufacturing. Each method has detection and access limits: integrated inspection does not automatically prove that every internal or external defect is absent. Deposition, finishing and inspection remain distinct operations even when performed within one machine.
Jones highlights post-processing automation: “The beauty of hybrid manufacturing is that often the post-processing can be fully automated. For metal parts, this routinely reduces the total cost of AM part production by 25-30% or more.”
The 25–30% saving is the manufacturer’s estimate for the cases discussed, not an established average for all parts.
Weber Additive describes a combination of pellet extrusion and five-axis milling. Its suitability depends on component size, compatible materials and the surfaces requiring finishing.
Metal systems can combine certain alloys, for example by cladding, where compatibility is established. Polymer systems can use pellets based on injection-moulding formulations or composites suited to extrusion. Bonding between materials and final properties require verification. Kolb describes the collaboration between Weber and Reichenbacher Hamuel: “consider the synergy effects of the know-how in the field of mechanical engineering (machine construction) and extrusion technology of the two companies Reichenbacher Hamuel GmbH and Weber Additive. These support the emergence of a variety of options for machine configurations and of the production of a wide range of component sizes.”
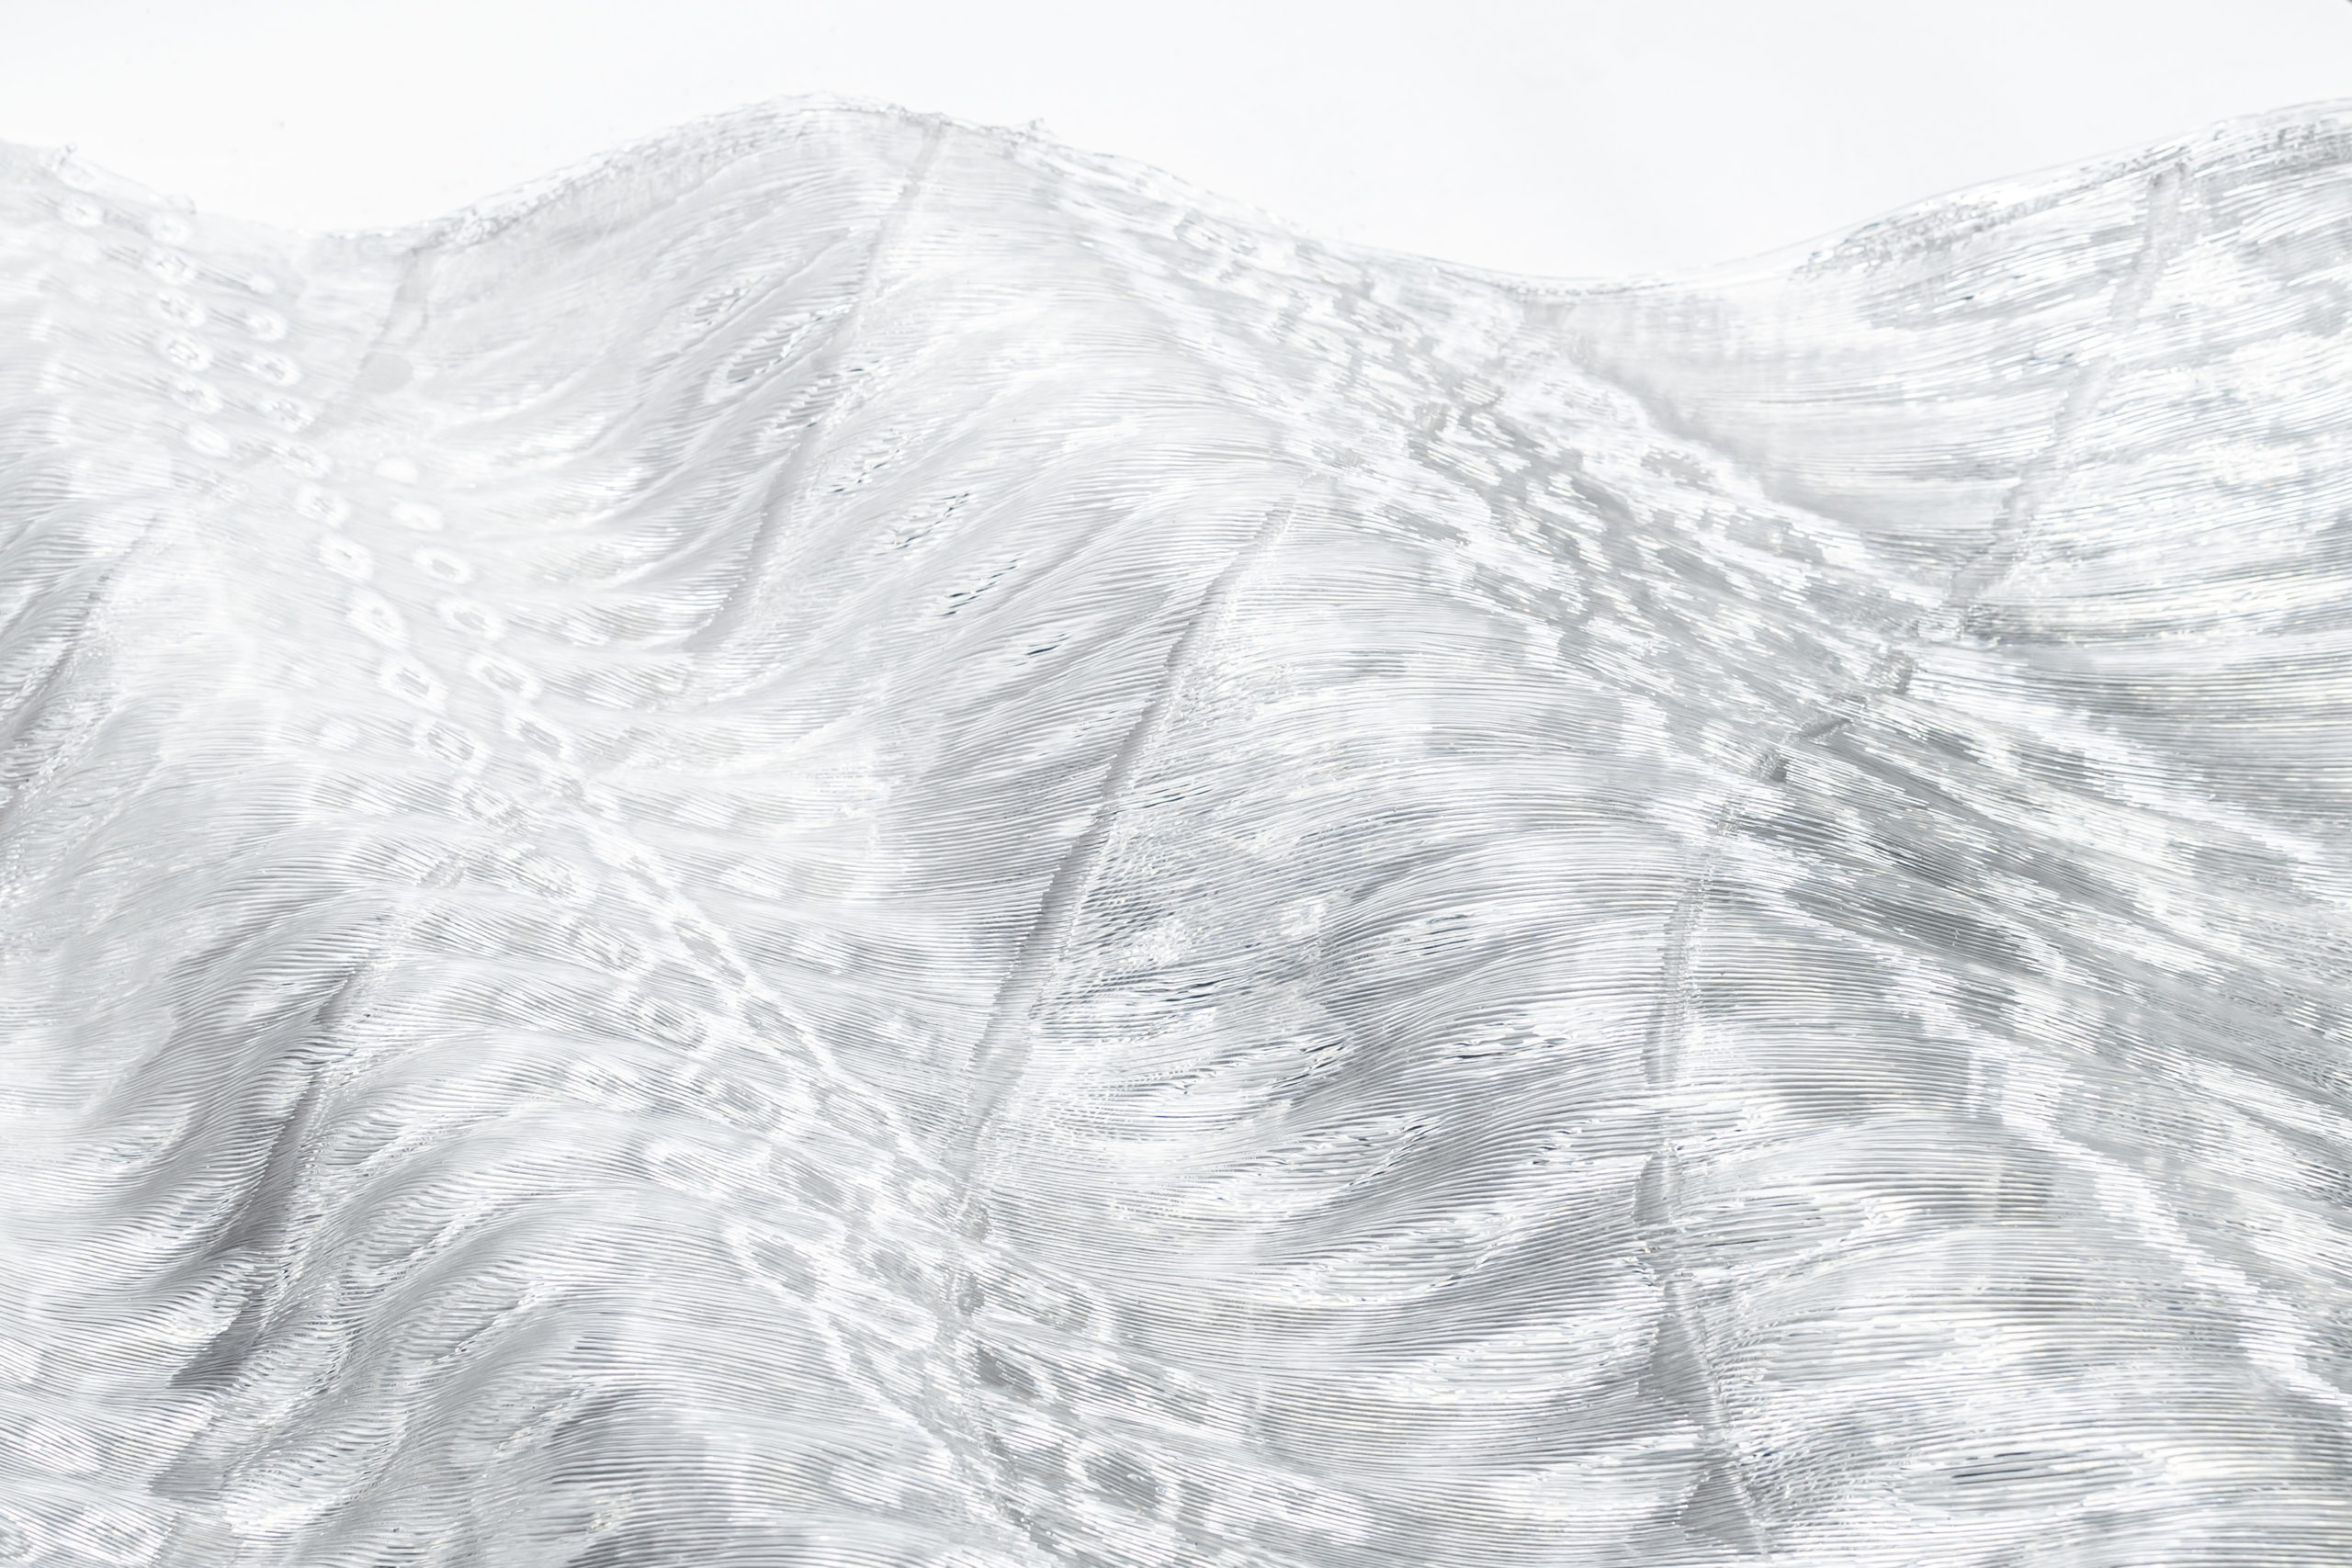
Kolb describes the intended benefits of this combination, particularly for large parts:
“We can extremely reduce the time to print large parts by printing fast with high material output and consequently with rough tolerances with high layer thicknesses. To achieve better geometric tolerances and a high-quality surface finish, the milling process is necessary to be carried out on the cooled down part. Therefore, applications for large parts will be much more economical in contrast to only additive technologies, where the build time would be extremely high. The thermally induced geometrical deformation gets worse with bigger parts. Whereas only AM processes will suffer from high deviations from the original geometry, the milling process solves this issue in a very straightforward way. Additionally, the automated removal of support structures can be also directly implemented in the milling process and saves valuable time for the part manufacturer”, Kolb continues.
Milling can correct accessible surfaces within the available stock allowance. It does not necessarily restore bulk material properties or, by itself, eliminate all residual stress.
A machined finish alone therefore does not establish equivalence with a component cut from a polymer billet. Kolb adds: “If these properties are not fulfilling the technical requirements, appropriate further post processing steps can be carried out. In some cases, the removal of support structures, a brim can take place first after the part was taken off from the build plate”, Kolb adds.
Applications & Costs
Examples discussed include aerospace, automotive, repair, moulds and dies. A medical application additionally requires device-specific validation; combining printing and machining does not establish this on its own.
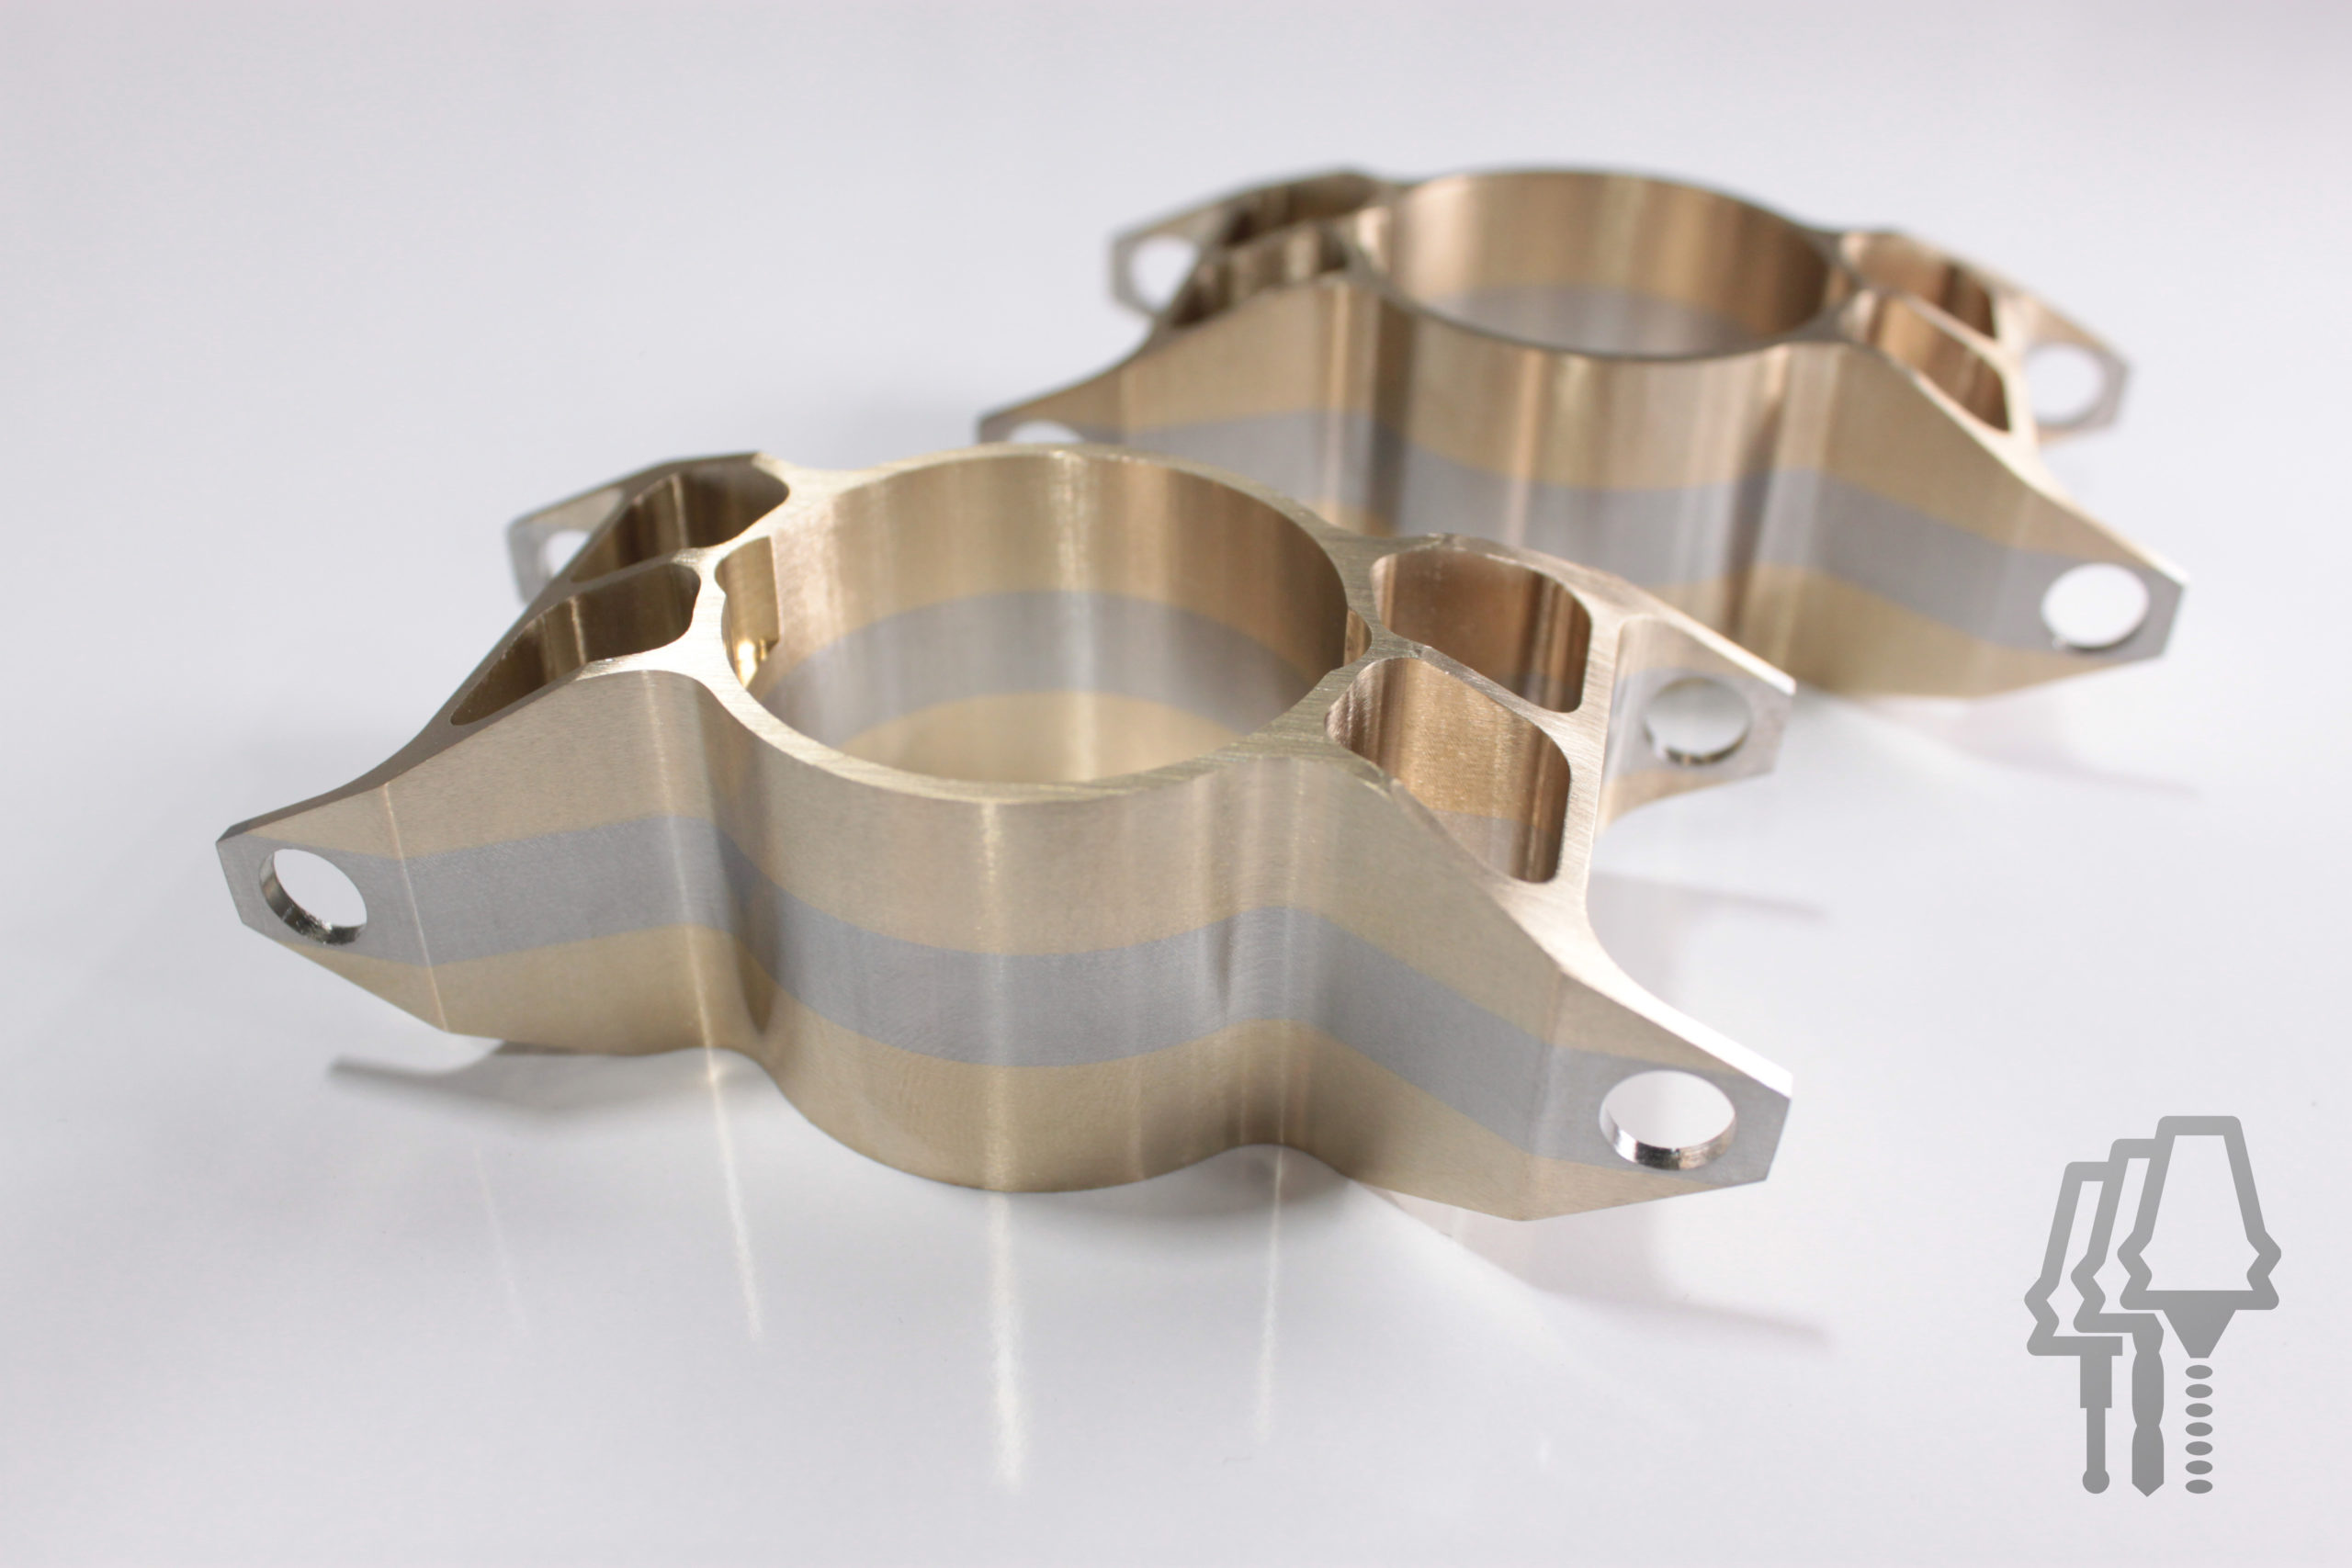
Compared to additive manufacturing technologies, three benefits we would keep from Hybrid Manufacturing Technologies’ CEO are:
“Hybrid machines bring three compelling capabilities. First, in-process finishing can create smooth surfaces on parts. This encourages faster deposition rates since the stair-step effect can quickly and easily be removed using machining. Second, in-process inspection enables assurance that the part produced is good inside and out before it leaves the machine. Lastly, interchangeable AMBIT™ brand heads mean that the most optimized tool or head can be used for each feature. This is a practical step that optimizes feedstock usage and cycle times.”
These benefits still need demonstrating for each application, including defect detectability and compliance with inspection requirements.
One documented example is the closed pump impeller described in Sulzer’s 2017 annual report.
Operators often opt for casting technologies to produce closed pump impellers.
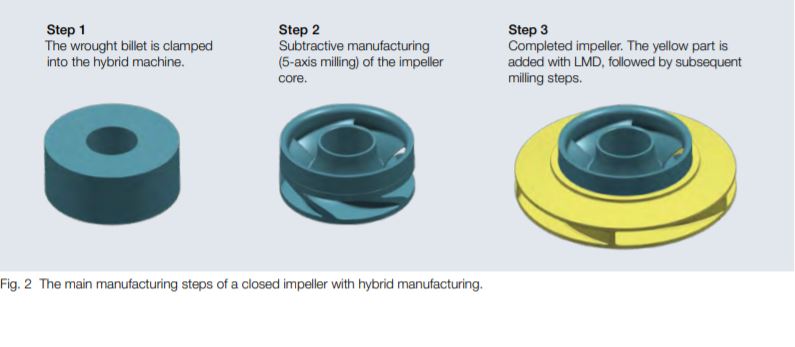
In Sulzer’s example, blade geometry restricts tool access to the internal surfaces of a closed impeller. The strategy machines a core from forged stock, then alternates deposition and milling to retain access to surfaces before the impeller is closed.
The team at Sulzer therefore used a hybrid manufacturing process that combines a laser metal deposition and a 5-axis milling. “With a hybrid process, the amount of additive build-up can be limited. This helps to keep costs of the process reasonable. Additive build-ups quite often need support structures – but with hybrid manufacturing, these structures are often not necessary due to the variable build direction. Thanks to the final 5-axis milling, the material surface quality complies with the accepted industry standards. Because of the high geometrical precision, these hybrid-manufactured parts require less post-processing efforts”, the company explains.
Investment needs to include equipment, any retrofit, safeguards, software, training and qualification. Adding AM to an existing machine may avoid some purchases without always costing less than separate equipment. Comparisons should cover total cost and planned volumes.
Companies that do not see the necessity to acquire a system, can always turn to service bureaus:
“Our in-house service bureau (hybridam.com) lets people use this technology without needing to invest in their own equipment. Next, AM can be added to their existing CNC and robotic equipment. This reduces implementation costs and allows for easy operator training and adoption. Also, hybrid machines generally reduce the amount of capital equipment needed to do AM by as much as 45%. This decisively contributes to the lowest total cost for each kilogram (or pound) of printed and finished material” Jones concludes. At Hans Weber Maschinenfabrik GmbH, leasing or solutions such as instalment purchase can be envisioned when it comes to acquisition. The company is open to alternative financial solutions to support investment decisions and give customers the possibility to explore how relevant and efficient their solution is during a trial use phase.
Jones’s 45% saving remains a commercial estimate whose scope is not detailed here. Service and financing options reflect the offers discussed in the 2021 interviews.
Advantages and areas for improvement of hybrid manufacturing platforms
The table summarises potential benefits to assess and their main limitations.
| Criterion | Opportunity | Condition or limitation |
|---|---|---|
| Accuracy and surface | Machine accessible surfaces after deposition | Allow stock and verify tolerances |
| Supports and access | Reduce some supports through process strategy | Workholding, tool access and any remaining supports still need planning |
| Materials | Combine selected materials and functions | Compatibility, interfaces and properties require qualification |
| Finishing and inspection | Integrate some operations within the machine | External treatment or inspection may still be necessary |
| Productivity and cost | Combine operations and reduce transfers | Compare total cost, throughput and volumes |
This dossier has first been published in the March/April issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.