


Feature published in the July/August 2022 issue of 3D ADEPT Mag and posted online in December 2022. Interviewee roles, prices and capabilities discussed reflect that period.
Casting and metal 3D printing can produce complex geometries, with different capabilities and constraints. Surface finish and internal cavities alone cannot determine the choice: mechanical properties, productivity, cost and qualification must also be compared. This feature chiefly examines their complementarity when 3D printing produces molds, cores or patterns.
Cast parts are used in many industrial products, vehicles and buildings. Combining AM with their manufacture can open new possibilities, but gains depend on the application and the complete production chain.
It is therefore useful to distinguish direct metal AM from additively manufacturing elements that will subsequently be used in a foundry.
Casting introduces molten metal into a mold cavity and allows it to solidify. The part can be solid or contain cavities formed using cores. The process and finishing operations are selected for the alloy, geometry and part requirements.
As manufacturers are increasingly looking for solutions that could deliver the most favorable price-time-quality conditions, how can we not imagine that additive manufacturing, one of the recent manufacturing technologies, can have its part to play in a fabrication process that involves casting?
This dossier aims to explore the different roads where AM & Casting can be seen as complementary processes, as opposed to the ones where they can be seen as competitive processes. To do so, this exclusive feature will discuss:
- The various casting processes that exist while laying emphasis on the ones that are a great match for AM;
- The software & materials standpoints for hybrid manufacturing approaches that involve AM & Casting;
- The various expectations in terms of productivity and costs that may arouse.
Types of casting processes
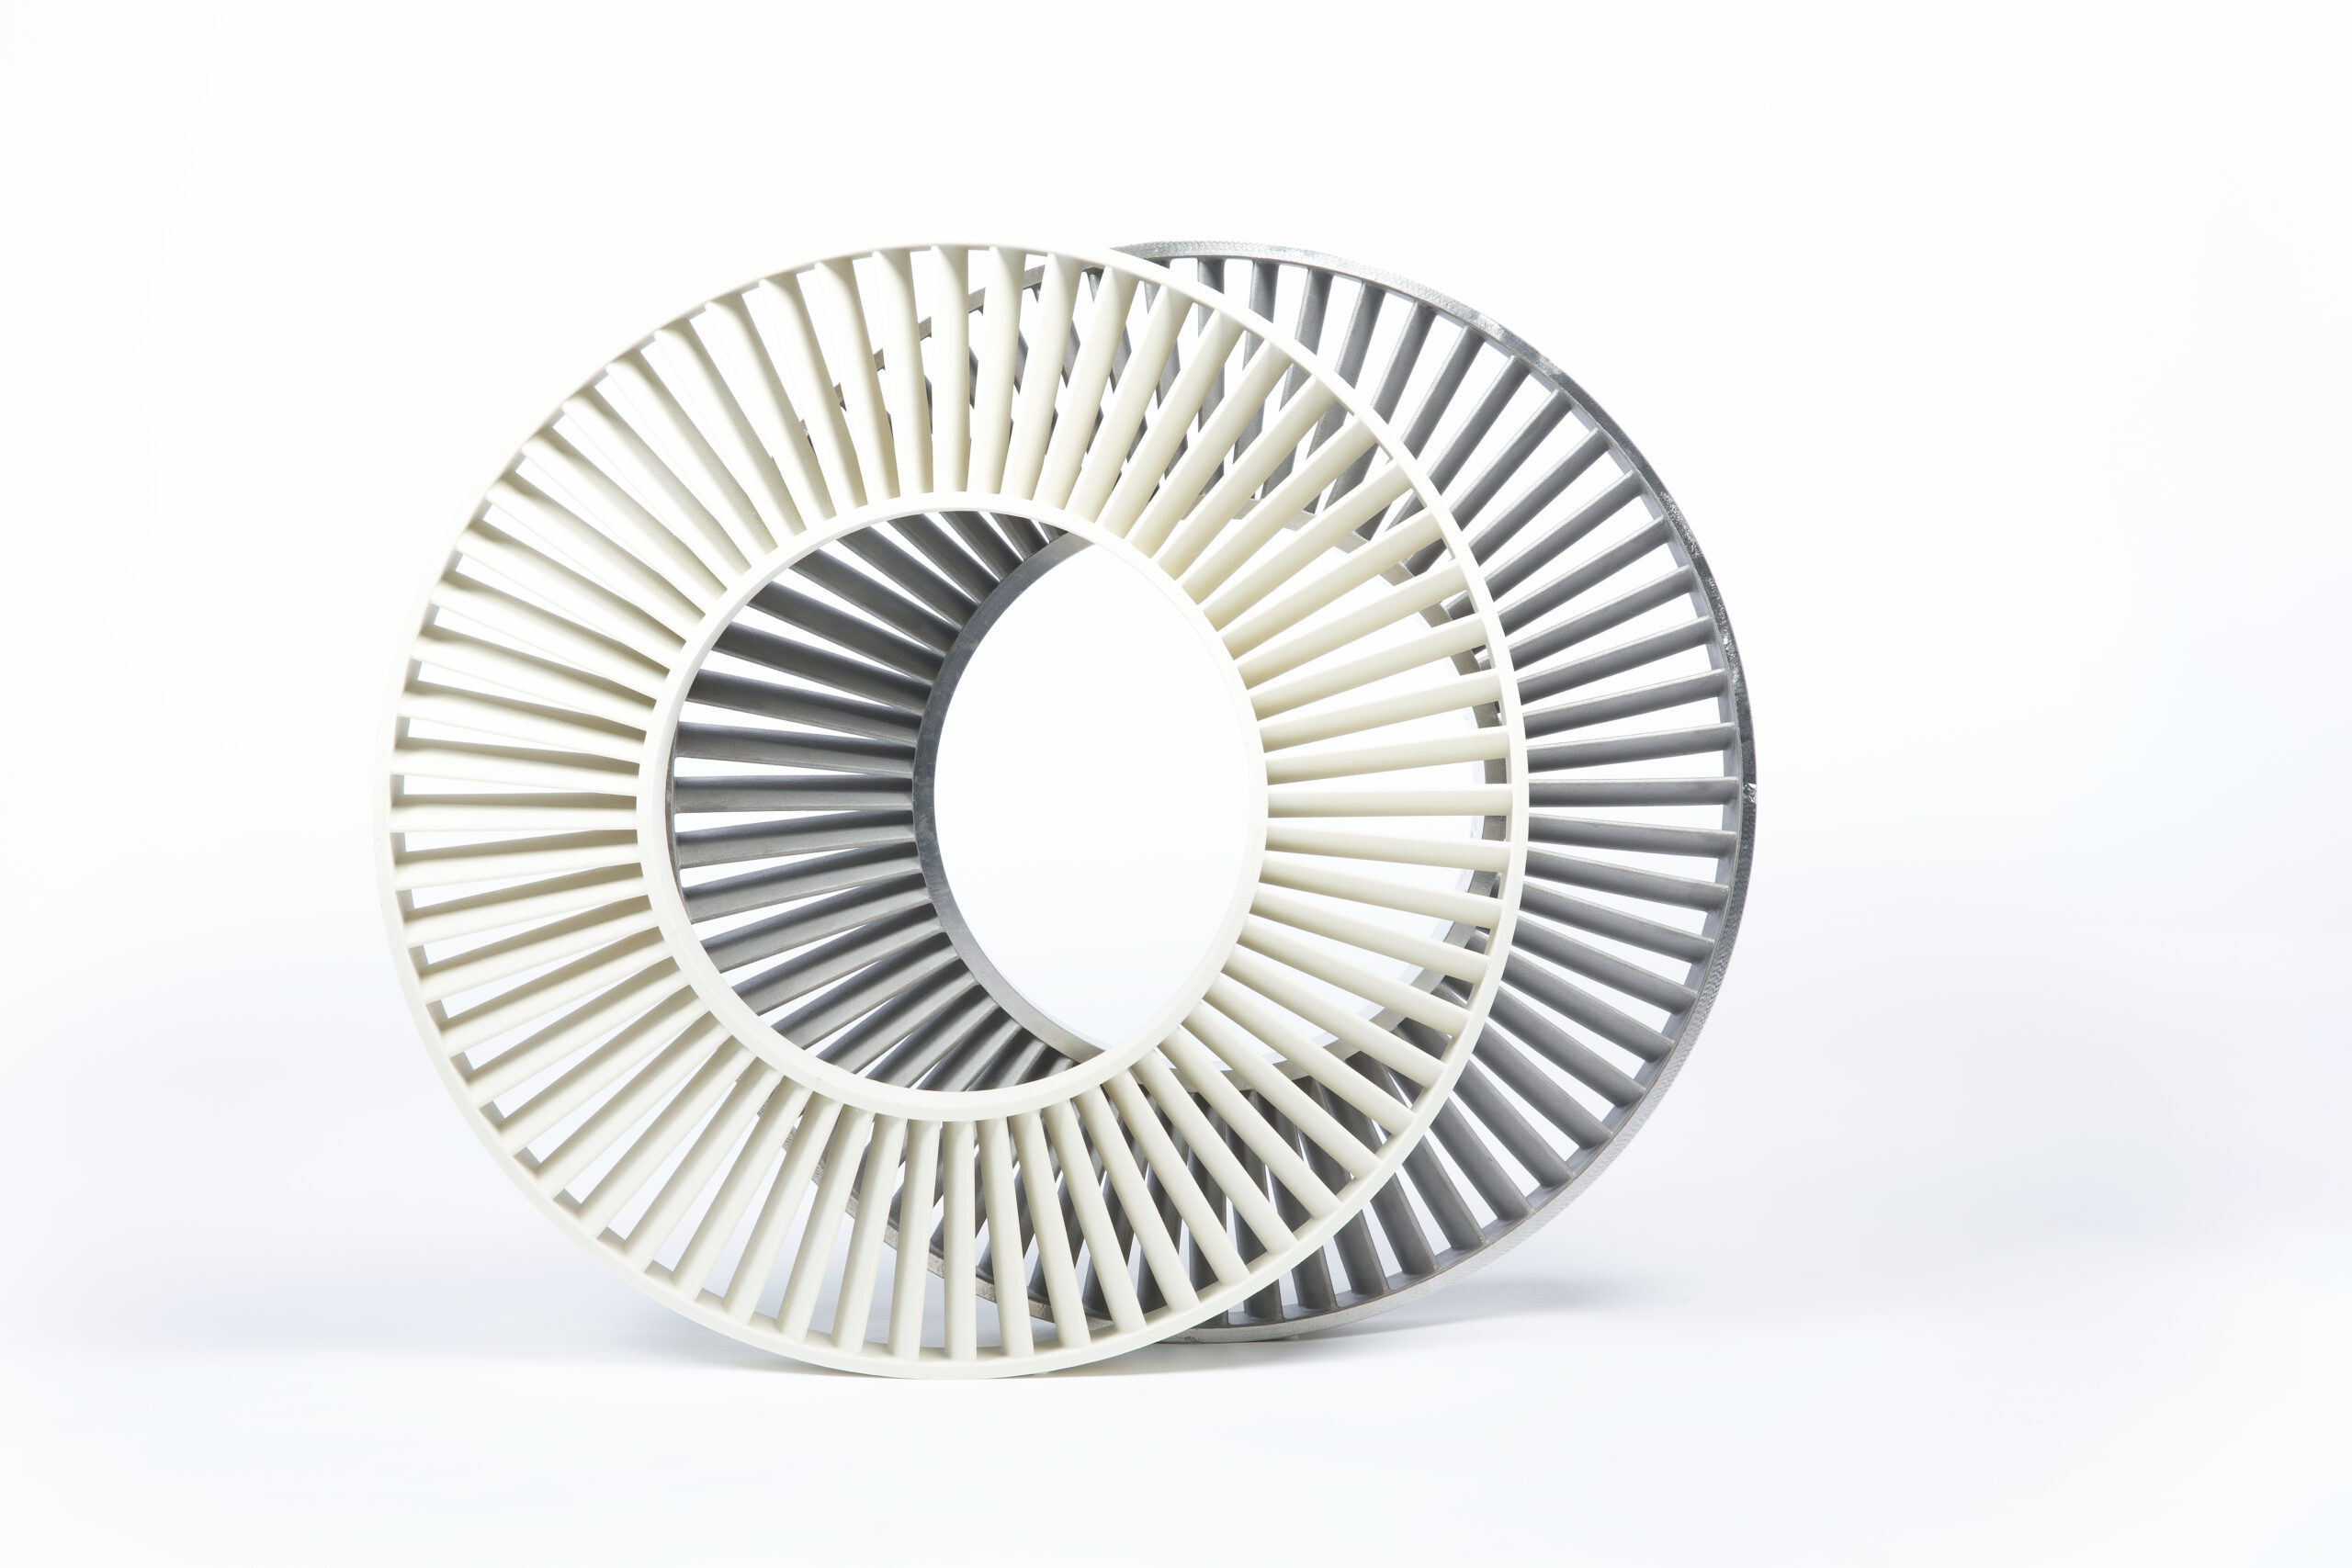
Three processes are considered here: sand casting, investment casting and pressure die casting. Other families exist; no fixed count describes every classification.
“the main casting processes that are being combined with AM are sand and investment casting. Both casting processes can be addressed with Binder Jetting. Either to print sand molds and cores directly and without the need for tools, or by printing PMMA plastic to create models for investment casting applications. By combining sand or investment casting with AM the costs and delivery time, especially for prototypes and small volumes or large single components can be reduced by up to 75 % due to the needlessness of tools”, says Christian Traeger, Director for Sales & Marketing at voxeljet in the 2022 interview.
The “up to 75%” figure is a supplier estimate for particular cases, not a guaranteed saving for every part.
In sand casting, molten metal is poured into a sand mold. The method can process steels, cast irons and various nonferrous alloys, subject to compatible molding materials and casting conditions.
| Potential advantages | Points to control |
|---|---|
| Potentially economical tooling for short runs. | Cost depends on geometry, molding process and finishing. |
| Large parts and cored cavities are possible. | Plan shrinkage, tolerances, mold strength and handling. |
| Broad range of ferrous and nonferrous alloys. | Define surface finish and machining allowances. |
Investment casting uses an expendable pattern, traditionally wax, surrounded by a refractory ceramic shell. After the pattern is removed and the shell prepared, metal is poured, solidified and released by removing the shell. Finishing, heat treatment and inspection follow as required.
| Potential advantages | Points to control |
|---|---|
| Detailed shapes, thin walls and good surface finish are possible. | Validate wall thickness and tolerances with the foundry; there is no universal threshold. |
| Several alloys and automation options. | Account for pattern, shell and inspection costs. |
| Printed patterns can avoid pattern-injection tooling. | Control size limits, pattern removal and shell strength. |
These editorial summaries draw in part on advantages and limitations presented by Suraj Kathale of HCL Technologies.
AM can also produce die-casting tooling or inserts. In pressure die casting, molten metal is injected into a reusable metal die and solidifies under controlled conditions.
| Potential advantages | Points to control |
|---|---|
| Reusable die and fast cycles suited to series production. | Tooling investment and lead time. |
| Near-net shapes can reduce machining. | Trimming, machining and inspection may still be needed. |
| Optimized cooling is possible in some printed tooling. | Size depends on press capacity, clamping force and die; large parts are not categorically excluded. |
Printed conformal cooling channels can improve heat management in a die, with potential effects on cycle time, rejects and tooling life. These gains need to be measured for the chosen design and process.
Which AM processes can be combined with casting?
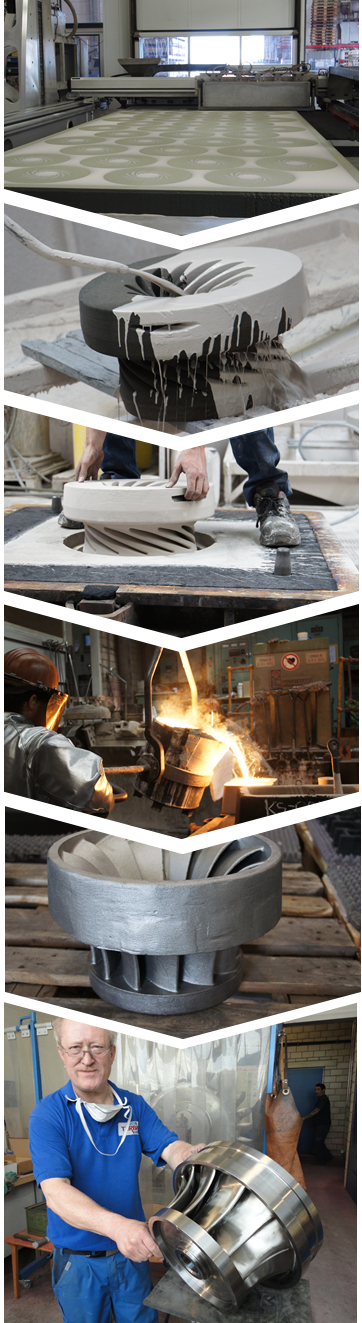
Sometimes, exploring routes where AM and casting are complementary, comes down to finding a faster (and somewhat affordable) way to create the mold before completing the manufacturing process. As you know, in this case, AM is often used to create the sand molds and cores that are thereafter used to fabricate parts by casting.
Binder jetting is an important route for printing sand molds and cores. A printhead selectively deposits binder into sand layers; bound regions form the foundry element. In 2022, voxeljet and ExOne were among the suppliers cited for this application. Binders can be organic or inorganic; machine, sand and curing conditions must be compatible.
For investment casting, stereolithography (SLA) can produce resin patterns. It does not directly manufacture the metal part: the pattern is removed from the shell before pouring. A suitable resin, a design permitting removal and a validated burnout cycle are required. 3D Systems describes this approach through its QuickCast patterns.
Filament extrusion (FFF/FDM) can also make certain expendable patterns. Its suitability depends on surface finish, materials and removal without damaging the shell; it is not invariably cheaper.
That being said, other items that are worth considering are the materials and software standpoints as well as the mechanical properties of the parts achieved.
The software standpoint
Very little credit is often given to the design software, yet it can play a crucial part in ensuring the success of the part. Every single manufacturing process starts with a design, and as always, operators will look to deliver the maximum performance of the part by making the most of the manufacturing process.
Needless to say that Sand Casting (3D printed Mold) and Investment Casting (3D printed pattern) have different manufacturing constraints, therefore imply many differences at the design level. As seen with some traditional AM processes, Martin Solina, Vice President, Inspire Manufacturing Solutions, Altair recommends foundries to ask themselves some basic questions before going to production: “Can I cast this shape?” This is key to have sound parts without defects and to minimize rejections. What will be the production cost? How does it compare with a traditional method? What are the benefits?”
Nevertheless, at the very beginning of the design stage, when AM and casting are explored in a hybrid manufacturing approach, one of the concerns that may arouse might be the right way to achieve the optimal geometry of the part. For Martin Solina, “this shouldn’t be a concern as this is a great advantage that can be obtained using a hybrid process.” “Hybrid casting has benefits from both worlds: additive manufacturing gives flexibility to design lightweight and optimal designs, while casting provides proven manufacturing method with good material properties. [This means that] by using 3D printing and casting, we are maximizing the design freedom while increasing performance and reducing weight of the parts”, he explains.
Furthermore, if in a solely traditional casting process, it’s possible to have a software tool that enables the investigation of the cast parameters and eliminates the possible failures of the casting process during the design phase, it makes sense to expect such dual function in this hybrid manufacturing approach. To make the business case for AM & Casting compelling, design software should allow users to do more than simply provide CAD tools. For Altair’s representative, this means that design engineers should – for example – be able to optimize the “performance of the part while defining manufacturing rules to ensure the manufacturability of the part for the particular manufacturing process. Design software must provide the freedom to the user to redefine the part and provide quick answers to questions regarding performance under different load cases, manufacturability, defect prediction or validation of the manufacturing process. Based on this, the role of a design software today has changed from a basic CAD tool to a simulation-driven design tool that provides feedback and information to improve and optimize the design of the part and processes integrating topology optimization and different type of analysis and simulation tools like structural, thermal or fluid analysis. Manufacturing simulation and many other tools help designers make decisions based on information, like:
- Create and Modify Designs with Ease: Create, modify and defeature solid models quickly, use PolyNURBS to create free-form smooth geometry and study multiple assembly configurations.
- Optimize for Manufacturability: Arrive at the ideal design direction extremely early in the process: topology optimization is based on physics and observes manufacturing process constraints.
- Simulate at the Speed of Design: Experience an interactive engineering design environment for rapid design exploration and product creation, without the need to invest in new computer hardware.”
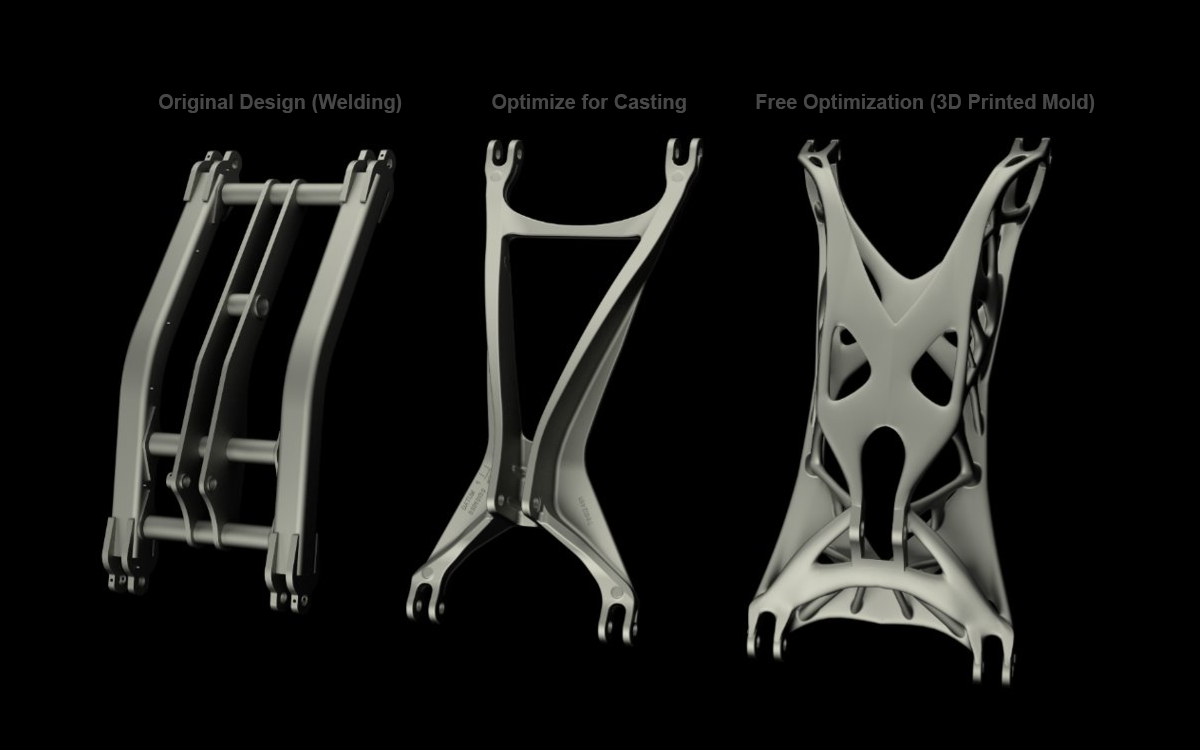
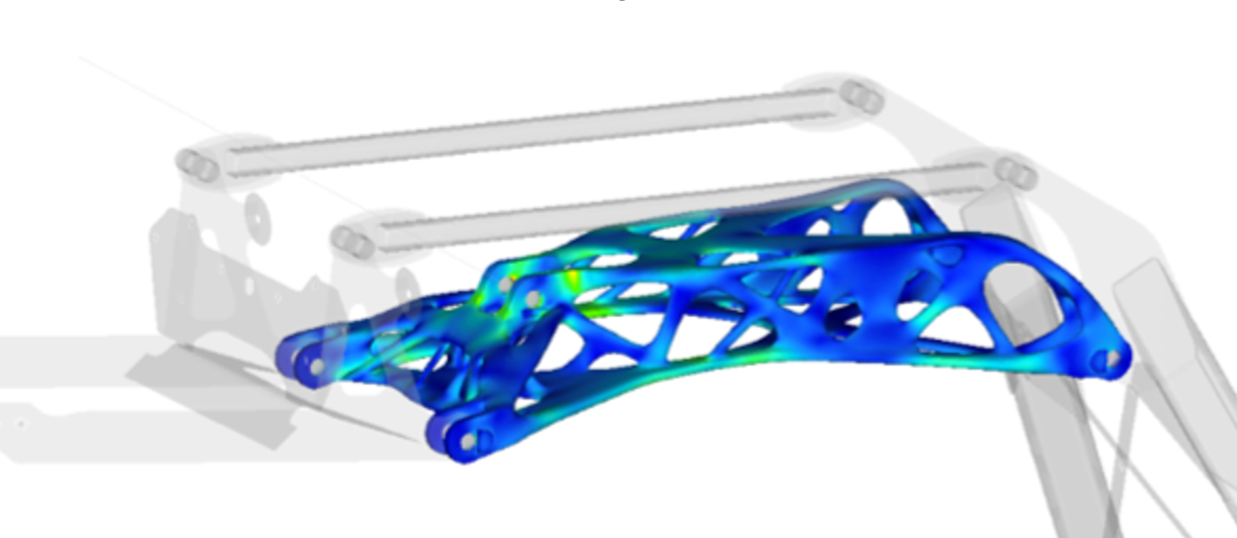
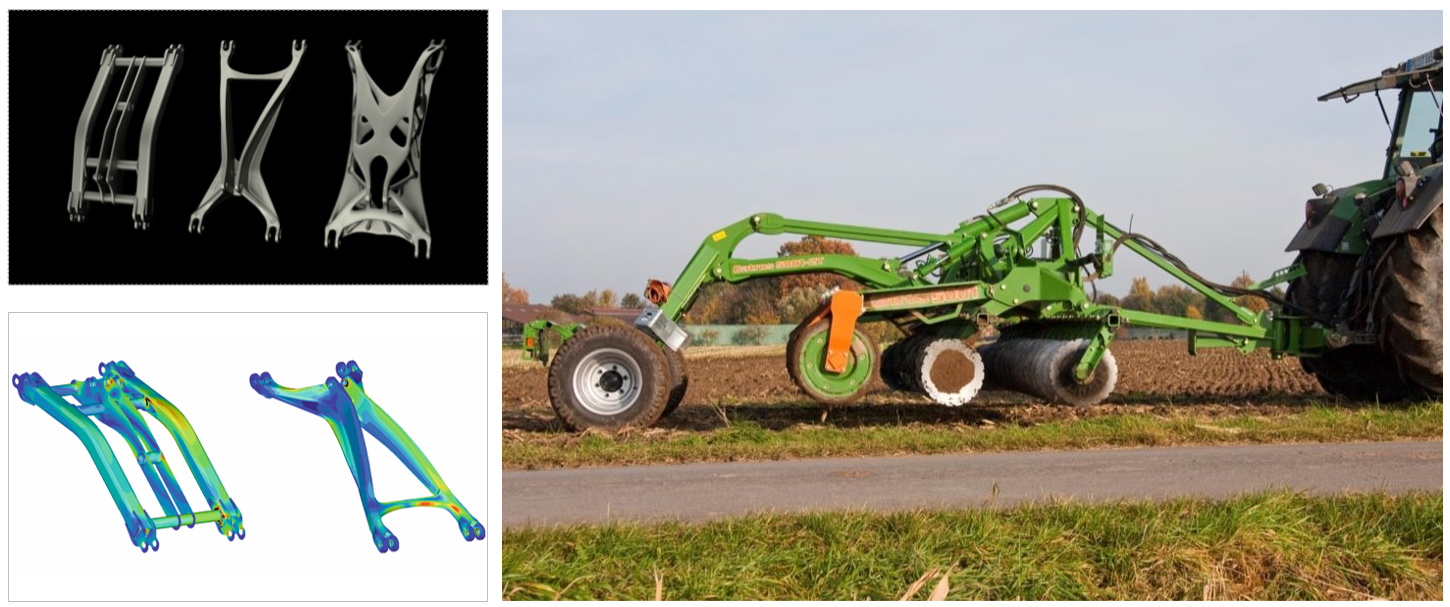
In the Amazone example shared by Altair, the original rocker arm was a 245 kg welded assembly with 16.5 m of weld seams. The presentation cited in this feature reports an 8% mass reduction for the cast version discussed, with fewer stiffness variations. That figure concerns this design stage and should not be confused with other project iterations.
At a practical level, one should not forget that “designing” is very much dependent on the “human element”, which means that two engineers designing the same part will not always obtain the exact same “rendering” not to mention that, the complexity of the part – if not well handled, may lead to defects, low part performance, excessive weight, excessive time to market and even expensive operations of redesign and having to revisit process conditions.
“To meet today’s requirements of performance, weight reduction and especially costs, it is necessary to take advantage of new processes and design components for these processes require the combination of new software features, including:
- Parametric Geometry: provides the ability to perform geometry modifications and changes based on analysis and simulation.
- Structural and Motion or dynamic analysis to understand the working conditions of the analyzed part.
- Topology Optimization to improve the part performance and reduce weight based on the working conditions.
- Manufacturing simulation to predict the Mold filling and thermal analysis for different types of casting process such as investment casting or gravity sand casting considering the different types of AM molds too.
And most importantly, all these features should be linked to one another in a seamless way to be transparent for the user”, Martin Solina emphasizes.
The materials standpoint
One of the main concerns often raised by materials is the one of mechanical properties. Do we have satisfying results when assessing the tensile strength, hardness, surface roughness, and microstructure of the part?
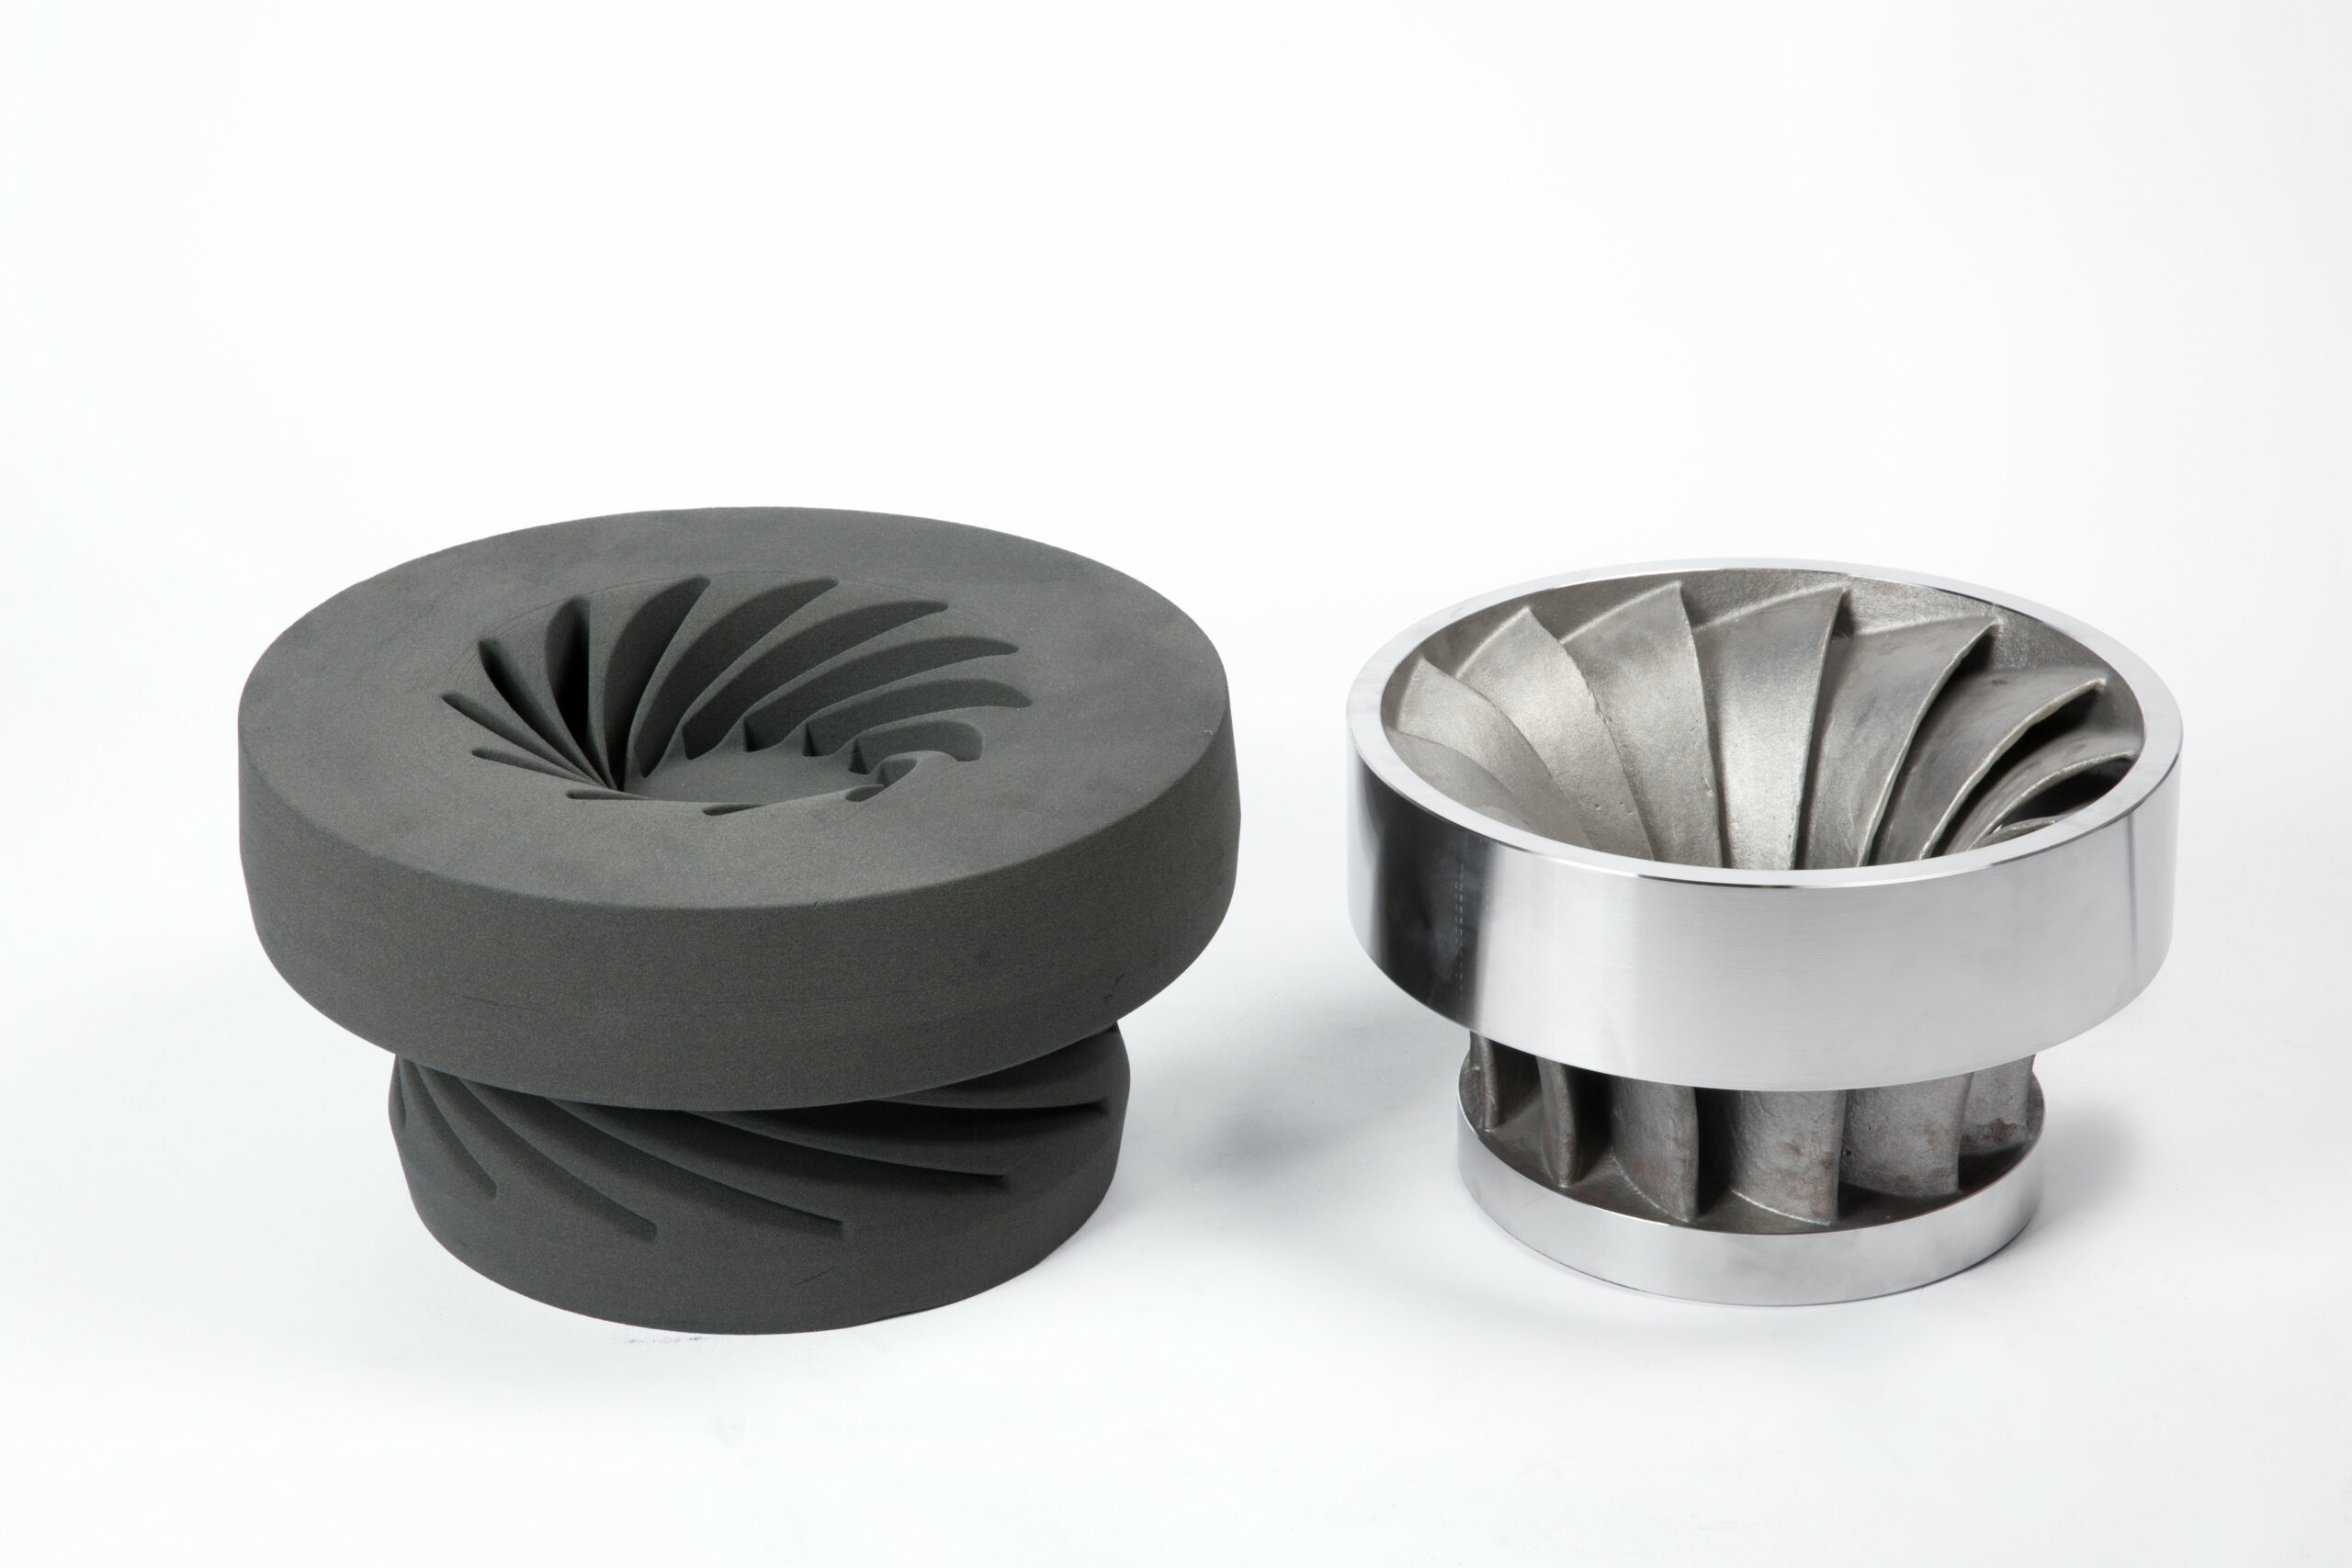
In a traditional sand casting process for instance, three materials/binding systems are often utilized and it’s easy to think that they can be directly transferred to AM production methods.
“When looking at sand casting the answer is a classic: it depends”, Christian Traeger brings a nuance. “Most of the materials used have been used in metal casting for centuries: sand and furanic resin. Other binder types, such as phenolic or inorganic binders are also capable with AM. Depending on the binder used, the system setup need to be adapted as well. Furanic direct binding requires the sand to be mixed with a promoter that reacts with the binder and glues the sand particles together. Both phenolic and inorganic binder work with unmixed sand. By irradiating the building platforms with temperature, the resins react and glue the sand particles together. Since unprinted sand is unmixed, it makes it a lot easier to recycle and reuse. In investment casting we see a great acceptance and growing market interest in the PMMA material set. The rapid production and flawless integration into existing process chains are the main benefits. The only way to optimize this material set further, is to further increase the surface quality.”
These explanations describe the supplier’s systems. Furan and phenolic binders are organic resins; inorganic binders are not. The reference to “centuries” should not be applied to modern furan resins. Sand reuse also depends on its condition and the process.
Sand particle size and flow, binder viscosity and curing conditions affect printing. Compatibility with a conventional foundry formulation is therefore not automatic. An experimental study of printed furan sands examines mechanical properties and thermal deformation.
We then asked voxeljet’s Christian Traeger if parts produced with AM and a casting method possess the same mechanical properties as parts produced via casting as the only production method. He said they do.
“Reason for that is that, the casting process itself remains the exact same as it was before. By using typical foundry materials such as silica and special sands and complementary furanic, phenolic or inorganic binders, we only change the way molds, models and cores are built. Within the foundry, 3D printed parts can be integrated into existing process chains. Since the mechanical properties of castings depend mainly on the properties of the alloy used, additive manufacturing has no influence on these. Of course, there are some details that need to be kept in mind when designing to mold or the model such as cleaning of the printed parts. Also, the surface quality depends on the material used and can show differences compared to the materials used in conventional manufacturing, but when all these details are accounted for, and the metal is casted, the parts show the exact same mechanical properties as conventional manufactured cast parts.”
This equivalence still requires verification for the mold–alloy combination and cycle: cooling, gas evolution, porosity and surface condition can affect part properties. Changing how the mold is made does not remove qualification requirements.
What about productivity and costs?
Compare the complete chain: preparation, mold or pattern production, casting, cooling, finishing and inspection. AM can remove some tooling steps without necessarily shortening total lead time in every case.
In the illustrative example discussed in this 2022 feature, the production time is calculated as from when the parts’ producer receives the 3D CAD geometry from a customer. The casting process of a part with an average complexity might require two additional core boxes for pattern equipment. The operators would need 3 days to redesign a 3D model with all necessary draft angles and prepare the 3D pattern geometries. Two additional weeks are allowed to move from 3D geometries to a ready pattern: this includes CNC machining for negatives, CNC machining for core boxes and copying epoxy models and making the gating system. Not to mention that extra time is necessary for the main production and forming.
The additive route discussed here allowed a few hours of preparation, up to three days of printing and several hours of finishing. These are illustrative times for preparing foundry elements, distinct from the lead time to an inspected metal part.
A mold can contain several cavities, and a print bed several items. Parts per cycle depend on size, production layout and available capacity: there is no general rule contrasting ten cast parts with a single printed part.
“AM works with digital CAD data and does not require any form of tooling. Conventional tooling can take up to 12 weeks to be produced and only then the casting process for this specific part can begin. Binder Jetting can create molds and models within hours or days, reducing the time needed to create e.g. a prototype by up to 75%. Binder Jetting is a quite easily scalable process technology, meaning that build volumes and productivity can be increased, making the technology not only suitable for prototype production but also for small to medium large batch sizes”, Christian Traeger comments.
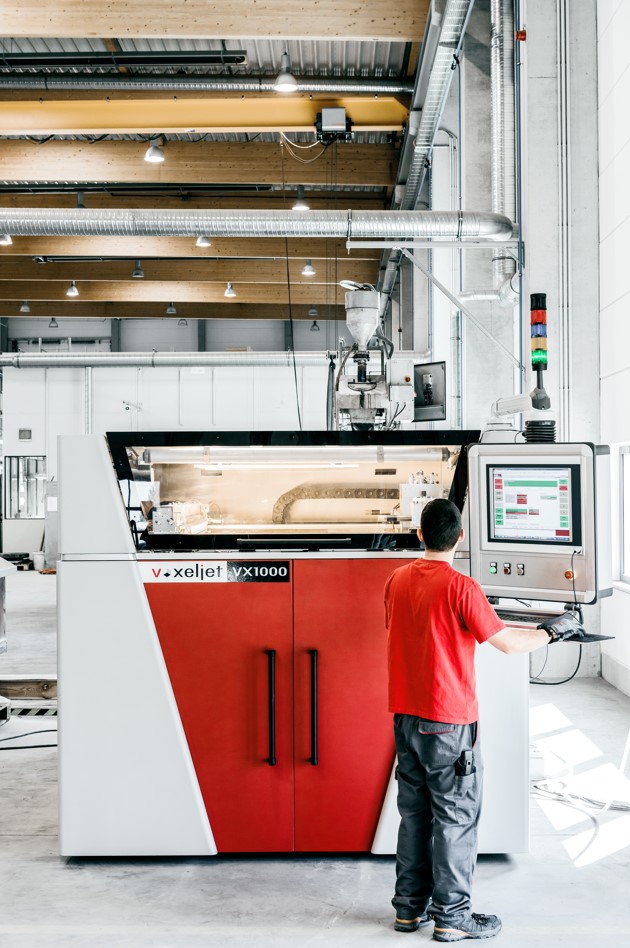
However, when asked if the combination of AM & casting is the most cost-effective way to produce parts – when looking at other metal AM processes, he said:
“This depends on the material and the required batch size. For prototypes and small series, AM supported casting process is much more cost-effective than e.g., Direct Metal Laser Sintering. Reason for that are the printing materials as well as the casting alloys. 1 kg of aluminum costs around 6,50 EUR when casting. Special Steel alloys can cost up to 38 EUR. The same materials but for AM technologies can cost something between 78-133 EUR per kilogram.
When it comes to batch sizes, binder jetting molds, cores and models is cost effective for prototypes and small to medium batch sizes. Binder Jetting is on one of the most productive AM technologies around and can also be scaled quite easily in order to meet larger batch size needs. Also, it offers build volumes beyond the capabilities of any existing metal printers. While metal binder jetting is of course a technology on the rise, the build volumes still lack the volume that sand printers offer. To say Binder Jetting supported metal casting is the most cost-effective way to produce metal parts is a strong statement and a little far-fetched. In certain scenarios, as described above, the cost effectiveness of Binder Jetting is very hard to beat, but those scenarios have to be identified and carefully evaluated to find the best fit and solution.”
The €6.50, €38 and €78–133 per kilogram figures are examples quoted by the interviewee in 2022. They are not current prices or a full-cost comparison, which also includes material yield, equipment, labor and qualification.
Concluding thoughts
AM can simplify complex pattern, mold and core production, particularly where conventional tooling dominates cost and lead time. Suitable production volume requires a case-specific assessment: it is neither universally limited to five parts nor economical for every series.
Furthermore, as mentioned by voxeljet, despite the high cost of AM equipment, one notes that machine manufacturers continue to invest time and resources to develop a portfolio that can easily enable industries to scale their production for larger batch size needs. Lastly, beyond these investments, it’s crucial to keep in mind that when looking at this hybrid manufacturing approach that involves AM & Casting, sometimes, the right design software and utilization of this software can make a whole difference, not only in casting the “un-castable”, but also in delivering the ideal benefits in terms of time, costs and performance.
This exclusive dossier was first published in the July/August 2022 edition of 3D ADEPT Mag. All resources and contributions can be found in page 13.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.