


Feature first published in the January–February 2021 issue of 3D ADEPT MAG, then online in August 2021. Reported specifications and commercial prospects reflect interviews from that period, rather than a current product catalogue.
Volumetric 3D printing explores another way to solidify resin: acting within a volume rather than successively depositing or exposing layers. This 2021 feature connects research with early offerings from Readily3D and xolo.
Volumetric printing covers a family of approaches. Tomographic reconstruction and xolography use different mechanisms; the terms are not interchangeable.
Manufacturing a solid object also differs from creating a volumetric display or hologram. The Southern Methodist University patent discussed here describes optical-switch devices, including printing configurations; its title is not another definition of all volumetric AM.
Three publications mark the approaches discussed here: CAL in 2019, high-resolution tomographic printing in 2020 and xolography in December 2020.
First, let’s find out what volumetric 3D printing is
Tomographic printing projects light patterns into rotating resin; the accumulated dose solidifies selected regions. Xolography uses two wavelengths and photosensitive molecules to localise polymerisation where beams intersect. Oxygen effects depend on the chemistry; they do not alone define the distinction from SLA or DLP.
Three teams and their approaches
Brett E. Kelly, Indrasen Bhattacharya, Hossein Heidari, Maxim Shusteff, Christopher M. Spadaccini and Hayden K. Taylor, from the University of California, Berkeley and Lawrence Livermore National Laboratory, describe their CAL method:
“We developed a method, computed axial lithography (CAL), that allowed us to synthesize arbitrary geometries volumetrically through photopolymerization. The CAL approach has several advantages over conventional layer-based printing methods. Our method may be used to circumvent support structures, as it can print into high-viscosity fluids or even solids. Printing 3D structures around preexisting solid components is also possible with our approach. CAL is scalable to larger print volumes and is several orders of magnitude faster, under a wider range of conditions, than layer-by-layer methods”.
Damien Loterie, Paul Delrot and Christophe Moser, EPFL researchers and founders of Readily3D, describe the start of their project:
“During our Ph.D. studies, we discussed on multiple occasions new concepts for photopolymerization that involved shaping light beams in 3D to create the desired object. Our project really took off when, in 2017, we decided to test experimentally whether we could make a 3D object by illuminating a photosensitive resin from multiple angles, which was the basis for tomographic printing. These initial experiments were surprisingly successful, and we realized that we were onto something”.

Readily3D uses a tomographic approach: photosensitive resin receives calculated projections from multiple angles. Formulations can be adapted to the applications under study.
Founded in January 2019, xolo explains its xolography principle:
“The xolography technology can very well be described as a process in which a planar printing zone is continuously – and with high speed – moving through a photopolymer tank rather than photopolymer slowly moving from a tank into the print zone of a conventional SLA/DLP printer.”
These processes build a geometry from digital data. An absence of layerwise deposition does not mean that nothing moves: the vat, exposure zone or optics may move, depending on the configuration.
“Most 3D printing technologies rely on an additive layer-by-layer process. Volumetric printing, however, relies on a photopolymer-filled vat in which each voxel (3D analogue of a pixel) can be selectively addressed to convert it from the liquid (uncured) state to the desired hard (cured) material state”, xolo explains.
Viscosity can help hold an object during exposure. Fillers and additives can alter light transmission or scattering, however; compatibility must be checked for each formulation.
Solidification requires sufficient light dose and exposure time. It is not instantaneous, even when fabrication is very fast.
Addressing one urgent issue in manufacturing
The demonstrations report seconds-to-minutes fabrication for selected parts. Exposure times do not necessarily include preparation, projection calculation, washing or subsequent treatment.
“The most spectacular aspect of our technology is speed: because the whole volume is solidified at the same time and not layer-by-layer, objects can be printed in just a few tens of seconds. This is revolutionizing as it is unmatched by any other method at similar scale and resolution”.
This is Readily3D’s assessment in the 2021 interview, for the scale and resolution it was discussing.
Xolo could not agree more as for the startup, the V3DP technology is the basis for unprecedented speed and design freedom “as printed parts do not need to be attached to a platform anymore.”
And there are other advantages as well:
“Printing directly within the resin volume also solves additional challenges of traditional AM systems. For example, we do not require temporary supports to print hollow structures or overhangs, because the object is held in place by the resin during the relatively short print time. The lack of mechanical contact between printer and resin also means that we can print within sealed, sterile containers. Finally, we are able to print soft and deformable materials, which tend to be challenging or impossible to make on AM systems based on deposition or recoating operations”.
“Volumetric 3D printing will challenge the state-of-the-art only where customers are unhappy with existing solutions. Think of time-sensitive applications or manual removal of support structures, the staircase effect, etc. With the release of the xube, we hope to inspire creative minds for applications that were not realizable before. We want to enable products that were unimaginable before’’, the team at xolo explained to us.
These advantages concern tested materials and geometries. A research offering does not establish validation for every proposed industrial or medical application.
Volumetric 3D printing technologies and their specifications
The following examples describe the situation studied for the January–February 2021 issue. They are not a current supplier inventory.
The University of Michigan’s 2019 work concerns continuous printing through polymerisation inhibition, distinct from the two approaches above. Siemens’ US20180250890A1 application was filed on 1 March 2017 and published on 6 September 2018. The passage describing an “optical molecular switch molecule, wherein the optical molecular switch molecule has a non-fluorescent state and a fluorescent state, wherein at one wavelength of optical excitation the molecule has a first state, and at a second state the optical molecular switch molecule fluoresces at a second wavelength of excitation.” comes from the Southern Methodist University patent. These documents describe principles; they do not establish that all these technologies are equivalent or commercialised.
Disney Enterprises also appears in application US20160107380A1, published on 21 April 2016, describing printing with a photocuring liquid. The document alone does not establish a commercial offering.
The two commercial offerings examined in this feature are those of xolo and Readily3D.
The xube volumetric 3D Printer
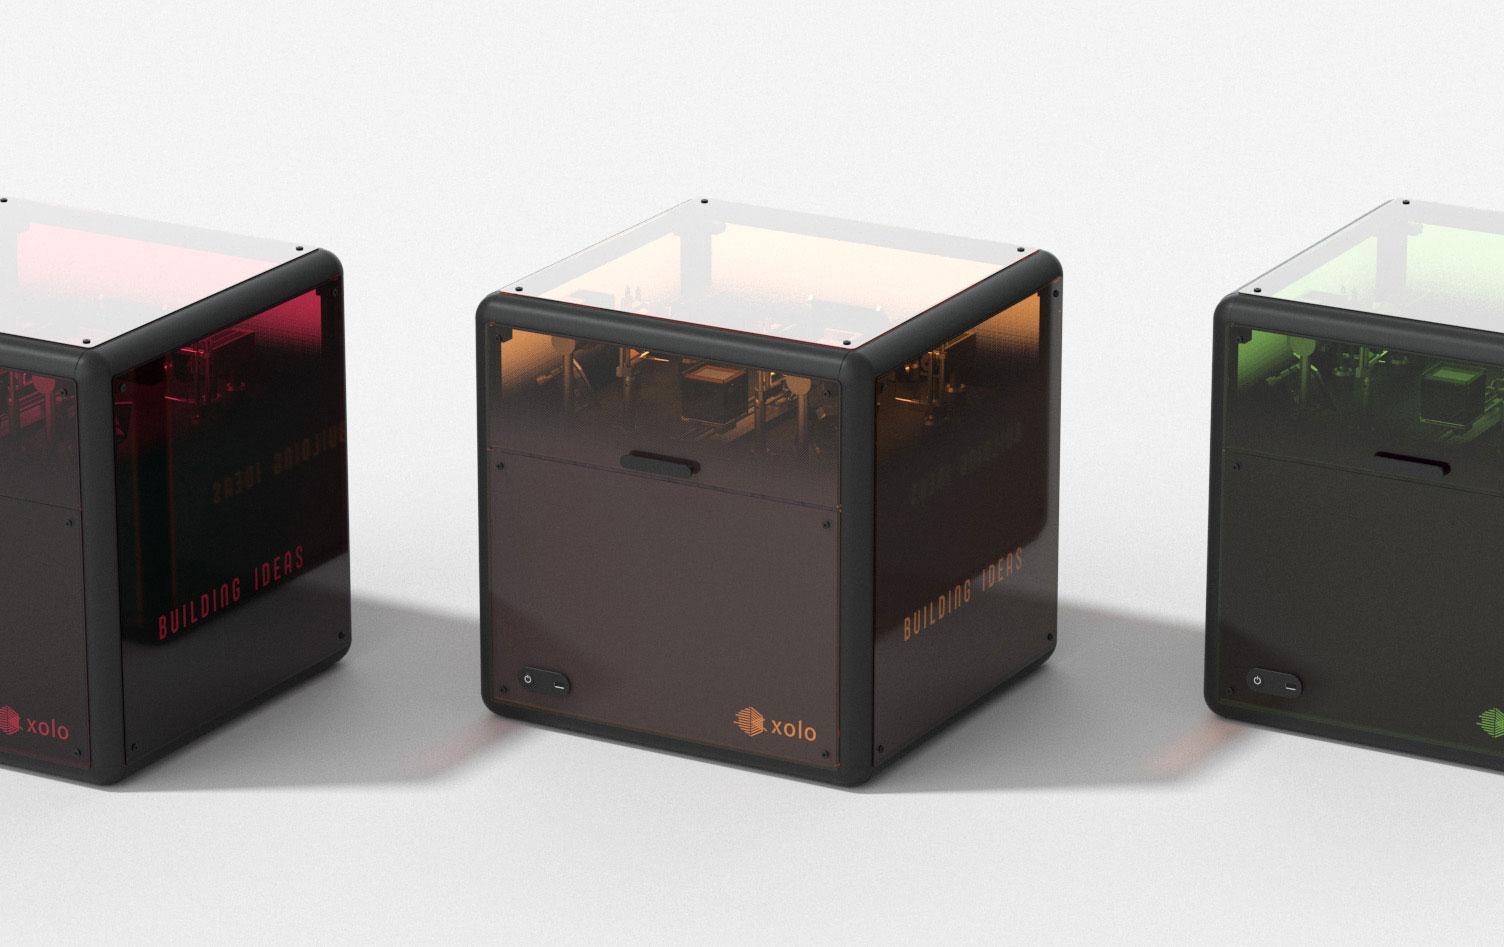
In late 2020, xolo presented xube, a xolography printer. It reported around 20 seconds for small parts and up to five minutes for larger parts under its demonstration conditions.
“The xube is specially designed for curious researchers: While standard protocols are available for printing acrylics, it is open to individualization, all printing parameters can be chosen freely and any self-made material can be employed. The customer loads the printer with a photopolymer vat with dimensions spanning from >50 mm to 10 mm along with the space coordinates. Within seconds to about a few minutes (depending on the print size), the object is solidified with high accuracy based on a standard STL input file”, xolo told 3D ADEPT Media.
The dimensions stated in this quotation are ambiguous and should not be used as purchasing specifications without manufacturer confirmation.
According to the company, once the printed part – or the “solidified object” as per the words of xolo – is removed from the vat, “residual resin is washed off and depending on the material used, final material properties can be attained by photo/thermal processing”.
At the time of the interview, xolo was addressing research organisations.
The Readily3D’s Tomolite printer
For the Tomolite version discussed in the interview, Readily3D reported an approximately 30 × 40 × 60 cm footprint and a cylindrical build volume 10 mm in diameter by 27.5 mm high. The company then reported CE marking.
Described as ultra-fast and user-friendly by its inventors, the unit can print “centimetre scale object, out of soft and hard materials, in a few tens of seconds with 40 um optical resolution.”
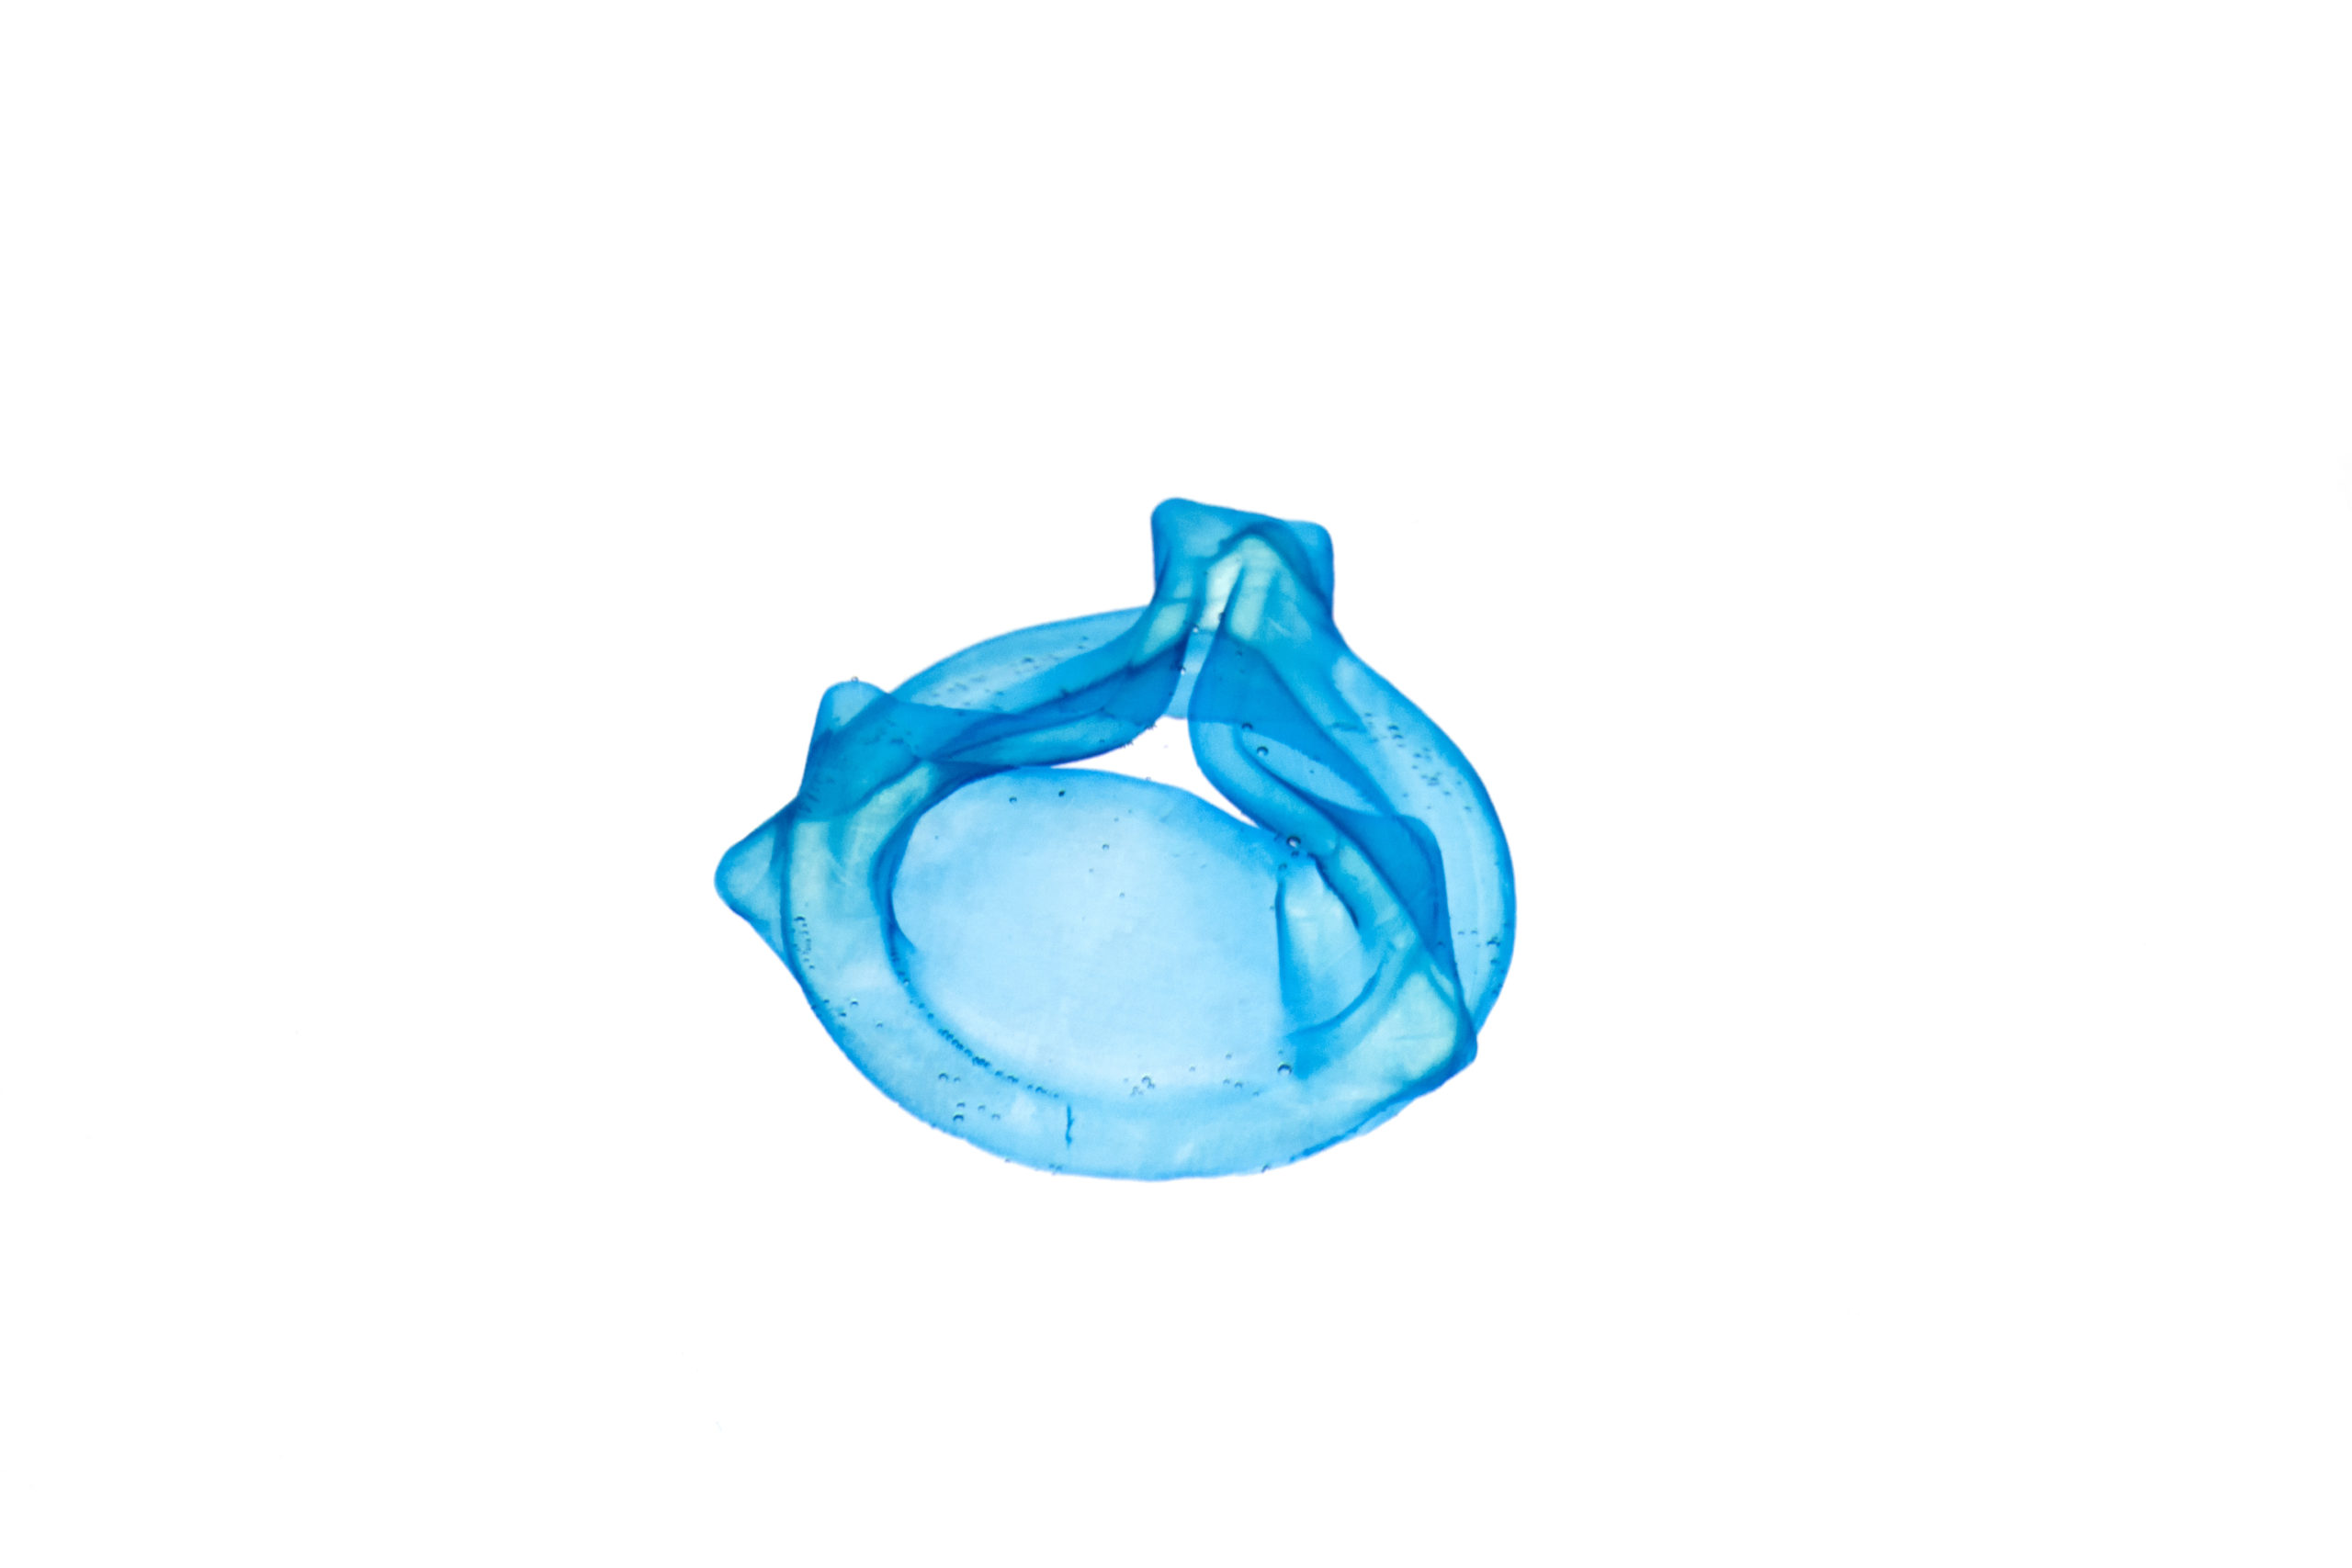
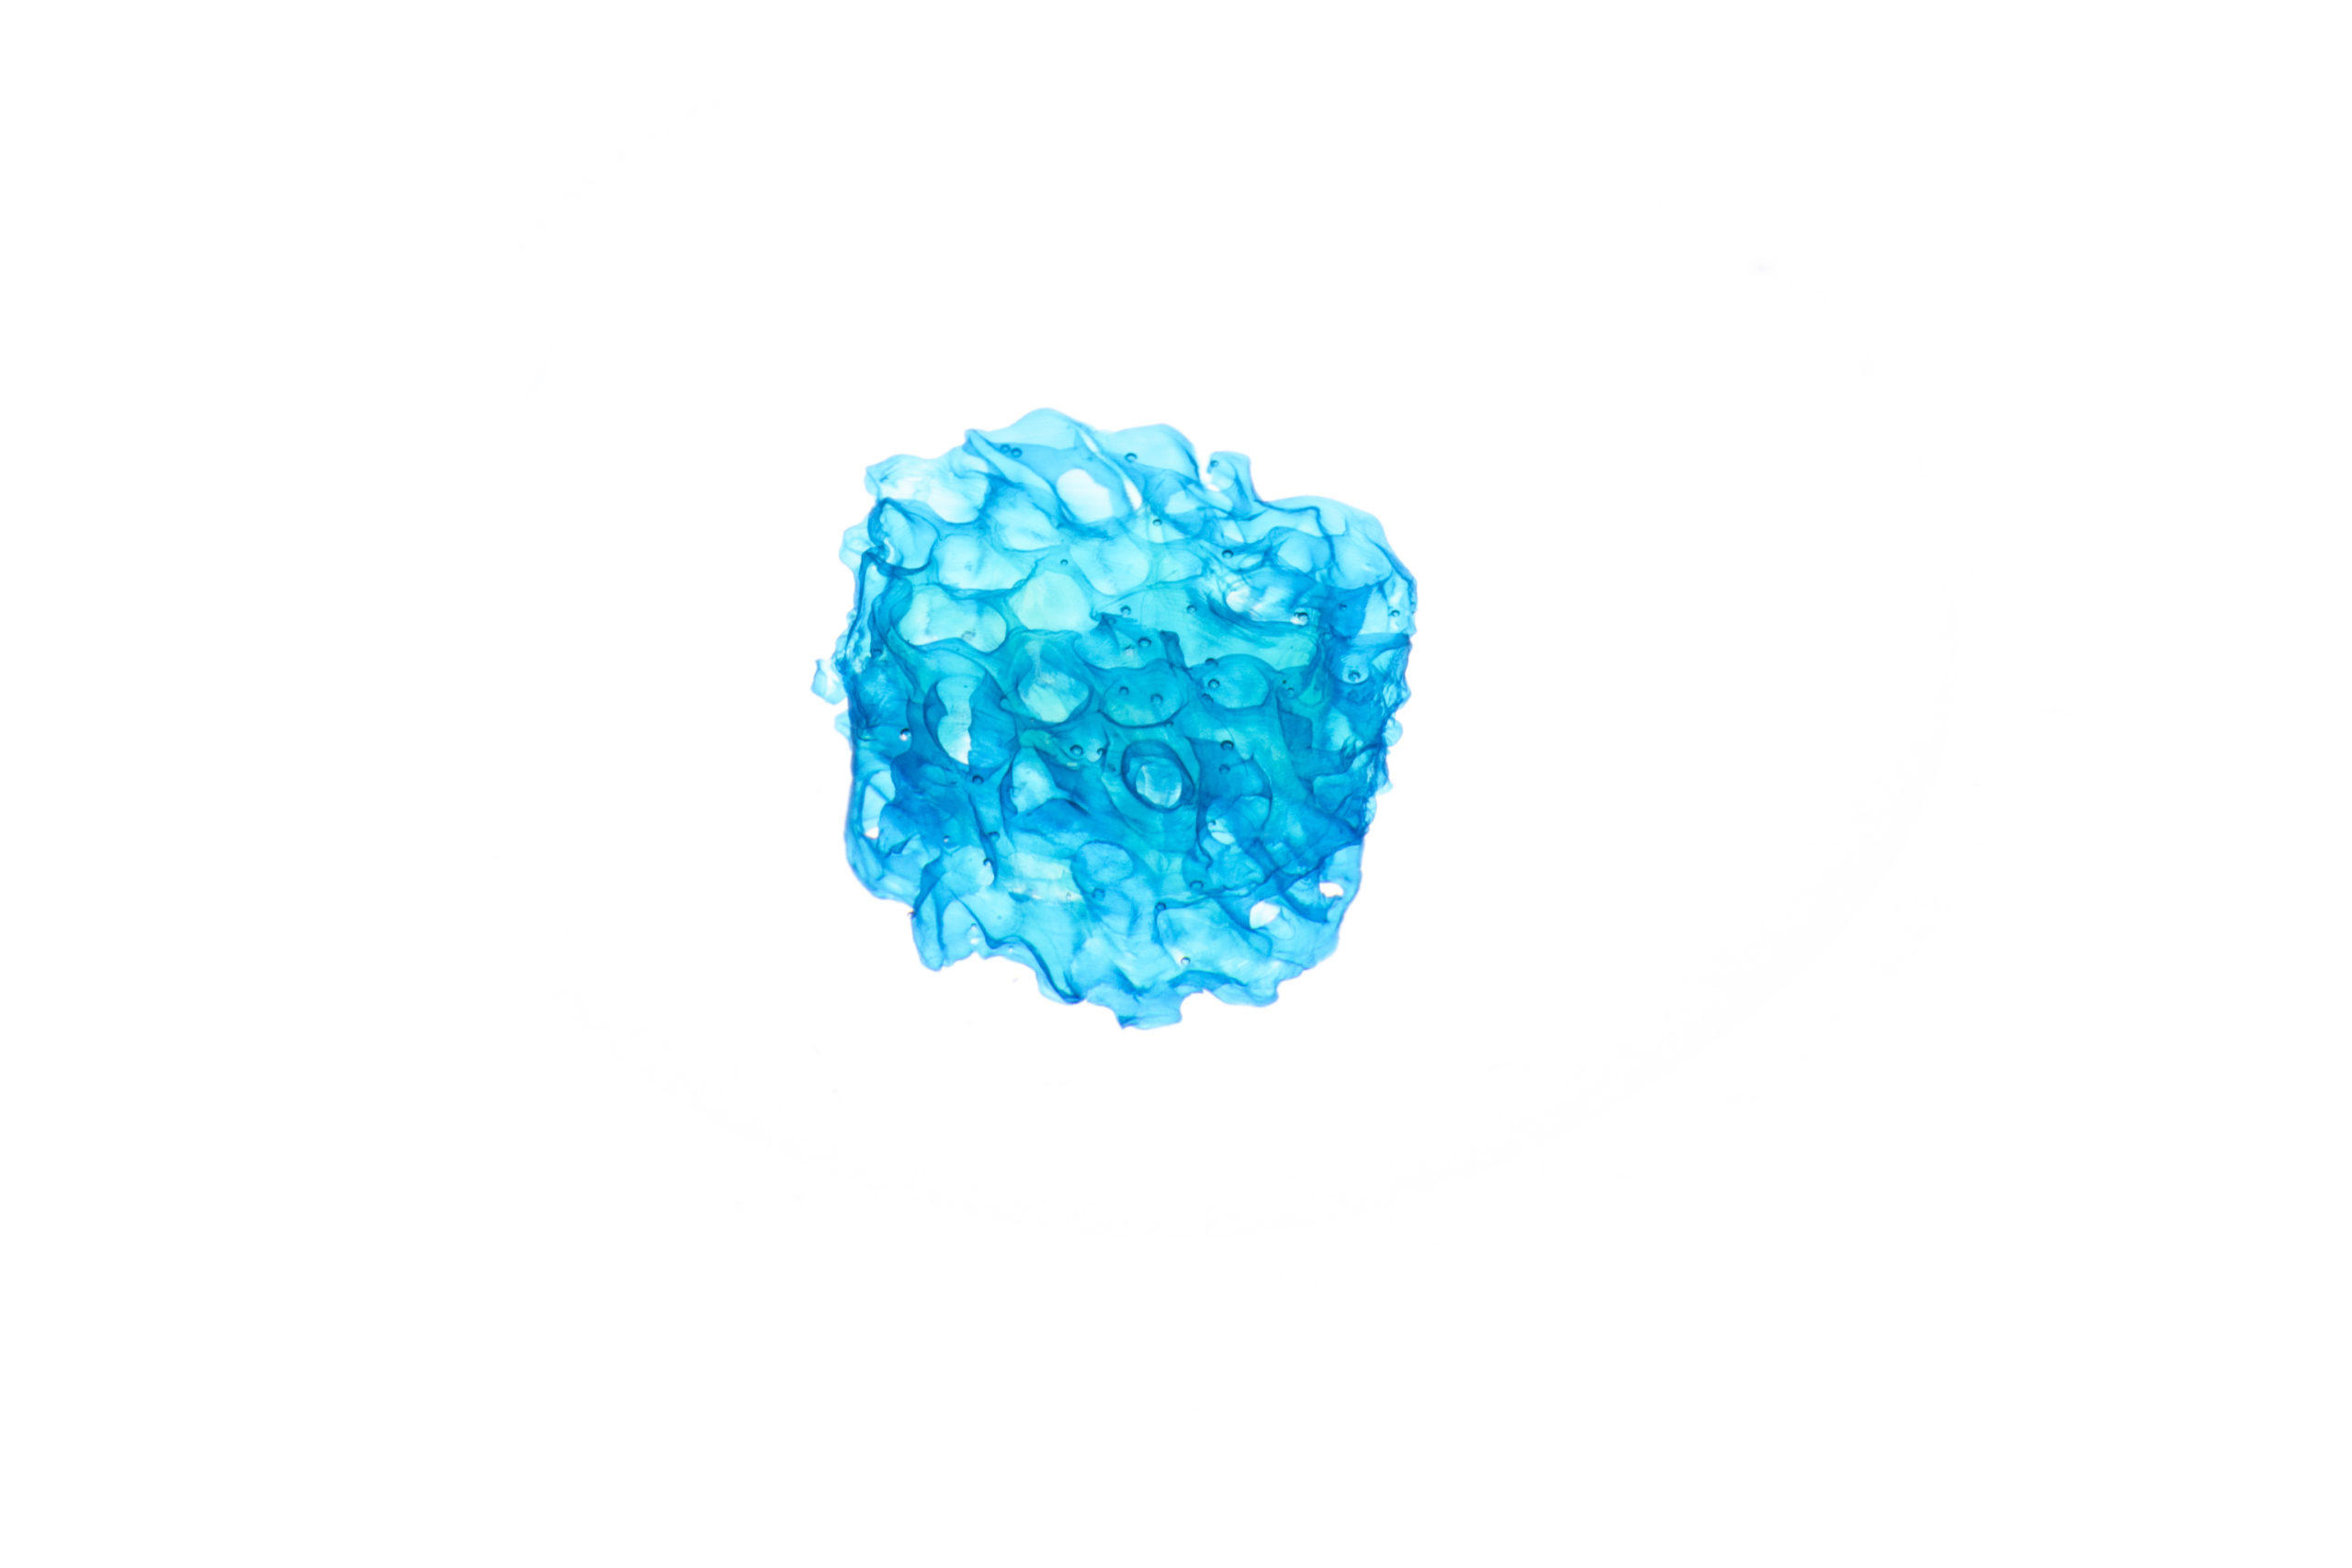
Readily3D stated that washing was sufficient after printing for the materials then presented. This should not be extrapolated to every resin or end use.
Speaking of the printing process, the company explains: “the resin is first poured into a cylindrical vial, which is then hand loaded in the printer. The STL file of the object to print is generated by a CAD program. The printer comes with the Apparite software, which allows for the loading and handling of STL files, as well as the configuration of dose settings and printing monitoring.”
To point out an application, the founders add: “our printer can shape light-sensitive bioresins into complex living constructs featuring vasculatures, pores and cavities that cannot be done with any other printers on the market with the same speed and resolution.”
Readily3D then reported offering the machine to companies and public institutions, with units installed at European research centres.
Main applications of volumetric 3D printing
The interviewees identified optics, dentistry, audiology, bioengineering, microfluidics and prototyping among the prospective fields.
Cell-laden constructs concern biofabrication; not every application listed requires cells. A laboratory demonstration does not establish clinical validation.
In this 2021 interview, Readily3D saw particular opportunities in dental and audiology customisation. This was a market assessment, not a medical-device authorisation.
These early systems opened access to new experiments. Process selection remains tied to the material, geometry, resolution and validation requirements of the application.
This exclusive feature has originally been published in the January/February issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.