

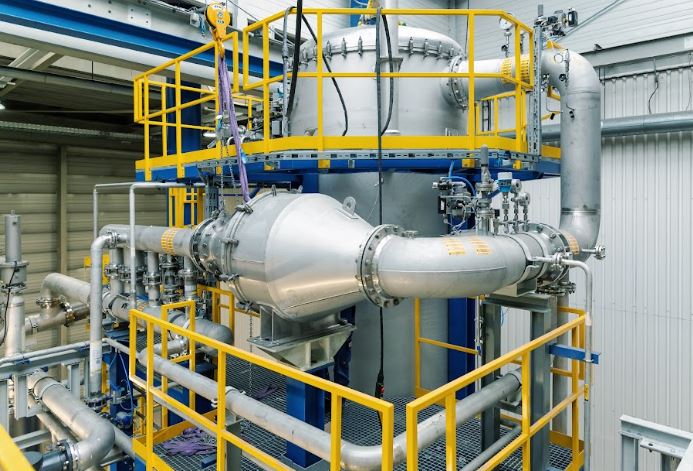
A contribution by Andoni Sanchez-Valverde Erice, identified at publication as a Sales/R&D engineer at Outokumpu. This feature appeared in the May/June 2023 issue of 3D ADEPT Mag; forecasts and the industrial launch refer to that period.
Corrosion resistance, mechanical properties and recycling opportunities motivate the use of stainless steels in additive manufacturing (AM). These qualities vary with the grade, process, heat treatment and environment, rather than guaranteeing longer life in every application. In this feature, Andoni Sanchez-Valverde Erice discusses technical considerations for spherical powder production at Outokumpu.
In its 2023 contribution, Outokumpu cited an AMPOWER forecast that stainless steel could reach 33% of the AM powder market in 2027, following titanium and nickel alloys in the ranking reported at the time. This was a projection, not an achieved share. The report’s scope and measurement basis need checking before comparison with other market figures.
Producing stainless steel powder
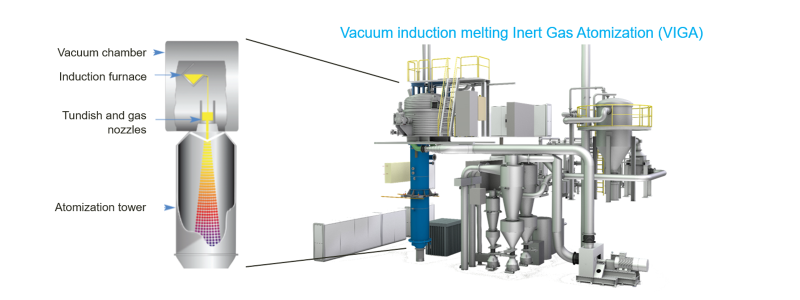
The process described here combines vacuum induction melting with gas atomization, commonly called VIGA. Outokumpu describes particles up to about 300 µm, subsequently classified by size. This is one route for stainless steel powder production, rather than the only possible method.
The details of the process equipment are shown in Figure 3.
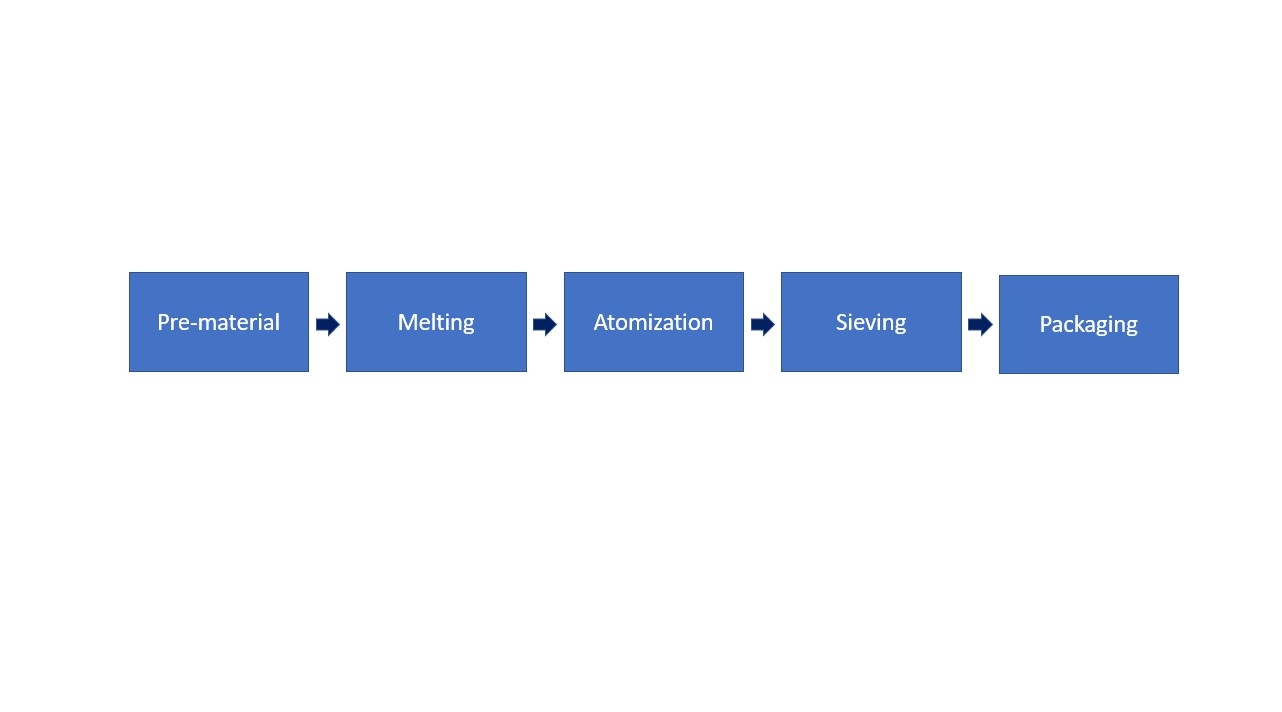
Feedstock: in the process described, scrap from flat-product processing is cut into pieces suited to the crucible, typically 25 × 25 mm and 1–4 mm thick. Its composition needs to match the intended grade.
Melting: vacuum conditions help limit oxidation and loss of alloying elements. Temperature, pressure and vacuum level are controlled. Chemical analysis indicates whether composition adjustments are required. The furnace is then backfilled with argon or nitrogen, depending on the process and alloy.
Atomization: liquid metal passes through the tundish and is broken into droplets by gas. For the equipment described, Outokumpu cites pressures up to 32 bar and gas temperatures up to 450 °C; these are not universal operating instructions. Droplets solidify, and the powder is separated from the gas and collected.
Sieving: The powder is separated into different fractions by mechanical sieving and an air classifier to target different powder metallurgy technologies. If, for example, a customer does not want to have more than 5% of their powder smaller than 20 µm, then the air classifier can be used to separate the smaller powders from the batch.
Why is the choice of atomization gas important?
Choosing between molecular nitrogen (N₂) and argon (Ar) affects several aspects of the process and must also be compatible with alloy chemistry.
Price: nitrogen is generally less costly than argon in the case described. Final powder cost also depends on consumption, particle-size yield and supply conditions.
Morphology: gas properties and heat-transfer conditions influence droplet cooling. The supplier describes sphericity differences between its argon- and nitrogen-atomized powders. Results also depend on nozzle design, alloy and settings, rather than gas heat capacity alone.
Fine-particle fraction: Outokumpu reports more fines with nitrogen under the compared conditions. This observation is not simply explained by “smaller atoms”. Atomization involves gas flow, liquid breakup, nozzle geometry and operating conditions, as discussed in NIST research.
Composition and properties: the gas can influence powder nitrogen content and, depending on the alloy, the behaviour of the resulting part. Effects on strength, corrosion and machinability need measurement for the grade and treatment rather than a general promise of improvement.
Limiting satellites on powder particles
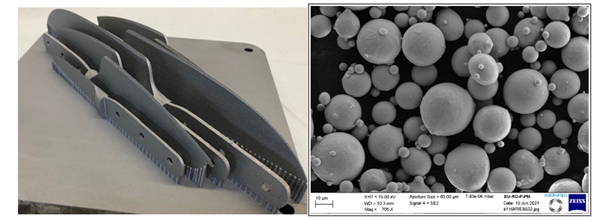
A crucial feature in powder production is the anti-satellite system. Satellites are small droplets that adhere to the larger spherical particles – see Figure 4. To avoid this, argon or nitrogen is recirculated into the atomization tower. This gas pushes the very small droplets to the bottom and the likelihood of satellites in the solidifying particles is reduced.
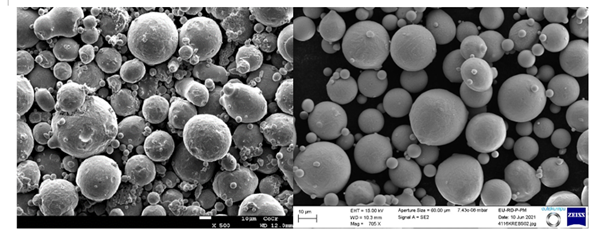
The presence of satellites rather than smooth, round powder will impact the quality of AM components in two ways:
Spreadability: The spreadability of the powder is decreased if it features satellites rather than perfectly spherical powders. This is important for the part of the process where the next layer of powder is spread onto the existing powder layer by the re-coater.
Density and particle packing: satellites can change powder flow, apparent density and packing. These characteristics affect bed uniformity, but final porosity also depends on manufacturing parameters. One powder measurement alone does not establish part conformity.
Matching particle size to the process
The supplier gives the following ranges as examples, not universal specifications. Machine, grade, application and distribution limits need agreement with the manufacturer. MIM and HIP are powder-metallurgy processes rather than 3D-printing processes in this list.
- Binder jetting technology (BJT): <20 µm
- Laser powder bed fusion (PBF-LB): 15 to 45 µm and 20 to 63 µm
- Electron beam powder bed fusion (PBF-EB): 20 to 150 µm
- Powder-fed directed energy deposition (DED): ranges starting around 20–45 µm and extending up to 150 µm, depending on the system.
- Metal injection molding (MIM): <20 µm
- Hot isostatic pressing (HIP): up to 300 µm in the example described.
Extending the scope of stainless steel grades
316L and 17-4PH are among the common grades cited in this 2023 overview. Other compositions broaden the options, subject to qualification for the intended process and use. Properties of a conventional grade do not automatically transfer to a printed part.
The “commodity” stainless steels grades used in AM technologies are:
316L (1.4404): a low-carbon alternative to 316. This minimizes carbide precipitation as a result of heat input, for example during welding, giving improved resistance against intergranular corrosion. 316L/1.4404 is suitable for a wide variety of applications in the automotive, chemical, petrochemical and medical industries. Typical products include flanges, valves, and medical devices.
17-4PH: a martensitic precipitation-hardening stainless steel used where strength and corrosion resistance need to be combined. Performance depends on metallurgical condition and heat treatment. The contribution cites aerospace, pulp-and-paper and nuclear uses, including pumps and mechanical components; each application has its own requirements.
Added-value special stainless steels grades include:
904L (1.4539): Special grade for high-corrosion environments. It is a high-nickel and molybdenum austenitic stainless steel with very high corrosion resistance. It was originally developed for handling sulfuric acid at ambient temperatures and is now used in a broad range of applications in the oil and gas and chemical industries. Typical parts produced from 904L are pumps, valves and flanges.
253MA (1.4835): an austenitic grade for certain high-temperature uses, with oxidation and creep resistance. The contribution cites a limit up to 1,150 °C; this is not a universal service temperature for every printed part. Load, duration, atmosphere and metallurgical condition remain decisive.
1.4116: a martensitic stainless steel capable of high hardness after suitable treatment, including for knives and some instruments. Wear and corrosion behaviour depend on material condition; no general superiority over all martensitic grades is implied.
Nickel-free austenitic powder based on modified 1.4678: Outokumpu presents it as an option to assess for certain body-contact products, including watches. Replacing 316L or a cobalt-chromium alloy requires application-specific validation. Absence of nickel does not guarantee absence of every allergic reaction or establish medical-device qualification.
Nickel (Ni) – based alloys are also available:
Alloy 625: a nickel-based alloy containing chromium, molybdenum and niobium, used for resistance in corrosive environments and at certain elevated temperatures. Applications include chemical processing, aerospace and marine engineering. The producer’s data sheet specifies properties and conditions; comparison with 718 requires a defined environment and metallurgical condition.
Alloy 718: a precipitation-hardenable nickel-chromium alloy containing niobium, molybdenum, titanium and aluminium, among other elements. Uses include engine, turbine and rocket components. Properties depend on heat treatment and fabrication. The producer’s data sheet does not justify declaring it universally more weldable or corrosion-resistant than 625.
Taking AM to the next level
The increased availability of stainless steel powders will open up new possibilities for designers who want to create AM parts that offer corrosion-resistance, durability and long life.
In 2023, Outokumpu announced a new powder business and commissioning of an atomization unit at its Krefeld site in Germany. Using scrap from existing production supports material recovery. Energy use, yields and the complete chain still require assessment to establish environmental performance.
This article has first been published in the May/June edition of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.