Feature published in the March–April 2020 issue of 3D ADEPT MAG, then online in December 2020. Roles, machines and expectations reflect that period.
“Professional users adopting 3D printing are not looking for a new hobby, they’re looking for solutions to their most pressing business problems”, Kevin Han.
Thermoplastic filament extrusion builds a part through successive deposits from a heated nozzle. FFF stands for Fused Filament Fabrication; FDM, or Fused Deposition Modeling, is the name associated with Stratasys. Here these terms concern material extrusion, without laser melting.
Scott Crump invented FDM and co-founded Stratasys with Lisa Crump. Many manufacturers have since developed extrusion systems for different applications. This feature examines improvements and market expectations with Kevin Han, then CEO of AON3D, and Charles Han, CEO of INTAMSYS.
Beyond layer-by-layer deposition, industrial suitability depends on repeatability, available materials and the performance achieved in parts. The two manufacturers discuss these criteria.
Systems range from desktop printers to industrial equipment. Comparing solutions requires examining achieved accuracy, compatible materials, build volume, temperature control, repeatability and production needs. A marketing label alone does not qualify a machine.
These characteristics interact: the machine, material, design and settings must suit the application.
Improvements made with regards to machine capabilities
Desktop printers are not limited to hobbyists, nor are industrial systems exclusive to large companies. SMEs and larger businesses can use different equipment for R&D, tooling or production.
The choice for one or the other might vary from one company to another but their interest in both systems has given another reason to manufacturers to improve the capabilities of their machines.
A manufacturer’s development priorities depend on target applications and user needs.
Consistent filament feeding and controlled extrusion are essential to process reliability.
A moving print head that deposits no material does not necessarily mean the printer has failed. Diagnosis may involve filament loading, flow, temperatures or an obstruction along the material path.
A nozzle too close to the bed or a feeding problem can also prevent extrusion. Cleaning and adjustments should follow the manufacturer’s procedure for the specific model; a needle is not a universal remedy.
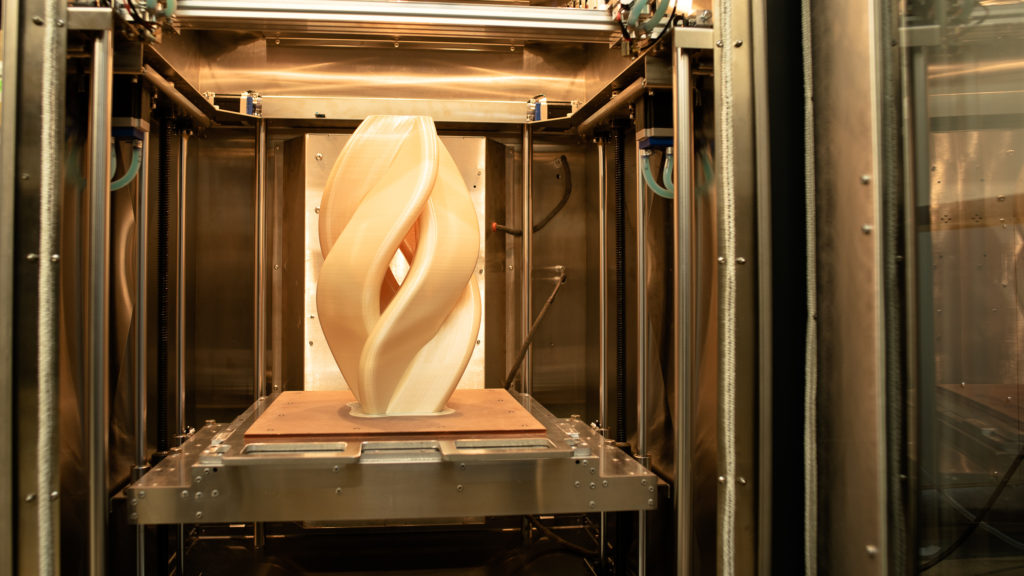
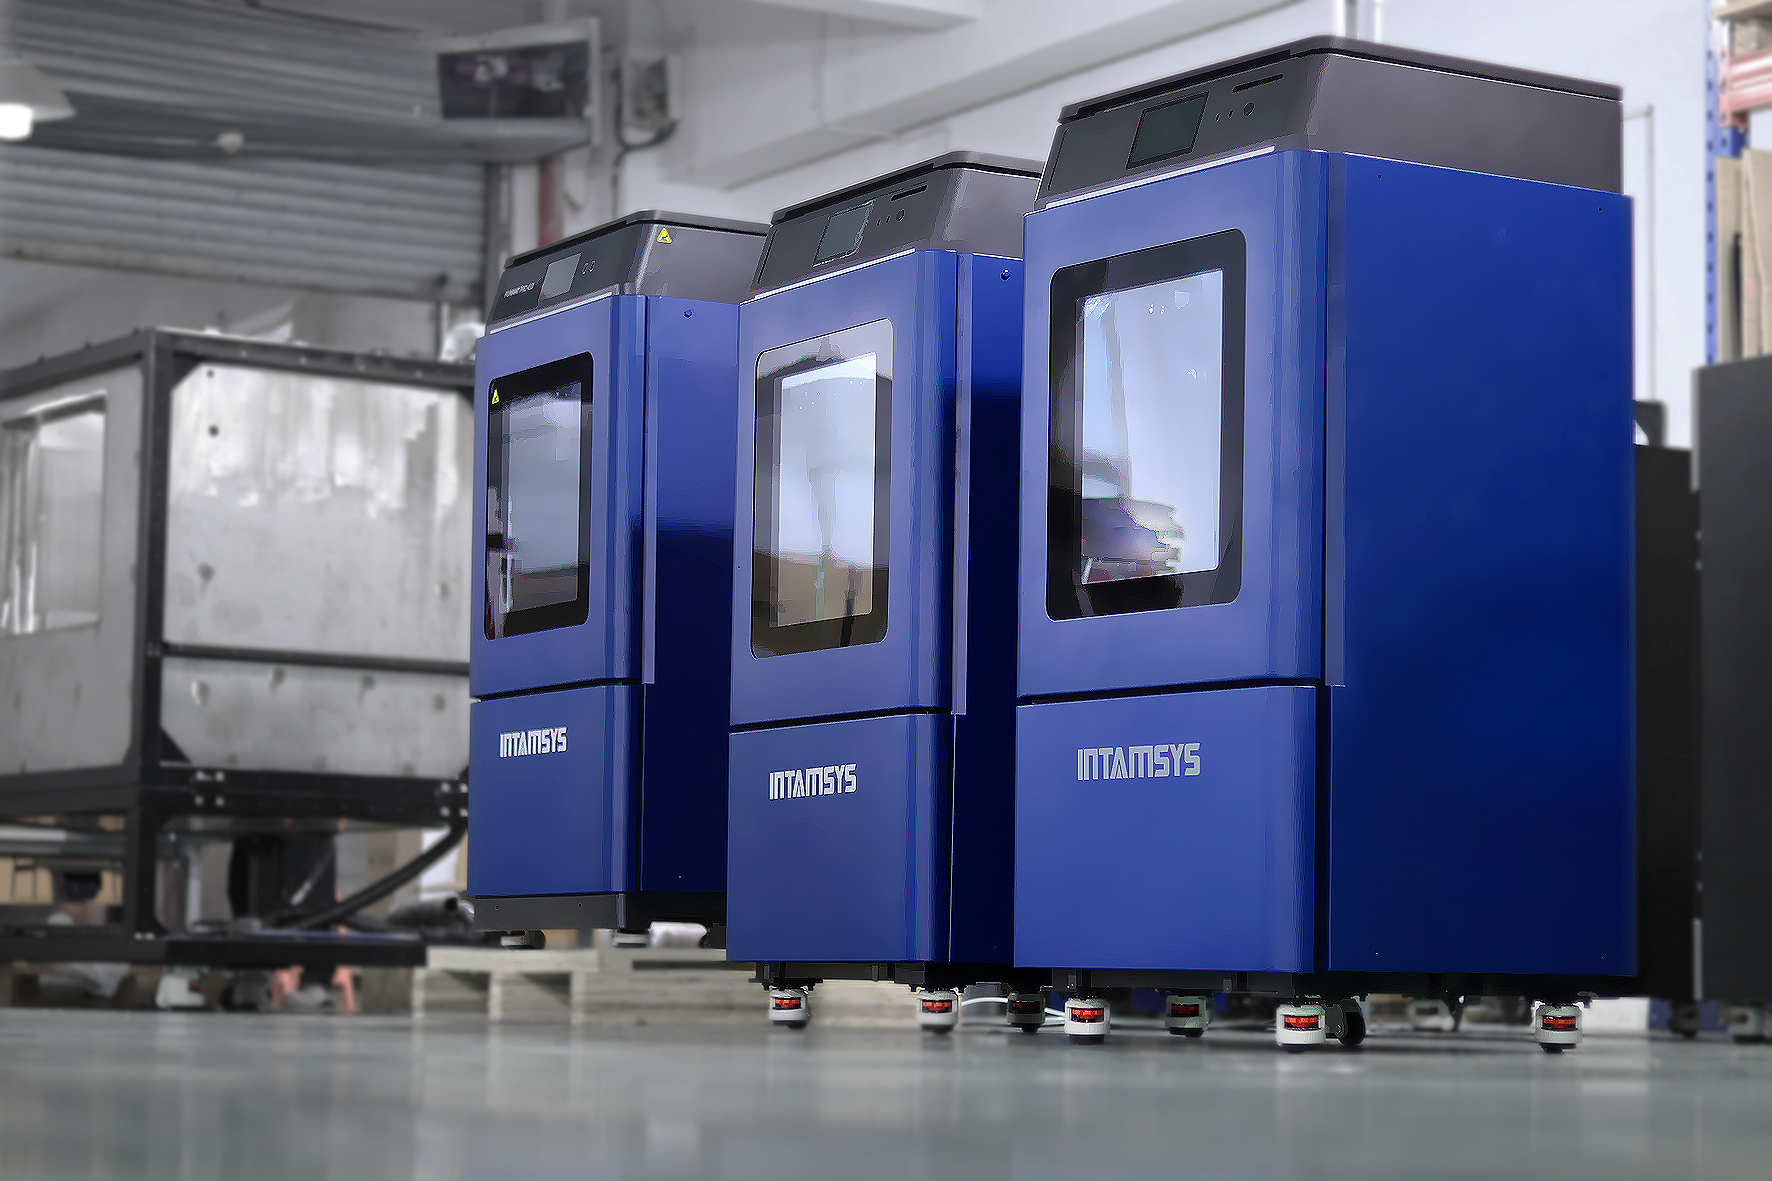
Printing speed and printing precision are the next features on the list. They remain key features that can be improved. INTAMSYS CEO, Charles Han explains that “printing speed helps to increase the production volume and thus to reduce cost, while printing precision improvement enables 3D printing applications to expand to more demanding industrial applications.”
For AON3D’s CEO & Founder Kevin Han on the other hand, improvements can go beyond printing speed and printing precision:
“Whatever it takes to improve repeatability, reliability, and process control – and this will be accomplished through a combination of both hardware and software. There’s a lot of hubbub right now over factors such as size and speed, but sophisticated users understand that without the foundation of repeatability, reliability, and control in place, the only thing a bigger or faster solution will do is create more scrap faster.
We’re approaching this challenge from multiple angles. Preventing variability from occurring in the first place with improved hardware, monitoring the build process with both hardware and software, and enabling continuous improvement to prevent future errors from repeating with data and software.”
Performance therefore results from the combination of equipment, software and process parameters.
Improvements with regards to the mechanical properties of the 3D printed part
Industrial expectations concern part properties as much as machine capabilities. Process improvements therefore need to be linked to each application’s mechanical requirements.
Partnerships between printer manufacturers and material suppliers contribute to this work. They also raise questions about access to materials and the settings needed to use them.
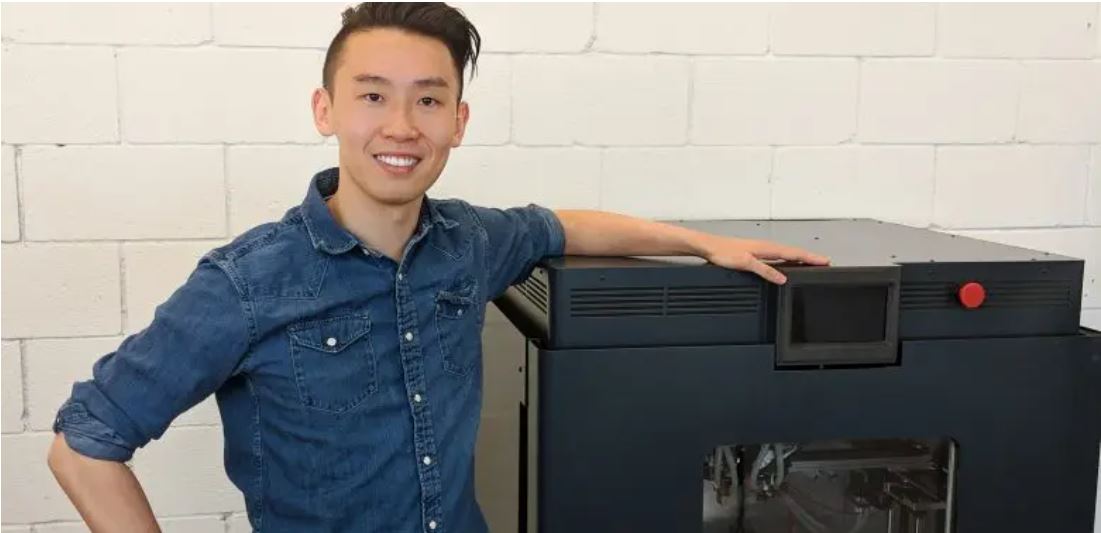
“It’s not just having access to high-performance polymers; it’s having access to the right high-performance polymers for the job at hand. If you break it down, every manufactured component can be described as a combination of three fundamental elements: Design + Material + Process. By limiting the availability of materials, the types of components that can be built are also limited”, comments Kevin Han.
Depending on the application, materials may include ABS, polycarbonate or PEI grades such as ULTEM. Properties depend on the grade and manufacturing conditions. A material designation guarantees neither part biocompatibility nor equivalence to an injection-moulded part: orientation, interlayer bonding, porosity and representative testing must be considered.
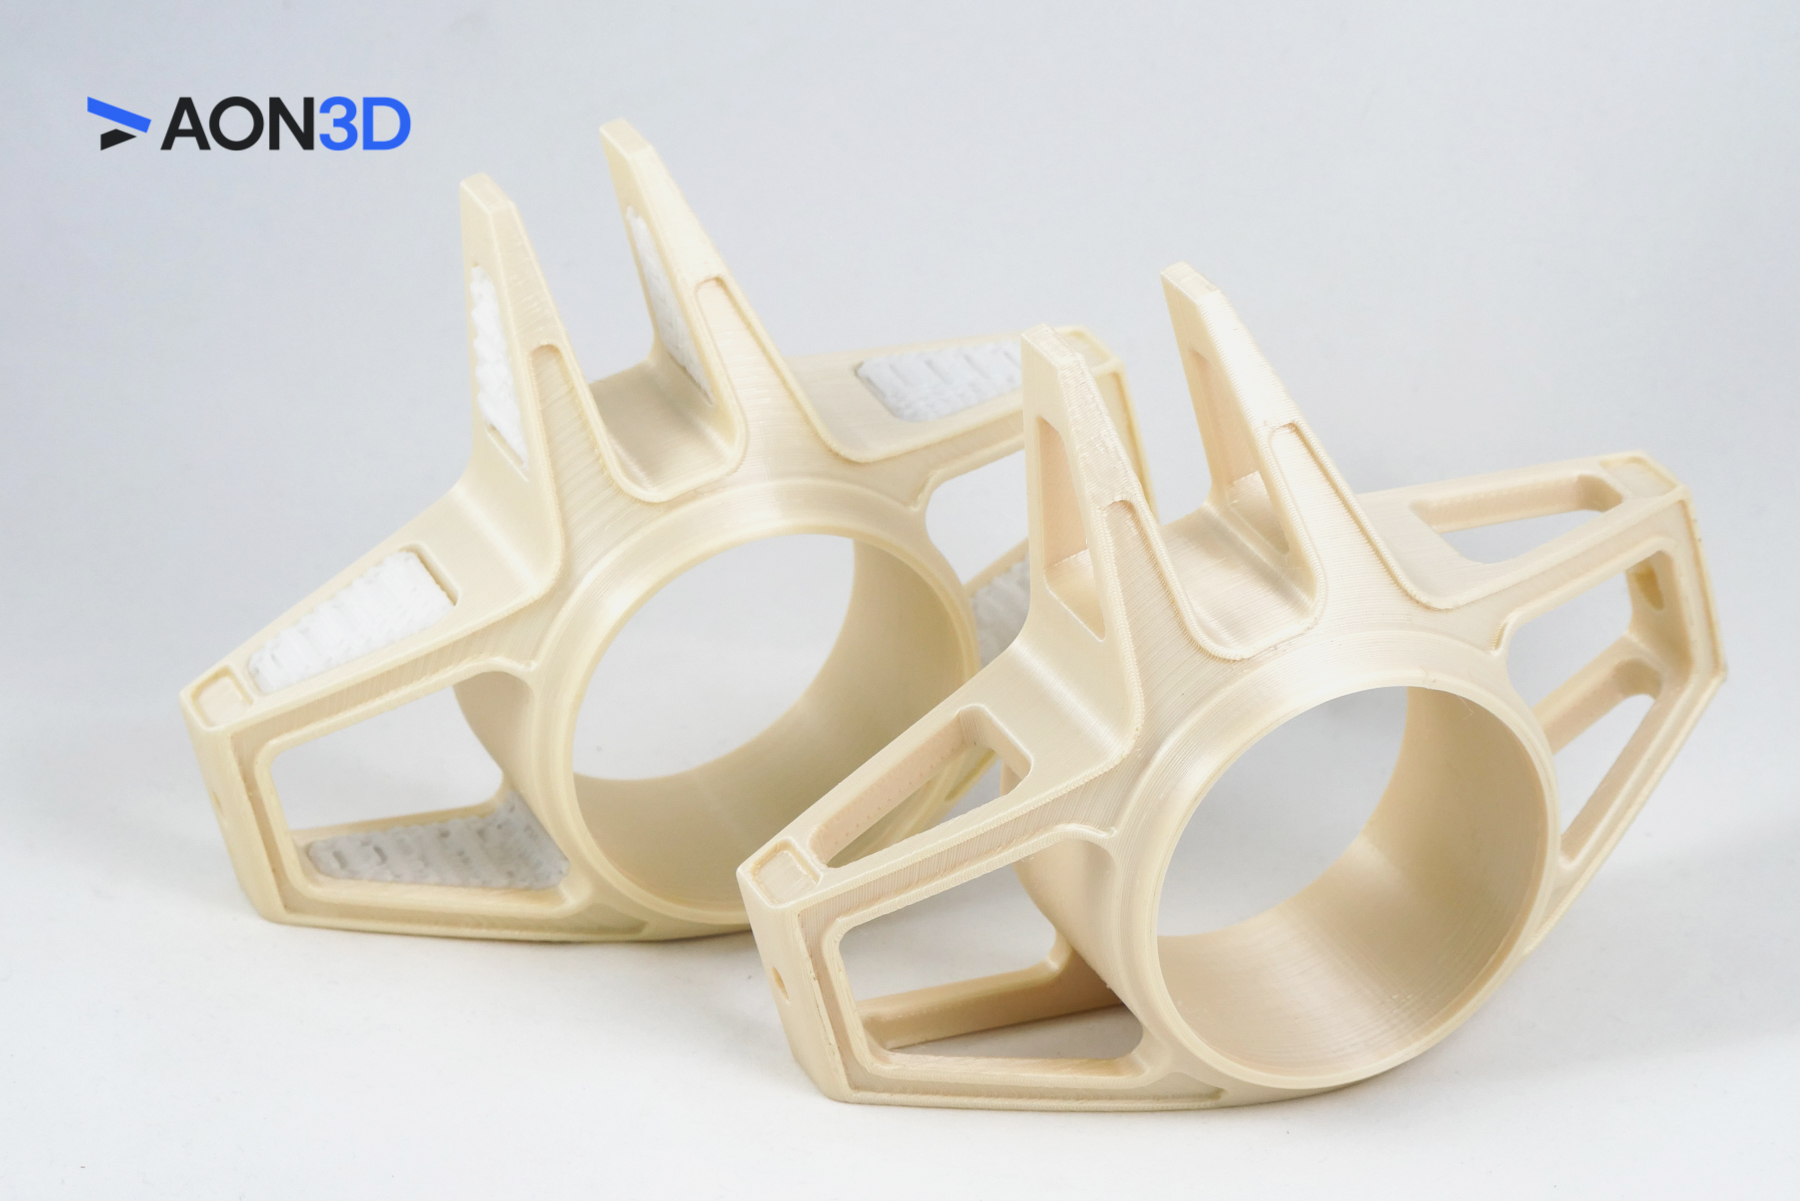

At the design level, “users bring the design element to the table, and it’s the OEM’s job to deliver on the rest. Users want the freedom to choose the right material for the job, at competitive prices, and without the need to undertake additional R&D. From Day 1 we have been committed to the idea of enabling an open material ecosystem through a combination of partnerships with material suppliers, a business model that doesn’t financially punish customers as they scale, and a technical service offering that eliminates the challenges associated with developing the process parameters for new materials”, continues AON3D’s CEO.
Kevin Han therefore emphasises material access and user support. Charles Han also stresses adapting engineering methods to the characteristics of the process.
“The overall engineering mindset can also be improved, as well as the engineering concepts that can be optimized to adapt to the characteristics of 3D printing. Based on our experience, we also found out that many raw data files generated by traditional engineering methods can deliver unexpected results if printed directly in FDM without any changes made. However, the printing performance can be improved by changing the internal structures of 3D models without any compromise on the quality delivered”, Charles Han explains.
For Kevin Han, improving mechanical properties is both an opportunity and a challenge. He emphasises manufacturing settings and process control.
“A block of marble and hammer & chisel in the hands of a master sculptor would yield quite a different result than in the hands of someone with less experience. Similarly, the same material and printer with optimized process parameters will yield a better part than with non-optimized process parameters”, completes the CEO of AON3D.
Industrial expectations expressed in 2020
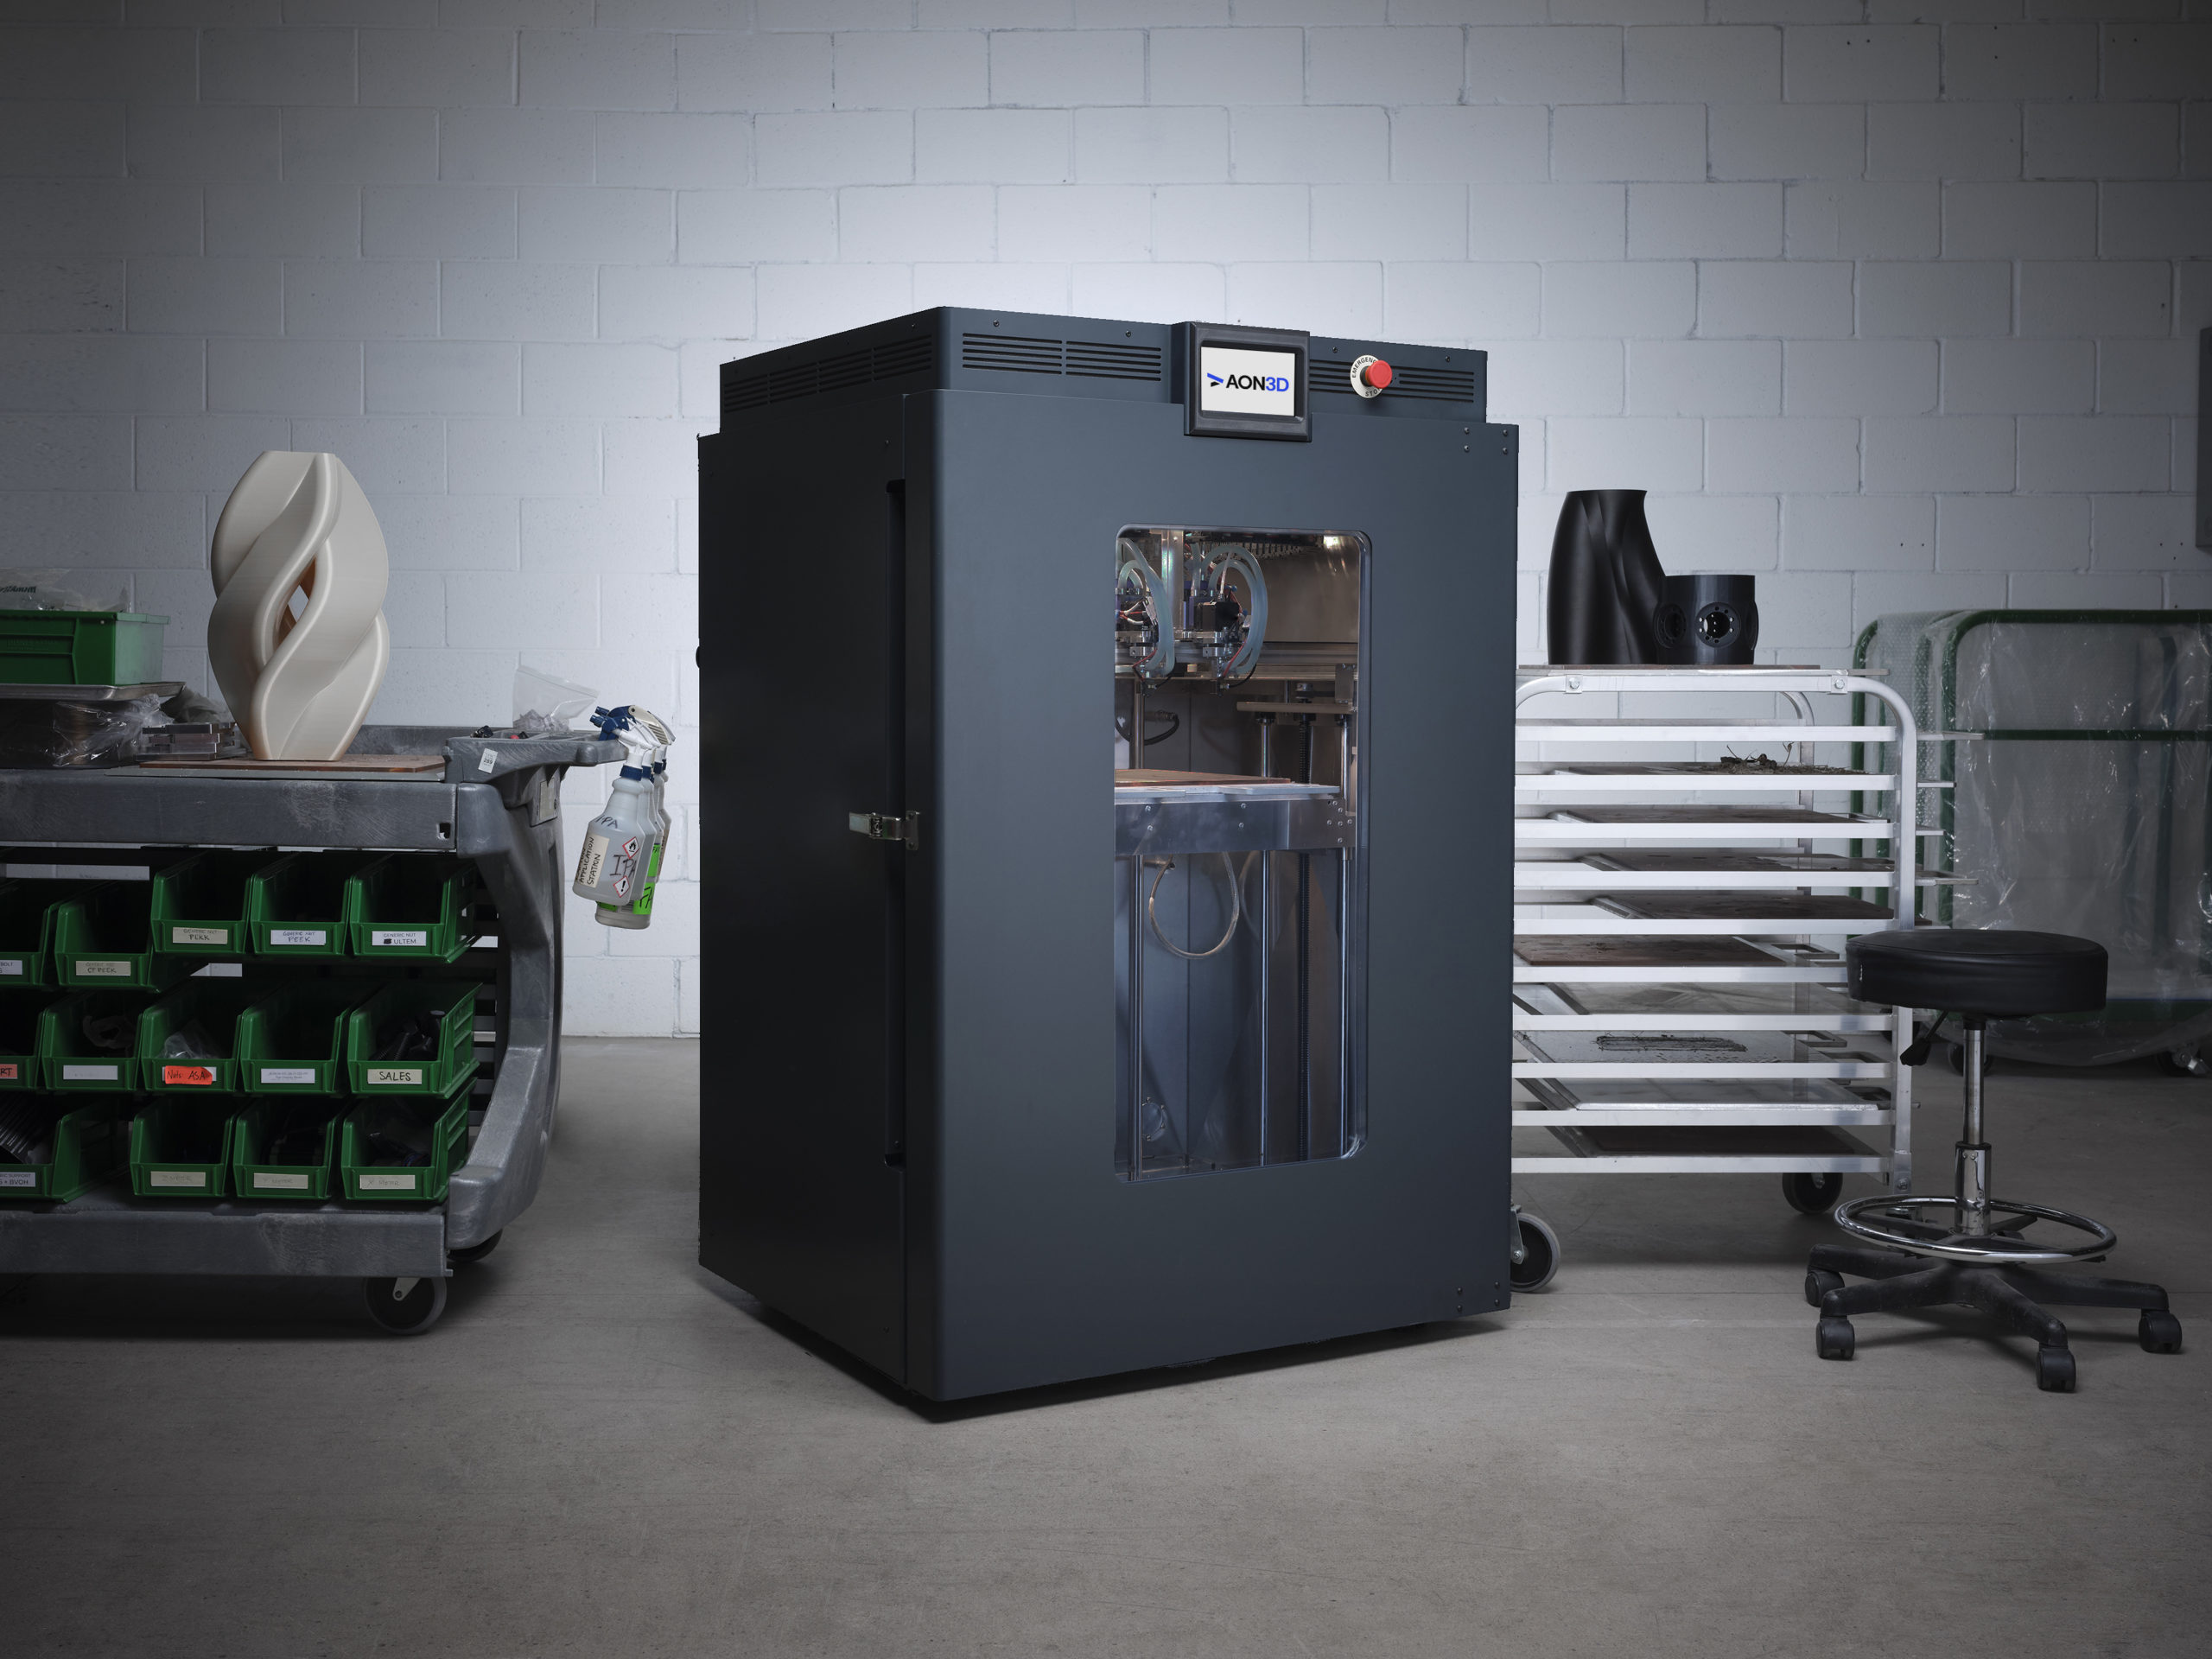
These accounts highlight the improvements sought in reliability, material control and part performance. System selection should start with the applications and required quality criteria.
Scaling up may require several printers, together with suitable preparation, monitoring, maintenance and part inspection. Machine numbers depend on volumes and workload.
“Depending on the application and the workload, some companies may want to use 3D printers for functional prototyping, in this case, a few 3D printers are enough. Some companies may have a lot of tooling applications in their factory; thus, they may need a larger number of 3D printers. There are also a lot of companies willing to use 3D printing for low volume production. These companies might want to build proper 3D printing factories with a significant number of 3D printers”, Charles Han concludes.
These 2020 perspectives show that the industrial value of extrusion is not determined by machine speed or size alone: it depends on a controlled process suited to the intended use.
This feature was first published in the March–April 2020 issue of 3D ADEPT MAG.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.