

Interview first published in the September/October 2021 issue of 3D ADEPT Mag, then placed online in March 2022. Roles, projects and targets reflect that period.
How can AM help reduce the impacts of procurement and maintenance in the energy sector? Brede Lærum and Pantea Khanshaghaghi discuss Equinor’s approach with 3D ADEPT Media. Their examples concern particular applications and are not, on their own, an assessment of the group’s overall climate trajectory.
At the time of the interview, the Norwegian energy group employed more than 21,000 people and had set a net-zero ambition for 2050. Its activities and plans covered oil and gas, renewables, carbon capture and storage, and hydrogen. An announced ambition is not an achieved outcome.
In this context, sustainability initiatives need measurements that track impacts and progress within clearly defined boundaries.
“There are two main areas that energy companies look into, when it comes to climate change and sustainability. The first one is the CO2 emissions from producing oil and gas – and we are working hard to reduce that as much as possible – and the second one is reducing the footprint for the product that is being used around the world. This second challenge makes it crucial to address the ‘carbon removal project’. We are actually developing a solution to capture the carbon and send it back into a place where there will be no risk of seeing it again”, Lærum told 3D ADEPT Media.
The carbon capture and storage discussed here should be distinguished from removing CO₂ already in the atmosphere. The claim of no risk is the interviewee’s statement; storage permanence and monitoring still require assessment.
The interview focuses on procurement, equipment production and maintenance, where AM can change material requirements and component life.
At the time, Lærum led Equinor’s Additive Manufacturing Centre of Excellence and chaired the Fieldmade Digital Inventory project and the international AM Energy network. Khanshaghaghi led business-development projects concerning sustainability through AM at Equinor.
From an additive manufacturing perspective, “we are looking into the CO2 emissions related to our procurement process, when we purchase equipment, goods and other products. This third area has a huge potential when it comes to reducing the consumption of raw materials and the corresponding energy consumption and CO2 emissions. Additive Manufacturing is perfectly fitted into a circular economy model” he adds.
“The oil and gas industry has several challenges to address but the whole world has a bigger challenge: the materials we are consuming. Hundreds of billions of tons of materials are consumed worldwide and we are not able to recycle them (We recycle less than 9% of them). This major concern raises several issues including pollution – because at least 1% of pollution comes from manufacturing (Manufacturing is responsible for 31% of global emission -which is the highest among different sectors)– and the security of supplies that the pandemic has highlighted, especially in Europe. Additive Manufacturing is uniquely positioned to play a role in these three main challenges. For example, when we say that we are going to achieve less waste and in all different phases of the manufacturing process, we can do so because the technology itself allows for less use of materials. Transitioning from conventional manufacturing processes to AM processes is just a first step in the actions that can be implemented.
Indeed, mining those materials is another problem. This means that, each production usually requires us to manufacture a lot of products in order to be commercially visible. We have to send these products to subsidiaries or partners across the world but also keep some of these products in case we would need them later. All of this requires a lot of materials, transportation, and resources that could be saved for other purposes. That’s the reason why, at Equinor especially, we are looking to transit into a digital world where we will not need to produce a lot and transport a lot. We would avoid this “overuse” of materials and send the products just when and where we will need them. By doing so, we are already able to cut CO2 emissions at multiple levels. On top of that, we are saving lots of time and money as a producer and for the end-user”, Khanshaghaghi outlines, speaking of these three main areas and why AM is a pivotal manufacturing tool for each of them.
The pollution percentages quoted in this interview do not have sufficiently specified boundaries to be compared. The Circularity Gap Report 2021 estimated global circularity at 8.6%: this concerns materials cycled back into the economy, not the recycling rate specifically for metals or AM powders.
As Khanshaghaghi explained the importance of these three scopes/ areas for an energy company (production of emissions, products used around the world as well as purchase & consumption of goods), she laid emphasis on the importance of the latter for AM professionals.
Indeed, one can extend the lifetime of equipment either by using AM to repair, by getting obsolete parts using 3D printing or by avoiding replacing certain components. “In the latter case, we would not need to take our raw materials, we don’t have to consume more energy to produce those parts, and therefore no CO2 emissions will be produced. So, by reducing the consumption of goods, we can actually quite contribute to the reduction of CO2 emissions. But that remains a relatively new area”, she said.
Avoiding replacement can avoid the associated manufacturing impacts, but repair or reprinting is not automatically emissions-free. Material, energy, transport and service life must be considered.
Additive manufacturing for maintenance
According to Lærum, Equinor’s AM activities began in 2016 with research into the processes’ reliability and potential value. At the time of the 2021 interview, the team reported about 34 FDM and SLS polymer printers used for educational purposes.
“We do not have an ambition to be a parts producer. We want the suppliers to continue producing parts, now using AM. That’s the reason why, although we keep a strong focus on metal AM technologies in our various activities, we do not invest in such technologies for our in-house activities. That being said, there are seven different and recognized AM technologies within this industry. Our activities and tangible examples of application explored so far, reveal a great potential for Powder bed fusion, DED aka LMD, and wire-arc AM”, the Head of AM emphasizes.
Terminology note: the seven categories describe process families. Laser metal deposition (LMD) and wire-arc AM (WAAM) are both forms of directed energy deposition (DED).
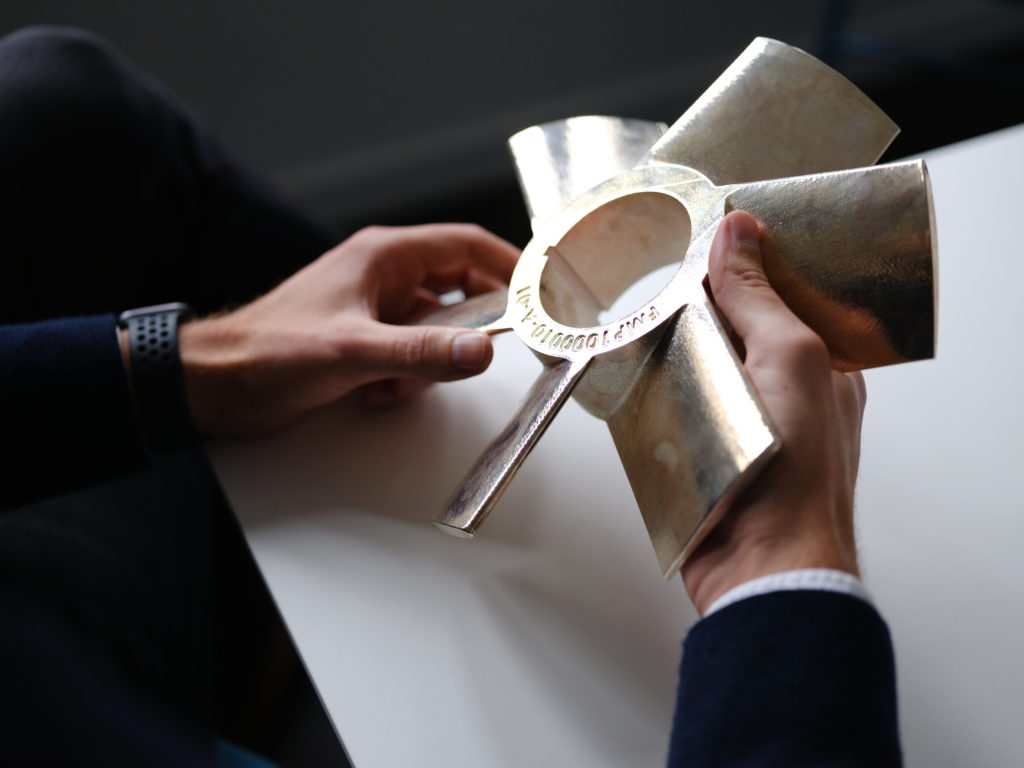
AM is not inherently sustainable: its impact depends on material, energy, finishing and the part’s use. Lærum presents a cooling-fan life-cycle assessment (LCA) to compare specific scenarios. Global warming potential over 100 years (GWP100) is expressed in kilograms of CO₂ equivalent.
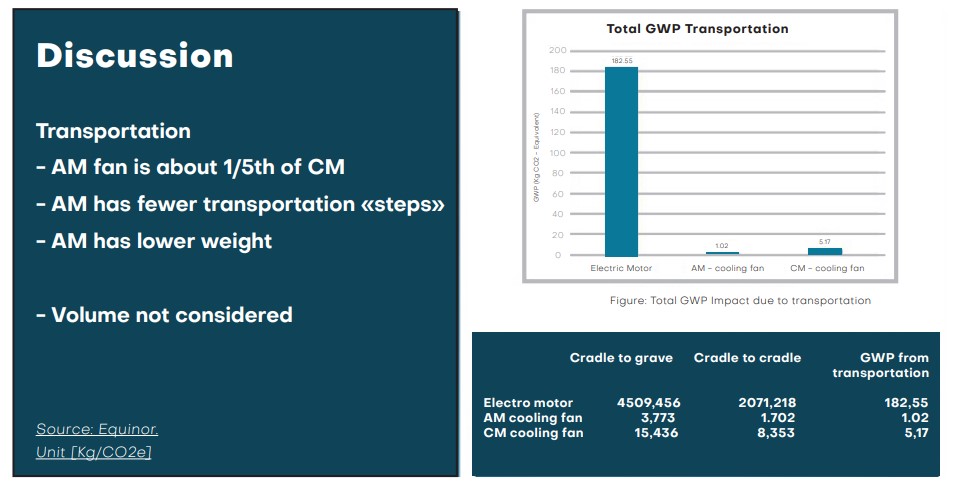
In the case Equinor describes, an obsolete cooling fan had broken and replacement of the complete motor, weighing about 1.5 tonnes, had been proposed. The document’s cradle-to-grave scenario attributes 3.773 kg CO₂e to the AM fan, 15.436 kg CO₂e to a conventionally made fan and 4,509.456 kg CO₂e to the complete motor. The rounded figures of 3.8 and 4,500 quoted in the interview therefore concern different objects. The graphics identify an electric motor; the quotation’s use of “pump” should not be confused with that label.
| Equipment | Cradle to grave | Circular scenario | Transport |
|---|---|---|---|
| Electric motor | 4,509.456 | 2,071.218 | 182.55 |
| AM cooling fan | 3.773 | 1.702 | 1.02 |
| Conventional cooling fan | 15.436 | 8.353 | 5.17 |
Transport is an impact item shown separately in the graphic; it should not automatically be added to the totals. Transported volume was not considered. Source: Equinor. View the original graphic.
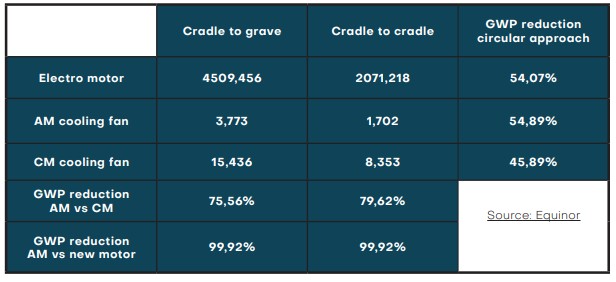
In the circular scenario presented, the reported GWP reductions are 54.07% for the motor, 54.89% for the AM fan and 45.89% for the conventional fan. These results depend on the study assumptions; they are not general rates applicable to every recycled component.
| Equipment or comparison | Cradle to grave | Circular scenario | Reduction from circular scenario |
|---|---|---|---|
| Electric motor | 4,509.456 | 2,071.218 | 54.07% |
| AM cooling fan | 3.773 | 1.702 | 54.89% |
| Conventional cooling fan | 15.436 | 8.353 | 45.89% |
| Reduction: AM / conventional | 75.56% | 79.62% | — |
| Reduction: AM / new motor | 99.92% | 99.92% | — |
The first three scenario rows are in kg CO₂e; the last two rows report percentages. Percentages are transcribed from the original and may differ slightly from calculations using rounded values. The full study assumptions are not reproduced in this interview. View Equinor’s original table.
“It’s a completely new scale. By extending the lifetime of that motor, we avoided 4 500 kg of CO2 emissions related to the production of a new pump. If you add that to all the different equipment we are considering to replace, this will add to a rather large sum of CO2 every year. It’s a really new era to look into when it comes to CO2 emissions. The whole industry should look into this “scope n°3” of emissions”, Lærum adds. As the expert explains, taking the example of the broken fan, looking at this “scope n°3” requires to look at the country where the components are being produced and where the raw components are being taken out. Furthermore, this production using AM refocuses the debate on the importance of circular economy and its ultimate purpose which goes beyond recycling.
Scope 3 covers indirect value-chain emissions, upstream and downstream. Production and transport locations matter, but do not alone define this scope. The fan results remain specific to Equinor’s selected scenarios.
“The main purpose of circular economy is to design the waste out and that’s exactly what AM does. First of all, we are using less materials, and thereafter, when we design the new part, we do so in a way that it will be recycled – or at least have a longer lifetime”, Khanshaghaghi notes. “By changing our behaviour and our way of dealing with all the equipment, we can of course contribute to reduce CO2 emissions”, the Head of AM completes.
Projects developed with partners
It’s one thing to know the process and identify the steps that one should take in this fight for climate change, it’s another one to have the right partners to do so.
The projects discussed included cooperation between Kongsberg Ferrotech, Equinor, SINTEF and Gassco to develop subsea metal repairs. Kongsberg Ferrotech dates this partnership to 2020; it formed part of the development work discussed in the interview.
Inspection, maintenance and repair robots create a locally dry environment while submerged. The composite-repair trials mentioned in the original interview should not be confused with qualification of subsea metal AM.
According to the sustainability expert, the concept of circular economy will once more play a key role here since AM will be used to repair instead of replacing. “That’s kind of designing the waste out again”, she reminds us. “From a manufacturing standpoint for instance, they will look at the way they can recycle all the metals they have. Amid the companies that will help us in this process, there is f3nice that recycles metal scraps into atomized powder.”
While AM is another great tool that illustrates the circular economy process in production, Khanshaghaghi highlights the importance for organizations to think about a better energy mix for that. “For instance, it is not interesting to use fossil fuels heavily in a country that is already planning to use renewable energies”, she notes. In the same vein, Equinor’s collaborators also note the enriching experience they have through collaborations with startups.
Lærum also discussed Fieldmade and the digital-inventory project involving Siemens Energy, TotalEnergies and Equinor. The aim was to organise spare-parts availability and on-demand production using suitable processes.
“Together, we are demonstrating that AM is contributing to sustainability throughout the whole circle of circular economy. In this specific case, the technology serves as a catalyst for the new digital ecosystem that we are building with Fieldmade and Siemens Energy. In the long-run, this platform will be a commercial product – promoted by Fieldmade – with two main functions: connect all operators and all suppliers in a huge digital network for spare parts. Secondly, all these suppliers could promote their own digital parts into the network so that the digital inventory will be driven by the ecosystem – not purchased by the operator-. Although AM is an important enabler for the digital inventory the main point is on-demand production of parts, using AM, CNC machining or any other fast, reliable and repeatable manufacturing method. The plan is to gradually reduce the physical inventory while building the content of the digital inventory”, Lærum explains.
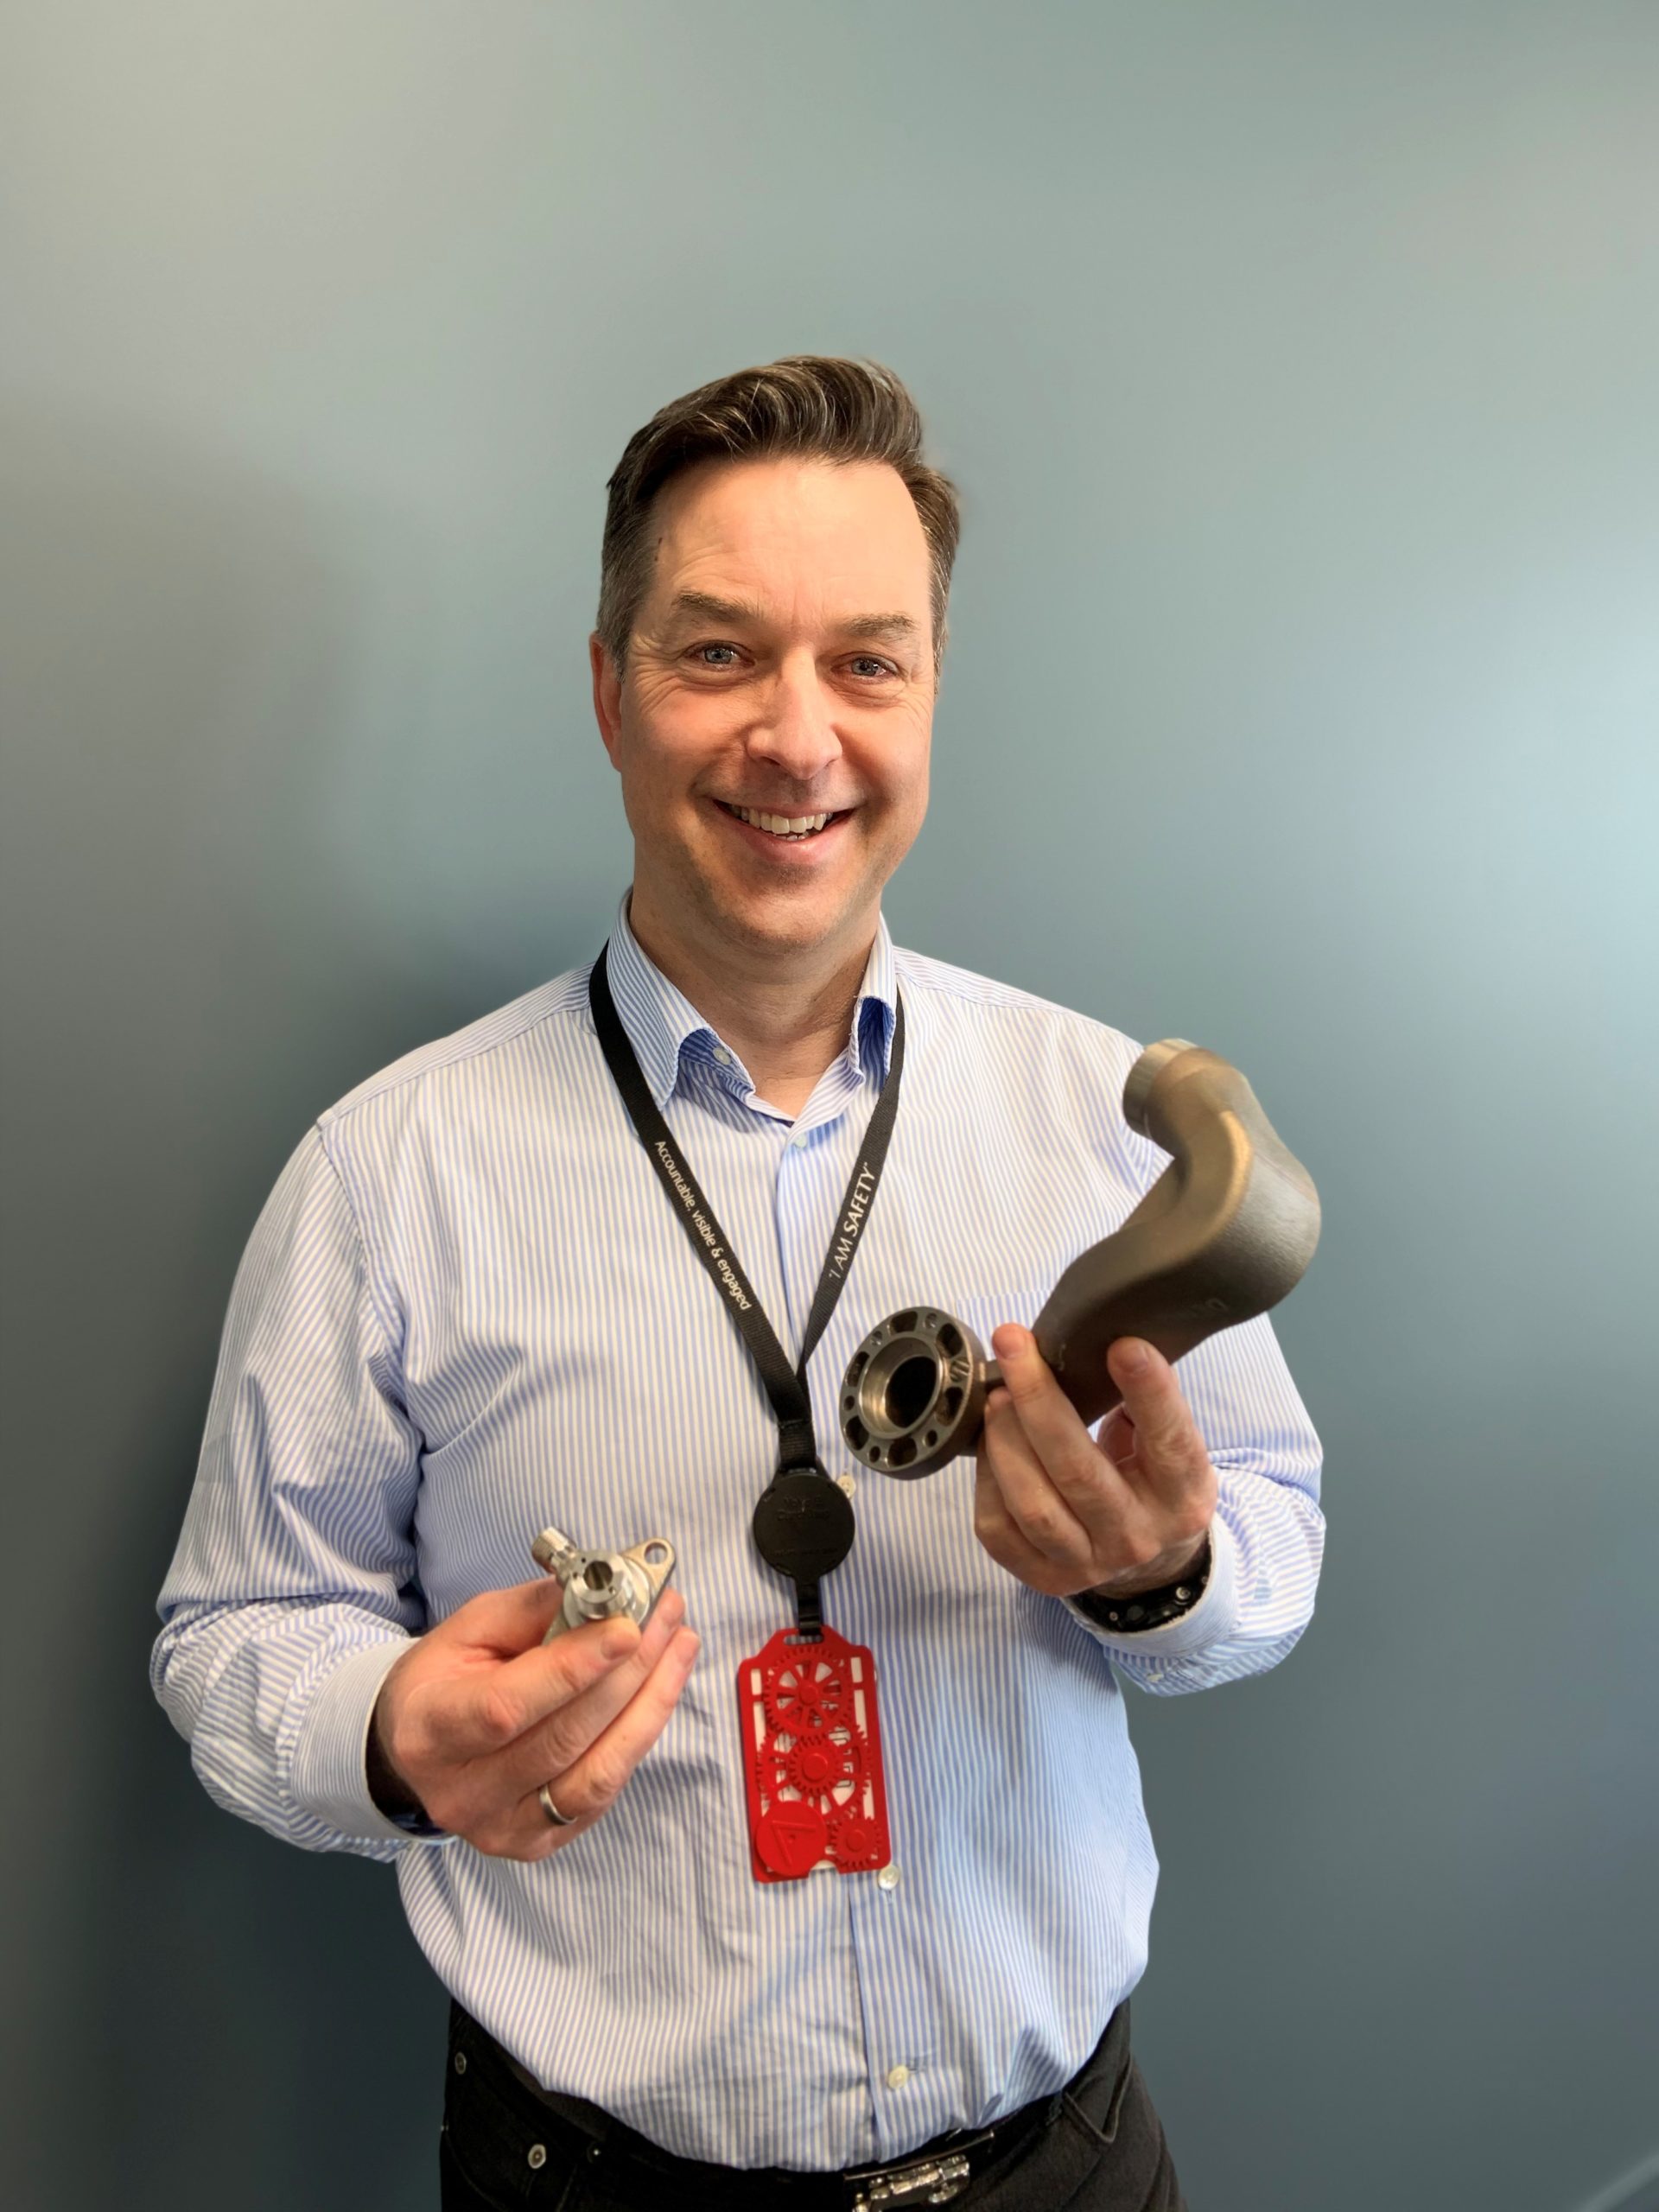
Opportunities to measure over time
Maintenance and reuse examples do not replace an assessment of an energy group’s total emissions. Operational emissions and those from the use of products still need to be considered within their respective boundaries.
AM’s value here lies in specific uses: keeping equipment available, adapting procurement and avoiding some replacements. Benefits need to be measured against an appropriate reference solution.
An ambition for more than USD 3 billion in cash-flow improvements over 2020–2025 already appeared in an Equinor presentation on digitalisation. This was a target covering digital solutions and ways of working, not a gain attributable solely to 3D printing or an outcome established by this interview.
Progress towards climate targets, including the 2050 ambition, needs to be assessed against measured outcomes. The applications discussed illustrate possible approaches and their conditions; they do not on their own guarantee that trajectory.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.