

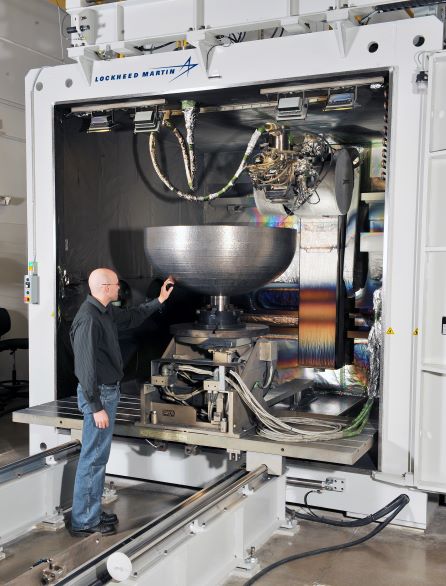
Interview published in 2023, first appearing in the May/June issue of 3D ADEPT Mag. John O’Hara discusses Sciaky’s wire-fed electron-beam deposition, large-part applications and qualification challenges. Dimensions and perspectives reflect that period.
Large metal parts can be made using several additive processes. Directed energy deposition (DED) can use an electron beam and wire feedstock. This is the basis of Sciaky’s EBAM® process discussed here; it differs from laser and electron-beam powder-bed systems.
In Sciaky’s process, an electron beam creates a wire-fed melt pool under vacuum. Melt-pool temperature depends on the alloy and should not be confused with powder-bed preheating. A figure of 1,000 °C is therefore not a general melting-temperature limit. Final properties depend on material and the complete manufacturing route.
Electron-beam additive manufacturing covers different architectures, which do not target identical build sizes or geometries. This feature concerns Sciaky’s wire-based systems, drawing on its electron-beam welding experience; it is not an exhaustive supplier survey.
Sciaky’s timeline records its founding in 1939, its first electron-beam welder in 1957 and the start of wire-deposition research in 1995. Electron Beam Direct Manufacturing became a service offering in 2009, followed by turnkey EBAM systems in 2014.
At the time of the 2023 interview, Sciaky was described as a Phillips Service Industries subsidiary, with about 50 people in Chicago and equipment deployed in several countries. John O’Hara, then Global Sales Director, discusses technical characteristics and economic barriers below.

EBAM’s key specifications for large-scale parts
Examples reported in the feature included a titanium aircraft spar about 3.7 m long and an aerospace part weighing over 1,360 kg, associated with a stated build time of 120 hours. These figures concern specific projects, not a guaranteed production rate or a schedule necessarily including all finishing and inspection.
One thing we quickly learned from O’Hara is that the size can always be tailor-made. Since they custom build their welding systems, it was only obvious for the team to build tailor-made chambers for their EBAM machines. “EBAM machines are typically made to order, with the sizes ranging in work envelopes of up to 6000mm x 2000mm x 1800mm as our largest machine, and our most common machine with a work envelope of 2000mm x 1100mm x 1500mm. EBAM is always done in a vacuum environment, which is ideal for reactive metals such as titanium, nickel, and refractory metals,” O’Hara explains.
To manufacture metal parts comparable to those made with traditional manufacturing methods such as casting, designers and engineers need to keep in mind a couple of constraints they will need to monitor and address at the design level and during the manufacturing process.
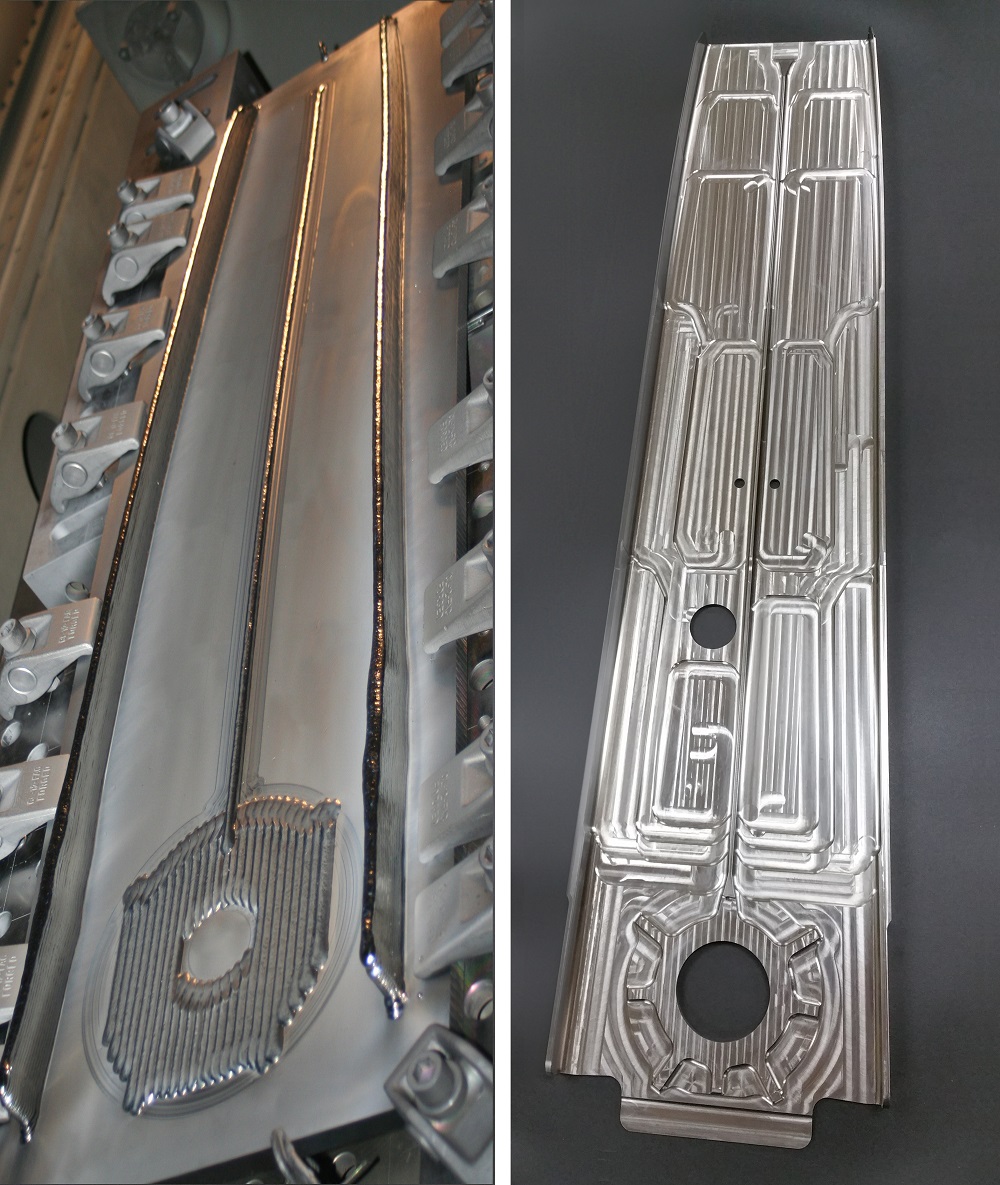
One of the considerations at the design level is that “EBAM must always maintain the melt pool in a horizontal orientation, and must always print onto existing metal. This reduces the opportunities to print hollow cavities. The feature resolution of EBAM at best is 2mm features at low deposition rates, but will typically have a resolution of 8-12 mm,” according to O’Hara.
Wire feedstock can reduce some material losses and simplify handling relative to powders. Availability, price and qualification still depend on grade and supplier. An economic comparison also needs to include energy, deposited machining allowance, finishing and inspection.
Deposition variation can affect geometry and metallurgy. Sciaky describes IRISS®, the Interlayer Realtime Imaging & Sensing System, as closed-loop control that measures the process and adjusts inputs including beam power, wire feed and motion. Monitoring does not remove the need for process qualification and part inspection.
EBAM produces a near-net-shape preform rather than eliminating post-processing. Sciaky’s documentation includes heat treatment, finish machining and inspection. Their details depend on alloy and application and belong in the industrial and economic assessment.
Qualification, investment and service providers
For O’hara, the main challenge is to fund the qualification of their metal technology for production processes.
“As a manufacturer, we always pursue cost-saving measures. However, regardless of the industry, making a big part remains expensive. The biggest challenge for large format machines is that they are very expensive. The investment that you make is rather large in the development cycle and the operational investment should be proportional to the type of parts you want to produce,” the Global Sales Director points out.
While EBAM lags far behind in adoption, compared to LPBF, “these two technologies have no overlap, and are not in competition with each other,” he adds. “LPBF cannot make parts the size of EBAM, and EBAM is not economical to use on parts with ideal sizes for LPBF. LPBF has been available longer, and has many more companies working on advancing the technology.”
This comparison expresses Sciaky’s positioning in the 2023 interview. The feature provides no quantitative evidence of an overall adoption gap, and suitable applications may overlap depending on equipment. Size, detail resolution, productivity and total cost should be compared for the intended part.
The million-dollar question that comes next is: how do we address this? Educating adopters on the potential of EBAM for large-scale parts is definitely one step to explore but it shouldn’t be the only one. A big part of the work also lies in the development of applications that are not always harnessed in industries with the most stringent requirements. In the end, the more demanding the qualification requirements are, the more time it will take to achieve applications.
On another note, one road adopters could always take – regardless of their industry – is the one that leads to the AM service provider.
“Most people are interested in working with AM service providers. Most of the machines we sell are used for in-house applications. However, Sciaky can take on a production contract. We help our customers justify the cost of the machine, develop the technology for their own use as well as the material properties ideal for their applications,” O’Hara concludes.
This article was first published in the May/June edition of 3D ADEPT Mag
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.