

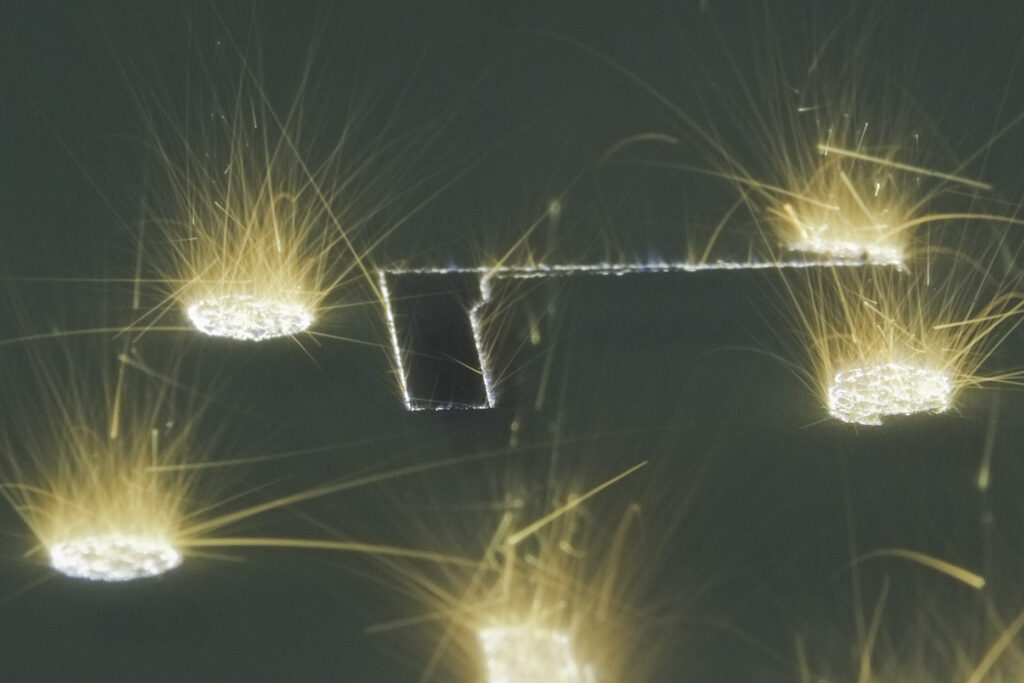
Feature from the January/February 2023 issue, with Kartik Rao (Additive Industries) and Dominik Schmid (Kennametal). Roles and reported examples reflect that period.
Adding lasers to a 3D printer can increase manufacturing capacity. The gain depends on their actual use, the operations shared by each layer and the required quality. This feature examines when a multi-laser approach can make sense.
Lasers concentrate energy to process material locally. Their effectiveness depends on material and process; they are not the optimum energy source for every AM application. Metal laser powder bed fusion generally operates in a controlled atmosphere, not simply in ambient air.
This feature focuses on metal laser powder bed fusion. Selective laser sintering (SLS), also a powder bed fusion process, can use several lasers for polymers. Some directed energy deposition (DED) and stereolithography systems also use multiple beams.
“In polymer AM there is selective laser sintering (SLS) that is also available with more than one laser source. There are some stereolithography machines with multiple lasers as well, however the required energy density for photopolymerization is low, so there are other methods that expose more than one area at a time”, Dr. Ing. Dominik Schmid, Sr. Engineer, at Kennametal comments.
According to Kartik Rao, Strategic Marketing Director at Additive Industries, the industry that probably shows us a path where we are going to head down is the laser cladding industry. “There are a lot of people that work with laser cladding in the oil and gas industries; so, they take big, long shafts and they are cladding the whole thing in wear-resistant materials with multiple robots working on a part. Ultimately, that’s probably where AM is headed”.
While each of the aforementioned technologies uses different types of laser and laser power and requires different beam sizes on the build plate, the ultimate goal for part producers is the same: enhance productivity while eventually reducing the cost per part. Here is the thing, a number of technical challenges may arise when working with multiple lasers in a powder-bed fusion process.
When does “more” mean “better”?
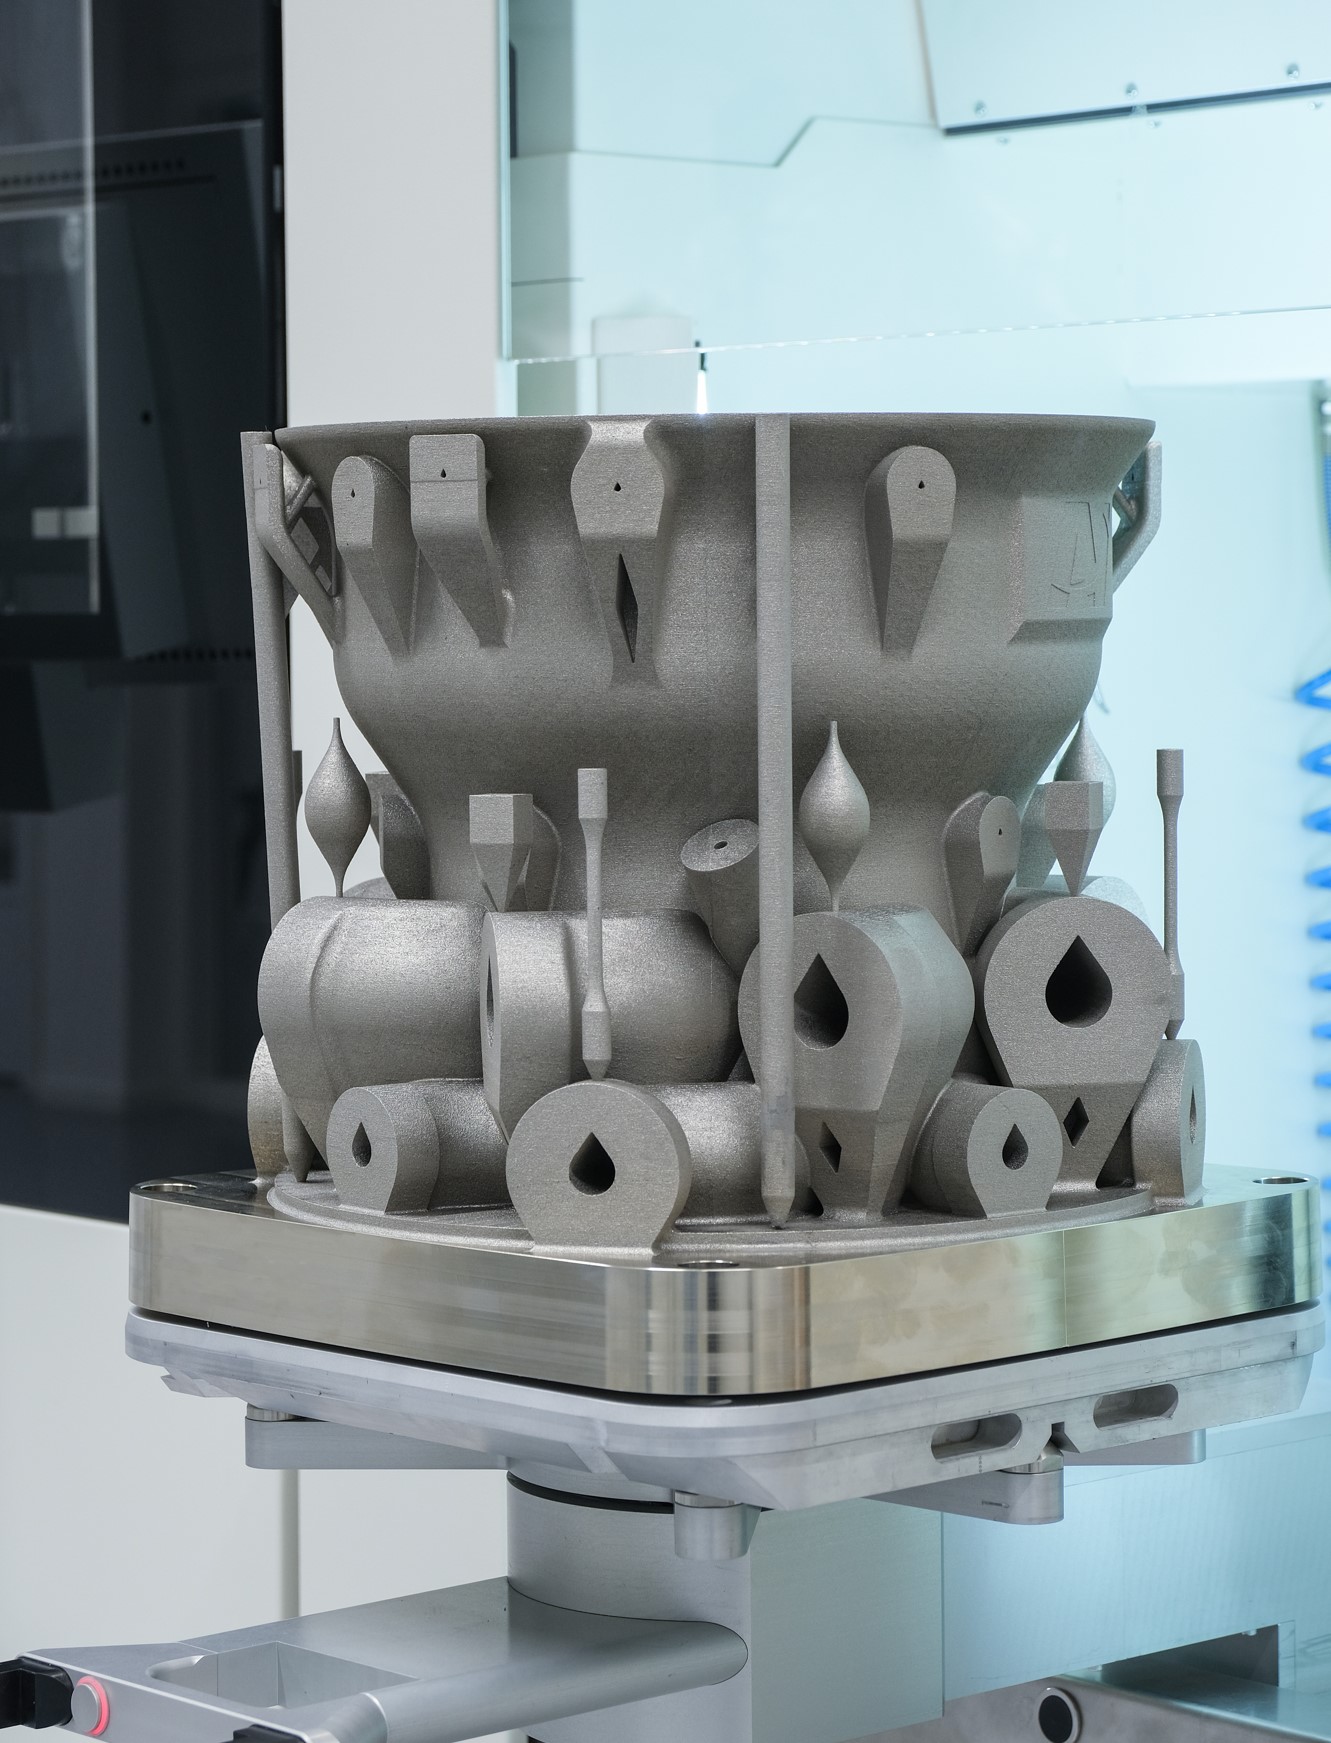
For limited prototyping or research needs, a single-laser system may be sufficient. The choice still depends on geometry, volume, material and how closely the work must represent future production.
Assessment of a multi-laser system should compare useful throughput, build-plate occupancy, preparation time and the cost of conforming parts. Questions include how many parts can be built together and which dimensions the machine can accommodate.
“Multi-laser systems have a higher build rate meaning the production capacity is higher compared to single-laser systems. On the other hand, they are more expensive than single laser systems. So, it is important to make usage of that additional capacity the systems provide. In short, the most vital factor in whether it makes sense to use multi laser systems is the demand for additive products”, Kennametal’s expert points out.
Emphasizing on the technical reasons why it makes sense to use multiple lasers in powder-bed fusion processes, Additive Industries’ speaker notes:
“In the powder-bed area, it makes more sense to have multiple lasers because ultimately, you want as much of the powder bed to be active as possible. The cost of the part may be a reason worth considering as well as the size of the parts you will be able to build. Very large parts for instance may require to have multiple lasers working on them, otherwise it may take up to 30 days to build, which is clearly a very long time and it will not be scalable for your business. It also makes sense if you have smaller parts on a large build tray.”
Depending on the architecture, scan fields may overlap partly or each cover the full plate. For example, Renishaw described four lasers accessing the full RenAM 500Q powder bed in 2019. Lasers are therefore not necessarily restricted to four fixed zones.
On another note, even if productivity is advocated, quality should also be part of the equation and that’s something that can be challenging when one is aware of the implications surrounding material properties, build strategies and other laser parameters relevant to additive manufacturing.
Laser parameters relevant to multi-laser AM systems
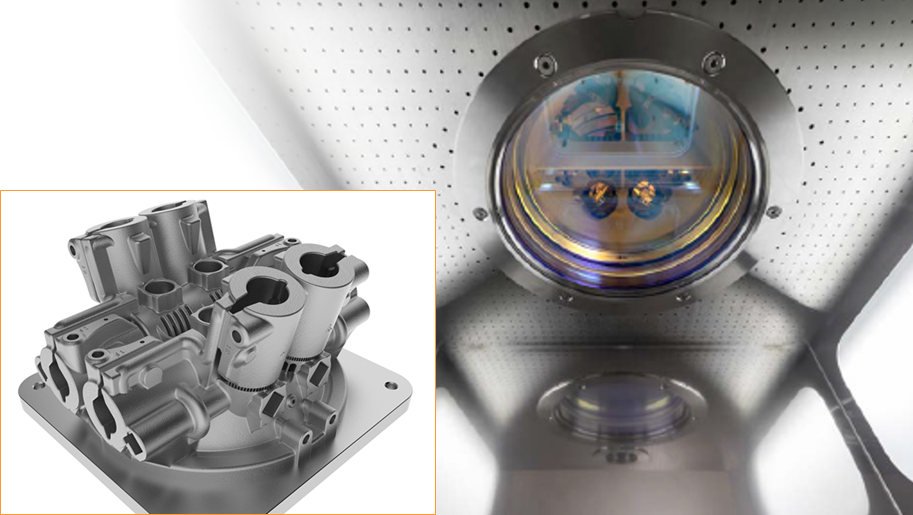
Equivalence with single-laser material properties needs demonstration through checks appropriate to the part and its use. Calibration, joining zones and interactions between beams can influence microstructure and defects.
Schmid explains that the scale with more laser sources is not linear. “A machine with four lasers might only be three times as fast as a single laser machine because the recoating time basically remains the same. Whether it is possible to reduce manufacturing costs with multi-laser systems depends on the specific application as well as the required investment in the machines themselves. Multi-laser manufacturing brings additional challenges, such as laser alignment or more complex design of the inert gas flow, so the ideal result is when quality can be achieved equal to a single laser machine”, he outlines.
Rao emphasizes that more lasers guarantee neither proportionally faster production nor higher quality. Points to control include:
- zoning/stitching of parts
- interaction of lasers with condensate from another active laser
- gas flow (heat management and waste removal)
- calibration of lasers (absolute and relative)
Spatter and condensate need removal without disturbing other beams. Here, stitching means joining regions processed by different lasers, not lasers physically being too close and “stitching” a part. Partitioning and overlap strategies require validation to avoid discontinuities and property variation.
Furthermore, the relative position of lasers with regard to the gas flow is pivotal, governed by laser assignment choices made during build preparation. Needless to say that gas flow configurations vary from one machine to another.
“In most cases some sort of attribution of the lasers to the parts has to be done by the operator. This means if you have multiple pieces on the build plate you need to assign which laser should work on which part. Because multi-laser machines are more expensive and build times are shorter, the scheduling of builds and planning of shifts becomes even more important to minimize unproductive time and maximize productivity and efficiency.”, Kennametal’s representative comments. Speaking of gas flow and thermal stability consideration, he adds: “When using more than one laser simultaneously, the fumes from one process zone should not interfere with the laser beam(s) active in another area. This needs to be resolved by the inert gas flow direction in combination with timing and local attribution of lasers. At the same time multiple lasers bring more energy and thus heat to the building chamber. A part of that heat goes into the gas flow, the other into the machine frame. This has to be taken into account at the machine design. The powder management is virtually independent of the number of lasers sources/optics.”
So, how do you determine your build strategy?
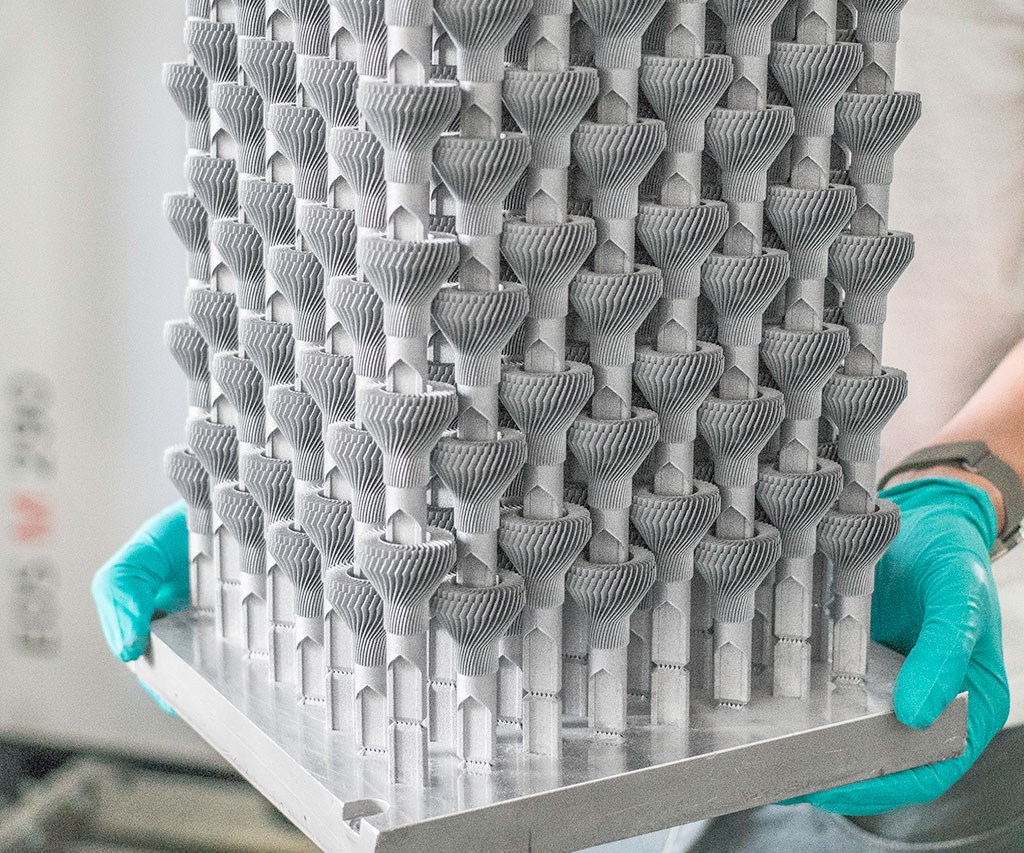
While manufacturers often use multiple lasers, either to build simultaneously a single component or to build individual parts with each laser, they should assess the turnaround time on the 3D printer, “as the goal remains to maximize laser utilization”, Rao highlights.
“What’s the point of having more than four lasers if you only take advantage of one or two? In the end, the more lasers you have, the more expensive the system is. The rise in capex needs to be offset by higher productivity. However, productivity is also influenced significantly by build time and shift patterns [and this depends a lot on the application you want to achieve]”, he continues.
Software supports laser assignment, scan-path preparation and calibration. In the interview, Rao described Additive Industries’ work on dynamic assignment, qualification and multi-beam calibration, alongside computational fluid dynamics (CFD) and testing. These tools support the process but do not replace part validation.
Conclusion
The appropriate number of lasers depends on demand, utilization and part geometry. Gains need measurement across the full cycle, including preparation, recoating, cooling, inspection and post-processing. Higher productivity and lower cost remain outcomes to demonstrate for the chosen application.
A few notes on the contributing companies
Kennametal reported using multi-laser powder bed fusion for certain hot-work tool steel products and binder jetting for carbide tools and wear components. These choices depend on the required properties and manufacturing chain.
Additive Industries is a Dutch manufacturer of metal AM systems serving industrial markets including aerospace, automotive and energy. Its contribution provides the machine manufacturer’s perspective.
This dossier has first been published in the January/February edition of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.