
Interview first published in the July/August 2022 issue of 3D ADEPT Mag, then published online in October 2022. Roles, production resources and plans reflect that period.
I knew, from day one, that Conflux Technology was the kind of company I would closely watch in this industry. Following seed funding in 2017, it caught my attention in 2021 by closing a Series A investment round of AUD $8.5 million to develop 3D printed heat exchangers. At the time, I had never talked to founder and CEO Michael Fuller. The reason why I knew I would watch this company is that its business combines heat exchanger design and production using additive manufacturing, and not just any applications, the one that most metal 3D printer manufacturers will create to demonstrate the capabilities of their technology.
It seemed simple, but it was not. When I spoke with Fuller for this interview in 2022, I couldn’t help but smile while listening to his story and company’s journey. Without knowing it, he gave me three more reasons to follow Conflux, and on top of that, discussed a misconception about the additive manufacturing of heat exchangers.
Three reasons that may raise interest in Conflux Technology
I don’t know about you, but I am the kind of person who looks beyond the quality of a product in business. For me to remain faithful to a product or service, I need to know something about the founder or the people behind the brand, or at least there should be something I respect or value in the company’s vision or values.
1. Seize and create opportunities
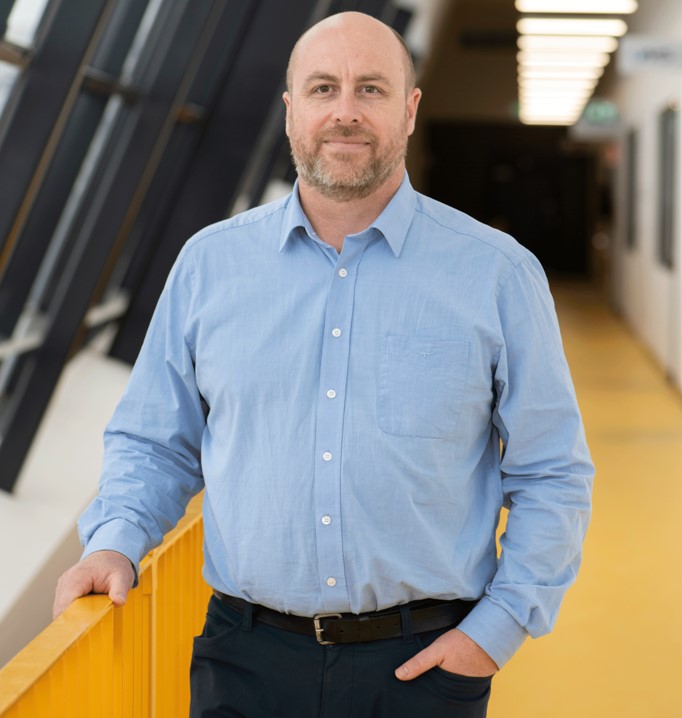
“There were a few different circumstances that led to a creative “ah ha” moment for me, these were off the back of a 15+ year career in the European motorsport industry, chasing my boyhood dream of designing racing cars. I found myself back in Australia for family reasons and I happened to have a broken ankle. So, I had my laptop out and I got designing”, he told 3D ADEPT Media.
2. Experience in design and motorsport
“I have history as a design engineer and had early adopter exposure to additive manufacturing in the motorsport industry. I also had quite a bit of experience with the pain point of heat transfer. Occasionally you have a good idea, and I wanted to pursue this one a bit further to see if I could get to a proof of concept from a technical feasibility point of view. From here I decided to put a bit of money into getting something made and then tested, and convinced myself to continue forward in terms of commercialization. At that point I needed to figure out how to start and then run a business. So just did a whole bunch of research and got stuck straight in”, he said.
3. Improve heat transfer across industries
Heat exchangers are used in many systems, including air conditioning, refrigeration, engine cooling and electronics. They transfer heat between fluids, or between a fluid and a surface. Their design must balance heat transfer, space, pressure losses and operating conditions.
For Fuller, “it’s so ubiquitous, that the opportunity to improve efficiency in heat transfer means that it can be transferred across almost every sector that you can imagine. For example, improvements in heat transfer efficiency can mean that your aircraft can use less fuel for the same flight. You can achieve that whether it’s in weight reduction or in fuel consumption directly. In the automotive sector, if you can package things into tighter stranger spaces, then you can improve overall aerodynamic drag and so you can improve efficiency there. In microelectronics, if you’re able to take the heat away from the chips more efficiently, then you can calculate more, and you can calculate faster. This then has knock-on effects – as you can imagine in medical research and space exploration- and in all sorts of things. The fundamental impact of improved heat transfer efficiency goes on and on”.
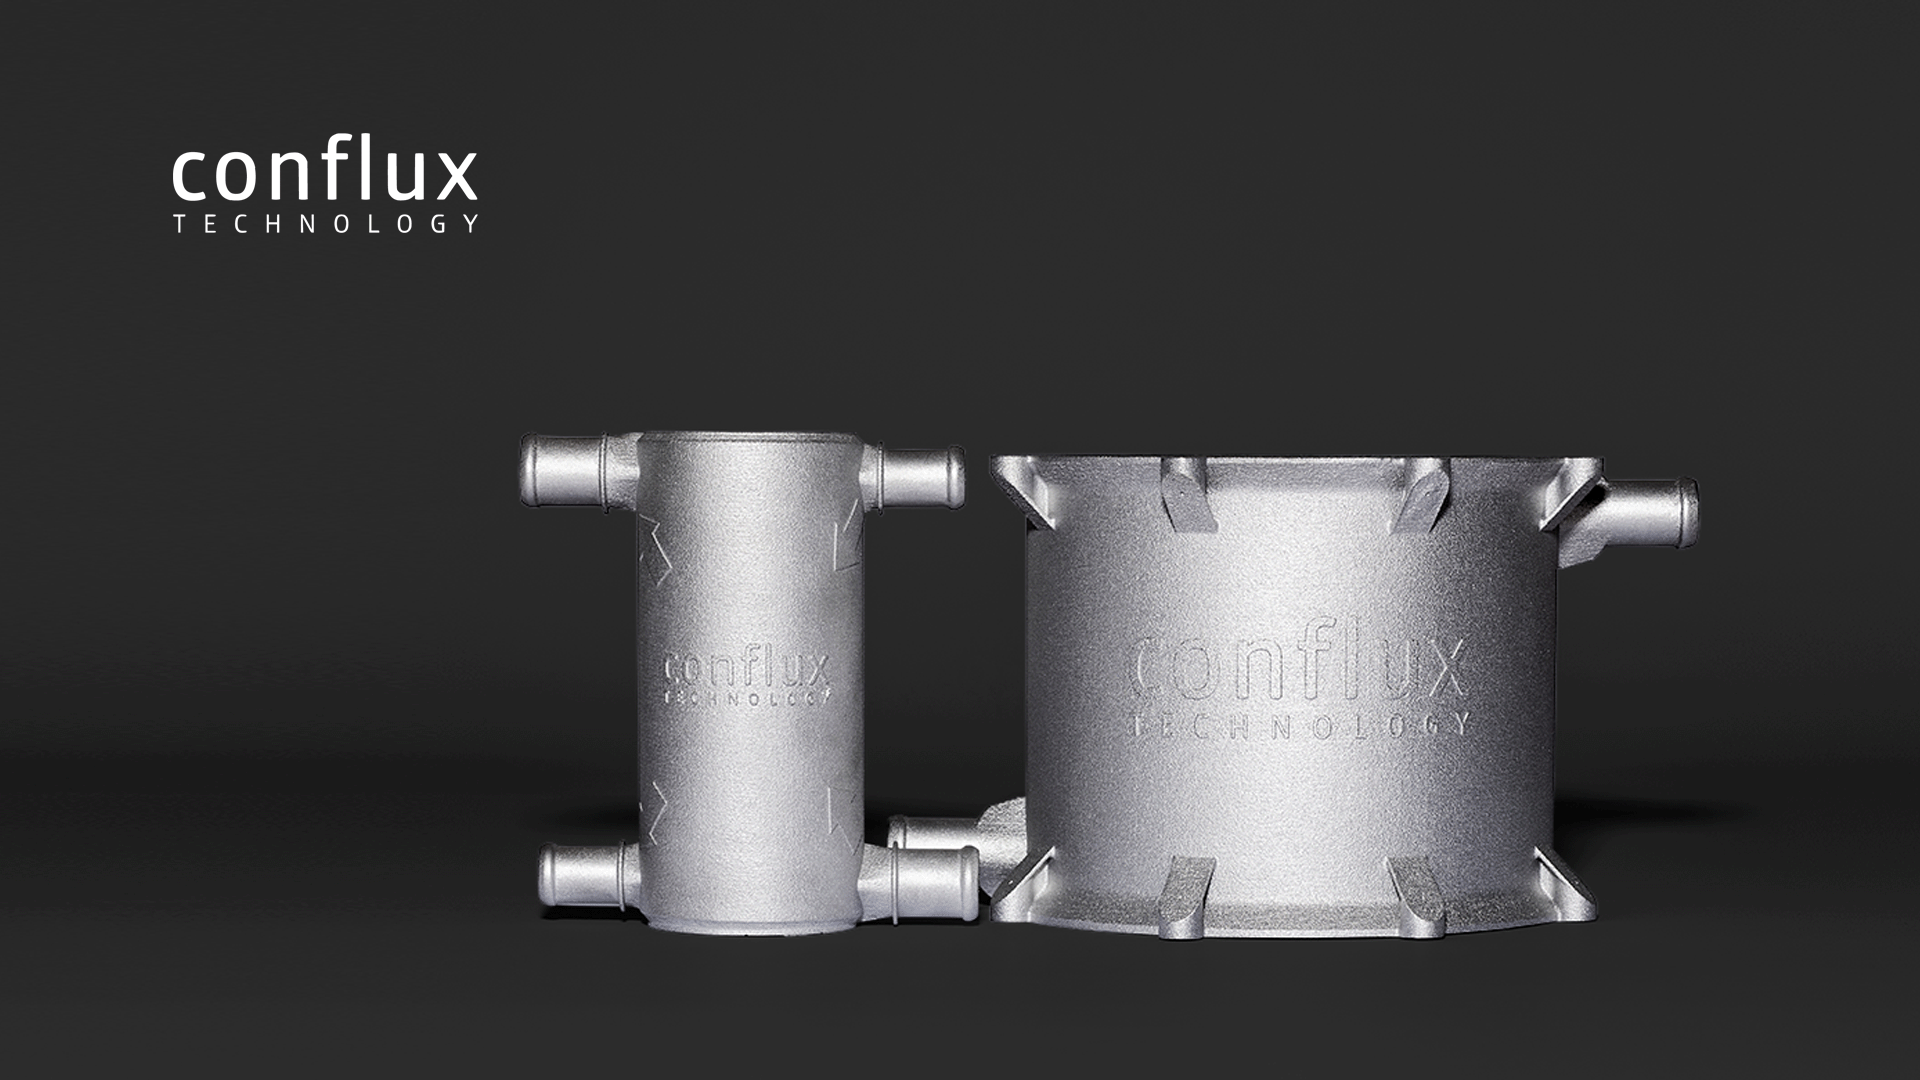
Furthermore, when you look at the way heat exchangers are usually produced, you quickly realize that the traditional manufacturing route may involve a combination of brazing, welding, extrusion, machining and molding. In one of the manual processes for example, if there’s a failure between any of those brazing joints it can lead to failure of the unit. Although our goal is not to make a sort of comparison between traditional manufacturing processes and AM processes, it’s fair to say that on a practical level, AM brings a number of pros that are hard to not mention: the ability to manufacture heat exchangers as a single component, the ability to manufacture smaller, lighter objects, more efficiently…However, all of this comes with its own share of challenges.
From design to production: what the manufacturing process looks like at Conflux
Conduction, convection and radiation are the three modes of heat transfer. Their relative importance varies with the exchanger and operating conditions. The design must also account for additive manufacturing, post-processing and inspection constraints.
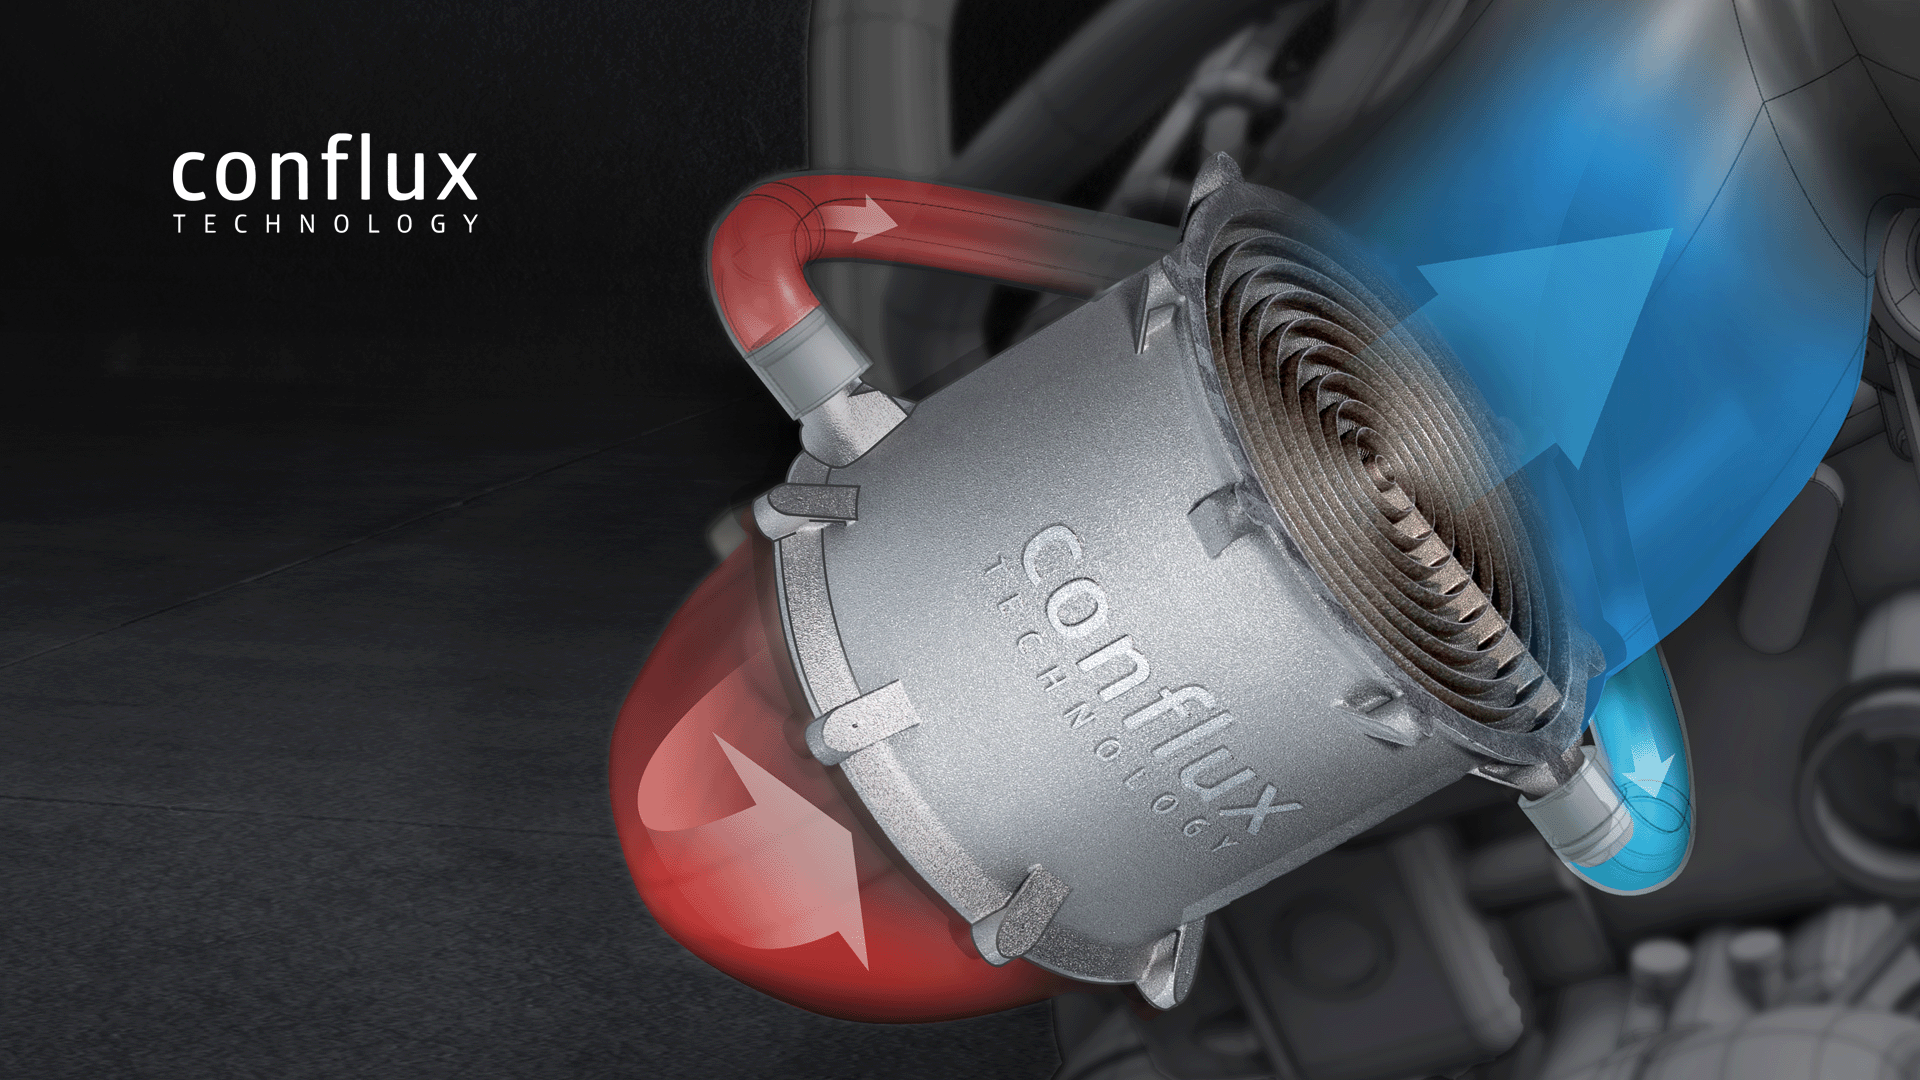
“We have our own series of product families, which are created based off market research and market understanding of what our customers’ pain points are, some of these being they need relatively off-the-shelf, yet highly configurable products. The problem definition is where we start our design process. We’ll then go into either concept selection or an ideation process where we have engineers that are experts in first principles, calculations and multi-physics modelling. We also have design engineers that have got a lot of history in CAD modelling. We run our physics modelling simulations on an in-house, high-performance compute cluster, and utilize the best tools such as CATIA for our CAD modelling. We also have these teams working with the AM process engineers that are in house as well”, Conflux’ CEO explains.
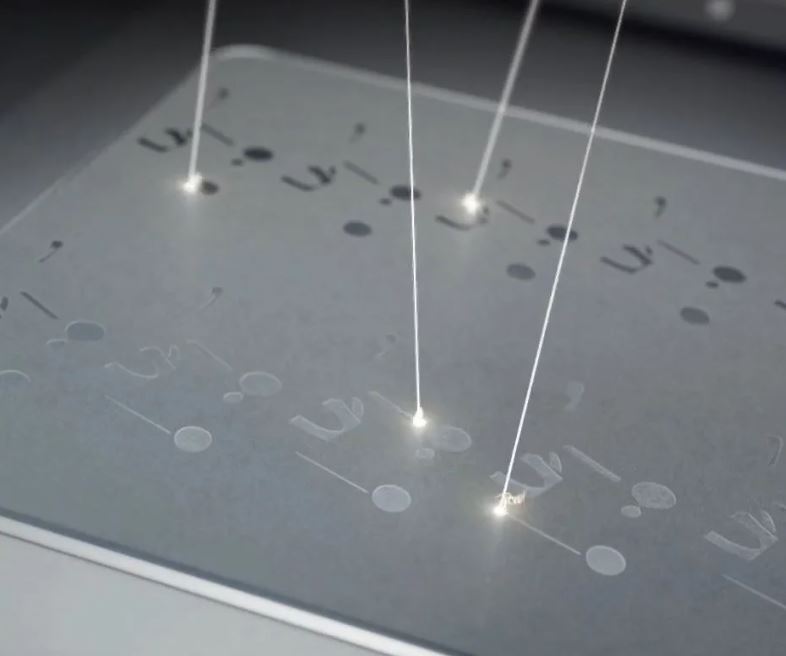
As far as manufacturing is concerned, Fuller first recalls that “the heat exchanger has intricate geometry with very thin walls, and fine feature distances. Quite often these are internal geometries within the device.” “And so what we needed to do was make sure that we had a technology that could print very dense structures, so highly dense that we could have gas type walls separating different heat transfer fluids. We also needed to make sure that we could remove any residual material from the manufacturing process that could be removed completely. Therefore, if you are looking at electron beam melting, this is not suitable, because you can’t get the thinness of walls that you need and you can’t get the internal powder out without having some pretty elaborate processes. With the metal binder jet process, this results in a lower density”.
These observations describe Conflux’s process selection for its geometries and resources in 2022. They do not mean that all binder-jetted parts have low density or that electron beam melting is excluded from every thermal application. Leak tightness, minimum wall thickness, surface condition and powder removal must be validated for each design.
This selection led Conflux to choose laser powder bed fusion of metal, or LPBF, for the applications described. The aim is to achieve the required thermal performance while allowing residual powder to be removed.
Thin-walled internal structures can increase the available heat-transfer area. The interview discusses wall thicknesses of 0.1 mm or less: this depends on material, geometry, orientation, parameters and inspection. It is not a guaranteed capability of every LPBF machine. Developing these parameters is part of Conflux’s process engineering work.
Another interesting advantage that is very often highlighted is the technology’s ability to deliver lighter parts. The advantage is so common to most AM applications that it might be easy to think that it’s an absolute must in all “heat exchangers” applications. Fuller said no to this misconception:
“A lot of heat exchangers, sit on the ground, and might be mounted to large concrete slabs on the ground. Heat exchangers in the energy generation industry, or in large scale renewables, or in the nuclear industry might be as big as a house, making it smaller in that case can be advantageous because there’s less real estate required, but in terms of light-weighting it’s not all heat exchangers applications. If you look at different industries then you can start seeing where light weighting is important; aerospace, automotive, particularly in the motorsports sector of automotive, increasingly more and more Electric Vehicles. Anything you can do to reduce weight results in fundamental energy efficiency. If you’ve got less weight, then you need less energy to move the thing around. And, you know, laptops, if they can be lighter, then that’s better.”
Challenges and objectives described in 2022
In 2022, announced collaborations with Dallara Automobili and GKN Additive illustrate the markets being targeted. Fuller nevertheless highlights commercialisation challenges following investment in research and development. “The industrialization of additive manufacturing is still quite nascent, and the cost of machines are still very high. One of the biggest challenges is making sure that we design and manufacture solutions for customers and markets that are in the right sweet spot for the sort of industrial maturity of the enabling technology which we’re doing”, Fuller notes.
According to Fuller, productivity is improving and costs are declining at the time of the interview. Conflux’s applications are not yet producing hundreds of thousands of units a year, however. The company is working to reduce cost per part further; this outlook is not a measured result for the sector as a whole.
In the outlook described in 2022, we could see Conflux apply the expertise they have built so far to other areas – an expertise that is characterized by “thin walls and high resolution geometries” as per Fuller’s words. Somehow, it was already being explored in 2022, as one of their clients who completed a project on heat exchangers with the team is now working with them on building substrates for catalytic converters in emissions reduction technology. “So, there is transfer there from the sort of expertise in high resolution AM geometries”, Fuller comments.
For the nearer term, Fuller outlined the following expansion plans in 2022:
“We’ve been lucky to have a first phase of the business housed at the back of Deakin University in Waurn Ponds, Geelong. They have a large parcel of land which is sectioned off for advanced manufacturing where young, advanced manufacturing businesses like Conflux can spend the first number of years getting settled, which is what we’ve done for nearly five years [now]. We’ll move at the end of this year to a larger facility with more production capacity as well as more testing capabilities.
We’ve got boots on the ground now in our key customer regions, with people based in Japan that are covering Japan, Korea, India, and non-Australia Asia region. We have a person based in Central Europe, just outside of Munich and we are also just about to have someone start in North America. So we’re getting a global footprint underway. This is so that we can be near our customers, so we can share time zones with our customers, which is quite tricky from Australia. This is really an expansion on all fronts, but our commercial activities will increase significantly in the coming 12 to 18 months” the CEO of Conflux Technology concludes.
This interview was first published in the July/August 2022 issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.