

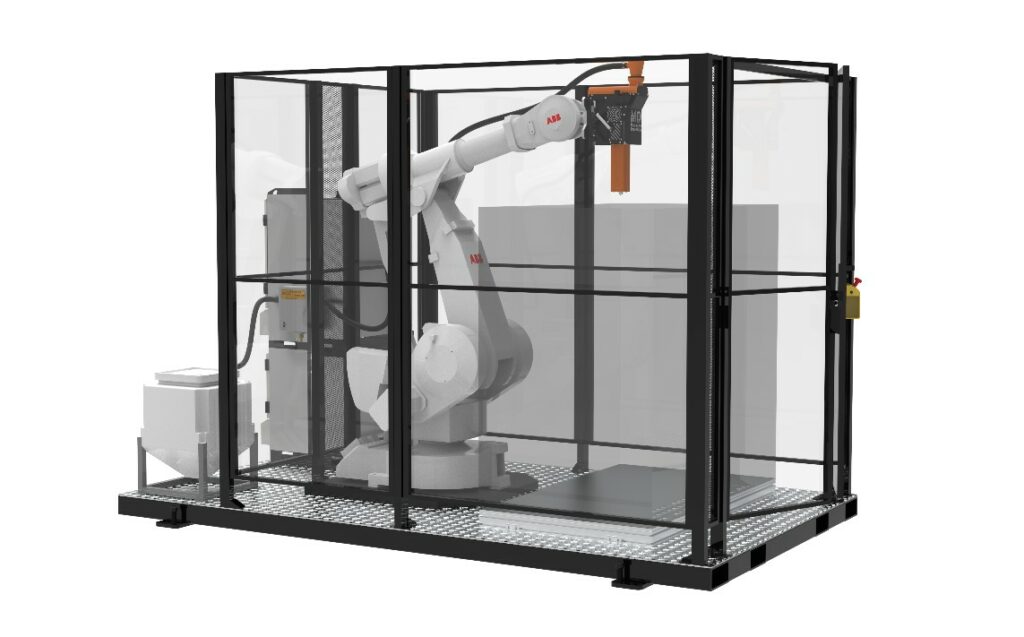
A 2023 feature with Tyler McNaney (Massive Dimension) and Justin Ferguson (Autodesk). Examples and job titles reflect that period; the supplier overview is not an updated catalogue.
Combining a robotic arm and a deposition head can enable large parts and complex toolpaths. Reach, accuracy and repeatability nevertheless depend on the complete cell. This feature examines the approach’s possibilities and the challenges of industrial adoption.
This article concerns robots used to deposit material and their role in an additive manufacturing workflow, rather than industrial robotics as a whole.
Robotics and 3D printing can be combined in two main ways.
One approach combines a deposition head with a multi-axis robotic arm. Robotic additive manufacturing (RAM) can use polymer, ceramic-paste or concrete extrusion, as well as metal deposition. Material and energy source determine the process. Many arms have six axes, sometimes supplemented by external axes; gantries are not universally limited to three axes.
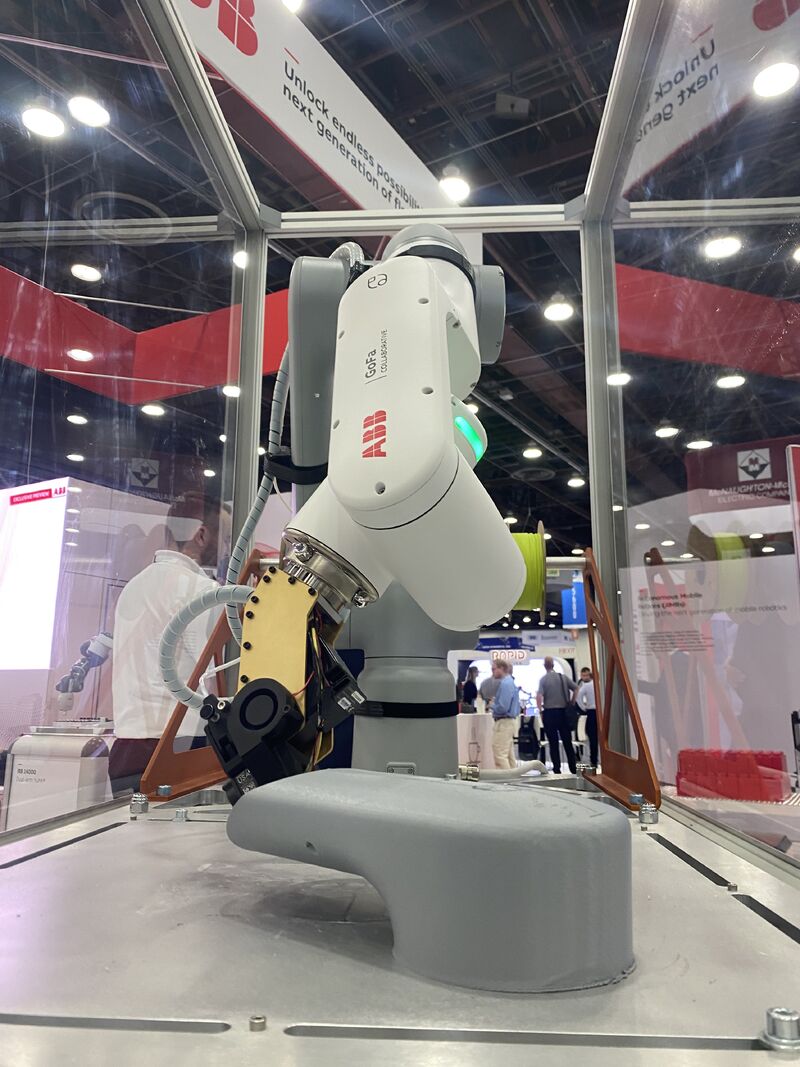
“There are many different types of end-of-arm tooling for robots for a 3D printing application. [They] range from thermoplastic, metal injection molding, ceramic to concrete systems [and more]. [They can be] optimized and built specifically for additive and robotic printing applications,” Tyler McNaney, Founder and Managing Director at Massive Dimension explains.
“Robots are very customizable and versatile. A single robot could be placed on a static pedestal and the print might move, or the robot could be made movable and the part is stationary. Both of these could change the DFAM, depending on the process. Let’s take for instance the buckling that can happen when printing a large part vertically: it may be necessary to create buckling mitigating features on the part. If the part has the ability to be printed on its side or upside down, then the physics of gravity on the part may impact the need for, or design of, these features.
Furthermore, robots can very easily be configured with multiple end effectors, thus it is very easy to repurpose a robot. This means someone who starts with a wire arc end effector can keep the same robot and change to a laser powder process. Imagine doing that with a powder-bed machine!
This also allows us to look toward multiple dissimilar materials being printed on one cell, like a plastic or elastomer on a metal – things that might normally be done with a plastic injection process.
Robots are not as precise as what we’ve come to see as the standard for AM, powder bed machines or SLA machines. Recognizing this inaccuracy at the design level, and that post-print processing will be required, is necessary,” Justin Ferguson, Autodesk, Senior Solutions Engineer adds.
That flexibility must be assessed at cell level: a process change requires compatible supplies, controls, calibration and safeguarding. Achievable accuracy also depends on stiffness, load, toolpath and process; the presence of a robot alone does not establish a ranking against every powder-bed or vat-photopolymerization machine.
On another note, 3D printing and robotics can also complete each other when one is looking to establish an integrated solution throughout the manufacturing process. In such cases, an industrial robot could replace a manual step of the manufacturing process. It could be replacing a 3D printer’s build plate or performing the washing, curing and final finishing steps in post-processing with robotic arms.
“A robotic additive printing solution is very flexible in terms of customization; the initial printing setup can be customized beyond what it was originally designed to produce. For example, a robotic printer could have one work volume on a fixed surface, in another location, a rotary positioner could be added, and furthermore, additional build areas can be installed for specific part build requirements. Within the printing process various deposition tools can be added to the end of the robotic arm, as well as post-processing tools such as mills, sanders, or other finishing tools,” McNaney outlines.
A double-edged sword
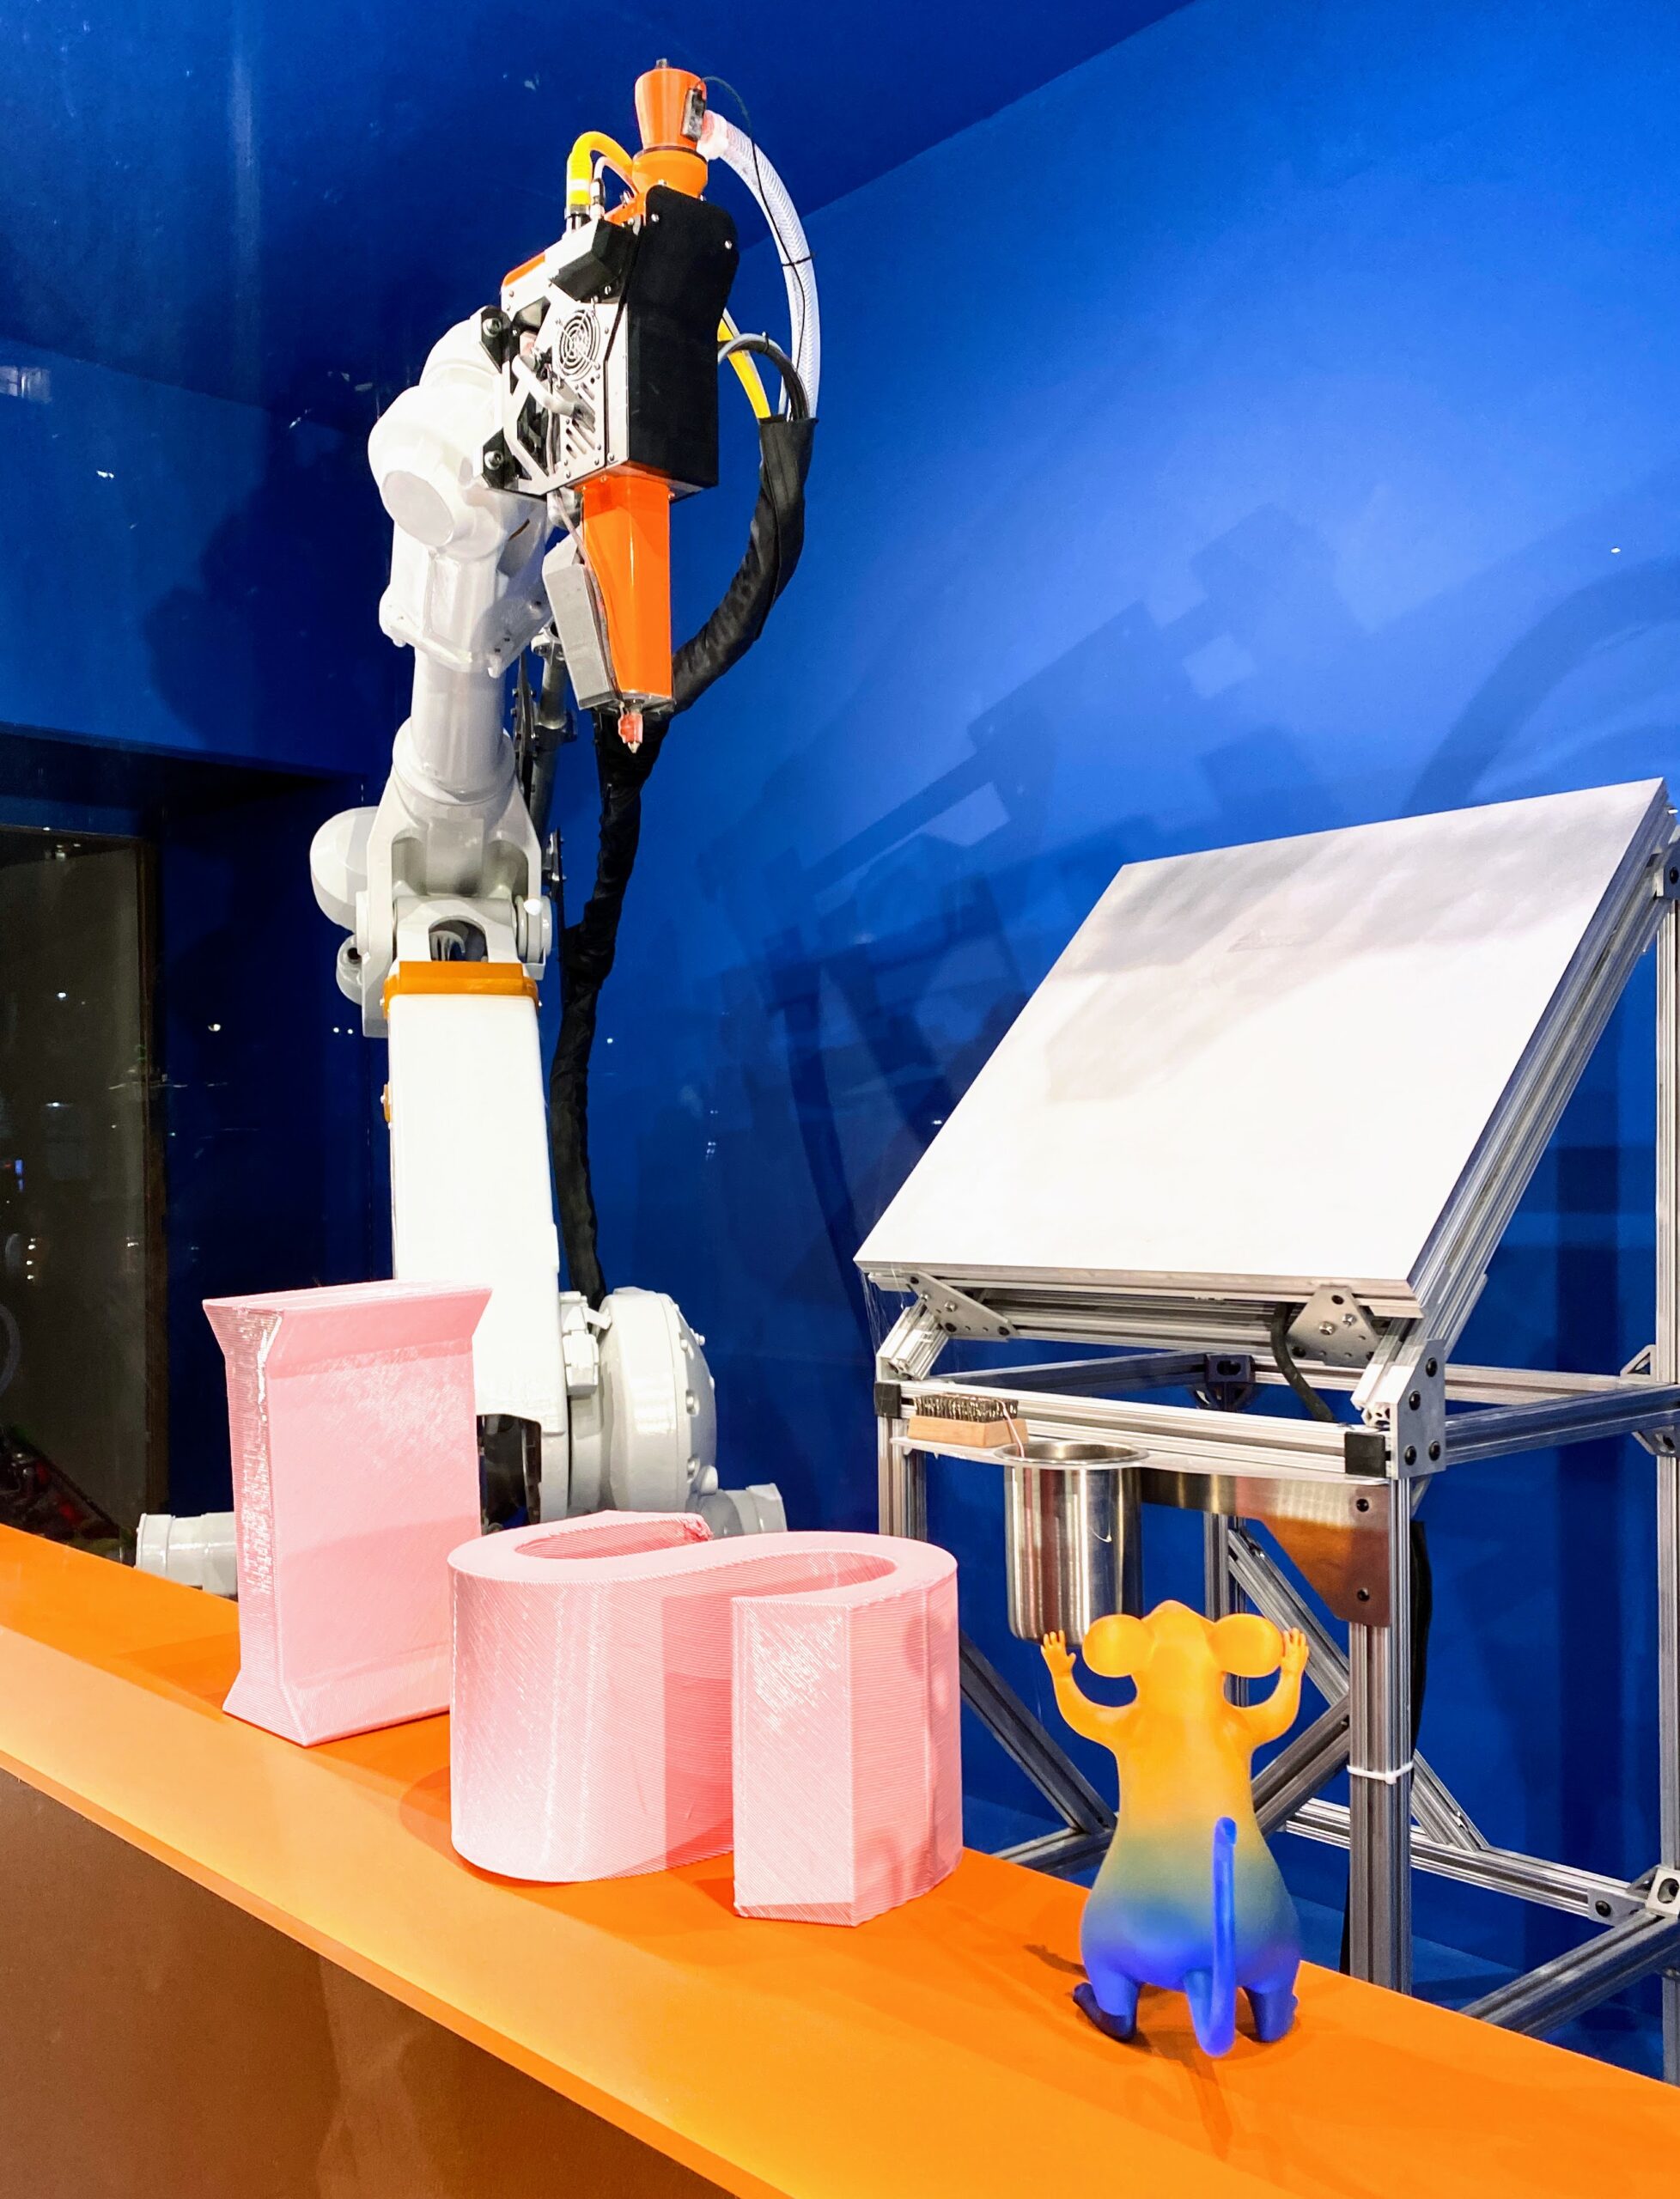
Arm joints and positioners can reorient deposition. For some geometries this reduces support structures or material use, but it does not automatically eliminate supports. Head access, deposit stability, gravity, collision avoidance and material behaviour remain relevant.
Here is the thing, these advantages can be a double-edged sword as with so many moving parts, the machine would need detailed computer instructions to meet the manufacturing requirements. Indeed, improper planning and control can influence the printing quality or can lead to the arm hitting the printed part, causing damage. Not to mention that the robot’s motion control systems can also influence the part quality or effectiveness of the printing process.
“Where a conventional XYZ printer can only build up, a robotic movement system can reach down after building an object; robot system can be quickly adapted for a range of printing methods such as non-planar, multiplanar, and angled printing,” McNaney points out before warning on the design considerations that should be taken into account: “features should be designed within the nozzle diameter size and should not exceed the capabilities of the printer or materials just as like desktop printing.”
Moving from CAD geometry to robot code requires software compatible with the controller, head and external axes. Formats and tools exist, while post-processors and integration remain configuration-dependent. OCTOPUZ already described CAM path import, simulation and robot-code generation in 2022; this is not a field without exchange solutions.
Toolpath preparation needs to account for the growing part and motion limits. Simulation helps detect collisions; shrinkage and distortion also require material and process knowledge. Software alone does not guarantee collision-free or defect-free production.
Applications and suppliers cited in 2023
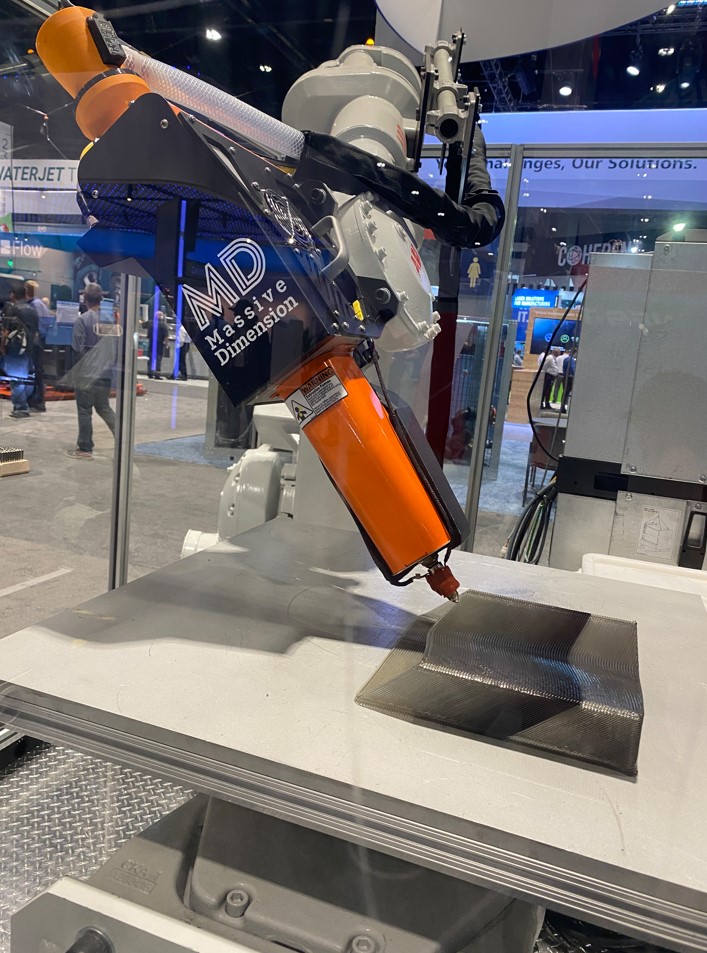
Hulls, bodywork elements, large moulds and tooling are among the applications considered or produced using these systems. Suitability depends on material, geometry, finishing and service requirements. A rotationally moulded object cannot automatically be replaced by a printed part.
The ecosystem includes software, deposition-head, robot-arm and complete-cell suppliers. An organization may cover more than one role. The selection below retains the names cited in the 2023 feature, classified by their principal role.
This is a non-exhaustive selection, not a service-provider directory or performance ranking. Availability of offerings should be checked with the suppliers.
| Software | Deposition heads and extruders | Robot-arm manufacturers | Robotic printing systems and solutions |
|---|---|---|---|
| ADAXIS | Weber Additive | Comau | CEAD AM Flexbot |
| AiBuild | Massive Dimension | ABB | MX3D M1 |
| Robotmaster | Dyze Design | Stäubli | Caracol |
| OCTOPUZ (OLRP) | Rev3rd | KUKA | Continuous Composites |
| RoboDK | Bloom Robotics | — | Vertico (concrete) |
| — | — | — | Orbital Composites |
| — | — | — | Twente AM (concrete) |
| — | — | — | Hyperion Robotics (construction) |
The business case needs to include the arm, head, software and integration, alongside calibration, safeguarding, training, maintenance and inspection. Some offerings combine several elements; others need integration between suppliers. Total cost depends on the project, utilization and intended parts.
Supplier collaboration can facilitate integration. Toolpaths, process, safety and part quality still need validation under actual production conditions.
This article has first been published in the May/June edition of 3D ADEPT MAG.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.