

Feature first published in the May/June 2022 issue of 3D ADEPT Mag. Interviews and commercial announcements reflect that period. The final interview concerns pure tungsten, which is distinct from WC-Co hardmetals.
Hardmetals combine a hard ceramic phase with a metallic binder. Their resistance to wear makes them valuable for tooling and demanding components, but adapting them to additive manufacturing presents challenges in shaping, densification and control of material properties.
Often called cemented carbides or sintered carbides, – often written “hard metals”, hardmetals are simply composite materials that are made up of a hard phase embedded in a metal matrix. Their development within additive manufacturing was a topic of this 2022 investigation and before we delve into its technical advancements, it feels right to clarify that their appellation often varies from one region to another. “In the US, the wording “cemented carbides” and “cermets” are often the most-widely used ones while hard metals or hardmetals are the preferred wording in Europe”, Dr. Johannes Pötschke, Group leader hardmetals and cermets at Fraunhofer IKTS told us from the outset.
Terminology varies, but cermets are a broader family of ceramic–metal composites; the terms are not interchangeable for every composition. This feature focuses on cemented carbides, particularly tungsten carbide–cobalt (WC-Co).
However, with the goal of remaining faithful to its origins, we would keep the wording “hardmetals” in this feature – which comes from the German word “Hartmetall”.
Anyway, these pioneering powder metallurgical materials refer to a category of materials that are sintered, hard, and wear-resisting. They are based on the carbides of one or more of the elements tungsten, tantalum, titanium, molybdenum, niobium and vanadium, bonded with a metal of lower melting point usually cobalt. Here, Tungsten carbide-cobalt (WC-Co) remains the most widely used hardmetal. “It is an alloy of a hard ceramic phase, tungsten carbide (WC) and a ductile metallic phase, cobalt (Co). In other words, this metal matrix composite is made up of cobalt particles embedded in a tungsten carbide matrix”, Pötschke adds.
For clarity, in WC-Co the hard WC grains are bonded by the metallic cobalt binder. The final sentence of the quotation above reverses these roles. WC-Co is a composite rather than a homogeneous alloy.
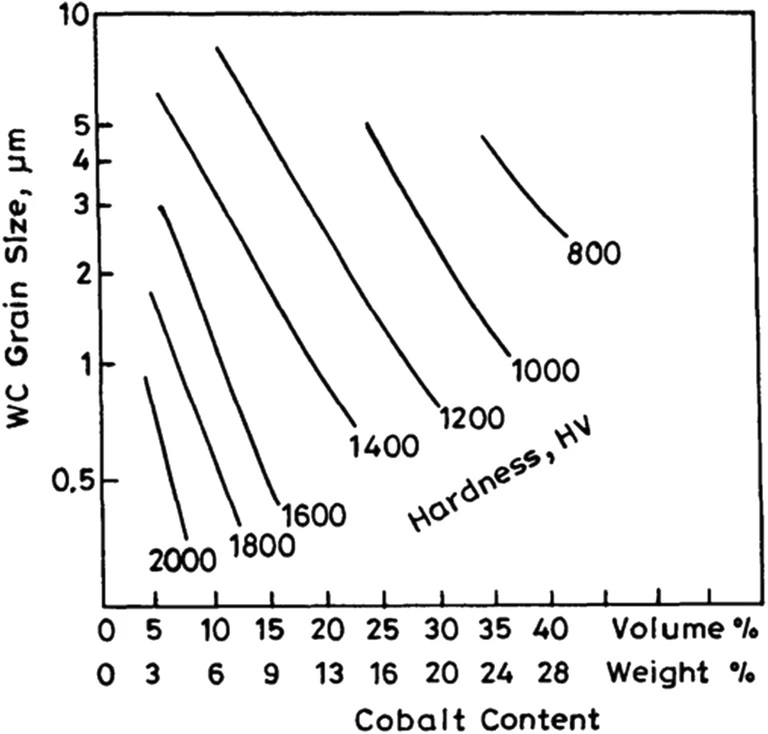
Hardness is one selection criterion, alongside fracture toughness, strength and behaviour under the intended loads. A material’s suitability cannot be inferred from hardness alone.
Hardness describes resistance to local indentation or scratching; it is distinct from bending strength and fracture toughness. The original feature cited upper values of 20 GPa, 5,000 MPa and 20 MPa·m1/2, respectively. These figures should not be treated as simultaneous properties of a single grade or as guarantees for printed components: the original text did not identify a common grade, test method or set of conditions. Composition and processing must be specified when comparing results.
Conventional powder-metallurgy routes shape a green compact and subsequently densify it by sintering. Finishing operations may then be needed to obtain the required geometry and surface condition.
Conventional pressing limits some geometries, and machining hardmetal can be demanding. Low porosity is generally a quality objective, not a defect. AM offers additional design possibilities, but the whole process must deliver the required density, dimensions and mechanical properties.
AM processes explored for WC-Co hardmetals
It’s easy to talk about AM in general because the same advantages tend to come back. What makes the conversation about AM captivating, is the nuances that may occur during the use of a specific AM process with a certain material, or for a given application.
The material–process combination matters: a process demonstrated for steel or titanium does not automatically work for WC-Co. In particular, intense heating can change the carbon balance and cobalt content, while cracking and porosity remain concerns.
According to Dr. Johannes Pötschke, many projects were under way at the time of the interview, and most of them involve the use of WC-Co hard metals on binder jet 3D printing and sinter-based AM processes in general.
Interestingly, with binder jet 3D printing, the “green part” obtained right after the manufacturing process can have enough strength to withstand the debinding step during which the polymer binder material will be removed before going on to a sintering process that will form a stronger and dense part. The only thing is that, given the fact that the manufacturing process requires a powder spreading step, the flowability is critical to the success of the printing operation.
Other additive manufacturing processes have been explored to process WC-Co hardmetals as well. They include SLM, Electron Beam Melting, 3D gel printing and FFF. While each of them presents its share of advantages and disadvantages, one thing we will keep in mind is that there are still a wide range of mechanical properties issues to address to deliver viable WC-Co 3D printed parts.
Indeed, in an AM production that involves WC-Co, density is a primary indicator for quality. Other indicators are related to the aforementioned main properties of hardmetals: hardness, fracture toughness and bending strength.
“The almost unavoidable defects, such as micro-cracks and porosities, and lack of dimensional accuracy, prevent AM processes from being widely used for producing WC-Co parts in the industry. Post-processing, such as heat treatment, hot isostatic pressing (HIP), infiltration, and machining, are often required, resulting in additional time and cost”, a research on “Additive manufacturing of WC-Co hardmetals” reads.
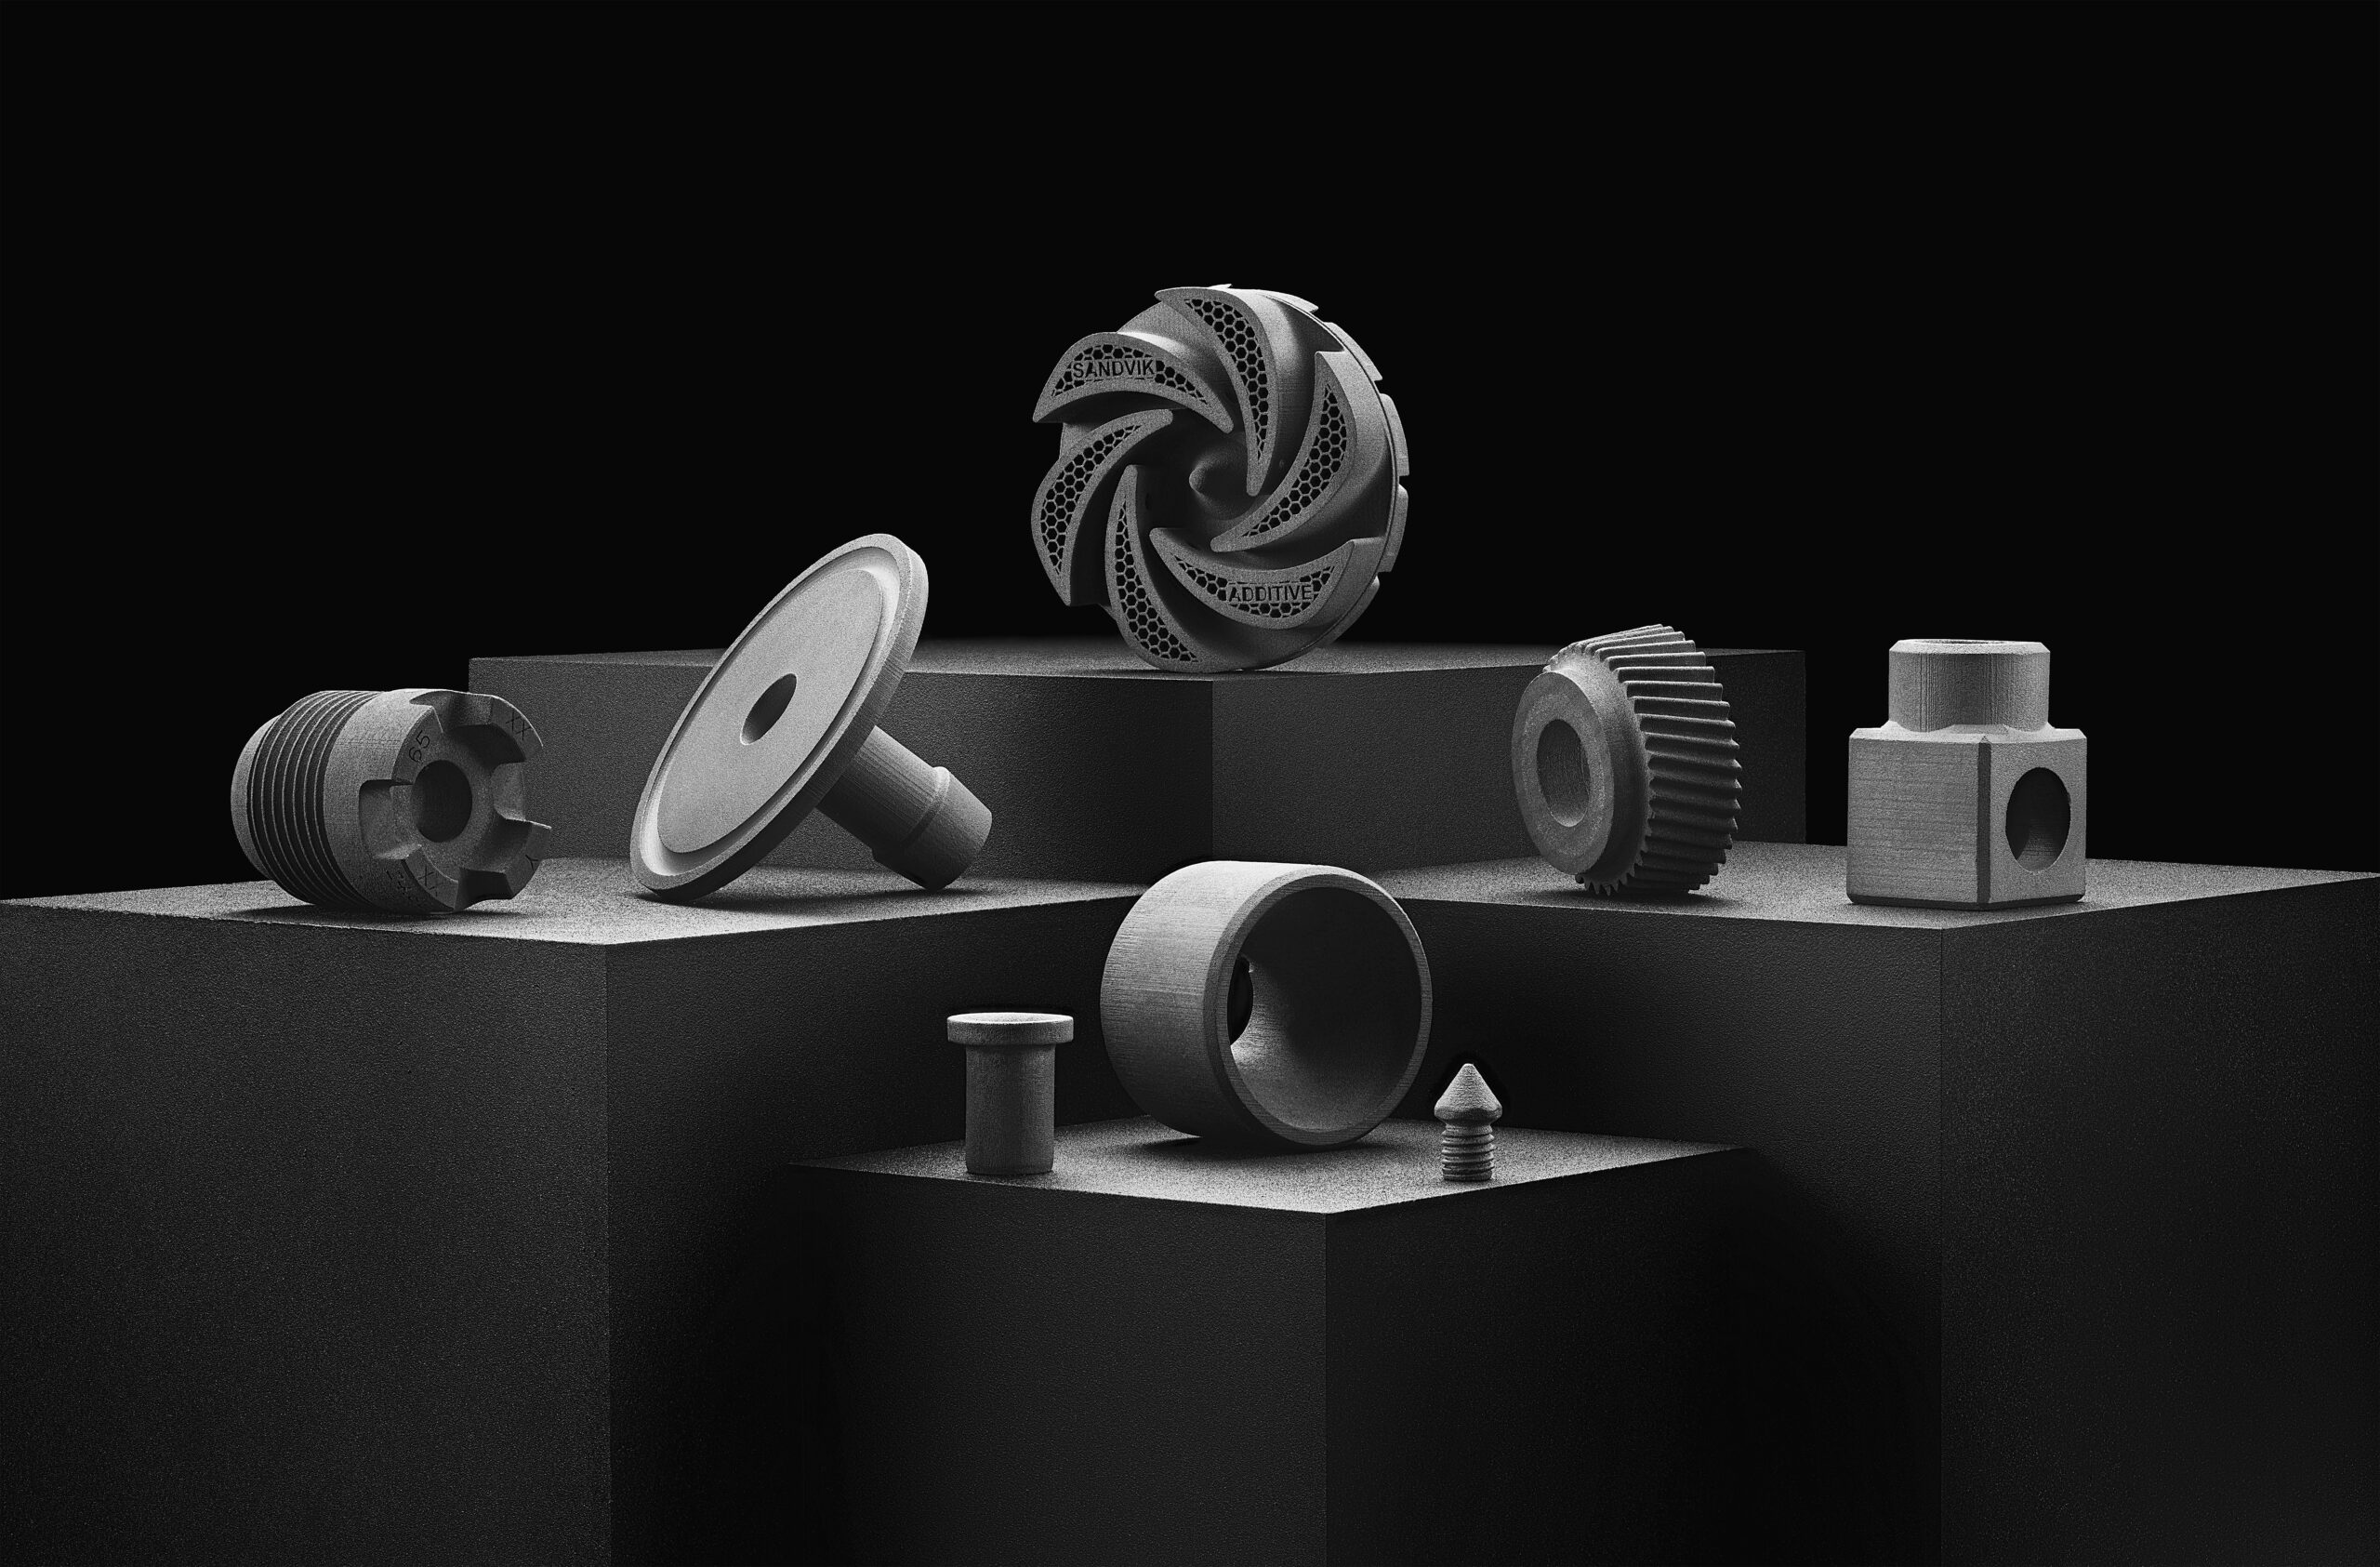
In April 2022, Sandvik announced 3D-printed cemented-carbide components using a proprietary process and tailored powder. The company was also involved in GE Additive’s binder-jet development programme, which Kennametal had joined. These announcements provide commercial context; they do not establish that every WC-Co process or application had reached the same maturity.
| Process | Potential | Points to verify |
|---|---|---|
| Laser powder bed fusion (L-PBF / SLM) | Complex geometry; direct shaping by selective melting. | Cracking, residual stress, microstructure, carbon loss and cobalt evaporation. |
| Electron-beam powder bed fusion (E-PBF / SEBM) | Selective melting using an electron beam. | Vacuum operation, equipment requirements and material-specific results. |
| Binder jetting | Shaping without melting during printing. | Powder spreading, green-part handling, shrinkage and final properties after sintering. |
| 3D gel printing | Shaping a powder-containing slurry. | Formulation, drying, shrinkage and densification. |
| Fused filament fabrication (FFF) | Shaping a powder-filled filament. | Feedstock, layer structure, debinding, shrinkage and surface finish. |
These are process considerations, not a ranking of grades. Claims of no material loss, universally high hardness or uniformly low cost would require evidence for the particular production route.
“In summary, the above five additive manufacturing processes can be divided into two types: selective melting process and shaping-debonding-sintering (SDS) process. Selective melting processes include SLM and SEBM, which make parts by melting powder with a heat source. This type of process is very simple and enables one-step molding. But sometimes post-processing is needed to eliminate stress and defects. The SDS process includes Binder Jet 3D printing, 3DGP, and FFF. The SDS type processes are characterized by forming a green part with organic compounds as binder and then sintering. Compared with the selective melting process, the SDS process is more complicated. Because SLM, SEBM, and BJT all contain a powder spreading step, all three processes require the powder to have good flowability. While 3DGP and FFF prepare powders as slurry and filament for printing, there is no need for powder flowability. The application of SEBM is limited by its very high equipment cost. SLM suffers from uneven microstructure, carbon loss, and evaporation of Co”, the research lays emphasis on.
Here, the binder-removal stage is debinding. The distinction concerns how the shape is formed; it should not be read as a promise that melting-based production delivers a finished, qualified part in one step.
What about applications?
“There are currently no commercial applications made possible via AM and hardmetals. Most projects are being conducted right now for prototyping or research purpose. One notable advancement is that sinter-based AM processes are ahead of the curve since they can meet the stringent requirements of hardmetals [assuming that the operators know how to deal with concerns raised by material composition, production speed, accuracy and desired part size]”, Pötschke told 3D ADEPT Media.
This was Pötschke’s assessment at the time of the interview. It is not an exhaustive statement about the market: Sandvik’s April 2022 announcement described commercial-scale capability, while individual uses still require qualification.
Conventional hardmetal uses in cutting tools and wear-resistant components provide potential directions for AM. Valves, nozzles and tooling are examples, but choosing AM must be justified for the geometry, production volume and service conditions.
Most importantly, in the medical and healthcare industries, Pötschke told us that hardmetals are mostly used with conventional manufacturing processes:
“Given the fact that they deliver the ideal [compromise between toughness and hardness], hardmetals are ideal for the fabrication of cutting tools. In the medical industry, they can serve applications in dentistry and bone tissue machining.” In a separate application area, Dunlee uses pure tungsten for medical 3D printing applications.
The following questions turn to pure tungsten and X-ray-related applications. Pure tungsten is a refractory metal; it is not the WC-Co composite discussed above.
If you are a regular reader of 3D ADEPT Media, you may have already discovered the company through our Opinion of the Week segment. In this exclusive feature, we have asked Jan Philippe Grage, Product & Business Development Manager 3D Printing at DUNLEE to answer a short list of questions that may help us understand how (fast/slow) this niche market evolves.
3DA: Has Dunlee only explored the use of tungsten for anti-scatter grids (ASGs)? (Are there any other applications?)
Our core business is anti-scatter grids and that is also what will be a driving force of our developments in the future. However, Dunlee is also actively providing components for other medical applications such as shielding windows or collimators for X-ray tubes. Going further we are also working on new applications outside of medicine, such as nuclear fusion, aerospace, automotive or even the mining industry. This is due to tungsten:
- high melting point making it ideal for extreme temperature environments
- High density making it ideal for radiation absorption or as a counterweight in small or complex geometries
- Long lifetime and resistance to corrosion
3DA: While there are many advantages to additive manufacturing with tungsten, there are obstacles to scaling the technology for mass production. In most cases it takes longer and is more expensive to make parts. How can we address this issue?
Indeed, there are cases where additive manufacturing is just not a fit in terms of price, scalability or even performance. Yet, there are still so many untapped opportunities where additive manufacturing can support production of components at volume, the right mix starting with part evaluation and design all the way to post processing need to be found. This takes time and effort but as can be seen with our major application, ASGs, is worth the development. Therefore, for companies entering these kinds of developments, they need to set the right expectations and understand that delays or even an unsuccessful investigation could be the result. When it comes to scaling, I believe a big element is finding the right partners. Partnering up within the AM field is key as many developments and potentials have not been unlocked yet, therefore you need partners across your value chain that constantly look to develop and invest the time required in order to continuously improve.
3DA: Are there any other hard metals the company has explored for medical 3D printing applications?
Till today, our strategy is to focus on pure tungsten and develop this niche metal industry. Of course, we receive requests for other refractory metals but we either managed to develop the application with tungsten or deemed the relation between that application and our capabilities a no match. We do however have it on our agenda to assess every new material opportunity that comes our way to see if there is a match.
3DA: Is there anything else you would like to share regarding the use of tungsten with AM?
For those looking into AM tungsten parts for the first time, do understand it is still not an easy task. We may be producing hundreds of thousands of parts a year but every new application has its challenges and for those new developments may be required. So do not shy away at hearing what needs to be developed first, the potential for tungsten in AM can save you costs, increase system performance or even a combination of both. What is increasingly being seen as well in the market is the opportunity to become more sustainable than with traditional manufacturing. With AM it’s possible to have much smaller supply chains and can close the loop on material usage/wastage. Especially in these times, where supply chain pressure is high and everyone is facing material shortages, recycling and circular economies are becoming that more important.
This feature was first published in the May/June 2022 issue of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.