

Feature first published in the August 2019 issue of 3D ADEPT MAG, then online in July 2021. Job titles, machines and practices reflect the 2019 interview.
In industry, pilot production tests a product, its manufacturing methods and its controls before scaling up. How does a 3D printer manufacturer organise this stage? And how can FDM support pilot runs of other products? MakerBot shares its experience.
MakerBot’s experience illustrates both uses without establishing a universal procedure.
Founded in 2009 by Bre Pettis, Adam Mayer and Zach “Hoeken” Smith, MakerBot is an American desktop 3D printer manufacturer. Its merger with Stratasys was completed in 2013. Education is among its application areas.
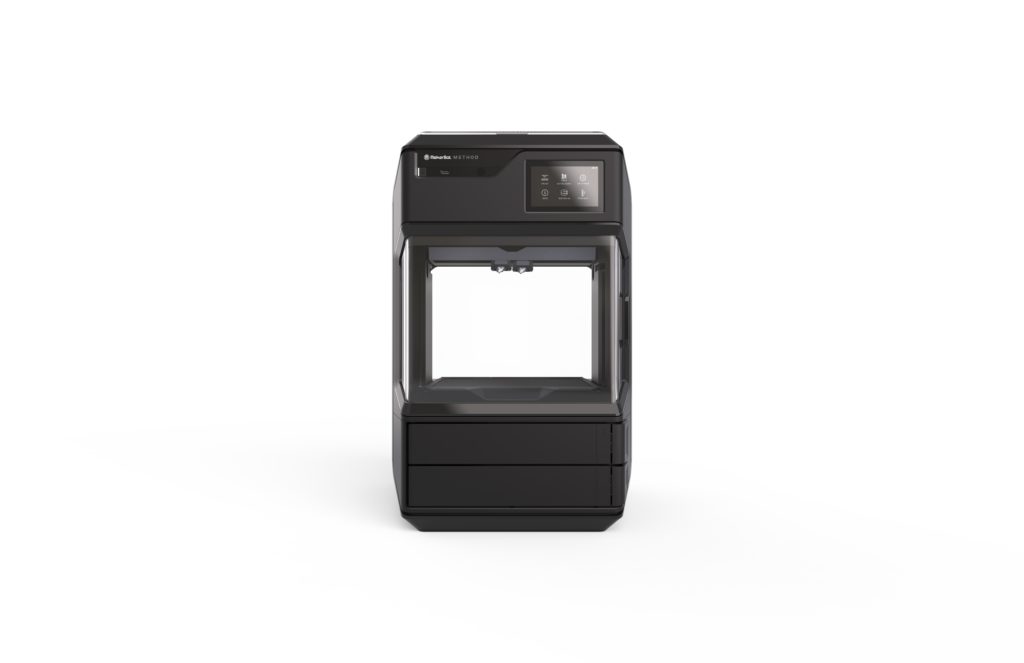
At the time of this interview, Nadav Goshen led the company. The METHOD range and METHOD X announced in August 2019 focused on controlled printing conditions and materials for professional applications.
Dave Veisz, then MakerBot’s vice president of engineering, discusses printer development and the criteria for choosing FDM for pilot production.
Pilot program of a 3D Printing system
Beyond new-machine announcements, a product’s validation process helps explain its maturity.
Test methods, unit counts and controls provide useful evidence when assessing an offering. Their relevance depends on the protocol and the requirements being addressed.
A pilot programme investigates how larger-scale production could work. Its organisation depends on the product, risks and manufacturing resources; the example here is not a standard for every manufacturer.
In May 2017, Impossible Objects announced Model One, its composite-based additive manufacturing (CBAM) system, with a pilot programme involving Jabil and other unnamed customers.
Dave Veisz then describes the stages followed for METHOD:
“In the development of the MakerBot METHOD 3D Printer, for example, there were several milestones build and test cycles leading up to the start of serial production and shipping. The initial builds are using primarily prototype (3D printed plastics, machined metals, quick turn electronics), but as the design matures, the builds become more production representative and consist of a mix of tooled parts and rapid prototyped parts, and the numbers of units increase so that more thorough testing can be performed.
For a new platform like METHOD, a “pilot run” for MakerBot is generally at least 100 full assemblies so that we have enough units to perform statistically relevant testing for reliability and performance as well as the manufacturing process and in-line quality control. One unit may be adequate for proving out early stage proof of concept, but for a Pilot run, the quantity needs to be enough to sufficiently test the variability in part quality and the manufacturing process”, explains Dave Veisz.
This account concerns METHOD development at MakerBot. The 100-assembly threshold is the company’s reported practice, not a mandatory minimum for every pilot run.
Now, before the launch of a consumer product, are processes exactly the same?
FDM 3D Printing and the launch of new products
FDM serves education, prototyping and selected end-use applications. Its suitability depends on material, geometry, tolerances and application requirements.
“FDM printers are used in primary schools to introduce students to design thinking and other STEAM topics, but are also used to produce end-use aerospace and defense parts that have extremely demanding requirements. Therefore, FDM printers cover a very wide range of use cases. FDM printing is a great introduction to 3D printing because it is an accessible and safe 3D printing process that does not require hazardous chemicals, or secondary processes to create a usable part quickly” said MakerBot Vice President of Engineering.
Technical clarification: this manufacturer assessment does not mean risk-free operation. NIOSH work published in 2018 measured particle and volatile-compound emissions during filament printing. Material, temperature, ventilation and suitable controls still need consideration.
Small-run tooling can be costly, especially when designs change. Market and manufacturing trials help identify problems before committing to larger production volumes.
3D printing can avoid dedicated mould tooling for selected small runs. Preparation, supports, post-processing and inspection still carry costs. For Dave Veisz, FDM’s value depends on both part requirements and production economics:
“Many companies are doing this in addition to using FDM 3D printers for the production of serial production parts. The main criteria are the requirements of the part (material properties, mechanical loading, etc.) to determine if FDM is the right technology in terms of capabilities, and the second consideration is economics. FDM is easy to justify for high mix, low volume production as there are no large expenditures or lead times for tooling in FDM parts in comparison to molded or other near net shape processes.
However, as volume goes up, dedicated tooling becomes more justifiable over FDM due to generally lower piece prices over the life of the product. Another point to make here is that there are part geometries that are possible to create in FDM that are not possible to create by traditional manufacturing methods. This includes designs with internal voids or variable cross-sections and dynamic “print-in-place” assemblies. Thus, high-tech industries like medical, aerospace, and advanced manufacturing are designing production parts that take advantage of the freedom of 3D printing and reducing part counts, improving strength to weight ratios, and achieving other advantages that justify the use of FDM in manufacturing production parts.”
FDM can therefore support iteration and market testing. Cost and lead-time benefits must be assessed for the particular product and volumes.
The next question that crosses our mind then is to know the characteristics of ideal FDM 3D Printers for pilot production.
Key features to consider when choosing FDM 3D Printers for pilot production
Selection criteria include build volume, temperature control, interlayer adhesion, supports, infill, wall thickness, compatible materials and post-processing.
As far as printer parameters are concerned, from a designer’s perspective, build size and layer height are very important.
Warping is influenced by shrinkage and thermal gradients. Build-plate adhesion, geometry, material and temperature control affect the risk. Choosing a printer simply because it has a large flat surface does not solve it.
Infill, walls, orientation and material affect part properties. Filaments include PLA and ABS, PA, TPU and PETG, and selected PEEK or PEI grades on suitable equipment. Not every FDM printer can process these high-temperature materials.
Finishing can include sanding, polishing, painting or specialist treatments compatible with the material. Chemical processes, coatings and metallisation require suitable conditions and controls; they cannot be applied interchangeably to every polymer.
Selection therefore concerns the complete machine–material–process combination and its repeatability for the intended part. Performance observed on one configuration does not automatically transfer to another.
Dave Veisz emphasises the fidelity and repeatability of the resulting part:
“The ideal characteristics of FDM printers are the incorporation of controls and features that enable the user to print accurately, repeatedly, and reliably. You need to be able to trust that the 3D printed part is an accurate representation of the design and that the part will have the same properties each time it is printed. In manufacturing, variability is the enemy, so you want a printer that has enclosed, sealed material bays to keep material dry and an enclosed, temperature-controlled chamber so there is consistency in the quality of the print regardless of the environment. Material capabilities per printer platform vary, so that will be consideration.
The other consideration is whether support material is required and the type of support (breakaway vs. soluble). With soluble support, it is possible to print geometry with voids and small support inclusions whereas certain geometries are not capable with breakaway support. There is a wide variety of cost options and the claims that manufacturers are making can be confusing. There is a difference between being able to print a material, and being able to print a material accurately and repeatedly. Accuracy and repeatability really do require the “industrial” feature set regarding controlled printer and material environments and soluble support in order to reduce process variability and allow geometric freedom.”
This feature was originally published in the August 2019 issue of 3D ADEPT MAG.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.