Archive — This 2019 feature brings together contributions from ARMOR/KIMYA, VBN Components and Malvern Panalytical. Roles and examples refer to that period; editorial clarifications distinguish stated properties from their conditions of use.
A component’s performance depends in part on material selection and processing conditions. High performance in one respect does not establish suitability for every application.
Selecting an additive manufacturing material requires matching service requirements with machine capabilities and finishing operations. Where this expertise is not available in-house, specialist support can help define the decision criteria.
Indeed, as technology advances, the rise of technical terms such as high-performance materials, engineering materials or advanced materials, is gaining momentum. In an era where companies tend to claim to be the “first” to launch their technology onto this market, it is easy for the prospective end-user to get lost by the (sometimes) abusive use of technical words by companies.
This article, therefore, aims to clarify the meaning of high-performance materials. It aims to help users identify the various types of high-performance materials, to understand materials characterization and to determine the additive manufacturing technology that suits those materials best. To discuss this topic, we have asked a number of questions to VBN Components, Armor Group and Malvern Panalytical B.V.
High-performance materials, engineering materials or advanced materials?
Material developments have enabled applications across transport, electronics and many other sectors. Their value must nevertheless be assessed for a specific use and manufacturing process.
The demand for improved components concerns additive manufacturing as well as moulding, machining and assembly.
Criteria may include mechanical strength, deformation and corrosion resistance, weight, service temperature and durability. One material does not necessarily maximise all of these properties.
According to Pierre-Antoine Pluvinage, Business Development Director at ARMOR GROUP, for the AM brand KIMYA, thermal resistance, mechanical resistance and shock resistance are often the first key performance indicators taken into account to identify high-performance materials:
“High-performance materials are first characterised by their thermal performance. Another key performance indicator may be their chemical or mechanical resistance, or shock resistance properties.
However, thermal performance is not necessarily the only defining feature of a high-performance material: it can provide functional properties that other engineering materials or readily-available materials would not provide.”
“Engineering material”, “advanced material” and “high-performance material” can overlap in industrial usage. The terms do not by themselves provide certification or a universal performance classification.
Engineering materials are selected to perform a technical function. Selection concerns a particular grade and measurable properties suited to the component’s requirements.
“Advanced materials” can refer to compositions, structures or properties developed for particular requirements. This does not make them interchangeable with everything described as high-performance material.
Broad families include metals, ceramics, polymers, composites and semiconductors. This feature focuses on polymers and metals.
High-performance polymers
A material is more complex than just its chemical composition. Its properties depend on its microstructure, which can evolve – during the process – or the life of the material.
In transport and aerospace, selected polymers can help reduce component weight. Their ability to replace another material must be assessed against loads, temperatures and the operating environment.
In this vein, the Business Development Director of ARMOR Group explains that we do not only talk about high-performance materials when it comes to additive manufacturing. As a matter of fact, high-performance materials are used in several production processes like injection moulding or machining processes. “The challenge is to assess how to use these materials and adapt them to 3D printing technologies while maintaining their native properties”, said the expert from ARMOR Group.
Examples include PAEKs, a family comprising PEEK and PEKK, as well as PEI and PPSU. ULTEM is a brand of PEI resins, rather than a separate polymer family. Properties vary with the grade and its condition after processing.
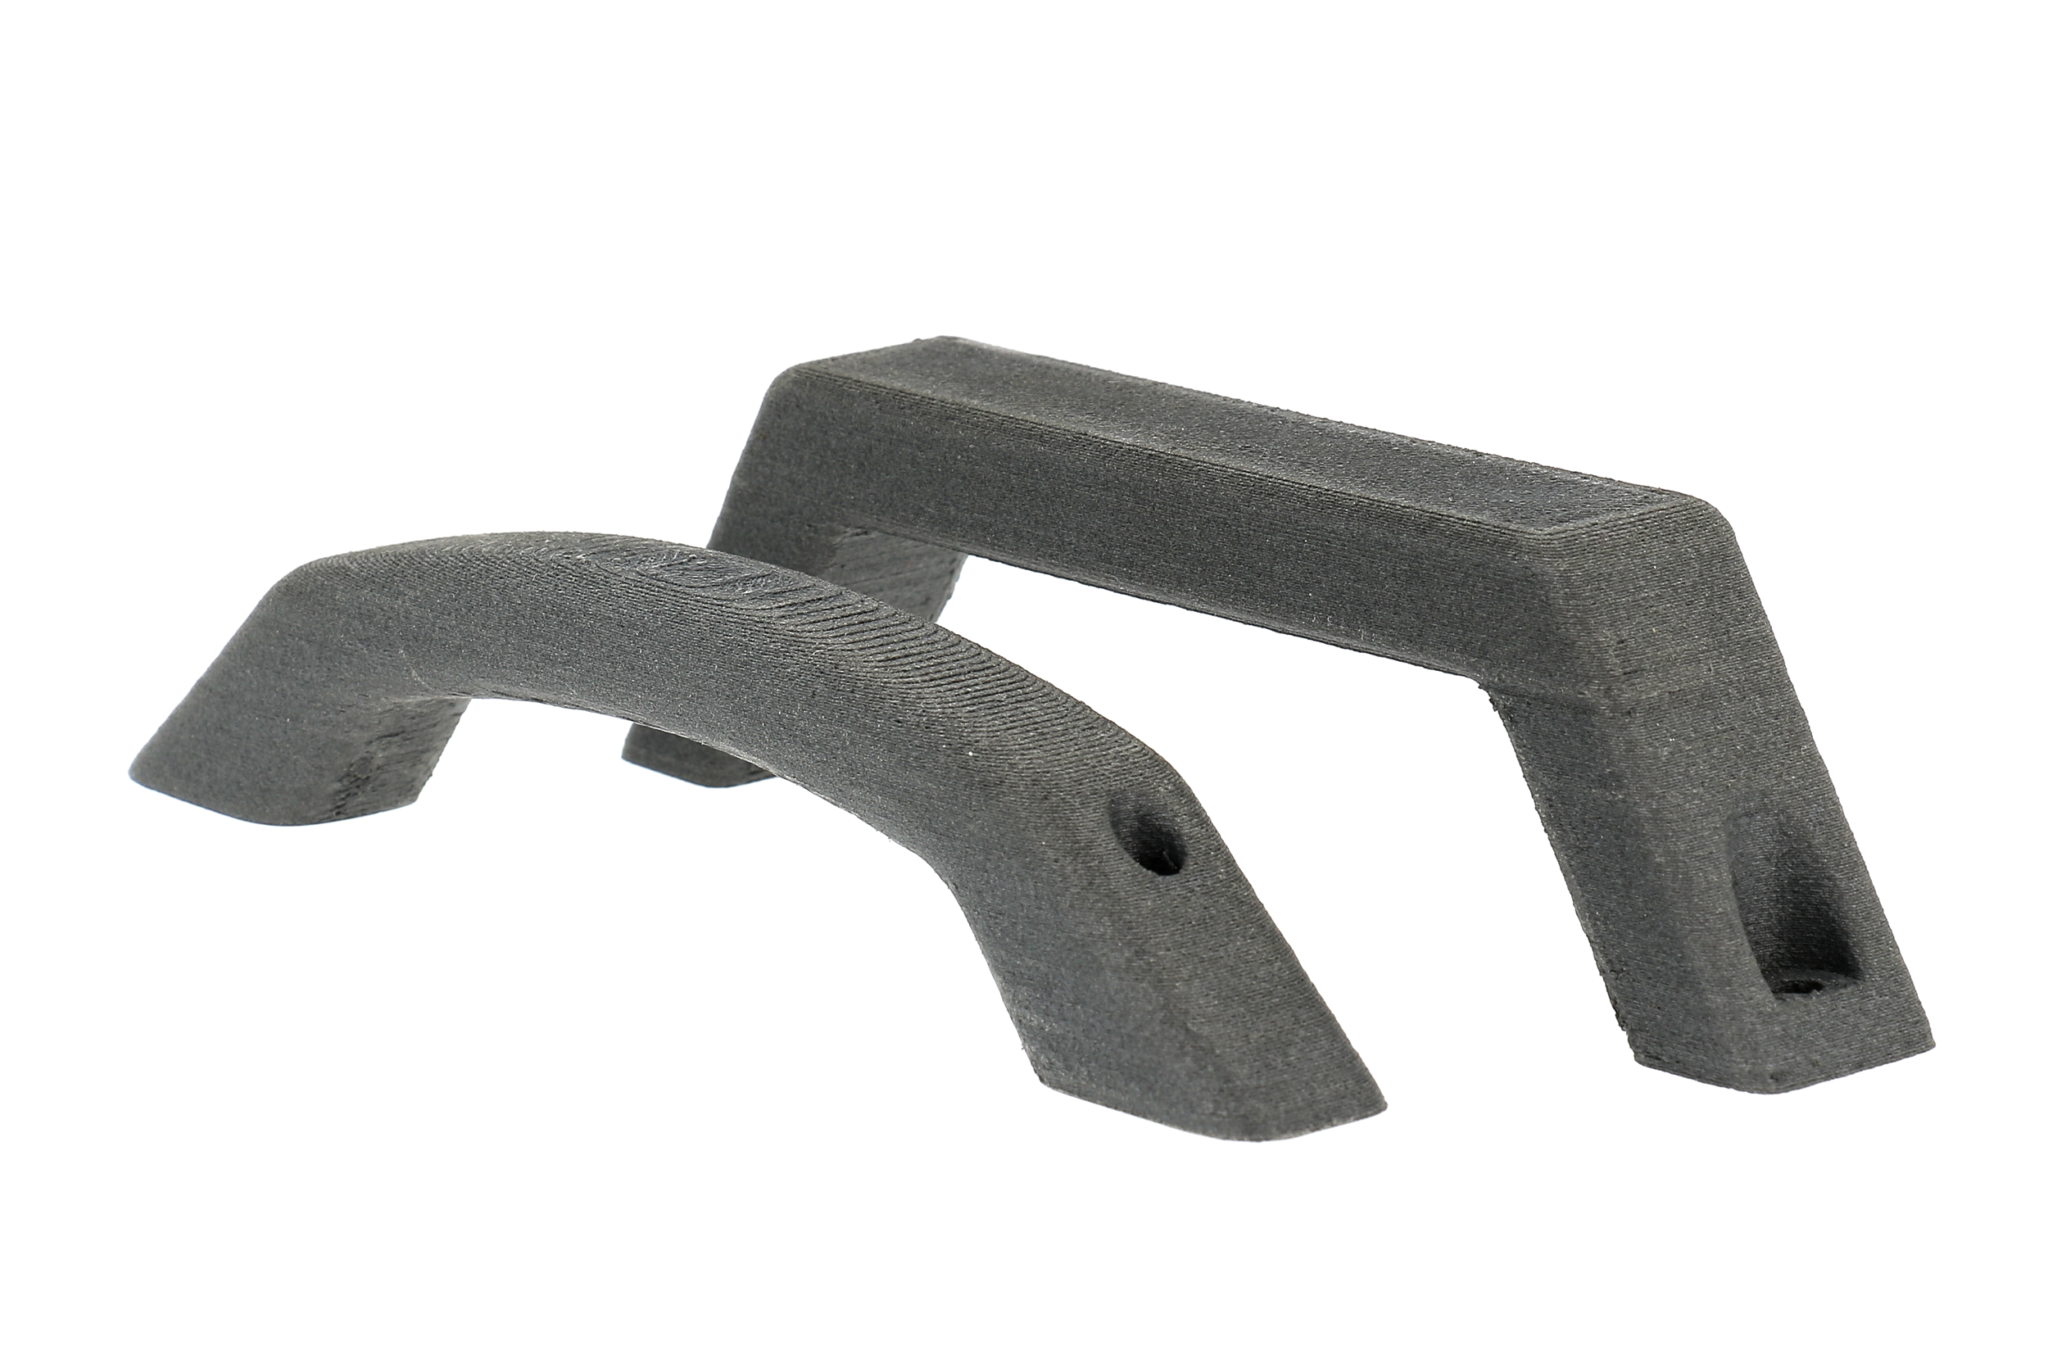
The Kimya PEKK-A discussed here uses a slow-crystallising Arkema Kepstan PEKK resin. The Kepstan 6000 series documentation distinguishes amorphous and semi-crystalline conditions depending on thermal history. A temperature figure alone therefore does not define a universal service limit for a printed part: the grade, any annealing, load and exposure duration must be specified.
Now, to attest to the quality of this material, and its ability to be processed on various 3D Printers, materials characterization comes into play.
Materials Characterization
As technology advances, material characterization increasingly becomes sophisticated. Several techniques exist to study and measure physical, chemical, mechanical and microstructural properties of materials. The process can be applied at several stages of materials development.
However, whatever the process is, the overall goal is, on the one hand, to understand key elements required to resolve important issues, such as causes of failure and process-related problems, on the other hand, to make critical materials decisions.
Both standardized analytical methods and specialized application-specific advanced techniques can be applied during such process.
Relevant tests depend on the material and application, and may include tension, bending, impact or thermal behaviour. For printed specimens, preparation, orientation, printing parameters and conditioning must be documented to make results comparable.
As far as ready-to-commercialize materials are concerned, Pierre-Antoine Pluvinage mentioned some of the criteria that are taken into account to attest to their quality :
“There are several criteria to consider when it comes to monitoring filaments’ quality: diameter checks, ovality checks, imperfections checks (air bubbles). We might also add printability, as well as the evaluation of the functional attributes linked to the product’s technical specifications”, explains ARMOR Group.
Selecting and controlling the process
Depending on formulation and feedstock form, selected high-performance polymers can be processed by filament extrusion or powder-bed fusion. Compatible equipment and parameters are required; one grade is not automatically usable in both processes. The following points concern filament extrusion.
Extrusion, build-plate and chamber temperatures must suit the grade and supplier recommendations. An excessive nozzle temperature can degrade the material; insufficient temperature can impair flow and interlayer bonding.
The build plate and its interface must provide first-layer adhesion while allowing removal after cooling. Settings depend on the material and build surface.
A heated chamber helps control temperature gradients during printing. It can reduce distortion, but does not eliminate material shrinkage during cooling.
Crystallisation also depends on the grade, time at temperature and cooling conditions. It can change part dimensions and properties. The thermal cycle, including any annealing, must therefore be defined and validated for the intended result.
“High-performance materials benefits lie precisely in their versatility and wide range of possible applications. Semi-crystalline materials typically offer outstanding chemical and mechanical properties including [the ability to withstand] high-temperature conditions. They can be used in structural applications as well in applications that imply rubbing and erosion. For example, PEKK-SC presents a high chemical and thermal resistance combined with electric and dielectric insulation properties. Amorphous materials such as PPSU or PEKK-A perfectly maintain their mechanical properties until glass transition temperature and present excellent electrical properties. Thanks to their exceptional dimensional stability, these materials are suitable for precision components”, concluded ARMOR GROUP’s spokesperson.
These descriptions are the interviewee’s. Slow-crystallising PEKK can change condition with thermal treatment; retention of properties under load cannot be inferred from glass-transition temperature alone.
High-performance materials: metals
Metal additive manufacturing provides further possibilities for alloy selection and component design. Qualification requirements depend on the process and application.
Ductility describes the ability to deform plastically before fracture; it is not the same as tensile strength. Metals and alloys differ in ductility, and their properties also depend on processing and subsequent treatments.
Powders available for suitable processes include titanium alloys, steels, aluminium, copper, cobalt-chromium and nickel-based alloys. Selected processes also use precious metals. Selection must concern a grade qualified for the relevant system.
Industrial value may come from geometry, wear resistance or other required performance. Economics must be evaluated across the complete production chain, including volumes and qualification; lower cost is not an intrinsic property of 3D printing.
In the same vein, it should be noted that to attest to the quality of the aforementioned powders, the same properties are not necessarily always tested.
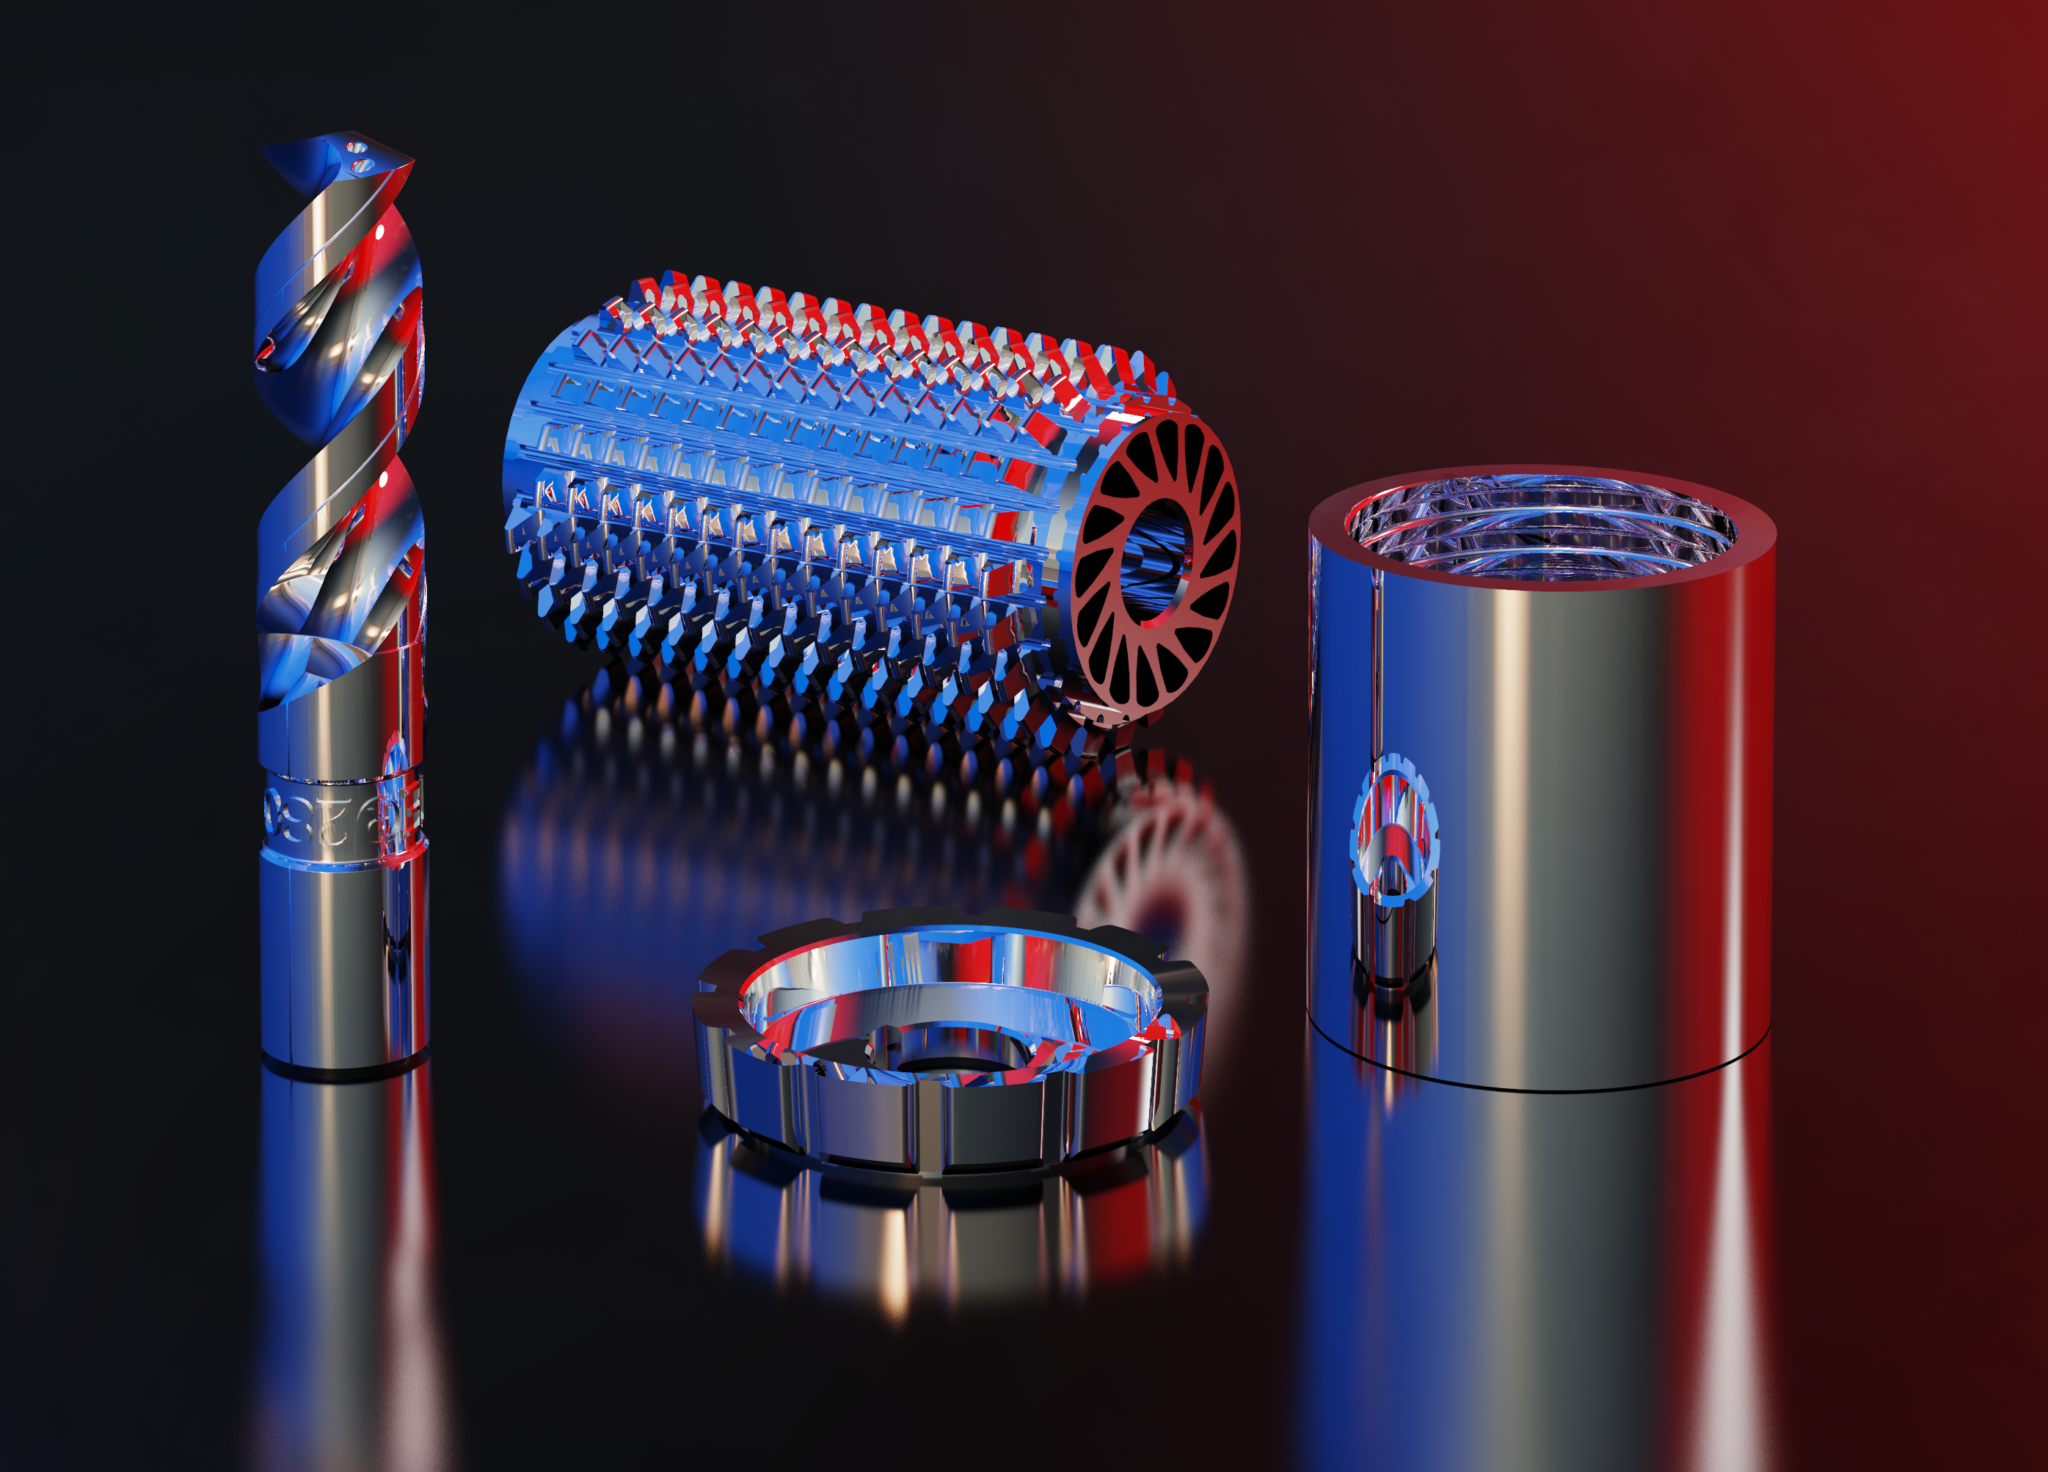
VBN Components for instance, develops a high-speed steel named Vibenite® 280, Isabelle Bodén, Customer relations manager, explained that for this material, the actual wear in usage (“how much material is worn off when exposed to i.e. abrasion”) and the long-term hardness are key characteristics that should be taken into account to attest to the quality of this material.
“Our materials are extremely wear-resistant. For example, our high-speed steel Vibenite® 280 is used in a gear hob, cutting twice as deep and lasting twice as long before needing regrinding, compared to a top, traditional steel in the same application. The carbides in our materials are very fine and well-dispersed, resulting in hardness levels up to 72 HRC and higher toughness than you would expect from such hard materials”, explained the spokesperson from the Sweden-based company.
VBN Components’ numerical comparisons concern the cited materials and application; they do not provide a guarantee for every component.
Characterising metal powders
The contribution of powder to production cost varies with material, process and reuse rate. Controlling supply and powder properties helps support consistent production. The following techniques are discussed in the context of powder-bed fusion.
According to Malvern Panalytical, “the chemical and physical properties of the powder directly impact the build process and final component quality and must be controlled and optimized to ensure process robustness and consistency. To achieve this powder, properties must be characterized at various stages in the supply chain, from new alloy development through to powder recycling. Laser diffraction, automated image analysis, X-ray fluorescence (XRF) and X-ray diffraction (XRD) are four key analytical techniques that are commonly used to characterize additive manufacturing powders.”
Laser diffraction is interesting to measure the particle size distribution of metal, ceramic and polymer powders for additive manufacturing. In powder-bed fusion processes, particle size distribution affects powder bed packing and flowability which in-turn impacts on build quality and final component properties. Using a laser diffraction process enables to achieve particle size distribution in a few minutes using either wet or dry dispersion techniques.
“Automated static image analysis can be used to classify and quantify the size and shape of metal, ceramic and polymer powders by combining particle size measurements such as length and width, with particle shape assessments such as circularity and convexity on a statistically representative sample (>10,000 particles)”, explained Malvern Panalytical.
X-ray fluorescence (XRF) provides elemental-composition information. X-ray diffraction (XRD) examines crystal structure and the phases present. These are complementary analyses, as explained in Malvern Panalytical’s additive manufacturing documentation.
Improvements in machine productivity do not replace material control. Characterisation links grade selection, manufacturing conditions and the required performance of the finished component.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.