Feature published in the October–November 2019 issue of 3D ADEPT MAG, then online in August 2020. Roles, software and perspectives reflect that period.
Design for Additive Manufacturing (DfAM) adapts part development to the capabilities and constraints of the process. This feature examines how it can contribute to part value.
It is, therefore, crucial for companies to master this stage of product development.
We explore this expertise through three companies’ accounts and software examples.
DfAM sits within Design for Manufacturing (DfM), accounting for the particularities of additive processes. Which principles and tools should designers use, and how should their contribution to the part be assessed?
We believe answering these questions will be helpful to beginners and experienced engineers alike. This article also aims to be an introductory guide for companies that are interested in starting or improving their experience in AM.
To connect theory with practice, Materialise, nTopology and Blueprint contributed to this feature. Their activities at the time are introduced at the end of the article.
Transition from DfM to DfAM
Let’s first try to explain what both concepts mean.
DfM incorporates manufacturing constraints and capabilities into product design.
Design for AM, on the other hand, refers to a set of design methods or tools whereby functional performance and/or other key product life-cycle considerations such as manufacturability, reliability, and cost can be optimized to leverage the full capabilities of additive manufacturing technologies.
In other terms, to take full advantage of AM capabilities, DFAM methods or tools are needed. However, it does not mean that the concept is separated from the broader techniques of DfM. Manufacturing some parts requires a combination of both additive and subtractive processes.
Both approaches seek to improve quality and control costs while accounting for the chosen process.
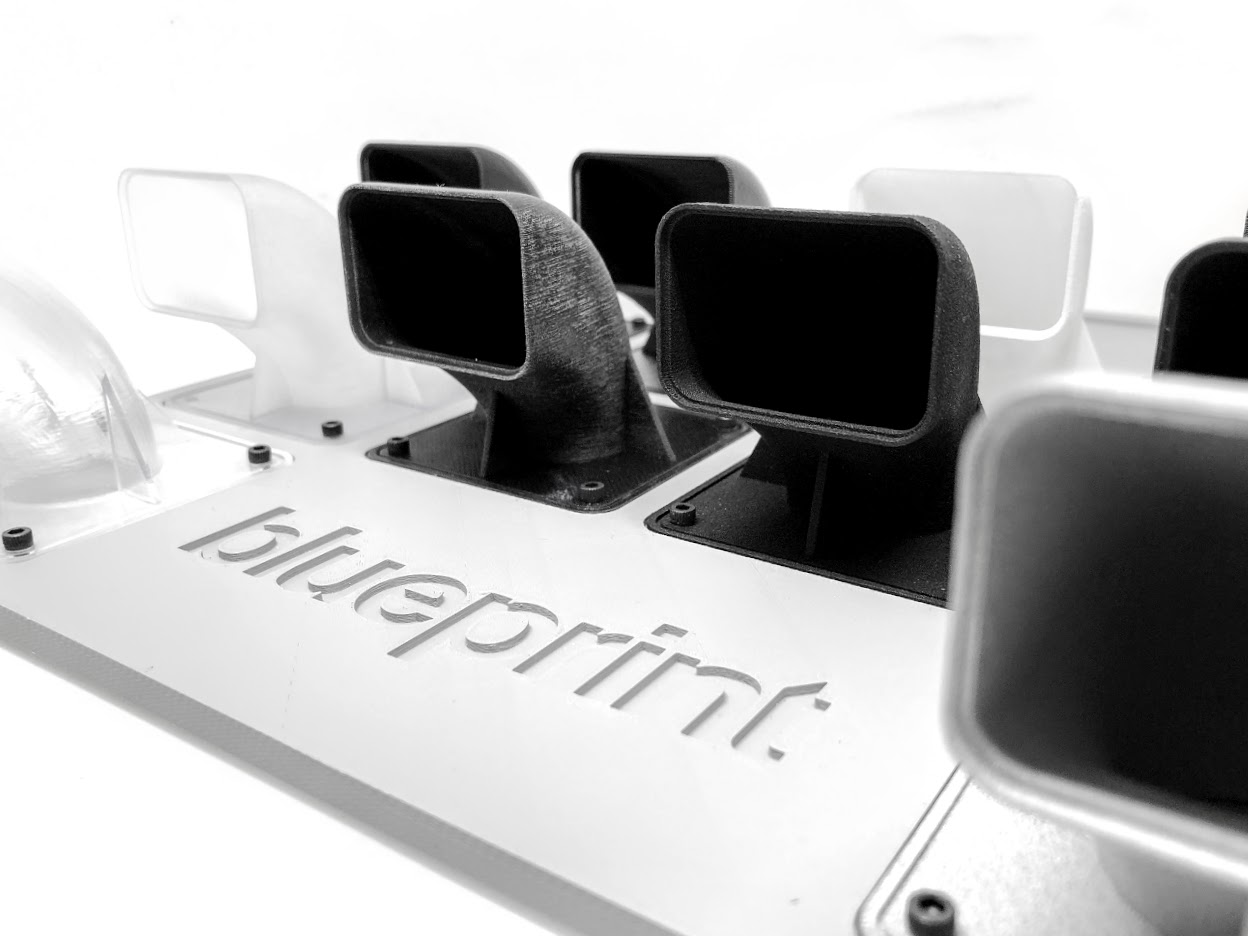
According to Loic Le Merlus, Consulting Manager at Blueprint, “when you design a part, you typically design for functionality, then figure out how to manufacture it. This often means changing geometries or even splitting a single part into several parts to be manufactured with different methods. Although you still need to design for manufacturability, AM can allow you to produce geometries closer to your design intent and can allow different optimisations than traditional methods. AM is a great tool for consolidating assemblies, reducing part sizes and weight, and creating prototypes close to the intended functionality.”
Design parameters depend on the material–process combination. Directly transferring geometry intended for another technique can therefore produce a poorly suited result. Stijn De Rijck, then Director of Training and Consultancy at Materialise, explains:
“Every design is created with a specific combination of material and production technology in mind, and that is not different for AM technologies. A mistake that is often made is to take a product that was designed for a given conventional technology and try to print it, for instance, as a spare part, without changing the design. There is an obvious chance that it will not optimally function or that production cost will rise significantly. If such sub-optimal design is used as the basis for a cost-comparison, you can be sure AM will lose the battle. But turn this around: what if you take a design that is optimized for AM and try to make it with a mould or through milling? A complex shape that is a piece of cake for AM, for instance, will create serious challenges in conventional technologies.”
nTopology’s CEO and founder Bradley Rothenberg agrees with Stijn De Rijck regarding this point. Indeed, in DfM, engineers should address the issue of optimum design that is required by various applications. In other terms, they should continuously look for the best compromise between the size, shape or topology of a part and using as little material as possible while ensuring the overall performance of the part. Those issues are addressed in the DfAM concept. Rothenberg takes the example of challenges materials might raise in a production process, to point out the differences between the two concepts and the type of parameters that should be taken into account when designing for AM:
“The requirements that the design must fulfil are very different — in fact even amongst conventional manufacturing constraints they can vary greatly — For subtractive manufacturing, the requirements for a 5-axis CNC part vs even 3-Axis will produce a part that might look totally different. There is also, of course, the cost aspect that one has to look into.
You can think of the design as the result of putting material in the best place that is balancing a number of requirements, so the final shape of a part, or what the part looks like, is a result of balancing the things that are important: cost, weight, manufacturing process, even aesthetics could be taken into account. When designing a part for AM, the geometric requirements are generally more free because you are building the part up from raw material (additive) instead of starting with a block and chipping away at it.
Also, parts designed for AM can take an architected materials approach if the design software is capable.”
These accounts emphasise designing for a specific process. DfAM builds on DfM principles with the constraints and capabilities of additive manufacturing.
DfAM: tools and impact on the part
Possible tools include topology optimisation, lattice structures, customisation and part consolidation. They are neither required for every project nor exclusive to AM; their value depends on the process and application.
In this vein, the first step for designers is to keep in mind the capabilities of AM: shape complexity, material complexity, functional complexity and hierarchical complexity.
As far as shape complexity is concerned, AM enables to “build near net shape, complex shape geometry and interconnected internal channels.”

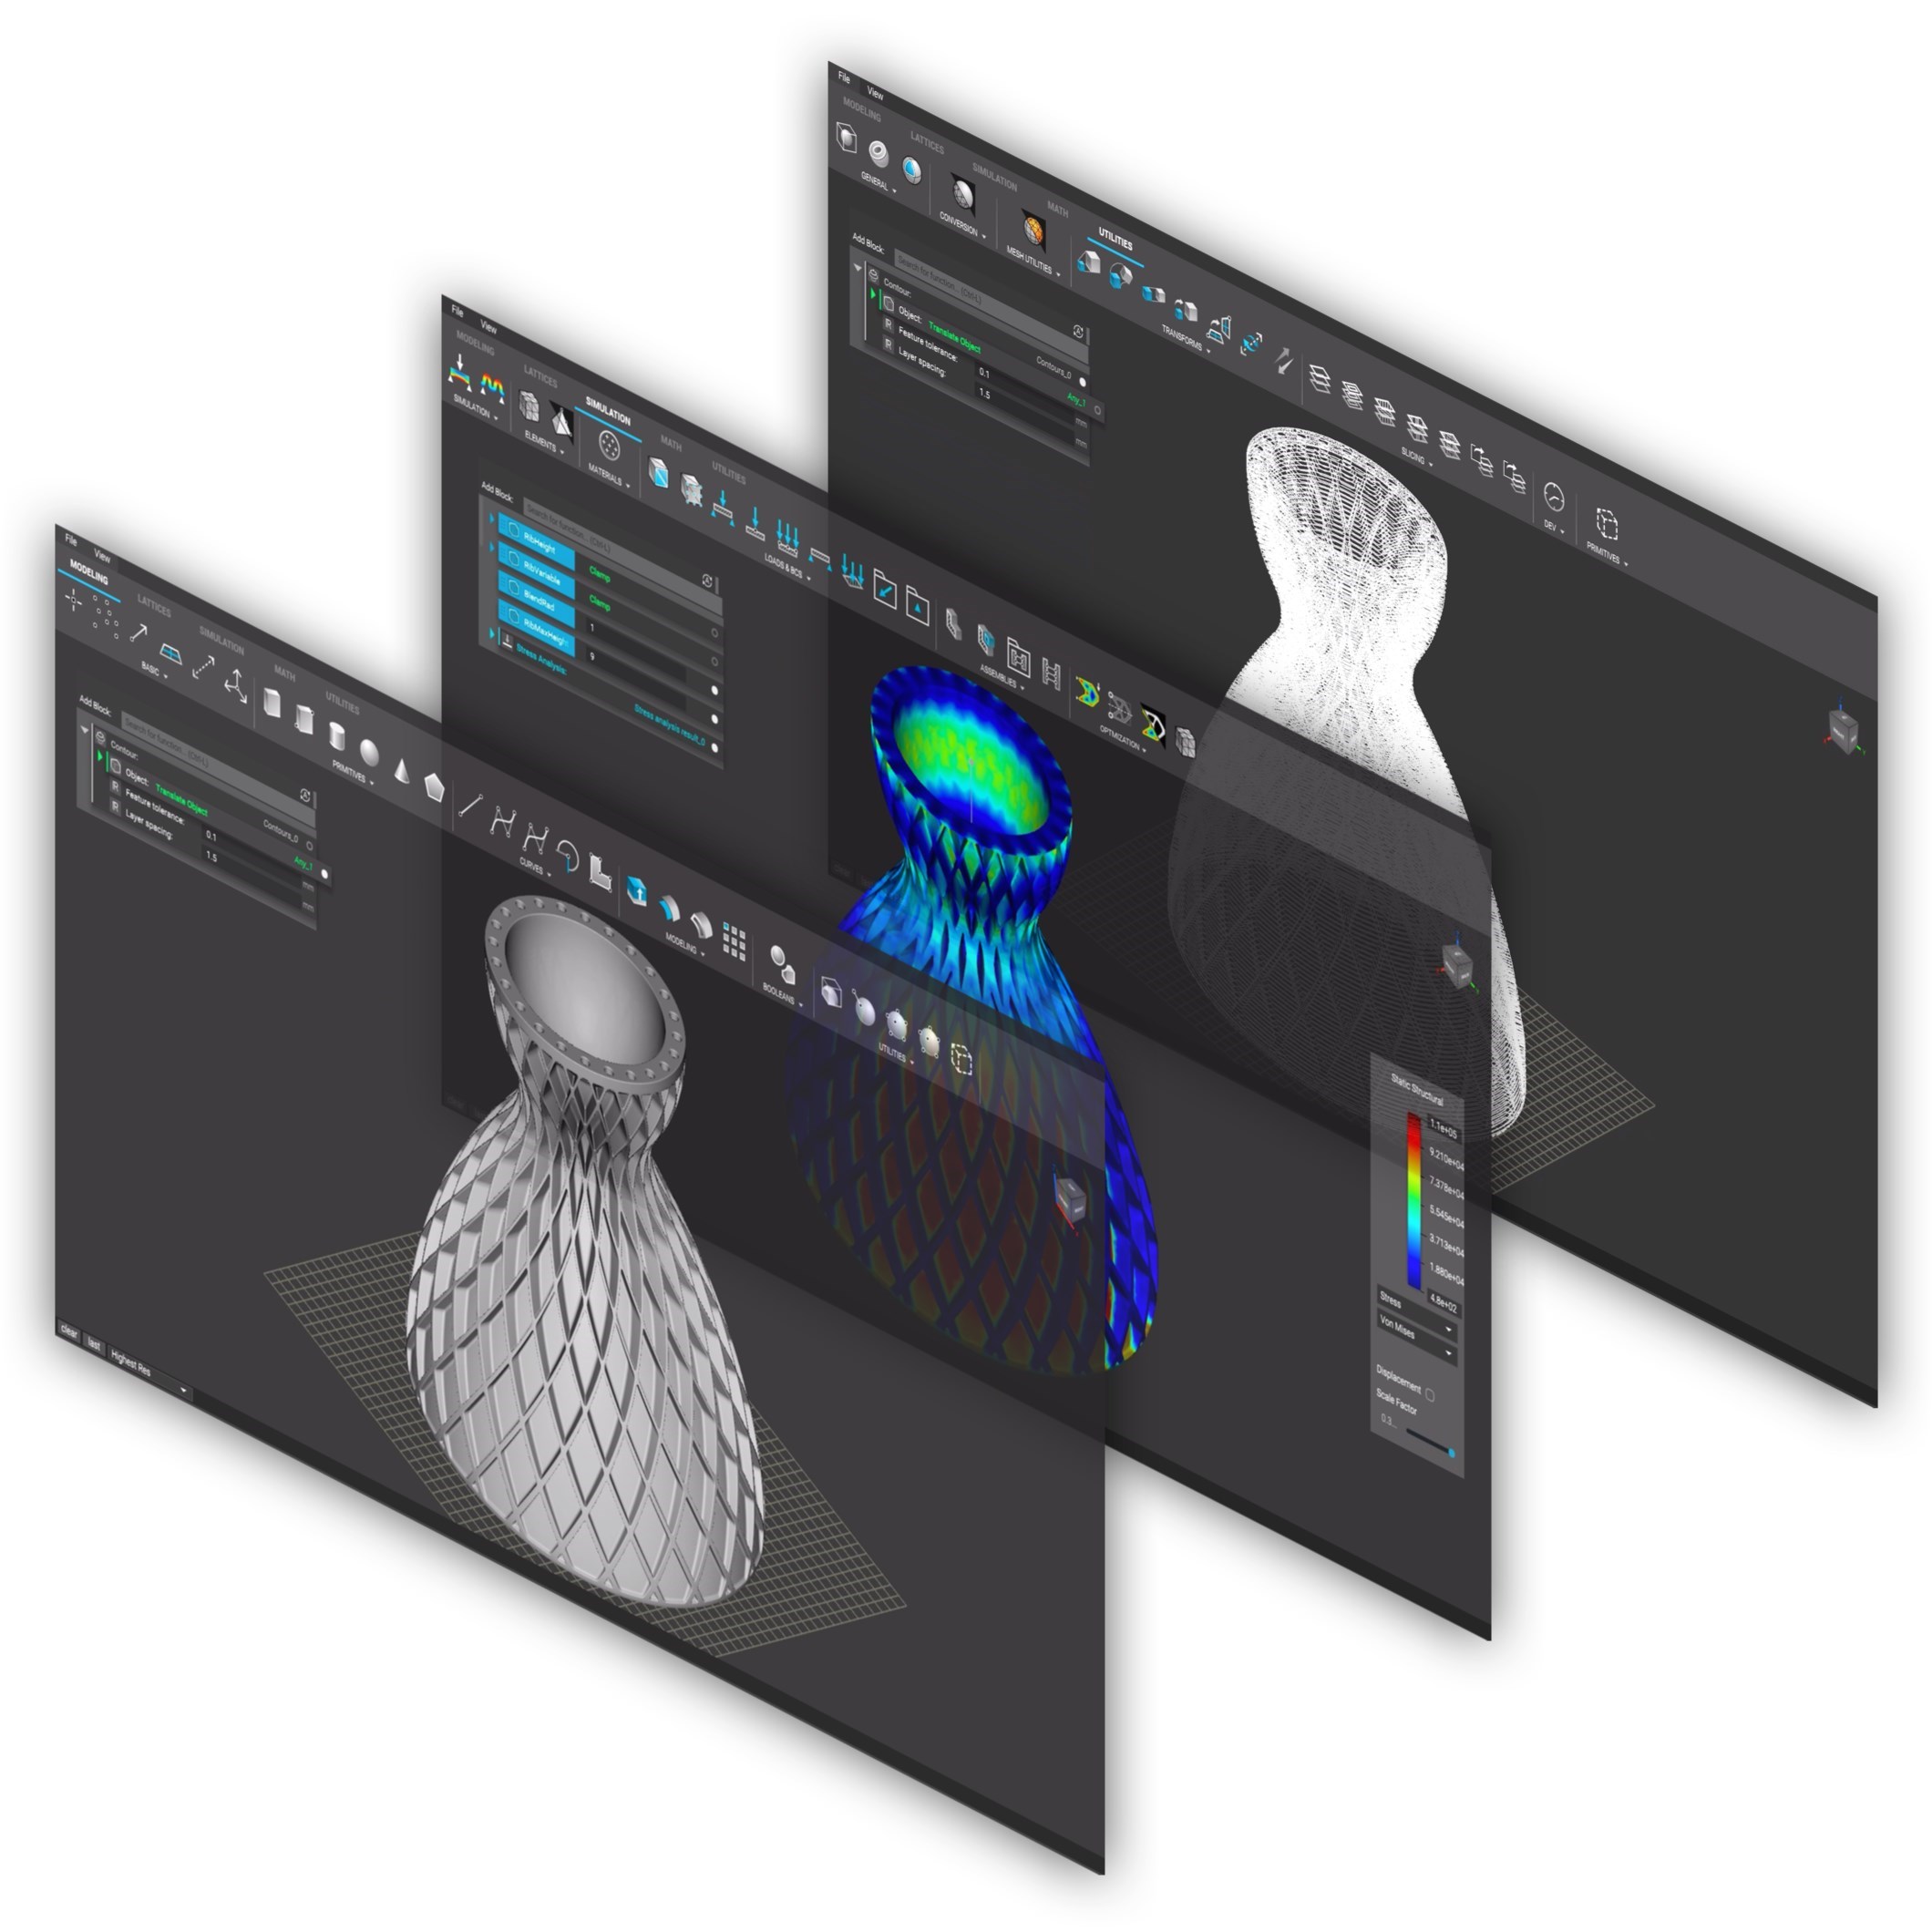
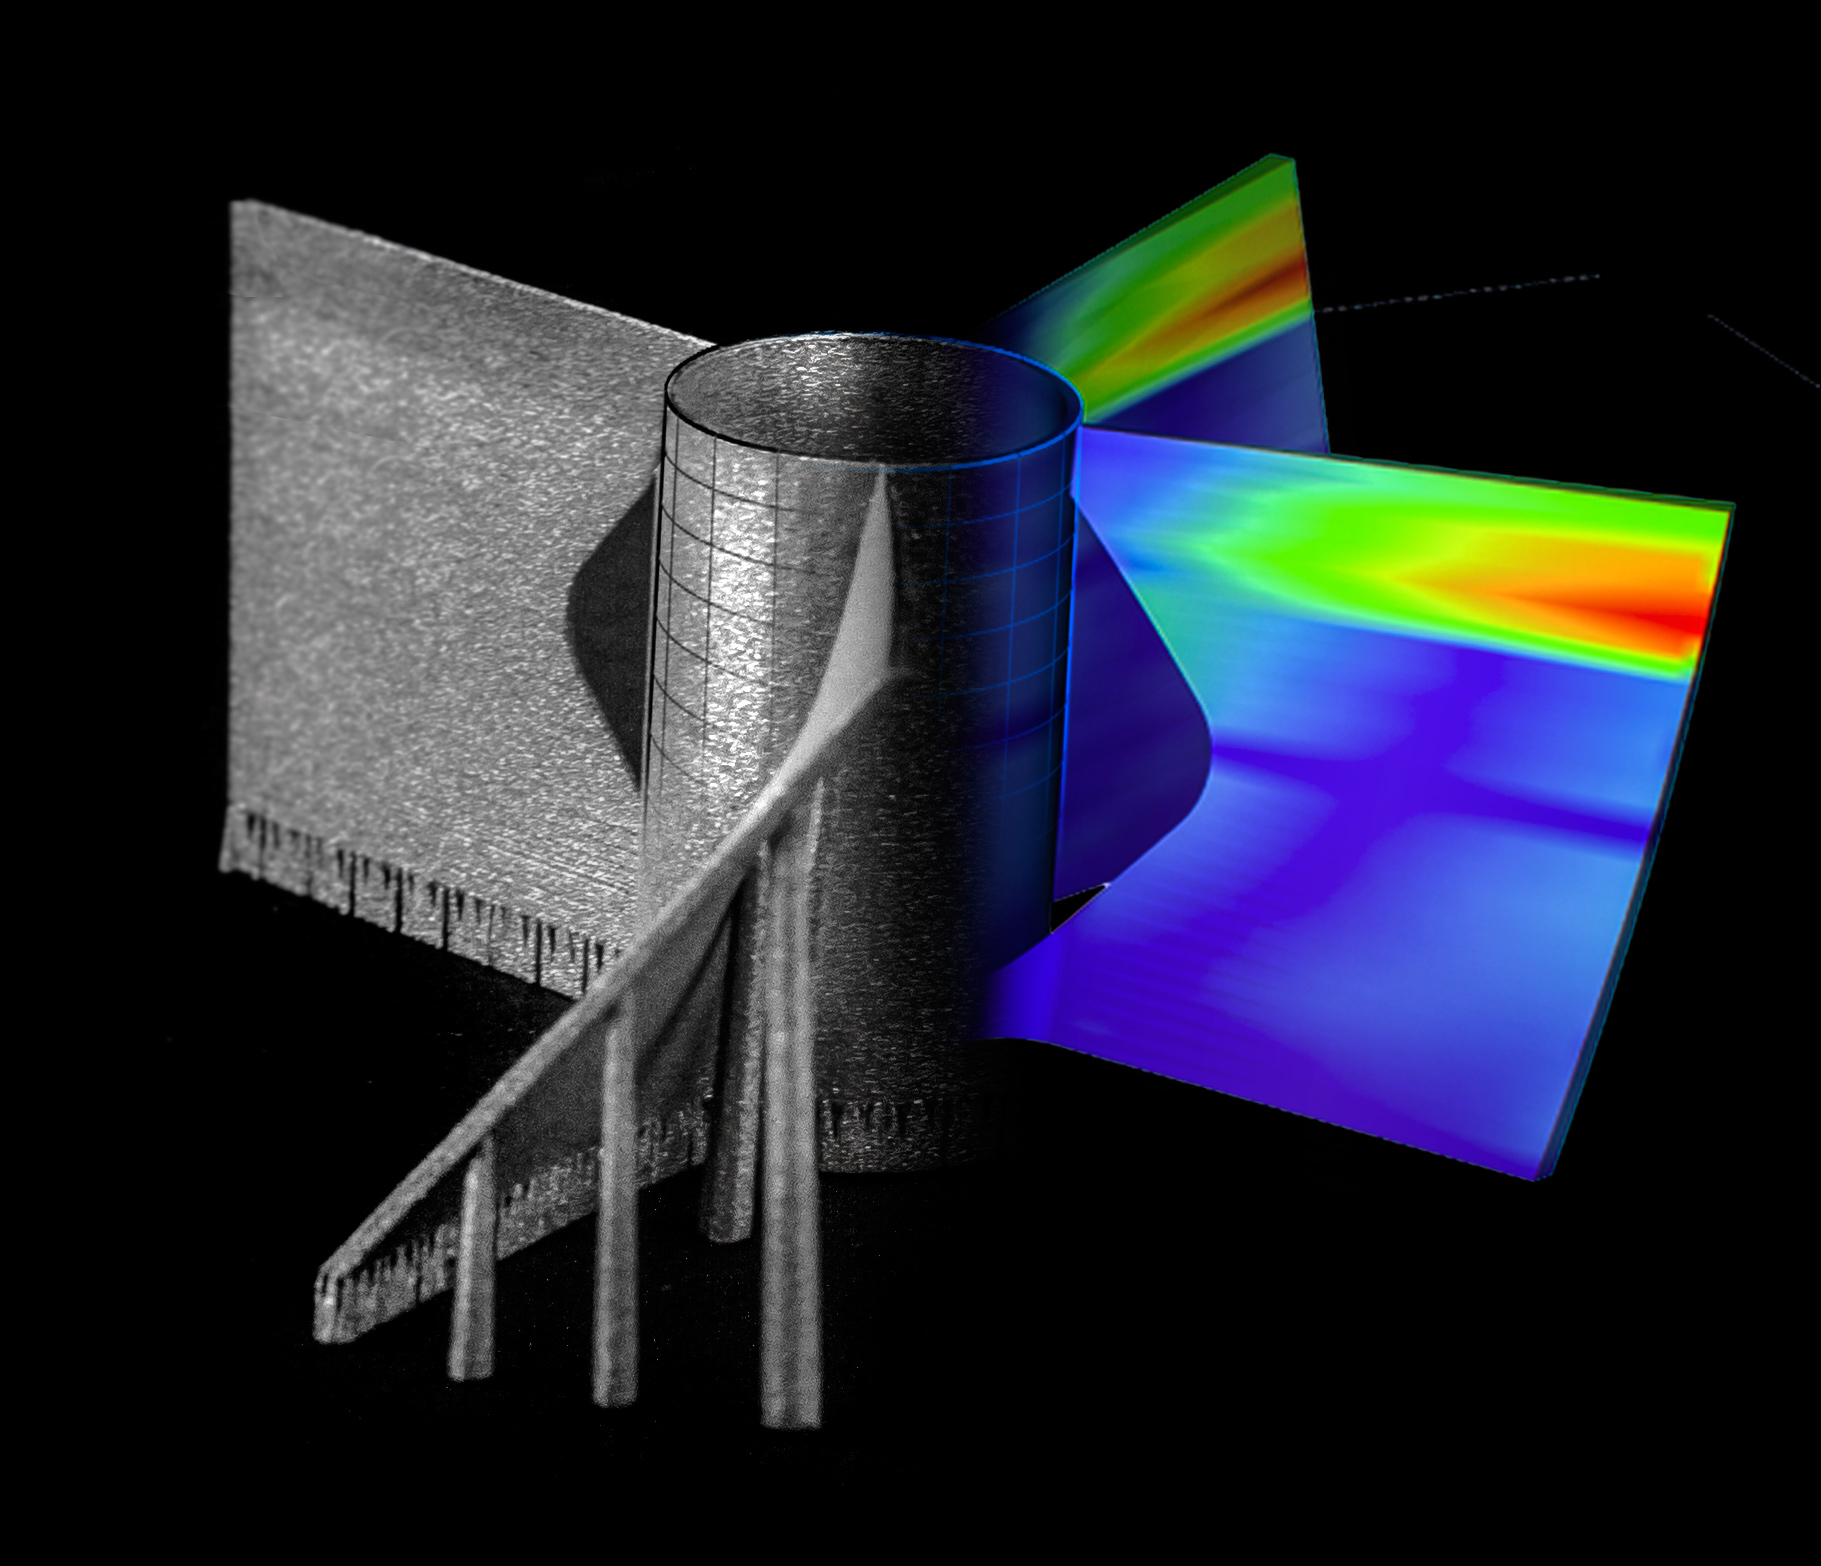
“AM has sort of flipped the relationship of software & hardware on its head — it used to be that you could come up with shapes in the computer that would be impossible to make (for example topology optimisation was popular amongst academics 30 years ago, but didn’t really make it to industrial uses until recently). Today, the manufacturing process is capable of making shapes that the current standard of design tools are not capable of representing. This is because those tools were designed at a time when drawings and traditional manufacturing were the paradigm”, explains nTopology’s Rothenberg.
Material selection, distribution and resulting properties impose design constraints. The ability to vary structure or composition locally depends on the machine, process and available materials.
“Unlike subtractive manufacturing where removing material is expensive, with AM, adding material is expensive. You also have the added complexity of support structure. The more material and support structure your part contains, the longer it takes to build. Tools like topology optimisation can generate highly-optimized organic shapes, but often at the cost of requiring more support structure. Surface roughness is another limitation, but this can be mitigated with clever design. A designer can re-orient a part to reduce roughness on critical faces, avoid certain angles, or even add texturing to hide surface imperfections”, explains Blueprint’s Loic Le Merlus.
Consolidation can reduce component and assembly counts. It does not guarantee a fully functional device straight from the machine: support removal, cleaning, finishing and inspection may still be required. Any remaining assemblies still need suitable tolerances.
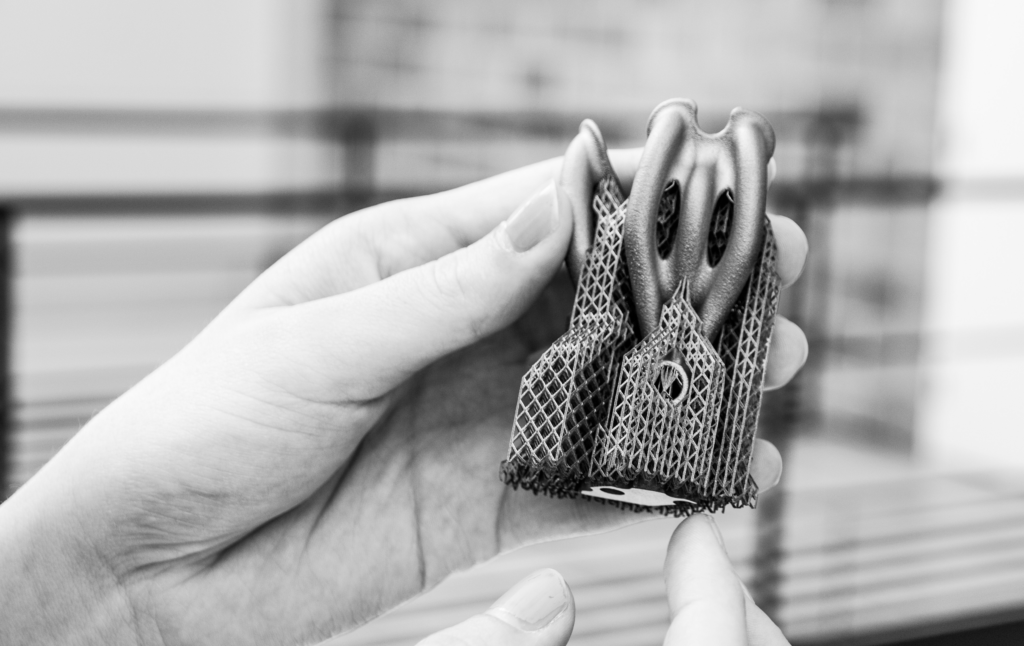
Cellular structures, honeycombs, foams and lattices distribute material across several scales. They can improve selected stiffness-to-weight or strength-to-weight ratios, depending on design and loading. Gains need verification and do not alone guarantee an overall cost saving.


Reality shows that it is interesting to know all these unique capabilities of AM. They are certainly a great help for engineers that want to design for AM. However, for Materialise, something more valuable is also important when it comes to DfAM: experience and creativity. As per the words of Stijn De Rijck:
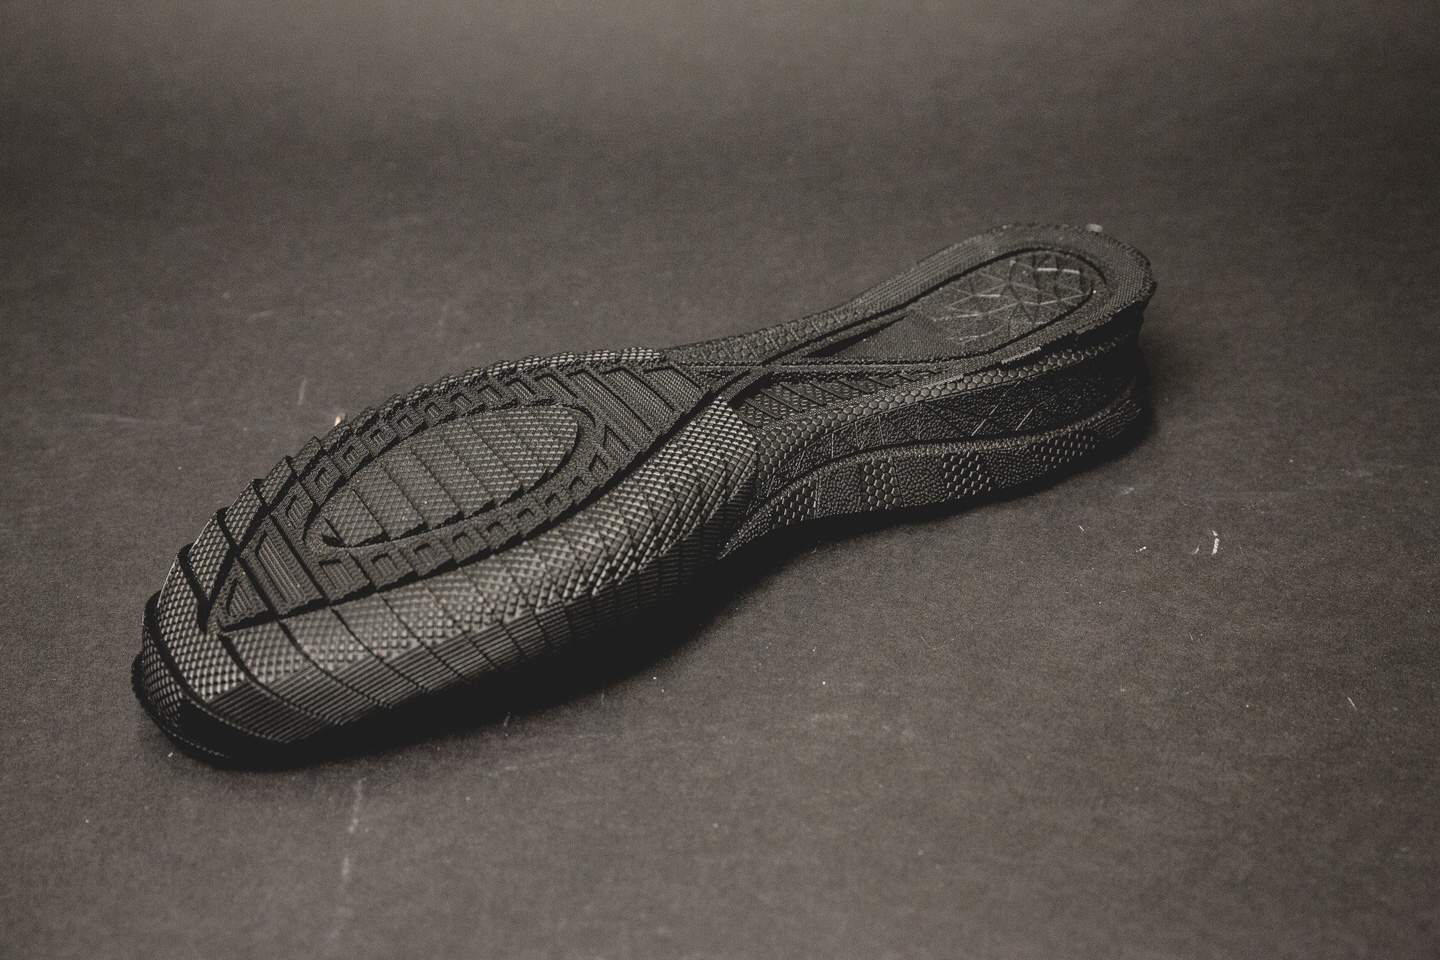
“Design engineers are trained to deal with the limitations of conventional production technologies. Thinking in limitations instead of opportunities leads to limited use of the design freedom of Additive manufacturing. You need to build up experience and use your creativity to look beyond the limitations, and start to make use of the real strengths of the technologies. Take the example of the midsole we created with Adidas in the Futurecraft project: at the time we had no AM material available that was soft enough to create the right cushioning in the midsole, so at first sight, we would never reach the requirements for optimal performance. But instead of getting blocked by that limitation, we created a structure that changed the part flexibility and as a bonus, we also reduced the weight of the running shoe significantly.”
These capabilities are interesting to keep in mind. But what happened when different AM processes are involved?
Design’s impact on process and part
We looked at the impact “Designing for AM” can have at two levels: the first one consists in knowing if the concept is the same for different processes and the second one consists in determining the impact on the part.
Adapting the design to the process
Our experts shared different views regarding DfAM and AM processes. When asked if the design remains the same whatever the AM process is, Blueprint, for instance, said it depends on some conditions:
“For simple parts that haven’t been optimized to a particular AM process, yes. If you are just looking to print a one-off part, then it often does not make sense to optimize for a process. But there are a lot of different AM processes, each with different materials and mechanical properties.
If you want to start using AM as a production technology then, like with every other manufacturing technology, you should spend the time, resources, and energy to make sure your part is optimized for the exact manufacturing process you are using. This is how you get the cost and business benefits of the technology.”
nTopology, on the other hand, remains categorical. For the spokesperson, the design does not remain the same whatever the AM process is:
“No, each process has different requirements — you might have heard of terms like “support structures” or “laser toolpaths” or “bead diameter” — there are many new design variables, or things that can be changed that affect the output and quality of the part. Understanding these variables and the limitations on them will produce in some cases variations on the same design (like using a different machine but with the same process). For example, building on two different industrial-scale polymer FDM machines, or an entirely new design or, as another example, building two metal parts using binder jet vs laser powder-bed fusion. Each AM process makes more sense for some parts and not others, depending on the requirements of the part, [if you need 10K parts for example, or if you really need high-quality material properties for strength].”
Materialise on its side presents a balance between the two arguments. For the company’s expert, “AM is a group of production technologies that have the basic principles in common, but each of them has its characteristics, possibilities and design rules.”
It is important to note that different technologies require different optimisation techniques. We understand our experts’ thoroughness regarding this point. Indeed, the path the operator chooses to implement AM will determine how useful the technology can be in a given project.
Directly reproducing an existing part may fail to exploit AM’s capabilities and can create manufacturing difficulties. The value of redesign should be assessed against requirements, volumes and total cost.
Part quality

What’s the impact of designing for AM on the part? That’s a crucial question because in the end, the most important is the result, the part value. If it is a success, then everybody is happy. If it is not, it is a waste of time and money. Answering this question inevitably raises the question of intelligent optimisation. Is intelligent optimisation a synonym of topology optimisation? What does it really mean?
The Consulting Manager at Blueprint outlines the distinction between the two terms:
“Software that can create highly optimized structures isn’t necessarily intelligent; it could be like your car’s navigation system, following a human-defined algorithm, to produce a result based on initial inputs. A more accurate label would be “algorithmic optimisation.” This can encompass all optimisation methodologies including topological, generative, and structural. Furthermore, the geometry generated from such an algorithm doesn’t necessarily ensure the manufacturability of the part. The intelligence still resides with the designer who sets the starting parameters or boundary conditions and then must interpret, approve, and sometimes tweak the output of that algorithmic process to ensure the design meets requirements and is manufacturable.”
The CEO of nTopology this time, agrees with Blueprint. The founder explains that topology optimisation can be a part of an “intelligent optimisation”: “I would define ‘intelligent optimisation’ as a workflow, or process that captures engineering intent within it in order to make a better part faster. This can be a manual process, a hybrid of some manual & some algorithmic, or fully algorithmic. Ideally, the inputs would be defined, and if changed you get a new output, a new part. Topology optimisation can be one component of an ‘intelligent optimisation’.”
Intelligent optimisation, therefore, lies in the ability to create a “smart” design and prepare it for the selected AM process. As De Rijck said while warning designers: “One thing is to create an intelligent design, the other thing is to prepare parts for successful building in AM. You should consider this build preparation work to be a design process as well. Take for instance metal 3D printing: each component that goes on a metal AM machine needs to be printed with a support structure to anchor the part to the build platform and to control the heat dissipation. The ideal support structure is strong enough to anchor the part, but very light, so it does not consume valuable machine time and material. Searching for the optimal combination is a daily challenge if you run a metal machine in AM.”
Editorial clarification: the remarks about anchoring and heat dissipation apply particularly to metal powder bed fusion. They do not apply indiscriminately to every metal AM process. The support functions described by Materialise depend on process and geometry.
In the end, the impact of the DfAM concept is huge. As per the words of Rothenberg, “it’s bigger than any of us thinks.” It looks like we are just at the beginning of a big chapter in the engineering software industry. The DfAM concept involves new tools and new ways to increase part value while taking into account materials and hardware. In terms of part quality, we do not only talk about higher performing parts anymore, but, according to Rothenberg, we also talk about the speed that these new parts can be iterated on.
Future prospects
Design tools and practices continue to evolve. The interviewees highlight the needs they observed when this feature was prepared.
In 2019, their priorities included skills, automation and data exchange between design and production.
“The data exchange between AM machines and ERP systems needs to be improved. Nowadays, companies want to know what is happening on the manufacturing floor all the time to identify problems and bottlenecks as fast as possible. AM is still too much of a black box to get all the required production intelligence”, said Blueprint.
What nTopology hears the “most often as barriers to wider adoption are: the need for more automation in design process (DOEs, etc.); STL files introducing uncertainty into the build process and causing data handling and build crash issues; part complexity making design process really long or really difficult and, in general, existing design software holding back engineers from optimizing parts to take full advantage of AM processes.”
For Materialise, connectivity is the key issue to tackle. “Connecting additive manufacturing into manufacturing setups, linking it to other technologies and business systems, is allowing fast-growing applications to grow even more rapidly. It allows scaling and fast adoption and it allows to combine technologies and software systems to get the best of all worlds in one production flow. Next to state-of-art software, in-depth knowledge of the AM-specific process, the adoption of industry standards like MT Connect & OPC-UA and last but not least access into a broad network of partnerships and collaborations, are crucial to turn Additive Manufacturing into a widely trusted manufacturing technology and create applications that open up new possibilities.”
This feature was originally published in the October–November 2019 issue of 3D ADEPT MAG.
A few notes on the participating companies
The profiles below describe the companies at the time of the feature; they are not current company profiles.
Blueprint
Blueprint is a Stratasys company that provides companies with strategic, operational and applications consulting that help them to navigate the additive manufacturing world. The company first appeared on our radar when they launched its “Think Additively program” but it traces its beginnings to early 2015 when Stratasys Services Group integrated the Econolyst team.
As part of this dossier, the company firmly believes that, “while there are software solutions to help with certain elements of design for additive, such as topology optimisation to minimize material, or simulation to predict deformation or defects, there isn’t a single, turnkey solution for all the steps in the design process. The human element is still very much at the heart of designing for AM. As an industry, [they] can build better tools, but [they] must teach people how to use them. Currently this skill shortage… the lack of knowledge of how to use the tools… is slowing down AM adoption.”
Materialise
Materialise presented its experience in software and 3D-printing services for medical and industrial applications, along with its collaborative approach with users.
Several reasons raise Materialise’s interest in this topic:
- First, they guide companies through the design process, and make sure to tailor the knowledge transfer to the specific technology-material combination for their specific case.
- Secondly, they “have created software tools that help designers and manufacturers to cope with the specific needs of AM. Materialise 3-matic for instance, is a package that allows [users] to enhance [their] design by creating 3D textures on surfaces or lattice structures in volumes, [just to name a few examples]. With the scripting function in 3-matic [the user] can easily automate repetitive tasks, [and] focus on the more creative part of Design for AM. Materialise Magics is [a] software used to prepare parts for production. It helps [the user] choose the orientation of parts and guides [him] in designing smart support structures. The recent simulation module allows manufacturers to predict and thus avoid build failures, so there is significantly less down time with machines.”
nTopology
Founded in 2015, nTopology was developing advanced design tools. The 2019 feature reported $31 million raised and an office in Germany: these figures describe that period, not the current situation.
The company highlighted lattice design, topology optimisation and manufacturing outputs that could avoid selected STL conversions. These capabilities depend on the workflow and equipment compatibility; modelling operations should not be regarded as infallible.
With regards to this dossier, Rothenberg strongly believes that “the impact that [has] the ability to take an architected-materials approach to part design is game changing and it is the combination of AM hardware and nTop Platform software that makes this possible.”
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.