


Archive — September 2019 interviews with Flow Science and AlphaSTAR. Features and examples refer to the software discussed at that time.
Manufacturing systems involve interactions between materials, equipment and process parameters. Simulation can investigate some of these interactions and compare choices before manufacturing. This feature examines its use, advantages and limitations in additive manufacturing.
We will tackle this issue by laying emphasis on their use, advantages and limitations. Pareekshith Allu, Senior CFD Engineer at FLOW Science, Inc. and Rashid Miraj, Director of Technical Operations at AlphaSTAR shared their expertise in this dossier.
Both companies have extensive experience in software solutions. They supply their services across a wide range of industries, and obviously, additive manufacturing is part of them.
Flow Science, Inc. is a software company that develops tools for computational fluid dynamics, also known as CFD. Among its CFD solutions, the company has developed FLOW-3D, a CFD software that provides solutions for free-surface flow problems.
AlphaSTAR Corporation on its side is a software company that provides advanced engineering services for physics-based simulation technologies. Dedicated to additive manufacturing, structural modeling and analysis of advanced composite structures its simulation technologies are exploited in the aerospace, automotive, defense and energy industries around the world. The company has developed GENOA3DP, an Additive Manufacturing Simulation tool that assists
the 3D printing process in predicting deformation, residual stress, damage initiation and crack growth formation associated with as-built AM parts.
Both resource persons will take examples from use cases developed by the company they are working in, to illustrate their arguments.
A simulation tool represents a process or system through models. It can investigate expected behaviour, compare designs or examine conditions that are difficult to reproduce. Results depend on assumptions, input data and validation.
Engineers can reduce some physical trials and explore designs before manufacture. Simulation helps target testing; predictions still need comparison with measurements representative of the process and part.
Software selection should therefore start with the phenomena to investigate, model scale, available data and decisions the calculation needs to support.
Main features of simulation software for additive manufacturing
According to Pareekshith Allu, Senior CFD Engineer at FLOW Science, Inc., “a simulation software needs to have three features: it needs to implement relevant physics accurately across a range of length and time scales, it needs to be computationally efficient, and it needs to be intuitive for the user.”
Even though simulation can be applied with various 3D printing technologies, the Senior CFD Engineer also lays emphasis on the different nuances that may rise in the use of simulation software for various AM technologies.
“In laser powder bed fusion (LPBF), directed energy deposition (DED) and selective electron beam melting (SEBM) for instance, we need to be able to simulate powder spreading and bed compaction, melt pool dynamics and associated defects such as balling, keyhole formation and porosity, and residual stresses and distortions in the finished part. Our modelling tool FLOW-3D® accurately simulates these AM processes by implementing all the relevant underlying physics at the micro- and meso-scales” adds Pareekshith Allu.
“Through such simulations, users can develop process windows for various parameters such as laser power, scan speed, hatch spacing, and powder size distributions, to successfully additively manufacture different alloys. Computational efficiency allows AM engineers to generate these process windows more quickly than running experiments.
Of course, ease of use is key to successfully incorporating simulation software. An intuitive, process-based interface lets users follow a logical sequence of setup that implements the necessary inputs like material properties, CAD geometries, meshing and boundary conditions in a meaningful way. This translates into a short learning curve for first time users, and a simulation tool that is accessible to a wider audience of industry and academic professionals.”
For AlphaSTAR on the other hand, an accurate simulation of an AM build must consist of the following components and techniques:
“A validated as-built virtual material model incorporating temperature dependent material properties.
• Quality assessment of the g-code, laser path, printing process, and printed part.
• Fully coupled thermal-structural process simulation analyzing build deformation and defects.
• Ability to submit virtual as-built part to in-service loading.”
AlphaSTAR also describes models for environmental effects and defects. These calculations can support qualification, but a software result does not by itself certify a part or process.
Moreover, additive manufacturing remains a relatively broad topic and one thing, we have already observed is that 3D printing technologies do not often really look alike and might require a wide range of materials. So, do simulation software solutions change according to a specific type of additive manufacturing process or according to the materials used?
Simulation software, additive manufacturing processes & materials
Physical principles may be shared across processes. The model, parameters, boundary conditions and validity range must nevertheless match the process and material being studied.
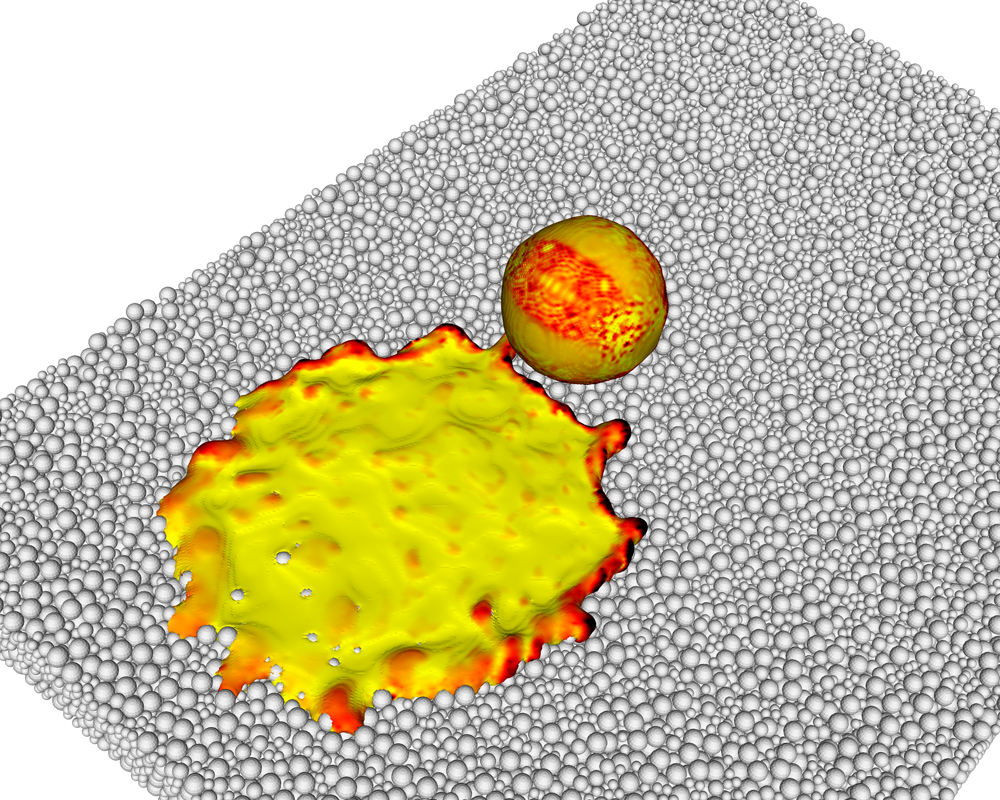
Laser and electron-beam powder bed fusion selectively melt a powder bed. Directed energy deposition feeds material into a melt zone; the feedstock may be powder or wire, depending on the equipment. Melting, flow and solidification are shared phenomena, but feedstock delivery and modelling are not identical.
Taking the example of FLOW-3D, Pareekshith Allu adds that: “Granted, the setup and analysis of such processes in a simulation tool will be different, but at the end of the day, in FLOW-3D, the users will still be taking a CFD-based approach and solving the relevant governing equations to model all these processes.”
For binder jetting, the deposition stage being discussed does not melt the particles. Flow Science proposes analysing binder–powder interaction using particle-size and droplet characteristics. Subsequent debinding and sintering, where required, are separate modelling problems.
“As for material properties, they are inputs into FLOW-3D. The software solution will not change in the sense that a physics-based tool still solves the same underlying governing equations, irrespective of the material properties that are input into the model.”, concludes Pareekshith Allu.
This being said, we still have to determine what a simulation software is capable to achieve in practice.
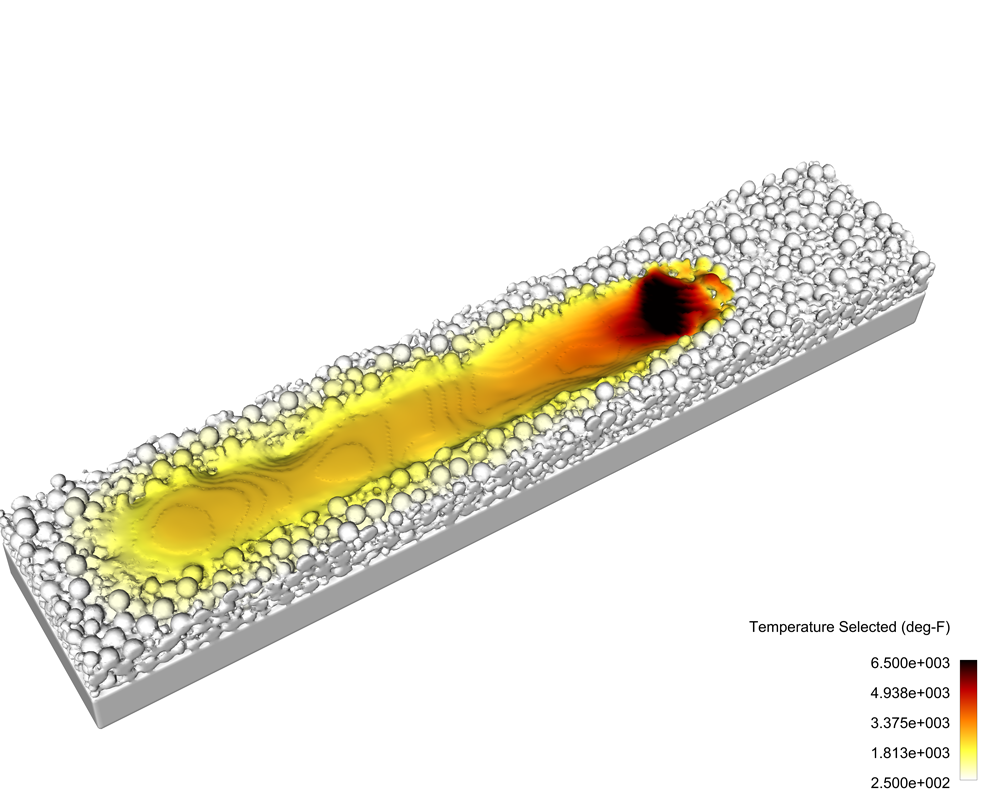
GENOA 3DP: the case presented by AlphaSTAR
– The case of a mount ring bracket for a defense agency
In this feature, AlphaSTAR presents GENOA 3DP as a virtual materials and process analysis tool. Parameters such as printing speed and temperature depend on the case being studied. Rashid Miraj describes its use for a mount ring bracket for a defence agency.
“GENOA 3DP is a micromechanical solution that allows users to virtually qualify each step of the AM process from material characterization, to build simulation/optimization to in-service loading of the printed part.
In the case of a mount ring bracket for a defense agency, GENOA 3DP was able to simulate the additive process from start to finish: beginning with a material model that accounted for temperature dependent properties and the effect of defects; secondly, the utilization of multi-scale progressive failure analysis, to simulate the build and identify manufacturing anomalies related to geometry (i.e. the need for supports) and damage initiation/propagation. Furthermore, the software allowed for Design of Experiments to identify an optimal build path and reduced manufacturing defects such as residual stress. Last and most importantly, the virtual as-built part was subjected to service load in order to ensure that finished product met specification and qualification.”
How does FLOW-3D distinguish itself among others of the same range?
– Effects of random powder distribution and material evaporation on melt pool dynamics
Flow Science presents FLOW-3D as a way to investigate local process phenomena and develop parameter windows. The following example concerns melt-pool dynamics.
Indeed, thanks to the company’s proprietary volume-of-fluid algorithm called TruVOF®, it is possible to track the evolution of the melt pool surface. Coupled to this algorithm are various physics models such as surface tension, viscous flows, laser heating, evaporation pressure, phase change, and solidification. A discrete element method (DEM) has also been integrated to simulate powder spreading and compaction.
For this feature, Flow Science presents a study of powder distribution and evaporation effects on the melt pool.
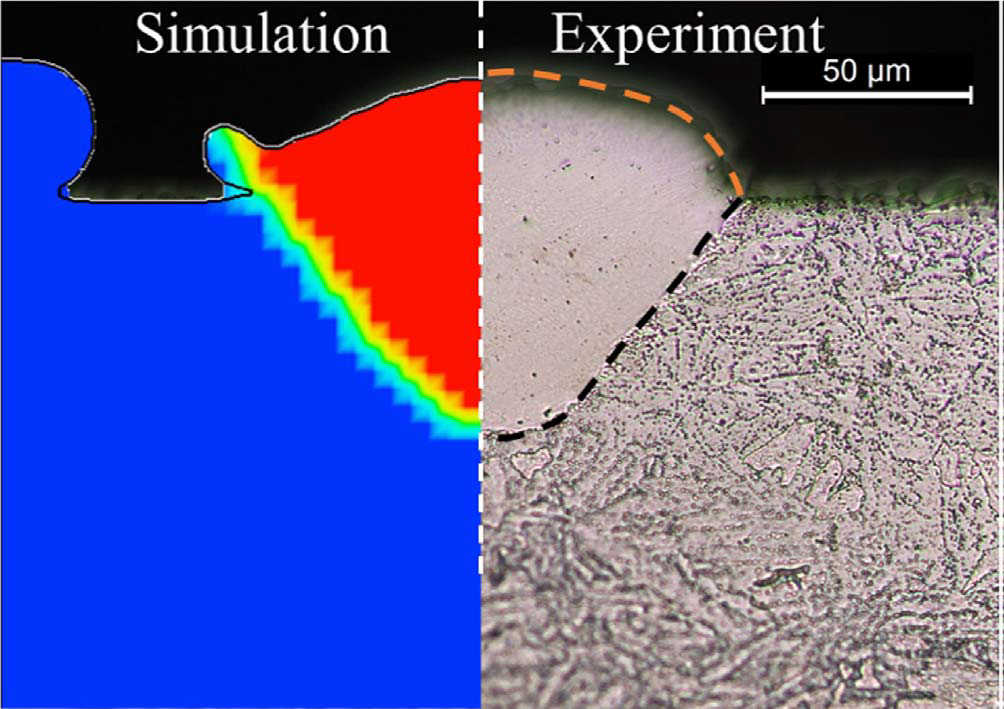
“A three-dimensional numerical model that incorporates a randomly-distributed powder bed and material evaporation was developed using FLOW-3D to investigate melt pool dynamics with keyhole formation in a laser powder bed fusion process. The discrete element method (DEM) was employed to simulate powder packing, which accounts for the motion of a large number of particles including particle/particle and particle/wall interactions. The model was validated by measuring the particle size distributions in specific areas and ensuring that no powder size segregation occurs. Next the flow behavior of the melt pool is characterized by calibrating parameters in the numerical model to achieve good agreement with the experimental results. The importance of including material evaporation in the numerical model is demonstrated by measuring the melt pool dimensions, which turn out to be narrower and deeper than when evaporation effects are not considered. Moreover, a keyholing effect is observed due to the recoil pressure resulting from evaporation, which affects surface morphology and surface temperatures of the melt pool. As illustrated in Figure 1, the contours of the cross-sections of the melt region including the dimensions and surface morphology compare very well between the simulations and experiments, justifying the importance of including evaporation effects.”
This comparison concerns the case and quantities studied. The NIST AM-Bench programme illustrates the role of controlled measurements in evaluating models; agreement for one example does not automatically validate every material, machine or build condition.
The evolution of the simulation software in the additive manufacturing industry
This overview in the world of simulation software gives an interesting perspective on the reasons and the features that users consider crucial to take advantage of a simulation software. Although those companies only share their insights based on their customers feedback or their own experience, keep in mind that, in the end, the most important is that the user is able to know how to produce a metal or polymer part with reliable and repeatable results.
As AlphaSTAR said: “the most important role of software in the AM industry is to see who can deliver finished goods that meet customer demands.”
In their 2019 interviews, the experts identify two needs: calculations completed in a useful time on available computing resources, and suitable material data. The trade-off between accuracy, calculation time and validation depends on the industrial decision being made.
Lastly, it goes without saying that every software company will have its own areas for improvement to watch in order to achieve its business objectives.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.