Feature first published in the September/October 2021 issue of 3D ADEPT Mag and placed online in April 2022. Interviews, roles, estimates and forecasts reflect that original period; later documentary notes are identified explicitly.
Climate change is a topic that is on everyone’s lips. Governmental authorities have sounded the alarm so loudly that both legal entities and individuals feel they have a mission: play their part in addressing climate change issues. Among the multiple fields this problem can be tackled on, there is manufacturing.
Manufacturing contributes to greenhouse-gas emissions through materials, energy and supply chains. The EPA’s 2019 US inventory attributed 23% of national greenhouse-gas emissions to the industrial sector, not solely to manufacturing CO₂. The original European figure of 880 million tonnes lacked a sufficiently defined year and scope for comparison and is not retained as a comparable total. AM is one possible means of changing these impacts, but its benefit must be demonstrated for a defined application.
Here is the thing, AM inevitably involves the contribution of different stakeholders for scaling manufacturing; stakeholders who include a wide range of software experts, material experts, 3D printer manufacturers, or post-processing specialists, just to name a few. How can each of them address climate change issues? This is the million-dollar question we are going to discuss in this exclusive feature.
Climate change: the basics
Climate change concerns sustained changes in climate, not only observations made during the twentieth century. The IPCC’s 2021 assessment attributes warming of the atmosphere, ocean and land to human influence. Increased greenhouse-gas concentrations alter the Earth’s energy balance; warming is accompanied by changes in sea level, ice and other parts of the climate system.

A product carbon footprint estimates greenhouse-gas emissions over a defined life-cycle boundary, expressed in CO₂ equivalents. It is not automatically measured for every product. Materials, production, transport, use and end of life can contribute, depending on the study’s scope.
Climate impact is one part of sustainability, alongside other environmental, social and economic considerations. These concepts should not be treated as interchangeable.
According to Dr. Runze Huang, researcher in sustainability, CEO and Cofounder of ExLattice Inc, “climate change and/or other environmental impacts might be the most mentioned challenges to be addressed, and that could be possibly addressed now, regarding sustainability. Sustainability consists of economic, social, and environmental aspects, which is a much larger concept than climate change. Among those aspects in sustainability, economics is assumed to be addressed most of the time because it’s the traditional fundamental block to business/industry; social aspects are generally complicated, can be extremely difficult to address, and not easily tangible. So, this seems to leave environmental aspects including climate change to be the lower hanging “unaddressed challenge”, and often it leads to thinking that sustainability is being addressed when progress is made regarding climate change.

Secondly or more importantly, it is because addressing climate change and environmental impacts, in many cases, could also benefit the economic and social aspects from a larger perspective. Many measures taken to reduce emissions are related to improving efficiency, reducing waste, and leveraging new technologies, which brings long-term tangible economic gains and job growth at the same time to the factory/business and the whole society.”
Life-cycle assessment (LCA) is an established method for evaluating environmental impacts; a life-cycle inventory is one phase of that assessment, not a synonym for the whole study. ISO 14040 distinguishes goal and scope definition, inventory, impact assessment and interpretation. Material extraction, manufacturing, transport, use and end of life are product-life stages that a study can cover. A relevant comparison requires equivalent function and a consistent boundary.
“A good LCA model generally contains parameterized sub-models for each life cycle stages to estimate energy use/GHG emissions from bottom-up with basic design/engineering data. And it also should include sub-models for various AM processes such as FDM or DMLS, and sub-models for traditional manufacturing processes like machining or injection molding for comparing purposes. The use phase sub-model should be customized for the specific application of the AM parts/products to be analyzed. Such model allows for estimation of the life cycle energy and emission net changes with changing inputs directly from AM users”, Huang notes.
How does this translate into each stakeholder influencing parts production via Additive Manufacturing?
The software perspective
The use of software in an additive manufacturing production requires various capabilities that can be categorized into five main types of software: Design (CAD), Simulation (CAE); Processing (CAM), Workflow (ERP/MES), and QA & Security. Depending on which software publisher an engineer relies on, it is possible to find a software that encompasses one or several of these capabilities.
Should every software company therefore apply the LCA model? The answer is much more complex than we think.
“We must be clear on the challenge we are up to: Not only do we need to reduce carbon emissions — this is where lightweighting could help — but we need to go to zero emissions, and likely less than zero, to stay below critical levels. Under our current engineering and manufacturing models, this change would take generations”, Lin Kayser, Founder and CEO of Hyperganic states from the outset.
According to Kayser, adopting a new engineering and manufacturing paradigm is an “absolute must” and while AM – as a manufacturing process – is a critical step under this paradigm, algorithmic design is another pivotal one.

“We need to engineer objects through computer code, not through the current manual visual process – instead of an engineer drafting a blueprint in a CAD program, this new way of engineering uses algorithms to craft the most intricate and advanced objects in much shorter amounts of time. Coincidentally, this is exactly how Nature works. Nature builds things additively using blueprints or code contained in the DNA. Under our new paradigm, Nature shows us the way forward”, he adds.
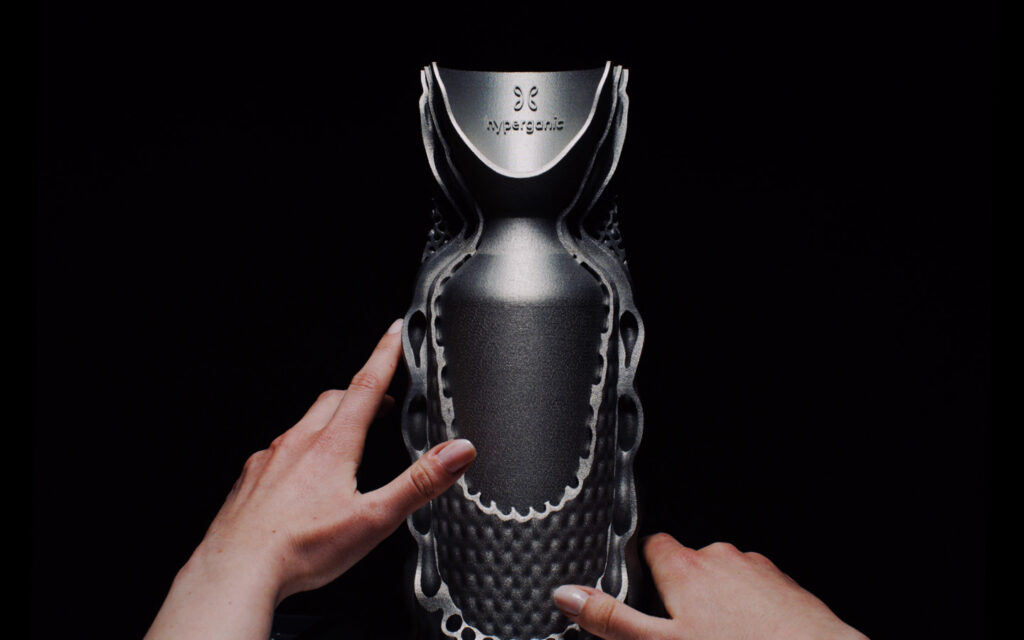
Taking example on Hyperganic Core, a voxel-based geometry platform for AI-based and algorithmic design developed by his company, Kayser explains how interesting it becomes, to create objects by encoding the process one goes through when one designs something into a computer algorithm.
“Instead of creating one object, you create a process that designs objects of that category. Now, you can engineer complex objects in minutes instead of weeks and test out different input parameters quickly, which may result in radically different designs. If you think about it, almost all innovation that we witnessed in the last 40 years came from the Information Technology sector, and is driven by Moore’s Law. A software paradigm encourages re-use, standardized interfaces and accelerated information exchange.
If someone builds a database, I can just use it, I do not need to learn how to build one. If someone builds a better one, I can probably just swap out that component, because it uses a standardized interface. This dramatically speeds up the development of complex software systems. In engineering, on the other hand, people are mostly busy designing the same thing all over again. Any improvement that you make to your objects rely on you, as an engineer, to learn some new tricks and apply new principles. There is little opportunity to share components and use what other people have done. The only way through is buying physical components, and that is a very limited way to re-use ideas”, he adds.
Reusing design logic may shorten engineering work, but this is not identical to reusing physical products or recycling materials. Any environmental benefit of an algorithmic workflow must be assessed through the resulting application and its life cycle.
While this is very interesting, we should recognize that it does not provide tangible data that proves its viability with regards to climate change. This makes us think that one way to measure the positive impact of this approach is through applications. How are applications made? And how do we measure improvements these new applications provide as compared to previous made using other manufacturing processes?
“Most people will think of having more lightweight components or functional integration. This is great, as it is important to save material and get away from “heavy metal” carbon-heavy processes. However, the real impact is going to come from radical innovation, enabled by AM. For example, 3D-printed copper spools for electric motors can have complex shapes that reduce eddy currents. This helps the motor get more efficient at high speeds. 3D-printed battery components can help us improve energy density and enable new types of energy storage in general. New types of AM-enabled rocket engines could enable single stage to orbit. These are just a few instances of how 3D printing can move entire industries towards more sustainable innovations” Hyperganic’s spokesperson said about the reduction of carbon footprint in vehicles.
These examples express Kayser’s expectations in 2021. They are not evidence that a single-stage-to-orbit system or every proposed application had been realised, nor that each would necessarily have a lower life-cycle footprint.
The materials’ perspective and “the dirty little secret of additive manufacturing”.
Energy consumption and carbon footprint are distinct indicators and must not be used interchangeably. Energy can be expressed in joules or kilowatt-hours; greenhouse-gas impact is expressed in CO₂ equivalents. The connection depends on the energy source and on other process emissions. Even low-carbon electricity does not make all upstream material impacts disappear.
Embodied energy refers to energy associated with supplying a material or product within a specified boundary. It should not be confused with thermodynamic internal energy. Changing feedstock and production methods can affect both this energy demand and material properties.
The boundary may include extraction, purification, processing and transport. It must be stated before figures from different materials or processes are compared.
AM can sometimes reduce material requirements through design or reduce use-phase energy through lighter or more efficient components. These possibilities do not establish that every additive route has lower energy demand or emissions than its conventional alternative.
6K Additive is drawing the industry’s attention here to the way materials – especially metals – are produced. According to Frank Roberts, Group President 6K Additive, “it’s at the material production stage that manufacturers can make a real change with regards to sustainability. In metal powder production, the industry is woefully behind on the environmental front. In fact, we refer to this as “the dirty little secret of additive manufacturing”. Specifically in metal powder production, the incumbent technologies use feedstock that needs to be created specifically for their process (such as wire) which consumes energy to manufacture and requires transport (often from overseas).
Their process also creates waste during the manufacturing process that either is sold for scrap value or in the case of titanium will most likely be burned or end in a landfill. Using traditional methods for metal AM powder production, up to 70 percent of the material produced can be waste. A substantial volume of material is produced at unusable sizes and this waste material either goes back into the process – burdening the material with two or three times the energy cost – or is sent to landfill, this process is extremely wasteful.”
Roberts is describing 6K’s assessment of competing processes. Off-size powder is not automatically waste sent to landfill: recovery routes, usable size fractions and allocation of recycling burdens affect the comparison.
At the time of the interview, 6K reported a usable-powder yield above 95% for UniMelt. This is a supplier claim about its process, not a universal guarantee across all alloys, size distributions or operating conditions.


“Additionally, the UniMelt process can use feedstock material sourced from various input streams including machining scrap, used powder, AM supports and failed AM builds. All of these feedstock sources essentially count as near zero carbon footprint, as they are often considered scrap material. 6K Additive recycles and upcycles this “scrap” material into premium powder for AM”, the company’s expert points out.
Recycled inputs do not automatically have a zero carbon footprint. Collection, preparation and conversion can require energy and generate emissions. The GHG Protocol product standard requires a consistent, disclosed approach to allocating impacts between product life cycles.
“The UniMelt system is the world’s first and only industrial-grade microwave plasma production process that has a yield of near 100 percent, almost eradicating the production of unusable powder, and in addition uses scrap or used material as feedstock. This represents a true circular economy by recycling powders and materials from many different sources to be used in the UniMelt process – certified scrap materials from CNC manufacturing, used AM powders, failed models, even condensate materials from AM equipment. Using the UniMelt system to recycle these materials into premium metal AM powders, without losing any performance credentials in the process, merits a true sustainable alternative.
Additionally, the UniMelt process uses significantly less energy and gas to produce powder. Because the material is pre-sized prior to being put through the process, the UniMelt is only spheroidizing the material using far less gas than atomization. Additionally, because the material coming out of the process is the correct size, the post-processing time and energy after is also far less in the 6K Additive process. Below are four charts that illustrate these points. We currently have contracted with a 3rd party environmental agency to conduct a Life Cycle Assessment on the 6K Additive process against the incumbent technologies. This report is expected to be finalized in mid-Q4, 2021. Based on information we’ve received from industry experts and customers the below charts illustrate the energy comparison against other material manufacturing processes”, Frank Roberts told 3D ADEPT Media.

Historical note: the quoted fourth-quarter 2021 deadline belonged to the original interview. 6K announced LCA results from Foresight Management on 20 April 2022. The results concern the powders and boundaries studied and should not be generalised to every metal or finished part. The four preliminary charts reproduced above omit numerical scales and units, so they cannot independently establish an energy-reduction percentage.
During the original reporting, 6K described work with Relativity on powder derived from scrap, as well as relationships with Form3D and Castheon. These statements concern the developments reported at that time. A powder specification or a supplier’s test result does not, on its own, qualify an end-use space component.
The original 6K graphic reported the following mechanical-property figures for specimens made using Ni718 and Ni625 powder. These are supplier-reported results and comparison values, not a certificate for an individual powder batch or part. The data are transcribed below to make them readable and accessible.
| Direction and condition | YS (MPa) | UTS (MPa) | EL (source label: “5%”) |
|---|---|---|---|
| XY — 6K (HT) | 1227 | 1455 | 19 |
| XY — 6K (HT & HIP) | 1220 | 1413 | 23 |
| XY — ASTM F3055 (HT) | 940 | 1240 | 12 |
| Z — 6K (HT) | 1241 | 1372 | 22 |
| Z — 6K (HT & HIP) | 1282 | 1413 | 24 |
| Z — ASTM F3055 (HT) | 940 | 1240 | 12 |
| Direction and condition | YS (unit not shown) | UTS (unit not shown) | EL | RA |
|---|---|---|---|---|
| XY — 6K (HT) | 429 | 897 | 54% | 60% |
| XY — ASTM F3056 | 275 | 485 | 30% | 30% |
| Z — 6K (HT) | 345 | 886 | 55% | 59% |
| Z — ASTM F3056 | 275 | 485 | 30% | 30% |
Source: 6K’s original graphic. YS: yield strength; UTS: ultimate tensile strength; EL: elongation; RA: reduction of area; HT: heat treatment; HIP: hot isostatic pressing. The Ni718 elongation heading and Ni625 strength units are not clearly specified in the image. Test details and standard editions must be checked before engineering use. View the original supplier graphic.
What about non-metals?
Polymer and composite routes can be alternatives where their mechanical, thermal and service requirements are suitable. Replacing metal with polymer does not automatically lower life-cycle impact; durability, the amount of material needed and end-of-life options also matter.
PolySpectra’s stated ambition was to develop durable AM polymers and processes with lower carbon footprints. That ambition must be distinguished from independently established performance across applications.
PolySpectra developed COR Alpha, a cyclic olefin resin, and promoted its mechanical and thermal properties for durable applications. Suitability relative to an injection-moulded polymer must be assessed against the particular requirements and test conditions.
We mention the material today because the producer strongly believes that “in order to have a chance of making an impact [in climate change], you first need 3D-printed materials with the performance and durability to displace traditional manufacturing processes.”
In its 2019 explanation of COR Alpha’s environmental potential, polySpectra provided the estimated figures reproduced below. They are expressed per kilogram of polymer, not per functionally equivalent finished product. They should not be read as a complete comparative LCA with identical service life, geometry and performance.
| Polymer | Material production | Part forming | Total |
|---|---|---|---|
| ABS | 3.6 | 1.3 | 4.9 |
| Nylon 6 | 6.7 | 1.3 | 8.0 |
| Epoxy thermoset | 8.0 | 1.3 | 9.3 |
| polySpectra COR Alpha | 4.0 | 0.1 | 4.1 |
Source: polySpectra’s 2019 estimates, reproduced in the original feature. This mass-based comparison does not establish equivalent functional performance or a full life-cycle advantage. View the original table image.
“With COR Alpha, we can 3D print parts with the strength, toughness, and working temperatures of today’s state-of-the-art polymers — with the bonus of a significantly reduced carbon footprint. If we’re successful at using polymers like COR Alpha to dramatically lower the energy required to manufacture durable goods, we’ll unlock a new paradigm of energy-efficient manufacturing by leveraging chemical bonds to displace the work currently performed by electrons. This could have a huge effect on the energy requirements and carbon footprint of manufacturing — and could be a climate change difference maker”, Raymond Weitekamp, Founder and CEO of PolySpectra declares.
The manufacturing perspective
Process energy varies with the AM technology, material, build utilisation, supporting equipment and post-processing. Some routes have substantial energy demands. Neither AM nor machining is uniformly better on this measure; comparable functional output and study boundaries are essential.
In the same 2019 explanation, Weitekamp stated that “DLP printing processes can use as little as 1% of the energy of an injection moulding tool.” This is a supplier comparison of selected equipment, not a demonstrated hundredfold improvement for equivalent finished parts across applications. Power, operating time, throughput and upstream impacts must be included before drawing that conclusion.
Measurement methods such as LCA already exist. The challenge is obtaining sufficiently transparent, representative data and making comparisons on consistent terms.
And…transportation?
Transport and storage form part of the supply-chain assessment. On-demand production can reduce some inventories and deliveries, but its effect depends on where feedstocks are made, machine utilisation, shipment modes and the local energy mix.
The Covid-19 pandemic encouraged experimentation with distributed manufacturing. Shorter supply chains can improve response times, but they do not automatically produce lower life-cycle emissions.
This also raises questions about how distributed production affects existing suppliers and employment. The outcome depends on the application and the economic context.
To this, Dr. Runze Huang responds that “the impact would be noticeable in the short term. Decentralized production is a nice concept but does not bring large enough benefits for a major shift for most of the companies. It was applied more recently due to the impact of COVID-19 and its disruption of the existing supply chains. As that supply chain gets stable, the scale of the economy still works and dominates. And it depends on whether having a decentralized model can lead to a reduction in footprints from a life cycle perspective.” For the expert, “companies should focus more on the application than the supply chains.
The potential benefits and impacts, both environmentally and economically, of the use phase are still greatly larger than the other life cycle stages combined in a lot of cases. The differences can be an order of magnitude. I think it applies to our AM industry, not just companies using distributed models. The best and fittest application wins.”
Concluding notes
AM can support new or complementary business models, but the necessary infrastructure varies. Digital coordination, skills, equipment utilisation and product requirements all affect whether a model is viable.
Complexity does not make LCA inapplicable. It makes transparent boundaries, assumptions and uncertainty more important. Other indicators can complement the assessment, especially for social and economic effects, without replacing a justified environmental comparison.
The 2020 framework proposed by Godina and colleagues illustrates roles for public bodies, suppliers, researchers, service providers and users. It is a framework for assessment, not proof of emissions savings. Evaluating a particular application remains central.

THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.