

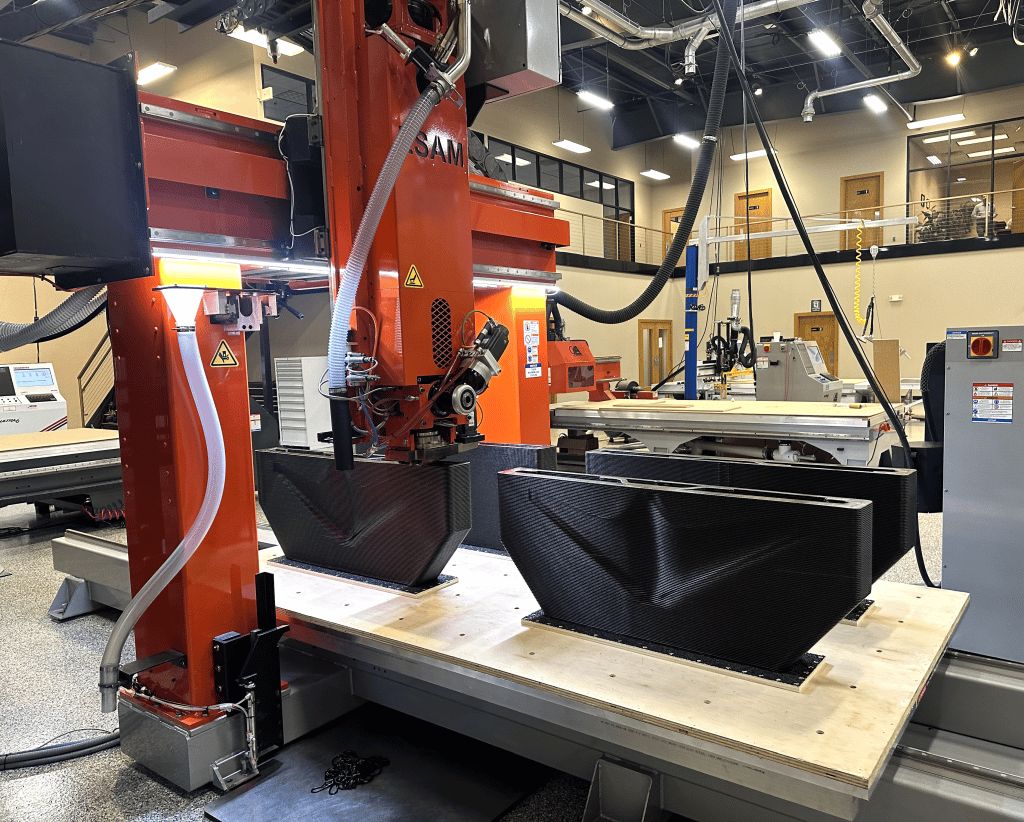
The conversation about AM certification has mainly focused on certified end-use parts governed by airworthiness authorities. In particular, these include metal components going into engines or airframes. In the meantime, the demand for large-scale parts continues to grow, as “we are past the “proof of concept” phase of large-format additive manufacturing”, in the words of Thermwood’s Scott Vaal.
Thermwood is one of the few companies providing very large format 3D printing hardware and services with composite chopped Fiber Reinforced Polymer (FRP) pellet materials. LSAM’s primary aerospace applications are tooling: autoclave molds, layup tools, jigs and fixtures. Knowing this, one might assume the qualification burden is lighter than for flight parts. Tooling never flies, after all. It just has to survive what happens on the ground.
Why aerospace tooling needs its own qualification
Vaal immediately warns us about this: “Don’t confuse a different burden with a lesser burden. The fundamental difference comes down to risk categorization: a flight part carries “life-and-death” airworthiness risks, whereas a tool carries “yield and economic” risks. Because the tool never leaves the ground, it isn’t directly governed by the FAA or EASA in the same strict, fatigue-life manner as a metal engine bracket.
Aerospace composite flight parts are cured on these tools in autoclaves under immense heat and pressure. If the tool fails, if it distorts or if the Coefficient of Thermal Expansion (CTE) isn’t compensated correctly, or if it loses vacuum integrity, you lose the highly expensive flight part being molded.
Therefore, the qualification of the tool is strictly tied to verifying its ability to repeatedly facilitate the production of a certified flight part without degrading. We aren’t proving the tool can fly; we are proving the tool can reliably survive extreme thermal cycling while maintaining tolerances of a few thousandths of an inch.”
The questions behind LSAM qualification
- – So, when does “achieving consistent quality” in LSAM begin?
- – Do certification programs built around metal powder bed fusion apply when it comes to large-format polymer composite AM?
- – Are the qualification and certification pathways of LFAM parts very different from what we see in aerospace?
We put these questions to Vaal and explored Thermwood’s approach to qualification & certification in this FOCUS. Vaal is one of the sharpest voices we know on the LFAM topic. As product manager of Thermwood’s LSAM, he has been close to it all: the breakthroughs, the setbacks, and the places where the industry still has work to do.
Qualification process for an LSAM-produced aerospace tool
In LSAM’s primary aerospace applications, tooling still has to meet demanding dimensional and thermal performance requirements. These include accurate CTE compensation, vacuum integrity, and autoclave cycle resistance.
According to Vaal, “achieving consistent quality begins long before the extruder heats up. It starts with the material formulation and pellet drying, and then moves into the slicing software. In LSAM, thermal management is everything. If your software doesn’t anticipate the thermal gradient of the layer below it, you won’t get good interlayer adhesion, period.
As for formal qualification today: there is no single, universally established framework across the industry just yet. Currently, each major aerospace customer defines their own acceptance criteria. A typical qualification process looks like this:
- – First, material testing (Tg verification, void content analysis, CTE measurement).
- – Second, printing a sub-scale tool to test vacuum integrity (this is the holy grail), because if a tool leaks vacuum, it’s useless for autoclave molding.
- – Finally, the tool is subjected to a certain number of autoclave cycles (e.g., 10 to 50 cycles at 350°F and 90 psi). After cycling, it is scanned with a CMM or laser tracker. If the dimensional drift is within their strict tolerances, and vacuum integrity holds, the tool is qualified for production use.”
Qualifying the part, however, is only half the equation. The harder question is how you qualify the machine that produced it in the first place. The industry is still working through this. No universally established framework exists in this space yet.
Beyond the parts: qualification of LSAM systems
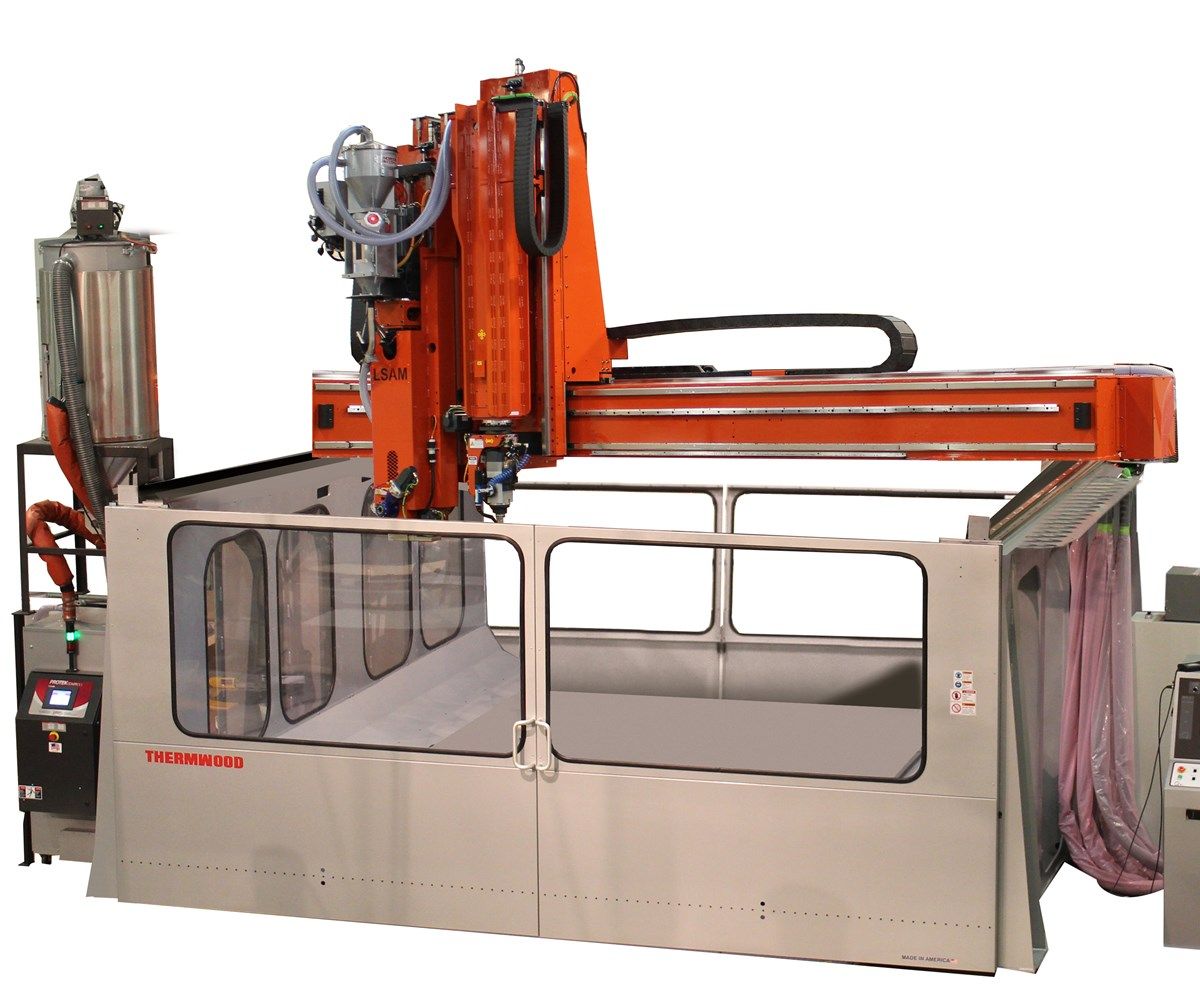
In additive manufacturing, parts, materials, machines, and manufacturing processes each carry their own qualification logic. Certification, meanwhile, is typically applied to the final part, the manufacturing organization, or the production process under a specific regulatory framework.
Some process-specific certification programs focus on metal powder bed fusion, while broader AM quality frameworks also cover other processes and materials. The ASTM AM CoE certification program addresses a specific gap. Traditional QMS standards like ISO 9001 and AS9100 do not specifically address the risks and processes of AM.
Large-format polymer composite AM nevertheless has its own qualification challenges. Vaal notes:
“Traditional Quality Management Systems (QMS) like ISO 9001 and AS9100 are heavily geared toward traceability and subtractive/traditional manufacturing processes. They don’t natively comprehend the variables of large-format polymer extrusion. Even the ASTM frameworks developed for metal Powder Bed Fusion (PBF) don’t map well to LFAM.
In LFAM, we are dealing with immense thermal mass. Variables like layer time, ambient environment, polymer melt temperature, and the specific mechanical compression force applied to the bead (which we at Thermwood control via our patented compression roller) dictate the z-axis strength and porosity of the part. Standardizing these macroscopic thermal-fluid dynamics requires a completely different set of metrics than laser-melting microscopic metal powders. ASTM and others are making strides, but there is still a gap that machine OEMs and material suppliers are bridging through rigorous internal standards.”
Verifying machine repeatability
Process qualification in aerospace typically requires demonstrating both material consistency and machine repeatability across runs, operators, and time.
Thermwood’s answer to this starts somewhere most AM companies don’t: in over 50 years of precision machine tool manufacturing. The company didn’t arrive at LFAM from the world of 3D printing. It came from building industrial-grade CNC routers. That heritage shapes everything about how it thinks about process qualification.
For Vaal, it’s the same rigorous protocol applied to a five-axis router. “Installation Qualification (IQ) involves standard machine-tool protocol: laser calibration, volumetric compensation, and leveling to ensure the gantry is perfectly true”, he notes, before adding: “For Operational and Performance Qualification (OQ/PQ), we absolutely support our customers; we do not just drop the machine off and wish them luck.
We conduct rigorous Factory Acceptance Testing (FAT) and Site Acceptance Testing (SAT). This involves printing standard geometries to verify volumetric extrusion rates, thermal controls, and layer bonding. Because we offer a vertically integrated “print-and-trim” system, PQ often culminates in printing and machining a demonstration tool with the customer’s chosen high-temp material (like carbon-filled PESU or PEI).
We prove out the machine’s repeatability across operators by handing over a system that has just successfully produced a vacuum-tight, dimensionally accurate tool in their facility.”
Qualification and certification pathways of LFAM parts beyond aerospace
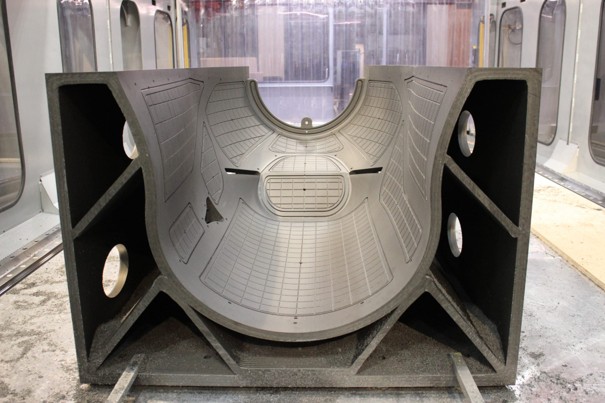
LFAM is no longer an aerospace-only story. As we observed at JEC 2026, the technology is making inroads across a much broader range of sectors such as automotive & motorsport, marine, architecture, furniture, and more. Each with its own logic, its own tolerance for risk, and its own definition of “good enough.”
Which raises an obvious question: are the qualification and certification pathways for LFAM parts radically different depending on the sector?
Short answer from Vaal:
“It’s night and day. Take the marine industry, or industrial thermoforming, for example. When we print large boat hull molds or plugs, the thermal and pressure requirements are drastically lower. These are often room-temperature or low-temperature cures.
In those industries, qualification is highly empirical and pragmatic: “Did the print hold the shape? Did it machine well? Does the final fiberglass or thermoformed part pop off the mold looking good?” If yes, the tool is qualified. They prioritize speed to market, massive cost reduction, and basic geometric fidelity.
Aerospace, on the other hand, requires a deep, data-driven paper trail proving the polymer chain didn’t degrade and dimensional stability of 0.005” was maintained over a 10-foot span under 90 psi.”
How to differentiate in the non-exhaustive list of LFAM OEMs?
When Thermwood first entered this space, only a handful of companies were providing very large format 3D printing hardware and services with composite chopped Fiber Reinforced Polymer (FRP) pellet materials. Technology and the market have matured considerably since then. The field now includes more players among which others entering from robotic and hybrid platforms.
“In the early days, the competitive differentiator was simply size: “Who can build the biggest printer?” Today, size is a given. The differentiation has shifted to reliability, vacuum integrity, and software integration.
At Thermwood, we differentiate ourselves by being a true machine tool builder. We are not simply mounting an extruder onto the end of a robotic arm. We engineer rigid, dual-gantry systems capable of both printing and machining on the same platform. This integrated approach provides the stability, precision, and repeatability required for industrial-scale additive manufacturing. LSAM systems deliver exceptional material consistency through our patented Melt Core technology.
Our patented bead compression roller technology has been proven to reduce inter-bead voids, improve interlayer bonding, and maximize lateral bead-to-bead integrity, all critical factors for high-temperature autoclave tools where vacuum integrity is non-negotiable. Then there is software, an often-unseen factor behind consistent results.
Our proprietary LSAM Print3D slicing software is purpose-built for the platform, and combined with dynamically managed Layer Time Control, it continuously maintains optimal print temperatures throughout the process,” Vaal says.
Repeatability and early collaboration
What Thermwood is betting on, in other words, is predictability as the LFAM market matures and consolidates. The companies that will hold ground are not those that built the biggest machines but those that built the most predictable ones. The differentiator is now the process envelope: the ability to deliver repeatable, production-grade results across operators, facilities, and programs. That means not treating every job as an experiment.
“LSAM is a proven, production-ready technology that is currently saving aerospace companies millions of dollars and months of lead time. My advice to any manufacturer looking into this is to collaborate early. Bring your material suppliers, your engineers, and your machine OEM to the table at the very beginning of a project. When you align the material chemistry, the print strategy, and the machining tolerances from day one, the results are nothing short of revolutionary,” Vaal concludes.
*This article was first published in the May/June edition of 3D ADEPT Mag
Source: ASTM AM CoE — Formnext 2025, certification across seven AM process families.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.