

Ultrasound can support several stages of additive manufacturing, from powder production and removal to inspection. Ultrasonic additive manufacturing (UAM) also names a distinct solid-state metal joining process. This feature explains the difference with Solukon and Fabrisonic.
Archive context: these interviews were first published in July/August 2024. Roles, prices and business observations refer to that period. EWI records subsequently announced Jason Riley as Fabrisonic CEO in September 2024 and its acquisition by United Performance Metals in March 2025.
Simply put, “ultrasonic” refers to a frequency greater than the upper limit of the audible range for humans —that is greater than 20 kilohertz. Frequency and amplitude are different properties: a high amplitude alone does not make a sound ultrasonic. This implies that the term itself is not limited to the manufacturing field. By sticking to this basic definition, Andreas Hartmann, CEO & Cofounder of Solukon Maschinenbau GmbH said “it is therefore always about the stimulation of a substance or material.”
In the AM industry, Hartmann identified two types of ultrasonic usage: “applications where the main purpose is to use ultrasound technology – This is the “Ultrasonic Additive Manufacturing as a fabrication process” but also, for example, ultrasonic cleaning equipment.” “The second area of application is, in my view, where ultrasound is used as a feature or add-on or extension of an existing technology. For example, as with our SFM-AT350-E powder removal system. In LPBF [for instance], ultrasonic excitation is used in various process steps like depowdering, powder recovery, powder preparation (sieving) or final cleaning in ultrasonic fluid baths. Ultrasonics are often required where certain material properties like flowability are challenging,” he adds.
Ultrasound as a tool in the AM process chain
Today, ultrasonic technology is utilized in several industrial applications, to measure distances, for parking assistance, flow-rate measurement, level detection, and composition analysis. The development of smart machines and the Internet of Things have paved the way for applications of ultrasonic sensors.
According to Hartmann, if little information is shared about the use of ultrasonic technology as an add-on to an existing technology, it’s probably because “the know-how usually lies with external experts who offer their ultrasound solutions for many industries”, not to mention that developers of ultrasound solutions are keen to protect their “intellectual property”.
We don’t often realize it, but different stages of the AM process chain can benefit from ultrasonics. “First of all, applying ultrasonic in powder removal is beneficial for the overall process chain. With the precise tracking of its parameters and the possibility of fine adjustment, it effortlessly achieves all the sophisticated objectives of process monitoring and therefore quality assurance.
As Ultrasonic works electrically with only little energy consumption it means significant energy-saving potential for the entire production chain and drives sustainability.
Furthermore, thinking of other steps of the production line, ultrasonics can be integrated into the AM process for real-time monitoring and quality control:
Defect Detection: ultrasonic sensors can detect internal defects such as porosity, cracks, and delamination during the build process. This allows for immediate correction or rejection of defective parts. Process Optimization: real-time feedback from ultrasonic sensors can help optimize process parameters, such as laser power and scanning speed, to improve part quality,” Hartmann explains.
These comments describe potential uses, not a universal guarantee of inspection coverage or automatic correction. Detectability and energy savings need to be assessed for the particular equipment, material and workflow. Depowdering is also distinct from internal-defect inspection.
Key examples
The experts from Zetec are using ultrasonics to support nondestructive testing (NDT) methods for 3D printed parts. Ultrasonic NDT Methods consist of using various ultrasonic imaging methods to detect porosity and other flaws in 3D printed metals.
In research announced by the University of Bristol in April 2024, a mathematical model was developed to guide the design of non-contact laser-based ultrasonic arrays. It models wave propagation through layered AM metals and how sensor parameters affect the information available. The work was preparation for experimental deployment, not an already qualified production inspection system.
“There is a potential sensing method using a laser-based ultrasonic array and we are using mathematical modeling to inform the design of this equipment ahead of its in situ deployment,” said Professor Anthony Mulholland, head of the School of Engineering Maths and Technology.
The researchers described collaboration and experimental validation as next steps. Their announcement did not establish a timetable for commercial adoption.
In the materials segment, we have seen AMAZEMET, a developer of laboratory-scale units for the in-house manufacturing of powders, use ultrasonic vibration for metal atomization. With its rePowder machine, metal is poured or melted directly on the vibrating part resulting in tiny droplets being ejected from the surface. Droplets solidify in the surrounding inert gas atmosphere forming powder particles. This leads to highly spherical metal powders with narrow particle size distribution – up to 80% is good to use in desired processes, the company explains.
The quoted powder yield is a manufacturer figure whose relevance depends on alloy, target size fraction and operating conditions. It should not be treated as a guaranteed yield for every AM process.
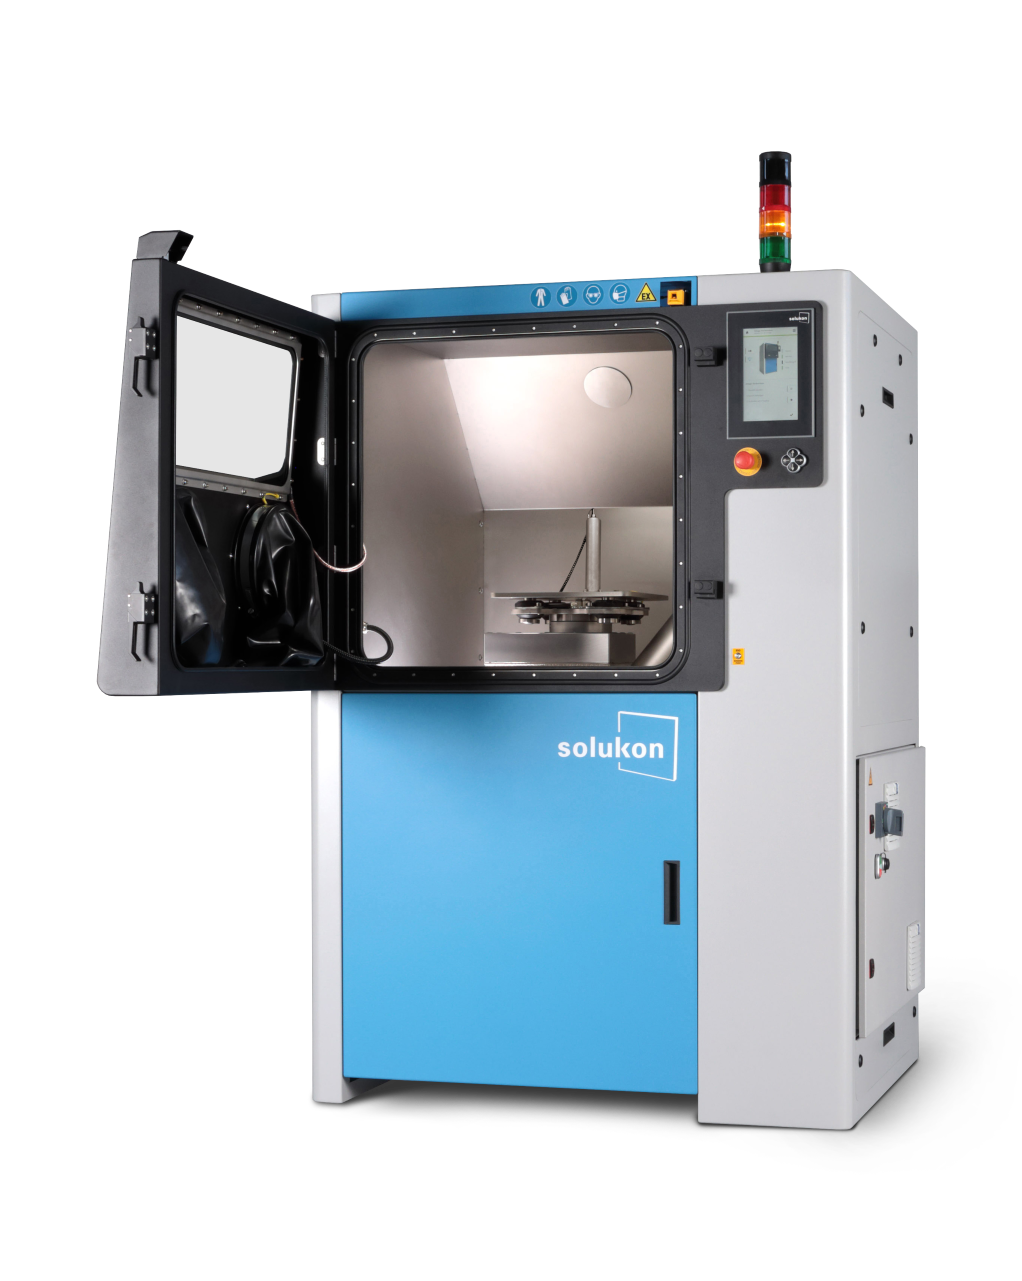
In depowdering, Solukon uses ultrasonic excitation as an option on its SFM-AT350-E. Selection between pneumatic and piezoelectric excitation depends on the component and cleaning requirements.
“From nearly a decade experience in depowdering, we saw that for certain geometries pneumatic excitation reaches its limits. This is especially the case for delicate structures like long winded channels or lattice structures like in medical industry. The main aim of ultrasonic excitation is to excite the component above the damaging natural frequency of the part. Initially, we had several tests with external ultrasonic exicators integrated into a depowdering machine. They proved to be successful and appeared to be a game-changer in some specific applications – for instance, copper. So, we decided to launch a dedicated depowdering system, the SFM-AT350-E with piezoelectric (=ultrasonic) excitation.
Ultrasonic depowdering solutions will not replace the well-established and proven solution with pneumatic excitation and an optional knocker. Pneumatic turbines are simple, robust and depowder very efficiently; especially for large and heavy parts, this is the way. Launching an ultrasonic depowdering solution, we have rather created a wealth of variants to adapt even better to the individual requirements of our customers. It is like a new dedicated tool in our big toolbox for powder fluidization,” Hartmann points out.
For Solukon’s CEO/CTO, the use case of ultrasound shows that there is always a need to further develop core technologies and exchange ideas with experts from other fields.
Ultrasonic additive manufacturing as a fabrication process
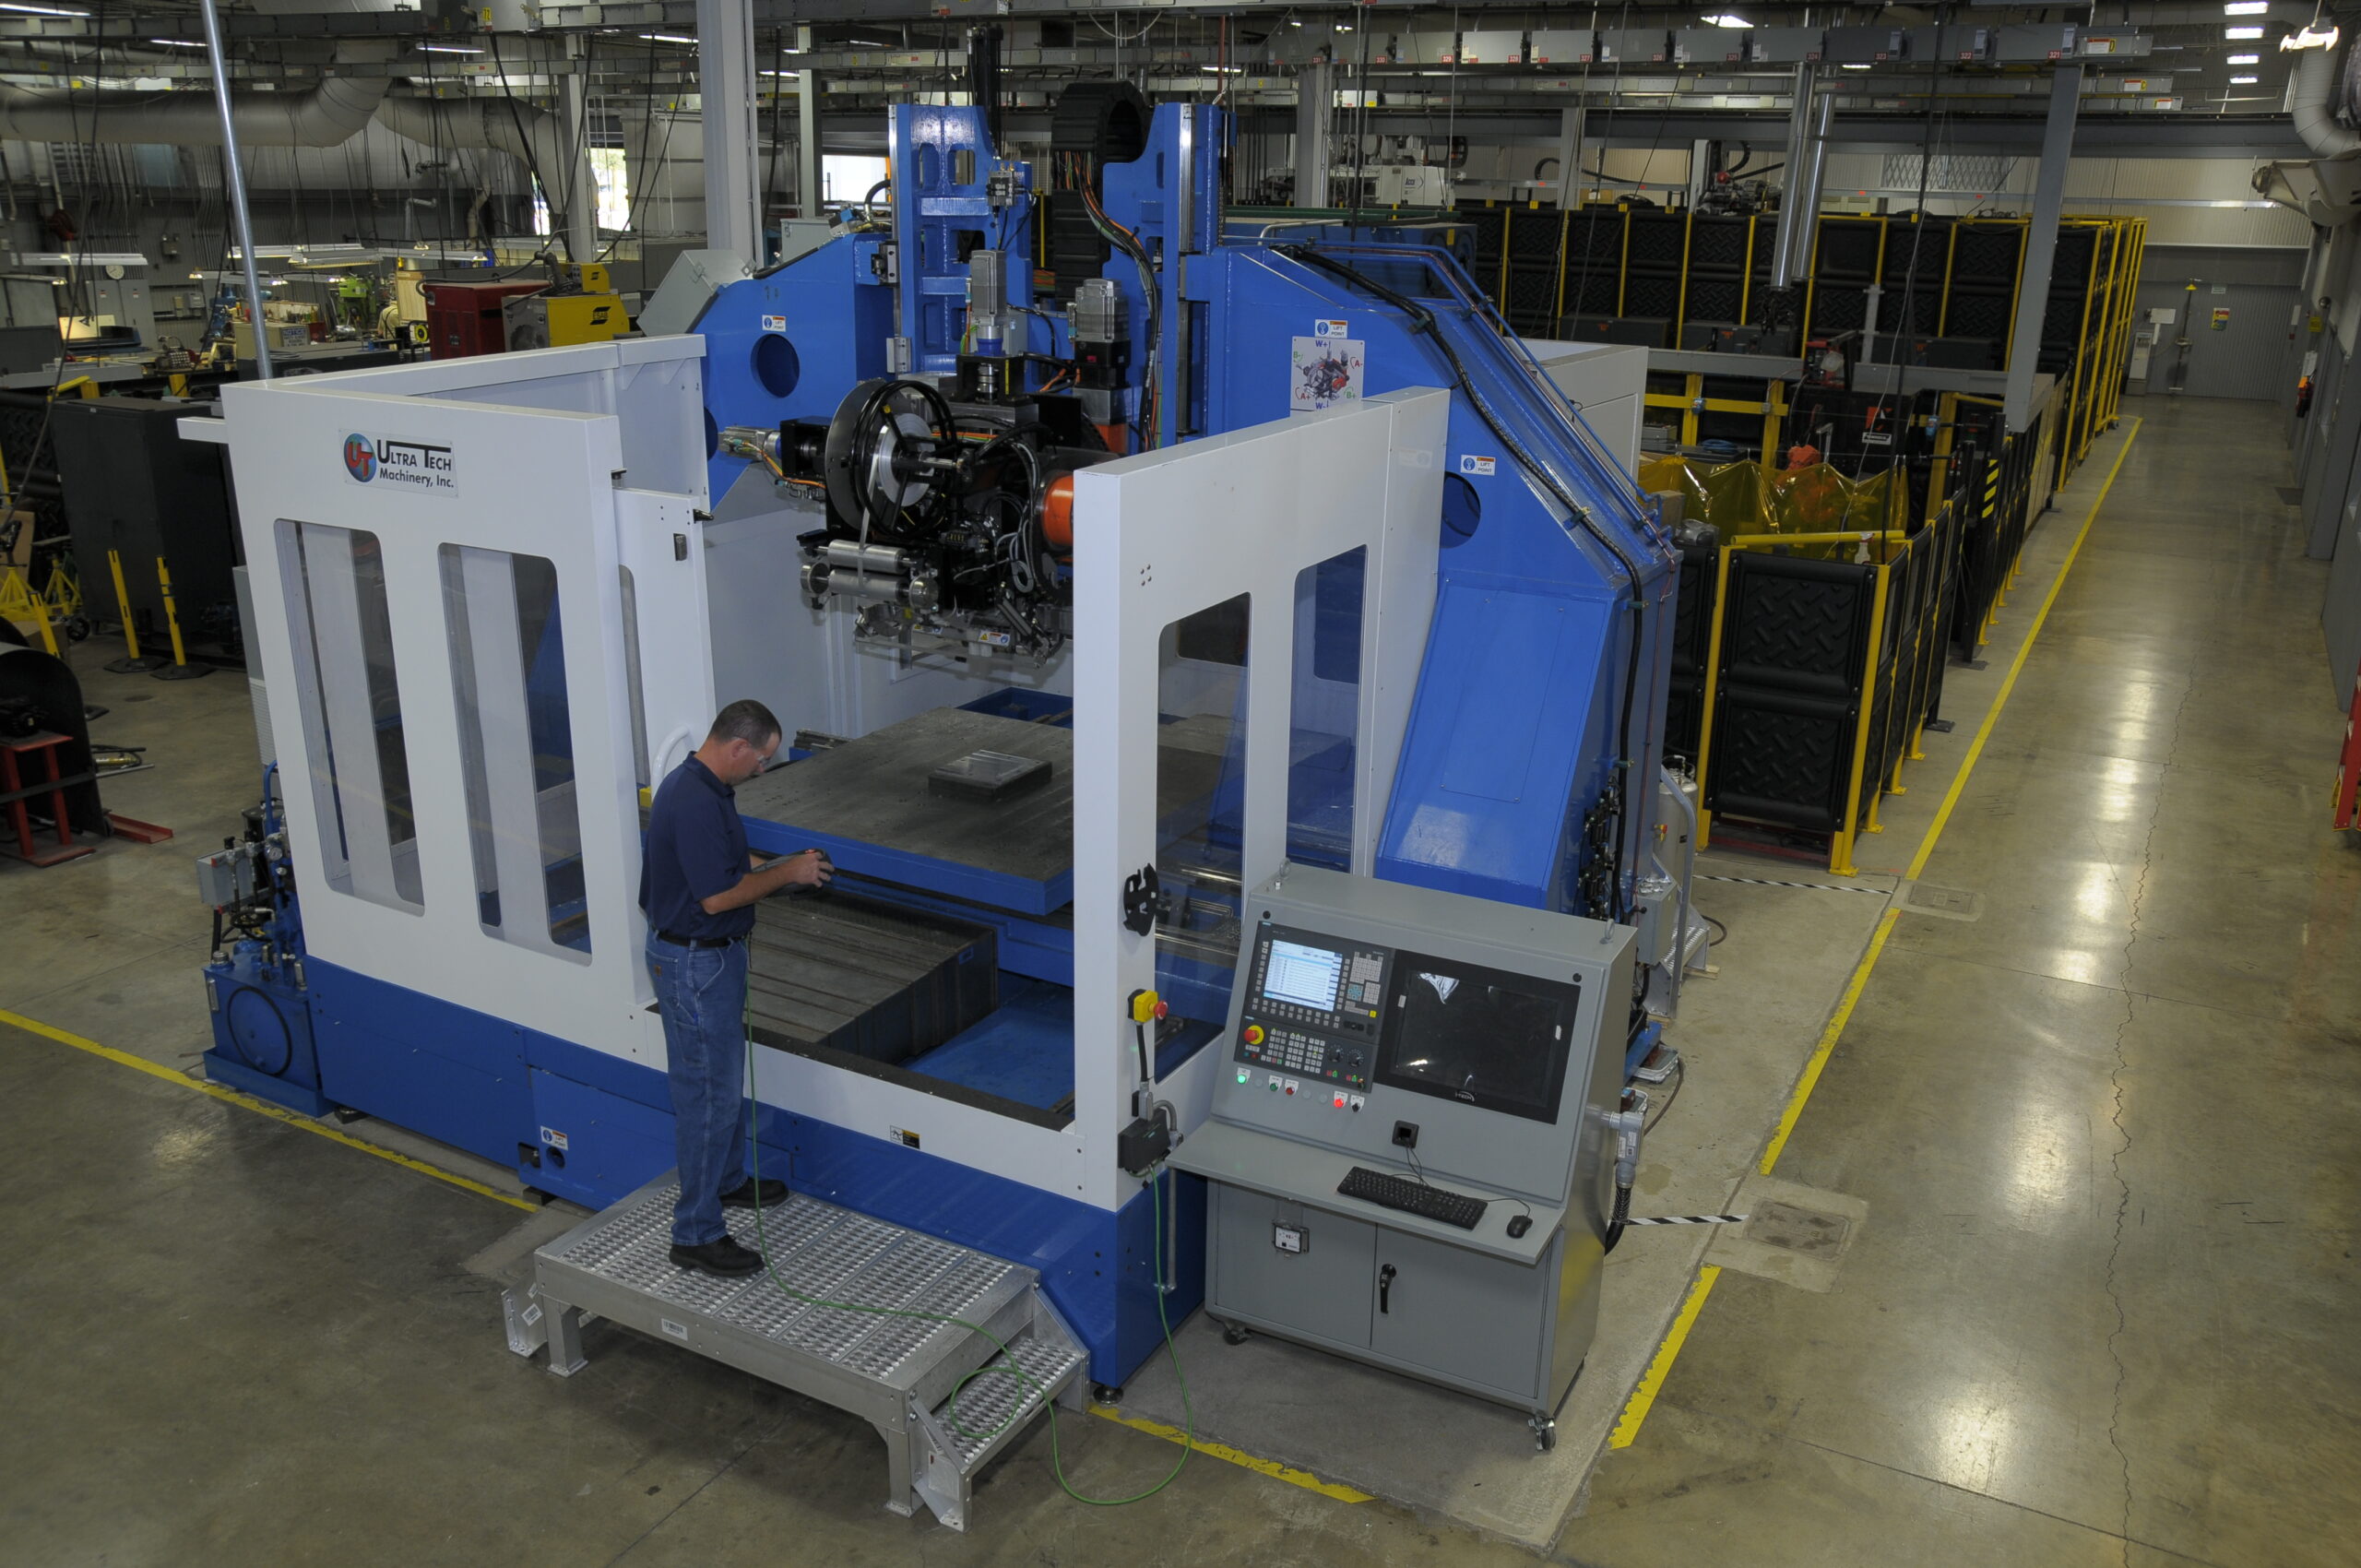
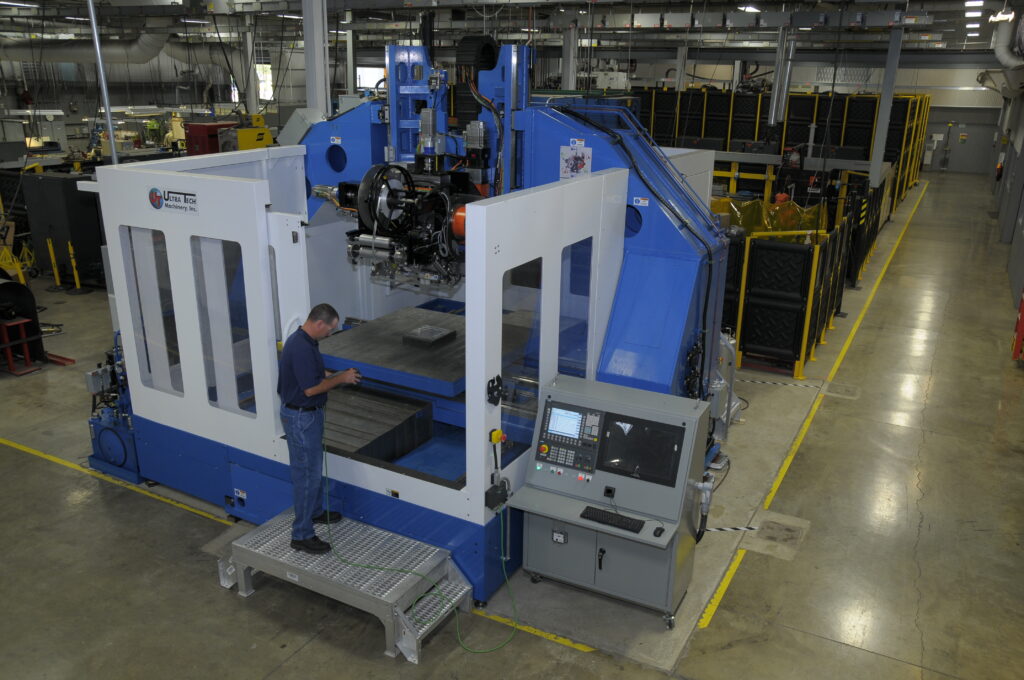
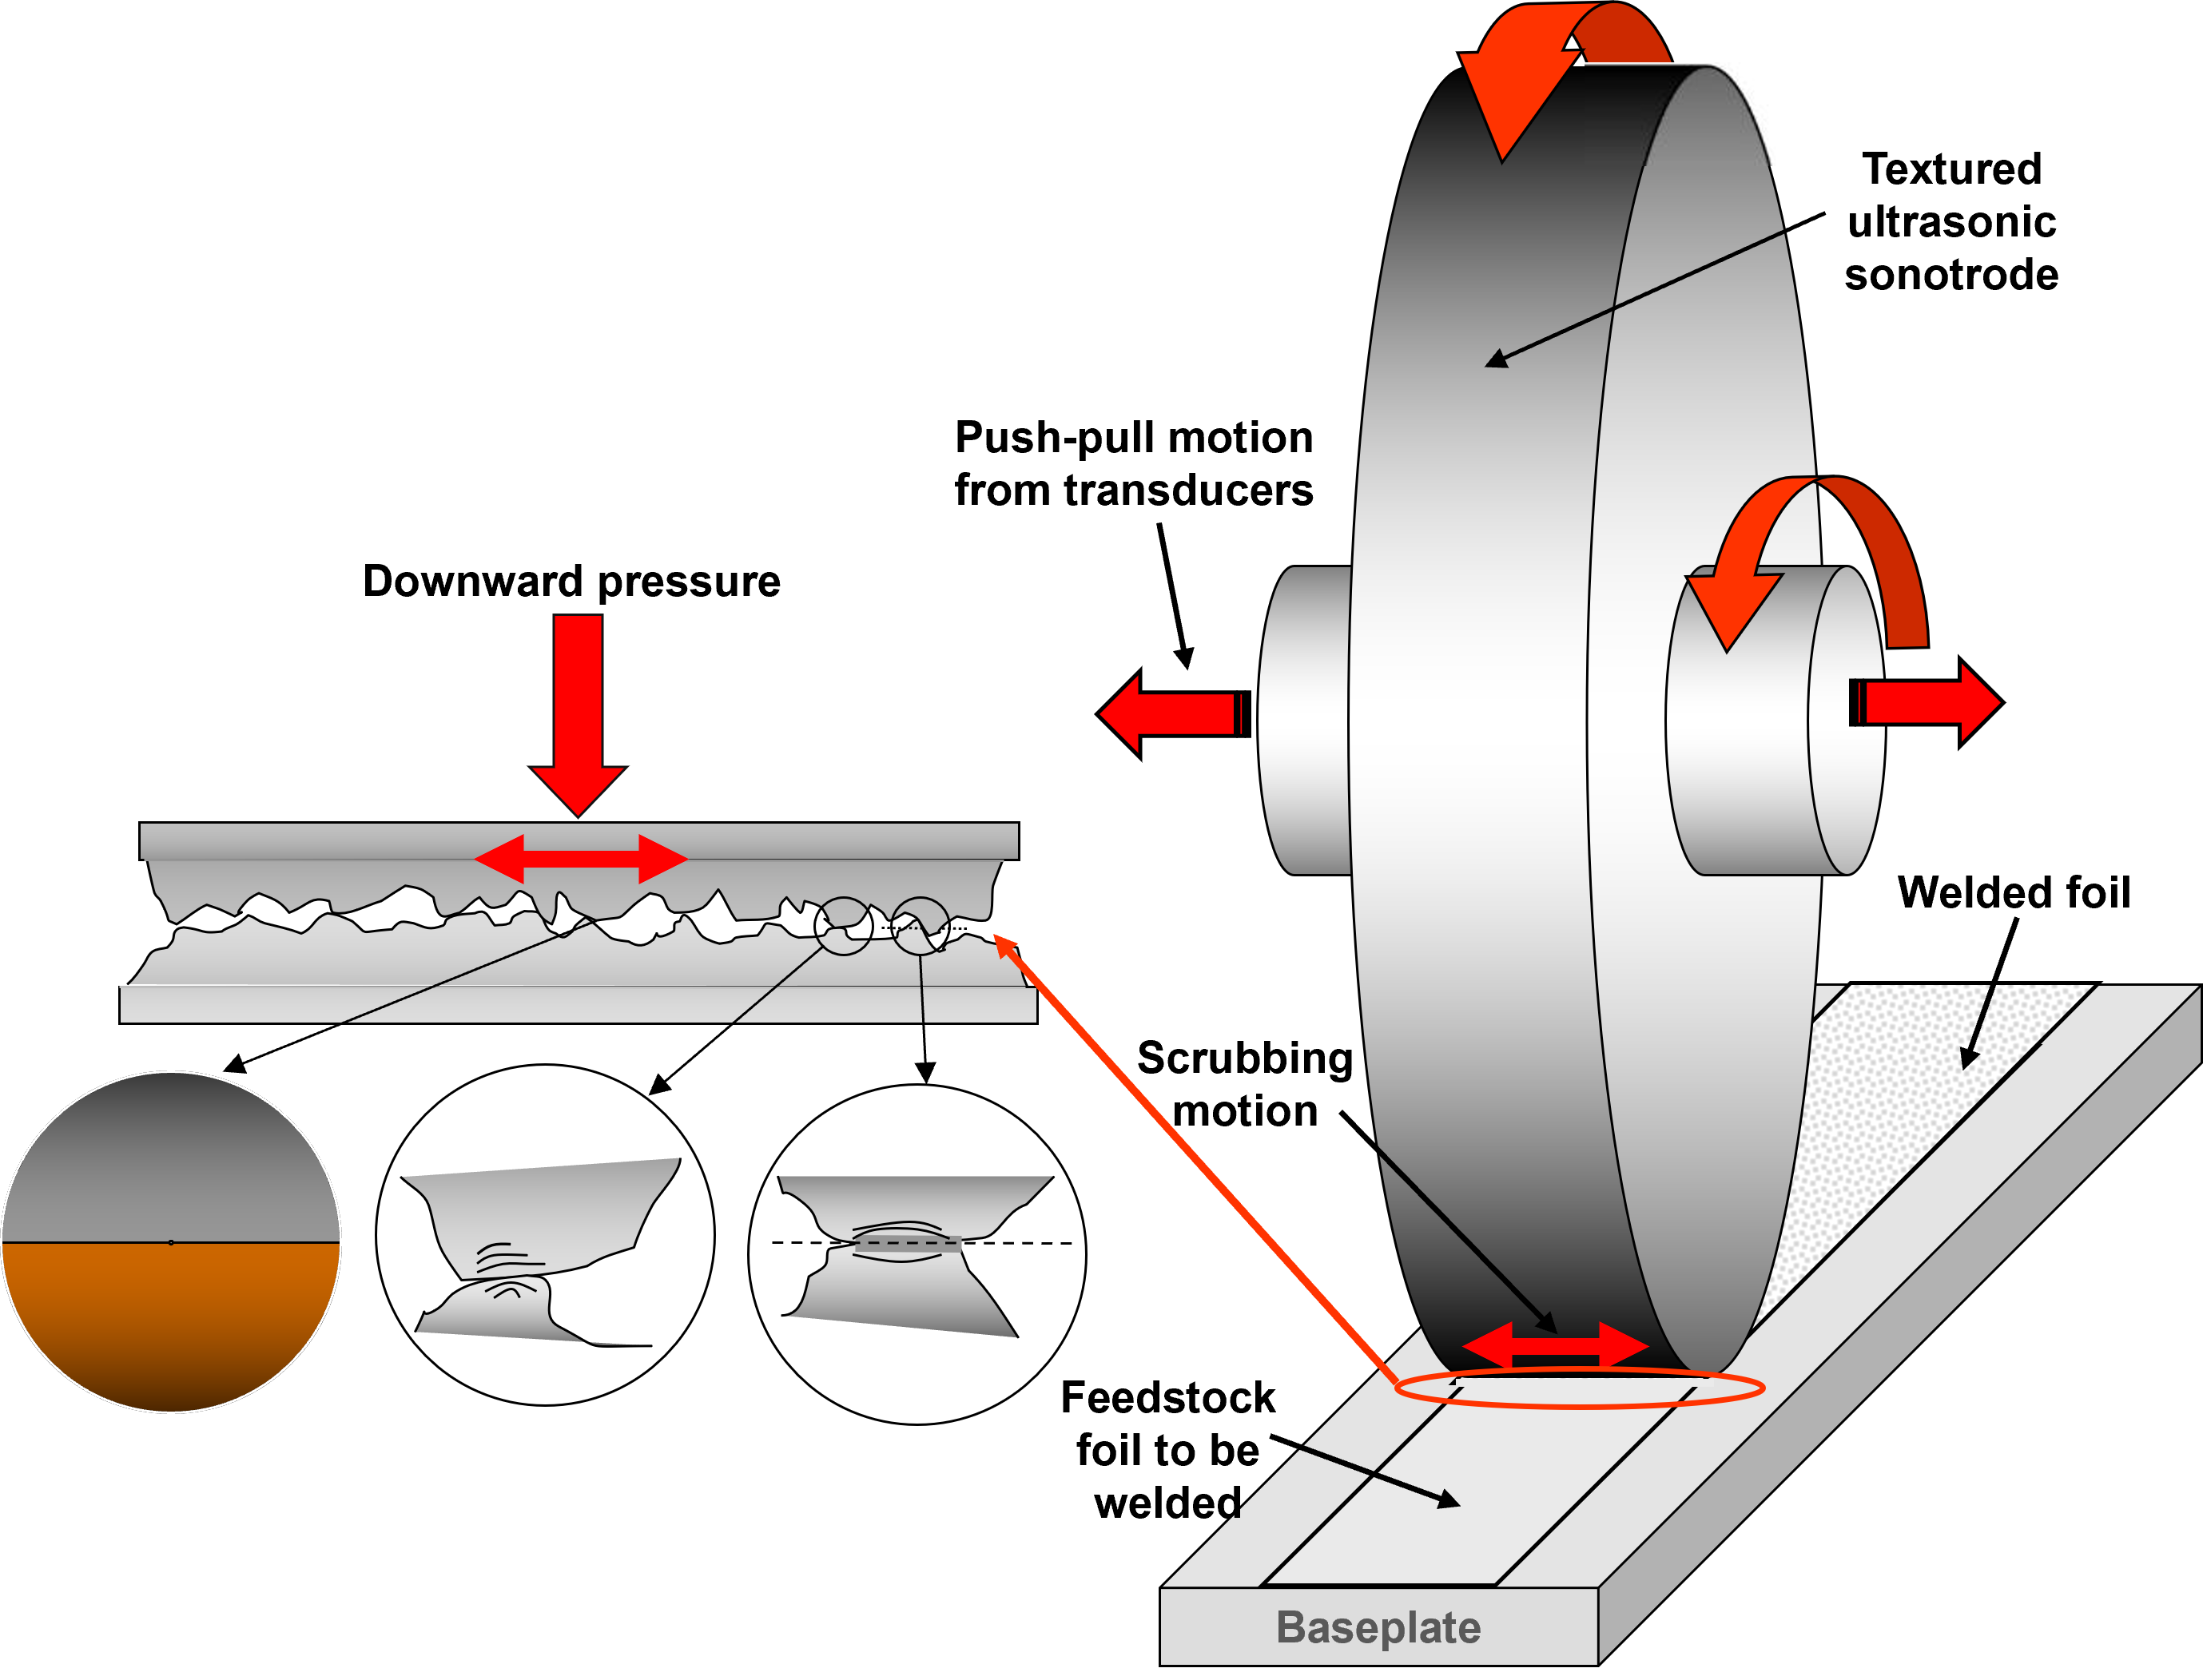
Ultrasonic additive manufacturing (UAM), also called ultrasonic consolidation, builds metal parts by joining foils in the solid state. Ultrasonic welding is combined with CNC milling in a hybrid sheet-lamination workflow. Avoiding bulk melting does not remove the need to qualify bond quality, material combinations and component properties.
Fabrisonic, a US company spun out of EWI, commercialises UAM equipment and manufacturing services. Its process combines foil bonding and machining.
According to Mark Norfolk, President & CEO at the time of the interview, the process always works as explained above. However, applications that can be achieved with this process can be of different sizes, depending on the size of the machine one uses. “It’s a matter of scale,” he says.
As you can understand from the definition, UAM can be combined with other processes.
“One problem in the AM industry is people feel like they have to 3D print the entire part and nothing could be further from the truth”, Norfolk said. “We have customers who provide us cast aluminum heat exchangers, and then we print additional features onto a casting. We have customers who send us preexisting weldments and we add features to those weldments.”
“Our process is not ideal for very organic, cellular-looking structures but powder bed fusion is fantastic at that. So, our partners can manufacture very complex organic shapes that we will embed in our product, through ultrasonic additive,” he adds.
These possible combinations with manufacturing techniques such as DED and LPBF facilitate the transition between materials or the creation of dissimilar metal joints that enhance said manufacturing technique.
As a matter of fact, dissimilar metals are the first area where the company sees a greater use of its technology. “We can combine titanium with tantalum, aluminum, or nickel, all in the same part without having to worry about metallurgical problems”, the CEO explains.
That statement concerns the combinations discussed by Fabrisonic. Different metals still require assessment of interface strength, service temperature, corrosion and compatibility; solid-state bonding is not a guarantee that all combinations will be suitable.
While Norfolk lays emphasis on the fact that UAM is just another manufacturing tool, we couldn’t help but think that the process is already serving emerging industries where AM applications are yet to be discovered. Those industries include energy and electrification – in addition to well-known sectors such as space and aerospace.
“The second area that highlights the benefits of our technology is embedded electronics”, Norfolk enthuses while remembering that one of their customers made 35 million parts last year in the electric vehicle space. “Our technology which uses foil as a feedstock lends itself to EV construction.” The build can be paused to insert a component before bonding resumes. Suitability depends on the embedded device, bonding conditions and required service life; a low-temperature process does not guarantee permanent operation or eliminate all deformation.
The 35-million-part example is an interview claim about an unnamed customer; this article does not independently verify its production route or volume.
Norfolk cited indicative feedstock prices of $100–200/kg for some powders and about $10/kg for some foils, with exceptions — “unless it’s something like gold”. These historical examples are not like-for-like quotations: alloy, thickness, specification, volume, machining and process costs affect the economic comparison.
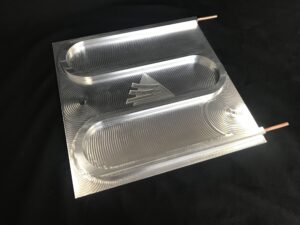
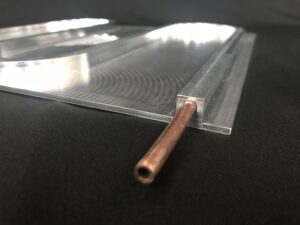
Legend: Embedded tubes. To avoid sealing issues, tubes can be embedded in place of machined channels. Credit: Fabrisonic.
What limits UAM adoption?
On paper, UAM has everything to be propelled in the AM industry: the possibility to achieve coveted applications such as heat exchangers, embedded sensors, dissimilar metals, selective reinforcement, to name a few; a wide range of opportunities in terms of materials and a low-temperature point which plays to the strengths of this process.
As no technology is perfect, Norfolk recognizes that they still need to work on their ability to deal with fine geometries: “We can’t weld on very delicate structures. The higher the strength of the metal, the harder it is to weld. We still need to do more research and development to get into production in this area.”
The geometry and material limitations described above are substantive engineering constraints, not merely minor adjustments. Their importance depends on the application.
At the time of the 2024 interview, Fabrisonic was associated with the nonprofit EWI. Norfolk related its marketing resources to that business setting. This account does not, by itself, establish why adoption differs from LPBF. The later change of ownership is noted above.
Fabrisonic reported installations in Europe. Equipment conformity must be checked for the particular machine and intended market; describing a manufacturing process itself as “CE-certified” is not an adequate conformity claim.
This dossier was first published in the July/August 2024 edition of 3D ADEPT Mag.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.