With a 30-year-plus pedigree in the industry, Additive Manufacturing continues to evolve. While it is clear to many that it is no longer just a solution for rapid prototyping, preconceptions regarding its usefulness as a production technology often need to be reassessed. As we evolve in a context where attention is shifting to higher-volume applications such as mass customization and the fabrication of standard parts, production losses due to process variability and inefficient machine use may be common concerns – leading AM users to ask themselves a million-dollar question: what are the key performance indicators for a “good” (metal) AM production?
Return on investment (ROI) expresses an economic result relative to the resources committed. It does not, by itself, measure the number of parts produced or machine utilisation. Assessing an additive manufacturing operation also requires measures of quality, lead time, equipment availability and cost per accepted part.
AM users therefore need another approach to assess the success metrics of AM. This dossier is at the intersection of general business considerations and manufacturing needs of industries.
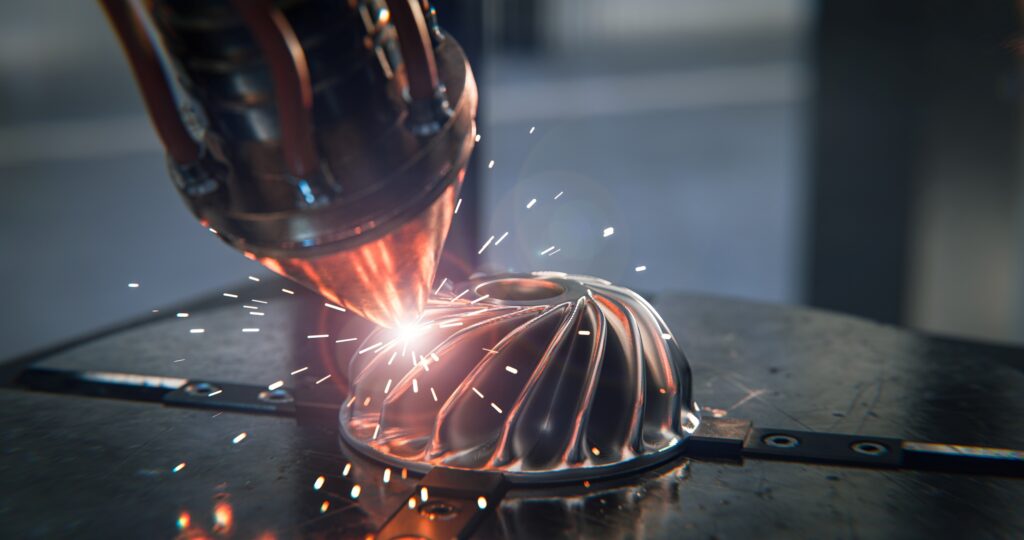
This dossier examines three approaches to metal additive manufacturing: directed energy deposition (DED), cold spray and material extrusion. Contributions from Nikon AM Synergy, Titomic and AIM3D explore process selection and machine performance for different applications and production volumes.
Reading context: this dossier was published in January 2025. Contributors’ roles, machine configurations and development plans refer to the time of their contributions. The stated values are not the results of a comparison under a shared test protocol.
The constant comparison with traditional manufacturing: is it still worth it?
In general, and for a long time, assessing the metrics of success of AM has been done in comparison with traditional manufacturing. This somehow makes sense when one knows the key advantages (design freedom and flexible and rapid fabrication) AM brings compared to traditional manufacturing processes (acknowledged for their ability to allow mass production or large economy of scales).
The truth is, talking about production and AM does not necessarily refer to mass production. “When talking about production and additive manufacturing, especially in metal AM, we do not necessarily always think of mass production. Production can involve a wide range of conditions from initial proof of concept (POC) and prototyping to custom or small batch production, low-rate initial production (LRIP), full rate production, and mass production,” Dr Behrang Poorganji, CTO of Nikon AM Synergy Inc explains.
Making a clear comparison with casting and forging, Herbert Koeck, then Managing Director at Titomic explains:
“Unlike casting and/or forging foundries that can require larger economy of scales to justify tooling investment and parts production, cold spray additive manufacturing (CSAM) in certain geometries can offer an alternative source for near net parts. CSAM can be setup for mass production, although the investment in CS has the added advantage of versatility, where one day the machine is producing as a titanium caster, and the next day running as copper foundry.”
However, this comparison may not always be applicable when one realizes that AM often comes to enhance existing processes, making them more efficient and effective. Furthermore, AM is sometimes a victim of its own success: the more the technology advances, the more complexity it brings to other areas of the manufacturing chain, even when the process reduces industrial costs, shortens lead times, or enhances the sustainability of manufacturing.
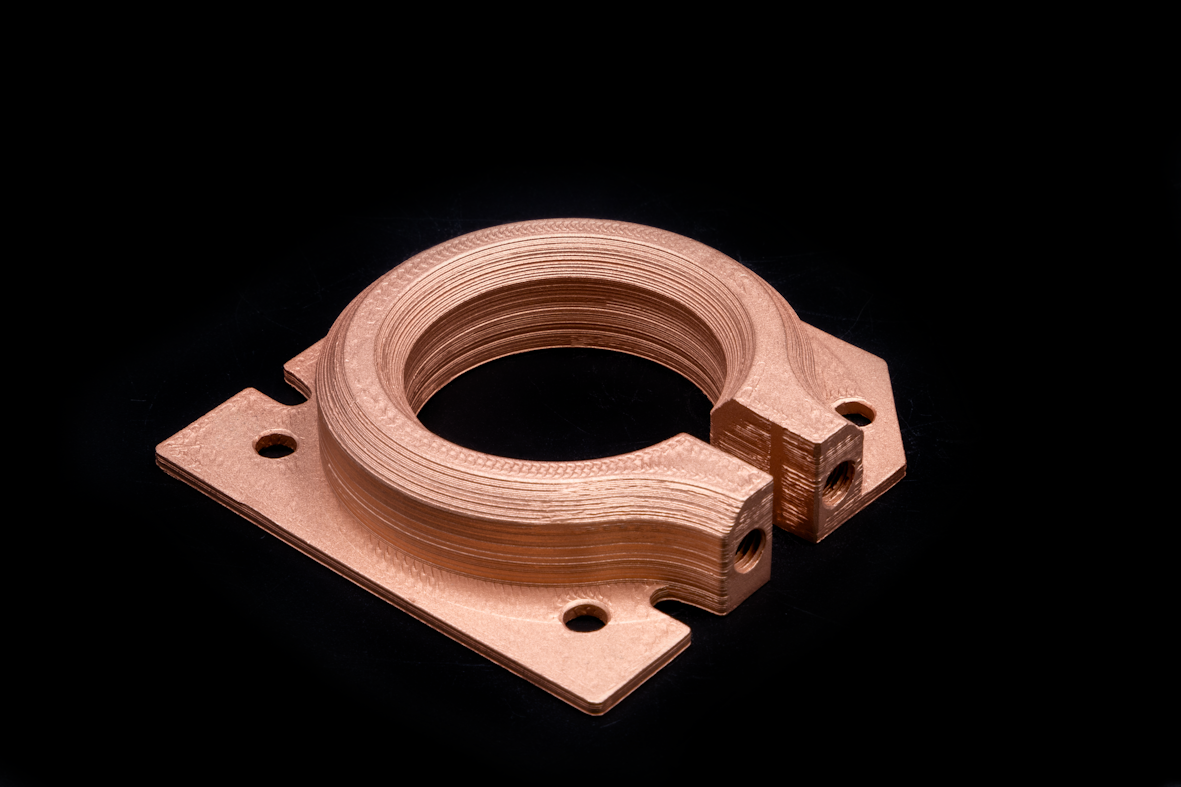
These considerations make the definition of AM evolve among its users, and often lead to a comparison between AM technologies themselves.
Metal additive manufacturing processes use different energy sources, feedstocks and finishing steps. Beyond laser powder bed fusion, the choice of DED, cold spray or material extrusion depends on part size, material, quality requirements and production volumes.
For a first adoption, ask suppliers about the intended applications, process limitations and test conditions, rather than comparing advertised build rates alone.
If we were to evaluate the appropriate use and scope of traditional manufacturing processes, we would have considered features such as cost and price, as well as other considerations related to mass production and the global supply chain. These considerations may include labor, energy, material feedstocks, production support, research, design and engineering amortization to name a few.
Manufacturing cost and selling price are different measures. A cost assessment can include feedstock, labour, energy, depreciation, inspection, scrap and finishing operations.
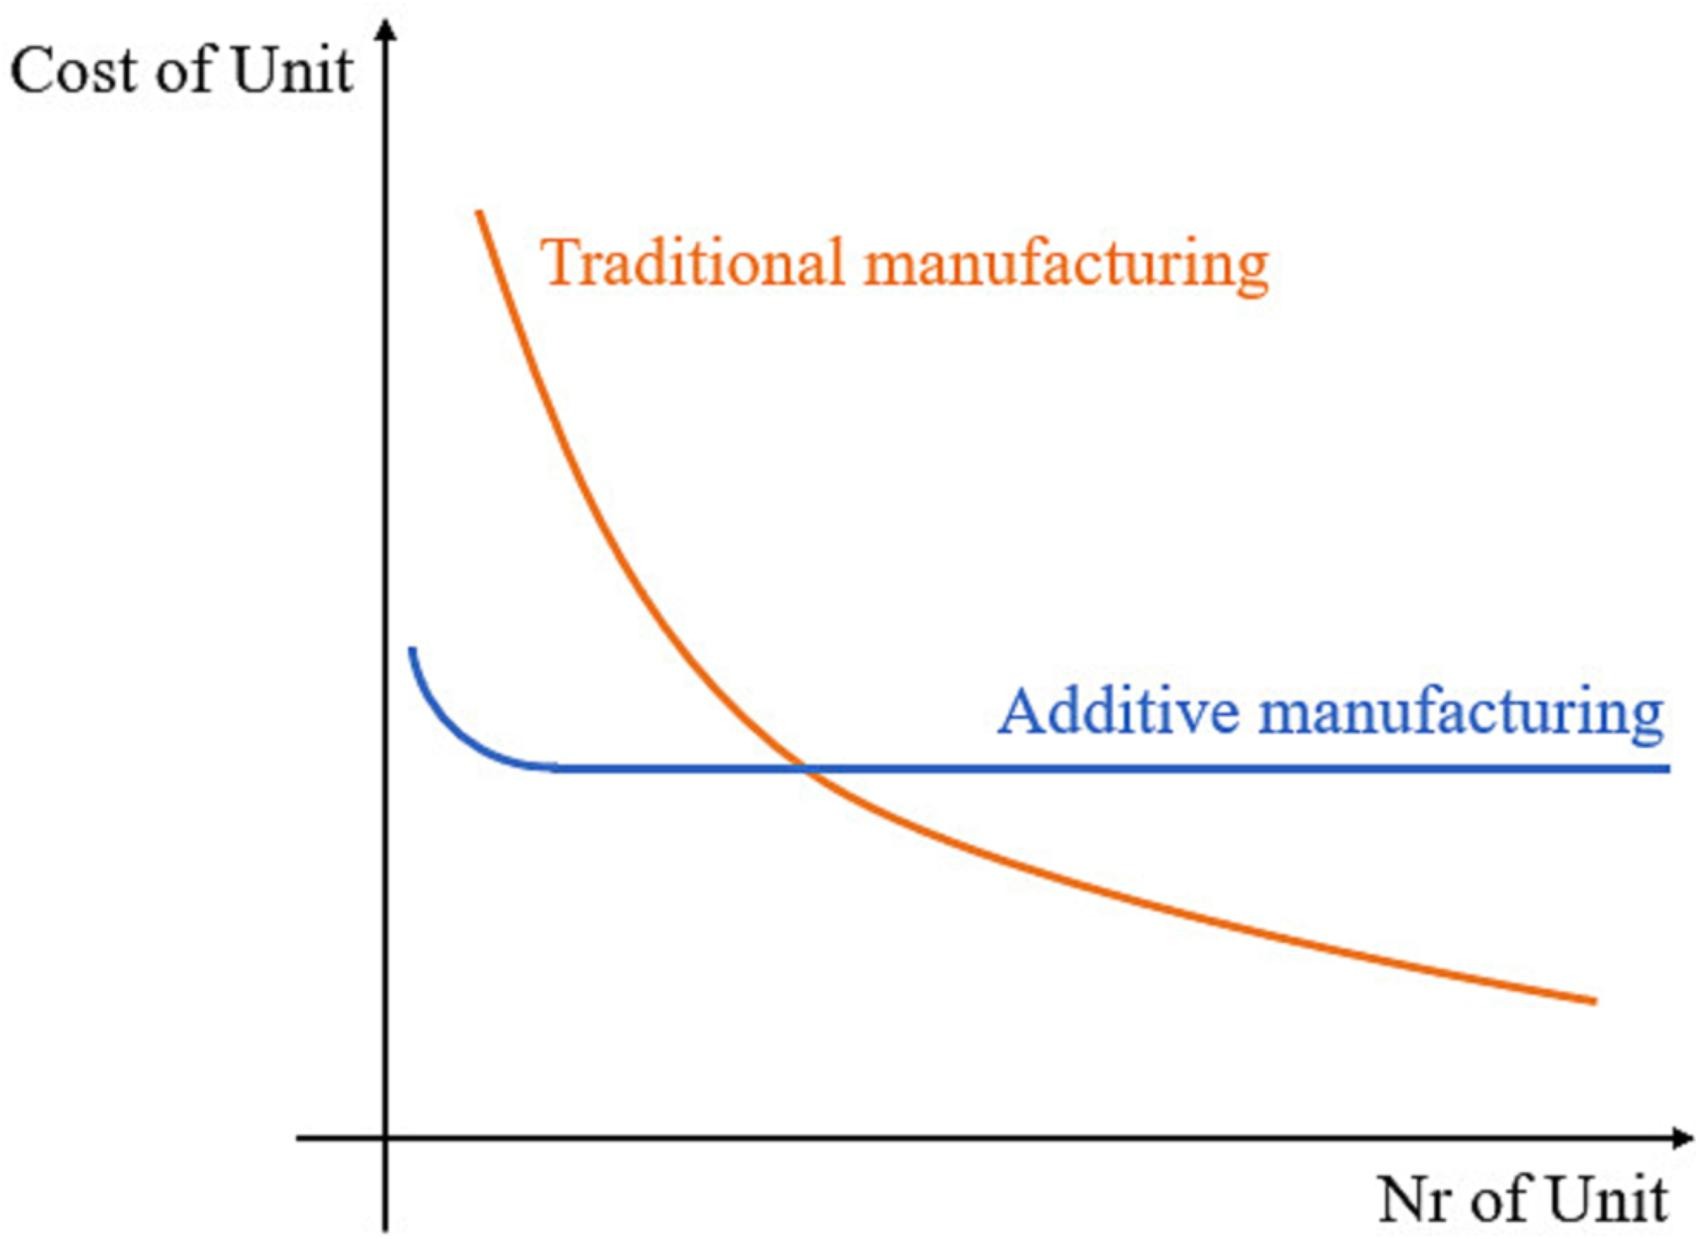
The cost graph illustrates a trend discussed by Calignano and Mercurio (2023). It provides neither current prices nor a universal break-even point.
In the case of metal AM, “the first question we should ask ourselves is why we would choose AM for mass production and consider using a global supply chain for that purpose. Are we considering cost, functionality, performance, lead time, environmental impacts and sustainability, security, etc. as our decision factors in choosing AM?
Cost efficiency, materials availability and materials properties, design complexity (where AM provides tremendous advantages), precision and quality requirements, and scalability all factor into the suitability of mass production. High-demand products experiencing a strained supply chain using conventional manufacturing processing technologies could be strong candidates for mass production using metal AM and implementing a global supply chain. IP considerations are also important when thinking of leveraging a global supply chain in metal AM,” Poorganji outlines.
For Clemens Lieberwirth, CTO at AIM3D GmbH, “there is no good business case for mass production with AM – but talking about small series production, there are three indicators in my opinion:
- Series Size – depending on part size/complexity up to 10.000 pcs/year
- AM-optimized product design (depends on AM process) – part size, wall thickness, overhangs, smallest details, and internal channels should be tuned to the specific AM process to get the best result concerning quality and cost
- Independency in terms of material choice and production location. Systems that have open material policies allow the best cost & quality performance and make the production line crisis-safe”
These views reflect different applications and business models. Lieberwirth’s figure of up to 10,000 parts a year is his reference for certain small-series cases, not a general limit for AM. Open material policies do not remove the need for material qualification or supply-risk management.
Comparison with a conventional process remains useful when choosing a manufacturing route. Customisation, part consolidation and on-demand production can provide additional value, which needs to be assessed for the industrial case.
The question of standardization
Standardisation matters in both additive and conventional manufacturing. Customising a part does not remove the need for traceability, repeatability and process qualification.
“For high-rate production in aerospace and defense, ISO/ASTM recognition assists in achieving consistent results as a product transition from development to full-scale production that require collaboration of larger teams,” Titomic’s expert outlines.
ISO/ASTM 52900:2021, developed jointly by ISO and ASTM International, distinguishes seven categories: material extrusion, material jetting, powder bed fusion, sheet lamination, binder jetting, directed energy deposition and vat photopolymerisation. This classification establishes vocabulary; it does not certify a machine or part.
The question is: does it matter? Experts have different opinions on the topic:
“Recognition under a globally used standard such as ISO/ASTM joint standards for AM is highly important, but whether it is absolutely necessary or not depends upon the industry and products. There are other standards and specifications such as SAE AMS, AWS, MIL that are necessary in certain contexts for specific products/industries. Standards are critical in assuring quality when it comes to repeatability and reliability of the process. They also establish a common language in building trust and credibility, and understanding risks, as well as in satisfying specific regulatory compliances defined by agencies such as the FAA, FDA, NASA, etc. by defining requirements and establishing certification processes,” Nikon AM Synergy Inc’s expert said.
“I [don’t] think it absolutely matters now. The standards are in part very general and try to merge different technologies, that have different technological principles of action. There are still many customers that are confused by the amount of different AM technologies and that cannot differentiate what is suited for one process or another. Standards that are mixing these processes won´t help with that. But of course, more enlightenment and suiting standards could also help with that in the future,” AIM3D’s CTO argues.
So, what performance indicators should one consider for an AM production and for a 3D printer?
Expected benefits such as customisation, complexity and on-demand manufacturing need measurable indicators. These can include total cost per accepted part, first-pass yield, scrap and rework, end-to-end delivery time and equipment availability. Each indicator needs a defined measurement period and scope, including post-processing and inspection.
Some technical considerations may emphasize this:
“In metal AM production, there are several key indicators of production success. Part quality, repeatability and reliability of the build process, cost effectiveness and production efficiency, lead time/ on time delivery, as well as sustainability with regards to reducing waste and being able to reuse and recycle materials are among these indicators.
When it comes to AM machine performance assessment, equipment uptime, reliability, ease of use and available services and maintenance are essential factors. Other critical considerations include machine throughput, build volume, printing resolution, process automation (especially in serial production, or when skilled operators are not readily available), and in-process monitoring integration for machine health and quality assurance purposes,” Dr Behrang Poorganji outlines.
Taking example on their technology, Titomic’s Herbert Koeck points out:
“Process consistency is of high importance and is measured in several ways by Titomic. A primary metric for Titomic’s systems is powder velocity and material deposition. With high deposition rates, Titomic produces large, strong titanium parts at 5kg per hour, depending on the application.”
Nikon announced the Lasermeister LM300A DED system and SB100 scanner in April 2024 for metal-component repair. Combining measurement, geometry compensation and toolpath generation is intended to automate repair preparation. The outcome still needs to be validated for the component, material and qualified process.
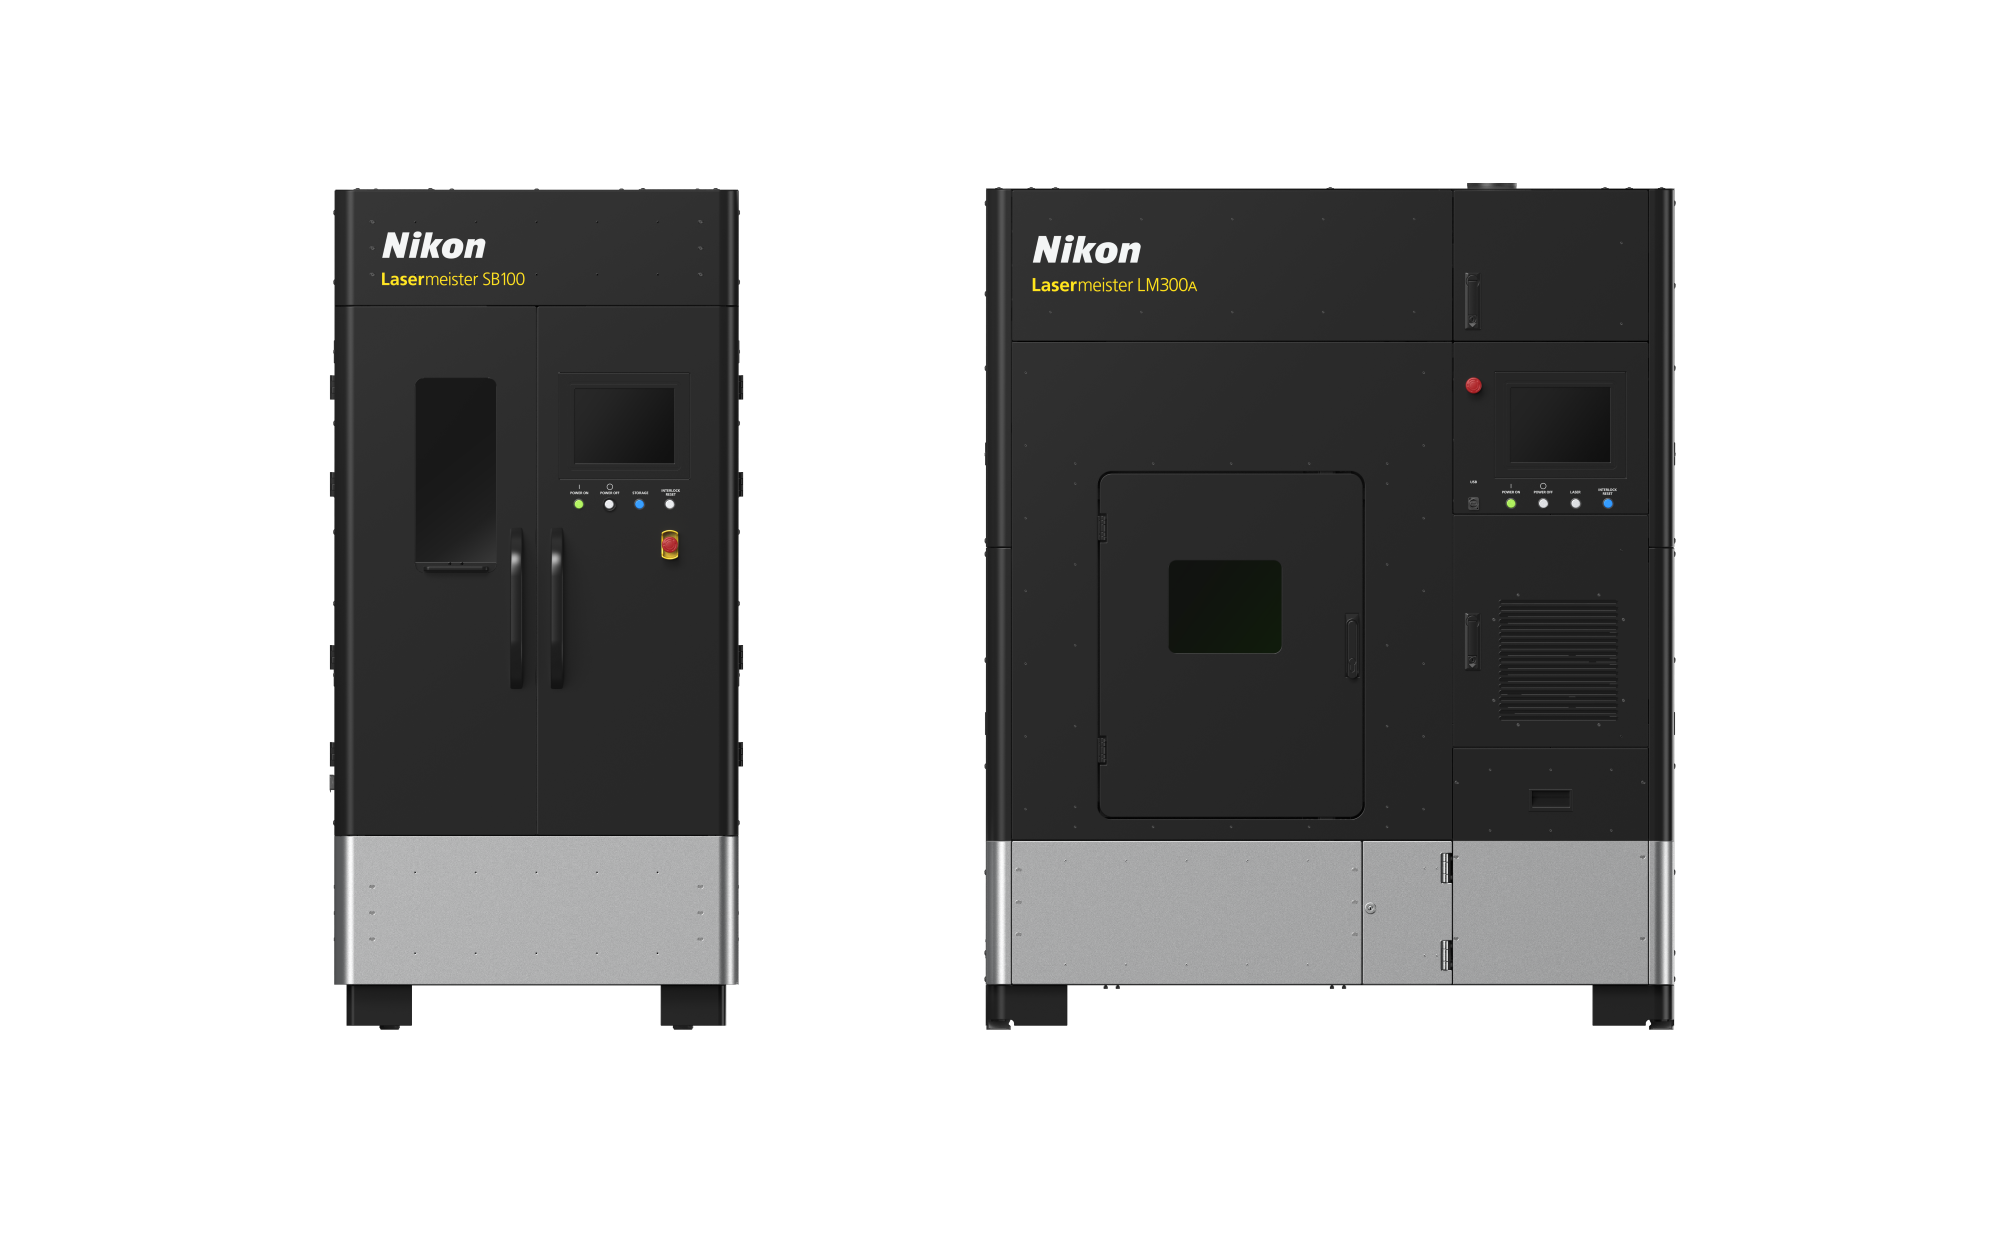
This is how Poorganji describes their 3D printer’s performance in light of the value benchmarks below.
The tables below reproduce the manufacturers’ responses at the time of their contributions. Targets stated for a “next generation” are not results verified here. Mass and volumetric build rates cannot be compared directly without the material and measurement conditions.
| Value benchmarks | Answers |
|---|---|
| Does it help to achieve wall thickness? | Nikon DED Lasermeister repair systems are very capable of delivering thin wall thicknesses and high-resolution features, down to 500 microns (0.5mm). Our next-generation high-throughput machines have even finer capabilities down to 200 microns resolution (0.2mm) |
| What’s the minimum and maximum part size feasible? | Our current generation system can produce up to 400mm tall parts with approximate cross section of 300 X 200mm. Our next-generation DED system will have capabilities for up to 650mm parts. |
| Build rate | Our current generation DED repair system can deliver 2-5 cc/hr. For our next-gen DED system, we are targeting +100cc/hr. |
| In-process quality assurance | We have in-process monitoring in our DED system for both the melt pool and powder feed rate. |
| Inspection and quality controls | Our DED repair solution is integrated with pre and post-3D optical scanning for dimensional accuracy. We at Nikon are also benefiting from our non-destructive Nikon X-CT inspection. |
| Finishing and post-processing? | Our DED repair system’s high resolution and fine material deposition enables very smooth surfaces as well as minimized heat affected zone (HAZ) and thermal distortion. Using our Nikon DED repair solution can thereby reduce time and cost at the post processing step. |
| Materials? | We have parameters for a variety of materials and our system is compatible with both reactive and non-reactive powders. As a few examples – we can process Steels, Ti alloys, Ni alloys, Cu alloys, and Nb alloys. |
| Quality sensitivity (Does it require specific tools to control defects for instance?) | Standard microstructural characterization, mechanical and physical material property, and standard non-destructive testing (NDT) are the conventional tools we use. |
Titomic offers cold spray systems for manufacturing, coating and repairing metal components, with configurations for research and industrial applications, including defence and aerospace.
Titomic presents the TKF-1000 as a modular cold spray system for prototyping, research and small-run production. Performance depends on the material, geometry and spray parameters.
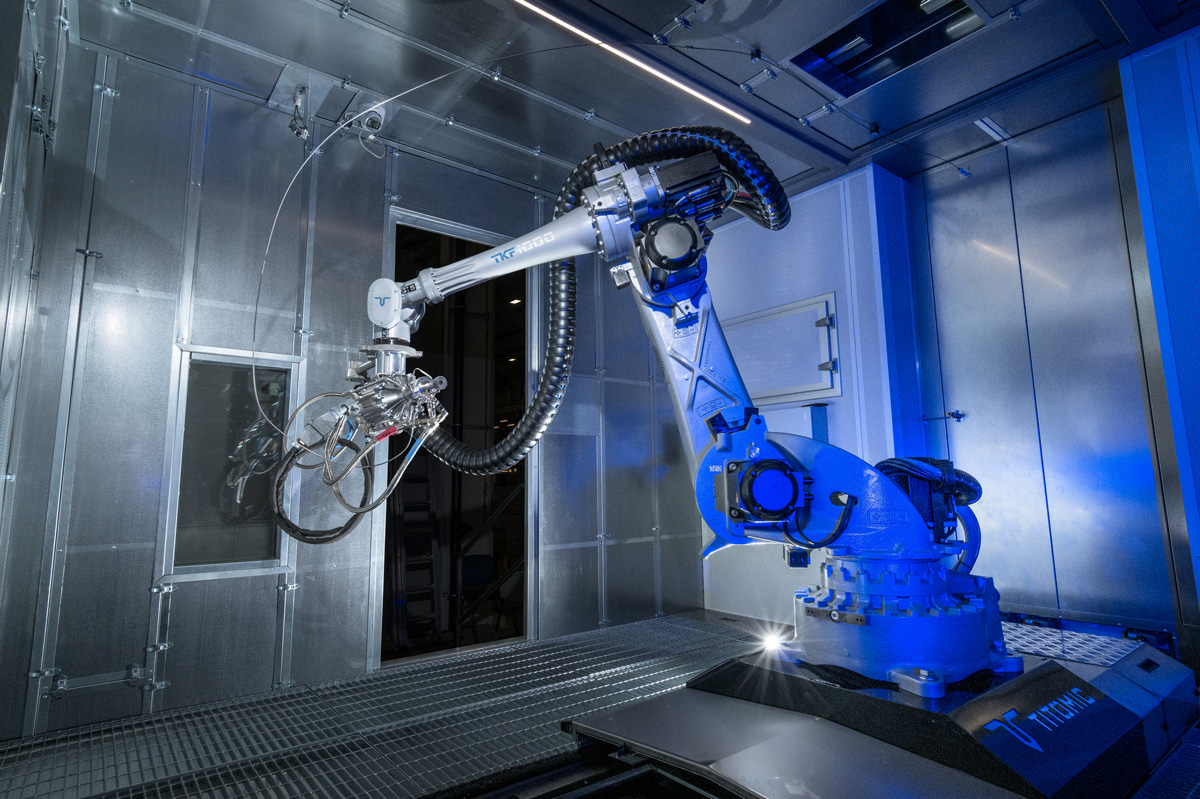
This is how Herbert Koeck describes their 3D printer’s performance in light of the value benchmarks below.
| Value benchmarks | Answers |
|---|---|
|
Does it help to achieve wall thickness? |
Yes. Wall thickness is dependent on the material, the cold spray parameters used, and the geometry being built (i.e., flat vs rotational parts). For example, Titomic has achieved wall thickness in CP-Ti of 75 mm. |
|
What’s the minimum and maximum part size feasible? |
The maximum limitation is either residual stress limits or post processing limitation such as the heat treatment size available.
The minimum does depend on the geometry and cold spray system used. With a [spray plume] diameter ranging from 3 to 12 mm, parts that are derived from near net casting or forgings can be well suited to cold spray. |
| Build rate | A reasonable build rate is 1 Liter per hour. For higher stressed materials this is dialled back to 0.5 and 0.25 Liters per hour.
Titomic can produce titanium and other parts at rates of 5kg/hour, depending on product application requirements, including optimisation of material properties. |
|
In-process quality assurance |
Titomic carefully records all cold spray parameters, such as [powder] feed rate, gas temperature, and pressure. |
|
Inspection and quality controls |
Non-destructive testing techniques can be used, such as ultrasound, to inspect parts for defects.
Titomic conducts further inspection with its on-site laboratory and machine finishing facility. |
|
Finishing and post-processing? |
Titomic parts can be used as sprayed in some applications. Otherwise, the as-sprayed part is directly machinable. As parts made with cold spray are near-net-shape, they may require machining to remove 5-10% of material to bring the part to final tolerance.
Once complete, the part may require heat treatment, depending on the final desired outcome or part application. Titomic has found very strong results in the use of hot isostatic pressing, with parts showing significant strength-to-weight values. |
| Materials? | Most metals that can be powdered can be cold sprayed, however, if a powder has a high strength-to-density ratio, it can be difficult to build with as it requires a high particle velocity and therefore can be highly stressed during deposition (for example carbon steels).
Titomic’s cold spray process excels at manufacturing and coating with copper and its alloys, titanium and its alloys, tantalum, stainless steels, and Inconel In718 and 625. |
|
Quality sensitivity (Does it require specific tools to control defects for instance?) |
Not specified in the contribution. |
Editorial note: the bracketed terms clarify typographical errors in the original contribution (“plum” and “power”). Numerical values have been retained.
AIM3D GmbH has developed a multi-material 3D printer that prints products made of metals, ceramics, plastics and reinforced plastics based on standard injection molding granules without costly machine conversions.
For metal-filled feedstocks, AIM3D explains that debinding and sintering follow printing. Their duration, capacity and part shrinkage must be included when assessing final production throughput.
This is how Clemens Lieberwirth describes their 3D pellet printing technology’s performance in light of the value benchmarks below.
| Value benchmarks | Answers |
|---|---|
|
Does it help to achieve wall thickness? |
Yes, it helps to achieve wall thicknesses. |
|
What’s the minimum and maximum part size feasible? |
Minimum part size ~ 0,125 cm³ (Size of a tooth)
Maximum part size ~ 500 cm³ (Size of a palm) |
| Build rate | ~ 60 -250 cm³/h |
| In-process quality assurance | Process parameter control (temperature, movement, extrusion, nozzle clogging) |
| Inspection and quality controls | Visual inspection, weight, dimensional measurements |
| Finishing and post-processing? | Deburring, Debinding, Sintering, cutting threads, sanding polishing if needed |
| Materials? | Stainless steels, low alloy steels, nonferrous metals like titanium, copper, brass, ferromagnetic alloys, hard metals, ceramics … |
|
Quality sensitivity (Does it require specific tools to control defects for instance?) |
Depends on use case |
In a nutshell…
The suitability of either additive or conventional production depends on part requirements and customer needs. Deposition rate is useful, but it is not the number of accepted parts delivered per hour. A comparison should include preparation, downtime, finishing, inspection and scrap, using comparable materials and measurement boundaries.
THE 3D ADEPT WEEKLY NEWSLETTER
The industry moves fast. Stay ahead.
Every week, the latest additive manufacturing news, in-depth features and real-world applications, straight to your inbox. Plus, be the first to know when a new issue of 3D ADEPT Mag is out.
Free · One email a week · Unsubscribe anytime
Clicking loads our email provider’s sign-up form, including its analytics and Google’s anti-bot protection. You’re only subscribed if you complete the sign-up. Read our privacy policy.